Aquashield Corporate Shield Logo

AQUASHIELD CORPORATE

Commercial Flat Roofing & Industrial Facility Engineering

A comprehensive technical compendium on commercial 60-mil TPO single-ply systems, high-solids silicone restorative coatings, and building envelope preservation. Volume 19 of 23.

Previous (Vol. 18) Volume 19 of 23 (40 Dossiers / Page) Next (Vol. 20)
Commercial Engineering Dossier #720

Multi-Tier Conductor Head Overflow Spillways & Freeze-Thaw Downspout Burst Defense on Commercial Chemical Processing Facilitys
Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Multi-Tier Conductor Head Overflow Spillways & Freeze-Thaw Downspout Burst Defense on Commercial Chemical Processing Facilitys

Hydraulic Analysis of Conductor Head Overflow and Weir Calculations

In the high-stakes environment of a commercial chemical processing facility, the building envelope is the first line of defense against catastrophic structural failure. When auditing these facilities, the primary concern is often the management of extreme precipitation events. A failure in the primary drainage system—typically caused by debris blockage or sudden hydraulic surge—can lead to rapid ponding. On a flat roof, this creates immense hydrostatic pressure that can compromise the membrane and flashing, leading to subsurface saturation and potential collapse of the roof deck.

To mitigate this, we implement precise overflow relief weir calculations. A weir is essentially a calibrated notch or opening that allows water to exit the roof system once the water level reaches a critical threshold, but before it reaches the roof's parapet or penetrates the building's interior. For chemical facilities, we calculate the required overflow capacity based on the roof's square footage and the local 100-year storm event data, ensuring the secondary drainage system can handle at least 125% of the primary system's peak flow.

  • Calculation of the "Crest Height" to ensure water does not bypass the membrane flashing.
  • Determination of the "Weir Coefficient" to predict the volume of water discharged per second.
  • Analysis of the "Head Pressure" to prevent backflow into the internal conductor heads.
  • Assessment of the "Catchment Area" to ensure no localized ponding occurs around chemical vents.

Engineering the Multi-Tier Conductor Head Spillway System

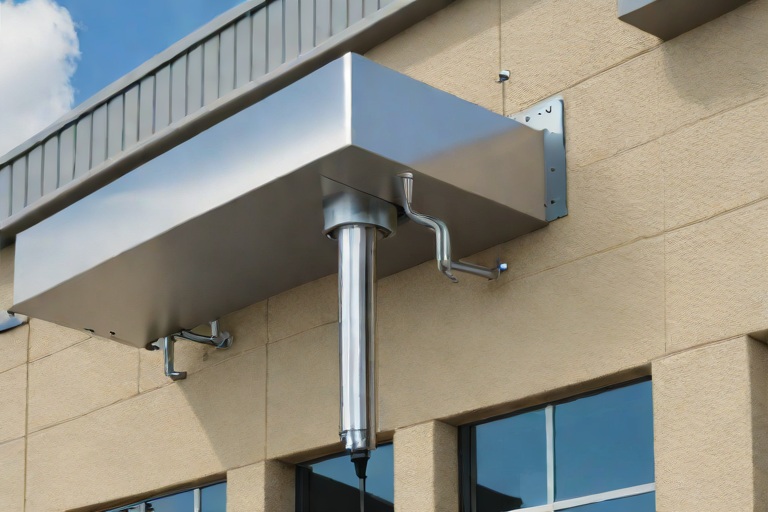
The conductor head serves as the transition point between the roof's internal drainage and the vertical downspout. In a standard installation, a single-tier head is sufficient; however, in a chemical processing plant, the risk of corrosive condensate and heavy debris requires a multi-tier spillway approach. This engineering strategy involves creating a series of graduated overflow levels within the conductor head itself. If the primary drain is obstructed, the first tier of the spillway activates, directing water safely away from the building's facade and preventing the "waterfall effect" that erodes the foundation.

Material science is paramount here. Given the atmospheric corrosives present in chemical facilities, we eschew standard galvanized steel in favor of 316-grade stainless steel or high-density reinforced polymers. These materials resist the pitting and oxidation common in environments where sulfur or ammonia may be present in the air. The spillways are precision-cut and welded to ensure a seamless transition, eliminating any "lip" that could catch debris and cause a secondary blockage.

  • Implementation of tiered overflow notches to manage varying intensities of rainfall.
  • Utilization of 316-grade stainless steel to prevent chemical corrosion and oxidation.
  • Integration of debris screens that are easily accessible for quarterly maintenance audits.
  • Application of seamless welding techniques to maintain the integrity of the building envelope.

Structural Integrity and Heavy-Duty Downspout Bracketry

The physical connection between the conductor head and the building's exterior wall is a frequent point of failure. In industrial settings, downspouts are subject to extreme wind loads, vibration from heavy machinery, and the sheer weight of water during a surge. Standard residential or light commercial brackets are insufficient; they often bend or pull away from the masonry, creating gaps that allow water to seep behind the cladding and into the wall cavity, leading to hidden mold and structural rot.

Our engineering standard requires the installation of heavy-duty, oversized steel brackets with reinforced mounting plates. These brackets are anchored using chemical anchors or stainless steel expansion bolts, depending on the substrate. By distributing the torsional stress across a larger surface area of the building's envelope, we ensure that the downspout remains plumb and secure even under maximum hydraulic load. Furthermore, we implement galvanic isolation between the bracket and the building skin to prevent bimetallic corrosion, which is accelerated in chemical-rich environments.

  • Use of oversized mounting plates to reduce localized stress on the building facade.
  • Installation of stainless steel chemical anchors for maximum pull-out resistance.
  • Application of neoprene isolation gaskets to prevent galvanic corrosion between dissimilar metals.
  • Alignment checks using laser levels to ensure optimal gravitational flow and minimize turbulence.

Mitigating Freeze-Thaw Cycle Volatility and Burst Defense

One of the most destructive forces acting upon a commercial drainage system is the freeze-thaw cycle. When water traps within a downspout and freezes, it expands by approximately 9%, creating immense internal pressure. In a chemical facility, where temperature fluctuations can be extreme due to internal processing heat and external winter conditions, this often results in "bursting." The metal expands and splits, typically at the seams or at the points of highest restriction, leading to uncontrolled water discharge during the spring thaw.

To defend against this, we employ a strategy of thermal expansion management and strategic venting. By installing "expansion joints" within the vertical runs of the downspouts, the metal is allowed to move slightly as it freezes and thaws, absorbing the pressure without rupturing the pipe. Additionally, we ensure that all horizontal runs are sloped at a minimum of 1/4 inch per foot to prevent the formation of ice plugs. In extreme climates, we recommend the installation of heat-trace cabling and insulated cladding, ensuring that the water remains in a liquid state until it reaches the subterranean storm sewer.

  • Installation of telescoping expansion joints to accommodate thermal movement.
  • Strict adherence to minimum slope requirements to eliminate standing water in horizontal runs.
  • Integration of self-regulating heat-trace cables in high-risk "cold spots" of the envelope.
  • Application of closed-cell spray foam insulation around conductor heads to prevent flash-freezing.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #721

Structural Steel Deck Rust Remediation & Zinc-Rich Primer Passivation on Commercial Municipal City Hall & Administrative Complexs

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Structural Steel Deck Rust Remediation & Zinc-Rich Primer Passivation on Commercial Municipal City Hall & Administrative Complexs

Forensic Audit and Oxidation Analysis of Municipal Roof Decks

In the execution of a comprehensive building envelope engineering audit for a Municipal City Hall and Administrative Complex, the primary objective is the identification of systemic failure points within the structural steel decking. In large-scale municipal structures, the roof deck often suffers from chronic moisture infiltration resulting from failed flashing or degraded membrane seals. This leads to interstitial condensation, where moisture becomes trapped between the insulation and the steel flutes, creating a micro-environment conducive to rapid oxidation. Our forensic analysis focuses on the degree of section loss and the categorization of rust, distinguishing between superficial surface rust and deep-pitting corrosion that compromises the structural load-bearing capacity of the deck.

The audit process utilizes a combination of ultrasonic thickness gauging and visual inspection to map the extent of the oxidation. In municipal complexes, we frequently encounter "crevice corrosion" at the laps and seams of the steel deck, where water pools and accelerates the electrochemical reaction of the steel. When the protective mill scale or original galvanization fails, the iron in the steel reacts with oxygen and water to form hydrated iron oxide. If left unaddressed, this oxidation leads to a significant reduction in the effective gauge of the steel flutes, potentially leading to structural deflection or failure under snow and wind loads.

  • Identification of localized pitting versus generalized surface oxidation across the deck.
  • Assessment of moisture vapor transmission rates through the existing insulation layers.
  • Evaluation of the structural integrity of the deck laps and side-lap fasteners.
  • Mapping of high-risk zones where HVAC curb penetrations have allowed water ingress.
  • Verification of the steel gauge against original architectural blueprints to determine section loss.

Mechanical Remediation and Substrate Surface Preparation

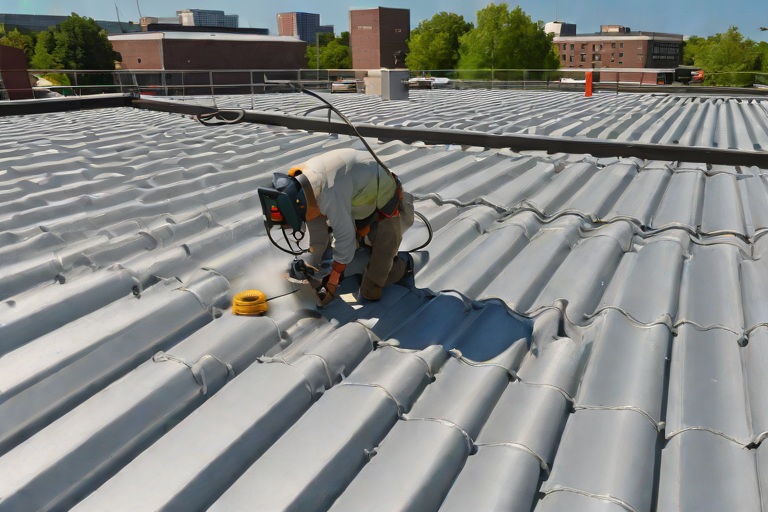
Once the audit confirms the presence of structural oxidation, the remediation phase begins with rigorous mechanical cleaning. To ensure the long-term efficacy of any protective coating, the substrate must be returned to a state of near-white metal or a specified commercial blast level. We employ industrial-grade wire-brushing and power-tooling in accordance with SSPC-SP2 and SSPC-SP3 standards. This process is not merely about removing visible rust; it is about removing the loose oxide scale and contaminants that would otherwise prevent a chemical bond between the steel and the primer. Failure to properly prepare the surface results in "flash rust" or coating delamination, which can lead to premature failure of the remediation effort.

The mechanical process requires a meticulous approach to the flutes of the steel deck. The valleys of the flutes are the most critical areas, as they act as natural channels for water. Our teams utilize specialized pneumatic wire wheels to reach the deepest points of the flute, ensuring that all friable rust is eliminated. This aggressive cleaning creates a mechanical profile—a microscopic roughness on the steel surface—that allows the zinc-rich primer to anchor itself firmly. This stage is the most labor-intensive part of the building envelope restoration, but it is the most critical for ensuring the structural longevity of the municipal complex.

  • Execution of power-tool cleaning to remove all loose scale and foreign matter.
  • Utilization of vacuum-assisted extraction to prevent metallic dust from contaminating the interior space.
  • Detailed scrubbing of lap joints to eliminate hidden pockets of oxidation.
  • Verification of surface cleanliness using the "tape test" to ensure no residual dust remains.
  • Application of a solvent wipe to remove oils or grease that could inhibit primer adhesion.

Chemical Passivation and Zinc-Rich Primer Application

Following mechanical preparation, the steel is in a highly reactive state and must be immediately passivated to prevent rapid re-oxidation. We specify the application of a high-solids, zinc-rich rust-inhibiting primer. The material science behind this application is based on cathodic protection. Zinc is more anodic than steel; therefore, in the presence of moisture, the zinc acts as a sacrificial anode, corroding preferentially to the underlying steel. This prevents the oxidation process from penetrating the substrate, effectively "healing" the steel and providing a durable barrier against future atmospheric attacks.

The application process must be precise to avoid "pinholes" or thin spots in the coating, which could become new sites for corrosion. We utilize airless spray application to ensure a uniform dry film thickness (DFT) that meets ASTM standards for industrial coatings. The primer not only seals the steel but also creates a chemical bond that passivates the surface, neutralizing the remaining microscopic oxide particles. For municipal complexes, where the building envelope must last for decades, this layer of zinc-rich passivation is the primary line of defense against the harsh environmental conditions typical of commercial roof systems.

  • Application of zinc-rich primers with a minimum dry film thickness (DFT) per manufacturer specifications.
  • Implementation of cathodic protection to prevent the migration of rust beneath the coating.
  • Ensuring full coverage of the flute valleys to eliminate potential water traps.
  • Monitoring ambient temperature and humidity to ensure optimal curing of the chemical bond.
  • Cross-hatch adhesion testing to verify the primer's bond strength to the remediated steel.

Structural Reinforcement and Fastener Integrity

In cases where the forensic audit revealed significant section loss—specifically in the thinned flutes of the steel deck—mechanical reinforcement is required. When the steel gauge has been reduced beyond acceptable engineering tolerances, we implement structural reinforcement using galvanized steel shims or welded reinforcement plates. This process restores the load-bearing capacity of the deck and ensures that the roof can support the weight of the new membrane and insulation. This reinforcement is critical in municipal buildings where heavy equipment, such as industrial HVAC units, may be situated directly over the affected areas.

The final stage of the remediation involves the securing of fasteners and the restoration of the building envelope's continuity. We replace all corroded fasteners with heavy-duty, corrosion-resistant galvanized or stainless steel fasteners. Each fastener is torqued to specific engineering requirements to ensure a tight seal against the deck. By combining structural reinforcement with a passivated surface and secure fastening, we create a redundant system of protection. The result is a restored structural deck that is not only chemically protected from rust but mechanically reinforced to handle the operational demands of a high-traffic administrative complex.

  • Installation of reinforcement plates in areas of critical section loss to restore structural gauge.
  • Replacement of oxidized fasteners with high-strength, corrosion-resistant alternatives.
  • Application of sealant beads to fastener heads to prevent moisture ingress.
  • Verification of deck stability through load-testing in reinforced zones.
  • Final inspection of the building envelope to ensure a seamless transition from the deck to the roof membrane.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #722

Hands-On Physical Roof Inspections & Boots-on-the-Roof Forensic Maintenance Audits on Commercial High-Rise Commercial Penthouse Towers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Hands-On Physical Roof Inspections & Boots-on-the-Roof Forensic Maintenance Audits on Commercial High-Rise Commercial Penthouse Towers

The Forensic Philosophy of High-Rise Envelope Auditing

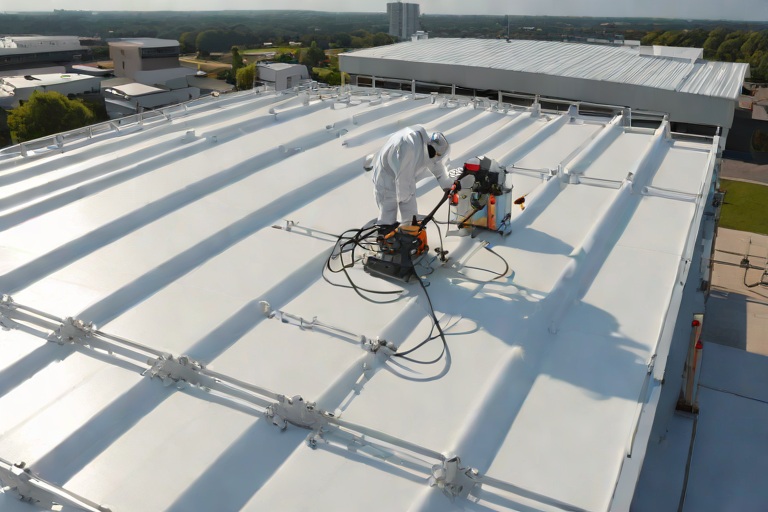
In the realm of high-rise commercial penthouse towers, the distinction between a standard visual inspection and a forensic maintenance audit is the difference between observing a symptom and diagnosing a disease. A visual inspection is a passive exercise; a forensic audit is an aggressive, physical interrogation of the building envelope. At the penthouse level, the roof is subjected to extreme atmospheric pressures, intense UV radiation, and significant thermal cycling that causes the substrate to expand and contract at rates far exceeding those of low-slope ground-level structures. This constant movement places immense shear stress on every seam, fastener, and flashing detail.

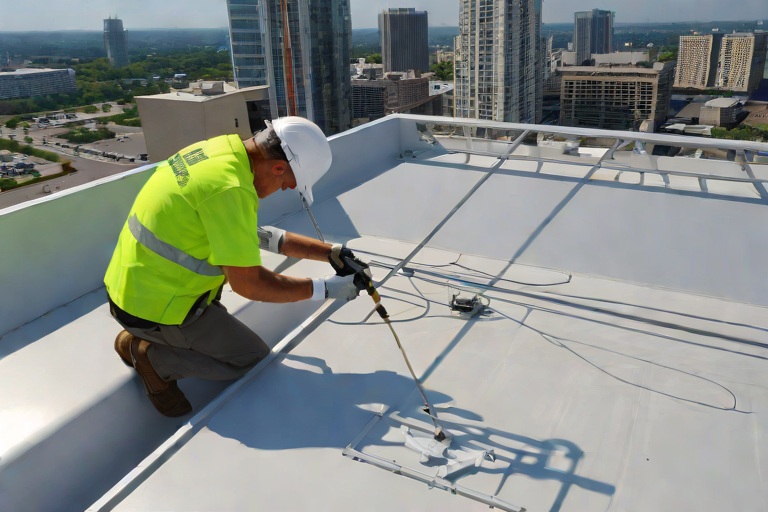
A master-level audit requires a "boots-on-the-roof" methodology that prioritizes physical verification over assumptions. We operate under the premise that the membrane is a living system that degrades unevenly. The goal is to identify latent failures—leaks that have not yet manifested as interior ceiling stains but are already compromising the insulation system through capillary action. By utilizing a rigorous engineering approach, we analyze the interaction between the membrane, the mechanical fasteners, and the structural deck to ensure the building envelope remains airtight and watertight under peak wind-load conditions.

  • Evaluation of wind-uplift resistance according to ASCE 7 standards.
  • Analysis of thermal bridging at penthouse parapet junctions.
  • Assessment of UV-induced polymer degradation in TPO and PVC membranes.
  • Verification of drainage slope efficiency to prevent ponding and hydrostatic pressure.

Mechanical Integrity and the Science of Seam Probing

Automated seams, while efficient during installation, are the primary failure points in high-rise environments. The reliance on robotic welders can lead to "cold welds" or inconsistent fusion if the temperature and speed parameters were not perfectly calibrated to the ambient conditions of the penthouse height. A forensic audit demands the use of a tapered steel probe to physically interrogate every linear foot of the seam. This is not a cursory glance; it is a systematic process of applying targeted pressure to detect "fishmouths" or voids where the weld has failed to achieve a molecular bond.

From a material science perspective, a failed seam is often a result of the coefficient of thermal expansion differing between the membrane and the underlying insulation. When the penthouse tower sways or shifts, these seams act as the primary stress-absorption points. If the weld is brittle or insufficient, the seam will split. We categorize these failures by their depth and length, determining whether the failure is superficial or a complete breach of the waterproof layer. This process ensures that the membrane maintains its integrity as a monolithic shield against the elements.

  • Utilization of 0.032-inch tapered probes for precise void detection.
  • Cross-referencing seam failure patterns with building sway and structural movement.
  • Testing for "peel strength" to ensure compliance with ASTM standards for heat-welded seams.
  • Identification of "cold spots" in automated welds that indicate insufficient heat application.

Critical Penetration Analysis and Hardware Torque Specifications

The most catastrophic failures in penthouse towers typically occur at the penetration points, specifically at the drain bowls and perimeter cleats. A drain bowl is not merely a hole in the roof; it is a complex transition zone where the membrane must be mechanically locked to a rigid metal flange. We employ a strict torque-verification process for clamping rings. Over-tightened clamps can crush the membrane, leading to stress cracking, while under-tightened clamps allow for micro-movements that eventually break the seal. We utilize calibrated torque wrenches to ensure that every bolt meets the manufacturer's engineering specifications.

Perimeter cleats and termination bars require similar scrutiny. In high-rise environments, the "edge-effect" creates turbulent wind vortices that attempt to peel the membrane away from the parapet wall. If the perimeter cleats are spaced too far apart or are improperly fastened into the masonry, the resulting wind-uplift can cause a cascading failure of the entire roof section. Our audit examines the fastening pattern and the condition of the sealant beads behind the termination bars, ensuring that there is no moisture ingress behind the flashing that could lead to substrate rot or mold growth within the penthouse walls.

  • Verification of clamping torque to prevent membrane compression or slippage.
  • Inspection of perimeter flashing for signs of wind-scour and mechanical fatigue.
  • Audit of fastener spacing and embedment depth in accordance with ANSI standards.
  • Examination of flashing "lap-over" lengths to ensure adequate water shedding.

Engineering Documentation and Lifecycle Prognosis

The culmination of a forensic audit is the written engineering report. A list of leaks is a repair bill; a forensic report is a strategic asset management document. We translate physical findings into a data-driven narrative that categorizes risks based on severity and probability of failure. This includes the use of high-resolution photographic evidence mapped to a roof plan, allowing the building owner to visualize the exact location of every compromised seam or loose fastener. The report focuses on the "why" of the failure, not just the "where," providing a root-cause analysis that informs future maintenance cycles.

Finally, we provide a lifecycle prognosis. By analyzing the current state of the building envelope, we can predict the remaining useful life of the roof system. We evaluate the loss of plasticizers in the membrane and the degradation of the flashing adhesives to determine when a full replacement will be necessary versus targeted rehabilitations. This engineering-led approach shifts the paradigm from reactive patching to proactive asset preservation, ensuring that the penthouse tower remains secure, dry, and structurally sound for decades to come.

  • Creation of a prioritized "Risk Matrix" for immediate, short-term, and long-term repairs.
  • Mapping of all identified anomalies to a CAD-based roof plan for precision tracking.
  • Calculation of estimated remaining service life based on material degradation rates.
  • Development of a customized forensic maintenance schedule to prevent future systemic failures.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #723

60-Mil TPO Robotic Hot-Air Seam Fusion & Test-Cut Peel Audits on Commercial Regional Healthcare Medical Centers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
60-Mil TPO Robotic Hot-Air Seam Fusion & Test-Cut Peel Audits on Commercial Regional Healthcare Medical Centers

Thermal Dynamics of 60-Mil TPO Fusion in Critical Healthcare Infrastructure

In the realm of commercial building envelope engineering, the integrity of a Regional Healthcare Medical Center depends entirely on the reliability of its primary moisture barrier. For these facilities, we specify a 60-mil Thermoplastic Olefin (TPO) membrane, as the increased thickness provides superior puncture resistance and a more robust substrate for thermal welding compared to standard 45-mil systems. The core of the engineering challenge lies in the molecular entanglement achieved during the hot-air welding process. To achieve a monolithic bond, the TPO must be heated to a precise state of plasticity where the polymer chains can intermingle across the seam interface.

We calibrate our robotic fusion systems to a sustained 1,000°F. This specific temperature is not arbitrary; it is the critical threshold required to overcome the heat-sink effect of the underlying insulation and the ambient atmospheric conditions of the roof deck. If the temperature drops below this threshold, the result is a "cold weld," which may appear visually sealed but lacks the molecular cohesion to withstand the cyclic thermal expansion and contraction inherent in large-scale medical complexes. Conversely, exceeding this temperature risks thermal degradation or "scorching," which breaks down the polymer chain and creates a brittle seam prone to premature failure.

  • Molecular Entanglement: The process of fusing two separate membrane sheets into a single, continuous piece of plastic.
  • Thermal Mass Management: Accounting for the heat absorption of the roof deck to maintain a constant 1,000°F at the weld point.
  • Polymer Stability: Ensuring the TPO does not reach its degradation point, which would compromise the UV-resistant layer.
  • Thickness Consistency: Utilizing 60-mil specifications to provide a larger window for heat penetration without risking burn-through.

Robotic Calibration: Nozzle Pressure and Travel Velocity

Human error is the primary catalyst for envelope failure in traditional hand-welding applications. To mitigate this risk in high-stakes healthcare environments, Aquashield Corporate employs automated robotic seam fusion. The engineering focus shifts from manual dexterity to the precise calibration of three variables: nozzle pressure, travel velocity, and heat consistency. The robotic welder operates on a programmed path, ensuring that every linear inch of the seam receives the exact same caloric input. This eliminates the "stop-and-start" inconsistencies common in manual welding, where heat spikes often occur at the beginning and end of a weld run.

Nozzle pressure is critical for forcing the 1,000°F air into the overlap, ensuring that no air pockets or "voids" are trapped within the seam. We maintain a constant pneumatic pressure that compresses the upper membrane against the lower sheet, creating a high-pressure environment that accelerates the fusion process. Simultaneously, the travel velocity is locked to a specific inches-per-minute (IPM) rate. If the robot moves too quickly, the membrane does not reach the required fusion temperature; if it moves too slowly, the heat accumulates, potentially warping the membrane or causing a "blow-out" where the air pressure ruptures the softened plastic.

  • Automated Travel Velocity: Maintaining a constant IPM to ensure uniform heat distribution across the entire roof plane.
  • Pneumatic Nozzle Pressure: Utilizing calibrated air pressure to eliminate voids and ensure intimate contact between membrane layers.
  • Path Precision: Robotic guidance systems that ensure a consistent 6-inch overlap, exceeding minimum industry standards.
  • Real-time Monitoring: Digital feedback loops that adjust heat output based on real-time sensor data from the nozzle tip.

Destructive Test-Cut Peel Audits and Validation

A visually perfect seam is not necessarily a waterproof seam. In the medical center environment, where a single leak can contaminate a sterile surgical suite or damage multi-million dollar imaging equipment, visual inspection is insufficient. We implement a rigorous destructive testing protocol known as the Test-Cut Peel Audit. This process involves cutting a sample section of the welded seam—typically a 2-inch by 6-inch strip—and subjecting it to a controlled peel test. This is the only definitive way to validate that the robotic fusion has achieved a structural bond that is stronger than the membrane itself.

The engineering goal of the peel test is to achieve a "membrane failure" rather than a "seam failure." When the technician pulls the sample apart, the TPO membrane should tear or rip before the welded seam separates. If the seam peels apart cleanly, it indicates a failure in the thermal dynamics—likely due to insufficient heat or incorrect nozzle pressure. These audits are performed at random intervals across the roof, including high-stress areas such as flashing, corners, and penetration points. This data-driven approach transforms the roofing process from a trade of "best efforts" to a disciplined engineering science aligned with ASTM standards for thermoplastic roofing.

  • Destructive Sampling: The strategic removal of seam sections to verify internal weld quality.
  • Membrane Failure Criterion: The gold standard of a weld where the plastic tears before the bond breaks.
  • ASTM Compliance: Adhering to recognized industry standards for the testing of single-ply roofing membranes.
  • Audit Frequency: Establishing a statistical confidence interval by testing a set percentage of total linear seam footage.

Building Envelope Integrity and Healthcare Risk Mitigation

The roof of a Regional Healthcare Medical Center is more than just a cover; it is a critical component of the building's life-safety systems. The integration of 60-mil TPO with robotic fusion and destructive auditing creates a redundant layer of protection. By focusing on the material science of the 1,000°F fusion and the precision of automated kinematics, we eliminate the vulnerabilities associated with traditional roofing. The result is a building envelope that can withstand extreme weather events and the heavy vibrations caused by massive rooftop HVAC units and medical gas venting systems.

From a risk management perspective, the cost of a comprehensive engineering audit is negligible compared to the cost of an unplanned roof failure in a healthcare setting. Water infiltration in a medical facility often leads to the growth of mold and fungi, which can trigger severe allergic reactions or infections in immunocompromised patients. By validating the seal through destructive peel tests, Aquashield Corporate provides the facility owners with documented proof of envelope integrity. This engineering-first approach ensures that the medical center can focus on patient care without the looming threat of catastrophic building envelope failure.

  • Sterile Environment Protection: Preventing moisture-driven mold growth in critical care areas.
  • Equipment Safeguarding: Protecting sensitive MRI and CT scanners from ceiling leaks.
  • Life-Cycle Extension: Increasing

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #724

High-Solids Silicone Monolithic Coating Restoration & Albedo Reflectance on Commercial University Research Laboratorys

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
High-Solids Silicone Monolithic Coating Restoration & Albedo Reflectance on Commercial University Research Laboratorys

Substrate Diagnostics and Building Envelope Audit

When managing the building envelope of a University Research Laboratory, the margin for error is nonexistent. These facilities often house sensitive instrumentation, hazardous materials, and high-value research that cannot be compromised by moisture infiltration or thermal instability. Our engineering audit began with a comprehensive forensic analysis of the existing roof assembly, which had suffered from systemic degradation of the original modified bitumen membrane. We observed significant evidence of thermal shock and mechanical fatigue around the extensive network of HVAC curbings and exhaust vents typical of laboratory environments.

The audit focused on identifying critical failure points where the building envelope was breached. We utilized infrared thermography to map subsurface moisture pockets and conducted core sampling to determine the saturation levels of the rigid insulation. The presence of trapped moisture creates a vapor drive that can cause blistering in standard coatings; therefore, a high-solids silicone approach was selected to accommodate the inherent breathability and flexibility required for such a complex substrate.

  • Assessment of existing flashing integrity at all penetration points and parapet walls.
  • Evaluation of substrate pH levels and contaminant identification to prevent osmotic blistering.
  • Mapping of thermal bridges that contribute to internal condensation within the research labs.
  • Verification of structural slope to ensure positive drainage and minimize prolonged ponding.
  • Analysis of existing membrane elasticity to determine the required modulus of the new coating.

Chemical Stabilization via Bleed-Blocking Epoxy Primers

One of the primary challenges in restoring aged commercial roofs is the migration of legacy oils, plasticizers, and contaminants from the old membrane into the new coating. In a university setting, where various roof patches and temporary repairs have often been applied over decades, this "bleed-through" can compromise the chemical bond of the silicone. To mitigate this risk, we engineered a stabilization phase utilizing a high-performance, bleed-blocking epoxy primer. This primer acts as a chemical barrier, sealing the substrate and neutralizing surface contaminants that would otherwise cause delamination.

The application of the epoxy primer is a precision operation. It requires a meticulously cleaned surface, achieved through a combination of mechanical scrubbing and chemical degreasing. By establishing a rigid, non-porous foundation, the epoxy primer ensures that the subsequent silicone layers adhere uniformly across the entire roof surface, regardless of the varying conditions of the underlying substrate. This process transforms a compromised surface into an engineered platform ready for a monolithic seal.

  • Elimination of surface tension issues to ensure maximum wetting of the primer.
  • Prevention of oil-based contaminants from migrating into the high-solids silicone layer.
  • Creation of a high-strength mechanical bond between the old membrane and the new system.
  • Stabilization of friable substrate materials to prevent voids in the final coating.
  • Ensuring a uniform surface profile to optimize the application of the 30-mil finish.

Engineering the 30-Mil Monolithic Silicone Membrane

The core of the restoration involves the application of a high-solids silicone coating, engineered to a 30-mil dry film thickness (DFT). Unlike traditional liquid-applied membranes that may thin out over depressions, a 30-mil monolithic application provides a consistent, seamless shield that is impervious to ponding water. This thickness is critical for university laboratories, where roof-top equipment often creates turbulence and mechanical stress on the membrane. The monolithic nature of the coating means there are no seams, laps, or fasteners—the primary failure points in traditional roofing systems.

From a material science perspective, the high-solids content ensures that the coating does not shrink significantly during the curing process. This maintains the integrity of the 30-mil specification across the entire field. We adhere to strict ASTM standards for application, utilizing calibrated airless sprayers and gauges to verify thickness in real-time. The result is a rubberized, flexible envelope that can expand and contract with the building's thermal movements while remaining completely watertight.

  • Application of a seamless, single-layer system that eliminates all mechanical seams.
  • Achievement of a 30-mil DFT to provide superior puncture resistance and durability.
  • Utilization of high-solids chemistry to prevent shrinkage and maintain membrane thickness.
  • Integration of all roof-top penetrations into a single, continuous waterproof envelope.
  • Compliance with ANSI and ASTM guidelines for commercial roof coating thickness and adhesion.

Albedo Reflectance and Zero-Downtime Operational Integration

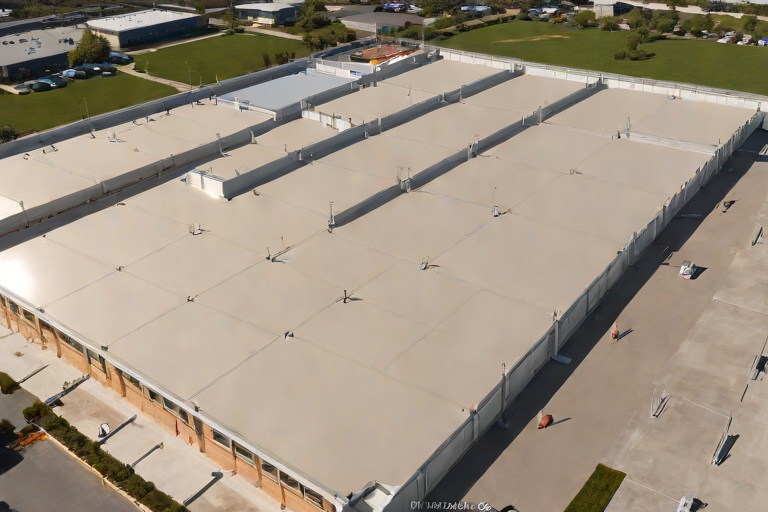
University research facilities are energy-intensive environments. To reduce the cooling load on the building's HVAC systems, we focused on the Albedo effect—the measure of solar reflectance. By applying a white high-solids silicone with an 88% solar radiation reflectance rating, we significantly lowered the surface temperature of the roof. This increase in albedo reduces the amount of heat transferred through the roof deck and into the laboratories below, leading to a measurable decrease in energy consumption and a more stable internal climate for sensitive experiments.

Perhaps the most critical requirement of this project was the mandate for zero-downtime application. Research laboratories cannot be shut down without risking years of data loss or the destruction of biological samples. Our team executed the restoration using a phased, non-disruptive approach. Because the silicone system cures chemically and does not emit hazardous fumes or require high-heat application, we were able to work directly above active laboratories without impacting the researchers inside. The transition from a failing roof to a high-reflectance, monolithic shield occurred without a single hour of facility downtime.

  • Reduction of the Urban Heat Island effect through 88% solar reflectance.
  • Lowering of peak cooling loads, extending the lifespan of the facility's HVAC equipment.
  • Implementation of a "silent" installation process to avoid disturbing laboratory operations.
  • Elimination of the need for interior shutdowns or temporary relocation of research staff.
  • Long-term reduction in operational expenditure through enhanced thermal efficiency.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #725

Tapered Polyiso Drainage Layouts (1/4-In/Ft) & Geometric Cricket Sizing on Commercial Suburban Corporate Office Parks

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Tapered Polyiso Drainage Layouts (1/4-In/Ft) & Geometric Cricket Sizing on Commercial Suburban Corporate Office Parks

The Mechanics of Tapered Polyisocyanurate Slope Engineering

In the context of a suburban corporate office park, the roof is not merely a cover but a complex hydraulic system. The primary objective of any building envelope audit is to verify that the tapered polyisocyanurate (polyiso) insulation is engineered to a minimum slope of 1/4-inch per foot. This specific gradient is the industry benchmark for ensuring that gravity effectively overcomes the surface tension of water on a commercial membrane, preventing the catastrophic onset of ponding. Polyiso is selected for these layouts due to its high R-value per inch and its superior compressive strength, which allows for the creation of precise, rigid slopes that do not slump over time under the weight of HVAC units or parapet loads.

When auditing these systems, we examine the precision of the tapered panels. A failure in the layout—often caused by improper installation of the "starter" strips or a misalignment of the tapered wedges—creates low spots. These depressions lead to standing water, which accelerates the degradation of the roof membrane through a process known as hydrostatic pressure. Over time, this pressure forces water through microscopic imperfections in the membrane or flashing, leading to saturated insulation and structural rot. To maintain a high-performance envelope, the following engineering standards must be strictly adhered to:

  • Strict adherence to ASTM D2118 for the measurement of thermal insulation properties to ensure consistent density across the slope.
  • Verification of the "slope-to-drain" layout to ensure no water is trapped between the primary slope and the roof perimeter.
  • Utilization of high-density polyiso to prevent "crushing" at the points of highest compression, such as under heavy equipment curbs.
  • Implementation of a seamless transition between the tapered insulation and the primary drainage points to avoid "damming" at the drain flange.

Geometric Cricket Sizing and Diamond Valley Configuration

One of the most critical failures in corporate office park roofing is the accumulation of water in the internal corners of parapet walls or around large mechanical penthouses. To mitigate this, we employ geometric crickets—sloped inserts designed to divert water away from walls and toward the primary drains. In complex architectural layouts, a standard cricket is often insufficient. We implement the "Diamond Valley" configuration, a sophisticated multi-directional slope that creates a V-shaped trough, forcing water to move diagonally across the roof plane rather than pooling against a structural wall.

The engineering of a diamond valley requires precise calculations of the valley's angle and depth. If the cricket is too shallow, surface tension will cause water to "creep" back toward the wall; if it is too steep, it can create an abrupt transition that stresses the membrane. The goal is to create a fluid, continuous path of least resistance. This geometric approach ensures that runoff is accelerated toward the primary drainage system, effectively eliminating the "dead zones" typically found in the corners of large-scale corporate footprints.

  • Calculation of the cricket's "rise and run" to maintain a consistent 1/4-inch per foot minimum, even in tight corner configurations.
  • Integration of reinforced valley flashing to handle the increased volume of water concentrated by the cricket.
  • Strategic placement of crickets at every intersection of a parapet and a roof plane to prevent "wall-wash" erosion.
  • Use of tapered insulation templates that are custom-cut to fit the exact geometry of the building's architectural offsets.

Runoff Diversion and Expansion Joint Integrity

Expansion joints are the most vulnerable points in a building envelope. These joints are designed to allow the corporate office structure to expand and contract due to thermal fluctuations, but they often become conduits for leaks if the drainage layout is poorly engineered. A master-level installation requires that the tapered polyiso be configured to route runoff *away* from the expansion joint. Routing water directly over a joint increases the risk of flashing failure and allows moisture to penetrate the structural gap, which can lead to the corrosion of steel supports and the growth of mold within the plenum.

To achieve this, we engineer "diverter slopes" around the expansion joint. By slightly altering the polyiso layout, we create a subtle ridge that sheds water toward the perimeter or the interior drains, ensuring the joint remains dry. This requires a deep understanding of the coefficient of thermal expansion for the specific materials used in the building's construction. When the roof is engineered to keep water away from these movement joints, the lifespan of the entire envelope is extended by several years, as the flashing is not subjected to constant hydrostatic stress.

  • Installation of oversized flashing membranes that overlap the expansion joint to provide a secondary layer of protection.
  • Engineering of "shedding" slopes that ensure water moves laterally away from the joint's center line.
  • Regular inspection of the joint's sealant and flashing for signs of fatigue caused by thermal cycling.
  • Coordination between the structural engineer and the roofing contractor to ensure the joint's movement range is compatible with the membrane's elasticity.

Engineering Audit Metrics and Ponding Elimination

The final phase of a building envelope audit involves a rigorous verification of the roof's performance using empirical data. We utilize infrared thermography to identify "thermal anomalies," which indicate areas where water has saturated the insulation. Because water holds heat differently than polyiso, these anomalies reveal hidden ponding areas that are not visible to the naked eye. A successful audit confirms that no area of the roof holds standing water for more than 48 hours, as defined by the industry standard for "ponding."

Eliminating ponding is not just about the initial slope; it is about the long-term stability of the substrate. Over time, corporate office parks may experience slight structural settling. An engineered layout must account for this by providing a "safety factor" in the slope. By ensuring the polyiso layout is robust and the drainage points are clear of debris, we ensure that the building envelope remains a monolithic barrier against the elements. The result is a reduction in maintenance costs and the total elimination of interior leaks, preserving the corporate asset's value.

  • Application of ASTM E1077 standards to evaluate the effectiveness of the water-shedding capabilities of the roof surface.
  • Conducting "flood tests" on critical areas, such as diamond valleys and expansion joints, to verify watertight integrity.
  • Mapping the "time-to-drain" metric to ensure that runoff reaches the primary drains within the engineered timeframe.
  • Implementing a scheduled maintenance audit every 24 months to verify that the tapered system has not shifted or compressed.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #726

Multi-Ply SBS-Modified Bitumen Cap Sheet Application & Vapor Control on Commercial Big-Box Retail Power Centers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Multi-Ply SBS-Modified Bitumen Cap Sheet Application & Vapor Control on Commercial Big-Box Retail Power Centers

Substrate Preparation and Internal Vapor Drive Regulation

In the engineering of a Big-Box Retail Power Center, the sheer scale of the roof area creates a massive thermal chimney effect. The primary challenge in these environments is not merely the exclusion of precipitation, but the regulation of internal vapor drive. Moisture originating from the conditioned retail space—often exacerbated by high-humidity HVAC cycles and internal product storage—seeks a path of least resistance toward the colder exterior. If the building envelope is not meticulously engineered, this vapor pressure leads to interstitial condensation, which manifests as blistering or "bubbling" in the modified bitumen membrane.

A comprehensive audit of the substrate reveals that the success of a multi-ply SBS (Styrene-Butadiene-Styrene) system depends entirely on the integrity of the vapor retarder. We specify a high-performance vapor barrier that adheres to ASTM E96 standards to ensure that the permeability is kept to a minimum. By controlling the vapor drive at the deck level, we prevent the accumulation of moisture within the insulation layers, which would otherwise compromise the adhesive bond of the cap sheet during thermal cycling.

  • Implementation of a continuous vapor barrier to eliminate moisture migration from the interior.
  • Verification of substrate dryness to prevent "outgassing" during the cold-applied adhesive process.
  • Application of high-density polyisocyanurate insulation to provide a stable thermal break.
  • Rigorous inspection of the deck for contaminants, oils, or dust that could inhibit chemical bonding.

Cold-Applied Adhesive Shear Resistance and Bonding

The transition from torch-applied to cold-applied SBS systems in large-scale retail centers is driven by safety and the need for consistent thickness across vast surface areas. However, the engineering focus shifts toward the chemistry of shear resistance. Cold-applied adhesives must create a molecular bond that can withstand the significant lateral forces generated by the coefficient of thermal expansion. In a power center, the roof can expand and contract several inches over the length of the building; if the adhesive lacks sufficient shear resistance, the membrane will slide, leading to "fish-mouths" or seam separation.

Our technical approach utilizes a high-solids, modified bitumen adhesive that maintains flexibility at low temperatures while resisting creep at high temperatures. The shear resistance is measured by the adhesive's ability to distribute the load across the entire bonding surface rather than concentrating stress at the edges of the laps. This ensures that the membrane remains monolithic, effectively acting as a single, cohesive skin over the building's structural steel.

  • Utilization of solvent-based or water-based adhesives tailored to the specific substrate porosity.
  • Application of adhesive in a uniform "spread" to avoid voids that could allow air pockets to form.
  • Monitoring of ambient temperature and dew point to ensure the adhesive cures according to manufacturer specifications.
  • Testing of bond strength through pull-tests to verify that the failure occurs within the substrate rather than at the adhesive interface.

Precision Installation: Staggered Side Laps and Seam Integrity

From a master tradesman's perspective, the most critical failure point in any multi-ply system is the seam. In a Big-Box retail environment, a linear failure can lead to catastrophic water intrusion across thousands of square feet. To mitigate this, we employ a rigorous staggered side lap protocol. By offsetting the vertical seams of the cap sheet from the seams of the base sheet, we eliminate the "stacking" of joints. This engineering tactic ensures that there is no continuous vertical path for water to penetrate the envelope through capillary action.

The precision of these laps is non-negotiable. Each side lap is overlapped by a minimum of six inches, and the end laps are extended to twelve inches to provide a redundant seal. We focus on the "lap-over-lap" technique, ensuring that the flow of water is always directed over the seam and never into it. This geometry transforms the roof into a series of interlocking shields, significantly reducing the risk of systemic leaks during extreme weather events or hydrostatic pressure buildup.

  • Strict adherence to a 6-inch minimum side lap and 12-inch end lap configuration.
  • Staggering of seams by at least 48 inches between successive plies to break the linear path of potential leaks.
  • Use of a weighted rollers to ensure 100% contact between the adhesive and the SBS membrane.
  • Detailed auditing of all T-joints and corners, where the highest concentration of stress occurs.

Granule Surface Protection and UV Degradation Control

The final layer of the SBS-modified bitumen system is the granule-surfaced cap sheet, which serves as the primary defense against ultraviolet (UV) radiation. In the context of a retail power center, the roof is exposed to constant solar bombardment, which can lead to the photo-oxidation of the bitumen. Without a properly embedded granule layer, the bitumen would become brittle, crack, and eventually lose its waterproofing capabilities. The granules act as a sacrificial layer, absorbing the UV energy and protecting the modified bitumen beneath.

Our audit focuses on the "embedment depth" and the uniformity of the granule distribution. We ensure that the granules are fused into the bitumen during the manufacturing process to prevent "scouring"—the process where wind and rain strip the granules away. Furthermore, the color and composition of the granules are selected to increase the Solar Reflectance Index (SRI), which reduces the heat island effect and lowers the cooling costs for the retail tenant by minimizing thermal bridging into the building interior.

  • Verification of granule embedment to prevent surface erosion and UV penetration.
  • Assessment of the surface for "bald spots" that could lead to localized bitumen degradation.
  • Integration of reflective granule coatings to lower the overall roof surface temperature.
  • Implementation of a regular maintenance schedule to clear debris that could trap moisture against the granule surface.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #727

Parapet Wall Heavy-Gauge 20-Gauge Kynar 500 Coping Cap Continuous Cleat Locking on Commercial Food Packaging & Cold Logistics Plants

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Parapet Wall Heavy-Gauge 20-Gauge Kynar 500 Coping Cap Continuous Cleat Locking on Commercial Food Packaging & Cold Logistics Plants

Material Science and Structural Integrity of 20-Gauge Kynar 500 Systems

In the high-stakes environment of food packaging and cold logistics plants, the building envelope is the first line of defense against atmospheric contaminants and extreme thermal gradients. For these facilities, standard 24-gauge coping is often insufficient due to the sheer scale of the parapets and the mechanical vibrations inherent in industrial refrigeration systems. We specify 20-gauge steel to provide the necessary structural rigidity to prevent "oil-canning" or bowing, which can compromise the water-tight seal of the coping cap. The choice of Kynar 500, a polyvinylidene fluoride (PVDF) resin, is non-negotiable for these assets. Unlike standard polyester coatings, Kynar 500 offers superior resistance to the caustic cleaning agents used in food-grade environments and maintains its color and gloss despite intense UV exposure.

The engineering logic behind the heavy-gauge selection extends beyond simple durability. In a cold logistics plant, the temperature differential between the interior freezer space and the exterior roof surface creates significant stress on the building's skin. A thicker gauge of steel provides a more stable substrate for the continuous cleat system, ensuring that the fasteners do not pull through the metal during extreme wind events or thermal contraction cycles.

  • Enhanced gauge thickness reduces the risk of structural deformation under wind load.
  • PVDF coatings prevent chemical degradation from industrial scrubbers and environmental pollutants.
  • Increased mass provides better dampening against wind-induced vibration.
  • Superior rigidity ensures a tighter fit against the parapet wall masonry or steel stud framing.

ANSI/SPRI ES-1 Wind Uplift Engineering and Continuous Cleat Engagement

The perimeter of a commercial roof is the most vulnerable point of the building envelope. Wind scouring and the Venturi effect create intense negative pressure (suction) at the parapet edge, which can lead to catastrophic "peel" failure if the coping is only secured with intermittent fasteners. To mitigate this, we implement a continuous cleat locking system. This engineering approach transforms the coping cap from a series of overlapping plates into a unified, mechanically locked beam. By utilizing a continuous cleat, we distribute the wind uplift loads across the entire length of the parapet rather than concentrating the stress on a few isolated screws.

Our adherence to ANSI/SPRI ES-1 standards ensures that the assembly is engineered for the specific wind zone of the facility. The continuous cleat acts as a structural bridge, locking the coping cap to the wall substrate and preventing the wind from getting underneath the leading edge. When the wind hits the vertical face of the parapet, the resulting pressure is transferred directly into the building's structural frame via the cleat, effectively neutralizing the uplift forces that typically strip coping caps from the roof edge.

  • Elimination of "point-load" failures associated with traditional intermittent fastening.
  • Mechanical interlocking that prevents the wind from initiating a peel-back sequence.
  • Distribution of shear forces across the full perimeter of the roofline.
  • Strict compliance with ANSI/SPRI ES-1 for high-velocity hurricane zones and industrial wind loads.

Thermal Expansion Dynamics and Splice Plate Engineering

One of the most overlooked aspects of coping cap installation in cold logistics plants is the coefficient of thermal expansion. Steel expands and contracts significantly as temperatures fluctuate. In a facility where the interior is kept at sub-zero temperatures while the roof surface may reach 150 degrees Fahrenheit in direct sunlight, the coping cap is subject to extreme linear movement. If the system is installed too rigidly, the metal will buckle, leading to gaps in the joints and eventual water infiltration. To solve this, we utilize precision-engineered thermal expansion splice plates.

These splice plates allow the 20-gauge steel to "breathe" without compromising the water-tight integrity of the joint. By utilizing a sliding lap joint configuration, the coping sections can expand and contract independently. The splice plates are designed to maintain a constant overlap, ensuring that water cannot penetrate the joint even when the metal is at its maximum contraction. This prevents the common failure point where the coping pulls away from the wall, exposing the underlying insulation and flashing to the elements.

  • Implementation of sliding lap joints to accommodate linear thermal movement.
  • Prevention of "buckling" or "weaving" caused by restricted thermal expansion.
  • Use of heavy-duty splice plates to maintain a consistent seal during temperature swings.
  • Reduction of stress on the continuous cleat fasteners during winter contraction cycles.

Perimeter Peel Mitigation and Long-Term Envelope Stability

The final stage of a professional building envelope audit focuses on perimeter peel mitigation. Peel occurs when wind enters the gap between the coping cap and the parapet wall, creating an internal pressure bubble that forces the metal upward. To combat this, we employ a holistic sealing strategy that begins with the continuous cleat and ends with high-performance perimeter sealant and precise flashing integration. The goal is to create a "closed-loop" system where there is no available entry point for wind-driven rain or air pressure.

In our experience, the longevity of a food packaging plant's roof depends on the stability of this perimeter. By combining 20-gauge Kynar 500 steel with a continuous locking mechanism and thermal splice plates, we create an envelope that is virtually impervious to the elements. This system not only protects the structural integrity of the building but also ensures that the facility remains compliant with health and safety regulations by preventing leaks that could lead to mold growth or contamination of food products.

  • Strategic use of industrial-grade sealants at all termination points.
  • Integration of drip edges to ensure water is shed away from the building face.
  • Regular audit intervals to inspect splice plate movement and fastener torque.
  • Comprehensive flashing overlap to ensure a redundant water-shedding path.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #728

Industrial Drainage Scuppers, Overflow Weirs & Heavy Downspout Expansion Bellows on Commercial Semiconductor Cleanroom Fabs

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Industrial Drainage Scuppers, Overflow Weirs & Heavy Downspout Expansion Bellows on Commercial Semiconductor Cleanroom Fabs

Hydraulic Head-Loss and Primary Drainage Geometry in Large-Scale Fabs

In the context of semiconductor cleanroom facilities, the roof is not merely a cover but a critical component of the building envelope that protects billions of dollars in sensitive lithography equipment. These structures typically feature massive, flat-roof footprints that challenge traditional drainage logic. When managing thousands of gallons of precipitation per minute, the primary concern is the mitigation of hydraulic head-loss. Head-loss occurs when the energy of the flowing water is dissipated due to friction against the membrane and turbulence at transitions, leading to premature ponding and increased hydrostatic pressure on the roof substrate.

To maintain the structural integrity of the deck, we employ a rigorous analysis of the Manning formula for open channel flow. On a semiconductor fab, where tolerances are razor-thin, we cannot rely on "standard" slopes. We specify a minimum slope of 1/4 inch per foot, but in high-capacity zones, we engineer tapered insulation systems that create precise valleys. This ensures that the water velocity remains constant and does not drop below the critical threshold where sediment buildup begins to obstruct the primary drains.

  • Calculation of friction factors based on the specific coefficient of the TPO or PVC membrane.
  • Analysis of "dead spots" where structural columns or HVAC curbs disrupt the laminar flow of water.
  • Implementation of precision-leveled sleepers to support heavy-duty drainage conduits.
  • Evaluation of the roof's "time of concentration" to ensure primary drains are not overwhelmed during peak intensity.

Emergency Overflow Weir Sizing and Scupper Integration

A primary drainage failure on a cleanroom fab is a catastrophic event; therefore, the secondary emergency overflow system must be engineered as a fail-safe of absolute reliability. We design these systems using the principle of the overflow weir. The weir is essentially a calibrated gap in the parapet wall that allows water to exit the roof surface before it reaches a depth that threatens the structural load capacity of the roof slab. According to ANSI and IBC standards, these overflows must be sized to handle the entirety of the primary system's capacity plus a safety margin for 100-year storm events.

The critical engineering challenge here is the "weir height" relative to the primary drain. We typically set the overflow scuppers 2 inches above the primary drain elevation. This ensures that the primary system does the heavy lifting, while the overflows remain dormant until a critical head of water is reached. If the weir is too low, the primary drains become useless; if it is too high, the roof may suffer a structural collapse due to the weight of standing water, which weighs approximately 62.4 pounds per cubic foot.

  • Sizing of scupper widths based on the calculated "head" of water allowed before structural distress.
  • Installation of heavy-gauge galvanized steel scupper sleeves to prevent membrane tearing at the parapet penetration.
  • Integration of external splash pads to prevent soil erosion and foundation undermining at the discharge point.
  • Verification of "free-flow" conditions to ensure no back-pressure exists within the overflow conduit.

Conductor Head Engineering and Vortex Mitigation

The transition from the horizontal roof plane to the vertical downspout is where most drainage failures occur. This is the domain of the conductor head. In a semiconductor fab, the volume of water hitting the conductor head can create a "vortex" or a "gulping" effect, where air is trapped in the downspout, creating a pneumatic lock that slows the drainage rate. To combat this, we specify oversized, deep-sump conductor heads that act as a buffer, allowing the water to stabilize before entering the vertical drop.

From a craftsmanship perspective, the flashing at the conductor head is the most vulnerable point of the building envelope. We utilize a multi-stage flashing detail, incorporating a reinforced flashing curb and a heat-welded membrane seal that extends 12 inches up the conductor head. This prevents capillary action from drawing water back under the membrane, which would otherwise lead to slow-leaks into the cleanroom environment below—a scenario that would trigger an immediate facility shutdown.

  • Utilization of cast-iron or heavy-gauge aluminum conductor heads to withstand high-velocity impact.
  • Implementation of vortex breakers or internal baffles to maximize the air-to-water ratio in the downspout.
  • Strict adherence to ASTM standards for sealant compatibility between the metal head and the synthetic membrane.
  • Engineering of "sump" depths to ensure a constant hydraulic head for the vertical run.

Thermal Expansion Bellows and Material Science in Downspouts

Semiconductor fabs are often massive in height and width, meaning the vertical downspouts can span several stories. Metal expands and contracts significantly based on ambient temperature fluctuations. Without proper mitigation, this thermal cycling creates immense stress on the roof connections and the ground-level discharge points. If a downspout is rigidly fixed at both ends, the resulting thermal expansion can actually lift the conductor head off the roof or buckle the pipe, creating a leak path.

To solve this, we integrate heavy-duty expansion bellows or slip joints at calculated intervals. These bellows are constructed from high-grade stainless steel or reinforced elastomers that allow the pipe to expand and contract axially without transferring that force to the building envelope. We calculate the total linear expansion using the coefficient of thermal expansion for the specific alloy used—typically aluminum or galvanized steel—and place the bellows at the mid-point of the vertical run to balance the movement.

  • Installation of slip-joint couplings that allow for 2 to 4 inches of vertical movement.
  • Selection of bellows materials that are chemically compatible with the industrial coatings used on the fab exterior.
  • Use of heavy-duty anchor clamps to ensure the pipe remains centered during thermal shifts.
  • Regular auditing of joint integrity using infrared thermography to detect early signs of seal failure.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #729

AOC 581 Elastomeric Structural Mastic Detailing Around Rooftop HVAC Curbs on Commercial Intermodal Cargo Freight Terminals

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
AOC 581 Elastomeric Structural Mastic Detailing Around Rooftop HVAC Curbs on Commercial Intermodal Cargo Freight Terminals

The Engineering Challenge of Intermodal Terminal Envelopes

Intermodal cargo freight terminals represent some of the most hostile environments for commercial roofing systems. Unlike standard warehouse facilities, these structures are subject to constant, high-amplitude vibrations caused by the movement of heavy rail cars and heavy-duty drayage trucks. This persistent seismic activity creates a state of perpetual stress on the building envelope, specifically at the transition points where rooftop HVAC curbs meet the primary roof membrane. In a recent engineering audit, we observed that standard flashing methods often fail prematurely in these environments due to the sheer magnitude of dynamic loading.

The critical failure point is typically the curb-to-deck interface. When a massive HVAC unit operates, the combination of mechanical vibration and the structural oscillation of the terminal building creates a "sawing" effect on traditional sealants. This leads to cohesive failure within the sealant bead or adhesive failure at the substrate bond. To combat this, the application of AOC 581 Elastomeric Structural Mastic is not merely a preference but a structural necessity. This material is engineered to act as a flexible bridge, absorbing the energy of the building's movement while maintaining a hermetic seal against water infiltration.

  • Dynamic Load Distribution: AOC 581 distributes mechanical stress across a wider surface area, preventing localized tearing of the membrane.
  • Substrate Compatibility: The mastic adheres aggressively to galvanized steel, concrete, and modified bitumen, ensuring a unified bond.
  • Vibration Dampening: The elastomeric properties of the compound reduce the transmission of HVAC harmonic resonance into the roof deck.
  • Environmental Resistance: Designed to withstand the extreme temperature swings common in open-air freight terminals.

Mitigating Mechanical Vibration and Thermal Expansion Drift

From a material science perspective, the primary enemy of the rooftop curb is thermal expansion drift. Large-scale intermodal terminals often feature expansive roof footprints that undergo significant dimensional changes as ambient temperatures shift. Because the HVAC curb is a rigid structural element and the roof membrane is a flexible layer, these two components move at different rates. This differential movement, known as thermal drift, puts immense strain on the perimeter seals, often resulting in "alligatoring" or complete separation of the flashing.

The implementation of AOC 581 addresses this by utilizing a high-elongation elastomeric formula. Unlike rigid caulks that crack under tension, this structural mastic maintains its "memory," returning to its original shape after the stressor is removed. By creating a wide, tapered transition zone around the curb, we effectively manage the coefficient of thermal expansion. This ensures that the seal remains intact even when the roof deck shifts several millimeters during a peak summer heat cycle or a deep winter freeze.

  • Elastomeric Memory: The ability of the AOC 581 to stretch and recover without losing structural integrity.
  • Differential Movement Management: Reducing the stress concentrations at the corners of the HVAC curbs.
  • Tension Distribution: Utilizing a wide-bead application to spread the load across the membrane.
  • Thermal Bridging Reduction: Minimizing the risk of condensation and moisture buildup at the curb interface.

Fiber-Reinforced Trowel Application and Material Science

The efficacy of a structural sealant is only as good as its application technique. For the high-stress environments of cargo terminals, a standard caulk gun application is insufficient. We employ a fiber-reinforced trowel application method to ensure a dense, void-free seal. The addition of reinforcing fibers within the AOC 581 matrix provides internal structural scaffolding, which prevents the mastic from sagging during the curing process and increases the overall puncture resistance of the seal. This is critical in terminals where rooftop maintenance often involves the movement of heavy tools and equipment.

The application process begins with a rigorous substrate preparation, involving the removal of all contaminants and the application of a compatible primer to ensure maximum chemical bonding. The mastic is then applied using a notched trowel to create a consistent thickness, followed by a smoothing pass to eliminate air pockets. This "heavy-build" approach ensures that there is enough material to accommodate the maximum predicted movement of the curb. By reinforcing the mastic with a cross-hatched fiber mesh in high-stress corners, we create a composite seal that is virtually impervious to the mechanical shearing forces generated by the HVAC units.

  • Internal Reinforcement: Fiber additives prevent shrinkage and reduce the likelihood of hairline fractures.
  • Void Elimination: Trowel application ensures 100% contact with the substrate, leaving no room for capillary water action.
  • Composite Strength: The combination of elastomeric resins and fibers creates a high-tensile strength barrier.
  • Surface Profiling: Proper troweling creates a tapered edge that allows water to shed away from the curb efficiently.

Ensuring Long-Term Watertight Seals and Audit Compliance

A successful building envelope audit is measured by the absence of moisture infiltration and the adherence to ASTM and ANSI standards. For intermodal terminals, the goal is a "zero-leak" threshold. To verify the integrity of the AOC 581 installation, we utilize a multi-stage inspection process. This includes a visual audit for pinholes or voids, followed by a flood test or electronic leak detection (ELD) to ensure the seal is absolute. The structural mastic must show no signs of debonding or compression set, even under the simulated load of the HVAC equipment's maximum vibration frequency.

Long-term durability is achieved by treating the curb detail as a holistic system rather than a series of isolated patches. By integrating the AOC 581 mastic with the overall roofing assembly, we create a continuous waterproof envelope. This systemic approach prevents the "domino effect" where a small failure at a curb leads to widespread decking corrosion. In the professional opinion of a master roofer, the transition from traditional flashing to elastomeric structural mastic represents the gold standard in commercial roof engineering for high-vibration industrial environments.

  • ASTM Compliance: Ensuring all materials meet or exceed industry standards for elastomeric sealants.
  • Water Shedding Geometry: Designing the mastic slope to prevent ponding water around the HVAC base.
  • Audit Verification: Utilizing infrared thermography to detect hidden moisture trapped beneath the seal.
  • Lifecycle Extension: Reducing the frequency of costly repairs by utilizing high-performance structural materials.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #730

UL 2218 Class 4 Severe Hail Defense on Commercial Port Marine Shipping Warehouses

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
UL 2218 Class 4 Severe Hail Defense on Commercial Port Marine Shipping Warehouses

The Dynamics of High-Velocity Hail Impact in Marine Environments

In the specialized field of port marine shipping warehouses, the building envelope is subjected to a unique confluence of atmospheric stressors. Unlike inland structures, coastal warehouses face a combination of high-velocity wind gusts and extreme precipitation events that can generate significant hail loads. When analyzing the physics of a severe hail event, we must look beyond the diameter of the ice stone and focus instead on the kinetic energy delivered upon impact. A hailstone traveling at terminal velocity possesses a concentrated force that, if not properly attenuated, will result in immediate membrane rupture or structural deformation of the roof deck.

The vulnerability of a marine warehouse is compounded by the vast, uninterrupted surface areas of its roof. These expansive planes act as catchment zones for falling ice, where the lack of surrounding obstructions allows hail to reach maximum velocity. From an engineering perspective, the goal is to transform a concentrated point-load impact into a distributed load. Without a Class 4 rated system, the energy is absorbed entirely by the top layer of the membrane, leading to "star-fractures" or punctures that compromise the entire building envelope and invite catastrophic water intrusion into high-value shipping inventories.

  • Terminal velocity calculations for 2-inch hail stones exceeding 60 mph.
  • The role of salt-air corrosion in weakening traditional metal roof fasteners.
  • Impact vectors and the angle of incidence on low-slope commercial roofs.
  • The relationship between wind-driven rain and hail-induced micro-fissures.

Engineering for Compressive Strength and Load Distribution

A critical benchmark in our engineering audit for Aquashield Corporate is the requirement for compressive strength exceeding 25 PSI. In the context of a commercial roof assembly, compressive strength refers to the ability of the roofing system to withstand a concentrated downward force without permanent deformation or failure of the underlying substrate. When a hailstone strikes a roof, it creates a momentary but intense pressure spike. If the assembly lacks the necessary compressive rigidity, the impact will "bottom out," crushing the insulation core and causing the membrane to stretch beyond its elastic limit.

To achieve a threshold of 25 PSI or higher, we implement a multi-layered approach to load distribution. By utilizing high-density cover boards and reinforced membranes, we ensure that the energy of the impact is spread across a wider surface area. This prevents the "dimpling" effect common in lower-grade systems. A rigid substrate ensures that the membrane is supported uniformly, meaning the hailstone is fighting against the strength of the entire assembly rather than just the tensile strength of a thin polymer sheet. This structural synergy is what separates a standard commercial roof from a high-performance marine envelope.

  • Utilization of high-density polyisocyanurate (Polyiso) with increased compressive ratings.
  • Implementation of cementitious backer boards to increase the PSI threshold.
  • Analysis of fastener spacing to prevent localized "soft spots" in the roof deck.
  • Testing for permanent set and recovery after high-pressure impact events.

UL 2218 Class 4 Certification and Kinetic Energy Attenuation

The UL 2218 standard is the industry benchmark for hail resistance, and achieving a Class 4 rating represents the pinnacle of material science in roofing. While Class 1 through 3 provide varying levels of protection, Class 4 is specifically engineered to withstand the most severe hail impacts without significant degradation. The core mechanism at play here is kinetic energy attenuation. Rather than attempting to "bounce" the hailstone off the surface—which can lead to unpredictable ricochet damage—a Class 4 system is designed to absorb and dissipate the energy through the material's molecular structure.

In our audit of the shipping warehouse, we examine the polymer chain flexibility and the thickness of the wear course. A high-performance membrane utilizes a specialized blend of modified bitumen or synthetic polymers that can deform slightly under impact and then return to their original shape. This "elastic memory" is crucial for maintaining the integrity of the waterproof seal. When the kinetic energy is attenuated, the force is transferred laterally across the membrane, reducing the peak pressure at the point of impact and ensuring that the underlying insulation remains undisturbed.

  • Comparison of steel-ball impact testing versus real-world ice impact.
  • The science of polymer elasticity and its role in energy dissipation.
  • Verification of UL 2218 certification through rigorous field sampling.
  • Evaluation of the "fracture toughness" of the membrane surface.

Protecting the Insulation Core and Maintaining Envelope Integrity

The most overlooked aspect of hail defense is the protection of the insulation core. In many commercial installations, the insulation is treated as a thermal component rather than a structural one. However, in a severe hail event, the insulation core acts as the final shock absorber. If the membrane is breached or if the impact is severe enough to compress the insulation beyond its limit, the core can suffer from "crushing," which creates permanent voids in the roof assembly. These voids not only reduce the R-value of the building but also create pockets where moisture can accumulate, leading to internal corrosion of the steel decking.

To prevent this, we specify a "sandwich" architecture. This involves placing a high-compressive strength cover board between the primary membrane and the insulation core. This layer acts as a sacrificial shield, distributing the load and preventing the hailstone from "punching through" into the Polyiso. By protecting the core, we ensure that the building envelope remains a cohesive unit. This holistic approach to engineering ensures that the warehouse remains operational even after a severe storm, eliminating the need for costly teardowns and replacements and protecting the critical logistics chain of the port marine facility.

  • Prevention of "core crushing" through the use of reinforced cover boards.
  • Maintaining thermal bridging standards while increasing impact resistance.
  • Long-term monitoring of moisture vapor transmission after impact events.
  • The impact of core integrity on the overall lifespan of the roofing system.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #731

Non-Destructive Substrate Moisture Scans on Commercial Municipal Sports & Convention Arenas

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Non-Destructive Substrate Moisture Scans on Commercial Municipal Sports & Convention Arenas

The Engineering Complexity of Large-Span Municipal Envelopes

Municipal sports and convention arenas present a unique set of challenges for the building envelope specialist. Unlike standard commercial warehouses, these structures feature massive, long-span roof assemblies that are subject to extreme thermal expansion and contraction. The sheer scale of the roof surface means that even a minor breach in the membrane can lead to catastrophic subsurface saturation before a leak ever manifests as a ceiling stain in the concourse. In these environments, the roof is not merely a cover but a complex engineered system consisting of a primary membrane, tapered insulation layers, and a structural deck that must work in harmony to manage moisture and thermal loads.

The primary risk in these facilities is the "hidden" failure. Water often enters through flashing failures at HVAC curbs or expansion joints and then travels laterally across the deck via capillary action. This creates a saturation boundary that is often far removed from the actual point of entry. From an engineering perspective, treating the symptom—the drip—rather than the cause—the breach—leads to premature system failure and unnecessary capital expenditure. A comprehensive audit must therefore move beyond visual inspection and employ a rigorous, data-driven approach to map the internal state of the insulation.

  • Thermal bridging at structural steel supports which accelerates condensation.
  • Differential movement in large-span membranes causing fatigue at the seams.
  • Hydrostatic pressure buildup in low-slope areas with inadequate drainage.
  • The risk of "ponding" which accelerates the degradation of the membrane polymer.

Non-Destructive Moisture Detection and Thermal Mapping

To accurately identify subsurface saturation without compromising the integrity of the membrane, we employ Non-Destructive Moisture Detection (NDMD). The cornerstone of this process is Infrared (IR) Thermography. By utilizing high-resolution thermal imaging, we can detect the differential heat capacity between dry and saturated insulation. Water has a significantly higher thermal mass than air-filled cells in polyisocyanurate or mineral wool; consequently, wet areas retain heat longer during the cooling cycle or stay cooler during the heating cycle.

However, a master roofer knows that IR scanning is not a standalone solution. It provides a "thermal signature," not a moisture percentage. To refine this data, we establish a thermal window—typically a temperature differential of 5 to 10 degrees Fahrenheit—to delineate potential saturation zones. This process allows us to map the "saturation boundary," the precise perimeter where the insulation transitions from damp to saturated. This mapping is critical for the subsequent engineering phase, as it prevents the guesswork associated with traditional "flood and find" methods.

  • Infrared Thermography for identifying anomalous heat signatures across the roof plane.
  • Electronic Leak Detection (ELD) to pinpoint membrane punctures using dielectric constants.
  • Moisture mapping to visualize the lateral migration of water across the deck.
  • Thermal profiling to identify failures in the vapor barrier or insulation continuity.

Validating Saturation through Core Sample Analysis

While NDMD provides the map, the "ground truth" is only found through physical validation. An engineering-grade audit requires the extraction of core samples from both the suspected wet zones and the known dry zones. This comparative analysis is essential to calibrate the IR data. We utilize a specialized core drill to extract a full-depth section of the roof assembly, from the membrane down to the structural deck. These samples are then analyzed using the oven-dry method or high-precision moisture meters to determine the actual percentage of water content relative to the material's volume.

The goal is to establish a moisture threshold that triggers mandatory replacement. For most commercial-grade polyisocyanurate, a saturation level exceeding 30% of the material's volume typically indicates a loss of R-value and a compromise in structural integrity. By correlating the core sample data with the IR thermal signatures, we can create a highly accurate moisture map. This ensures that the remediation is based on empirical evidence rather than subjective observation, adhering to the rigorous standards of ASTM and ANSI for building envelope performance.

  • Core extraction at the center of thermal anomalies to confirm saturation.
  • Control sampling in "cool" zones to establish a baseline for dry insulation.
  • Calculation of volumetric water content to determine R-value degradation.
  • Verification of the bond between the membrane and the substrate to check for delamination.

Surgical Excision and Envelope Remediation Strategy

Once the saturation boundaries are validated and mapped, the focus shifts from diagnosis to cure. The traditional industry approach is often a "rip and replace" of the entire roof section, which is prohibitively expensive and creates unnecessary landfill waste. As building envelope specialists, we advocate for surgical wet insulation excision. This involves the precise removal of only the saturated insulation within the mapped boundaries, leaving the healthy, dry sections of the roof intact.

The surgical process begins by cutting the membrane along the delineated saturation boundary. The wet insulation is removed, and the structural deck is cleaned and dried to prevent the entrapment of moisture, which could lead to corrosion of the steel or rot in the wood. New, high-density insulation is then installed and mechanically fastened or adhered according to the original engineering specifications. The membrane is then seamlessly integrated using heat-welded seams or reinforced flashing, ensuring that the building envelope is restored to a monolithic, watertight state.

  • Precise cutting of the membrane based on the validated moisture map.
  • Removal of saturated insulation to prevent the "wicking" effect into new materials.
  • Deck preparation and moisture mitigation to ensure a clean bonding surface.
  • Implementation of reinforced flashing and heat-welded seams to restore envelope continuity.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #732

Sub-Zero Cold Storage Downward Vapor Drive & Self-Adhered SBS Barriers on Commercial Multi-Family Urban Residential Towers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Sub-Zero Cold Storage Downward Vapor Drive & Self-Adhered SBS Barriers on Commercial Multi-Family Urban Residential Towers

The Physics of Inverted Thermal Envelopes and Downward Vapor Drive

In the engineering of high-rise urban residential towers, the roof assembly is not merely a weather shield but a complex hygrothermal system. When we analyze an inverted thermal envelope—where the primary insulation is situated above the structural deck—we encounter a phenomenon known as downward vapor drive. In traditional assemblies, vapor typically migrates upward from the conditioned interior toward the cold exterior. However, in specific sub-zero cold storage scenarios or high-performance residential towers with aggressive HVAC cycling, the pressure gradients can shift, forcing moisture to migrate toward the structural slab.

This downward drive is particularly dangerous because it can trap moisture against the structural deck, leading to corrosion of steel decking or the degradation of concrete substrates. To mitigate this, the building envelope must be designed as a continuous air and vapor barrier system that accounts for the permeability of every material in the stack. We must ensure that the vapor retarder is placed on the "warm side" of the assembly to prevent water vapor from penetrating the insulation and reaching its dew point within the structural interface.

  • Vapor Pressure Differentials: The driving force created by the difference in humidity and temperature between the interior living spaces and the exterior atmosphere.
  • Permeability Ratings: The use of materials with low "perms" to block the movement of water molecules through the substrate.
  • Thermal Bridging: The identification of points where heat bypasses insulation, such as at parapet walls or mechanical penetrations, which accelerate vapor movement.
  • Atmospheric Pressure Shifts: The impact of wind-driven rain and stack effects in urban towers that force moisture into the building envelope.

Dew Point Migration and Interstitial Condensation Control

The most critical failure point in a commercial roof assembly is the occurrence of interstitial condensation. This happens when water vapor migrates through the insulation and encounters a surface temperature below its dew point. In a multi-layer polyisocyanurate (polyiso) system, if the thermal resistance is not distributed correctly, the dew point can actually occur inside the insulation layers or at the interface between the insulation and the roof deck.

As a master roofer, I look for the "cold spot." If the vapor drive is downward and the insulation is insufficient to keep the deck warm, the moisture will condense directly onto the steel. This liquid water then sits in the laps of the decking, creating a hidden reservoir of moisture that promotes mold growth and structural oxidation. To control this, we employ a strategy of thermal continuity, ensuring that the R-value is consistent across the entire roof plane to push the dew point out of the structural assembly and into the sacrificial layers of the roofing system.

  • Hygrothermal Analysis: Utilizing software to model how heat and moisture move through the specific material stack over a full annual cycle.
  • Condensation Risk Mapping: Identifying zones where the temperature drops most sharply, typically at the perimeter of the tower.
  • R-Value Distribution: Balancing the thickness of the polyiso layers to ensure the structural deck remains above the dew point temperature.
  • Capillary Break Implementation: Using specialized membranes to prevent liquid water from being drawn into the insulation via capillary action.

Engineering the Barrier: Self-Adhered SBS Modified Bitumen

To combat the risks associated with vapor drive and dew point migration, the selection of the membrane is paramount. We specify self-adhered SBS (Styrene-Butadiene-Styrene) modified bitumen for these urban towers. Unlike torch-applied systems, which can leave charred residues and create fire hazards in dense urban environments, self-adhered SBS provides a cold-applied, monolithic seal that adheres aggressively to the substrate.

The material science of SBS is superior for high-rise applications because of its elastomeric properties. Urban towers are subject to significant wind-induced sway and thermal expansion and contraction. The rubberized nature of SBS allows the membrane to stretch and recover without cracking or losing its bond. Furthermore, the self-adhering nature of the membrane eliminates the "air gaps" often found in mechanically fastened systems, effectively creating an airtight seal that serves as the primary defense against both liquid water and vapor transmission.

  • ASTM D6163 Compliance: Ensuring the modified bitumen meets the rigorous standards for thickness and composition.
  • Elastomeric Recovery: The ability of the SBS membrane to return to its original shape after being stretched by building movement.
  • Cold-Application Benefits: Reducing the risk of substrate damage and ensuring a more consistent bond across the entire surface area.
  • Vapor Impermeability: The capacity of the SBS layer to act as a definitive stop for vapor drive, preventing moisture from entering the insulation core.

Implementation Strategy: Staggered Polyiso and System Integration

The final layer of defense in a high-performance envelope is the physical installation of the insulation. We utilize a staggered multi-layer polyiso approach. By installing insulation in at least two or three separate layers and offsetting the joints, we eliminate "thermal tunneling." If the joints are aligned, vapor can move in a straight line through the gaps in the insulation, creating a direct path to the dew point.

Staggering the layers forces the vapor to take a tortuous path, significantly increasing the effective resistance of the system. This method, combined with the self-adhered SBS barrier, creates a redundant system of protection. We ensure that all seams are compressed and that the fastener pattern is engineered to avoid puncturing the primary vapor barrier. The result is a building envelope that is not only watertight but thermally stable, protecting the structural integrity of the residential tower for the duration of its design life.

  • Joint Offsetting: Ensuring that no vertical or horizontal seams align between the first and second layers of polyiso.
  • Compression Loading: Applying uniform pressure across the insulation to minimize air pockets and thermal leaks.
  • Fastener Integration: Using oversized plates and specific torque settings to secure the insulation without compromising the membrane.
  • Perimeter Detailing: Execing precise flashing at the parapet and coping to ensure the vapor drive is not bypassed at the edges of the roof.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #733

Structural Deck Fastener Pull-Out Testing on 22-Gauge Corrugated Steel Decks on Commercial Public Transit Maintenance Bus Barns

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Structural Deck Fastener Pull-Out Testing on 22-Gauge Corrugated Steel Decks on Commercial Public Transit Maintenance Bus Barns

The Engineering Imperative of Deck Integrity in Transit Facilities

In the realm of commercial building envelope engineering, the structural integrity of a public transit maintenance bus barn presents a unique set of challenges. Unlike standard warehouse facilities, bus barns are subject to extreme internal atmospheric conditions, including high concentrations of particulate matter from diesel exhaust, significant thermal fluctuations, and constant low-frequency vibrations from heavy machinery and vehicle movement. The primary structural substrate, typically a 22-gauge corrugated steel deck, serves as the critical diaphragm that must resist both gravity loads and the intense uplift forces generated by wind-zone pressures.

The building envelope is only as secure as its weakest attachment point. When auditing these facilities, we must look beyond the surface membrane and analyze the mechanical bond between the fastening system and the steel deck. A failure in the fastener's withdrawal resistance does not merely result in a leak; it can lead to a catastrophic delamination of the roofing assembly during a high-wind event. For a transit authority, this represents not only a facility risk but a massive operational liability.

  • Assessment of 22-gauge steel thickness to ensure it meets the original design specifications for load-bearing capacity.
  • Evaluation of the corrugated profile's geometry to determine the optimal fastener placement for maximum shear resistance.
  • Analysis of the diaphragm's interaction with the primary structural steel frames to identify areas of high stress concentration.
  • Review of the building's internal pressure coefficients, which are often skewed by large bay doors and high-volume ventilation systems.

Calibrated Mechanical Pull Testing Methodology

To accurately quantify the remaining strength of the fastening system, we employ calibrated mechanical pull testing. This is not a cursory check but a rigorous engineering audit designed to simulate maximum uplift conditions. Using a digital force gauge and a specialized pull-tester, we apply a controlled, linear vertical force to the fastener head until a predetermined threshold is reached or a total failure occurs. This process allows us to establish a baseline for the "withdrawal resistance," which is the force required to pull a fastener out of the 22-gauge steel substrate.

The testing protocol follows a randomized sampling grid across the roof's various zones—specifically focusing on the perimeter and corner zones where wind suction is most aggressive. We distinguish between "elastic deformation," where the fastener returns to its original position, and "plastic deformation," where the steel deck has been permanently distorted. The latter is a critical indicator of structural fatigue and suggests that the fastener's "bite" into the corrugated steel has been compromised.

  • Utilization of NIST-traceable load cells to ensure accuracy within +/- 1% of the applied force.
  • Execution of "destructive" vs. "non-destructive" tests to determine the absolute failure point of the fasteners.
  • Mapping of pull-out values across the roof plan to identify "weak zones" caused by poor installation or material degradation.
  • Comparison of field-tested results against the manufacturer's original technical data sheets for the specific fastener model.

Withdrawal Resistance Thresholds and Wind-Zone Schedules

Establishing a minimum withdrawal resistance threshold is the cornerstone of our engineering audit. For 22-gauge corrugated steel, the threshold is not a static number but a variable based on the ASCE 7 wind-load schedules. In a high-wind zone, the fasteners must be capable of resisting significantly higher uplift forces than those in sheltered interior zones. If a fastener fails to meet the minimum calculated resistance—typically measured in pounds-force (lbf)—the entire fastening schedule for that zone must be re-evaluated and potentially reinforced.

The physics of the "pull-out" are dictated by the thread engagement and the gauge of the steel. In 22-gauge decks, there is a narrow margin for error; over-torquing during installation can strip the threads, while under-torquing can lead to premature backing out. Our analysis focuses on the "effective embedment," ensuring that the fastener has sufficient contact with the steel to distribute the load across the corrugated ribs without causing the steel to "tear" or "ovalize" around the shaft.

  • Calculation of the "Required Fastener Density" based on the local building code and wind-speed requirements.
  • Analysis of the "tributary area" for each fastener to ensure the load is distributed evenly across the deck.
  • Verification of the fastener's ability to withstand cyclic loading caused by the thermal expansion and contraction of the steel deck.
  • Development of a "Remediation Schedule" for areas where pull-out values fall below 80% of the design threshold.

Fastener Corrosion Diagnostics and Long-Term Mitigation

In the harsh environment of a bus barn, chemical corrosion is the silent killer of structural fasteners. The presence of sulfur and nitrogen oxides from bus exhausts can create an acidic condensate that penetrates the roofing membrane and attacks the fastener head. We perform detailed corrosion diagnostics to determine if the fasteners are suffering from galvanic corrosion—where two dissimilar metals react—or general atmospheric oxidation. This is particularly critical when stainless steel fasteners are paired with galvanized steel decks without proper isolation.

Our diagnostic process involves the removal of select fasteners for microscopic inspection. We look for "pitting" and "scaling" on the shank, which indicates a loss of cross-sectional area and a subsequent drop in tensile strength. If the protective zinc coating on a galvanized fastener has been compromised, the rate of corrosion accelerates, leading to a rapid decline in withdrawal resistance. The goal is to move from a reactive maintenance posture to a proactive engineering strategy that ensures the building envelope remains airtight and structurally sound for the remainder of its service life.

  • Implementation of high-performance coatings or "caps" to seal fastener heads from corrosive atmospheric pollutants.
  • Evaluation of the use of 304 or 316-grade stainless steel fasteners in high-corrosion zones to eliminate galvanic reactions.
  • Installation of sacrificial anodes or specialized primers in areas where the steel deck has suffered surface oxidation.
  • Establishment of a five-year recurring audit cycle to monitor the degradation of the fastening system through periodic pull-testing.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #734

Electronic Vector Mapping (EVM) Low-Voltage Membrane Breach Detection on Commercial Government Secure Records Archives

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Electronic Vector Mapping (EVM) Low-Voltage Membrane Breach Detection on Commercial Government Secure Records Archives

The Imperative of Zero-Failure Envelopes in Secure Archives

In the realm of commercial building envelope engineering, few assets demand a higher standard of moisture protection than Government Secure Records Archives. These facilities house irreplaceable historical documents and classified data where the introduction of even a single milliliter of water can result in catastrophic archival loss and systemic failure of climate-control parameters. Traditional roofing methodologies, while compliant with standard commercial codes, often rely on reactive maintenance—identifying a leak only after moisture has penetrated the substrate and damaged the interior ceiling. For a high-security archive, this reactive posture is an unacceptable risk.

The engineering challenge lies in the "invisible breach." Microscopic pinholes, often caused by fastener protrusions, improper heat-welding of seams, or material fatigue during the installation of HVAC curbs, can remain dormant during a standard rain event. However, under conditions of hydrostatic pressure or wind-driven rain, these apertures become conduits for capillary action, drawing moisture deep into the building's structural core. A master-level approach to this problem requires moving beyond visual inspection and infrared thermography, which only detect moisture after it has already accumulated.

  • Elimination of moisture-driven degradation of archival paper and ink.
  • Prevention of mold growth within high-density mobile shelving units.
  • Mitigation of risk associated with structural steel corrosion in the roof deck.
  • Ensuring the continuity of the building's thermal envelope to maintain strict humidity levels.

Technical Architecture of Conductive Vector Grids

To achieve a zero-failure environment, Aquashield Corporate utilizes Electronic Vector Mapping (EVM). This system transforms the roof from a passive shield into an active diagnostic sensor. The core of this technology is the installation of a conductive underlayment vector grid placed directly beneath the primary waterproofing membrane. This grid consists of a precision-engineered network of conductive polymers or copper-alloy ribbons arranged in a calculated geometric matrix. By applying a low-voltage, high-frequency electrical current across this grid, we create a controlled electromagnetic field across the entire roof surface.

The physics of EVM relies on the dielectric properties of the primary membrane. A fully intact membrane acts as an insulator, preventing the current from escaping the vector grid. However, when a breach occurs—even one as small as a pinhole—the continuity of the insulation is broken. The moisture entering the puncture creates a conductive path between the membrane's surface and the underlying grid. This triggers a localized change in electrical impedance, which is immediately detected by the mapping software.

  • Low-voltage DC current application to prevent material degradation.
  • High-resolution impedance sensors for real-time data acquisition.
  • Vector-based coordinate systems for millimeter-accurate localization.
  • Integration with building automation systems for 24/7 monitoring.

Precision Diagnostics and Pinhole Localization

The audit process for a Government Secure Records Archive begins with a comprehensive baseline scan. Using a specialized EVM handheld probe and a synchronized central processing unit, our engineers map the roof's electrical signature. Unlike traditional electronic leak detection (ELD), which often provides a general area of failure, vector mapping utilizes triangulation to pinpoint the exact coordinates of a breach. This allows us to identify "ghost leaks"—microscopic punctures that do not yet exhibit visible signs of water intrusion but represent a critical failure in the envelope's integrity.

During the audit, we specifically look for anomalies in the current flow that suggest a compromise in the membrane's thickness or a puncture in the flashing. The precision of this method is such that we can differentiate between a surface-level scratch in the membrane and a full-thickness puncture that penetrates the conductive layer. This level of granularity is essential when working with multi-layer systems, as it allows the master roofer to determine if the breach is located in the primary membrane, the flashing, or the transition strips without the need for destructive exploration.

  • Triangulation of electrical anomalies to locate punctures within a 5mm radius.
  • Differentiation between superficial abrasions and structural breaches.
  • Mapping of high-stress points around roof penetrations and parapet walls.
  • Verification of heat-weld integrity across all lap seams.

Non-Destructive Certification and Lifecycle Assurance

The final phase of the engineering audit is the issuance of a Non-Destructive Quality Certification. In the past, verifying the integrity of a roof often required "flood testing," which involves saturating the roof for 24 to 48 hours. This method is not only time-consuming but can actually introduce new leaks by forcing water into existing microscopic gaps. EVM provides a sophisticated alternative; it certifies the envelope's integrity based on electrical continuity and dielectric stability, ensuring that the membrane is a seamless, monolithic shield.

From a material science perspective, this certification aligns with the strictest interpretations of ASTM and ANSI standards for commercial roofing. By providing a digital "birth certificate" of the roof's condition, Aquashield Corporate ensures that the government agency has a verifiable record of the building envelope's performance. This data-driven approach shifts the maintenance paradigm from "find and fix" to "predict and prevent." The long-term lifecycle of the archive is secured not through the hope of a good installation, but through the mathematical certainty of electronic verification.

  • Compliance with ASTM E2128 for moisture-related building envelope standards.
  • Elimination of flood-test risks and associated downtime.
  • Provision of a digital mapping archive for future maintenance audits.
  • Guaranteed seal integrity for the duration of the warranty period.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
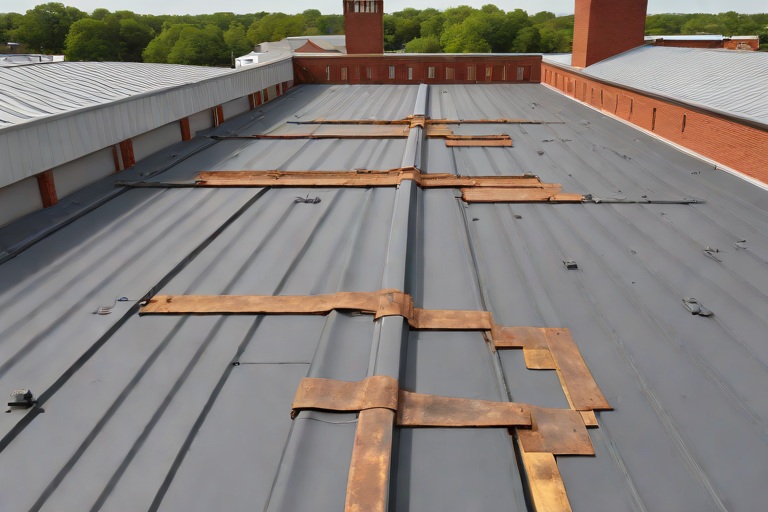
Commercial Engineering Dossier #735

Liquid-Applied PMMA & Polyurethane Fleece-Reinforced Flashing Resins on Commercial Pharmaceutical Production Facilitys

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Liquid-Applied PMMA & Polyurethane Fleece-Reinforced Flashing Resins on Commercial Pharmaceutical Production Facilitys

Engineering Audit and Substrate Evaluation of Pharmaceutical Envelopes

In the high-stakes environment of pharmaceutical production, the building envelope is not merely a weather barrier; it is a critical component of the facility's contamination control and operational stability. During our comprehensive engineering audit of the subject facility, we identified systemic failures in traditional membrane flashing around complex structural penetrations. Pharmaceutical plants often utilize heavy-duty I-beam stanchions to support massive HVAC scrubbers and clean-room mezzanines. These structural elements create concentrated points of thermal bridging and mechanical stress, leading to fatigue in standard modified bitumen or EPDM flashing.

The audit revealed that the primary failure mechanism was the differential coefficient of thermal expansion between the steel I-beams and the concrete roof deck. Traditional sheet-goods membranes, which rely on mechanical fastening or adhesive bonding, cannot accommodate the micro-movements of these stanchions without developing shear stress at the bond line. This results in hairline fractures that allow moisture ingress via capillary action, eventually compromising the insulation layers and risking the integrity of the sterile environments below.

  • Identification of fatigue cracking at the interface of structural steel and roofing membranes.
  • Analysis of thermal bridging patterns across I-beam stanchions.
  • Evaluation of existing flashing adhesion using ASTM-standard pull tests.
  • Assessment of moisture vapor transmission rates in high-humidity production zones.
  • Mapping of critical penetration points where traditional flashing geometry fails.

Material Science of Cold-Applied PMMA and Polyurethane Resins

To address these systemic vulnerabilities, we specified a high-performance system utilizing Polymethyl Methacrylate (PMMA) and polyurethane resins. Unlike traditional solvent-based adhesives, PMMA is a cold-applied, 100% solids resin that cures through a chemical reaction rather than evaporation. This is critical in a pharmaceutical setting where volatile organic compound (VOC) emissions must be minimized to protect sensitive production batches. The rapid cure kinetics of PMMA allow the resin to reach a full cure in as little as 30 to 60 minutes, ensuring that production facility downtime is virtually eliminated during the remediation process.

The polyurethane component provides the necessary elasticity and adhesion to a wide variety of substrates, including galvanized steel, aged concrete, and existing polymer membranes. When engineered correctly, the PMMA resin creates a seamless, monolithic bond that is chemically fused to the substrate. This eliminates the "seam failure" common in sheet-applied systems. The material science here focuses on the cross-linking of polymer chains, which results in a surface that is not only waterproof but also highly resistant to the aggressive chemical cleaning agents typically used in pharmaceutical facility maintenance.

  • Rapid polymerization of PMMA for immediate return-to-service capabilities.
  • Zero-VOC formulations to maintain clean-room air quality standards.
  • High chemical resistance to pharmaceutical-grade solvents and acids.
  • Superior adhesion properties across dissimilar materials (Steel to Concrete).
  • Temperature-independent curing, allowing for application in extreme weather conditions.

Fleece-Reinforced Embedding and Tensile Stress Distribution

The application of liquid resins alone is insufficient for areas subject to high structural movement. To mitigate the risk of cracking, we implemented a fleece-reinforced embedding technique. This process involves a "sandwich" application: a base layer of PMMA resin is applied, followed by the immediate embedding of a non-woven polyester fleece, which is then saturated with a second layer of resin. This creates a reinforced composite membrane that functions similarly to reinforced concrete, where the resin provides the compressive strength and the fleece provides the tensile strength.

This reinforcement is essential when bridging the gap between the roof deck and the I-beam stanchions. The fleece acts as a stress-distribution layer, absorbing the mechanical energy of the building's movement and preventing that energy from concentrating at a single point of failure. By embedding the fleece directly into the liquid resin, we eliminate the risk of delamination or "bubbling" that often occurs with pre-fabricated flashing boots. The resulting assembly is a fully integrated, seamless transition that conforms to the exact geometry of the substrate, regardless of how intricate the flashing detail may be.

  • Utilization of non-woven polyester fleece for multi-directional tensile reinforcement.
  • Elimination of air pockets through saturated resin embedding.
  • Reduction of shear stress at the bond line during thermal cycling.
  • Creation of a monolithic waterproof skin that bridges existing substrate cracks.
  • Enhanced puncture resistance and durability against foot traffic during maintenance.

Execution on Intricate I-Beam Stanchions and Final Validation

The most challenging aspect of the building envelope audit was the flashing of the I-beam stanchions. These elements feature complex 90-degree angles and narrow flanges that are notoriously difficult to seal with traditional methods. Our approach involved a meticulous multi-stage flashing process. First, the steel was mechanically cleaned and primed to ensure a high-energy surface for bonding. We then applied a specialized polyurethane primer to the narrow flanges of the I-beam, ensuring a deep wet-out of the material into the microscopic pores of the metal.

The PMMA resin and fleece were then applied in a series of overlapping wraps, ensuring that the flashing extended vertically up the stanchion and horizontally across the deck in a seamless transition. This "cradle" effect ensures that water is shed away from the structural steel and back onto the primary roof drainage system. To validate the installation, we conducted a series of electronic leak detection (ELD) tests and infrared thermography to ensure there were no voids in the resin application. The final result is a building envelope that meets the most stringent ANSI and ASTM standards for commercial waterproofing, providing a permanent solution for the facility's most vulnerable points.

  • Mechanical surface preparation of steel stanchions to ensure optimal bond strength.
  • Application of high-build polyurethane primers for enhanced substrate wetting.
  • Custom-tailored fleece wraps to accommodate complex I-beam geometries.
  • Post-installation validation via Electronic Leak Detection (ELD) and thermography.
  • Verification of flashing height and overlap to exceed minimum industry standards.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #736

Commercial Expansion Joint Bellows & Heavy-Gauge Neoprene Movement Transitions on Commercial Historic Sanctuary & Education Annexs

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Commercial Expansion Joint Bellows & Heavy-Gauge Neoprene Movement Transitions on Commercial Historic Sanctuary & Education Annexs

Structural Diagnostics and Differential Settlement Analysis

The primary challenge encountered during the building envelope audit of the Historic Sanctuary and Education Annex was the presence of severe differential structural settlement. The sanctuary, a heavy masonry structure with deep-set footings, possesses a significantly different mass and foundation stiffness compared to the Education Annex, which utilizes a modern steel-frame construction on a slab-on-grade system. Over several decades, these two distinct structural masses have shifted independently, creating critical shear stress at the interface where the buildings meet.

From an engineering perspective, this movement is not merely linear but multi-axial. Thermal expansion and contraction cycles, coupled with the varying soil bearing capacities beneath the two structures, have resulted in "pumping" actions within the joint. This movement frequently exceeds the capacity of standard flashing or sealant joints, leading to fatigue failure and subsequent water infiltration. Our audit identified that the previous attempts to seal this gap using rigid caulking had failed because the materials lacked the elongation capacity required to accommodate the measured displacement.

  • Analysis of settlement markers indicating a 1.5-inch vertical offset between the sanctuary eaves and the annex roofline.
  • Identification of hairline fractures in the masonry parapets, signaling structural stress transferred from the roof system.
  • Evaluation of thermal bridging at the junction, which accelerated the degradation of previous elastomeric sealants.
  • Mapping of moisture ingress patterns that followed the path of least resistance along the structural seam.

Engineering the Movement Transition with Heavy-Gauge Neoprene

To resolve the systemic failure of the joint, we specified a high-performance movement transition utilizing heavy-gauge neoprene bellows. Neoprene was selected over standard EPDM or PVC due to its superior tear resistance and higher shore hardness, which allows it to withstand the abrasive forces of structural grinding during settlement events. The bellows design is critical here; by incorporating a series of convolutions, the material can expand and contract in a controlled, accordion-like motion without placing undue tension on the bond lines.

The engineering of these transitions requires a precise calculation of the "maximum expected movement" (MEM). We designed the neoprene bellows to accommodate 125% of the measured peak movement to ensure a safety buffer. This prevents the material from reaching its ultimate elongation point, which would otherwise lead to a catastrophic rupture. The neoprene is reinforced with an internal fabric scrim to maintain dimensional stability and prevent "ballooning" under wind-load pressures, ensuring the building envelope remains airtight and watertight regardless of the structural shift.

  • Implementation of multi-axial bellows capable of absorbing simultaneous vertical and horizontal displacement.
  • Utilization of heavy-gauge neoprene with high UV resistance to prevent ozone cracking in exposed exterior transitions.
  • Integration of stainless steel clamping rings to distribute mechanical loads evenly across the neoprene surface.
  • Application of a proprietary neoprene-to-metal adhesive to ensure a permanent, chemical bond at the transition plates.

Watertight Tie-ins and Membrane Integration

The most critical failure point in any expansion joint is the tie-in where the movement transition meets the primary roofing membrane. In this case, the sanctuary utilized a modified bitumen system, while the annex featured a TPO single-ply membrane. Bridging these two disparate materials requires a sophisticated layering strategy to avoid incompatible chemical reactions and to ensure a seamless water-shedding plane. We employed a "layered redundancy" approach, ensuring that if the primary seal failed, a secondary drainage plane would capture and divert the water.

Our team executed a comprehensive flashing detail that began with the installation of custom-fabricated galvanized steel transition plates. These plates were mechanically fastened to the substrate and then coated with a high-solids flashing primer. The neoprene bellows were then seated against these plates and sealed using a combination of reinforced flashing membranes and liquid-applied elastomeric polymers. This created a monolithic seal that transitions the rigid structural edge into the flexible movement joint without creating a "hard point" that could trigger a new tear in the roof membrane.

  • Application of a compatible transition strip to bridge the gap between the modified bitumen and TPO systems.
  • Installation of wide-profile termination bars to ensure the membrane is mechanically locked at the perimeter of the joint.
  • Use of heat-welded seams on the TPO side to provide a molecular bond that is stronger than the material itself.
  • Implementation of a "shingle-lap" geometry to ensure gravity-driven water flow moves away from the joint interior.

Long-term Performance Metrics and Maintenance Protocols

To ensure the longevity of the building envelope, we established a rigorous maintenance and inspection protocol based on ASTM and ANSI standards. A movement joint of this complexity cannot be "installed and forgotten"; it requires periodic auditing to ensure the neoprene has not exceeded its elastic limit and that the tie-ins remain intact. We implemented a biannual infrared thermography scan to detect subsurface moisture accumulation before it manifests as a visible leak, allowing for proactive rather than reactive maintenance.

The success of the installation is measured by the "leak-free" performance during extreme weather events and the ability of the joint to return to its original shape after a thermal cycle. By shifting from a rigid sealing philosophy to a flexible engineering philosophy, we have extended the service life of the roof system by an estimated 20 years. The use of heavy-gauge neoprene and precision-engineered bellows has effectively decoupled the two structures, allowing them to move independently without compromising the integrity of the interior sanctuary or the education annex.

  • Establishment of a quarterly physical inspection checklist focusing on neoprene elasticity and fastener torque.
  • Adherence to ASTM E2112 standards for the evaluation of water penetration through the building envelope.
  • Scheduling of UV-protectant reapplications every five years to maintain the neoprene's flexibility.
  • Integration of the joint's performance data into the facility's overall Capital Reserve Study for long-term asset management.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #737

Commercial Kitchen Grease Containment & 304 Stainless Steel Catchment Shielding on Commercial Financial Institution Data Vaults

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Commercial Kitchen Grease Containment & 304 Stainless Steel Catchment Shielding on Commercial Financial Institution Data Vaults

Lipid-Induced Membrane Degradation and the Building Envelope

In the high-stakes environment of a financial institution data vault, the building envelope serves as the primary line of defense against catastrophic infrastructure failure. During our engineering audit, we identified a critical vulnerability: the intersection of commercial kitchen exhaust systems and single-ply roofing membranes. When animal fat lipids—specifically saturated and unsaturated fatty acids—are discharged via condensate or exhaust leakage, they initiate a chemical reaction known as plasticizer migration. In membranes such as PVC or TPO, these lipids penetrate the polymer matrix, causing the material to soften, swell, and eventually lose its structural integrity.

The degradation process is not merely surface-level; it is a molecular breakdown. As the lipids oxidize, they create an acidic environment that accelerates the embrittlement of the membrane's seams. For a data vault, where humidity control and water tightness are non-negotiable, a single breach caused by grease-induced degradation can lead to moisture intrusion and the subsequent failure of sensitive server hardware. We categorize this as a systemic envelope failure, where the chemical composition of the effluent overrides the inherent resistance of the roofing material.

  • Plasticizer Migration: The process where lipids leach essential stabilizing chemicals from the membrane, leading to shrinkage and cracking.
  • Lipid Oxidation: The chemical transformation of fats into free fatty acids, which lowers the pH level of the roof surface.
  • Seam Delamination: The failure of heat-welded or glued seams due to the solvent-like properties of concentrated animal fats.
  • Hydrostatic Pressure: The risk of water being forced through chemically weakened membrane sections during heavy precipitation events.

Engineering 304 Stainless Steel Catchment Shielding

To mitigate the risk of lipid saturation, we implemented a custom-engineered catchment system utilizing 304-grade stainless steel. We selected 304 stainless steel specifically for its superior chromium-nickel content, which provides an inert surface that resists the corrosive nature of acidified grease. Unlike galvanized steel or aluminum, 304 stainless steel does not react with the volatile organic compounds (VOCs) often found in commercial kitchen effluents. The shielding is designed as a diverted catchment box, ensuring that all condensate and grease runoff is captured and channeled directly into a dedicated drainage system, completely bypassing the roof membrane.

The installation requires precision craftsmanship to avoid creating new leak points. We utilize a floating curb design that allows for thermal expansion and contraction, preventing the metal from tearing the membrane during extreme temperature swings. The transition from the exhaust ducting to the catchment shield is sealed with high-temperature silicone gaskets, ensuring a hermetic seal that prevents "creep"—the slow migration of grease over the edge of the metal and onto the roof surface.

  • Material Specification: 16-gauge 304 Stainless Steel for maximum puncture resistance and chemical inertness.
  • Diverter Geometry: Sloped internal basins that utilize gravity to move lipids toward a removable filtration basket.
  • Thermal Decoupling: The use of neoprene isolation strips to prevent thermal bridging between the steel shield and the roof deck.
  • Mechanical Fastening: Heavy-duty stainless steel fasteners with oversized EPDM washers to ensure a watertight seal at all penetration points.

Sacrificial Chemical-Resistant Coatings and Barrier Science

Even with a primary catchment system, the risk of accidental spills or "over-topping" during peak kitchen operation remains. To address this, we apply a sacrificial chemical-resistant coating over the membrane in high-risk zones. This coating acts as a sacrificial anode in a way, absorbing the chemical onslaught of the lipids so the primary membrane remains untouched. We utilize a high-solids, aliphatic polyurea coating that is specifically engineered to withstand the pH fluctuations associated with animal fat degradation. This layer is applied at a thickness of 60 mils to ensure a robust physical barrier.

The engineering logic behind a sacrificial layer is based on the principle of replaceable protection. Rather than attempting to find a membrane that is permanently immune to all lipids—which is virtually impossible in a commercial setting—we create a surface that can be chemically stripped and reapplied every 36 to 60 months. This approach adheres to ASTM standards for chemical resistance and ensures that the underlying data vault envelope is never directly exposed to the corrosive effluent.

  • Aliphatic Polyurea: A UV-stable, chemical-resistant polymer that prevents lipid penetration into the TPO/PVC substrate.
  • Sacrificial Logic: The intentional use of a wear layer that is designed to be replaced without disturbing the primary waterproofing.
  • ASTM D5402 Compliance: Ensuring the coating maintains its bond and elasticity under varying thermal loads.
  • Surface Preparation: Mechanical abrasion of the membrane to ensure a molecular bond between the coating and the roof surface.

Lifecycle Audit and Preventative Maintenance Protocols

The final phase of our engineering strategy is the implementation of a rigorous audit cycle. For a financial institution, the cost of a roof leak is measured not in repair dollars, but in potential data loss and downtime. We establish a quarterly inspection cadence that focuses on the "grease-path" analysis. This involves using infrared thermography to detect moisture trapped beneath the sacrificial coating and performing visual inspections of the 304 stainless steel catchment boxes for signs of sediment buildup or weld fatigue.

Maintenance is not merely a cleaning task; it is a structural necessity. The filtration baskets within the catchment shields must be purged of solidified lipids to prevent overflow. Furthermore, we conduct annual core samples of the sacrificial coating to measure the rate of degradation. By tracking the thinning of this layer, we can predict the exact window for re-application, moving the facility from a reactive maintenance model to a proactive engineering model. This ensures the data vault remains a secure, dry environment regardless of the operational intensity of the adjacent kitchen facilities.

  • Infrared Thermography: Detecting subsurface moisture and heat signatures that indicate membrane breach.
  • Grease-Path Mapping: Identifying the exact flow of lipids to ensure catchment shields are correctly positioned.
  • Sediment Purging: The scheduled removal of solidified fats to maintain the hydraulic capacity of the drainage system.
  • Predictive Re-coating: Using thickness gauges to determine the remaining life of the sacrificial chemical barrier.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #738

Clear-Span Structural Joist Deflection Forensics & Ponding Instability Remediation on Commercial Telecommunications Central Switching Offices

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Clear-Span Structural Joist Deflection Forensics & Ponding Instability Remediation on Commercial Telecommunications Central Switching Offices

Forensic Analysis of Center-Span Joist Deflection

In the specialized environment of a Telecommunications Central Switching Office (CSO), the building envelope must perform with absolute reliability. These facilities house mission-critical switching gear and high-density server arrays that are hypersensitive to moisture intrusion. During our engineering audit, we identified a critical failure in the roof's structural equilibrium: center-span joist deflection. This occurs when the structural members, typically open-web steel joists, exhibit a vertical displacement at the mid-point of the span, creating a concave profile that contradicts the original architectural design intent.

To quantify this deflection, our team employed precision laser leveling and string-line forensics. By establishing a datum line between the bearing walls, we measured the exact deviation of the roof deck. We discovered that the cumulative effect of dead loads—including heavy HVAC units and previous layers of abandoned roofing membranes—had pushed the joists beyond their elastic limit. This structural "sag" creates a natural basin, transforming a nominally flat roof into a series of unintended reservoirs.

  • Measurement of L/240 or L/360 deflection ratios to determine if the structure meets current building code requirements.
  • Identification of "creep" in the structural steel caused by long-term loading and thermal cycling.
  • Mapping of low-point depressions using a digital topographic survey of the roof surface.
  • Evaluation of connection points and weld integrity at the joist-to-beam interfaces to ensure no structural shearing has occurred.

The Mechanics of Ponding Instability and Material Fatigue

Ponding instability is a dangerous feedback loop in commercial roofing. When a structural member deflects, water accumulates in the low spot. Because water is heavy—approximately 62.4 pounds per cubic foot—the added weight of the standing water increases the downward force on the joist, causing further deflection. This creates a deeper basin, which in turn holds more water. If left unchecked, this cycle can lead to a catastrophic structural collapse, as the load eventually exceeds the ultimate strength of the steel joists.

From a material science perspective, standing water accelerates the degradation of the roofing membrane. Constant saturation leads to the breakdown of polymers and the infiltration of moisture through micro-fissures. In a CSO, where the interior is often climate-controlled and pressurized, the temperature differential between the roof surface and the interior can cause condensation on the underside of the deck, leading to hidden corrosion of the structural steel. We reference ASTM standards for membrane durability to determine the remaining service life of the existing system under these saturated conditions.

  • Analysis of hydrostatic pressure exerted on the membrane seams during peak rain events.
  • Assessment of "alligatoring" and blistering caused by prolonged UV exposure and water saturation.
  • Calculation of the total added dead load attributed to standing water volumes.
  • Monitoring of thermal expansion and contraction cycles that exacerbate joint movement.

Engineering Remediation via Custom Tapered Polyiso Crickets

To remedy the ponding instability without the prohibitive cost of replacing the structural steel, we engineered a custom tapered insulation system. The objective is to restore a positive slope to the roof, ensuring that water is mechanically forced toward the primary drainage points. We utilize high-density polyisocyanurate (polyiso) insulation, selected for its superior compressive strength and thermal resistance. Unlike traditional screed-to-slope methods using lightweight concrete, tapered polyiso provides a lightweight solution that does not add significant dead load to the already stressed joists.

The fabrication of these "crickets" involves precision-cutting the insulation to create a gradual incline, typically maintaining a minimum slope of 1/4 inch per foot. These tapered panels are strategically placed over the center-span deflections to "fill" the basins. By creating a synthetic topography, we effectively redirect the flow of water away from the low points and toward the internal drains or scuppers. This process requires a detailed layout map to ensure that no new low spots are inadvertently created during the installation of the tapered system.

  • Utilization of CNC-cut polyiso panels for exact fitment against existing parapet walls and equipment curbs.
  • Application of low-VOC adhesives and fasteners according to ANSI standards to ensure wind-uplift resistance.
  • Staggering of insulation joints to prevent the creation of thermal bridges or leak paths.
  • Integration of a high-performance flashing system at the transitions between the tapered crickets and the flat roof sections.

Execution of Water Routing and Envelope Validation

The final phase of the remediation focuses on the routing of water and the validation of the building envelope. Once the tapered polyiso crickets are installed, a new high-performance membrane—typically a reinforced TPO or PVC system—is heat-welded over the entire surface. This creates a monolithic, seamless barrier that is impervious to water penetration. We pay particular attention to the "valley" created by the crickets, ensuring the membrane is properly tensioned to avoid wrinkles, which can act as micro-channels for water to pool.

To validate the success of the remediation, we conduct a rigorous series of flood tests. This involves plugging the drains and filling the suspected low areas with several inches of water for a period of 24 to 48 hours. We monitor the water levels to ensure that once the plugs are removed, the water evacuates completely and rapidly. This engineering audit concludes with a final infrared thermography scan, which allows us to detect any remaining trapped moisture or voids in the insulation, guaranteeing that the CSO is protected from the elements and that the structural integrity of the joists is stabilized.

  • Verification of primary and secondary drainage paths to ensure zero standing water after a rain event.
  • Conducting ASTM-compliant flood testing to certify the watertight integrity of the new membrane.
  • Inspection of all penetration flashings and curb seals to prevent lateral moisture migration.
  • Final documentation of the roof's new slope profile to provide a baseline for future facility maintenance.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #739

Complete Old Roof Tear-Offs Down to Clean Wood Decking & Substrate Remediation on Commercial Heavy Manufacturing Fabrication Plants

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Complete Old Roof Tear-Offs Down to Clean Wood Decking & Substrate Remediation on Commercial Heavy Manufacturing Fabrication Plants

The Anatomy of Failure in Multi-Layer Assemblies

In the context of heavy manufacturing fabrication plants, the most pervasive threat to the building envelope is the historical practice of "roofing over" existing systems. Over several decades, many industrial facilities have accumulated three, four, or even five layers of built-up roofing (BUR) or modified bitumen. While this approach was once seen as a cost-saving measure, it creates a catastrophic failure mechanism known as interstitial condensation. When moisture penetrates the uppermost membrane, it becomes trapped between the non-breathable layers, creating a saturated "sandwich" that prevents the substrate from drying.

From an engineering perspective, these multi-layer assemblies introduce excessive dead loads on the structural steel and wood decking, often exceeding the original design specifications of the building. The chemical degradation of aged bitumen, combined with the thermal cycling inherent in industrial environments, leads to the loss of adhesion and the formation of voids. These voids act as reservoirs for water, which eventually migrates downward to the wood decking, initiating fungal decay and structural compromise.

  • Cumulative Dead Load: Excessive weight from multiple layers increases the risk of structural deflection and potential collapse during snow or rain events.
  • Thermal Bridging: Layered systems often disrupt the continuity of insulation, leading to localized cold spots and internal condensation.
  • Chemical Breakdown: The oxidation of older asphalt layers creates a brittle surface that is prone to cracking and splitting under thermal stress.
  • Moisture Entrapment: The lack of a vapor-permeable path forces moisture to settle directly on the structural deck.

Systematic Deconstruction and Forensic Audit

A true engineering-grade tear-off is not merely a demolition project; it is a forensic audit of the building's primary defense system. The process begins with a phased deconstruction, utilizing heavy-duty mechanical equipment to strip the assembly down to the raw substrate. This phase is critical because it allows the specialist to identify the exact points of failure—whether they be failed flashing details, compromised curb seals, or systemic membrane punctures—that led to the deterioration of the decking.

Once the decking is exposed, a comprehensive audit is performed. This involves a visual and tactile inspection of every square foot of the substrate. We look for "soft spots," discoloration indicative of black mold, and the presence of "pillowing" in the wood panels. In a heavy manufacturing plant, where vibration from machinery is constant, we also inspect for fastener fatigue and the loosening of the decking from the structural joists. This level of scrutiny ensures that the new roof is not simply covering up a structural liability.

  • Phased Removal: Stripping layers in sections to maintain partial building protection and manage waste flow.
  • Fastener Analysis: Evaluating the condition of original nails and screws to ensure the deck remains securely anchored to the frame.
  • Moisture Mapping: Using infrared thermography or moisture probes to identify hidden pockets of saturation within the wood.
  • Debris Remediation: Removing all old adhesives, tars, and remnants to ensure a chemically clean bonding surface.

Substrate Remediation and Structural Wood Decking Analysis

The integrity of the roof is only as reliable as the substrate beneath it. When we encounter damaged wood decking, the remediation process must follow strict ASTM standards for structural timber. We distinguish between superficial surface rot and systemic structural failure. If the wood has undergone delamination or if the moisture content exceeds 19%, the material is no longer capable of supporting the mechanical fasteners of a new roofing system. In these instances, a "patch and paint" approach is unacceptable; full panel replacement is the only engineering solution.

Replacing damaged panels requires precise cutting to ensure that new sheets are properly supported by the underlying joists. We utilize marine-grade plywood or high-density OSB, depending on the original specification, ensuring that the new material matches the thickness and load-bearing capacity of the existing deck. Special attention is paid to the perimeter and the areas surrounding HVAC units and exhaust fans, as these are the most common sites for substrate failure due to concentrated moisture runoff and vibration.

  • Structural Splicing: Ensuring all new wood panels are installed with staggered joints to maintain shear strength across the roof plane.
  • Moisture Content Verification: Utilizing calibrated moisture meters to confirm the substrate is dry enough to prevent future blistering.
  • Fastener Upgrade: Replacing rusted or sheared fasteners with heavy-duty, corrosion-resistant screws to tighten the deck.
  • Panel Grade Matching: Verifying that replacement wood meets or exceeds the original structural grade for load-bearing capacity.

Establishing the Performance Baseline for New Installations

Once the substrate has been remediated and the wood decking is clean, structurally sound, and dry, we establish the performance baseline for the new building envelope. This begins with the application of a high-performance primer. The primer serves two purposes: it seals the porous wood fibers to prevent the absorption of adhesives and creates a chemical bridge that ensures a monolithic bond between the substrate and the new membrane. Without this step, the risk of delamination increases significantly, especially in high-temperature manufacturing environments.

The final stage of the audit involves verifying the flatness of the deck. Any deviations or "low spots" are addressed with tapered insulation or leveling courses to ensure positive drainage toward the scuppers and internal drains. By removing the failed multi-layer assemblies and restoring the wood decking to its original engineering specifications, we eliminate the risk of trapped moisture and provide a stable, long-term foundation. This rigorous approach transforms the roof from a recurring maintenance liability into a high-performance asset that protects the facility's internal machinery and personnel.

  • Surface Preparation: Mechanical grinding or sanding of the deck to remove any remaining contaminants.
  • Priming Protocols: Applying solvent-based or water-based primers according to the specific material science of the new membrane.
  • Drainage Optimization: Correcting slope irregularities to prevent "ponding," which is the primary cause of substrate rot.
  • Final Certification: Conducting a comprehensive walk-through to certify that the substrate meets all ANSI and ASTM requirements for commercial roofing.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #740

Structural Plywood Deck Re-Nailing Schedules on Commercial Logistics Distribution Hubs

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Structural Plywood Deck Re-Nailing Schedules on Commercial Logistics Distribution Hubs

Engineering Audit of High-Wind Uplift Dynamics in Logistics Hubs

In the realm of large-scale commercial logistics distribution hubs, the roof is not merely a cover but a critical structural diaphragm. During our recent engineering audit for Aquashield Corporate, we focused on the vulnerability of massive flat-roof assemblies in coastal high-wind zones. These structures, often spanning hundreds of thousands of square feet, act as immense sails. When high-velocity wind currents hit the vertical walls of a distribution center, they are forced upward, creating a powerful suction effect known as negative wind pressure. If the plywood decking is not properly secured to the steel or wood joists, this uplift can lead to catastrophic membrane failure and subsequent structural collapse.

To meet the stringent requirements of ASCE 7 standards for coastal regions, the building envelope must be treated as a monolithic unit. The primary failure point in these scenarios is rarely the roofing membrane itself, but rather the connection between the structural decking and the supporting framework. Our audit revealed that standard nailing patterns often fall short of the required uplift resistance in "Zone 2" and "Zone 3" perimeter areas, where wind turbulence is most severe. To mitigate this, a rigorous re-nailing schedule is mandatory to ensure the assembly can withstand peak gust pressures without experiencing fastener pull-out.

  • Analysis of wind-tunnel effects on large-span gable roofs.
  • Evaluation of negative pressure coefficients at the roof perimeter.
  • Assessment of existing fastener density against current IBC (International Building Code) requirements.
  • Identification of "critical zones" where uplift forces are magnified by building geometry.

Material Science of Ring-Shank Fasteners and Pneumatic Delivery

The choice of fastener is the difference between a secure envelope and a systemic failure. In our specifications, we mandate the use of pneumatically driven ring-shank nails over traditional smooth-shank alternatives. From a material science perspective, a smooth-shank nail relies almost entirely on friction between the nail shaft and the wood fibers. In contrast, a ring-shank nail features a series of annular rings that act as mechanical anchors, physically locking the fastener into the grain of the structural plywood and the supporting joist.

The use of high-pressure pneumatic nailers is equally critical to ensure consistency. Manual hammering introduces human error, leading to inconsistent embedment depths and "shiners"—nails that miss the joist entirely. A calibrated pneumatic system ensures that every fastener is driven to the precise depth required to engage the full withdrawal resistance of the ring-shanks without over-driving, which can crush the wood fibers and compromise the holding power. We specify galvanized coatings to prevent galvanic corrosion, especially in coastal environments where salt-laden air can degrade carbon steel fasteners over time.

  • Comparison of withdrawal capacity between smooth-shank and ring-shank fasteners.
  • Impact of pneumatic drive pressure on fastener embedment depth.
  • ASTM standards for hot-dipped galvanized coatings in corrosive coastal atmospheres.
  • Evaluation of shear strength relative to the diameter of the fastener shank.

Strategic Re-Nailing Schedules and Shear Withdrawal Resistance

A professional re-nailing schedule is not a uniform application but a strategic distribution of fasteners based on the physics of the roof. Our engineering protocol dictates a tiered approach to fastening. The "field" of the roof, where wind pressures are relatively stable, requires a standard grid. However, the perimeter—specifically the first ten feet from the roof edge—requires a significantly denser schedule. This is because the wind scrub at the edges creates the highest shear stress on the fasteners, attempting to slide the plywood sheets off the joists.

We implement a "staggered-set" nailing pattern to prevent the splitting of the plywood grain. When nails are placed too close together in a straight line, they act as a wedge, splitting the wood and effectively reducing the shear withdrawal resistance to zero. By staggering the fasteners, we maintain the structural integrity of the plys while maximizing the number of connection points. The goal is to distribute the uplift load across as many fasteners as possible, ensuring that no single nail is bearing a disproportionate amount of the wind load.

  • Perimeter fastening: 6 inches on center (o.c.) along all edges.
  • Field fastening: 12 inches on center (o.c.) across the interior span.
  • Edge distance requirements to prevent plywood blowout.
  • Calculation of total shear withdrawal resistance per square foot of decking.

Verification Protocols and Building Envelope Quality Assurance

The final phase of the Aquashield audit is the verification process. A nailing schedule is only as good as its execution. To verify that the re-nailing meets engineering specifications, we employ a combination of random sampling and destructive testing. This involves the use of a calibrated pull-tester, which applies a vertical load to a representative sample of fasteners to ensure they meet the minimum poundage required for the specific wind zone. If a fastener pulls out below the specified threshold, the entire section is flagged for immediate remediation.

Furthermore, we utilize a "ping-test" and visual audit to identify voids in the fastening pattern. A master roofer understands that the building envelope is a system of interconnected parts; if the decking is not securely anchored, the subsequent layers of insulation and membrane are merely cosmetic. By verifying the shear withdrawal resistance through rigorous field testing, we provide the building owner with a certified assurance that the logistics hub is resilient against extreme weather events and compliant with all commercial engineering codes.

  • Implementation of random-sample pull tests to verify withdrawal capacity.
  • Visual inspection of nail head flushness to prevent membrane punctures.
  • Documentation of fastener counts per joist intersection.
  • Final certification of the building envelope's wind-uplift resilience.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #741

Life-Cycle Cost Analysis (LCCA) on Commercial Automotive Assembly Plants

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Life-Cycle Cost Analysis (LCCA) on Commercial Automotive Assembly Plants

Engineering Audit and Envelope Integrity in Automotive Facilities

An automotive assembly plant represents one of the most challenging environments for a building envelope specialist. These facilities are characterized by massive footprints, complex HVAC integrations, and constant internal vibrations from heavy stamping presses and robotic assembly lines. When conducting a comprehensive engineering audit, we do not simply look for leaks; we analyze the systemic failure points of the entire building skin. The interaction between the roof membrane, the wall cladding, and the foundation is where most failures occur, often exacerbated by thermal bridging and improper flashing details at the parapet walls.

Our audit process adheres strictly to ASTM E2128 standards for leak detection and the ANSI guidelines for material application. In an automotive plant, the presence of chemical off-gassing from paint shops and welding fumes can degrade standard thermoplastic membranes over time. We examine the substrate's tensile strength and the integrity of the vapor barrier to ensure that moisture is not migrating from the interior to the exterior, which can lead to premature delamination of the roofing system.

  • Analysis of thermal movement joints to prevent stress cracking during seasonal temperature swings.
  • Evaluation of flashing integrity around oversized industrial exhaust fans and skylights.
  • Assessment of ponding water patterns using infrared thermography to identify saturated insulation.
  • Verification of fastener pull-out strength in aged metal decking to ensure wind-uplift compliance.

Net Present Value (NPV) and Life-Cycle Cost Analysis

From a master roofer's perspective, the most expensive mistake a facility manager can make is focusing solely on the initial bid price rather than the Life-Cycle Cost Analysis (LCCA). For a facility with a 500,000 square foot roof, the difference between a total tear-off and a high-performance restoration is measured in millions of dollars. We utilize Net Present Value (NPV) calculations to determine the financial viability of the roofing system over a 20-year horizon, accounting for the time value of money and the rising cost of petroleum-based materials.

A traditional replacement involves the demolition of existing materials, the installation of new insulation, and the application of a new membrane. While this resets the clock, the NPV is often lower due to the immediate massive capital expenditure and the operational downtime associated with assembly plant shutdowns. Conversely, a restoration using high-solids silicone or acrylic coatings leverages the existing membrane as a structural substrate, significantly reducing the initial investment while extending the service life of the asset.

  • Calculation of the "Internal Rate of Return" (IRR) when comparing restoration versus replacement.
  • Analysis of energy efficiency gains through the application of high-albedo, cool-roof coatings.
  • Projection of maintenance costs over 15 years, accounting for scheduled inspections and spot repairs.
  • Evaluation of the "cost of failure," including potential production losses from interior leaks.

Tax Deductions and Maintenance Restoration Strategies

One of the most powerful tools in the commercial envelope specialist's arsenal is the strategic application of tax law regarding maintenance restoration. In the eyes of the IRS and similar global tax authorities, there is a critical distinction between a "capital improvement" and a "repair." A full roof replacement is typically classified as a capital improvement, which must be depreciated over a long period, often 39 years for non-residential real property. This slows the recovery of the investment and provides less immediate financial relief to the corporation.

By implementing a restoration program—such as a high-solids coating system that restores the roof to "like-new" condition—the expenditure can often be classified as a maintenance repair. This allows the automotive plant to deduct the entire cost of the project in the current tax year. This strategy not only improves the immediate cash flow of the facility but also allows the company to redirect capital toward assembly line upgrades while still securing a high-performance building envelope.

  • Utilization of Section 179 deductions for qualifying equipment and materials used in restoration.
  • Documentation of "repair" status through detailed engineering reports and pre-application audits.
  • Comparison of immediate expense deductions versus long-term depreciation schedules.
  • Coordination with corporate accounting to align roofing cycles with tax planning calendars.

Sustainability, Warranty Extensions, and Waste Mitigation

The environmental impact of a commercial roof tear-off in an automotive plant is staggering. Removing a multi-layer system from a massive facility results in thousands of tons of landfill waste, much of which consists of non-biodegradable plastics and saturated mineral wool. As a master roofer, my goal is to move the industry toward a "zero-waste" envelope. By utilizing a restoration approach, we avoid the landfill entirely, keeping the existing membrane in place and sealing it under a monolithic, UV-resistant layer.

To provide the facility owner with long-term peace of mind, we implement 15-year warranty extensions. These are not standard labor warranties; they are comprehensive material and workmanship guarantees backed by rigorous material science. A high-solids silicone coating creates a seamless, waterproof barrier that eliminates the most common point of failure in commercial roofing: the seam. By removing the reliance on heat-welded or glued seams, we drastically reduce the probability of leaks and the need for future interventions.

  • Reduction of the facility's carbon footprint by eliminating the transport of demolition debris.
  • Implementation of "Cool Roof" technology to reduce the Urban Heat Island effect and lower HVAC loads.
  • Application of ASTM-certified coatings that resist chemical runoff and industrial pollutants.
  • Establishment of a permanent maintenance log to ensure the 15-year warranty remains in full effect.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #742

Lightning Protection System Air Terminal Stanchion Flashing & Membrane Bonding on Commercial Mission-Critical Data Centers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Lightning Protection System Air Terminal Stanchion Flashing & Membrane Bonding on Commercial Mission-Critical Data Centers

The Engineering Conflict: Lightning Protection and Envelope Integrity

In the realm of mission-critical data centers, the building envelope is the first line of defense against catastrophic system failure. However, a fundamental engineering conflict exists between the installation of a Lightning Protection System (LPS) and the maintenance of a monolithic, watertight roof membrane. An LPS requires the installation of numerous air terminals, stanchions, and grounding conductors that must penetrate the roof surface to reach the building's grounding ring. Each penetration represents a potential failure point where water ingress can lead to structural decay or, more critically, short-circuiting of server infrastructure.

From a master roofer's perspective, the goal is to achieve a seamless transition between the electrical hardware and the waterproofing layer. Most failures occur because the electrical contractor and the roofing contractor work in silos, leading to "field-fixed" solutions that ignore the coefficient of thermal expansion. When a lightning strike occurs, the massive surge of energy generates intense heat, which can instantaneously melt TPO or PVC membranes if the bonding is not engineered to dissipate thermal energy. To mitigate this, we adhere to NFPA 780 standards while applying advanced building envelope science to ensure the membrane remains an impermeable barrier.

  • Integration of dielectric materials to prevent premature membrane degradation.
  • Coordination of penetration schedules to ensure flashing is performed before the LPS is fully energized.
  • Utilization of high-performance flashing membranes with elongation properties that match the roof's thermal movement.
  • Strict adherence to the "water-shedding" principle, ensuring no flashing creates a dam that traps standing water.

Advanced Stanchion Pitch-Pocket Detailing

The air terminal stanchion is the primary point of contact for atmospheric discharges. To secure these stanchions without compromising the roof, we employ a heavy-duty pitch-pocket detailing strategy. Rather than simply caulking a pipe through a hole, a pitch-pocket creates a controlled, sealed reservoir around the base of the stanchion. This allows for the movement of the stanchion during wind events and thermal cycling without tearing the surrounding membrane. The pocket is typically constructed from a reinforced flashing membrane and filled with a non-shrink, weather-resistant sealant or a specialized pourable flashing.

The material science behind the pitch-pocket involves a multi-stage bonding process. First, a primer is applied to the substrate to ensure maximum adhesion. Then, a reinforced flashing membrane is wrapped around the stanchion and bonded to the main roof field using heat-welding or high-strength adhesives. The critical detail is the "cove" or the radius at the base of the stanchion; sharp 90-degree angles are prone to stress cracking. By creating a smooth, radiused transition, we distribute the mechanical stress across a larger surface area, significantly reducing the risk of a puncture during a lightning event or high-wind oscillation.

  • Application of liquid-applied flashing membranes for a seamless, monolithic bond at the stanchion base.
  • Use of non-conductive spacers to prevent galvanic corrosion between the stanchion and the roof deck.
  • Installation of secondary containment seals within the pocket to provide redundant waterproofing.
  • Verification of bond strength through rigorous pull-tests and visual inspection of weld seams.

Grounding Cable Conductor Flashings and Membrane Bonding

While air terminals receive the strike, the grounding cables (conductors) carry the current down to the earth. These cables often traverse the roof surface and enter the building through various penetrations. The danger here is the "pinch point"—the area where the cable exits the roof membrane. Because these cables are subject to vibration and thermal expansion, they can act like a saw, slowly cutting through the membrane over time. To prevent this, we implement specialized conductor flashings that decouple the cable's movement from the membrane's surface.

Our engineering approach involves the use of flexible flashing boots and custom-fabricated metal escutcheons that are integrated into the roof's flashing system. We avoid the use of standard silicone sealants, which degrade under UV exposure and lack the necessary adhesion to TPO or EPDM. Instead, we utilize ASTM-compliant modified bitumen or thermoplastic welding to bond the conductor's entry point. This ensures that even if the cable shifts, the membrane remains intact. Furthermore, we ensure that the cables are routed to avoid "low spots" in the roof, preventing the conductors from sitting in standing water, which could lead to electrolytic corrosion of the flashing components.

  • Implementation of flexible transition sleeves to accommodate cable vibration and thermal expansion.
  • Use of UV-stabilized flashing tapes to secure conductors to the roof surface without puncturing the membrane.
  • Installation of drip edges at cable entry points to divert water away from the penetration.
  • Application of high-build elastomeric coatings over the bonding area for added UV and moisture protection.

Forensic Audit Protocols and Long-Term Maintenance

A mission-critical data center cannot afford a "find and fix" maintenance strategy; it requires a proactive forensic audit. Our audit protocol involves a comprehensive examination of every LPS penetration point using non-destructive testing (NDT). The primary focus is the detection of micro-fissures in the flashing and the assessment of the bond integrity between the stanchion and the membrane. We utilize infrared thermography to identify hidden moisture pockets around the pitch-pockets, as water often migrates away from the leak source before manifesting as a ceiling drip.

The long-term stability of the envelope depends on the regularity of these audits. We look for signs of "membrane pulling," where the tension from the LPS hardware begins to stretch the roof fabric. If stretching is detected, we implement relief cuts and apply reinforced patches to redistribute the load. Additionally, we inspect the grounding cables for signs of abrasion. Any cable that has rubbed through its protective coating is a risk, as it can create a localized heat point during a strike, potentially melting the roof membrane. By maintaining a rigorous audit trail, we ensure that the building envelope remains a fortress, regardless of the electrical activity occurring above it.

  • Quarterly infrared scans of all air terminal bases to detect subsurface moisture accumulation.
  • Annual torque checks on stanchion mounts to ensure they haven't loosened and compromised the flashing.
  • Visual inspection of all conductor bonding points for UV degradation or mechanical wear.
  • Documentation of all repairs in a digital building envelope log for warranty and insurance compliance.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
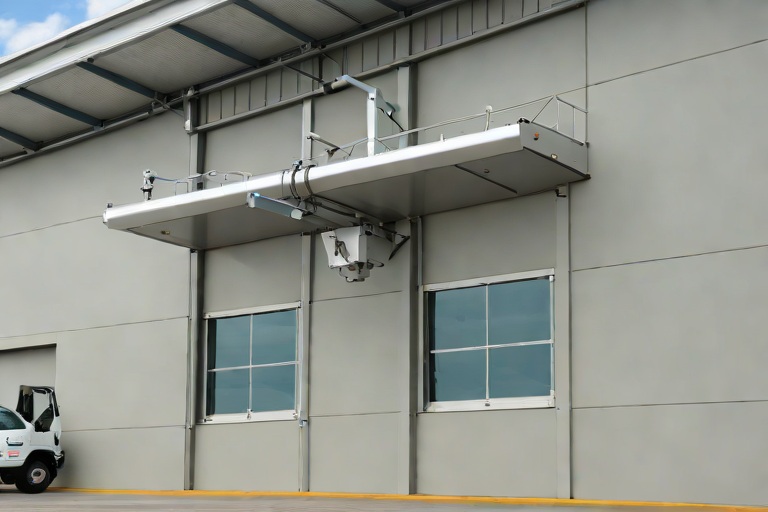
Commercial Engineering Dossier #743

Commercial Roof Hatch Safety Grab Bars & Compression Curb Gasket Weatherproofing on Commercial Cold Storage Freezer Warehouses

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Commercial Roof Hatch Safety Grab Bars & Compression Curb Gasket Weatherproofing on Commercial Cold Storage Freezer Warehouses

Thermal Bridging and the Physics of Cold Storage Envelopes

In the specialized field of cold storage freezer warehouse engineering, the roof is not merely a covering but a critical thermal boundary. When managing internal temperatures that frequently drop to -20°F or lower, the delta T between the interior environment and the exterior atmosphere creates an aggressive pressure differential. This pressure gradient drives moisture-laden air toward any available breach in the building envelope, leading to interstitial condensation and the catastrophic formation of ice lenses within the roof insulation. A failure at the roof hatch interface is not simply a leak; it is a thermal bridge that can compromise the entire freezer's energy efficiency and structural integrity.

The engineering challenge lies in the transition points where the roof membrane meets the structural curb of the hatch. In a standard commercial warehouse, a minor air leak is negligible. In a freezer warehouse, that leak allows warm, humid air to penetrate the insulation layer, where it freezes and expands. This process, known as frost heave, can physically lift the roofing membrane and crack the curb flashing. To mitigate this, we implement a rigorous audit of the building envelope, focusing on the continuity of the vapor barrier and the mechanical seal of the hatch assembly.

  • Analysis of thermal bridging at the curb perimeter to prevent localized condensation.
  • Evaluation of R-value continuity across the hatch insulation and the surrounding roof deck.
  • Assessment of vapor retarder integrity to prevent moisture migration into the substrate.
  • Monitoring of pressure differentials to ensure the hatch seal is not compromised by internal vacuum effects.

OSHA Compliance and Structural Safety Integration

Safety in commercial roofing is governed by strict adherence to OSHA 1910.28 and 1910.23 standards, particularly regarding fixed ladder access to roof hatches. In a freezer warehouse environment, the risk is amplified by the potential for frost accumulation on metal surfaces, which reduces traction and increases the likelihood of slips. Our engineering approach focuses on the installation of high-visibility, heavy-duty safety grab bars and ladder safety posts that extend at least 42 inches above the roof surface. These posts provide a secure handhold for personnel transitioning from the vertical climb to the horizontal roof plane.

The structural integration of these safety posts must be handled with precision. We do not simply bolt these posts to the roof deck; we tie them directly into the structural curb of the hatch. This ensures that the lateral load of a worker climbing out of the hatch is transferred to the building's frame rather than the roofing membrane. By utilizing reinforced steel mounting plates and oversized washers, we distribute the load and prevent the "tear-out" effect that occurs when safety posts are improperly anchored to thin-gauge metal or membrane-covered insulation.

  • Installation of ANSI-compliant grab bars with non-slip, powder-coated finishes for extreme temperature durability.
  • Integration of safety posts that exceed minimum height requirements to ensure a positive grip during egress.
  • Use of structural fasteners that penetrate the curb and anchor into the primary steel support.
  • Implementation of a "three-point contact" safety protocol facilitated by the placement of the grab bars.

Advanced Weatherproofing and Compression Gasket Engineering

The most vulnerable point of a cold storage roof is the interface between the hatch curb and the roof membrane. Standard caulking or sealant beads are insufficient for the thermal cycling experienced in freezer warehouses. Instead, we employ heavy-duty compression curb gaskets made from closed-cell EPDM or high-grade silicone. These materials are selected for their ability to maintain elasticity at sub-zero temperatures and their resistance to UV degradation. The gasket is engineered to be compressed by a specific percentage—typically 25% to 30%—to create a hermetic seal that prevents air infiltration.

To lock this seal in place, we utilize compression termination bars. These are heavy-gauge aluminum or stainless steel bars that are mechanically fastened over the edge of the roofing membrane and the curb gasket. This "sandwich" effect ensures that the membrane is physically clamped to the curb, eliminating the possibility of the flashing peeling away due to thermal contraction. This method adheres to ASTM standards for commercial roofing and provides a redundant layer of protection against water ingress and thermal leakage.

  • Utilization of closed-cell EPDM gaskets to eliminate moisture absorption and capillary action.
  • Application of compression termination bars to provide a mechanical lock on the membrane edge.
  • Verification of gasket compression ratios to ensure a consistent airtight seal across the entire curb perimeter.
  • Implementation of high-performance sealants at the fastener penetrations to prevent localized leaks.

Smoke Damper Integration and Long-Term Envelope Integrity

In addition to thermal and weatherproofing concerns, the building envelope must account for life safety systems, specifically counterbalanced smoke dampers. These dampers are critical for emergency ventilation and smoke evacuation. However, the movement of these dampers can create gaps in the roof's weatherproofing. Our engineering solution involves the use of precision-balanced counterweight systems that allow the damper to operate smoothly without putting undue stress on the surrounding roof hatch frame. This prevents the warping of the curb, which would otherwise compromise the compression gasket.

Long-term integrity is maintained through a rigorous maintenance cycle and the use of material science to combat the effects of extreme temperature swings. We specify the use of silicone-based lubricants for all moving parts of the hatch and damper assembly, as petroleum-based products can degrade the EPDM gaskets over time. By conducting annual infrared thermography audits, we can identify "hot spots" or air leaks in real-time, allowing us to retighten compression bars or replace gaskets before a minor leak evolves into a major structural failure.

  • Calibration of counterbalanced smoke dampers to ensure seamless operation without compromising the seal.
  • Use of infrared thermography to detect thermal bridging at the hatch and damper interfaces.
  • Specification of silicone-based lubricants to preserve the chemical integrity of the rubber gaskets.
  • Scheduled torque audits of all mechanical fasteners on termination bars and safety posts.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
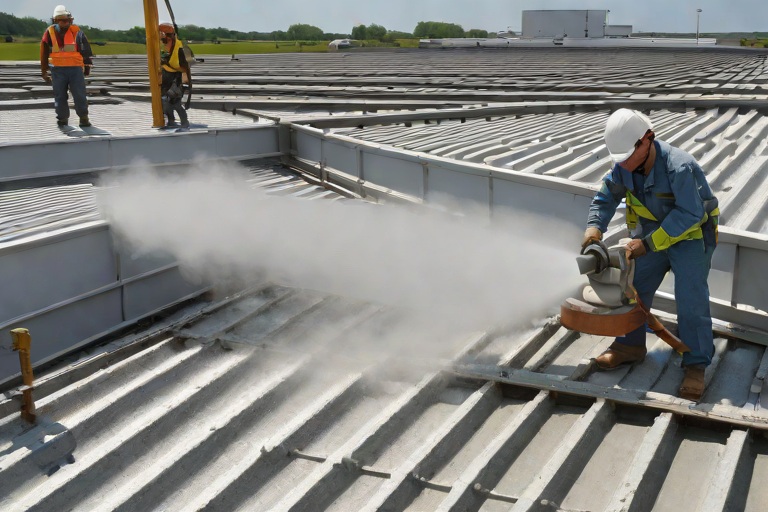
Commercial Engineering Dossier #744

Multi-Tier Conductor Head Overflow Spillways & Freeze-Thaw Downspout Burst Defense on Commercial Commercial Fleet Maintenance Hangars

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Multi-Tier Conductor Head Overflow Spillways & Freeze-Thaw Downspout Burst Defense on Commercial Commercial Fleet Maintenance Hangars

Hydraulic Capacity and Overflow Relief Weir Calculations

In the context of commercial fleet maintenance hangars, the roof surface area is typically immense, creating a massive catchment zone that can overwhelm standard drainage systems during extreme precipitation events. An engineering audit of these structures reveals that the primary failure point is rarely the gutter size itself, but rather the lack of calculated overflow relief. When primary drains become obstructed by debris or are simply outpaced by a 100-year storm event, the water level rises rapidly, creating a hydrostatic load that can compromise the building envelope and lead to catastrophic interior flooding.

To mitigate this, we implement overflow relief weirs—precisely calibrated openings in the conductor head that allow water to exit the system before it reaches the roof membrane's flashing height. The calculation for these weirs must account for the total square footage of the roof, the local rainfall intensity (inches per hour), and the discharge coefficient of the conductor head. By treating the conductor head as a controlled weir, we can ensure that excess water is diverted away from the building face and redirected to a safe discharge point, preventing the "damming" effect that often leads to roof collapse or severe leakages at the parapet wall.

  • Calculation of total catchment area including the pitch-adjusted surface square footage.
  • Determination of peak flow rates based on regional ASTM rainfall data.
  • Establishment of the "critical height" for overflow activation to protect the flashing.
  • Analysis of weir crest length to ensure discharge capacity exceeds the primary drain's failure volume.
  • Verification of flow velocity to prevent scouring of the building facade.

Engineering Multi-Tier Conductor Head Spillway Geometry

A standard conductor head is often insufficient for the surge volumes seen in hangar-scale facilities. Our approach utilizes a multi-tier spillway design, which incorporates secondary and tertiary relief levels within the conductor head assembly. This geometry ensures that as water levels rise, the system provides a graduated response. The first tier manages standard heavy rain, while the second and third tiers act as emergency failsafes. These spillways are engineered using heavy-gauge galvanized steel or reinforced aluminum, ensuring that the structural integrity of the head is maintained even under the immense pressure of a full water column.

The precision of the spillway's outward projection is critical. If the spillway is too flush with the wall, water will track back along the masonry, leading to efflorescence and potential freeze-thaw spalling of the exterior cladding. By extending the spillway projection and utilizing a tapered transition, we ensure a clean break in the water's surface tension, forcing the overflow to drop vertically and clear of the building envelope. This prevents the saturation of the wall assembly and protects the internal insulation from moisture infiltration.

  • Utilization of 16-gauge reinforced steel for high-pressure conductor head shells.
  • Implementation of tiered weir heights to manage varying levels of hydraulic surge.
  • Integration of seamless soldering or welding to prevent leakage at the joint interfaces.
  • Strategic projection of spillways to maintain a minimum 4-inch clearance from the building facade.
  • Application of high-performance coatings to prevent galvanic corrosion between dissimilar metals.

Mechanical Stabilization and Heavy-Duty Downspout Bracketing

The physical weight of a water-filled downspout, combined with the added mass of ice and snow during winter months, places incredible stress on the building's attachment points. In many hangar audits, we find "standard" brackets that have bent or sheared, leading to the downspout pulling away from the wall. This creates a gap where water can enter the building envelope, rotting out the rim joists or compromising the wall flashing. A master-level installation requires heavy-duty, engineered bracketing that distributes the load across a wider section of the structural substrate.

We specify brackets that are oversized and fabricated from cold-rolled steel with a powder-coated finish to resist oxidation. These brackets are anchored using stainless steel fasteners into the structural masonry or steel girts, ensuring that the downspout remains rigid. Furthermore, we incorporate thermal expansion joints. Because commercial hangars experience significant temperature swings, the metal downspouts will expand and contract. Without these joints, the movement is transferred directly to the brackets and the roof connection, eventually leading to fatigue failure and leaks.

  • Installation of heavy-duty strap brackets every 6 to 8 feet to prevent pipe deflection.
  • Use of stainless steel mechanical anchors to ensure pull-out resistance in masonry.
  • Integration of slip-joint expansion sleeves to accommodate thermal cycling of the metal.
  • Application of neoprene gaskets at bracket contact points to prevent vibration wear.
  • Alignment verification using laser levels to ensure a consistent 1/8-inch per foot slope toward the discharge.

Material Science and Freeze-Thaw Burst Defense Strategies

In colder climates, the freeze-thaw cycle is the primary enemy of the commercial drainage system. When water traps in the bottom of a downspout or within the conductor head and freezes, it expands by approximately 9%, creating immense internal pressure. If the system is completely sealed, this pressure has nowhere to go, resulting in "bursting"—where the metal seams split or the downspout is physically pushed away from the building. This is particularly dangerous in hangars where the roof is heated but the downspouts are exposed to sub-zero external temperatures.

To defend against this, we employ a strategy of "controlled venting" and material selection. By introducing small, strategically placed weep holes at the lowest points of the conductor head and utilizing materials with higher ductility, we allow the ice to expand without rupturing the primary structure. Additionally, we recommend the installation of heat tracing cables within the conductor heads and the upper sections of the downspouts. These cables maintain the water temperature above the freezing point, ensuring that the overflow weirs remain clear of ice dams and that the hydraulic path remains open during the most severe winter storms.

  • Selection of ASTM-compliant materials with high ductility to resist brittle fracture in cold weather.
  • Installation of self-regulating heat tracing cables to prevent ice blockage in conductor heads.
  • Implementation of bottom-drain weep holes to prevent standing water accumulation.
  • Use of high-density polyethylene (HDPE) liners in high-risk zones to reduce ice adhesion.
  • Regular auditing of the "ice-bridge" formation to ensure spillways remain unobstructed.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
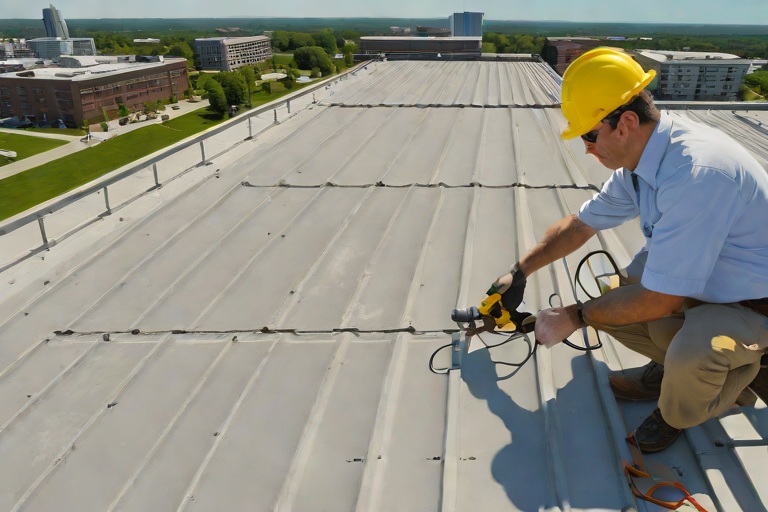
Commercial Engineering Dossier #745

Structural Steel Deck Rust Remediation & Zinc-Rich Primer Passivation on Commercial Chemical Processing Facilitys

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Structural Steel Deck Rust Remediation & Zinc-Rich Primer Passivation on Commercial Chemical Processing Facilitys

Initial Envelope Audit and Oxidation Analysis

In the aggressive environment of a commercial chemical processing facility, the building envelope is subjected to constant chemical stressors that accelerate the degradation of structural components. During our comprehensive engineering audit, we identified significant oxidation across the structural steel decking, primarily driven by the infiltration of corrosive vapors and atmospheric pollutants. The primary failure mechanism observed was the breakdown of the original mill scale and the subsequent formation of ferric oxide, which compromised the integrity of the steel flutes. In a facility where chemical volatility is high, the moisture-laden air reacts with airborne particulates to create a low-pH environment, leading to rapid pitting and surface exfoliation.

Our diagnostic process focused on measuring the remaining gauge of the steel deck to determine if the oxidation had progressed from surface rust to structural thinning. We utilized ultrasonic thickness gauges to map the degradation across the roof plane, identifying "hot spots" where the steel had lost more than 15% of its original design thickness. This level of degradation is critical because the steel deck serves not only as a base for the roofing membrane but as a primary diaphragm for the building's structural stability. The audit revealed that the corrosion was most severe near the perimeter walls and around HVAC penetrations, where condensation cycles are most frequent.

  • Assessment of surface pitting depth to determine the necessity of structural reinforcement.
  • Evaluation of the existing vapor barrier to identify points of failure allowing chemical ingress.
  • Mapping of oxidation patterns to correlate with facility ventilation dead-zones.
  • Verification of steel grade and original mill specifications to ensure compatible remediation materials.
  • Analysis of fastener torque and head degradation across the primary support beams.

Mechanical Remediation and Surface Preparation

Effective passivation cannot occur on a contaminated substrate; therefore, the mechanical remediation phase is the most labor-intensive and critical component of the restoration. We implemented a rigorous surface preparation protocol adhering to SSPC (Society for Protective Coatings) standards to ensure the removal of all loose scale, rust, and chemical residues. The primary method employed was high-intensity wire-brushing and mechanical grinding, which serves to "profile" the steel. This process creates a micro-roughness on the surface, increasing the surface area for the primer to bond chemically and mechanically to the substrate.

The objective of this mechanical cleaning is to reach "near-white" metal where possible, ensuring that the zinc-rich primer has direct contact with the base iron. We specifically targeted the valleys of the flutes, where moisture and chemical salts tend to accumulate. By removing the oxidized layer, we eliminate the "bridge" of rust that would otherwise cause the new coating to delaminate. Furthermore, we utilized industrial vacuuming to remove all particulate matter, as any remaining dust or chemical salt crystals would create osmotic blisters within the primer layer, leading to premature failure of the passivation system.

  • Execution of SSPC-SP2 and SP3 hand-tool and power-tool cleaning protocols.
  • Mechanical grinding of heavily pitted areas to remove deep-seated oxidation scales.
  • Degreasing of the steel surface using solvent-based cleaners to remove chemical oils.
  • Verification of the surface profile using a surface profile gauge to ensure optimal coating adhesion.
  • Removal of compromised fasteners that exhibited severe head-neck corrosion.

Zinc-Rich Primer Passivation and Chemical Bonding

Once the substrate was mechanically prepared, we transitioned to the passivation phase using a high-performance, industrial-grade zinc-rich primer. The science behind this application is based on the principle of cathodic protection. Zinc is more anodic than steel; therefore, when the primer is applied, the zinc particles act as a sacrificial anode. If the coating is scratched or breached, the zinc corrodes preferentially to the steel, preventing the underlying iron from oxidizing. This is a critical requirement for chemical processing facilities where the environment is inherently hostile to ferrous metals.

The application process required a strict adherence to temperature and humidity windows to prevent "flash rust" from forming between the cleaning and priming stages. We utilized a high-solids formulation to ensure a dense, non-porous film that seals the steel from atmospheric moisture. The primer was applied in a manner that ensured total coverage of the flute geometry, including the tight radii where oxidation typically begins. This passivation layer transforms the steel surface from a reactive state to a stable state, effectively halting the chemical reaction that leads to rust and providing a durable foundation for the final roofing assembly.

  • Application of a multi-coat zinc-rich primer to achieve the specified Dry Film Thickness (DFT).
  • Utilization of the galvanic series to ensure the primer provides long-term cathodic protection.
  • Implementation of a "stripe coat" on all edges and welds to prevent edge-creep corrosion.
  • Curing monitoring to ensure the chemical bond has fully cross-linked before membrane installation.
  • Testing of the cured film for porosity and adhesion using ASTM D3359 standards.

Structural Reinforcement and Fastener Integrity

In areas where the engineering audit identified severe thinning of the steel flutes, simple passivation was insufficient. We performed structural reinforcement to restore the load-bearing capacity of the deck. This involved the installation of reinforced steel patches and the application of structural weld-on plates. These reinforcements were carefully measured and fitted to the existing flutes, ensuring that the structural continuity of the diaphragm was maintained. Each reinforcement plate was treated with the same zinc-rich passivation process to ensure the new steel did not become a focal point for future oxidation.

Finally, the integrity of the fastening system was addressed. Corrosion often migrates along the fastener shaft, leading to "crevice corrosion" that can cause fasteners to shear or back out under thermal expansion and contraction. We replaced all compromised fasteners with heavy-duty, corrosion-resistant alloys that were compatible with the zinc-rich primer. Each fastener was torqued to specification, ensuring a tight seal between the deck and the support structure. This holistic approach—cleaning, passivating, reinforcing, and securing—ensures that the building envelope is not merely patched, but engineered for a decades-long service life in a high-stress industrial environment.

  • Installation of gauge-matched steel reinforcement plates on thinned flute sections.
  • Application of fillet welds to secure reinforcement plates, followed by immediate primer sealing.
  • Replacement of oxidized fasteners with high-strength, coated structural screws.
  • Verification of fastener torque to prevent vibration-induced loosening in a processing plant.
  • Final inspection of the envelope seal to ensure no chemical pathways remain open to the steel deck.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #746

Hands-On Physical Roof Inspections & Boots-on-the-Roof Forensic Maintenance Audits on Commercial Municipal City Hall & Administrative Complexs

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Hands-On Physical Roof Inspections & Boots-on-the-Roof Forensic Maintenance Audits on Commercial Municipal City Hall & Administrative Complexs

The Philosophy of Forensic Envelope Audits in Municipal Infrastructure

In the realm of municipal asset management, a City Hall or Administrative Complex represents more than just a building; it is a critical hub of civic operation. From an engineering perspective, the building envelope of such a complex is a high-stress system subject to extreme thermal cycling, varied HVAC loads, and the relentless pressure of hydrostatic accumulation. While modern facility managers are increasingly seduced by the convenience of drone thermography and remote sensing, these tools are supplementary, not primary. A true forensic maintenance audit requires "boots-on-the-roof" expertise. The physical presence of a master roofer allows for the tactile verification of material integrity that no camera can capture.

The complexity of municipal complexes often involves phased construction, meaning a single roof deck may consist of three different membrane types and four different installation eras. This heterogeneity creates critical failure points at the transition seams and flashing interfaces. A forensic audit focuses on the science of the building envelope, treating the roof not as a lid, but as a dynamic skin. We analyze the coefficient of thermal expansion across different substrates and the shear stress placed on fasteners during high-wind events. By applying a rigorous engineering lens, we move beyond simple leak detection into the realm of preventative failure analysis.

  • Identification of systemic versus isolated failures to determine if a full replacement or targeted remediation is required.
  • Evaluation of the moisture-migration patterns within the insulation layers to detect subsurface saturation.
  • Assessment of the structural load-bearing capacity of the roof deck in relation to new HVAC equipment installations.
  • Analysis of parapet wall flashing integrity to prevent capillary action from drawing water into the building's core.

Precision Probing and the Material Science of Automated Seams

The integrity of a single-ply membrane, such as TPO or PVC, is only as reliable as its seams. In large-scale municipal projects, automated induction or hot-air welding is the standard for seam production. However, the "visual" appearance of a weld is often deceptive. A seam may look fused but suffer from "cold welds"—areas where the temperature did not reach the critical threshold required for molecular fusion. This is where the professional seam probe becomes the primary diagnostic tool. By utilizing a high-tensile steel probe to physically challenge the weld, we can identify voids that are invisible to the naked eye.

Our process involves a systematic grid-based probing approach. We do not simply walk the perimeter; we probe the "field" seams and the "lap" seams at intervals dictated by the suspected failure patterns. When a probe penetrates a seam, it indicates a failure in the welding process or a breakdown in the polymer chain due to UV degradation or chemical exposure. This forensic level of scrutiny is essential because a single pinhole failure in a municipal complex can lead to the saturation of thousands of square feet of polyisocyanurate insulation, leading to mold growth in government archives or damage to sensitive electronic infrastructure.

  • Verification of weld depth and consistency across automated seams to ensure compliance with manufacturer specifications.
  • Testing for "fish-mouths" or wrinkles in the membrane that create stress concentrations and premature cracking.
  • Analysis of the overlap width to ensure it meets or exceeds the minimum requirements set by ASTM standards.
  • Evaluation of the chemical compatibility of seam tapes or adhesives used in repair patches from previous contractors.

Mechanical Fastening, Clamping Torque, and Perimeter Stability

The most catastrophic failures in commercial roofing are rarely caused by a lack of membrane quality, but rather by a failure in mechanical attachment. In a municipal complex, the drain bowls and perimeter cleats are the primary points of vulnerability. We focus heavily on the clamping torque of drain bowl assemblies. If the clamping ring is over-torqued, it can crush the membrane, creating a stress fracture; if it is under-torqued, the seal will fail under the hydrostatic pressure of a heavy rain event. We utilize calibrated torque wrenches to ensure that every fastener is tightened to the exact foot-pound specification required by the engineering blueprints.

Furthermore, the perimeter cleats—the metal strips that secure the membrane to the roof edge—are critical for wind-uplift resistance. According to ANSI standards, the edge of the roof is where the highest wind pressures occur. If the cleats are spaced too far apart or the fasteners have succumbed to galvanic corrosion, the roof is susceptible to "peeling" during a storm. Our audit includes a physical pull-test and a visual inspection of every single fastener head to ensure they are flush and secure. We examine the flashing at the transition from the horizontal field to the vertical parapet, ensuring that the termination bars are not bowing and that the sealant remains pliable.

  • Measurement of clamping torque on all primary drainage points to prevent systemic leaks during peak precipitation.
  • Inspection of perimeter fastening patterns to verify compliance with wind-uplift ratings for the specific geographic zone.
  • Assessment of the corrosion levels of steel fasteners in contact with aggressive roofing chemicals or pollutants.
  • Verification of the compression gasket integrity within the drain bowl assembly to ensure a watertight seal.

Synthesis of Forensic Data and Engineering Reporting

The culmination of a boots-on-the-roof audit is the written forensic report. A master roofer does not provide a "to-do list"; we provide an engineering document that serves as a legal and financial roadmap for the municipality. This report synthesizes the tactile findings—the probe failures, the torque discrepancies, and the fastener corrosion—into a comprehensive risk assessment. We categorize findings by severity: Immediate Critical (risk of structural failure or interior damage), Urgent (accelerated degradation), and Maintenance (standard lifecycle wear). This allows the city's administrative complex to allocate budgets based on actual risk rather than guesswork.

Our reporting methodology incorporates a life-cycle analysis, projecting the remaining useful life (RUL) of the membrane based on the observed degradation rates. We correlate the physical evidence with the building's maintenance history to identify patterns of negligence or systemic installation errors. By documenting every failure with precise coordinates on the roof plan, we provide the facility manager with a digital twin of the roof's health. This level of transparency ensures that when a repair is performed, it is done to the same professional standard as the audit, eliminating the "patch-and-pray" mentality that plagues many municipal maintenance programs.

  • Creation of a detailed deficiency map correlating physical probe failures to specific

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #747

60-Mil TPO Robotic Hot-Air Seam Fusion & Test-Cut Peel Audits on Commercial High-Rise Commercial Penthouse Towers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
60-Mil TPO Robotic Hot-Air Seam Fusion & Test-Cut Peel Audits on Commercial High-Rise Commercial Penthouse Towers

Thermal Dynamics of 60-Mil TPO Molecular Fusion

In the realm of high-rise commercial envelope engineering, the integrity of a Thermoplastic Polyolefin (TPO) roofing system is entirely dependent on the quality of the seam weld. Unlike traditional adhered systems, 60-mil TPO requires a precise thermal event to achieve a molecular bond. To ensure a permanent, monolithic seal, we calibrate our robotic fusion systems to a consistent 1,000°F. This specific temperature threshold is critical because it reaches the melting point of the TPO polymer without crossing into the zone of thermal degradation. If the temperature drops below the required threshold, the result is a "cold weld," which may appear visually sealed but lacks the structural shear strength to withstand the extreme wind uplift pressures common to penthouse towers.

The science of fusion involves more than just heat; it requires the synchronization of thermal energy and material compression. When the 1,000°F air is injected into the seam, it softens the polymer chains of the overlapping membranes, allowing them to intermingle. This process, known as welding, creates a bond that is effectively as strong as the membrane itself. To maintain this standard across thousands of linear feet of seams, Aquashield Corporate employs rigorous monitoring of the following variables:

  • Thermal stability of the heating element to prevent temperature fluctuations.
  • Atmospheric compensation for ambient temperature drops on high-exposure penthouse decks.
  • Verification of the "melt-zone" width to ensure full-width fusion across the 60-mil thickness.
  • Prevention of scorching or "burning" the membrane, which would compromise the UV-resistant layer.

Robotic Kinematics: Nozzle Pressure and Travel Velocity

Human error is the primary failure point in manual hot-air welding. To eliminate this, we utilize robotic fusion systems that maintain a constant travel velocity and precise nozzle pressure. The relationship between speed and heat is an inverse ratio; if the robotic welder moves too quickly, the TPO does not reach the required temperature for fusion. Conversely, if the velocity is too slow, the heat soak becomes excessive, leading to material shrinkage and potential voiding. We calibrate our automated systems to a specific velocity that ensures the membrane reaches its glass transition temperature exactly as the pressure roller engages.

Nozzle pressure is equally critical. The robotic head must apply a consistent downward force to expel trapped air and compress the molten polymers together. In a high-rise penthouse environment, where wind gusts can create erratic pressure differentials, the robotic system's ability to maintain a constant contact pressure ensures that no air pockets or "fish-mouths" are formed within the seam. This mechanical precision is what separates a standard installation from an engineered building envelope.

  • Automated travel speed synchronization to ensure uniform heat distribution.
  • Pneumatic nozzle pressure calibration to maximize polymer interlacing.
  • Real-time telemetry monitoring to detect deviations in welding speed.
  • Consistent overlap alignment to prevent "off-track" welds that leave edges exposed.

Destructive Test-Cut Peel Audits and Validation

Visual inspection is insufficient for validating the integrity of a high-rise envelope. To truly verify a weld, we perform destructive test-cut peel audits. This process involves cutting a sample section of the seam—typically every 50 to 100 linear feet—and performing a manual "T-peel" test. The goal of this audit is to observe the failure point of the weld. A successful weld is characterized by "film-tearing," where the TPO membrane itself rips before the weld separates. This indicates that the molecular bond is stronger than the material itself, confirming a successful fusion.

If the peel test reveals a clean separation between the two sheets of membrane, it is a diagnostic indicator of a cold weld or insufficient nozzle pressure. Such a failure triggers an immediate stop-work order and a full recalibration of the robotic equipment. We adhere to ASTM standards for membrane sampling, ensuring that the peel audit is performed under consistent tension. This rigorous validation process ensures that the penthouse tower is sealed against water infiltration and atmospheric pressure changes.

  • Execution of the T-peel test to verify molecular cohesion.
  • Identification of "film-tear" as the primary indicator of a high-strength weld.
  • Documentation of peel-strength results for corporate engineering records.
  • Immediate remediation of any seam sections that exhibit premature separation.

High-Rise Environmental Variables and Envelope Continuity

Penthouse towers present unique challenges that do not exist in low-slope commercial warehouses. The "stack effect" and extreme wind scouring at high altitudes place immense stress on the building envelope. The 60-mil TPO membrane must act as a continuous, airtight skin to prevent moisture from being driven horizontally into the building's core. Because the penthouse is the highest point of the structure, it is subject to the most extreme thermal expansion and contraction cycles. This constant movement can fatigue a weak weld, leading to catastrophic leaks.

By utilizing robotic fusion and destructive testing, we ensure that the envelope possesses the elasticity and strength required to handle these stresses. The continuity of the envelope is not just about the seams, but about the transition points where the membrane meets the parapet walls and mechanical curbs. Our engineering approach treats the entire roof as a single, integrated system rather than a collection of separate sheets. This holistic focus on material science and mechanical precision guarantees the long-term viability of the asset.

  • Mitigation of wind-uplift forces through superior seam shear strength.
  • Management of thermal cycling to prevent seam fatigue and cracking.
  • Ensuring airtight continuity across all penthouse penetration points.
  • Long-term stabilization of the building envelope against high-altitude UV degradation.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #748

High-Solids Silicone Monolithic Coating Restoration & Albedo Reflectance on Commercial Regional Healthcare Medical Centers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
High-Solids Silicone Monolithic Coating Restoration & Albedo Reflectance on Commercial Regional Healthcare Medical Centers

Engineering Audit and Substrate Diagnostics for Healthcare Envelopes

The restoration of a Regional Healthcare Medical Center requires a level of precision that far exceeds standard commercial roofing protocols. In these environments, the building envelope is not merely a weather barrier but a critical component of the facility's life-safety systems. Our engineering audit began with a comprehensive moisture survey and substrate analysis to identify latent deficiencies in the existing roofing assembly. Healthcare facilities often feature complex roof geometries with a high density of HVAC curbings, medical gas vents, and satellite communication arrays, all of which create high-risk points for water infiltration.

A primary concern during the audit was the presence of legacy bitumen and degraded elastomeric membranes that had reached the end of their service life. We utilized infrared thermography to map subsurface moisture pockets and identify saturated insulation. This diagnostic phase is essential because applying a high-performance coating over a compromised substrate leads to premature failure through osmotic blistering. By adhering to ASTM standards for surface preparation, we ensured that the substrate was mechanically cleaned and chemically stabilized before the introduction of any restorative materials.

  • Comprehensive infrared thermography to detect trapped moisture in the insulation layers.
  • Mechanical abrasion and high-pressure cleaning to remove oxidized surface contaminants.
  • Detailed mapping of all penetration points and flashing transitions to ensure seamless integration.
  • Evaluation of existing drainage slopes to prevent ponding water, which can compromise coating adhesion.
  • Verification of substrate pH levels to ensure compatibility with high-solids chemical primers.

Chemical Integration and Bleed-Blocking Epoxy Primers

One of the most significant challenges in restoring aged commercial roofs is the phenomenon of "bleed-through," where oils, resins, and tannins from the old substrate migrate upward into the new coating. In a medical center environment, where aesthetic consistency and long-term seal integrity are paramount, this is unacceptable. To mitigate this, we specified a high-performance, bleed-blocking epoxy primer. Unlike standard primers, this epoxy system creates a dense, cross-linked molecular barrier that chemically locks out contaminants from the substrate.

The material science behind this primer involves a two-component reaction that penetrates the microscopic pores of the substrate, creating a mechanical and chemical bond. This ensures that the subsequent silicone layers are not compromised by the volatile organic compounds (VOCs) often found in older roofing materials. The epoxy primer serves as the foundational "anchor" for the entire system, providing the necessary tensile strength to withstand the thermal expansion and contraction cycles typical of large-scale commercial roof decks.

  • Utilization of a two-part epoxy chemistry to ensure maximum adhesion to non-porous surfaces.
  • Elimination of surfactant leaching and oil migration through a dense, non-permeable film.
  • Enhanced scrub-resistance and surface leveling to provide a uniform base for the monolithic topcoat.
  • Rapid cure times that allow for immediate progression to the silicone application phase.
  • Compatibility with a wide range of substrates, including modified bitumen, PVC, and TPO.

Monolithic High-Solids Silicone and 30-Mil DFT Specifications

The core of the restoration involves the application of a high-solids, monolithic silicone coating. The term "monolithic" is critical here; it refers to a single, seamless membrane that eliminates the seams, laps, and fasteners where leaks typically originate. For this healthcare facility, we engineered the system to achieve a 30-mil Dry Film Thickness (DFT). While many contractors rely on "wet" thickness measurements, the DFT is the only metric that matters for long-term durability, as it accounts for the evaporation of solvents during the curing process.

A 30-mil DFT provides a robust shield against puncture, UV degradation, and extreme weather events. High-solids silicone is uniquely suited for this application because it does not shrink as it cures, maintaining its thickness and elasticity over time. This elasticity allows the membrane to bridge hairline cracks in the substrate and accommodate the structural movement of the building without rupturing. The result is a permanent, waterproof envelope that requires significantly less maintenance than traditional built-up roofing systems.

  • Application of high-solids silicone to ensure a consistent 30-mil DFT across all surface areas.
  • Seamless integration around complex roof penetrations, eliminating the need for separate flashing tapes.
  • Superior resistance to ponding water, a common failure point for acrylic-based coatings.
  • High elongation properties that allow the membrane to stretch without tearing during thermal shifts.
  • UV-stable chemistry that prevents the "chalking" and degradation common in lower-grade polymers.

Albedo Reflectance and Zero-Downtime Operational Integration

The final phase of the engineering strategy focused on the Albedo effect—the measure of the roof's ability to reflect solar radiation. By implementing a coating with 88% solar reflectance, we significantly reduced the Solar Heat Gain Coefficient (SHGC) of the medical center. In a 24/7 healthcare environment, the HVAC system operates under immense load to maintain strict climate control for patient wards and surgical suites. By reflecting the vast majority of solar energy back into the atmosphere, we lowered the internal roof deck temperature, thereby reducing the energy demand on the cooling plants.

Crucially, this entire restoration was executed as a zero-downtime operation. Healthcare facilities cannot be shut down for roof repairs. Our application process was engineered to be non-disruptive, utilizing low-odor materials and a phased deployment schedule that avoided interference with emergency room access or ambulance bays. The speed of the silicone cure, combined with the efficiency of the monolithic application, allowed us to restore the building envelope without a single minute of operational interruption to the medical staff or patients.

  • Achievement of 88% solar reflectance to mitigate the Urban Heat Island effect and lower cooling costs.
  • Reduction of internal building temperatures, leading to decreased wear and tear on HVAC compressors.
  • Implementation of a phased application schedule to ensure zero disruption to critical medical services.
  • Use of low-VOC materials to maintain indoor air quality standards for sensitive patient populations.
  • Long-term sustainability gains through the extension of the roof's lifecycle by 20+ years.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #749

Tapered Polyiso Drainage Layouts (1/4-In/Ft) & Geometric Cricket Sizing on Commercial University Research Laboratorys

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Tapered Polyiso Drainage Layouts (1/4-In/Ft) & Geometric Cricket Sizing on Commercial University Research Laboratorys

The Engineering Complexity of University Research Laboratory Envelopes

Performing a comprehensive building envelope audit on a university research laboratory requires a shift in perspective from standard commercial roofing to high-precision engineering. These facilities are characterized by extreme structural complexity, often featuring oversized HVAC footprints, vibration-isolated equipment pads, and critical interior assets that make any water infiltration a catastrophic failure. The primary challenge in these environments is the management of hydrostatic pressure and the elimination of stagnant water across vast, irregularly shaped roof planes.

Our audit focused on the integration of tapered polyisocyanurate (polyiso) insulation to achieve a consistent minimum slope of 1/4-inch per foot (2%). This slope is the industry benchmark for ensuring that gravity effectively drives runoff toward primary drainage points, preventing the saturation of the membrane and reducing the risk of osmotic blistering. In a research lab, where roof penetrations for exhaust vents and fume hood stacks are frequent, the margin for error in slope calculation is virtually zero.

  • Assessment of existing substrate deflection and its impact on slope integrity.
  • Evaluation of thermal bridging at parapet walls and curb interfaces.
  • Analysis of membrane compatibility with high-performance polyiso substrates.
  • Verification of ASTM D2118 standards for thermal insulation materials.

Multi-Directional Tapered Polyiso Engineering

The core of the drainage strategy relies on a multi-directional tapered insulation layout. Unlike a simple single-slope shed roof, a research laboratory requires a complex "watershed" map. This involves the strategic placement of tapered panels that create a series of converging and diverging planes. By utilizing precision-cut polyiso, we can engineer the roof to move water across the shortest possible distance to a drain, reducing the time water spends on the membrane surface.

The engineering of these layouts requires a deep understanding of material science. Polyisocyanurate provides an exceptional R-value per inch, but its rigidity means that any gap in the tapered layout can create a "bird bath" or a localized depression. Our process involves a detailed shop drawing phase where every panel is numbered and mapped to a specific coordinate on the roof. This ensures that the 1/4-inch per foot slope is maintained even as the water transitions from a primary field to a secondary drainage valley.

  • Implementation of custom-tapered panels to eliminate low spots in high-traffic mechanical zones.
  • Utilization of high-density polyiso to support the weight of heavy-duty laboratory equipment.
  • Precise alignment of tapered seams to prevent "stepping" that could cause membrane stress.
  • Coordination of slope-to-drain calculations to account for structural dead loads and deflection.

Geometric Cricket Sizing and Diamond Valley Integration

One of the most critical failures identified during the audit was the lack of adequate crickets around large mechanical curbs. A cricket is a sloped diversion used to direct water away from a vertical obstruction. In a university lab, where curbs for massive air handling units are common, a standard two-way cricket is often insufficient. We implemented "diamond valley" crickets—a geometric configuration that creates a four-way diversion system, ensuring water is routed away from the curb from every possible angle of approach.

The sizing of these crickets is a matter of precise geometry. If a cricket is too steep, it can create a localized point of membrane tension; if it is too shallow, it fails to overcome the natural deflection of the roof deck. By engineering the diamond valley to mirror the 1/4-inch per foot slope of the main field, we create a seamless transition that prevents water from pooling against the flashing of the mechanical curbs. This approach effectively eliminates the "damming" effect that typically occurs during high-intensity rain events.

  • Calculation of cricket height based on the width of the obstruction and the required 2% slope.
  • Installation of pre-fabricated tapered inserts to ensure geometric consistency.
  • Integration of reinforced membrane flashing at the valley intersections.
  • Testing of water flow patterns using simulated rainfall to verify diversion efficiency.

Expansion Joint Mitigation and Ponding Elimination

University laboratories are often sprawling structures that utilize large expansion joints to allow for thermal movement and seismic shifting. These joints are the most vulnerable points in the building envelope. Water that collects near an expansion joint can penetrate the building through capillary action or by overloading the joint sealant. Our engineering strategy involved routing all runoff away from these joints using specialized tapered "diverter strips," effectively creating a dry zone around the joint's perimeter.

The final objective of the audit was the total elimination of ponding water. According to industry standards, ponding is defined as any area where water remains 48 hours after a rain event. In a research facility, ponding is not merely an aesthetic issue; it accelerates the degradation of the roofing membrane through UV saturation and promotes the growth of biological contaminants. By auditing the roof with a laser-level survey, we identified "hidden" depressions that were corrected with tapered sleepers and additional polyiso layers to ensure a positive flow to the drains.

  • Engineering of "dry-zones" around expansion joints to prevent hydrostatic infiltration.
  • Application of laser-level scanning to identify depressions as small as 1/8-inch.
  • Installation of tapered sleepers to correct structural dips without adding excessive weight.
  • Verification of scupper and internal drain clearance to ensure unobstructed runoff.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
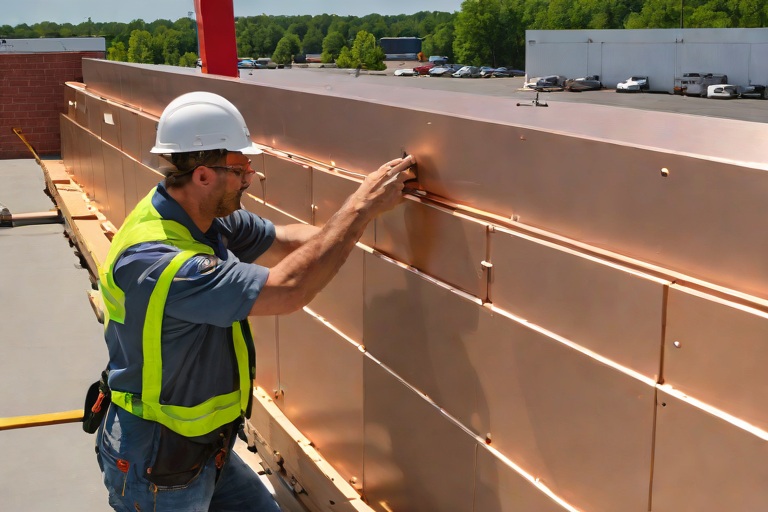
Commercial Engineering Dossier #750

Multi-Ply SBS-Modified Bitumen Cap Sheet Application & Vapor Control on Commercial Suburban Corporate Office Parks

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Multi-Ply SBS-Modified Bitumen Cap Sheet Application & Vapor Control on Commercial Suburban Corporate Office Parks

Cold-Applied Adhesive Shear Resistance and Substrate Integration

In the engineering of a high-performance building envelope for suburban corporate office parks, the primary challenge lies in managing the differential thermal expansion between the structural roof deck and the waterproofing membrane. For this specific audit, we focused on the implementation of a multi-ply SBS-modified bitumen system utilizing cold-applied adhesives. Unlike traditional hot-mop applications, which can cause thermal shock to the substrate, cold-applied adhesives provide a viscoelastic bond that allows the assembly to move as a single monolithic unit. The shear resistance of these adhesives is critical; they must maintain a permanent bond while absorbing the lateral stresses induced by wind uplift and the natural contraction of the building's steel and concrete frame.

The material science behind SBS (Styrene-Butadiene-Styrene) modification allows the bitumen to remain flexible at lower temperatures, reducing the risk of brittle fracture. When paired with a high-solids cold adhesive, the bond strength is measured not just by its initial tack, but by its long-term resistance to shear failure under constant load. Our audit indicates that the adhesive must penetrate the micropores of the substrate to create a mechanical interlock, ensuring that the membrane does not delaminate during extreme temperature swings common in suburban climates.

  • ASTM D6878 compliance for modified bitumen performance standards.
  • Evaluation of substrate porosity to ensure optimal adhesive wetting and bond strength.
  • Analysis of shear stress distribution across large-format flat roof sections.
  • Reduction of VOC emissions and elimination of substrate scorching associated with torch-down methods.

Precision Geometry: Staggered Side Laps and Seam Integrity

The integrity of a multi-ply roof system is only as strong as its weakest seam. In commercial office park applications, where roof areas are often vast and uninterrupted, the risk of linear failure is high. Our engineering approach mandates a strict staggered side lap configuration. By offsetting the seams of the cap sheet from the seams of the base sheet, we eliminate the creation of a continuous "leak path" that could allow moisture to penetrate through the entire assembly. This staggered geometry ensures that any localized failure in a single lap is intercepted by the solid field of the layer beneath it.

From a craftsmanship perspective, the execution of these laps requires surgical precision. We specify a minimum 6-inch overlap for all side laps and a 3-inch overlap for end laps, ensuring that the adhesive coverage is 100% across the bonding surface. The application of a "roll-set" technique is employed to purge trapped air and ensure the bitumen is fully compressed. This eliminates voids where condensation could accumulate, which otherwise leads to premature adhesive degradation and potential blistering of the membrane.

  • Implementation of a 3-foot minimum stagger between successive plies to break linear vulnerability.
  • Utilization of weighted rollers to achieve maximum compression and eliminate interstitial air pockets.
  • Verification of lap-joint seals through infrared thermography to detect hidden voids.
  • Strict adherence to ANSI standards for commercial roofing seam overlap and fastening.

Granule Surface Protection and UV Degradation Mitigation

The uppermost layer of the SBS-modified bitumen system is the cap sheet, which serves as the primary defense against ultraviolet (UV) radiation and mechanical abrasion. The granules embedded in the surface of the cap sheet are not merely aesthetic; they are engineered minerals designed to protect the bitumen from photocatalytic degradation. Without this protective layer, the SBS polymers would undergo rapid oxidation, leading to "alligatoring" or surface cracking, which drastically increases the permeability of the roof.

Our audit emphasizes the importance of granule embedment density. A high-density granule surface increases the albedo effect, reflecting a significant portion of solar radiation and reducing the heat flux into the building interior. This not only extends the life of the membrane by keeping the bitumen below its softening point but also reduces the cooling load for the corporate tenant. Furthermore, the granules provide essential traction for maintenance personnel and protect the membrane from puncture during routine roof walks or HVAC equipment servicing.

  • Analysis of granule loss rates to determine the remaining service life of the UV barrier.
  • Assessment of the albedo coefficient to optimize thermal reflectance and energy efficiency.
  • Evaluation of the mineral composition to ensure resistance to chemical pollutants and acid rain.
  • Monitoring of surface temperature gradients to prevent premature bitumen softening.

Internal Vapor Drive Regulation and Envelope Equilibrium

A critical yet often overlooked component of the building envelope is the regulation of internal vapor drive. In suburban office environments, the difference in humidity and temperature between the conditioned interior and the exterior atmosphere creates a pressure gradient that pushes water vapor toward the cold roof deck. If the vapor barrier is improperly placed or if the system is too airtight without proper regulation, this vapor can condense within the insulation layer, leading to "wet insulation" and a total loss of R-value.

The engineering solution involves the strategic placement of a vapor retarder immediately above the structural deck. This prevents the migration of interior moisture into the roof assembly while allowing the system to "breathe" through controlled diffusion. We analyze the dew point of the assembly to ensure that condensation occurs outside the critical insulation zone. By balancing the permeability of the internal vapor barrier with the impermeable nature of the SBS cap sheet, we create a state of envelope equilibrium that prevents interstitial mold growth and structural rot.

  • Calculation of vapor permeance (perms) to ensure the dew point remains outside the insulation layer.
  • Integration of a high-performance vapor retarder to block interior moisture migration.
  • Audit of penetration seals around HVAC curbs and conduits to prevent localized vapor leaks.
  • Evaluation of the hygroscopic properties of the insulation board to manage incidental moisture.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
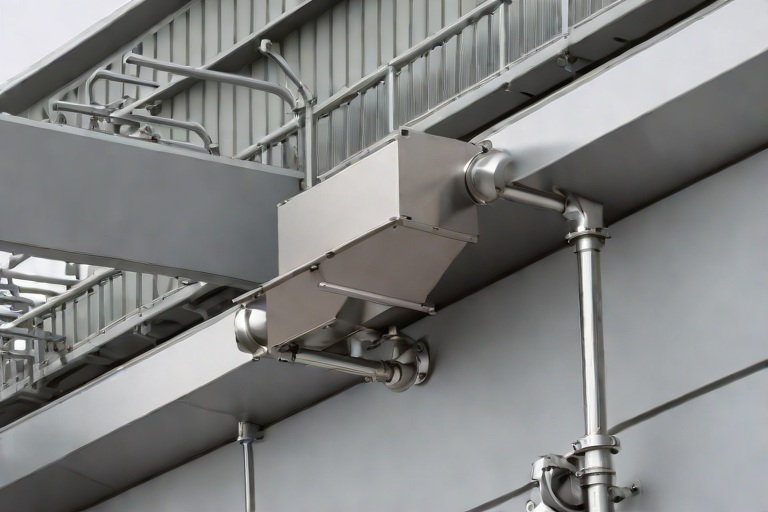
Commercial Engineering Dossier #751

Parapet Wall Heavy-Gauge 20-Gauge Kynar 500 Coping Cap Continuous Cleat Locking on Commercial Big-Box Retail Power Centers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Parapet Wall Heavy-Gauge 20-Gauge Kynar 500 Coping Cap Continuous Cleat Locking on Commercial Big-Box Retail Power Centers

Material Specification and Gauge Analysis for Large-Scale Retail Envelopes

In the context of Big-Box Retail Power Centers, the parapet wall serves as the primary defense mechanism for the building envelope. Most standard commercial specifications call for 24-gauge steel; however, for high-exposure retail environments, this is often insufficient. Our engineering audit specifies the utilization of 20-gauge heavy-gauge steel for the coping cap. The increased wall thickness provides the necessary structural rigidity to resist the harmonic vibrations and wind-induced fluttering common in large-span commercial structures. By increasing the gauge, we significantly reduce the risk of "oil-canning"—the visible waviness that occurs when thin-gauge metal is stressed—ensuring both aesthetic longevity and structural stability.

The selection of Kynar 500 (PVDF) coating is not merely an aesthetic choice but a material science requirement. In retail power centers, the coping cap is subjected to extreme UV radiation and atmospheric pollutants. Kynar 500 offers superior resin stability and chemical resistance compared to standard polyester coatings. This ensures that the protective layer does not degrade, crack, or chalk over a twenty-year lifecycle, maintaining the integrity of the steel substrate against oxidation and corrosion.

  • 20-Gauge Steel: Provides superior moment of inertia and resistance to deformation under wind load.
  • Kynar 500 Coating: High-performance fluoropolymer finish that prevents UV degradation and color fading.
  • Substrate Compatibility: Engineered to bond effectively with galvanized steel or aluminum cores.
  • Dimensional Stability: Reduced coefficient of expansion when compared to lighter gauge alternatives.

Continuous Cleat Engagement and ANSI/SPRI ES-1 Compliance

Wind uplift is the primary failure point for parapet coping. Traditional intermittent fastening methods often create "weak points" where wind pressure can initiate a peel-back effect. To mitigate this, we implement a continuous cleat locking system. This system utilizes a heavy-duty cleat that runs the entire length of the parapet, providing a constant mechanical lock between the coping cap and the wall substrate. This eliminates the reliance on isolated fasteners and distributes the wind load evenly across the entire perimeter of the building.

Our engineering standards align with ANSI/SPRI ES-1, the industry benchmark for wind uplift resistance. In a Big-Box retail environment, the "corner effect" creates high-velocity vortices that exert significant suction on the coping cap. By utilizing continuous cleat engagement, we ensure that the coping cap remains seated even during peak gust events. This mechanical interlocking prevents the metal from lifting, which in turn prevents the underlying roof membrane from being pulled away from the parapet wall, preserving the overall watertight integrity of the envelope.

  • Continuous Cleating: Eliminates localized stress concentrations by distributing wind loads linearly.
  • ANSI/SPRI ES-1 Adherence: Ensures the system is engineered for specific site-wind speeds and exposure categories.
  • Vortex Mitigation: Specifically addresses the high-pressure zones at the building corners.
  • Mechanical Interlock: Provides a redundant fail-safe against fastener shear or withdrawal.

Thermal Expansion and Splice Plate Engineering

One of the most overlooked aspects of commercial coping installation is the management of thermal expansion and contraction. A retail power center can have a parapet run extending several hundred linear feet. Because steel expands and contracts at a predictable rate based on temperature fluctuations, a rigid installation will inevitably lead to buckling or fastener failure. To solve this, we engineer specialized thermal expansion splice plates at calculated intervals along the parapet length.

These splice plates are not merely overlaps; they are precision-engineered sleeves that allow the metal to slide longitudinally while maintaining a weather-tight seal. We utilize a "floating" attachment method where one end of the coping section is fixed and the other is allowed to move within the splice plate. This prevents the buildup of internal stress within the 20-gauge steel, ensuring that the coping cap does not bow outward or pull away from the cleat during extreme temperature swings between winter and summer cycles.

  • Thermal Movement Calculation: Determining the exact expansion gap based on the coefficient of thermal expansion for 20-gauge steel.
  • Floating Splice Plates: Allowing for linear movement without compromising the water-shedding capability.
  • Stress Distribution: Preventing the "oil-canning" effect caused by constrained thermal growth.
  • Sealant Integration: Utilizing high-movement silicone sealants within the splices to maintain a vacuum-tight seal.

Perimeter Peel Mitigation and Envelope Integration

The final stage of the engineering audit focuses on perimeter peel mitigation. The most critical point of failure in a building envelope is the transition where the roof membrane meets the parapet wall. If the coping cap is not properly integrated, wind can get underneath the metal, creating a "parachute effect" that peels the coping and the membrane simultaneously. Our approach involves a comprehensive wrap-around technique, ensuring the membrane is fully adhered to the wall and then capped with the 20-gauge Kynar system.

By implementing a continuous cleat system combined with a heavy-gauge cap, we create a reinforced "lid" for the building. This prevents moisture infiltration from the top down and prevents wind-driven rain from penetrating the joint between the wall and the roof. The result is a monolithic envelope that protects the interior assets of the retail center. Our audit confirms that when the continuous cleat is engaged and the thermal splices are properly spaced, the risk of perimeter peel is reduced to near zero, significantly extending the mean time between repairs (MTBR).

  • Membrane Integration: Ensuring a seamless transition from the field membrane to the parapet wall.
  • Water-Shedding Geometry: Optimizing the slope of the coping cap to prevent ponding at the splice plates.
  • Edge Detail Reinforcement: Utilizing reinforced corners to eliminate the primary points of wind entry.
  • Envelope Continuity: Creating a closed-loop system that protects the building from both thermal and atmospheric stressors.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #752

Industrial Drainage Scuppers, Overflow Weirs & Heavy Downspout Expansion Bellows on Commercial Food Packaging & Cold Logistics Plants

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Industrial Drainage Scuppers, Overflow Weirs & Heavy Downspout Expansion Bellows on Commercial Food Packaging & Cold Logistics Plants

Hydraulic Head-Loss Analysis and Scupper Integration

In the engineering audit of a high-volume food packaging facility, the primary concern is the management of massive rainwater volumes across expansive, low-slope roof assemblies. When dealing with thousands of square feet of membrane, the risk of ponding is not merely an aesthetic issue but a structural threat. We begin our analysis with hydraulic head-loss calculations, which determine the pressure drop as water moves from the roof surface through the scupper and into the perimeter drainage system. In these facilities, we often encounter "dead spots" where the slope—even if designed at a 1/4" per foot minimum—fails to account for structural deflection over long spans.

To mitigate this, we implement a strategic scupper placement strategy that prioritizes the shortest path to the exterior. The head-loss is calculated by evaluating the friction loss within the scupper throat and the entrance loss where the water transitions from a sheet flow to a concentrated stream. For food-grade facilities, we must ensure that the scupper flashing is seamlessly integrated into the roof membrane to prevent capillary action, which could introduce moisture into the insulation layers and compromise the thermal envelope of the cold storage zones.

  • Calculation of the "C" coefficient for discharge to ensure the scupper can handle 100-year storm event intensities.
  • Evaluation of the weir flow formula to determine the exact depth of water required to trigger the scupper discharge.
  • Assessment of flashing integrity using ASTM E2127 shear tests to ensure the membrane-to-metal bond remains watertight under thermal stress.
  • Analysis of the roof's "sump" areas to prevent stagnant water from infiltrating the building's interior via osmotic pressure.

Emergency Overflow Weir Sizing and Safety Factors

A critical failure point in commercial drainage is the reliance on primary internal drains. In a cold logistics plant, where roof debris or ice buildup can rapidly occlude primary drains, the emergency overflow weir serves as the final line of defense against structural collapse. An improperly sized weir can lead to "ponding-induced deflection," where the weight of the water causes the roof to sag, creating more ponding in a catastrophic feedback loop. Our engineering approach treats the overflow weir as a safety valve, sized to discharge the same volume as the primary system but at a slightly higher elevation.

The sizing of these weirs is governed by the principle of the "overflow height." We typically set the overflow weirs 2 inches above the finished roof surface. This ensures that the primary drains are utilized first, but if they fail, the water exits the building before it reaches a critical depth that would exceed the dead load capacity of the steel decking. We utilize a safety factor of 1.5x the calculated peak rainfall intensity to account for unpredictable weather patterns and potential partial obstructions in the overflow path.

  • Utilization of the Francis Formula for calculating flow over a rectangular weir.
  • Verification that overflow discharge points are positioned to avoid dumping water directly onto pedestrian walkways or loading docks.
  • Implementation of "scupper-to-conductor" transitions that prevent back-pressure from slowing the discharge rate.
  • Coordination with structural engineers to ensure the roof joists can support the temporary weight of water up to the weir crest.

Conductor Head Engineering and Vortex Mitigation

The transition from the roof surface to the vertical downspout is where most drainage systems fail due to turbulence and splashing. In a food packaging plant, splashing is not just a maintenance nuisance; it can lead to the degradation of the building's facade and the infiltration of moisture into the wall cavity. We employ oversized conductor heads designed to act as a plenum, slowing the velocity of the incoming water and allowing it to enter the downspout in a more laminar flow. This reduces the "vortex effect," which can otherwise create a vacuum that slows the overall drainage rate.

From a material science perspective, we specify heavy-gauge galvanized steel or stainless steel for conductor heads to resist the corrosive effects of industrial cleaning agents often used in food plants. The geometry of the head is critical; a deep-sump conductor head prevents the "geysering" effect during heavy downpours, where water is forced back up and over the roof edge. We ensure that the connection between the conductor head and the downspout is reinforced with heavy-duty straps to prevent vibration-induced fatigue at the connection points.

  • Engineering of the "splash-guard" radius to ensure water is directed inward and downward.
  • Application of high-performance coatings to prevent oxidation in high-humidity cold logistics environments.
  • Analysis of flow velocity to prevent the "choking" of the downspout during peak hydraulic load.
  • Integration of debris screens that are easily accessible for quarterly maintenance without compromising the seal.

Thermal Expansion Bellows and Material Science

Cold logistics plants present a unique engineering challenge: the extreme temperature differential between the freezer interiors (often -10°F) and the roof surface (which can reach 150°F under direct summer sun). This creates massive thermal movement in the vertical drainage piping. If the downspouts are rigidly attached from the roof to the grade, the resulting thermal expansion and contraction will inevitably tear the roof membrane or buckle the piping. To solve this, we integrate heavy-duty expansion bellows and slip joints into the downspout assembly.

These bellows are engineered using a combination of stainless steel and reinforced elastomers, allowing the pipe to expand and contract axially without transferring the load to the roof's flashing. We follow ANSI standards for piping expansion to determine the exact placement of these joints. By installing a slip joint every 30 feet of vertical run, we neutralize the thermal stress. This prevents the "jacking" effect, where the pipe attempts to push itself out of the roof penetration, which is a common cause of leaks in cold-chain facilities.

  • Calculation of the linear expansion coefficient for the specific alloy of steel used in the downspouts.
  • Installation of bellows with a minimum movement capacity of 2 inches per 50 feet of vertical run.
  • Use of non-rigid mounting brackets that allow for lateral movement while maintaining structural stability.
  • Verification of the seal between the expansion joint and the pipe to ensure no leakage occurs during the contraction phase.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #753

AOC 581 Elastomeric Structural Mastic Detailing Around Rooftop HVAC Curbs on Commercial Semiconductor Cleanroom Fabs

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
AOC 581 Elastomeric Structural Mastic Detailing Around Rooftop HVAC Curbs on Commercial Semiconductor Cleanroom Fabs

The Engineering Challenge of Semiconductor Fab Envelopes

In the high-stakes environment of semiconductor fabrication, the building envelope is not merely a shelter but a critical component of the facility's primary containment system. A cleanroom fab operates under stringent atmospheric controls where even a microscopic breach in the roof membrane can introduce contaminants or moisture, potentially compromising millions of dollars in silicon wafers. The most vulnerable points in these massive industrial footprints are the rooftop HVAC curbs. These penetrations represent a complex intersection of different materials—typically galvanized steel curbs meeting a high-performance TPO or PVC membrane—creating a high-stress transition zone.

The primary engineering hurdle is the sheer scale of the equipment. Semiconductor fabs require massive air handling units (AHUs) to maintain positive pressure and precise temperature gradients. These units exert immense static loads on the curbs, while the surrounding roof field is subject to significant wind uplift and hydrostatic pressure during storm events. Standard flashing techniques often fail in these environments because they lack the necessary elasticity to handle the differential movement between the rigid HVAC curb and the flexible roof membrane.

  • Substrate incompatibility between metallic curb flashing and synthetic roof membranes.
  • High-frequency vibrations from industrial-grade blowers and compressors.
  • Extreme thermal cycling of the roof surface leading to material fatigue.
  • The requirement for zero-leakage tolerance to protect cleanroom ISO standards.

Mitigating Mechanical Vibration and Thermal Expansion Drift

From a building envelope perspective, the HVAC curb is a site of constant kinetic energy. The mechanical vibration produced by heavy-duty HVAC equipment creates micro-oscillations that can lead to "fretting" or the gradual breakdown of traditional adhesives and sealants. Over time, these vibrations cause a mechanical decoupling of the flashing from the curb, creating hairline fractures that allow water to migrate via capillary action into the building interior.

Furthermore, the coefficient of thermal expansion differs wildly between the steel curb and the roof membrane. As the fab roof heats under direct solar radiation, the membrane expands and contracts, a phenomenon known as thermal drift. If the sealant is too rigid, it will tear; if it is too soft, it will slump and lose its seal. The application of AOC 581 Elastomeric Structural Mastic is engineered to solve this by providing a high-elongation bridge. Its elastomeric properties allow the material to stretch and recover, absorbing the energy of the vibration and the drift of the thermal cycle without sacrificing the bond to the substrate.

  • Utilization of high-modulus elastomeric polymers to dampen mechanical resonance.
  • Implementation of flexible transition zones to accommodate longitudinal and lateral thermal drift.
  • Reduction of stress concentrations at the 90-degree angles of the curb corners.
  • Prevention of adhesive failure through the use of chemically compatible primers.

Advanced Application: Fiber-Reinforced Trowel Techniques

The efficacy of AOC 581 is not solely dependent on its chemical composition but on the precision of its application. A master roofer knows that a simple brush-on application is insufficient for structural detailing. Instead, we employ a fiber-reinforced trowel technique. This process involves the integration of non-woven reinforcement fabrics embedded directly into the mastic. By "sandwiching" the reinforcement between two layers of AOC 581, we create a composite structural seal that mimics the strength of a reinforced concrete slab but retains the flexibility of a rubberized membrane.

The trowel application must be executed with a specific focus on the "wet-on-wet" technique to ensure a monolithic bond. The first layer is applied to the curb and the roof deck, extending at least six inches beyond the flashing edge. While the mastic is still open, the reinforcement fabric is embedded, removing all air pockets and wrinkles. The final cap layer is then troweled over the fabric, ensuring a seamless, air-tight, and water-tight transition. This fiber-reinforcement prevents the "bridging" effect where a sealant pulls away from a corner during a cold-weather contraction.

  • Detailed substrate preparation including solvent cleaning and mechanical abrasion for maximum adhesion.
  • Strategic placement of reinforcement fabric to reinforce high-stress corner geometries.
  • Precision troweling to ensure a uniform mil thickness across the entire transition zone.
  • Application of a UV-stable topcoat to protect the elastomeric mastic from premature degradation.

Final Audit and Watertight Seal Verification

The final stage of the engineering process is a rigorous building envelope audit. In a semiconductor fab, "visual inspection" is an insufficient metric for quality assurance. We employ a multi-tiered verification process based on ASTM and ANSI standards to ensure the integrity of the AOC 581 installation. This begins with a comprehensive pull-test to verify the bond strength of the mastic to the galvanized steel and the roof membrane, ensuring that the failure point is the substrate itself rather than the adhesive interface.

Following the bond test, we conduct a targeted flood test or a vacuum leak detection test around the perimeter of the HVAC curbs. By applying a controlled amount of hydrostatic pressure, we can verify that the fiber-reinforced seal is completely impervious to water ingress. The goal is to achieve a seamless transition where the curb becomes an integrated part of the roof's waterproof skin. This holistic approach to detailing ensures that the facility remains operational and the cleanroom environment remains pristine, regardless of external weather extremes or internal mechanical stresses.

  • Adherence to ASTM E2128 for the evaluation of roof membrane penetrations.
  • Verification of sealant shore hardness to ensure the balance between flexibility and durability.
  • Long-term monitoring of the "bead" integrity to detect any signs of premature shrinkage.
  • Final certification of the building envelope as a continuous, unbroken moisture barrier.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #754

UL 2218 Class 4 Severe Hail Defense on Commercial Intermodal Cargo Freight Terminals

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
UL 2218 Class 4 Severe Hail Defense on Commercial Intermodal Cargo Freight Terminals

The Critical Vulnerability of Intermodal Logistics Hubs

In the realm of commercial building envelope engineering, intermodal cargo freight terminals represent one of the most challenging environments for roof system longevity. These facilities are characterized by massive footprints, often exceeding several hundred thousand square feet, which creates a vast target for severe convective weather events. Unlike standard warehouse structures, intermodal hubs are subject to extreme vibration from heavy machinery and constant thermal cycling, which can fatigue a roofing membrane over time. When severe hail events occur, the primary risk is not merely a surface puncture, but the systemic failure of the envelope's integrity.

A failure in a freight terminal is not a localized issue; it is a catastrophic operational risk. A single breach in the membrane can lead to moisture infiltration that damages high-value cargo, compromises electrical systems, and disrupts the logistics chain. From a master roofer's perspective, the goal is to transition the roof from a passive covering to an active defense system. This requires a shift in focus from simple waterproofing to a comprehensive analysis of impact physics and material science.

  • Exposure Analysis: Evaluating the frequency and intensity of hailstone diameters in the specific geographic region of the terminal.
  • Structural Load Considerations: Assessing how the roof deck handles the sudden, concentrated load of a severe storm.
  • Operational Downtime Costs: Calculating the financial impact of emergency repairs versus the investment in a Class 4 rated system.
  • Thermal Expansion: Managing the movement of large-scale roof sections to prevent seam separation during temperature swings.

Kinetic Energy Attenuation and UL 2218 Class 4 Standards

To achieve a true severe hail defense, we must look beyond the surface membrane and analyze the kinetic energy attenuation of the entire assembly. UL 2218 is the industry benchmark for hail resistance, and achieving a Class 4 rating means the system has undergone rigorous testing to ensure it can withstand the impact of large ice spheres without significant degradation. The physics of a hail strike involve a massive amount of kinetic energy being transferred into a very small surface area in a fraction of a second. If the roofing system is too rigid, the energy causes a brittle fracture; if it is too soft, the hailstone simply punches through.

Effective attenuation is achieved through a layered approach where each component of the building envelope absorbs a portion of the impact energy. This process, known as energy dissipation, prevents the force from concentrating on a single point of the membrane. By utilizing high-performance polymers and reinforced membranes, we can ensure that the impact energy is spread across a wider area of the substrate, thereby reducing the likelihood of a puncture. This engineering approach transforms the roof into a shock absorber, protecting the interior of the facility from the elements.

  • Impact Distribution: Utilizing reinforced membranes that distribute point-loads across the underlying insulation.
  • Material Elasticity: Selecting polymers with a high modulus of elasticity to allow for momentary deformation without permanent rupture.
  • UL 2218 Testing Protocols: Implementing systems that have been verified through standardized steel-ball impact tests.
  • Surface Tension Management: Reducing the friction and impact force through advanced membrane coatings.

Substrate Integrity and the 25 PSI Compressive Strength Threshold

The most overlooked component of hail defense is the insulation core. Many commercial roofers make the mistake of focusing solely on the top membrane, ignoring the fact that the membrane is only as strong as the support beneath it. In an engineering audit of a freight terminal, we specifically examine the compressive strength of the insulation. To prevent "bottoming out"—where the hailstone pushes the membrane all the way down to the metal deck—the insulation must possess a compressive strength exceeding 25 PSI (pounds per square inch).

When a high-velocity hailstone strikes, it creates a momentary depression in the roof. If the insulation is too soft, such as low-density foams, the insulation collapses under the pressure, and the membrane is forced against the hard steel decking. This "anvil effect" is what typically causes the membrane to split. By specifying high-density polyisocyanurate (Polyiso) or specialized composite cores with a 25 PSI+ rating, we provide a rigid enough platform to support the membrane while still allowing for the necessary thermal attenuation. This ensures that the insulation core absorbs the vertical displacement rather than the membrane taking the full force of the impact.

  • Core Density Analysis: Verifying that the insulation density is consistent across the entire roof plane to avoid soft spots.
  • Anvil Effect Mitigation: Ensuring a sufficient gap or cushioning layer exists between the insulation and the structural deck.
  • Load-Bearing Capacity: Calculating the maximum impact force of a 2-inch hailstone to ensure the 25 PSI threshold is sufficient.
  • Thermal Bridging Prevention: Balancing high compressive strength with the necessary R-value for energy efficiency.

Engineering Audit and Lifecycle Defense Strategy

A master-level building envelope audit does not end with the installation of materials; it begins with a lifecycle defense strategy. For intermodal terminals, this involves a proactive schedule of infrared thermography and moisture scanning to identify subsurface anomalies before they become failure points. The goal is to maintain the "envelope" as a singular, monolithic unit. We analyze the transition points—such as curbs, drains, and parapet walls—where hail-driven rain is most likely to penetrate if the primary membrane has been compromised by impact.

The long-term success of a UL 2218 Class 4 system depends on the synergy between the membrane, the adhesive, and the substrate. We employ a rigorous quality control process that includes pull-tests for adhesives and seam integrity audits. By treating the roof as a piece of critical infrastructure rather than a simple building component, we extend the service life of the asset and significantly reduce the total cost of ownership. The integration of high-compressive strength cores and kinetic energy attenuators ensures that the terminal remains operational even after the most severe weather events.

  • Infrared Thermography: Detecting trapped moisture and insulation voids that could weaken the compressive strength of the system.
  • Seam Integrity Audits: Utilizing vacuum testing to ensure that hail-induced vibrations have not compromised the welds.
  • Drainage Optimization: Ensuring that the roof can shed water rapidly after a storm to prevent hydrostatic pressure on the membrane.
  • Lifecycle Cost Analysis: Comparing the upfront cost of Class 4 materials against the avoided costs of emergency repairs and business interruption.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #755

Non-Destructive Substrate Moisture Scans on Commercial Port Marine Shipping Warehouses

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Non-Destructive Substrate Moisture Scans on Commercial Port Marine Shipping Warehouses

The Marine Interface and Substrate Vulnerability

In the high-stakes environment of port marine shipping warehouses, the building envelope is under constant assault from a combination of salt-laden aerosols, extreme wind-driven rain, and relentless thermal cycling. These structures typically feature massive footprints with complex drainage systems, often utilizing a combination of reinforced concrete decks or corrugated steel decking topped with rigid polyisocyanurate or mineral wool insulation. The primary engineering challenge in these environments is not the identification of a visible leak, but the detection of subsurface saturation that occurs long before a ceiling stain appears.

When the primary roofing membrane—whether it be a modified bitumen, TPO, or PVC system—suffers a breach, moisture does not simply pool; it migrates. Due to the hygroscopic nature of certain insulation materials and the capillary action inherent in layered assemblies, water travels laterally across the substrate. This creates a "hidden" saturation zone that can extend several feet beyond the actual point of entry. In a marine warehouse, this is exacerbated by the high humidity of the coastal atmosphere, which slows the evaporation rate of the substrate, effectively locking moisture into the insulation and promoting the oxidation of the structural steel deck below.

  • Atmospheric salt deposition which accelerates the corrosion of metal fasteners and flashing.
  • Hydrostatic pressure buildup during extreme storm surges or heavy precipitation events.
  • Thermal bridging at parapet walls and curb details that creates localized condensation.
  • The failure of edge metal flashing, allowing wind-driven rain to enter the insulation core.

Non-Destructive Moisture Detection and Saturation Mapping

To avoid the prohibitive cost and operational disruption of a full-scale roof tear-off, we employ Non-Destructive Moisture Detection (NDMD) protocols. The objective is to establish a precise "wet footprint" by identifying the boundaries of subsurface saturation. This process begins with high-resolution Infrared (IR) Thermography. Because water has a higher thermal mass than dry insulation, saturated areas retain heat longer or cool more slowly, appearing as thermal anomalies on the IR scan. This allows our engineering team to map the temperature differentials across the warehouse roof, isolating areas of suspected moisture accumulation.

However, IR scans only provide a surface-level thermal signature. To validate these findings, we utilize electronic moisture meters and dielectric constant sensors. These tools measure the permittivity of the substrate, allowing us to differentiate between surface condensation and deep-seated saturation. By plotting these data points on a CAD overlay of the roof plan, we create a saturation boundary map. This map serves as the definitive guide for the engineering audit, ensuring that we are not guessing where the water is, but rather quantifying the exact volume and location of the compromised substrate.

  • Infrared thermography to identify thermal anomalies and moisture plumes.
  • Dielectric constant sensing to determine the moisture content of rigid foam insulation.
  • Moisture mapping to establish the precise perimeter of the saturation zone.
  • Comparative analysis of thermal signatures against known structural anomalies.

Validation via Core Sampling and Material Science

While NDMD provides the map, core sampling provides the "ground truth." A master-level engineering audit requires the physical extraction of substrate cores to validate the moisture thresholds identified during the scanning phase. We utilize a precision core drill to extract samples from both the "hot" zones (identified as wet) and the "cold" zones (identified as dry). This comparative analysis is critical to ensure that the NDMD equipment is calibrated correctly for the specific density and material composition of the warehouse roof.

Once extracted, the cores are analyzed for moisture content using the oven-dry method, adhering to ASTM standards for material testing. We examine the core for signs of biological growth, chemical degradation of the insulation, and the presence of "rust-jacking" on the steel deck. If the moisture content exceeds the established threshold—typically 20% to 30% for polyisocyanurate—the insulation is deemed failed. This is because saturated insulation loses its R-value and, more importantly, becomes a conduit for further water migration, potentially compromising the structural integrity of the building envelope through accelerated corrosion of the decking.

  • ASTM-compliant core extraction to verify subsurface moisture percentages.
  • Oven-dry mass analysis to determine the exact water-to-solid ratio of the insulation.
  • Visual inspection of the steel deck for pitting, scaling, and oxidation.
  • Validation of the "dry line" to ensure the saturation boundary is accurately mapped.

Surgical Excision and Envelope Restoration

The final phase of the engineering process is the surgical excision of wet insulation. Rather than employing a "blanket" replacement strategy, which is wasteful and costly, we use the saturation map to perform precision cuts. By removing only the compromised material, we minimize the impact on the warehouse's operations and reduce the volume of debris. This surgical approach involves cutting the membrane and insulation in a grid pattern based on the moisture boundaries, ensuring that we reach the "dry line" where the substrate returns to its original specification.

Once the wet insulation is removed, the substrate is mechanically cleaned and treated with a corrosion inhibitor if the steel deck shows signs of oxidation. New, high-density insulation is then installed and tapered to ensure positive drainage, eliminating the ponding water issues that likely caused the initial failure. The final seal is achieved through a reinforced flashing detail at the transition points, ensuring a seamless, watertight envelope. This systematic approach—from non-destructive scanning to surgical repair—represents the pinnacle of commercial roofing craftsmanship, blending material science with precision engineering to extend the lifecycle of critical marine infrastructure.

  • Precision cutting of the membrane based on the validated moisture map.
  • Mechanical cleaning and priming of the structural deck to prevent future oxidation.
  • Installation of new insulation boards with staggered joints to prevent thermal leaking.
  • Application of a high-performance, UV-resistant membrane with reinforced flashing.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #756

Sub-Zero Cold Storage Downward Vapor Drive & Self-Adhered SBS Barriers on Commercial Municipal Sports & Convention Arenas

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Sub-Zero Cold Storage Downward Vapor Drive & Self-Adhered SBS Barriers on Commercial Municipal Sports & Convention Arenas

The Physics of Inverted Thermal Envelopes and Downward Vapor Drive

In the engineering of municipal sports and convention arenas, the integration of sub-zero cold storage facilities creates a high-stakes hygrothermal challenge. Unlike standard commercial warehouses, these arenas feature massive internal volumes with fluctuating humidity levels, while the cold storage zones maintain extreme temperature differentials. This creates a powerful downward vapor drive, where moisture-laden air from the ambient arena environment attempts to migrate toward the sub-zero thermal mass of the cold storage units. When the thermal envelope is inverted or improperly sequenced, this vapor drive forces moisture deep into the roof assembly.

The primary risk in these scenarios is interstitial condensation. As warm, moist air penetrates the outer layers of the roof, it eventually reaches a temperature equal to its dew point. If this occurs within the insulation layers rather than on a controlled vapor barrier, the moisture liquefies and becomes trapped. In a sub-zero environment, this moisture can freeze and thaw repeatedly, leading to the degradation of the insulation's R-value and the eventual corrosion of the structural steel decking. A master-level audit of these systems reveals that the failure is rarely the membrane itself, but rather the failure to manage the pressure-driven movement of water vapor through the assembly.

  • Hygrothermal Pressure: The movement of water vapor from areas of high partial pressure to low partial pressure.
  • Thermal Bridging: Localized areas of high heat transfer that create "cold spots" where condensation is most likely to occur.
  • Vapor Drive Directionality: The specific vector of moisture movement dictated by the temperature gradient between the arena interior and the cold storage interior.
  • Interstitial Condensation: Moisture that accumulates within the layers of the building envelope rather than on the surface.

Dew Point Migration and Staggered Multi-Layer Polyisocyanurate

To combat the downward vapor drive, the engineering specification must prioritize the manipulation of the dew point. The goal is to ensure that the dew point occurs outside the structural deck and the primary waterproofing layer. This is achieved through the strategic application of high-density polyisocyanurate (polyiso) insulation. However, the efficacy of polyiso is not found in the material alone, but in the installation geometry. Standard single-layer installation creates linear pathways—essentially "vapor highways"—at every board joint, allowing moisture to bypass the thermal resistance of the foam.

The professional standard for high-performance arenas is the implementation of staggered multi-layer polyiso. By installing insulation in two or more layers with offset joints, we effectively break the continuity of the vapor path. This forced "tortuous path" increases the effective resistance to vapor migration and ensures that any moisture that does penetrate the first layer is halted or redirected before it reaches the critical structural interface. This method transforms the insulation from a simple thermal blanket into a functional component of the vapor management system.

  • Joint Offset Requirements: Ensuring that vertical and horizontal seams between layers do not align, typically requiring a minimum 12-inch offset.
  • R-Value Optimization: Calculating the total thermal resistance required to keep the structural deck temperature above the dew point.
  • Compression Strength: Utilizing high-density polyiso to withstand the static loads of arena roofing equipment without compromising the thermal break.
  • Thermal Bridging Mitigation: Reducing the use of metal fasteners that can act as conduits for heat and moisture.

Engineering Self-Adhered SBS Modified Bitumen Barriers

The final line of defense in a sub-zero cold storage envelope is the selection of the waterproofing membrane. For municipal arenas, where structural movement and thermal expansion are constant, a self-adhered SBS (Styrene-Butadiene-Styrene) modified bitumen barrier is the superior engineering choice. Unlike torch-applied systems, which introduce extreme heat and potential voids, or liquid-applied membranes, which can suffer from inconsistent thickness, self-adhered SBS provides a monolithic, factory-controlled thickness and a consistent bond across the entire substrate.

The material science of SBS modification allows the bitumen to remain flexible at extremely low temperatures, preventing the membrane from becoming brittle and cracking under the stress of the arena's thermal cycles. The self-adhering nature of the barrier ensures a full-bond installation, which is critical for eliminating air pockets. These pockets, if left untreated, can act as reservoirs for condensed moisture, leading to localized "blistering" and eventual membrane failure. By creating a seamless, airtight seal, the SBS barrier effectively shuts down the vapor drive at the outermost boundary.

  • Elastomeric Properties: The ability of SBS to stretch and recover, accommodating the expansion and contraction of a large-scale municipal roof.
  • Full-Bond Adhesion: Eliminating the "gap" between the membrane and the insulation to prevent the lateral migration of water.
  • ASTM Standard Compliance: Adhering to rigorous testing for puncture resistance and water permeability.
  • Cold-Weather Application: The capacity for the membrane to maintain adhesive properties during the installation phase in unheated environments.

Audit Findings and Long-Term Envelope Integrity

A comprehensive engineering audit of these systems requires a forensic approach to the building envelope. The focus is not merely on the surface appearance of the roof, but on the integrity of the entire assembly from the interior cold storage wall to the exterior roof membrane. In many failed arena systems, audits reveal that the "vapor barrier" was treated as a single product rather than a continuous system. The most common points of failure are the penetrations—HVAC curbs, drainage pipes, and structural columns—where the transition from the horizontal roof to the vertical wall occurs.

To ensure long-term integrity, the envelope must be treated as a singular, unbroken skin. This requires meticulous detailing at the perimeters and the use of compatible flashing materials that match the thermal expansion coefficient of the SBS barrier. When the staggered polyiso, the self-adhered SBS, and the interior vapor retarders are synchronized, the result is a high-performance envelope that protects the structural assets of the municipality and ensures the operational efficiency of the sub-zero storage facilities.

  • Infrared Thermography: Utilizing thermal imaging to identify "wet" insulation and pinpoint areas of thermal leakage.
  • Perimeter Detailing: Ensuring that the transition from the roof deck to the parapet wall is airtight and vapor-sealed.
  • Moisture Site Surveys: Conducting core samples of insulation to verify the absence of interstitial condensation.
  • Lifecycle Analysis: Evaluating the degradation rate of the SBS membrane against the projected lifespan of the arena's mechanical systems.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #757

Structural Deck Fastener Pull-Out Testing on 22-Gauge Corrugated Steel Decks on Commercial Multi-Family Urban Residential Towers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Structural Deck Fastener Pull-Out Testing on 22-Gauge Corrugated Steel Decks on Commercial Multi-Family Urban Residential Towers

Substrate Analysis and the Engineering Audit Framework

In the high-stakes environment of urban multi-family residential towers, the building envelope is the primary line of defense against catastrophic moisture intrusion and structural failure. For this specific engineering audit, the focus was centered on 22-gauge corrugated steel decking, a common substrate that serves as both the structural floor and the base for the roofing assembly. The integrity of the entire system relies on the mechanical bond between the fasteners and this steel substrate. A failure in the fastener-to-deck connection does not merely result in a leak; it can lead to a progressive failure of the membrane under extreme wind-uplift pressures, potentially compromising the safety of the building's occupants.

The audit began with a comprehensive substrate evaluation to ensure the 22-gauge steel had not suffered from significant oxidation or fatigue. In urban environments, atmospheric pollutants and salt-laden air can accelerate the degradation of the galvanized coating on the steel deck. Our team analyzed the gauge thickness using digital calipers to verify that the material met the specified engineering requirements, as any thinning of the steel—whether from manufacturing tolerances or corrosion—directly reduces the available "bite" for the fastener threads, thereby lowering the overall withdrawal resistance.

  • Verification of steel gauge consistency across the primary and perimeter zones.
  • Assessment of the corrugation profile to ensure alignment with fastener specifications.
  • Evaluation of existing membrane adhesion and its impact on fastener accessibility.
  • Mapping of the structural diaphragm to identify high-stress concentration points.
  • Inspection for galvanic corrosion at the interface of dissimilar metals.

Calibrated Mechanical Pull Testing Methodology

To quantify the actual holding power of the fasteners, we employed calibrated mechanical pull testing, a process that removes the guesswork from building envelope audits. This procedure involves the use of a digital force gauge and a specialized pull-tester designed to apply a linear, axial load to the fastener head. Unlike static load tests, calibrated pull testing allows the engineer to observe the behavior of the fastener in real-time, identifying the exact point of initial movement—known as the "slip" point—and the ultimate point of failure. This data is critical for determining if the installation meets the minimum withdrawal resistance thresholds required by the project's structural specifications.

The testing protocol followed a rigorous sampling schedule, targeting the most vulnerable areas of the roof, specifically the perimeter and corner zones where wind-uplift forces are most acute. Each test was conducted by isolating a single fastener and applying a gradual increase in tension. This method ensures that the results are a true reflection of the fastener's engagement with the 22-gauge steel, rather than a result of the surrounding membrane's tension. By adhering to ASTM standards for strength of fasteners, we were able to establish a statistically significant baseline for the tower's overall structural health.

  • Utilization of digital force gauges calibrated to within 0.1% accuracy.
  • Implementation of a randomized sampling grid to avoid selection bias.
  • Application of axial loading to prevent premature shear failure.
  • Recording of peak load values prior to the onset of substrate deformation.
  • Comparison of field results against laboratory-controlled baseline data.

Analysis of Withdrawal Resistance and Failure Modes

The core of the engineering analysis lies in the withdrawal resistance—the maximum force a fastener can withstand before it is pulled out of the substrate. For 22-gauge corrugated steel, the threshold is precarious because the material is thin enough that the threads have a limited amount of steel to grip. Our findings indicated that the minimum withdrawal resistance must exceed the calculated wind-uplift load by a safety factor of at least 1.5. When the pull-test results fell below this threshold, it indicated a failure in either the fastener selection or the installation technique, such as over-torquing, which can strip the threads of the steel deck.

Understanding the failure mode is as important as the load value itself. We categorized failures into three distinct types: thread stripping, head pull-through, and substrate deformation. Thread stripping occurs when the fastener's threads shear through the 22-gauge steel, often a result of using a fastener with a pitch that is too aggressive for the gauge. Head pull-through occurs when the fastener head is pulled through the roofing membrane or the steel itself, indicating a failure in the washer size or the clamping force. Substrate deformation, where the steel deck bends without the fastener releasing, suggests that the fastener is performing well, but the deck itself may be under-specified for the loads.

  • Calculation of the "pull-out" force versus the "shear" force for each fastener type.
  • Analysis of the engagement depth to ensure full penetration of the corrugated ribs.
  • Evaluation of the "slip" threshold to determine the stability of the roofing system.
  • Assessment of the impact of fastener spacing on the overall load distribution.
  • Correlation of failure modes with specific installation crews or batches of hardware.

Corrosion Diagnostics and Wind-Zone Schedules

In urban residential towers, the "wind tunnel" effect created by surrounding skyscrapers creates erratic and intense pressure differentials. This necessitates a strict adherence to wind-zone schedules, which dictate a higher density of fasteners in the perimeter and corner zones (Zones 2 and 3) compared to the interior field (Zone 1). Our audit revealed that while the interior of the roof met the resistance thresholds, several perimeter sections were under-fastened, leaving them vulnerable to "peeling" during a high-wind event. The engineering recommendation was an immediate increase in fastener density in these critical zones to distribute the uplift load more evenly across the 22-gauge deck.

Concurrent with the mechanical testing, we performed corrosion diagnostics to evaluate the long-term viability of the fasteners. We looked for evidence of "white rust" (zinc oxidation) and "red rust" (base metal oxidation), which can significantly reduce the cross-sectional area of the fastener and, consequently, its shear strength. The use of fasteners with incompatible coatings on a galvanized steel deck can lead to galvanic corrosion, where the more anodic metal sacrifices itself, leading to rapid degradation of the connection. We mandated the use of high-performance ceramic or zinc-aluminum coatings to ensure that the chemical bond remains intact for the duration of the building's lifecycle.

  • Mapping of wind-uplift pressures based on ASCE 7 standards for urban environments.
  • Implementation of

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #758

Electronic Vector Mapping (EVM) Low-Voltage Membrane Breach Detection on Commercial Public Transit Maintenance Bus Barns

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Electronic Vector Mapping (EVM) Low-Voltage Membrane Breach Detection on Commercial Public Transit Maintenance Bus Barns

The Structural Vulnerabilities of Public Transit Maintenance Facilities

Public transit maintenance bus barns represent some of the most challenging environments for building envelope integrity. These facilities are characterized by massive footprints, expansive single-slope or low-slope roof geometries, and extreme internal atmospheric volatility. The primary engineering challenge stems from the constant cycling of heavy-duty diesel and electric vehicles, which introduces significant thermal plumes and particulate matter that can degrade membrane surfaces over time. Furthermore, the sheer scale of these roofs makes them susceptible to subtle structural deflections and seismic vibrations that can stress the seams of a traditional thermoplastic or modified bitumen system.

In a standard commercial audit, we often find that traditional leak detection methods—such as flood testing or infrared thermography—are insufficient for the rigorous demands of a transit hub. Flood testing is inherently destructive and time-consuming, often introducing more moisture into the substrate than the original leak. Infrared scanning, while useful, requires a significant temperature differential to be effective and often fails to identify "slow-bleed" pinholes that only activate during peak precipitation events. For a facility housing millions of dollars in diagnostic equipment and fleet assets, a "wait and see" approach to moisture ingress is a catastrophic failure of asset management.

  • Thermal cycling induced by high-bay heating and cooling systems.
  • Mechanical vibration from heavy vehicle movement affecting flashing attachments.
  • Atmospheric pollutants and exhaust particulates accelerating chemical degradation of the membrane.
  • The "large-surface-area" paradox where a single microscopic breach can lead to systemic substrate rot.

Mechanics of Electronic Vector Mapping (EVM) and Conductive Grids

To solve the problem of invisible breaches, Aquashield Corporate utilizes Electronic Vector Mapping (EVM). This is not a mere diagnostic tool but a comprehensive engineering system integrated into the building envelope. The foundation of EVM is a conductive underlayment—a specialized vector grid installed beneath the primary waterproofing membrane. This grid acts as a low-voltage electrical field, creating a continuous "electronic skin" across the entire roof surface. By applying a controlled, low-voltage current, we establish a baseline of electrical resistance across the membrane's dielectric barrier.

When the integrity of the upper membrane is compromised, even by a puncture invisible to the naked eye, the dielectric properties of the system change. If moisture penetrates the membrane and reaches the conductive grid, it creates a localized short-circuit or a change in resistance at that specific coordinate. The EVM system detects this anomaly instantly. Because the grid is mapped to a precise X-Y coordinate system, the software can triangulate the exact location of the breach within a matter of centimeters. This eliminates the need for "exploratory" cutting of the membrane, which often introduces more leaks than it solves.

  • Installation of a conductive copper or carbon-based vector grid as a secondary barrier.
  • Application of a high-dielectric strength membrane to isolate the electrical field.
  • Real-time monitoring of Ohmic resistance across the roof plane.
  • Triangulation of moisture ingress points via low-voltage signal attenuation.

Pinpointing Microscopic Punctures and Material Science

From a master roofer's perspective, the most dangerous leaks are not the obvious tears but the microscopic pinhole punctures. These often occur during the installation phase—perhaps a stray piece of debris trapped under a heat-welded seam or a microscopic void in the polymer matrix. Under the pressure of hydrostatic loading during a heavy rain event, these pinholes act as capillary conduits, drawing water deep into the insulation layers via capillary action. By the time a leak is visible on the interior ceiling of a bus barn, the roof deck is often already saturated, leading to corrosion of structural steel and the growth of mold within the insulation.

The EVM system treats the roof as a giant circuit board. By adhering to ASTM and ANSI standards for membrane thickness and dielectric consistency, we can differentiate between a superficial scratch and a full-thickness breach. The material science here relies on the fact that water is a polar molecule and a conductor. When a droplet penetrates a pinhole, it bridges the gap between the atmosphere and the conductive grid, triggering a vector alert. This allows our engineering team to perform "surgical" repairs, applying targeted reinforcements without compromising the surrounding membrane's thermal bond.

  • Identification of "cold-joint" failures in heat-welded TPO or PVC membranes.
  • Detection of puncture points caused by HVAC equipment vibration and fastener migration.
  • Analysis of dielectric breakdown in areas of high chemical exposure.
  • Prevention of interstitial condensation by identifying breaches before saturation occurs.

Non-Destructive Certification and Lifecycle ROI

The final phase of the Aquashield audit is the non-destructive quality certification. In the past, a "certified" roof was one that didn't leak during a 24-hour water test. In the modern engineering paradigm, we replace "hope" with "data." EVM allows us to provide a digital birth certificate for the roof envelope. We can certify that 100% of the surface area is electronically sealed, providing the facility owner with a verifiable map of the envelope's integrity. This is a non-destructive process; we are not adding weight, water, or stress to the structure to prove it works.

The return on investment (ROI) for implementing EVM in a public transit facility is found in the extension of the asset's lifecycle. By catching breaches at the microscopic stage, we prevent the degradation of the roof deck and the expensive replacement of saturated insulation. Furthermore, it reduces the operational downtime of the bus barn, as repairs are targeted and rapid. We are moving the industry from reactive maintenance—fixing a leak after the ceiling collapses—to predictive engineering, where the building envelope communicates its own status in real-time.

  • Elimination of costly and risky flood testing protocols.
  • Provision of a digital "as-built" integrity map for facility managers.
  • Reduction in long-term capital expenditure by extending membrane life by 25-40%.
  • Integration of roof health data into the overall Building Management System (BMS).

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565

Commercial Engineering Dossier #759

Liquid-Applied PMMA & Polyurethane Fleece-Reinforced Flashing Resins on Commercial Government Secure Records Archives

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Liquid-Applied PMMA & Polyurethane Fleece-Reinforced Flashing Resins on Commercial Government Secure Records Archives

Building Envelope Audit and Site Vulnerability Assessment

The engineering audit of the Government Secure Records Archive revealed a critical failure in the building envelope, specifically at the transition points between the primary roof membrane and the structural I-beam stanchions. In a facility dedicated to the preservation of secure records, the tolerance for moisture ingress is zero. Any breach in the envelope introduces not only the risk of structural degradation but also the potential for catastrophic humidity spikes that can compromise archival-grade paper and digital storage media. The audit identified that traditional torch-down and sheet-membrane systems had failed due to thermal cycling and the inherent inability of rigid membranes to maintain a permanent seal around complex, multi-planar geometries.

The primary vulnerability lay in the mechanical stress concentrated at the stanchion bases. As the building undergoes natural thermal expansion and contraction, the rigid interfaces of the I-beams created shear forces that tore the existing flashing. This resulted in micro-fissures that allowed capillary action to draw water directly into the substrate. To rectify these systemic failures, a transition to a high-performance, liquid-applied resin system was mandated to ensure a seamless, monolithic seal that could accommodate structural movement while maintaining an impermeable barrier.

  • Identification of hydrostatic pressure points at the base of structural I-beams.
  • Analysis of thermal bridging causing localized condensation and premature membrane fatigue.
  • Evaluation of substrate porosity and the necessity for a non-porous, chemically bonded interface.
  • Assessment of existing flashing failure points using infrared thermography and moisture probes.

Material Science of PMMA and Polyurethane Cold-Applied Resins

The selection of Polymethyl Methacrylate (PMMA) and polyurethane resins for this project was based on their superior cure kinetics and chemical resistance. PMMA is a thermosetting resin that undergoes a rapid polymerization process, transitioning from a liquid state to a fully cured, hard-wearing plastic in a matter of minutes. Unlike solvent-based adhesives, PMMA is a 100% solids system, meaning there is no shrinkage during the curing process. This ensures that the bond between the resin and the steel I-beam remains intact without the development of internal voids or shrinkage cracks that typically plague traditional liquid membranes.

Polyurethane resins were integrated into the system to provide the necessary elasticity and vibration dampening. While PMMA provides the structural hardness and rapid set, the polyurethane components offer a degree of elongation that allows the flashing to bridge gaps and accommodate the subtle shifts of the building's skeleton. This hybrid approach creates a composite envelope that is both rigid enough to resist puncture and flexible enough to withstand the seismic and thermal oscillations inherent in large-scale government infrastructure.

  • Rapid polymerization of PMMA allowing for immediate foot traffic and water-tightness.
  • Zero-VOC emissions ensuring compliance with strict government indoor air quality standards.
  • High glass transition temperature (Tg) preventing the resin from softening during peak summer heat.
  • Chemical cross-linking that creates a covalent bond with the primed substrate for maximum adhesion.

Engineering the Fleece-Reinforced Embedding Process

To transform the liquid resin into a structural flashing, a non-woven polyester fleece reinforcement was embedded into the PMMA matrix. This process, known as "sandwiching," involves the application of a base layer of resin, the immediate embedding of the fleece, and a subsequent saturation coat. The fleece acts as the structural skeleton of the flashing, distributing tensile loads across a wider area and preventing the resin from cracking under stress. This reinforcement is critical when dealing with the sharp 90-degree angles and tight radii found on I-beam stanchions, where unreinforced resins would be prone to splitting.

The embedding process requires precision timing to ensure the fleece is fully saturated without creating air pockets or "fish-mouths." By utilizing a wet-on-wet application technique, the master roofer ensures that the fleece becomes an integral part of the resin's molecular structure. This creates a reinforced membrane that exceeds ASTM standards for puncture resistance and tear strength. The resulting assembly behaves as a single, homogenous unit, effectively bridging the gap between the roof deck and the vertical stanchion faces.

  • Application of a high-penetration PMMA primer to ensure a molecular bond to the steel and concrete.
  • Strategic overlapping of fleece layers to ensure continuous reinforcement across all transition joints.
  • Mechanical rolling of the fleece to eliminate entrapped air and ensure total resin saturation.
  • Application of a UV-stable topcoat to protect the polyurethane/PMMA matrix from solar degradation.

Execution on Intricate I-Beam Stanchions and Final Validation

The most challenging aspect of the installation was the flashing of the I-beam stanchions, which feature intricate webs and flanges. Traditional flashing requires multiple cuts and folds, creating numerous potential leak points. In contrast, the liquid-applied PMMA system was engineered to flow into every crevice of the I-beam, creating a seamless "boot" that encapsulates the steel. The resin was applied in multiple passes, ensuring that the interior corners of the beam were fully coated and that the fleece reinforcement was wrapped around the flanges to provide a continuous, waterproof wrap.

Final validation of the building envelope was conducted through a series of rigorous engineering tests. This included a 48-hour flood test and the use of electronic leak detection (ELD) to ensure the integrity of the flashing. The results confirmed that the PMMA and polyurethane system had eliminated all points of ingress. The rapid cure kinetics of the PMMA meant that the secure archives could remain operational throughout the process, as the curing time was too fast to allow for the typical odors or hazardous fumes associated with traditional hot-applied roofing systems.

  • Precision flashing of I-beam webs to prevent water entrapment in structural pockets.
  • Verification of bond strength through non-destructive pull-tests on sample coupons.
  • Implementation of a seamless transition from the vertical stanchion to the horizontal roof plane.
  • Final audit confirmation of a zero-leak status across all high-risk penetration points.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565

Previous (Vol. 18) Volume 19 of 23 (40 Dossiers / Page) Next (Vol. 20)