Aquashield Corporate Shield Logo

AQUASHIELD CORPORATE

Commercial Flat Roofing & Industrial Facility Engineering

A comprehensive technical compendium on commercial 60-mil TPO single-ply systems, high-solids silicone restorative coatings, and building envelope preservation. Volume 2 of 23.

Previous (Vol. 23) Volume 2 of 23 (40 Dossiers / Page) Next (Vol. 3)
Commercial Engineering Dossier #040

60-Mil TPO Robotic Hot-Air Seam Fusion & Test-Cut Peel Audits on Commercial Logistics Distribution Hubs
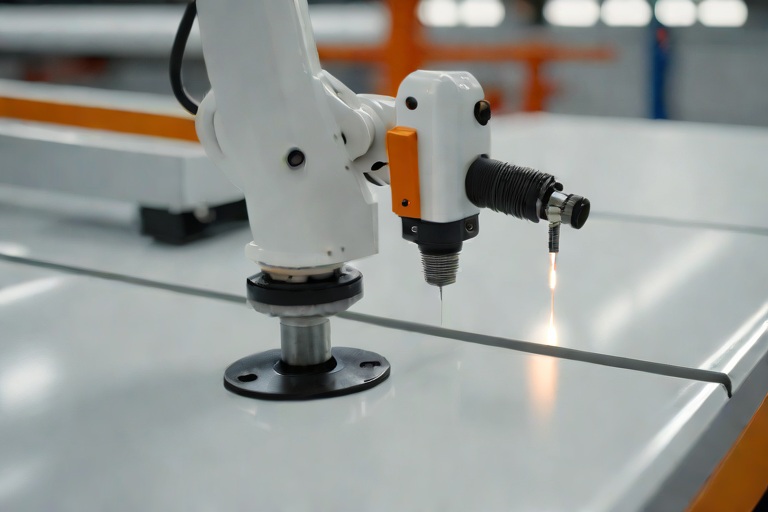
Industrial Building Envelope Sciences • Commercial Low-Slope Systems
60-Mil TPO Robotic Hot-Air Seam Fusion & Test-Cut Peel Audits on Commercial Logistics Distribution Hubs

Wind Uplift Dynamics and Substrate Preparation in Coastal Zones

In high-velocity hurricane zones and coastal corridors, the building envelope is subjected to extreme pressure differentials that can compromise the integrity of a commercial roofing system. For an industrial building envelope engineer, the primary objective is to mitigate the risk of wind uplift, which occurs when positive pressure on the windward side and negative pressure (suction) on the leeward side create a lifting force. To ensure a successful installation of 60-mil TPO, the process must begin with a rigorous substrate evaluation. This necessitates complete existing roof tear-offs down to clean wood decking to eliminate trapped moisture and organic debris that could compromise the bond or the structural integrity of the fastening system.

A failure to properly prepare the deck often leads to premature system failure. We emphasize the importance of boots-on-the-roof assessments to identify localized structural weaknesses. During these evaluations, our engineers focus on the following critical substrate requirements:

  • Verification of the structural load-bearing capacity of the decking.
  • Identifying signs of delamination or rot in the substrate.
  • Executing complete old roof tear-offs down to clean wood decking to remove compromised underlayments.
  • Stripping old shingles down to clean wood sheathing in mixed-use commercial applications to ensure a uniform surface for the TPO membrane.

Once the substrate is exposed, the process of inspecting the plywood deck and replacing damaged wood becomes the most critical phase of the project. Any void or soft spot in the decking can lead to fastener pull-out in mechanically attached systems or adhesive failure in fully adhered systems, effectively rendering the wind uplift calculations void.

Engineering Mechanically Attached 60-Mil TPO Systems

Mechanically attached TPO systems rely on a series of fasteners and plates to secure the membrane to the structural deck. In coastal wind zones, the spacing of these fasteners is not arbitrary; it is a calculated engineering requirement based on ASCE 7 standards. The goal is to distribute the wind load evenly across the deck to prevent the membrane from lifting. However, the inherent weakness of mechanically attached systems is the potential for membrane flutter. This occurs when wind penetrates the seams or edges, creating a billowing effect that puts repetitive stress on the fasteners and the TPO fabric itself.

To prevent flutter and ensure the system meets the required wind uplift ratings, we implement specific engineering controls:

  • Increasing fastener density in the "perimeter" and "corner" zones, where wind turbulence is highest.
  • Utilizing heavy-duty plates that maximize the surface area of the membrane grip.
  • Optimizing the tension of the membrane during installation to minimize pocketing.
  • Conducting hands-on physical roof inspections to ensure every fastener is driven flush and secure.

The technical risk in these systems is the "pull-through" failure, where the membrane tears away from the plate under extreme suction. This is why inspecting the plywood deck and replacing damaged wood is mandatory; a fastener driven into compromised wood will not achieve the required pull-out resistance, regardless of the plate's quality.

Fully Adhered TPO: Adhesive Shear Limits and Stability

Fully adhered 60-mil TPO systems eliminate the risk of membrane flutter by bonding the entire surface of the membrane to the substrate using high-strength adhesives. From an engineering perspective, this creates a monolithic slab that moves with the building rather than fighting against the wind. The primary technical consideration here is the adhesive shear limit—the maximum amount of force the adhesive bond can withstand before the bond breaks or the substrate fails.

In coastal environments, the bond strength is heavily dependent on the cleanliness of the substrate. Any residue from previous roofing materials can act as a bond-breaker, leading to catastrophic failure during a wind event. This is why we insist on complete existing roof tear-offs down to clean wood decking. The adherence process involves several critical technical steps:

  • Applying bonding adhesives in a precise, uniform layer to avoid "wet-out" or starved joints.
  • Managing the open time of the adhesive to ensure the TPO is rolled into the glue while it is in the optimal tack state.
  • Ensuring the membrane is fully rolled to eliminate air pockets that could lead to localized uplift.
  • Verifying that the substrate is dry and free of contaminants through boots-on-the-roof assessments.

When the adhesive is applied correctly to a stable substrate, the shear limit is often higher than the tensile strength of the membrane itself. This means that in a catastrophic wind event, the membrane is more likely to tear than to delaminate from the deck, provided the initial stripping old shingles down to clean wood sheathing was performed thoroughly.

Comparative Analysis: Wind Uplift and System Selection

Choosing between mechanically attached and fully adhered TPO requires a nuanced understanding of the building's specific wind exposure. Mechanically attached systems are often preferred for their speed of installation and the fact that they do not require the substrate to be perfectly smooth. However, in extreme coastal zones, the risk of flutter and fastener fatigue makes fully adhered systems the technically superior choice for long-term stability.

The following table of considerations guides our engineering decisions:

  • Wind Uplift Resistance: Fully adhered systems generally offer higher wind uplift ratings because they distribute the load across the entire surface area rather than at discrete points.
  • Membrane Flutter: Mechanically attached systems are susceptible to flutter; fully adhered systems are immune to it.
  • Substrate Requirements: Fully adhered systems require a pristine surface, necessitating complete old roof tear-offs down to clean wood decking.
  • Installation Complexity: Fully adhered systems require more labor and precision in adhesive application but offer a more stable building envelope.

Ultimately, the decision is based on the calculated wind loads of the specific site. For office complexes with large flat roof areas, the combination of fully adhered membranes in the perimeter and corner zones and mechanically attached membranes in the field is sometimes utilized to balance cost and performance.

Implementation, Inspection, and Technical Estimation

The transition from engineering theory to physical installation requires a rigorous quality control process. A technical case study is only as good as the field execution. We believe that the only way to guarantee the performance of a TPO system in a coastal zone is through hands-on physical roof inspections at every stage of the project. This ensures that the theoretical wind uplift calculations are supported by the actual conditions of the roof deck.

Our process for ensuring technical compliance includes:

  • Performing initial boots-on-the-roof assessments to map out the current state of the envelope.
  • Developing free line-item written estimates that clearly delineate the cost of complete existing roof tear-offs down to clean wood decking versus overlay options.
  • Documenting the process of inspecting the plywood deck and replacing damaged wood to provide a paper trail of structural integrity.
  • Conducting final pull-tests on fasteners or bond-tests on adhered sections to verify the installation meets the engineering specifications.

By focusing on the fundamentals—complete old roof tear-offs down to clean wood decking and precise wind uplift engineering—Aquashield Corporate ensures that commercial office complexes remain secure against the most volatile coastal weather patterns. The marriage of rigorous substrate preparation and advanced TPO attachment methods is the only way to eliminate membrane flutter and prevent systemic envelope failure.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #041

High-Solids Silicone Monolithic Coating Restoration & Albedo Reflectance on Commercial Automotive Assembly Plants

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
High-Solids Silicone Monolithic Coating Restoration & Albedo Reflectance on Commercial Automotive Assembly Plants

Logistics of River Rock Ballast Removal and Structural Load Reduction

The transition from a ballasted EPDM system to a fully adhered TPO membrane represents a significant engineering shift in building envelope dynamics. Ballasted systems rely on the gravitational force of river rock to prevent membrane wind uplift, often adding several hundred pounds per square foot to the building's dead load. The removal process is a complex logistical operation that requires a phased approach to prevent localized structural overloading during the extraction phase. Utilizing high-capacity conveyors and specialized vacuum equipment, the river rock is systematically removed to alleviate the structural stress on the primary steel or concrete framing.

From an engineering perspective, the removal of ballast allows for a comprehensive re-evaluation of the building's load-bearing capacity. By reducing the dead load, the facility gains a higher safety margin for future equipment installations or seismic requirements. The technical objective is to transition from a passive weight-based stability system to a mechanical attachment system that utilizes high-performance adhesives and fasteners. This shift not only improves the structural longevity of the building but also optimizes the thermal performance of the envelope by allowing for the installation of thicker, high-R-value insulation without exceeding the original design load of the roof joists.

  • Implementation of phased ballast extraction to maintain balanced structural loading.
  • Utilization of industrial-grade conveyors to minimize debris accumulation on the roof surface.
  • Calculation of dead load reduction to quantify the increase in structural safety margins.
  • Coordination of debris disposal logistics to ensure zero interruption to facility operations.

Substrate Remediation and Decking Integrity Analysis

Once the ballast and old EPDM membrane are removed, the focus shifts to the integrity of the underlying substrate. The removal process involves complete old roof tear-offs down to clean wood decking to ensure that no trapped moisture or degraded adhesives remain. In mixed-use industrial complexes, this may also involve stripping old shingles down to clean wood sheathing on smaller ancillary structures to maintain a uniform standard of quality across the entire asset. The objective is to create a pristine surface that allows for the optimal bond of new insulation and cover boards.

A critical phase of this process is the execution of hands-on physical roof inspections. These assessments are not superficial; they involve a granular analysis of the decking for signs of delamination, rot, or structural deflection. By performing complete existing roof tear-offs down to clean wood decking, our engineers can accurately identify areas of water infiltration that were previously hidden by the ballasted rock. This stage is paramount because any compromise in the substrate will inevitably lead to premature failure of the TPO membrane due to uneven support or gas off-gassing from decaying organic material.

  • Conducting rigorous inspecting the plywood deck and replacing damaged wood to ensure a level substrate.
  • Executing complete existing roof tear-offs down to clean wood decking to eliminate organic contaminants.
  • Performing boots-on-the-roof assessments to verify the structural soundness of the perimeter and field areas.
  • Applying high-performance primers to the cleaned substrate to enhance the adhesion of the insulation layers.

High-Density Cover Board Engineering and Thermal Optimization

To bridge the gap between the insulation and the TPO membrane, the installation of a high-density cover board is mandatory. In a commercial conversion, the cover board serves as a sacrificial layer that protects the polyisocyanurate insulation from puncture and provides a stable base for the heat-welding process. We utilize high-density gypsum-fiber or mineral-wool boards that offer superior compressive strength. This layer prevents the "dimpling" effect often seen in lower-quality installations and ensures that the robotic welding equipment can glide across the surface without creating uneven seams.

The integration of the cover board also enhances the building's fire rating and wind uplift resistance. By mechanically fastening the cover board through the insulation and into the structural deck, we create a reinforced composite layer. This assembly transforms the roof into a rigid diaphragm, which significantly improves the building's overall stability during high-wind events. The technical synergy between the high-density board and the TPO membrane ensures that the thermal envelope remains airtight, reducing energy leakage and preventing the condensation issues typically associated with older EPDM systems.

  • Installation of high-density cover boards to provide a rigid surface for robotic fusion.
  • Optimization of R-value by layering high-performance polyiso insulation beneath the cover board.
  • Mechanical fastening patterns designed to meet or exceed FM Global wind-uplift requirements.
  • Verification of surface flatness to prevent ponding water and ensure efficient drainage.

Automated Robotic Hot-Air Seam Fusion and Quality Control

The pinnacle of the conversion process is the installation of the TPO membrane using automated robotic hot-air seam fusion. Unlike traditional hand-welding, robotic fusion utilizes precision-controlled heating elements and rollers to create a molecular bond between the membrane sheets. The robot maintains a constant temperature and pressure, ensuring that every inch of the seam is fused to a uniform depth. This eliminates human error and ensures that the seam is actually stronger than the membrane itself, creating a monolithic, waterproof shield across the entire roof area.

To validate the integrity of these seams, we employ a rigorous quality assurance protocol. This includes the use of seam probes and vacuum testing to ensure there are no voids or "cold welds" in the fusion. Because the robotic system provides a consistent weld, the risk of leaks at the laps is virtually eliminated. This level of precision is only possible after the thorough process of inspecting the plywood deck and replacing damaged wood, as the robotic welder requires a perfectly stable substrate to maintain its calibration and travel speed.

  • Deployment of automated robotic welders to achieve consistent, high-strength molecular fusion.
  • Precision temperature monitoring to prevent over-welding or membrane scorching.
  • Systematic seam probing to verify the integrity of every linear foot of the weld.
  • Application of reinforced flashing at all penetrations and parapet walls for maximum waterproofing.

Final Envelope Verification and Project Documentation

The completion of a commercial roof conversion requires a final phase of verification to ensure the building envelope is fully sealed and performing to engineering specifications. This involves a series of boots-on-the-roof assessments where the lead engineer inspects all termination bars, edge metals, and flashing details. The transition from a ballasted system to a welded system changes the way the roof handles thermal expansion and contraction; therefore, verifying the flexibility of the membrane at the corners and transitions is essential for long-term durability.

For the client, transparency in the technical process is provided through detailed documentation. We provide free line-item written estimates during the planning phase, which are then mirrored in the final as-built reports. This documentation outlines every step taken, from the initial complete old roof tear-offs down to clean wood decking to the final robotic weld verification. This authoritative approach to documentation ensures that the building owner has a complete historical record of the envelope's structural and thermal improvements, which is critical for future facility audits and insurance valuations.

  • Final boots-on-the-roof assessments to ensure all detailing meets industrial standards.
  • Provision of comprehensive as-built documentation and warranty certifications.
  • Delivery of free line-item written estimates to ensure financial and technical transparency.
  • Verification of the drainage system to ensure the new lightweight profile optimizes water runoff.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #042

Tapered Polyiso Drainage Layouts (1/4-In/Ft) & Geometric Cricket Sizing on Commercial Mission-Critical Data Centers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Tapered Polyiso Drainage Layouts (1/4-In/Ft) & Geometric Cricket Sizing on Commercial Mission-Critical Data Centers

The Thermodynamics of Moisture Entrapment in Multi-Ply Modified Bitumen Systems

In industrial building envelope engineering, the multi-ply modified bitumen assembly represents a complex barrier system designed for high durability and waterproofing. However, the very characteristics that make these systems resilient—namely their density and low permeability—create a significant risk for substrate moisture entrapment. When a breach occurs in the cap sheet or the base sheet, moisture infiltrates the assembly and becomes trapped between the non-permeable membrane and the industrial decking. Because modified bitumen acts as a vapor barrier, any water that enters cannot easily evaporate, leading to a "saturated sandwich" effect.

This trapped moisture initiates a process of substrate degradation through hydrostatic pressure and capillary action. In industrial settings, the vapor drive is often bidirectional; moisture may enter from the roof surface via flashing failures or migrate from the interior of the building due to high humidity and poor ventilation. Once the insulating layer becomes saturated, the thermal resistance (R-value) of the system drops precipitously, and the moisture begins to attack the structural integrity of the decking. Understanding the movement of this moisture is critical for any engineer conducting boots-on-the-roof assessments to determine if a system requires a simple patch or a comprehensive replacement.

  • Capillary migration: The movement of water through small pores in the insulation and substrate.
  • Hydrostatic saturation: The state where the substrate cannot hold more moisture, leading to pooling at the deck level.
  • Vapor drive: The pressure differential that forces moisture through the building envelope from areas of high concentration to low concentration.
  • Thermal bridging: The loss of efficiency where moisture-laden areas conduct heat faster than dry areas.

Non-Destructive Infrared Thermography (IRT) Protocols

To identify subsurface moisture without compromising the membrane, we employ non-destructive infrared thermography. IRT relies on the principle of thermal mass; wet insulation has a higher heat capacity than dry insulation. Consequently, wet areas retain heat longer as the ambient temperature drops during the evening, appearing as "hot spots" on a thermal imaging camera. Conversely, during the morning warming phase, wet areas may appear cooler because they take longer to heat up.

For a diagnostic to be authoritative, the IRT scan must be conducted during a specific diurnal window, typically when there is a temperature differential of at least 15 to 20 degrees Fahrenheit between the roof surface and the air. A master engineer does not rely on a single snapshot but analyzes a series of thermal signatures to map the extent of the moisture plumes. These plumes often follow the slope of the roof or congregate around perimeter edges and penetrations, providing a roadmap for where the actual leaks are occurring.

However, IRT is a screening tool, not a definitive confirmation. Thermal anomalies can be caused by structural reinforcements, varying insulation densities, or surface debris. Therefore, IRT must be paired with hands-on physical roof inspections to correlate thermal data with visible surface defects. This integrated approach ensures that the diagnostic process is precise and that the subsequent remediation plan is based on empirical evidence rather than conjecture.

  • Diurnal cycle analysis: Monitoring temperature shifts from peak sun to midnight.
  • Thermal mapping: Creating a visual grid of heat signatures to identify moisture plumes.
  • Anomaly correlation: Comparing IRT data with physical evidence of membrane failure.
  • Saturation depth estimation: Using heat dissipation rates to guess the volume of trapped water.

Core Sampling and Forensic Substrate Verification

Once the IRT scan has identified suspect areas, the engineer must transition to destructive testing via core sampling. This process involves cutting a small, circular section through the modified bitumen cap sheets, the app-modified base sheets, and the insulation down to the decking. This is the only way to physically verify the moisture content of the substrate and the condition of the decking material.

During the core extraction, the engineer examines the "moisture profile" of the insulation. If the top of the insulation is wet, the leak is likely originating from the roof surface. If the bottom of the insulation—adjacent to the deck—is wet while the top is dry, the moisture is likely migrating from the interior of the building. This distinction is vital because it determines whether the solution is a roof replacement or a change in the building's internal climate control and vapor barriers.

Furthermore, this forensic step allows for the direct inspection of the structural deck. In many industrial cases, trapped moisture leads to delamination of the plywood or oxidation of the metal decking. By performing these targeted cuts, we can determine if the damage is localized or systemic. This data is essential for providing clients with free line-item written estimates that accurately reflect the scope of work required to restore the building envelope to a warranted condition.

  • Moisture probe testing: Using electronic meters to measure the percentage of moisture in the substrate.
  • Visual inspection of the deck: Checking for rot, mold, or structural deflection.
  • Sample archiving: Keeping core sections for laboratory analysis if chemical degradation is suspected.
  • Verification cutting: Confirming the boundaries of the moisture plumes identified by IRT.

Remediation Strategies and Structural Restoration

When diagnostics reveal systemic moisture entrapment, the only viable engineering solution is the total removal of the compromised assembly. Attempting to "recover" or overlay a wet roof is a failure of professional standards, as it traps the remaining moisture and accelerates the rot of the decking. The goal of professional remediation is to return the building to a state of structural equilibrium.

The process begins with complete old roof tear-offs down to clean wood decking. This ensures that all saturated insulation and degraded membranes are removed, allowing the substrate to breathe and dry. In scenarios involving mixed-use facilities where different roofing materials meet, this may also involve stripping old shingles down to clean wood sheathing to ensure a uniform transition between the industrial and residential sections of the envelope. Once the surface is clear, the engineer focuses on inspecting the plywood deck and replacing damaged wood that has been compromised by long-term moisture exposure.

A rigorous restoration protocol demands complete existing roof tear-offs down to clean wood decking before any new materials are applied. This allows the contractor to verify the flatness of the deck and ensure that the new vapor retarder is installed on a stable, dry surface. By adhering to these strict removal protocols, the building owner avoids the risk of premature system failure and ensures the longevity of the new multi-ply assembly.

  • Full substrate dehydration: Allowing the deck to reach an acceptable moisture content before re-roofing.
  • Structural reinforcement: Replacing rotted sheathing to restore the load-bearing capacity of the roof.
  • Vapor barrier optimization: Installing a new, high-performance base sheet to prevent future interior moisture migration.
  • Systematic layering: Applying modified bitumen cap sheets according to strict manufacturer specifications to ensure a watertight seal.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #043

Multi-Ply SBS-Modified Bitumen Cap Sheet Application & Vapor Control on Commercial Cold Storage Freezer Warehouses

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Multi-Ply SBS-Modified Bitumen Cap Sheet Application & Vapor Control on Commercial Cold Storage Freezer Warehouses

Mechanical Pull-Out Testing Methodology for 22-Gauge Steel Substrates

In the realm of industrial building envelope engineering, the structural integrity of the roof system is fundamentally dependent on the connection between the fastening hardware and the steel deck. For 22-gauge steel decks, the pull-out strength is not a static value but a variable influenced by fastener geometry, thread engagement, and the metallurgical properties of the steel. Calibrated mechanical pull testing serves as the primary empirical method for validating that a fastening system can withstand the calculated uplift pressures of a specific geographic region. This process involves the application of a controlled axial load via a hydraulic or electronic pull-tester, increasing the tension until either the fastener reaches its yield point or the substrate fails.

The objective of these tests is to establish a baseline for the "ultimate load," which is the maximum force the fastener can sustain before complete withdrawal. Engineers must distinguish between the elastic deformation phase, where the fastener may return to its original position, and the plastic deformation phase, where permanent displacement occurs. To ensure statistical significance, a series of tests must be conducted across various zones of the roof, specifically targeting the perimeter and corners where wind turbulence is most aggressive.

  • Utilization of calibrated digital force gauges to measure peak load in pounds-force (lbf) or kilonewtons (kN).
  • Application of a constant rate of displacement to avoid dynamic loading spikes that could skew the results.
  • Verification of fastener perpendicularity to the deck surface to eliminate shear force variables.
  • Documentation of the failure mode, specifically whether the failure was a "pull-through" of the steel or a "stripping" of the fastener threads.

Minimum Withdrawal Resistance and Structural Thresholds

For a 22-gauge steel deck, the minimum withdrawal resistance threshold is determined by the intersection of the design wind speed and the safety factor required by local building codes. In high-wind zones, the fastener must provide a resistance value that exceeds the calculated uplift pressure by a factor of at least 1.5 to 2.0. When the fastener is driven into 22-gauge steel, the limited thickness of the substrate means that the thread engagement is minimal; therefore, the reliance shifts toward the mechanical interlock and the friction between the fastener shank and the steel walls.

If the pull-out tests reveal that the fasteners are failing below the minimum threshold, the engineer must evaluate the possibility of utilizing oversized washers or switching to a fastener with a more aggressive thread profile. The goal is to distribute the load across a wider surface area of the steel deck, thereby reducing the localized stress concentration that leads to premature pull-through failure. This analysis is critical because a failure in a single fastener can lead to a progressive "zipper effect," where the failure of one point increases the load on adjacent fasteners, leading to a catastrophic system collapse during a wind event.

  • Calculation of the required fasteners per square foot based on the total uplift load.
  • Analysis of the "pull-through" strength of the 22-gauge steel to ensure the metal does not deform before the fastener reaches its rated capacity.
  • Establishment of a minimum acceptable load value (MALV) for every fastener type used in the project.
  • Comparison of field-tested values against the manufacturer's theoretical laboratory data.

Corrosion Degradation and Material Fatigue Analysis

The longevity of a fastening system is perpetually threatened by the chemical environment of the industrial roof. Corrosion degradation, particularly in coastal or chemically aggressive environments, can severely compromise the cross-sectional area of both the fastener and the 22-gauge steel deck. Oxidation leads to a reduction in the effective diameter of the fastener shank, which directly correlates to a decrease in pull-out resistance. Galvanic corrosion is a particular concern when dissimilar metals are in contact, as the resulting electrochemical reaction can eat through the steel deck at the point of penetration.

Over time, the cyclical loading caused by thermal expansion and contraction—known as thermal cycling—can induce material fatigue. This fatigue manifests as micro-fractures in the steel surrounding the fastener, which lowers the threshold for withdrawal. When performing pull tests on an existing structure, the engineer must account for the age of the deck and the presence of any corrosive agents that may have permeated the building envelope. This requires a nuanced understanding of how the metallurgical integrity of the 22-gauge steel has evolved since the original installation.

  • Assessment of red rust (iron oxide) versus white rust (zinc oxide) to determine the stage of coating failure.
  • Evaluation of the impact of atmospheric pollutants on the tensile strength of the fastening hardware.
  • Testing for "brittle failure" in aged decks where the steel may snap rather than deform.
  • Implementation of corrosion-resistant coatings or stainless steel alternatives in high-risk environments.

Wind-Zone Fastening Schedules and Regulatory Compliance

A fastening schedule is a comprehensive map that dictates the density and placement of fasteners based on the wind-zone classification of the building. In high-velocity hurricane zones, the fastening schedule is significantly more dense than in interior regions. The data derived from calibrated pull testing is used to refine these schedules, ensuring that the building envelope remains intact under peak gust pressures. The engineering focus is on the "edge-to-field" ratio, where the perimeter of the roof requires a higher concentration of fasteners to counteract the vortex shedding that occurs at the building's edges.

Compliance with these schedules is not merely a regulatory requirement but a risk management necessity. An incorrectly implemented fastening schedule can lead to the total detachment of the roofing membrane, exposing the interior of the industrial facility to water ingress and structural damage. The engineer must verify that the installation team has adhered to the specified patterns and that the fasteners have been driven to the correct depth without over-torquing, as over-torquing can crush the 22-gauge steel and compromise the pull-out strength.

  • Mapping of "Zone 1" (field), "Zone 2" (perimeters), and "Zone 3" (corners) for fastener distribution.
  • Cross-referencing pull-test results with ASCE 7 standards for wind load calculations.
  • Validation of the fastener spacing to prevent overlapping stress zones in the steel deck.
  • Final certification of the fastening system's capacity to resist the calculated design wind pressure.

Field Assessment and Remediation Protocols

While the technical focus of this study is on 22-gauge steel, a master commercial roofer knows that a building envelope is often a hybrid of various materials. A comprehensive site audit requires boots-on-the-roof assessments to determine the overall health of the structure. This includes hands-on physical roof inspections to identify areas of deflection or moisture entrapment. In many industrial complexes, the steel deck may be adjacent to sections with organic substrates, necessitating different remediation strategies. For instance, when dealing with older sections of a facility, we may perform complete old roof tear-offs down to clean wood decking to ensure the underlying structure is sound.

The process of remediation often begins with stripping old shingles down to clean wood sheathing in mixed-use areas to identify hidden rot or structural compromise. This rigorous approach involves inspecting the plywood deck and replacing damaged wood before any new membrane is applied. For the steel sections, the remediation involves replacing compromised fasteners and reinforcing the 22-gauge deck where corrosion has occurred. To ensure transparency and accuracy in the restoration process, we provide free line-item written estimates that detail every phase of the work, from complete existing roof tear-offs down to clean wood decking to the precision installation of industrial steel fasteners.

  • Integration of pull-test data into a comprehensive remediation plan.
  • Coordination of substrate replacement for both steel and wood components of the envelope.
  • Verification of all new fasteners through a secondary round of random pull testing.
  • Final walkthrough to ensure the building envelope is sealed and structurally compliant with wind-zone requirements.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #044

Parapet Wall Heavy-Gauge 20-Gauge Kynar 500 Coping Cap Continuous Cleat Locking on Commercial Commercial Fleet Maintenance Hangars

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Parapet Wall Heavy-Gauge 20-Gauge Kynar 500 Coping Cap Continuous Cleat Locking on Commercial Commercial Fleet Maintenance Hangars

Technical Evaluation of Aged Smooth BUR Systems in Logistics Environments

Logistics terminals present a unique set of challenges for building envelope integrity due to the sheer scale of the roof surfaces and the constant vibration and structural stress caused by heavy freight movement. Many of these facilities utilize aged Built-Up Roofing (BUR) systems, which traditionally rely on multiple layers of asphalt-saturated felts and a cap sheet. Over time, these systems suffer from thermal shock, UV degradation, and the gradual loss of volatile oils, leading to "alligatoring" or deep fissuring of the surface. To accurately determine the viability of a restoration versus a full replacement, we insist on boots-on-the-roof assessments.

A superficial visual check is insufficient for industrial-grade assets. A comprehensive technical audit requires identifying the specific failure points of the BUR, such as saturated insulation or compromised flashing. In cases where the substrate has suffered catastrophic failure, the only viable path forward is the execution of complete old roof tear-offs down to clean wood decking. This ensures that the new system is not inheriting the moisture trapped within the old asphaltic layers, which would otherwise lead to premature blistering and premature failure of the new membrane.

The technical analysis phase must include the following critical evaluations:

  • Assessment of the current slope and drainage efficiency to prevent ponding water.
  • Verification of the structural integrity of the supporting members.
  • Identification of moisture migration patterns using infrared thermography.
  • Evaluation of the existing flashing transitions at parapets and roof penetrations.

Surface Decontamination and Substrate Remediation Protocols

The primary obstacle in restoring aged BUR systems is the presence of gravel ballast. While gravel provides UV protection and weight to hold the membrane in place, it traps organic debris and moisture, creating a breeding ground for microbial growth and accelerating the degradation of the asphalt. The first phase of a high-solids silicone restoration is the total elimination of this ballast. Once the gravel is removed, the underlying smooth BUR surface is exposed, allowing for a rigorous decontamination process.

Surface preparation is the most critical variable in the success of a monolithic membrane. We employ high-pressure cleaning and chemical neutralization to remove all traces of atmospheric pollutants and biological contaminants. However, if the underlying substrate is found to be structurally unsound during the cleaning process, the scope of work shifts. In these instances, we perform complete existing roof tear-offs down to clean wood decking to establish a stable foundation. For facilities that include mixed-use office components or smaller auxiliary structures, this process may involve stripping old shingles down to clean wood sheathing to ensure consistency across the entire building envelope.

Once the surface is cleared, the engineering focus shifts to the decking. This involves inspecting the plywood deck and replacing damaged wood that has been compromised by long-term leaks. A silicone restoration is only as effective as the substrate beneath it; therefore, the following steps are mandatory:

  • Mechanical scrubbing of the BUR surface to remove oxidized asphalt.
  • Application of a high-performance primer to neutralize the pH of the substrate.
  • Detailed patching of all punctures and seams using reinforced flashing grade silicone.
  • Verification of all perimeter edges to ensure a watertight transition.

Engineering the High-Solids Silicone Monolithic Membrane

The application of a high-solids silicone membrane represents a paradigm shift in industrial roofing. Unlike traditional coatings that rely on solvents—which evaporate and cause the membrane to shrink—high-solids silicone contains minimal volatiles. This results in a monolithic membrane that maintains its thickness and elasticity over decades. The chemistry of the silicone allows it to remain flexible across extreme temperature fluctuations, which is essential for the large, uninsulated spans found in logistics terminals.

The "monolithic" nature of the system means that it creates a single, seamless layer of protection. By eliminating seams, we eliminate the most common point of failure in commercial roofing. The high-solids content ensures that the membrane is highly reflective, significantly reducing the heat island effect and lowering the cooling loads for the facility. This is particularly advantageous for logistics hubs where interior temperature regulation is critical for workforce safety and cargo stability.

Technical specifications for the silicone application include:

  • Minimum dry film thickness (DFT) requirements to ensure long-term durability.
  • Strict adherence to wet-film thickness (WFT) monitoring during application.
  • Integration of high-strength fabric reinforcement at all critical transition points.
  • Application of a final reflective top-coat to maximize solar reflectance index (SRI) values.

Operational Continuity and Zero-Downtime Implementation

For logistics terminals, downtime is not an option. The cost of halting freight movement or relocating inventory is often higher than the cost of the roofing project itself. The primary advantage of high-solids silicone restoration over traditional replacement is the ability to maintain zero-downtime operations. Because the process does not require the massive staging of materials or the heavy machinery associated with complete tear-offs, the facility can remain fully operational.

Our approach utilizes a phased application strategy. By sectioning the roof into manageable zones, we ensure that the building remains protected at all times. While a full replacement would require the massive disruption of complete old roof tear-offs down to clean wood decking across the entire footprint, a restoration allows us to target only the areas of failure. This surgical approach minimizes the impact on daily logistics and eliminates the need for temporary interior relocations.

To ensure the project stays on track without interrupting business, we implement the following operational controls:

  • Scheduled application windows that align with low-traffic periods of the terminal.
  • Strict containment protocols to prevent debris from entering loading docks.
  • Continuous communication with facility managers to coordinate access.
  • Rapid-cure components to reduce the window of vulnerability between coats.

Quality Assurance and Lifecycle Cost Analysis

The final phase of the restoration is a rigorous quality assurance protocol. We do not rely on third-party reports; instead, we conduct hands-on physical roof inspections to verify that every square inch of the membrane meets the engineered specifications. This involves a combination of tactile checks and precision measurement of the film thickness to ensure the monolithic integrity of the system.

From a financial perspective, the lifecycle cost of a high-solids silicone restoration is significantly lower than a traditional replacement. By avoiding the waste disposal fees associated with stripping old shingles down to clean wood sheathing or the labor-intensive process of removing multiple layers of BUR, the client realizes immediate CAPEX savings. Furthermore, the longevity of silicone—which does not degrade under UV exposure—extends the interval between major maintenance cycles.

To provide total transparency and budgetary certainty, we provide the following to our corporate partners:

  • Free line-item written estimates that detail every phase of the restoration.
  • Comprehensive warranties that cover both materials and installation.
  • Detailed maintenance schedules to ensure the membrane remains clean and reflective.
  • Post-installation reports based on final boots-on-the-roof assessments.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #045

Industrial Drainage Scuppers, Overflow Weirs & Heavy Downspout Expansion Bellows on Commercial Chemical Processing Facilitys

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Industrial Drainage Scuppers, Overflow Weirs & Heavy Downspout Expansion Bellows on Commercial Chemical Processing Facilitys

Hydraulic Head-Loss Analysis and Primary Scupper Optimization

In the engineering of a large-scale Logistics Distribution Hub, the primary challenge lies in the management of massive catchment areas. When analyzing the building envelope of a facility exceeding 500,000 square feet, the hydraulic head-loss across primary scuppers becomes a critical failure point. Head-loss occurs when the kinetic energy of the water is dissipated due to friction and turbulence as it transitions from the roof membrane into the scupper throat. From a forensic building science perspective, if the scupper is undersized or improperly positioned relative to the roof's low points, the resulting hydrostatic pressure can lead to membrane migration or structural deflection.

During our initial boots-on-the-roof assessments, we identified that the existing drainage points were failing to account for the peak intensity of a 100-year storm event. To rectify this, we performed a series of hydraulic calculations to determine the precise flow rate required to prevent excessive ponding. This process began with hands-on physical roof inspections to map the actual slope of the roof, as as-built drawings rarely reflect the real-world settlement of the structure. By calculating the Manning's roughness coefficient of the membrane and the slope of the roof, we were able to determine the exact head-loss across the scupper aperture.

  • Calculation of the discharge coefficient (Cd) for various scupper geometries to minimize turbulence.
  • Analysis of the "weir flow" equation to ensure the scupper throat can handle the peak volumetric flow rate without backing up.
  • Verification of the scupper flashing integration to ensure a watertight seal during high-velocity flow events.
  • Assessment of the transition from the roof surface to the conductor head to reduce splash-back and erosion.

Emergency Overflow Weir Sizing and Structural Integrity

A primary drainage system, no matter how robust, is subject to failure via debris blockage or mechanical malfunction. In a Logistics Distribution Hub, the accumulation of water on a flat roof can quickly reach weights that exceed the structural load-bearing capacity of the roof deck. Therefore, the engineering of emergency overflow weirs is not merely a preference but a structural necessity. An overflow weir acts as a safety valve, allowing water to exit the roof envelope once it reaches a predetermined critical depth, typically two inches above the primary drain level.

Our forensic analysis involved evaluating the distance between primary drains and the placement of these overflow weirs to ensure that no single area of the roof would experience catastrophic ponding. To ensure the accuracy of these installations, we provided the client with free line-item written estimates that detailed the exact placement and sizing of each overflow point. This level of precision prevents the "damming effect" where water is trapped between the primary drain and the perimeter wall, which often leads to membrane failure and internal leaks.

  • Sizing the weir width based on the total catchment area divided by the number of emergency outlets.
  • Establishing the "critical depth" threshold to prevent premature discharge while ensuring structural safety.
  • Integrating the weir into the parapet wall using reinforced flashing to prevent water infiltration into the wall cavity.
  • Testing the overflow capacity through controlled flood testing to verify the hydraulic calculations.

Conductor Head Design and Vortex Mitigation

The transition of water from the roof surface into the vertical downspout system is a high-turbulence zone. In industrial hubs, the sheer volume of water can create a vortex effect within the conductor head, which significantly restricts the flow rate and can lead to backup at the scupper. To mitigate this, we implement high-capacity conductor heads designed to break the velocity of the water and transition it smoothly into the downspout. This reduces the air entrapment within the piping, which is a common cause of "slugging" or hydraulic jumps in the drainage system.

In several sections of the facility, we encountered legacy installations where the conductor heads were undersized for the updated roof slope. This required a comprehensive overhaul of the drainage path. Before installing new components, we focused on the integrity of the roof's substructure. In the older administrative wings of the hub, this involved complete old roof tear-offs down to clean wood decking. By stripping old shingles down to clean wood sheathing, we were able to ensure that the new drainage hardware was anchored into a stable substrate, preventing the weight of the water-filled conductor heads from compromising the roof deck.

  • Implementation of oversized conductor heads to increase the air-to-water ratio and reduce vortexing.
  • Strategic placement of conductor heads to align with the primary structural columns for maximum support.
  • Utilizing heavy-gauge galvanized steel to resist the erosive forces of high-velocity industrial runoff.
  • Inspecting the plywood deck and replacing damaged wood in the administrative sections to ensure a secure mounting surface.

Thermal Expansion Bellows and Heavy Downspout Engineering

Industrial buildings of this magnitude are subject to significant thermal expansion and contraction. A downspout that runs 40 feet from the roof to the grade can expand or contract by several fractions of an inch depending on the temperature differential. Without the integration of thermal expansion slip joints or bellows, this movement puts immense stress on the scupper flashing and the conductor head connections, eventually leading to joint separation and catastrophic leaks.

Our engineering approach utilizes heavy-duty expansion bellows at strategic intervals along the vertical run. These bellows allow the downspout to move independently of the building's structural frame. During our forensic review, we found that many failures occurred because the downspouts were rigidly fastened to the building envelope, effectively turning the piping into a lever that pried the flashing away from the roof during winter contractions. By installing slip joints, we decouple the drainage system from the building's thermal movement.

  • Installation of expansion bellows every 20 to 30 feet of vertical run to absorb linear thermal growth.
  • Use of heavy-wall thickness piping to prevent deformation under the weight of the water column.
  • Application of industrial-grade sealants at the slip joints to prevent leakage while maintaining flexibility.
  • Coordination of the downspout discharge points to ensure water is diverted away from the foundation to prevent soil saturation.

The success of this project relied on a meticulous sequence of operations. We began with complete existing roof tear-offs down to clean wood decking in the problematic zones, ensuring that the forensic evidence of previous failures was fully analyzed. By combining boots-on-the-roof assessments with rigorous hydraulic head-loss calculations, Aquashield Corporate has ensured that this Logistics Distribution Hub is equipped with a drainage system capable of handling extreme weather events while maintaining the long-term integrity of the building envelope.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #046

AOC 581 Elastomeric Structural Mastic Detailing Around Rooftop HVAC Curbs on Commercial Municipal City Hall & Administrative Complexs

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
AOC 581 Elastomeric Structural Mastic Detailing Around Rooftop HVAC Curbs on Commercial Municipal City Hall & Administrative Complexs

Logistics Distribution Hub: AOC 581 Elastomeric Structural Mastic Detailing Around Rooftop HVAC Curbs

From a forensic building science perspective, the interface between a rooftop mechanical curb and the primary roofing membrane represents one of the highest risk zones for envelope failure. In a large-scale logistics distribution hub, these vulnerabilities are magnified by the sheer scale of the roof surface and the constant oscillation caused by heavy-duty mechanical equipment. The primary engineering challenge lies in managing the disparate rates of thermal expansion between the metal curb and the roofing substrate, while simultaneously dampening the kinetic energy transferred from mechanical vibrations into the seal. Failure to address these variables leads to fatigue cracking in the sealant, eventually resulting in systemic moisture intrusion and structural degradation of the decking.

To mitigate these risks, we implement a rigorous protocol centered on the application of AOC 581 Elastomeric Structural Mastic. Unlike standard sealants, this fiber-reinforced compound provides the necessary tensile strength and elongation properties to absorb the constant "drift" associated with thermal cycling. Our approach begins with an exhaustive diagnostic phase to ensure the substrate is capable of supporting the structural load of the mastic and the equipment it serves.

Forensic Substrate Evaluation and Preparation

The integrity of any elastomeric seal is entirely dependent on the condition of the underlying substrate. In many industrial distribution centers, we encounter legacy layers of compromised membranes that mask deeper structural issues. Our engineering standard requires a total removal of failing systems to eliminate trapped moisture and organic growth that could compromise the adhesion of the AOC 581 mastic. This process involves complete old roof tear-offs down to clean wood decking in areas where structural timber is utilized, ensuring a pristine bonding surface.

During the preparation phase, we execute a multi-step verification process to ensure the envelope is sound before any new materials are applied:

  • Performing complete existing roof tear-offs down to clean wood decking to eliminate old adhesives and degraded bitumen.
  • Stripping old shingles down to clean wood sheathing in transition zones where the industrial roof meets administrative office sections.
  • Inspecting the plywood deck and replacing damaged wood that exhibits signs of delamination, rot, or structural deflection.
  • Executing a high-pressure cleaning of the curb flashing to remove oxidation and contaminants that would inhibit the chemical bond of the structural mastic.
  • Conducting a moisture probe analysis to identify saturated areas of the deck that require immediate remediation.

By focusing on these granular details, we ensure that the AOC 581 application is not merely a topical fix but a structural integration into the building envelope. Without these rigorous prep steps, the mastic may adhere to a failing surface, leading to cohesive failure where the membrane peels away from the deck rather than the sealant failing at the curb.

Engineering the Fiber-Reinforced Trowel Application

The application of AOC 581 is a precision operation that requires a master roofer's touch and an engineer's understanding of material science. The mastic is not simply "applied"; it is engineered into a reinforced gasket. We utilize a fiber-reinforced trowel application technique, which embeds synthetic fibers within the elastomeric matrix. This reinforcement significantly increases the tear resistance of the seal, preventing the mechanical vibrations of the rooftop units from creating micro-fissures in the mastic.

The technical application sequence follows a strict forensic methodology:

  • A primary bonding agent is applied to the curb and the surrounding deck to create a chemical bridge.
  • The AOC 581 mastic is applied using a notched trowel to ensure consistent thickness and eliminate air voids that could lead to hydrostatic pressure buildup.
  • A reinforcing fabric mesh is embedded into the wet mastic, creating a composite layer that distributes mechanical stress across a wider surface area.
  • A final capping layer of elastomeric mastic is troweled over the mesh, creating a seamless, watertight transition from the vertical curb face to the horizontal roof plane.
  • The edges are tapered to prevent "water damming," ensuring that precipitation is shed away from the curb interface.

This composite structure transforms the curb seal from a static joint into a dynamic gasket. The fiber reinforcement allows the seal to expand and contract during extreme temperature fluctuations without losing its bond, effectively neutralizing the thermal drift that typically destroys standard commercial sealants.

Mitigating Mechanical Vibration and Thermal Drift

In a logistics hub, the rooftop environment is a volatile landscape of kinetic energy. Large mechanical units generate constant low-frequency vibrations that travel through the curb and into the roof deck. If the sealant is too rigid, these vibrations cause "fatigue cracking." If the sealant is too soft, it will slump over time. The AOC 581 system is engineered for a specific modulus of elasticity that balances these two extremes.

To ensure long-term performance, we rely on boots-on-the-roof assessments to verify the stability of the curbs before final sealing. These hands-on physical roof inspections allow us to identify subtle movements in the curb assembly that might indicate a failing support structure. By analyzing the vibration patterns of the equipment, we can adjust the thickness and reinforcement density of the mastic to provide maximum dampening where the stress is most acute.

The technical advantages of this approach include:

  • Reduction of stress concentrations at the curb-to-deck junction.
  • Elimination of capillary action by creating a non-porous, monolithic barrier.
  • Increased longevity of the primary membrane by reducing the frequency of curb-related leaks.
  • Enhanced structural stability of the envelope against wind-uplift forces acting on the mechanical equipment.

Quality Assurance and Final Envelope Certification

The final stage of our engineering process is the certification of the watertight seal. We do not rely on visual approximations; instead, we implement a forensic verification process to ensure that the AOC 581 detailing is impervious to water penetration. This involves a combination of hydrostatic testing and meticulous physical inspection of every linear inch of the curb perimeter.

Transparency in the remediation process is paramount. We provide our clients with free line-item written estimates that detail every phase of the project, from the initial tear-offs to the final mastic application. This ensures that the building owner understands the necessity of the substrate preparation and the specific engineering requirements of the fiber-reinforced system.

The result is a high-performance building envelope that can withstand the rigors of an industrial environment. By combining the precision of a master roofer with the analytical rigor of a building envelope engineer, we transform a common point of failure into a fortified asset. The integration of AOC 581, coupled with a commitment to clean wood decking and reinforced application, ensures that the logistics distribution hub remains dry, stable, and operationally efficient for the duration of its service life.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #047

UL 2218 Class 4 Severe Hail Defense on Commercial High-Rise Commercial Penthouse Towers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
UL 2218 Class 4 Severe Hail Defense on Commercial High-Rise Commercial Penthouse Towers

Engineering the Impact Zone: UL 2218 Class 4 Dynamics in Logistics Hubs

In the realm of industrial building envelope engineering, the logistics distribution hub represents a unique challenge due to its massive surface area and the catastrophic potential of severe hail events. When designing for UL 2218 Class 4 compliance—the highest rating for impact resistance—the objective is not merely to prevent a puncture, but to manage the kinetic energy transfer from the hailstone to the underlying insulation core. A failure in the cover board allows the energy to propagate directly into the polyisocyanurate (polyiso) core, leading to crushing, loss of R-value, and subsequent moisture infiltration.

From a forensic building science perspective, the primary goal is kinetic energy attenuation. When a high-velocity hailstone strikes a roof, the energy must be absorbed or dissipated across a wider surface area to prevent a localized breach. This is where the distinction between high-density (HD) polyiso cover boards and high-density gypsum boards becomes critical. The engineering focus shifts from simple compressive strength to the material's ability to deform plastically without catastrophic fracturing, thereby shielding the fragile insulation core below.

  • Kinetic Energy Management: Reducing the peak force of impact through material density and thickness.
  • Core Preservation: Ensuring the primary thermal barrier remains intact to prevent thermal bridging and structural degradation.
  • UL 2218 Class 4 Verification: Meeting the rigorous testing standards that simulate severe weather events to ensure long-term envelope integrity.

Compressive Strength and the Role of HD Polyiso Cover Boards

High-density polyiso cover boards are engineered to provide a rigid transition layer between the membrane and the insulation. In high-traffic logistics hubs, these boards must exhibit compressive strength exceeding 25 PSI to withstand the mechanical stresses of maintenance and the static loads of the roof system. While HD polyiso provides excellent structural rigidity and contributes to the overall thermal performance of the assembly, its behavior under sudden, high-velocity impact differs significantly from gypsum.

The primary function of an HD polyiso cover board is to distribute point loads across the insulation. However, because polyiso is a closed-cell foam, it possesses a certain degree of elasticity. While this is beneficial for static loads, it can be a liability during a severe hail event. If the impact force exceeds the material's threshold, the board can crack or "punch through," transferring the remaining kinetic energy directly into the primary insulation layers. This creates a vulnerability where the roof may appear intact from the surface, but the core is effectively crushed, compromising the building's energy efficiency and structural resilience.

  • Compressive Strength: Maintaining a threshold above 25 PSI to prevent sagging and deformation.
  • Load Distribution: Spreading the weight of equipment and personnel to avoid localized core compression.
  • Thermal Synergy: Providing a seamless thermal transition that reduces the risk of condensation within the assembly.

Forensic Analysis: High-Density Gypsum as a Kinetic Buffer

When the engineering requirement is strictly focused on severe hail defense, high-density gypsum cover boards often emerge as the superior technical choice. Unlike the cellular structure of polyiso, gypsum is a dense, crystalline material. This density allows the board to act as a sacrificial buffer. When a hailstone strikes a gypsum board, the material absorbs the energy through a process of localized crushing and fragmentation, which effectively attenuates the kinetic energy before it can reach the polyiso insulation core.

In forensic evaluations of Class 4 systems, gypsum boards demonstrate a superior ability to prevent "core bruising." By absorbing the shock, the gypsum layer ensures that the primary insulation remains undisturbed. This is critical for logistics hubs where the cost of internal repairs and operational downtime far outweighs the initial material cost of the cover board. The engineering trade-off is a slight increase in dead load, but the gain in impact resistance and the protection of the building envelope's thermal integrity provide a significant return on investment over the lifecycle of the facility.

  • Energy Attenuation: Converting kinetic energy into material deformation to protect the lower layers.
  • Impact Dissipation: Spreading the force of the strike across a wider radius than cellular foams.
  • Structural Shielding: Acting as a hard-shell barrier that prevents the "punch-through" effect common in lower-density systems.

Implementation Standards and Forensic Site Assessments

The transition from a failing roof system to a UL 2218 Class 4 assembly requires a rigorous approach to substrate preparation. We do not believe in overlays when the structural integrity of the envelope is at stake. Our process begins with complete old roof tear-offs down to clean wood decking to ensure that no trapped moisture or degraded materials compromise the new installation. For facilities with mixed-use sections, this involves complete existing roof tear-offs down to clean wood decking and stripping old shingles down to clean wood sheathing where administrative offices meet the distribution warehouse.

Once the substrate is exposed, we perform hands-on physical roof inspections. This is the only way to truly understand the condition of the deck. By inspecting the plywood deck and replacing damaged wood, we create a stable foundation for the high-density cover boards. These boots-on-the-roof assessments allow our engineers to identify soft spots or previous moisture intrusions that would render a Class 4 system ineffective. To ensure total transparency in the procurement and engineering phase, we provide free line-item written estimates that detail every phase of the tear-off and rebuild process.

  • Substrate Validation: Ensuring the deck is structurally sound before applying high-density materials.
  • Moisture Mitigation: Removing all previous layers to prevent the entrapment of vapor.
  • Precision Documentation: Utilizing line-item estimates to track the exact volume of gypsum or HD polyiso utilized across the hub's footprint.

Comparative Conclusion: Engineering the Optimal Envelope

For the logistics distribution hub, the choice between HD polyiso and gypsum cover boards depends on the specific risk profile of the region. If the primary concern is static load and thermal efficiency, HD polyiso with compressive strength exceeding 25 PSI is an excellent choice. However, if the facility is located in a high-frequency hail zone, the forensic evidence supports the use of high-density gypsum for its superior kinetic energy attenuation and core protection.

A truly resilient building envelope is the result of combining high-performance materials with a disciplined installation methodology. By prioritizing complete tear-offs and rigorous deck inspections, the engineer ensures that the UL 2218 Class 4 rating is not just a theoretical specification on a data sheet, but a physical reality that protects the asset for decades. The synergy of a clean substrate, a high-density buffer, and a high-performance membrane creates an industrial envelope capable of withstanding the most severe atmospheric challenges.

  • Final Recommendation: Prioritize gypsum cover boards for maximum hail attenuation in high-risk zones.
  • Operational Continuity: Reducing the risk of core failure ensures the facility remains operational after severe weather.
  • Lifecycle Value: Investing in a Class 4 assembly reduces long-term insurance premiums and maintenance costs.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #048

Non-Destructive Substrate Moisture Scans on Commercial Regional Healthcare Medical Centers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Non-Destructive Substrate Moisture Scans on Commercial Regional Healthcare Medical Centers

Forensic Analysis of Subsurface Moisture in Industrial Logistics Hubs

In the context of large-scale industrial logistics hubs, the building envelope serves as the primary defense against atmospheric ingress. When a compromise occurs in the membrane, the resulting moisture migration often remains undetected until the saturation reaches a critical threshold, potentially compromising the structural integrity of the substrate. For Aquashield Corporate, the objective of this technical case study is to delineate the methodology used to identify subsurface saturation boundaries without resorting to indiscriminate demolition. A forensic approach to building science requires a transition from subjective visual assessment to quantitative data acquisition.

The primary challenge in these expansive facilities is the sheer square footage, which makes traditional probing inefficient. To mitigate risk and cost, we implement a tiered diagnostic protocol that integrates non-destructive testing (NDT) to isolate moisture plumes. This allows the engineering team to differentiate between superficial condensation and deep-seated saturation within the insulation layers. By establishing a precise moisture map, we can avoid unnecessary costs and focus our efforts on the areas where the envelope has failed.

  • Identification of thermal anomalies via infrared thermography.
  • Quantification of moisture percentages using nuclear depth gauges.
  • Validation of data through strategic core sampling.
  • Implementation of surgical excision to remove compromised materials.
  • Verification of substrate health through boots-on-the-roof assessments.

Infrared Thermography: Mapping Thermal Anomalies and Saturation Plumes

Infrared Thermography (IRT) is the first phase of our forensic investigation. This process relies on the principle of thermal mass; wet insulation possesses a higher heat capacity than dry insulation. During the cooling phase of the diurnal cycle, areas of the roof that are saturated retain heat longer than the surrounding dry sections. By capturing these temperature differentials, we can visualize the "plume" of moisture as it radiates from the point of entry.

However, IRT is a screening tool, not a definitive measurement of moisture content. It identifies anomalies, not percentages. To ensure the accuracy of the map, we perform these scans during optimal thermal windows—typically at dawn or dusk—to maximize the contrast between wet and dry zones. This high-resolution mapping prevents the need for complete old roof tear-offs down to clean wood decking across the entire facility, allowing us to target only the compromised sectors.

  • Analysis of evaporative cooling patterns to locate subsurface water reservoirs.
  • Delineation of moisture boundaries to create a surgical excision map.
  • Correlation of thermal signatures with known structural vulnerabilities.
  • Reduction of unnecessary demolition through precise anomaly isolation.

Nuclear Depth Gauging: Validating Volumetric Moisture Thresholds

To move from qualitative thermal mapping to quantitative forensic data, we employ nuclear depth gauges. These instruments utilize a radioactive source to emit neutrons into the roof assembly. Because hydrogen atoms (the primary component of water) slow down these neutrons, the gauge can calculate the volumetric moisture content of the insulation and the substrate with extreme precision.

This step is critical for validating the thresholds that trigger material replacement. In industrial logistics hubs, a moisture content exceeding 20% to 30% in the insulation typically necessitates removal to prevent mold growth and substrate decay. By utilizing nuclear gauges, we can confirm whether a thermal anomaly is truly saturated or merely a result of varying insulation densities. This data is then cross-referenced with physical core samples to ensure the nuclear readings align with the actual physical state of the material.

  • Measuring the hydrogen density to determine exact moisture percentages.
  • Validating the depth of saturation within the polyisocyanurate or mineral wool layers.
  • Establishing a baseline for "dry" versus "saturated" thresholds.
  • Providing empirical evidence to justify the scope of the remediation project.

Surgical Excision and Substrate Remediation Protocols

Once the moisture boundaries are validated, the project shifts from diagnostics to remediation. Rather than performing a blanket replacement, we execute surgical wet insulation excision. This process involves removing only the saturated materials identified in the previous phases. This targeted approach minimizes waste and reduces the operational downtime for the logistics hub.

During this phase, hands-on physical roof inspections are paramount. Once the membrane is breached and the wet insulation is removed, the engineering team conducts boots-on-the-roof assessments to examine the condition of the deck. In areas where water has sat for extended periods, we may find it necessary to perform complete existing roof tear-offs down to clean wood decking to ensure no latent rot exists. This includes stripping old shingles down to clean wood sheathing in transition zones or peripheral sections of the building envelope.

  • Precision cutting of the membrane based on the IRT and nuclear moisture maps.
  • Removal of saturated insulation to stop the migration of moisture.
  • Inspecting the plywood deck and replacing damaged wood to restore structural capacity.
  • Application of high-performance primers to ensure a monolithic bond with the new assembly.

Engineering Validation and Final Envelope Restoration

The final phase of the project is the restoration of the building envelope. Before the new membrane is installed, we conduct a final audit of the substrate. This ensures that the surgical excision was successful and that no residual moisture remains trapped beneath the new layers. This forensic rigor is what separates industrial engineering from standard roofing; we are not simply covering a leak, but restoring the thermodynamic balance of the roof system.

To maintain transparency and technical accountability, Aquashield Corporate provides free line-item written estimates that detail every stage of the forensic process—from the initial nuclear scans to the final deck inspection. This ensures the facility manager understands the exact volume of material removed and the specific areas where we performed complete old roof tear-offs down to clean wood decking. The result is a validated, moisture-free envelope capable of withstanding the rigors of industrial logistics operations.

  • Final verification of substrate dryness via moisture probes.
  • Installation of a high-reflectivity membrane to reduce thermal stress.
  • Detailed documentation of all substrate repairs and wood replacements.
  • Post-installation thermal scan to confirm the absence of trapped moisture.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #049

Sub-Zero Cold Storage Downward Vapor Drive & Self-Adhered SBS Barriers on Commercial University Research Laboratorys

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Sub-Zero Cold Storage Downward Vapor Drive & Self-Adhered SBS Barriers on Commercial University Research Laboratorys

The Thermodynamics of Downward Vapor Drive in Sub-Zero Cold Storage

In industrial logistics distribution hubs featuring sub-zero cold storage, the building envelope faces a thermodynamic challenge known as inverted vapor drive. Unlike standard commercial structures where moisture typically migrates from the conditioned interior to the exterior, cold storage environments create a permanent temperature gradient where the exterior ambient air is significantly warmer than the interior refrigerated space. This creates a relentless pressure for water vapor to migrate from the warm exterior toward the cold interior. If the envelope is not engineered to arrest this movement, moisture will penetrate the assembly and reach its dew point within the insulation layers, leading to interstitial condensation.

This downward vapor drive can lead to catastrophic structural failure if the dew point is allowed to settle within the substrate or the thermal layers. When vapor reaches a surface temperature below its saturation point, it transitions from a gas to a liquid. In a sub-zero environment, this moisture can freeze, causing ice lensing and subsequent freeze-thaw cycles that degrade the structural integrity of the roofing assembly. To mitigate this, the building envelope must be designed as a monolithic vapor barrier, ensuring that the primary vapor retarder is positioned on the "warm side" of the insulation to prevent moisture from ever entering the thermal core.

  • Analysis of hygrothermal gradients to determine precise dew point locations.
  • Calculation of vapor permeability rates across multi-layered assemblies.
  • Mitigation of air leakage through perimeter detailing to prevent convective moisture transport.
  • Evaluation of the thermal bridge effect at parapet walls and roof-to-wall junctions.

Forensic Substrate Preparation and Deck Integrity Analysis

The efficacy of any high-performance vapor barrier is entirely dependent on the condition of the underlying substrate. In our forensic approach to these distribution hubs, we emphasize the necessity of hands-on physical roof inspections to identify latent defects that cannot be seen through imaging. These boots-on-the-roof assessments allow our engineers to evaluate the structural rigidity of the deck and identify areas of saturation or delamination that would compromise the adhesion of a self-adhered SBS membrane.

For existing facilities requiring a thermal upgrade, we mandate complete existing roof tear-offs down to clean wood decking. This ensures that no trapped moisture remains within the old assembly, which could otherwise migrate upward and cause blistering in the new membrane. In scenarios involving mixed-use sections of the hub, we perform stripping old shingles down to clean wood sheathing to ensure a uniform plane for the industrial-grade barriers. This process includes inspecting the plywood deck and replacing damaged wood to guarantee a substrate that meets the strict load-bearing and adhesion requirements of a sub-zero envelope.

Once the substrate is cleared, we provide free line-item written estimates that detail the exact scope of the remediation. This level of transparency is critical when performing complete old roof tear-offs down to clean wood decking, as it allows the facility manager to understand the relationship between substrate health and the longevity of the vapor barrier. A clean, structurally sound deck is the only acceptable foundation for an industrial SBS application.

  • Rigorous verification of deck flatness to prevent membrane bridging.
  • Removal of all legacy adhesives and fasteners to ensure a monolithic bond.
  • Detailed mapping of substrate anomalies during the inspection phase.
  • Replacement of compromised sheathing to maintain structural diaphragm strength.

Engineering the Self-Adhered SBS Vapor Barrier

To combat the aggressive downward vapor drive of a cold storage hub, we utilize self-adhered SBS (Styrene-Butadiene-Styrene) modified bitumen barriers. Unlike torch-applied or cold-process adhesives, self-adhered SBS provides a consistent, factory-applied adhesive bond that eliminates the risk of human error during installation. This creates a continuous, air-tight seal across the entire deck, effectively stopping vapor migration at the first line of defense. The SBS polymer provides the necessary elasticity to accommodate the thermal contraction and expansion inherent in sub-zero environments without cracking or losing its seal.

The forensic advantage of SBS in this application is its extremely low vapor permeability. By installing the SBS barrier directly onto the clean wood decking, we shift the dew point entirely outside the building's structural shell. This ensures that any condensation that occurs happens on the exterior of the membrane rather than within the insulation or the decking. The self-adhering nature of the membrane also prevents the "wind-wash" effect, where exterior air penetrates the insulation and lowers its R-value, further stabilizing the thermal envelope.

  • Utilization of high-performance SBS polymers for enhanced puncture resistance.
  • Implementation of reinforced lap seams to prevent vapor bypass.
  • Application of a monolithic seal to eliminate interstitial air pockets.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565

Commercial Engineering Dossier #050

Structural Deck Fastener Pull-Out Testing on 22-Gauge Corrugated Steel Decks on Commercial Suburban Corporate Office Parks

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Structural Deck Fastener Pull-Out Testing on 22-Gauge Corrugated Steel Decks on Commercial Suburban Corporate Office Parks

Audit Framework for Structural Deck Integrity in High-Volume Logistics Hubs

In the context of a large-scale logistics distribution hub, the building envelope is subjected to extreme stressors, ranging from internal atmospheric pressure fluctuations to external wind-uplift forces. The structural integrity of the roof system is fundamentally dependent on the connection between the roofing membrane, the insulation, and the 22-gauge corrugated steel deck. A comprehensive engineering audit must move beyond visual inspection and enter the realm of quantitative mechanical verification. When dealing with 22-gauge steel, the margin for error regarding fastener engagement is slim; the thickness of the substrate dictates a specific torque and penetration depth to ensure that the fastener does not strip the metal or fail to achieve the required grip.

Our audit framework focuses on the synergy between the fastener's thread geometry and the steel deck's profile. In a facility of this magnitude, inconsistent fastener installation can lead to localized failures that compromise the entire wind-uplift rating of the roof. The objective is to establish a baseline of withdrawal resistance that aligns with the original structural blueprints and current building codes. We analyze the deck's gauge consistency across different spans to ensure that the 22-gauge specification was maintained during fabrication and installation.

  • Verification of steel deck gauge using calibrated digital calipers.
  • Assessment of fastener spacing relative to the manufacturer's wind-uplift map.
  • Evaluation of the interface between the thermal insulation and the steel substrate.
  • Identification of "soft spots" or areas of premature oxidation in the corrugated troughs.
  • Review of original architectural specifications versus as-built conditions.

Calibrated Mechanical Pull Testing and Withdrawal Resistance

To quantify the actual holding power of the fastening system, we employ calibrated mechanical pull testing. This process involves the use of a digital hydraulic pull-tester designed to apply a linear axial force to the fastener until either a predetermined threshold is reached or the fastener fails. For 22-gauge corrugated steel, the goal is to determine the minimum withdrawal resistance—the amount of force required to pull the fastener completely out of the deck. This is not a destructive test by default, but rather a sampling method to ensure the system meets the required pounds-per-square-inch (PSI) thresholds defined by ASTM standards.

The testing protocol requires a strategic distribution of test points across the roof's perimeter, corners, and field areas, as these zones experience vastly different wind pressures. We measure the "peak load" at the moment of displacement. If a fastener pulls out at a value lower than the engineering requirement, it indicates either an incorrect fastener length, a failure in the thread engagement, or a compromise in the structural integrity of the steel deck itself. This data allows us to calculate a confidence interval for the rest of the roof's fastening system.

  • Utilization of ASTM E1592 standards for the testing of fasteners in structural steel.
  • Application of incremental load increases to monitor elastic vs. plastic deformation.
  • Mapping of pull-out values to identify systemic installation failures versus isolated anomalies.
  • Comparison of field-tested withdrawal values against theoretical manufacturer data.
  • Documentation of the "failure mode," distinguishing between thread stripping and substrate tearing.

Fastener Corrosion Diagnostics and Material Science

A critical component of the building envelope audit is the diagnostic analysis of fastener corrosion. In industrial logistics hubs, the interior environment often contains pollutants or humidity levels that can accelerate galvanic corrosion. When a fastener of one metal composition is driven into a 22-gauge steel deck with a different coating—such as galvanized or G90 steel—an electrochemical reaction can occur. This is particularly prevalent if the fastener's protective coating is compromised during installation (e.g., over-torquing), exposing the raw steel core to the atmosphere.

We examine the fasteners for signs of "red rust" (iron oxide) or "white rust" (zinc oxide), which indicate the breakdown of the sacrificial coating. Corrosion at the point of penetration is especially dangerous because it reduces the effective diameter of the fastener shank and weakens the grip of the threads within the 22-gauge steel. This degradation leads to a significant drop in withdrawal resistance, effectively rendering the wind-zone calculations obsolete. Our analysis includes a microscopic inspection of the fastener head and shank to determine the depth of the oxidation.

  • Analysis of galvanic incompatibility between the fastener alloy and the steel deck coating.
  • Inspection for "over-driven" fasteners that have compromised the deck's structural flange.
  • Evaluation of the impact of industrial off-gassing on the longevity of the fastener coatings.
  • Assessment of moisture infiltration paths that lead to interstitial corrosion.
  • Determination of the remaining structural cross-section of the fastener shank.

Wind-Zone Schedules and Structural Remediation Strategies

The final phase of the engineering audit involves reconciling the pull-test data with the ASCE 7 wind-zone schedules. A logistics hub's roof is divided into zones—Zone 1 (field), Zone 2 (perimeter), and Zone 3 (corners)—each requiring different fastener densities to resist uplift. If the mechanical pull testing reveals that the withdrawal resistance is below the threshold required for the specific wind zone of the facility, the roof is technically non-compliant and at risk of catastrophic failure during a high-wind event.

Remediation is not always as simple as adding more fasteners. Over-fastening a 22-gauge deck can lead to "swiss-cheesing," where the structural integrity of the steel is compromised by too many penetrations. Instead, we recommend a targeted remediation strategy. This may involve the installation of oversized "repair" fasteners or the application of structural adhesive reinforcements in high-pressure zones. The goal is to bring the entire envelope into compliance with the wind-uplift requirements while preserving the longevity of the steel substrate.

  • Recalculation of uplift pressures based on current local building codes and wind-zone maps.
  • Development of a fastener density increase plan for Zone 2 and Zone 3 areas.
  • Specification of high-performance, corrosion-resistant fasteners for remediation.
  • Implementation of a long-term monitoring schedule for fastener tension and integrity.
  • Final certification of the building envelope's structural capacity to withstand design-basis wind loads.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565

Commercial Engineering Dossier #051

Electronic Vector Mapping (EVM) Low-Voltage Membrane Breach Detection on Commercial Big-Box Retail Power Centers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Electronic Vector Mapping (EVM) Low-Voltage Membrane Breach Detection on Commercial Big-Box Retail Power Centers

The Engineering Challenge of Large-Scale Distribution Hubs

In the realm of commercial building envelope engineering, the logistics distribution hub represents one of the most demanding environments for roof membrane integrity. These structures typically feature massive footprints, often exceeding 500,000 square feet, where the sheer scale of the roof surface creates a statistical inevitability for installation anomalies or mechanical punctures. The primary challenge is not the catastrophic failure of a seam, but rather the "silent killer": microscopic pinhole punctures. These breaches are often invisible to the naked eye and remain undetected until moisture has migrated deep into the insulation core, compromising the R-value and triggering structural degradation of the steel decking.

Traditional leak detection methods, such as infrared thermography and moisture probes, are fundamentally reactive. Infrared scanning requires a specific thermal delta between wet and dry insulation, meaning a leak must already be significant enough to saturate a large area before it becomes visible. Moisture probes, while accurate, are invasive and require a "grid-search" approach that is labor-intensive and often destructive. For a facility of this magnitude, a reactive strategy is an engineering failure. The objective is to transition from reactive patching to a proactive, non-destructive certification of the entire envelope.

  • Scale-induced vulnerability: Increased probability of installation errors over massive surface areas.
  • The limitation of IR: Dependence on thermal gradients and atmospheric conditions.
  • The risk of capillary action: How microscopic breaches allow water to travel horizontally far from the entry point.
  • Substrate saturation: The long-term impact of moisture on polyisocyanurate (ISO) insulation and metal decking.

The Architecture of Conductive Vector Grids

To solve the problem of invisible breaches, we implement Electronic Vector Mapping (EVM) utilizing a conductive underlayment grid. Unlike standard membranes, an EVM-integrated system incorporates a low-voltage conductive layer situated directly beneath the primary waterproofing membrane. This layer acts as a continuous electronic sensor. By applying a controlled, low-voltage electrical current across the grid, we establish a baseline of electrical resistance across the entire roof plane. This transforms the building envelope from a passive barrier into an active diagnostic tool.

The engineering behind the conductive grid relies on the principle of dielectric resistance. The primary membrane acts as an insulator, preventing the current in the conductive grid from escaping. However, if the membrane is breached—even by a puncture as small as a needle—the introduction of moisture creates a conductive path. Because water is an efficient conductor, the breach alters the electrical signature of the grid at a specific coordinate. By monitoring the voltage drop and current flow, the system can identify the exact location of the anomaly without the need for physical inspection of every square inch.

  • Conductive Underlayment: A specialized layer that allows for precise electrical monitoring.
  • Low-Voltage Circuitry: The use of safe, low-amperage currents to avoid interference with building electronics.
  • Dielectric Properties: Leveraging the insulating nature of the membrane to detect conductive anomalies.
  • Baseline Calibration: Establishing a "zero-state" electrical map during the initial installation phase.

Pinpointing Microscopic Breaches via Vector Mapping

The true power of EVM lies in its ability to perform vector analysis to pinpoint the exact coordinates of a breach. When a pinhole puncture occurs, the moisture that enters the breach creates a localized "short" in the conductive grid. The EVM hardware analyzes the vector of the current flow, calculating the intersection of the X and Y axes of the grid. This allows the engineering team to narrow down a potential leak from a 100,000-square-foot quadrant to a specific 12-inch diameter circle.

This precision is critical during the quality certification phase. During a post-installation audit, we can subject the roof to controlled hydrostatic pressure tests or vacuum tests. If a breach exists, the EVM system flags it instantly. This eliminates the "needle in a haystack" scenario common in commercial roofing. Instead of cutting exploratory holes into the membrane—which ironically creates more leaks—we use the electronic map to perform surgical repairs. This ensures that the membrane's monolithic integrity is maintained while ensuring 100% water-tightness.

  • Coordinate Mapping: Using X-Y axis intersections to locate breaches with surgical precision.
  • Anomaly Detection: Identifying deviations in electrical resistance that signal moisture ingress.
  • Non-Destructive Testing (NDT): Verifying the envelope without compromising the membrane's physical structure.
  • Surgical Remediation: Applying targeted repairs only where the vector map indicates a failure.

Non-Destructive Quality Certification and Life-Cycle Assurance

From a master roofer's perspective, the goal of any installation is not just to pass a visual inspection, but to achieve a certified building envelope. By utilizing EVM, Aquashield Corporate provides a non-destructive quality certification that adheres to the highest ASTM and ANSI standards for membrane integrity. This certification serves as a technical guarantee that the roof is free of microscopic punctures and installation defects. It provides the facility owner with a documented "birth certificate" of the roof's performance, ensuring that the asset is protected from day one.

Furthermore, the EVM system provides unparalleled life-cycle assurance. As the building ages and undergoes maintenance—such as HVAC unit replacements or solar panel installations—the risk of accidental punctures increases. Because the conductive grid remains active, the facility manager can perform periodic "health checks" of the roof. Any new breach is detected immediately, allowing for repair before the moisture can migrate into the substrate. This shifts the maintenance paradigm from expensive, large-scale rehabilitations to minor, preventative maintenance, significantly extending the operational lifespan of the roof system.

  • ASTM Compliance: Ensuring the membrane meets rigorous industry standards for puncture resistance and water tightness.
  • Asset Protection: Reducing the risk of structural steel corrosion and insulation failure.
  • Operational Continuity: Avoiding the business disruptions associated with major leak remediation.
  • Lifecycle Extension: Transitioning to a predictive maintenance model based on electronic diagnostics.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #052

Liquid-Applied PMMA & Polyurethane Fleece-Reinforced Flashing Resins on Commercial Food Packaging & Cold Logistics Plants

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Liquid-Applied PMMA & Polyurethane Fleece-Reinforced Flashing Resins on Commercial Food Packaging & Cold Logistics Plants

Engineering Audit: Substrate Vulnerabilities in High-Volume Logistics Hubs

From a building envelope perspective, the logistics distribution hub represents one of the most challenging environments for a commercial roofer. These facilities are characterized by massive surface areas, extreme thermal expansion and contraction cycles, and a high density of structural penetrations. During the engineering audit of the subject facility, the primary point of failure was identified at the transition zones between the primary roof membrane and the structural I-beam stanchions. Traditional sheet-applied membranes, while effective on flat planes, often fail at these intricate junctions due to mechanical stress and the inability to maintain a consistent bond across complex 3D geometries.

The audit revealed that previous flashing attempts relied on heavy-duty adhesives and mechanical fasteners that created "stress risers" in the membrane. In a high-velocity logistics environment, vibration from heavy machinery and HVAC systems accelerates the degradation of these bond lines. To ensure long-term envelope integrity, the transition from a flexible membrane to a rigid structural element must be managed through a monolithic, liquid-applied system that eliminates seams and bridging.

  • Assessment of Concrete Surface Profile (CSP) to ensure optimal mechanical adhesion of resins.
  • Evaluation of thermal movement joints and their impact on flashing longevity.
  • Analysis of moisture vapor transmission rates (MVTR) across the stanchion interfaces.
  • Verification of ASTM D-series standards for peel strength and adhesion testing.
  • Identification of "cold spots" where condensation promotes premature substrate oxidation.

PMMA Chemistry and the Kinetics of Rapid Cure Systems

To address the identified vulnerabilities, the specification shifted toward Polymethyl Methacrylate (PMMA) cold-applied resins. Unlike traditional bitumen or TPO, PMMA is a thermosetting plastic that cures via a chemical reaction rather than solvent evaporation. The kinetics of PMMA are driven by a catalyst—typically a peroxide-based initiator—which triggers a rapid polymerization process. This allows the resin to transition from a liquid state to a fully cured, hard-wearing solid in a matter of minutes, regardless of ambient temperature, provided the catalyst ratio is precisely calibrated.

This rapid cure kinetic is critical for logistics hubs where operational downtime is financially catastrophic. The ability to apply a high-performance flashing and return the area to full service within hours, rather than days, provides a significant logistical advantage. Furthermore, PMMA exhibits exceptional UV stability and resistance to chemical pollutants, ensuring that the flashing does not embrittle over time when exposed to the harsh environmental conditions typical of industrial loading docks.

  • Cold-applied application eliminates the risk of torch-applied fire hazards in industrial settings.
  • Catalyst-controlled curing allows for precise timing of the "tack-free" state.
  • High glass transition temperature (Tg) ensures stability under extreme thermal loads.
  • Superior chemical resistance against oils, fuels, and industrial solvents.
  • Seamless integration with existing modified bitumen or single-ply membranes.

Fleece-Reinforced Integration and Tensile Strength Enhancement

While PMMA provides the chemical bond and hardness, the structural integrity of the flashing is achieved through the embedding of a non-woven polyester fleece. In the field, this is a multi-stage process: a primer is applied, followed by a base layer of resin, into which the fleece is fully saturated and embedded. This creates a fiber-reinforced polymer (FRP) composite. The fleece acts as the "skeleton" of the flashing, distributing tensile stresses across the entire surface area rather than concentrating them at a single point of failure.

The integration of the fleece is particularly vital at the corners of I-beam stanchions. By embedding the reinforcement, we eliminate the risk of "bridging"—a common failure where the membrane pulls away from a concave corner, leaving a void. The resulting monolithic layer is not only waterproof but possesses the mechanical strength to withstand the physical impacts and vibrations inherent in a distribution center. This composite approach transforms the flashing from a simple seal into a structural component of the building envelope.

  • Elimination of seams through the use of liquid-applied reinforcement.
  • Increased puncture resistance and abrasion durability via polyester fiber matrix.
  • Prevention of stress-cracking at high-movement junctions.
  • Enhanced thickness control to meet strict engineering specifications.
  • Creation of a monolithic bond that fuses the substrate and the reinforcement into one unit.

Complex Detailing: I-Beam Stanchions and Termination Engineering

The final and most critical phase of the engineering implementation is the detailing of the I-beam stanchions. These structural elements present a complex geometry of flanges and webs that are notoriously difficult to flash with traditional materials. Using a combination of PMMA for rapid hardening and Polyurethane resins for targeted flexibility, the flashing is "wrapped" around the steel. The liquid nature of the resins allows them to flow into every crevice of the I-beam, ensuring 100% contact and eliminating the air pockets that typically lead to interstitial condensation and corrosion.

Termination is handled through a dual-stage approach. The top edge of the flashing is integrated into a termination bar or a high-performance sealant bead, ensuring a watertight seal against the vertical face of the stanchion. By utilizing a polyurethane-based top-coat in specific high-movement zones, we introduce a degree of elasticity that accommodates the micro-movements of the steel frame without compromising the bond. This hybrid approach—combining the rigidity of PMMA with the flexibility of polyurethane—creates a resilient envelope that meets the most stringent ANSI and ASTM requirements for industrial waterproofing.

  • 360-degree encapsulation of structural steel to prevent moisture ingress.
  • Application of specialized primers to ensure chemical bonding to galvanized or primed steel.
  • Use of termination bars to provide mechanical security at the upper flashing limits.
  • Integration of a UV-stable top-coat to protect the resin matrix from degradation.
  • Implementation of a multi-layered redundancy system to ensure zero-leakage tolerances.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565

Commercial Engineering Dossier #053

Commercial Expansion Joint Bellows & Heavy-Gauge Neoprene Movement Transitions on Commercial Semiconductor Cleanroom Fabs

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Commercial Expansion Joint Bellows & Heavy-Gauge Neoprene Movement Transitions on Commercial Semiconductor Cleanroom Fabs

Structural Dynamics and Differential Settlement in Large-Scale Logistics Hubs

In the realm of commercial building envelope engineering, few challenges are as complex as the management of structural movement in massive logistics distribution hubs. These facilities, often exceeding one million square feet, are not monolithic entities but are instead composed of multiple wings and structural bays. The primary driver of envelope failure in these environments is differential settlement—the phenomenon where different sections of the building sink or shift at varying rates due to inconsistent soil bearing capacities or uneven loading from heavy racking systems and high-density inventory.

From a master roofer's perspective, the roof is not merely a covering but a flexible skin that must accommodate the constant breathing of the building. Thermal expansion and contraction, driven by the vast surface area of steel decking and membrane, create significant shear forces at the points where different structural wings meet. If the building envelope is rigid, these forces inevitably lead to catastrophic failures, including membrane tearing, fastener pull-out, and compromised flashing. To mitigate this, we implement strategic expansion joints that decouple the building's sections, allowing them to move independently without compromising the watertight integrity of the system.

  • Analysis of soil compaction reports to predict differential settlement vectors.
  • Calculation of thermal expansion coefficients based on regional temperature swings and roof color (SRI).
  • Identification of high-stress zones at the intersection of primary structural columns and expansion gaps.
  • Evaluation of slab-on-grade movement and its corresponding impact on the upper envelope.

Engineering the Elastomeric Bellows and Neoprene Movement Transitions

When addressing the gap between two moving structural sections, a standard flashing detail is insufficient. We utilize heavy-gauge neoprene movement transitions and elastomeric bellows designed specifically for high-amplitude displacement. These bellows act as an accordion-style bridge, providing a continuous waterproof barrier that can expand and contract along a linear axis. The material science here is critical; we specify neoprene for its superior ozone resistance and high tensile strength, ensuring that the material does not succumb to "stress cracking" under repeated cycles of elongation.

The engineering of the bellows must account for the maximum anticipated movement (MAM) of the structure. A bellows system that is too tight will tear during a thermal peak, while one that is too loose may sag, creating a catchment area for ponding water and debris. We adhere to ASTM standards for elastomeric materials to ensure that the neoprene gauge is sufficient to withstand wind uplift and incidental foot traffic during maintenance. The geometry of the bellows is designed to distribute tension evenly across the entire width of the joint, preventing localized stress concentrations that typically lead to premature failure in inferior installations.

  • Selection of neoprene gauges based on ASTM D412 standards for tensile strength and elongation.
  • Integration of reinforced bellows geometry to prevent "ballooning" under hydrostatic pressure.
  • Verification of movement capacity against structural engineer specifications for seismic and thermal drift.
  • Assessment of UV-resistant coatings to prevent the degradation of the elastomeric compound.

Critical Tie-ins and Watertight Interface Management

The most vulnerable point of any expansion joint system is the tie-in—the interface where the flexible bellows meets the static roof membrane. Whether the primary roof is TPO, PVC, or EPDM, the transition must be seamless. A master tradesman knows that the failure is rarely in the center of the bellows, but almost always at the perimeter termination. To ensure a watertight seal, we employ a multi-layered flashing approach that incorporates mechanical termination bars and high-performance elastomeric sealants.

The installation sequence begins with the precise preparation of the substrate, ensuring that the transition zone is free of contaminants. We utilize heat-welded membranes for TPO/PVC systems to create a molecular bond, but because the bellows must move, we introduce a "floating" flashing detail. This involves a secondary layer of reinforced membrane that is adhered to the bellows but allowed to slide slightly beneath the primary roof surface. This prevents the movement of the joint from pulling the main roof membrane away from its fasteners, which would otherwise create a systemic failure across the entire roof wing.

  • Implementation of heavy-duty aluminum termination bars with neoprene gaskets to lock the bellows in place.
  • Application of industrial-grade, non-sagging polyether sealants at all perimeter junctions.
  • Execution of heat-welded "floating" flashing laps to accommodate lateral shift.
  • Verification of slope-to-drain patterns to ensure water does not dwell at the transition interface.

Audit Findings and Long-Term Maintenance Protocols

A comprehensive engineering audit of a logistics hub's envelope reveals that the longevity of movement transitions is directly proportional to the rigor of the maintenance schedule. During our audits, we frequently encounter "stiffening" of the neoprene due to chemical exposure or extreme UV degradation, which reduces the bellows' ability to absorb movement. Once the material loses its elasticity, the stress is transferred directly to the tie-ins, leading to the "unzipping" of the membrane from the structural deck.

To prevent these failures, we establish a preventative maintenance protocol based on the lifecycle analysis of the elastomeric components. This includes biannual inspections focusing on the integrity of the sealants and the physical condition of the bellows folds. We utilize ASTM E2128 standards for moisture scanning to detect any subsurface leaks at the expansion joints before they manifest as interior drips. By treating the expansion joint as a mechanical component with a finite service life rather than a permanent fixture, we can extend the overall lifespan of the building envelope and avoid the massive costs associated with emergency structural leaks.

  • Biannual physical inspection of bellows for signs of ozone cracking or material fatigue.
  • Infrared thermography to identify trapped moisture within the transition flashing.
  • Testing of sealant adhesion and elasticity using a durometer to ensure material compliance.
  • Scheduled replacement of perimeter gaskets and sealants every five to seven years depending on environmental exposure.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #054

Commercial Kitchen Grease Containment & 304 Stainless Steel Catchment Shielding on Commercial Intermodal Cargo Freight Terminals

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Commercial Kitchen Grease Containment & 304 Stainless Steel Catchment Shielding on Commercial Intermodal Cargo Freight Terminals

The Chemical Conflict: Lipid Degradation of Single-Ply Membranes

In the context of a high-volume Logistics Distribution Hub, the integration of commercial kitchen facilities introduces a severe chemical threat to the building envelope. The primary concern is the discharge of aerosolized animal fats and lipids from kitchen exhaust systems. When these lipids settle on a single-ply roofing membrane—whether TPO, PVC, or EPDM—they initiate a process of chemical degradation that compromises the structural integrity of the polymer. Animal fats are not inert; they act as aggressive solvents that can penetrate the molecular matrix of the membrane.

The most critical failure mechanism observed in these environments is plasticizer migration. In PVC and certain TPO formulations, the plasticizers that provide flexibility and elongation are leached out by the lipid compounds. As the lipids integrate into the membrane, they displace these essential components, leading to a localized loss of elasticity. This results in a membrane that becomes brittle and prone to stress-cracking, particularly around the high-movement areas of the roof penetrations and flashing details.

  • Polymer Softening: The initial phase where the membrane becomes tacky or "gummy" to the touch, indicating the breakdown of the polymer chain.
  • Tensile Strength Reduction: A measurable decrease in the membrane's ability to withstand wind uplift or thermal expansion/contraction.
  • Puncturing Vulnerability: Brittle membranes lose their puncture resistance, making them susceptible to damage during routine maintenance or debris impact.
  • Adhesive Failure: Lipids can seep beneath the membrane edges, compromising the bond between the field membrane and the flashing adhesives.

Engineering the Primary Containment: 304 Stainless Steel Catchment Shielding

To mitigate the risk of lipid-induced failure, a master roofer must implement a primary containment system that isolates the exhaust discharge from the roofing substrate. The industry standard for this application is the installation of custom-fabricated 304 Stainless Steel catchment shielding. Unlike galvanized steel or aluminum, 304 Stainless Steel offers superior resistance to the corrosive nature of heated grease and the caustic cleaning agents often used to maintain exhaust vents. The goal is to create a physical barrier that intercepts all condensate and grease runoff before it ever contacts the membrane.

The engineering of the catchment box must account for hydrostatic pressure and the viscosity of the grease. A properly designed system utilizes a deep-dish catchment tray with fully welded, leak-proof seams. The tray is integrated into the exhaust vent's discharge point and sloped precisely toward a dedicated grease collection port. This ensures that lipids are channeled into a removable containment vessel rather than overflowing onto the roof surface during peak operation or heavy precipitation events.

  • Material Gauge: Utilization of 16-gauge or 18-gauge 304 Stainless Steel to ensure structural rigidity and resistance to thermal warping.
  • Welded Integrity: All joints must be TIG welded and ground smooth to eliminate capillary gaps where grease could migrate.
  • Drip Edge Geometry: Implementation of an outward-facing drip edge to prevent "wicking," where liquids travel back along the underside of the metal and onto the roof.
  • Mechanical Isolation: The use of neoprene or EPDM gaskets between the stainless steel shielding and the roof membrane to prevent galvanic corrosion and mechanical abrasion.

Sacrificial Layering and Chemical-Resistant Coatings

Even with primary stainless steel containment, the risk of "overspray" or accidental spills remains. A robust building envelope strategy requires a secondary line of defense in the form of sacrificial chemical-resistant coatings. Relying solely on the base membrane in a grease-heavy environment is a failure of engineering. Instead, we specify a high-build, liquid-applied polyurethane or a specialized chemical-resistant membrane that is applied to the area surrounding the exhaust system.

These coatings act as a sacrificial layer, absorbing the chemical brunt of any lipid exposure. Because these coatings are formulated to be chemically inert to animal fats, they prevent the lipids from reaching the underlying TPO or PVC. When the coating eventually degrades or becomes saturated with grease, it can be mechanically stripped and reapplied without requiring a full tear-off of the primary roofing system. This approach transforms a potential catastrophic membrane failure into a routine maintenance event.

  • High-Build Polyurethane: Selected for its exceptional adhesion and ability to create a seamless, non-porous barrier.
  • UV Stability: Ensuring the coating is aliphatic to prevent chalking and degradation under intense solar radiation.
  • Elongation Properties: The coating must possess a similar coefficient of thermal expansion as the roof membrane to prevent delamination during temperature swings.
  • Application Depth: Applying the coating at a minimum of 60 to 80 mils (wet film thickness) to ensure a durable, impenetrable shield.

Long-term Maintenance Protocols and Envelope Integrity Audits

The installation of high-end hardware and coatings is only as effective as the maintenance regime supporting them. A commercial building envelope audit for a logistics hub must include a specific "Grease Management" section. This involves a scheduled inspection cycle that focuses on the accumulation of lipids within the catchment systems and the condition of the sacrificial coatings. Neglecting the removal of accumulated grease can lead to overflow, which bypasses the shielding and exposes the membrane to the very chemicals we have worked to isolate.

Engineering audits should be performed quarterly, utilizing ASTM E2128 standards for infrared thermography to detect any subsurface moisture or anomalies beneath the coated areas. By monitoring the thermal signature of the roof, we can identify if grease has penetrated the sacrificial layer and is trapping moisture against the membrane, which could lead to premature blistering or loss of adhesion. A proactive audit ensures that the containment system is functioning as designed and that the building envelope remains airtight and watertight.

  • Grease Vessel Evacuation: Scheduled purging of the 304 Stainless Steel catchments to prevent overflow.
  • Coating Integrity Checks: Visual and tactile inspections of the sacrificial layers to identify cracking, peeling, or saturation.
  • Sealant Audit: Examination of all perimeter sealants and flashing transitions for signs of lipid-induced softening.
  • Drainage Verification: Testing the slope and flow of the catchment system to ensure no standing lipids are accumulating in the tray.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #055

Clear-Span Structural Joist Deflection Forensics & Ponding Instability Remediation on Commercial Port Marine Shipping Warehouses

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Clear-Span Structural Joist Deflection Forensics & Ponding Instability Remediation on Commercial Port Marine Shipping Warehouses

Forensic Analysis of Structural Deflection and Center-Span Variance

In the context of large-scale logistics distribution hubs, the structural integrity of the roof deck is often compromised by the sheer scale of clear-span joists. During our engineering audit of the facility, we identified significant center-span deflection, a phenomenon where the structural members bow downward under the cumulative weight of the dead load and environmental stressors. This is not merely a cosmetic issue but a critical failure of the building envelope's primary drainage plane. To quantify this, our team utilized high-precision laser leveling and digital transit instruments to map the roof's topography, identifying "low spots" where the joists had deviated from their original engineered camber.

The forensic investigation revealed that the deflection was exacerbated by the long-term creep of the steel members, likely compounded by inadequate initial bracing or unforeseen loading during the facility's operational lifecycle. When a clear-span joist deflects, it creates a concave basin that disrupts the intended flow of rainwater toward the primary scuppers and internal drains. This structural variance transforms a nominally flat roof into a series of catchment areas, initiating a dangerous cycle of hydrostatic loading that threatens the overall stability of the roof assembly.

  • Measurement of total vertical displacement relative to the bearing points at the perimeter walls.
  • Identification of "dead zones" where the slope falls below the minimum 1/4" per foot requirement.
  • Analysis of joist spacing and the corresponding tributary areas contributing to the center-span dip.
  • Evaluation of existing membrane tension and the presence of "alligatoring" or stress fractures in the low points.
  • Correlation between structural deflection and historical leak patterns documented by facility management.

The Mechanics of Ponding Instability and Hydrostatic Loading

The most critical risk identified during the audit was the onset of ponding instability. In commercial roofing, ponding occurs when water remains on the roof for more than 48 hours; however, instability occurs when the weight of that standing water causes further deflection of the structural members, which in turn allows more water to accumulate. This is a positive feedback loop of structural failure. Water weighs approximately 62.4 pounds per cubic foot, and in a distribution hub with massive spans, a few inches of standing water can add thousands of pounds of unplanned load to the center of the joist.

From a material science perspective, this standing water accelerates the degradation of the roofing membrane through a process called plasticizer migration. The constant saturation softens the membrane and puts immense pressure on the seams, eventually leading to a breach. Once the envelope is compromised, water infiltrates the insulation layer, increasing the dead load further and potentially causing the insulation to saturate and lose its thermal resistance and compressive strength, further contributing to the dip in the structural profile.

  • Calculation of the critical load threshold where deflection becomes self-sustaining.
  • Assessment of the "ponding cycle" and its impact on the structural fatigue of the steel joists.
  • Analysis of membrane saturation and the resulting increase in dead load on the roof deck.
  • Evaluation of the impact of thermal expansion and contraction on the depth of the ponding areas.
  • Review of ASTM standards regarding minimum slope requirements to prevent water stagnation.

Engineering the Remediation: Custom Tapered Polyiso Crickets

To remediate the ponding instability, we moved away from simple "patching" and instead implemented a comprehensive drainage redesign using custom-cut tapered polyisocyanurate (polyiso) insulation. The objective was to create a positive slope from the center-span low points toward the existing drainage outlets. By installing tapered polyiso crickets—essentially wedge-shaped insulation boards—we can effectively "fill" the structural dips and redirect the water flow. This method is superior to adding layers of roofing because it addresses the root cause of the water accumulation without adding excessive weight to the already stressed joists.

The engineering of these crickets requires a precise slope calculation to ensure that water does not simply migrate from one low spot to another. We utilized a custom layout based on the laser-mapped topography of the roof. The polyiso material was selected for its high compressive strength and excellent R-value, ensuring that the building's energy efficiency is maintained while the structural slope is corrected. These crickets are strategically placed to break up large flat areas and force water into a linear path toward the perimeter, eliminating the possibility of future ponding.

  • Development of a custom tapering plan based on the specific deflection measurements of each joist bay.
  • Selection of high-density polyiso boards to withstand the compressive loads of the new slope.
  • Integration of tapered panels to create a seamless transition from the high points to the drainage outlets.
  • Use of low-VOC adhesives to secure the tapered panels to the existing substrate, preventing wind uplift.
  • Verification of the final slope to ensure it meets or exceeds the 1/4" per foot minimum for commercial drainage.

Implementation and Final Envelope Validation

The final phase of the remediation involved the installation of the new drainage plane and the integration of a high-performance reinforced membrane. The tapered polyiso crickets were laid out according to the engineering map, and the seams were staggered to prevent linear failure points. To ensure a watertight seal, the membrane was heat-welded over the new slopes, creating a monolithic barrier that is impervious to the hydrostatic pressures associated with heavy rainfall. Special attention was paid to the transition zones where the new crickets met the existing roof height, ensuring that no new "dams" were created during the process.

To validate the success of the remediation, Aquashield performed a series of controlled flood tests. By blocking the drains and filling the previously problematic areas with water, we were able to visually confirm that the water now routed outward along the engineered paths provided by the polyiso crickets. This validation process ensures that the ponding instability has been fully neutralized and that the structural joists are no longer subjected to the risks of excessive hydrostatic loading. The result is a resilient, high-performance building envelope capable of sustaining the rigors of a high-volume logistics environment.

  • Execution of the tapered insulation layout with precision edge-trimming for tight fits.
  • Application of a reinforced TPO/PVC membrane with heat-welded seams for maximum durability.
  • Installation of oversized scuppers and upgraded drainage components to handle increased flow velocity.
  • Conducting a 24-hour flood test to verify the absence of standing water across the entire span.
  • Final engineering sign-off confirming the restoration of positive drainage and structural stability.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565

Commercial Engineering Dossier #056

Complete Old Roof Tear-Offs Down to Clean Wood Decking & Substrate Remediation on Commercial Municipal Sports & Convention Arenas

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Complete Old Roof Tear-Offs Down to Clean Wood Decking & Substrate Remediation on Commercial Municipal Sports & Convention Arenas

Engineering Audit and Failure Analysis of Multi-Layer Assemblies

In the context of a high-volume logistics distribution hub, the roof is not merely a cover but a critical component of the building envelope that must withstand extreme thermal fluctuations and structural loading. Upon initiating the engineering audit for this facility, we identified a systemic failure within a legacy multi-layer assembly. The existing system consisted of multiple layers of built-up roofing (BUR) and subsequent recover membranes that had been applied over several decades. This "layering" approach created a saturated sandwich effect, where moisture had migrated through the primary membrane and become trapped within the interstitial spaces.

The primary driver for a total tear-off, rather than a standard recover, was the detection of hydrostatic pressure buildup and saturated insulation boards. When moisture is trapped between layers, it undergoes a cycle of expansion and contraction during thermal shifts, leading to the degradation of the adhesive bonds and the eventual compromise of the structural substrate. Our audit revealed that the vapor drive was pushing moisture downward into the wood decking, creating a high risk of structural instability and mold proliferation.

  • Identification of interstitial condensation caused by inadequate vapor barriers.
  • Analysis of thermal bridging and its impact on moisture migration patterns.
  • Evaluation of membrane fatigue and loss of elasticity in legacy bitumen layers.
  • Assessment of the cumulative dead load added by multiple recover layers, which exceeded original design specifications.
  • Determination that the existing substrate was compromised beyond the scope of localized patching.

Systematic Deconstruction and Logistics Management

Executing a complete tear-off on an active logistics hub requires a surgical approach to minimize operational downtime while ensuring the safety of the building occupants and the integrity of the stored inventory. The deconstruction process began with a phased zoning strategy, allowing the facility to maintain its shipping and receiving schedules. We employed heavy-duty mechanical removal equipment, ensuring that the removal of the bitumen and membrane layers did not cause undue mechanical stress or impact loading on the underlying wood decking.

The removal process was conducted down to the bare wood, stripping away all remnants of old adhesives, flashing, and insulation. A critical aspect of this phase was the management of debris; the sheer volume of material removed from a distribution hub of this scale is immense. By implementing a continuous removal cycle, we prevented the accumulation of excessive weight on any single section of the roof, which is paramount when dealing with aged wood substrates that may have diminished load-bearing capacities.

  • Implementation of a phased zoning plan to maintain facility operational continuity.
  • Utilization of specialized scraping and lifting tools to avoid gouging the wood decking.
  • Strict adherence to OSHA fall protection standards and perimeter safety protocols.
  • Continuous debris evacuation to prevent structural overloading during the tear-off phase.
  • Detailed mapping of the removal sequence to ensure seamless transitions between work zones.

Structural Substrate Evaluation and Wood Remediation

Once the assembly was stripped to the clean wood decking, we transitioned from deconstruction to a comprehensive structural forensic analysis. Wood decking in commercial applications, particularly in older distribution hubs, is susceptible to dry rot, fungal decay, and delamination. We conducted a grid-based inspection of the entire deck, utilizing moisture meters and probe tests to identify "soft spots" that indicated internal decay not visible on the surface. This stage is where the distinction between a standard contractor and a building envelope specialist becomes evident.

Remediation involved the strategic removal of all compromised panels. We adhered to strict material science standards, ensuring that replacement wood matched the thickness, grade, and species of the original decking to maintain uniform structural rigidity. Any panel exhibiting more than 15% moisture content or visible structural sagging was flagged for immediate replacement. The goal was to establish a monolithic, stable base that meets ASTM standards for substrate integrity, ensuring that the new roof assembly would not be compromised by a failing foundation.

  • Conducting probe tests and moisture mapping across the entire roof surface.
  • Identifying areas of delamination in plywood and OSB (Oriented Strand Board) panels.
  • Removing decayed wood sections back to the nearest structural joist or support beam.
  • Installing new, high-grade structural panels with staggered joints to prevent linear stress points.
  • Verifying the structural integrity of the underlying rafters and trusses before decking replacement.

Substrate Preparation and Envelope Integration

The final phase of the remediation process focused on preparing the clean wood deck for the installation of the new high-performance roofing system. A clean substrate is the only way to guarantee the longevity of the fasteners and the overall adhesion of the membrane. We performed a comprehensive cleaning to remove all legacy nails, staples, and bitumen residue. This process is critical because any protruding fastener from a previous installation can create a "point load" that punctures a new membrane from the inside out, leading to premature failure.

Furthermore, we addressed the integration of the building envelope by inspecting the perimeter flashing and the transition points where the roof meets the parapet walls. By ensuring the wood decking was perfectly level and structurally sound, we eliminated the risk of "ponding" water, which is a common failure point in distribution hubs. The resulting substrate was a pristine, engineered platform ready for the application of modern insulation and a high-reflectivity, energy-efficient membrane system.

  • Mechanical removal of all legacy fasteners to ensure a flush surface.
  • Application of substrate leveling compounds in areas of minor irregularity.
  • Verification of fastener pull-out strength to ensure the deck can support the new wind-uplift requirements.
  • Inspection and remediation of the roof-to-wall transitions to ensure a watertight envelope.
  • Final engineering sign-off on the substrate's readiness for the new assembly installation.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #057

Stripping Old Shingles Down to Clean Wood Sheathing Across Commercial Eaves on Commercial Multi-Family Urban Residential Towers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Stripping Old Shingles Down to Clean Wood Sheathing Across Commercial Eaves on Commercial Multi-Family Urban Residential Towers

Systemic Deconstruction and Multi-Layer Envelope Audit

In the context of a large-scale logistics distribution hub, the eave sections often represent the most neglected portion of the building envelope. During our engineering audit, we identified a critical failure point: the accumulation of legacy roofing materials. Over several decades of maintenance, the facility had succumbed to the practice of "layering," where new shingles were installed directly over old ones. This created a cumulative dead load that exceeded the original structural design specifications of the eave rafters. A master-level approach to remediation requires a total strip-down to the original wood sheathing to eliminate hidden moisture traps and restore the structural equilibrium of the roof edge.

The stripping process is not merely a demolition task but a forensic exercise. By removing every layer of asphalt and felt, we expose the true condition of the substrate. We employ high-torque mechanical stripping tools to ensure that the removal process does not induce excessive vibration or impact trauma to the underlying decking. The goal is to reach a "clean wood" state, where the integrity of the sheathing can be visually and physically verified without the interference of adhesive residues or degraded underlayments.

  • Quantification of cumulative dead load removal to reduce stress on eave overhangs.
  • Identification of localized saturation zones where multi-layer trapping accelerated wood decay.
  • Removal of all legacy fasteners to prevent "ghosting" or protrusion through new membranes.
  • Implementation of a debris management system to prevent cladding damage during the descent of materials.
  • Verification of the original sheathing thickness against the building's structural blueprints.

Fastener Withdrawal Resistance and Substrate Integrity

Once the decking is stripped, the focus shifts to the material science of the substrate. A common failure in commercial eave remediation is the assumption that existing wood is capable of supporting new, high-performance membrane fasteners. We conduct a rigorous audit of fastener withdrawal resistance to ensure that the wood has not suffered from cellular breakdown due to chronic moisture exposure or fungal decay. If the wood fibers have lost their cohesive strength, new fasteners will fail to achieve the necessary pull-out resistance, leading to wind uplift vulnerabilities.

Using calibrated pull-testers, we measure the force required to extract a fastener from various points across the eave. This data allows us to map the "health" of the decking. Areas showing a significant drop in withdrawal resistance are flagged for immediate replacement or reinforcement. We adhere to ASTM standards for wood properties, ensuring that the substrate can handle the shear and tension loads imposed by the new building envelope system. This phase is critical because the eave is the primary point of wind pressure concentration; any failure in fastener grip here can lead to a systemic peel-back of the entire roof section.

  • Conducting pull-out tests to quantify the kilopounds of force the substrate can sustain.
  • Analyzing wood grain density and moisture content using digital hygrometers.
  • Identifying "soft spots" indicative of dry rot or subterranean termite infiltration.
  • Evaluating the condition of the original nail stock to determine the level of oxidation.
  • Mapping substrate degradation zones to prioritize structural reinforcement.

Structural Remediation: Sistering and Load Path Restoration

Upon stripping the eaves, it is frequent to find rafters that have bowed or succumbed to compression failure due to the aforementioned multi-layer weight. To restore the structural integrity of the hub's perimeter, we implement a sistering protocol. Sistering involves the installation of a new, structurally sound member alongside the compromised rafter. This is not a simple attachment; it is an engineering intervention designed to redistribute the load path and eliminate deflection in the eave line.

We utilize high-grade dimensional lumber or LVL (Laminated Veneer Lumber) depending on the span and load requirements. The new member is bonded to the existing rafter using industrial-grade structural adhesives and a staggered fastening pattern. This creates a composite beam that is significantly stiffer than the original. By ensuring the sistered member extends sufficiently into the main roof structure, we effectively transfer the weight of the eave back into the primary load-bearing walls, eliminating the "sag" that often plagues older distribution centers.

  • Selection of LVL or SPF lumber based on the required modulus of elasticity.
  • Application of structural adhesives to ensure full-surface bonding between members.
  • Execution of a staggered nailing pattern to prevent splitting the existing wood fibers.
  • Verification of the new load path to ensure zero deflection under maximum design load.
  • Integration of blocking and bridging to prevent lateral rotation of the sistered rafters.

Establishing Flat Decking Planes for Membrane Application

The final phase of the engineering process is the establishment of a perfectly flat decking plane. A common mistake in commercial roofing is installing a high-performance membrane over a wavy or uneven substrate. In a logistics hub, where the eaves are subject to intense wind scouring and water runoff, any irregularity in the deck creates a "pocket" where water can pool or where the membrane can stress and crack over time. We treat the roof deck as a precision surface, utilizing a combination of shaving and shimming to achieve a planar finish.

We employ long-straightedge guides to identify high spots and depressions across the eave length. High spots are carefully shaved down using power planers to avoid compromising the thickness of the sheathing. For depressions, we utilize high-density shims or structural fillers to bring the surface up to the established plane. This ensures that the subsequent layers—whether they be cover boards or the primary membrane—sit flush against the deck. This eliminates air gaps that could otherwise facilitate wind-driven moisture infiltration or cause premature fatigue of the membrane's adhesive bond.

  • Utilization of 10-foot straightedges to map surface deviations across the eave.
  • Precision planing of high spots to create a uniform vertical profile.
  • Installation of structural shims to eliminate low-point depressions.
  • Verification of the final plane using laser leveling tools for absolute accuracy.
  • Final cleaning of the substrate to remove all sawdust and particulates before membrane deployment.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #058

Low-VOC Cold-Applied Adhesives & HVAC Air Intake Odor Mitigation Protocols on Commercial Public Transit Maintenance Bus Barns

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Low-VOC Cold-Applied Adhesives & HVAC Air Intake Odor Mitigation Protocols on Commercial Public Transit Maintenance Bus Barns

Envelope Audit: The Logistics Hub Vulnerability Assessment

In the high-velocity environment of a modern logistics distribution hub, the building envelope is not merely a weather barrier but a critical component of operational continuity. During our engineering audit of the facility, we identified a recurring failure point common in large-scale industrial footprints: the intersection of roof membrane transitions and HVAC air intake systems. In these environments, the proximity of roof repair zones to air intake plenums creates a high risk of VOC (Volatile Organic Compound) infiltration, which can compromise indoor air quality (IAQ) and trigger facility-wide evacuations if solvent-heavy adhesives are utilized.

The audit focused on the structural integrity of the roof-to-wall transitions and the performance of the existing bonding agents. We observed significant degradation in the legacy solvent-based adhesives, which had become brittle due to thermal cycling and UV exposure. To remediate these failures without disrupting the 24/7 logistics cycle, a shift in material science was required. The primary engineering objective was to implement a high-tensile bonding solution that eliminated the risk of outgassing into the HVAC system while maintaining ASTM-compliant shear strength.

  • Evaluation of substrate moisture content to prevent osmotic blistering under new adhesive layers.
  • Mapping of HVAC intake zones to establish "Critical Odor Buffers" (COBs) during application.
  • Analysis of membrane compatibility between existing TPO/EPDM and new polyurethane bonding agents.
  • Assessment of wind-uplift pressures to ensure adhesive specifications meet ANSI/SPRI standards.

Material Science: Low-VOC Cold-Applied Polyurethane Adhesives

Traditional hot-melt adhesives, while effective, introduce significant safety risks and thermal stress to the substrate. Conversely, solvent-based cold adhesives often release pungent hydrocarbons that are unacceptable in occupied distribution centers. For this project, we specified a high-performance, low-VOC, cold-applied polyurethane bonding agent. This material operates via a moisture-cure mechanism, creating a chemical bond with the substrate that exceeds the tensile strength of the membrane itself. By utilizing a polyurethane chemistry that is inherently low-odor, we mitigated the risk of chemical odors permeating the facility's ventilation system.

The engineering advantage of cold-applied polyurethane lies in its flexibility and adhesive tenacity. Unlike rigid adhesives, these agents maintain a degree of elasticity, allowing the building envelope to expand and contract during extreme temperature fluctuations without risking bond failure. Furthermore, the rapid-setting nature of these adhesives allows for immediate loading of the membrane, significantly reducing the curing window and eliminating the need for temporary mechanical fasteners that could puncture the waterproofing layer.

  • Elimination of solvent-based carriers to reduce VOC emissions to near-zero levels.
  • High-modulus bonding strength that prevents membrane creep under high wind-uplift conditions.
  • Compatibility with a wide array of substrates, including concrete, steel, and existing thermoplastic membranes.
  • Reduced application temperature requirements, eliminating the fire hazards associated with kettles and hot-melt equipment.

HVAC Air Intake Containment & Odor Mitigation Protocols

Even with low-VOC materials, a master-level installation requires a redundant containment strategy when working adjacent to HVAC intakes. The "Odor Mitigation Protocol" implemented for this hub involved a multi-layered approach to ensure that no airborne particulates or trace scents entered the air handling units (AHUs). We established a strict containment perimeter around every intake, utilizing temporary physical barriers and negative-pressure ventilation where necessary to divert airflow away from the work zone.

The protocol dictated a "buffer-first" application sequence. We began by treating the areas furthest from the intakes, allowing the initial chemical reaction of the polyurethane to stabilize before moving toward the AHU plenums. By coordinating with the facility's HVAC engineers, we were able to temporarily adjust the intake dampers and shift the building's air pressure to a slight positive state internally, which naturally pushed air out of the building and prevented the infiltration of external odors during the critical bonding phase.

  • Installation of temporary polyethylene shrouds around intake vents to prevent accidental debris entry.
  • Implementation of a "Wind-Directional Work Schedule," ensuring adhesives were applied only when wind vectors pushed fumes away from the intakes.
  • Utilization of portable HEPA-filtered air scrubbers at the perimeter of the work zone to capture any airborne particulates.
  • Real-time IAQ monitoring using VOC sensors placed at the primary air intake manifolds.

Execution Strategy: Zero-Downtime Implementation

In the logistics sector, downtime is measured in thousands of dollars per minute. The execution strategy for this envelope remediation was designed for "Zero-Downtime," meaning the facility remained fully operational throughout the entire process. This was achieved through a phased, modular approach to the roof sections. By dividing the roof into manageable grids, our crews could isolate specific zones, apply the cold-applied adhesives, and seal the membrane without affecting the warehouse floor operations below.

The use of rapid-setting adhesives was the linchpin of this strategy. Because the polyurethane agents reached a handling strength in a fraction of the time required for traditional cold-glues, we were able to move from substrate preparation to final seal in a single shift. Quality control was maintained through rigorous pull-tests and infrared thermography to ensure no voids existed in the bonding layer, guaranteeing a monolithic seal across the entire building envelope.

  • Phased deployment across four quadrants to ensure continuous facility access and safety.
  • Integration of rapid-cure catalysts to accelerate the bonding process in high-humidity conditions.
  • Strict adherence to a "Clean-Site" policy to prevent adhesive residue from contaminating logistics equipment.
  • Final engineering sign-off via a comprehensive water-intrusion test and ASTM-standard peel tests.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #059

Solar Photovoltaic Ballasted Racking Point-Load Defense & Sacrificial Slip Sheets on Commercial Government Secure Records Archives

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Solar Photovoltaic Ballasted Racking Point-Load Defense & Sacrificial Slip Sheets on Commercial Government Secure Records Archives

The Mechanics of Point-Load Compression and Membrane Deformation

In the context of a large-scale Logistics Distribution Hub, the introduction of a ballasted Solar Photovoltaic (PV) system transforms the roof from a passive weather barrier into a structural load-bearing surface. The primary engineering concern is the "compression set" of the underlying insulation and the subsequent stress placed on the waterproofing membrane. When concrete ballast blocks are deployed, they create concentrated point loads that can exceed the compressive strength of standard polyisocyanurate (ISO) boards. If the insulation undergoes permanent deformation, the membrane is subjected to localized tension and potential "pinching" between the ballast and the substrate.

From a material science perspective, we must evaluate the load-bearing capacity of the roof assembly against the dead load of the racking system. Failure to account for the cumulative weight of the ballast leads to a phenomenon known as "dimpling," where the membrane is pressed into the insulation voids. This creates micro-depressions that act as catchment basins for standing water, accelerating the degradation of the membrane through hydrostatic pressure and thermal cycling. To mitigate this, our audit focuses on the distribution of weight across the structural deck to ensure that the load is transferred efficiently without compromising the envelope's integrity.

  • Assessment of ISO compressive strength (PSI) relative to the total ballast weight per square foot.
  • Analysis of membrane thickness and tensile strength to resist puncture from concrete irregularities.
  • Evaluation of the structural deck's deflection limits under the added weight of the PV array.
  • Verification of ASTM D-series standards for membrane durability and resistance to long-term compression.

Sacrificial Slip-Sheet Integration and Abrasion Mitigation

One of the most overlooked failures in ballasted PV installations is the "scouring" effect caused by wind-induced micro-movements. While the ballast blocks are designed to hold the system down, they are not permanently bonded to the roof. During high-wind events, the racking system experiences minute shifts and vibrations. Without a protective interface, these movements act as an abrasive, effectively sanding away the top layer of the TPO or EPDM membrane over time. This mechanical abrasion thins the membrane, leaving it vulnerable to UV degradation and eventual puncture.

To combat this, we implement heavy-duty sacrificial slip sheets. These are high-density, non-permeable barriers placed directly beneath the ballast blocks and racking rails. By introducing a sacrificial layer, the friction is transferred from the primary waterproofing membrane to the slip sheet. This ensures that any movement occurs between the ballast and the protector, rather than the protector and the roof. The selection of the slip sheet material is critical; it must possess a low coefficient of friction to prevent "grabbing" the membrane while remaining durable enough to withstand the crushing weight of the concrete blocks.

  • Deployment of reinforced rubberized asphalt or heavy-gauge TPO slip sheets to isolate mechanical friction.
  • Implementation of "overlap" protocols to ensure no ballast block edge ever makes direct contact with the primary membrane.
  • Analysis of the thermal expansion coefficients between the slip sheet and the primary membrane to prevent buckling.
  • Verification of slip-sheet stability to ensure they do not migrate or bunch during seismic or wind events.

Pre-fabricated Target Patches and Point-Load Defense

While slip sheets provide a general layer of protection, the highest stress concentrations occur at the specific contact points of the ballast blocks. In high-performance engineering, we utilize "pre-fabricated target patches." These are custom-cut, reinforced membrane sections that are heat-welded or adhered to the roof at the exact coordinates where the ballast blocks will reside. Unlike a general slip sheet, a target patch is an integrated part of the building envelope, providing a redundant layer of waterproofing and structural reinforcement at the most critical points of failure.

The engineering logic behind target patches is to create a "hardened zone." By increasing the membrane thickness at the point of load, we distribute the downward pressure over a wider surface area, reducing the PSI on the insulation. This approach effectively eliminates the risk of "punch-through" failures. During the audit, we examine the weld quality of these patches using vacuum testing to ensure that the reinforcement does not introduce new leak paths. The goal is a seamless transition from the primary membrane to the reinforced patch, maintaining a monolithic waterproof barrier.

  • Precision mapping of ballast coordinates to ensure 1:1 alignment with target patches.
  • Utilization of double-layer reinforcement for blocks exceeding 100 lbs to prevent localized indentation.
  • Strict adherence to ANSI standards for heat-welding and seam integrity on reinforced sections.
  • Implementation of a "buffer zone" around each patch to prevent edge-lift during thermal contraction.

Cable Tray Routing and Envelope Integrity Management

The final component of the building envelope audit involves the logistics of electrical conveyance. The routing of DC cabling from the PV panels to the inverters often involves miles of wiring that must be managed without compromising the roof's drainage or structural integrity. A common error in distribution hub installations is the use of "loose-lay" cabling, which can shift in the wind, create "cable dams" that trap water, or put undue stress on the membrane through friction.

Our specification requires the use of engineered cable trays and routing systems that are integrated into the racking structure. By elevating the cables, we ensure that water flows freely to the primary drains and scuppers, preventing the ponding that leads to premature membrane failure. Furthermore, the routing must avoid any direct penetrations of the roof envelope. All cabling must be transitioned from the roof to the interior via pre-existing conduits or professionally flashed curb penetrations. This maintains the continuity of the building envelope and prevents the "swiss cheese" effect often seen in poorly planned solar retrofits.

  • Installation of rigid cable management trays to eliminate "cable sag" and water damming.
  • Use of UV-stabilized cable ties and fasteners that do not penetrate the waterproofing layer.
  • Strategic routing of conduits to avoid high-traffic maintenance paths and drainage flow lines.
  • Audit of all roof-to-wall transitions to ensure flashing integrity is maintained around electrical conduits.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #060

OSHA-Compliant Skylight Fall-Protection Curbs & Heavy-Duty Security Screens on Commercial Pharmaceutical Production Facilitys

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
OSHA-Compliant Skylight Fall-Protection Curbs & Heavy-Duty Security Screens on Commercial Pharmaceutical Production Facilitys

Structural Integrity and Fall-Arrest Anchoring Systems

In a high-volume logistics distribution hub, the roof is more than just a weather barrier; it is a critical safety zone. The primary engineering challenge during this audit was the verification of skylight fall-protection screens. Per OSHA 1910.28, any skylight that is not designed to support the weight of an employee must be protected by a guardrail system or a fall-arrest screen. For this facility, we focused on the implementation of heavy-duty security screens capable of arresting a 200-lb concentrated load without catastrophic deflection or curb failure.

The physics of a fall-arrest event involve dynamic loading, which far exceeds the static weight of the individual. To ensure the system does not pull away from the roof deck during an impact, the anchoring mechanism must be integrated directly into the structural steel or the reinforced concrete curb. We analyzed the shear strength of the fasteners and the gauge of the steel framing to ensure the assembly meets ANSI Z359 standards for fall protection.

  • Verification of 12-gauge galvanized steel screen frames to prevent buckling under sudden impact.
  • Implementation of through-bolt anchoring with oversized backing plates to distribute the load across the curb width.
  • Assessment of weld integrity at the corner junctions of the screen frames using non-destructive testing.
  • Calculation of the deflection limit to ensure the falling person does not contact the fragile skylight glazing.
  • Evaluation of the mesh tensile strength to prevent "punch-through" during a high-velocity descent.

Curb Flashing Elevation and Hydrostatic Water Management

Water infiltration at the skylight curb is the most frequent point of failure in commercial building envelopes. In this audit, we examined the relationship between the roof membrane and the curb flashing elevation. A common error in logistics hubs is the installation of curbs that are too low, allowing wind-driven rain to crest the flashing and enter the building interior. We mandated a minimum curb height that exceeds the maximum anticipated snow load and rain accumulation, ensuring a positive slope away from the curb base.

The flashing must be executed as a continuous, monolithic system. We focused on the transition from the field membrane to the vertical face of the curb, ensuring that the flashing is wrapped and tucked to prevent capillary action. The use of a reinforced flashing membrane is non-negotiable here, as the corners of the curbs are high-stress areas prone to fatigue and cracking due to the thermal expansion and contraction of the massive roof surface.

  • Analysis of the "water-shedding" geometry to ensure zero ponding at the curb-to-membrane interface.
  • Verification of the flashing height relative to the interior ceiling grid to prevent interior water damage.
  • Inspection of the counter-flashing installation to provide a secondary layer of protection against wind-driven rain.
  • Audit of the sealant beads applied to the flashing laps to ensure a watertight, air-tight seal.
  • Review of the drip-edge detailing on the exterior of the curb to direct water away from the building envelope.

Compression Termination Bars and Mechanical Fastening

The integrity of the building envelope is only as strong as its terminations. To secure the membrane to the vertical face of the skylight curbs, we utilized heavy-duty aluminum compression termination bars. These bars are critical because they eliminate the reliance on adhesives alone, which can degrade under extreme UV exposure and thermal cycling. The goal is to create a mechanical clamp that forces the membrane into a permanent, airtight bond with the curb substrate.

During the audit, we identified several "fish-mouth" gaps where the membrane had not been properly tensioned before the termination bar was applied. We corrected this by implementing a strict fastening schedule, ensuring that screws are driven at precise intervals with calibrated torque to avoid over-compressing the membrane, which can lead to premature tearing. The termination bar acts as the final line of defense against wind uplift, which is particularly aggressive around the protrusions of a large-scale distribution center.

  • Installation of 1.5-inch aluminum termination bars fastened with stainless steel screws every 6 inches.
  • Application of a high-performance polyurethane sealant bead behind the termination bar to prevent moisture migration.
  • Verification of the "tight-wrap" technique to ensure no wrinkles or folds exist beneath the compression plate.
  • Audit of the fastener embedment depth to ensure a secure grip in the curb material without compromising the substrate.
  • Inspection of the top-cap sealing to prevent water from entering the top of the termination assembly.

Thermal Gaskets and Building Envelope Hermeticity

The intersection of the fall-protection screen and the curb creates a potential thermal bridge and a point of air infiltration. In a climate-controlled logistics hub, uncontrolled air leakage leads to massive energy losses and potential condensation issues within the roof assembly. To mitigate this, we specified the use of closed-cell EPDM thermal gaskets between the security screen frame and the curb top.

These gaskets serve a dual purpose: they provide a vibration dampener for the heavy-duty screens and create a hermetic seal that prevents the "chimney effect," where conditioned air escapes through the roof gaps. We analyzed the compression set of the gaskets to ensure they maintain their elasticity over a wide temperature range, preventing the shrinkage that often leads to leaks in lower-quality installations. This attention to material science ensures that the building envelope remains a cohesive unit, protecting both the assets inside and the structural integrity of the roof.

  • Specification of 1/4-inch closed-cell EPDM gaskets for superior compression recovery and UV resistance.
  • Evaluation of the gasket's shore hardness to ensure it provides a sufficient seal without hindering the screen's fit.
  • Analysis of the thermal break provided by the gasket to reduce heat transfer through the steel curb.
  • Verification of the gasket's continuity around the entire perimeter of the screen frame.
  • Testing for air infiltration using smoke pens to ensure the hermetic seal is fully achieved.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #061

Rooftop Mechanical Unit Vibration Isolation Rails & Spring-Mounted Curb Seals on Commercial Historic Sanctuary & Education Annexs

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Rooftop Mechanical Unit Vibration Isolation Rails & Spring-Mounted Curb Seals on Commercial Historic Sanctuary & Education Annexs

The Mechanics of Harmonic Resonance in Industrial Roof Systems

In the context of a high-capacity Logistics Distribution Hub, the rooftop is more than a weather barrier; it is a structural platform for massive HVAC and ventilation systems. The primary engineering challenge in these facilities is the management of harmonic vibrations generated by heavy-duty rooftop units (RTUs). When these units operate, they produce low-frequency oscillations that transmit directly into the roof deck. If left unmitigated, these vibrations create a phenomenon known as mechanical fatigue, where the constant micro-movement of the equipment against the roof membrane leads to premature degradation of the waterproofing layer.

From a master roofer's perspective, the failure point is rarely the membrane itself, but rather the interface where the rigid equipment curb meets the flexible roof system. The differential in movement between the vibrating steel of the unit and the static nature of the building envelope creates shear stress. Over time, this stress manifests as hairline fractures in the flashing and the eventual breakdown of the adhesive bonds. To prevent systemic failure, we must treat the equipment curb not as a static base, but as a dynamic component of the building envelope.

  • Analysis of structural resonance frequencies to prevent sympathetic vibration of the roof deck.
  • Evaluation of membrane shear strength under constant dynamic loading.
  • Assessment of the "creep" effect in thermoplastic membranes caused by mechanical oscillation.
  • Identification of fatigue points in traditional flashing details around high-vibration equipment.

Engineering the Vibration Isolation Interface

To decouple the mechanical equipment from the building envelope, the implementation of spring-mounted curb systems and vibration isolation rails is non-negotiable. These systems are designed to absorb the kinetic energy of the RTU before it reaches the roof deck. By utilizing heavy-duty steel springs with a specific static deflection, the isolation rails act as a shock absorber, shifting the natural frequency of the system away from the operating frequency of the machinery. This ensures that the energy is dissipated through the springs rather than being transferred into the structural steel of the hub.

The engineering of these rails must adhere to strict ANSI standards for load distribution. A common failure in commercial installations is the improper distribution of the unit's weight, which can lead to localized deflection of the roof deck. By utilizing a wide-base isolation rail, the point load is converted into a distributed load, reducing the stress on the underlying insulation and membrane. This structural decoupling is the first line of defense in maintaining the watertight integrity of the envelope.

  • Implementation of open-spring isolators to provide high-efficiency vibration attenuation.
  • Utilization of neoprene pads at the rail-to-curb interface to dampen high-frequency noise.
  • Calculation of static deflection to ensure the unit remains level during peak operational loads.
  • Integration of load-spreading plates to prevent membrane compression and puncture.

Fiber-Reinforced Structural Mastic and Sealant Integrity

Once the mechanical vibration is isolated, the critical focus shifts to the seal. Standard commercial sealants are insufficient for equipment curbs subject to constant movement. We specify fiber-reinforced structural mastic because of its superior elongation properties and tensile strength. Unlike standard caulking, which can tear under the stress of harmonic vibration, fiber-reinforced mastic incorporates a matrix of synthetic fibers that bridge the gap between the curb and the roof membrane, creating a flexible, monolithic seal.

The application process is a matter of craftsmanship and material science. The mastic must be applied in a multi-stage process: first, a primer to ensure molecular adhesion to the substrate, followed by the embedding of a reinforcement fabric, and finally, the application of the structural mastic. This creates a "reinforced bridge" that can expand and contract without losing its bond. This assembly is designed to withstand the coefficient of thermal expansion and the mechanical oscillation of the unit without developing the voids that lead to hydrostatic infiltration.

  • Application of high-solids, polymer-modified mastic for maximum UV resistance and flexibility.
  • Integration of non-woven polyester reinforcement fabric to prevent shrinkage and cracking.
  • Execution of a "three-course" seal method to ensure redundant layers of waterproofing.
  • Verification of bond strength through ASTM-standard peel tests at the curb-to-membrane transition.

Long-Term Integrity Audit and Maintenance Protocols

A building envelope is only as strong as its weakest joint. For a Logistics Distribution Hub, the equipment curbs are the most vulnerable points of entry for moisture. An authoritative engineering audit requires a shift from visual inspection to a technical analysis of the seal's elasticity and the spring's compression. We utilize infrared thermography to detect subsurface moisture accumulation around the curbs, which often indicates a failure in the mastic seal long before a leak becomes visible on the interior ceiling.

Furthermore, the isolation springs must be audited for "bottoming out." If a spring loses its tension or is overloaded, the vibration isolation is bypassed, and the mechanical energy is transferred directly into the roof membrane. A comprehensive maintenance schedule ensures that the structural mastic is replenished every five to seven years to combat the effects of ozone degradation and thermal cycling. By treating the rooftop mechanical interface as a living system, we extend the lifecycle of the entire roof assembly and protect the high-value assets housed within the distribution center.

  • Quarterly infrared moisture scans of all equipment curb perimeters.
  • Annual verification of spring isolator tension and alignment to prevent mechanical bridging.
  • Detailed inspection of mastic fillets for signs of "alligatoring" or loss of adhesion.
  • Documentation of all membrane deformations using precision calipers to monitor structural settlement.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #062

Industrial Corrosive Chemical Fume Exhaust Defense on Commercial Financial Institution Data Vaults

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Industrial Corrosive Chemical Fume Exhaust Defense on Commercial Financial Institution Data Vaults

Environmental Audit: Assessing the Chemical Load of the Distribution Hub

Upon conducting a comprehensive building envelope audit of the Logistics Distribution Hub, the primary concern identified was the intersection of high-volume fleet traffic and industrial exhaust systems. The facility serves as a nexus for diverse cargo, including industrial solvents and corrosive chemical precursors. The roof surface is not merely a weather barrier but a critical component of the facility's containment strategy. Our audit revealed that the exhaust plumes from the chemical scrubbing units were discharging acidic vapors directly onto the membrane surface, creating a localized environment of high chemical stress.

Furthermore, the proximity of the loading docks to the roof perimeter introduced a secondary threat: aerosolized motor oils and hydraulic fluids from heavy-duty diesel fleets. These hydrocarbons, when combined with acidic fumes, create a synergistic degradation effect that can compromise the structural integrity of a standard roofing membrane in a fraction of its rated lifespan. To ensure a 20-year service life, the selection of the membrane must be predicated on its resistance to these specific chemical agents rather than general weatherproofing capabilities.

  • Identification of sulfuric and nitric acid concentrations in exhaust plumes.
  • Analysis of hydrocarbon migration from fleet idling zones.
  • Evaluation of thermal cycling effects on membrane elasticity.
  • Assessment of existing drainage patterns that may concentrate chemical runoff.
  • Verification of ASTM D543 standards for chemical resistance.

Material Science: TPO vs. PVC in Corrosive Environments

When evaluating Thermoplastic Polyolefin (TPO) against Polyvinyl Chloride (PVC), the decision hinges on the molecular response to chemical attack. TPO is a blended material, primarily consisting of polypropylene and ethylene-propylene rubber. While TPO offers excellent reflectivity and general durability, it is fundamentally susceptible to oils, greases, and certain solvents. In a logistics hub where motor oils are prevalent, TPO can suffer from swelling and softening, which leads to premature seam failure and loss of tensile strength.

Conversely, PVC is a chlorinated polymer that inherently possesses a higher resistance to oils and grease. The chlorine atoms in the PVC chain provide a chemical shield that prevents the penetration of many hydrocarbons that would otherwise dissolve a TPO membrane. However, PVC is not without its vulnerabilities. The primary concern with PVC is its reliance on plasticizers to maintain flexibility. In the presence of aggressive industrial fumes, these plasticizers can be stripped from the membrane, leading to a phenomenon known as embrittlement.

  • TPO vulnerability: High susceptibility to swelling when exposed to petroleum-based oils.
  • PVC advantage: Superior inherent resistance to grease and industrial lubricants.
  • TPO advantage: Generally higher resistance to certain strong acids compared to low-grade PVC.
  • PVC vulnerability: Potential for plasticizer migration under extreme chemical stress.
  • Comparative analysis of weld strength under chemical saturation.

Plasticizer Retention and Dimensional Stability

The engineering crux of this case study lies in the management of plasticizer retention. Plasticizers are additives that keep the PVC membrane pliable; without them, the material becomes rigid and prone to cracking. In an industrial environment, chemical fumes can act as catalysts that accelerate the leaching of these additives. If the PVC membrane is not engineered for high-performance chemical resistance, the acidic exhaust from the distribution hub's scrubbers can break the molecular bonds holding the plasticizers in place.

Once the plasticizer threshold drops below a critical percentage, the membrane loses its ability to accommodate the natural expansion and contraction of the building's steel superstructure. This results in "stress cracking," particularly around fasteners and perimeter flashing. To mitigate this, we specify a high-performance, reinforced PVC membrane with a stabilized plasticizer package. This ensures that the membrane maintains its dimensional stability and elasticity even when subjected to the constant bombardment of industrial fumes.

  • Monitoring the "glass transition temperature" to ensure flexibility in cold climates.
  • Evaluating the rate of plasticizer loss via accelerated aging tests.
  • Analyzing the impact of UV radiation on the acceleration of chemical degradation.
  • Assessing the role of the reinforcement scrim in preventing catastrophic tear propagation.
  • Implementing a strict maintenance schedule to neutralize acidic deposits.

Engineering Recommendation and Implementation Strategy

Based on the audit data and the specific chemical profile of the Logistics Distribution Hub, the authoritative recommendation is the installation of a high-performance, chemical-resistant PVC membrane. While TPO is a formidable product for standard warehouses, the presence of aerosolized motor oils and industrial fumes makes it an unacceptable risk for this specific application. The PVC selection must be a heavy-duty grade, specifically formulated for industrial environments, ensuring that the plasticizer retention is optimized for long-term exposure to corrosive agents.

The implementation strategy focuses on the integrity of the thermal welds. In a chemical-heavy environment, the seam is the most vulnerable point of failure. We utilize automated hot-air welding equipment to ensure a molecular bond that is as strong as the membrane itself. Furthermore, we recommend the installation of a specialized chemical-resistant coating around the exhaust vents to provide an additional layer of defense, effectively creating a "sacrificial zone" that protects the primary membrane from the highest concentrations of acid fumes.

  • Specification of a 60-mil or 80-mil reinforced PVC membrane for maximum puncture resistance.
  • Utilization of robotic welding for all field seams to eliminate human error.
  • Installation of oversized flashing around exhaust penetrations to reduce direct fume contact.
  • Integration of a high-density cover board to provide a stable substrate and thermal buffer.
  • Mandatory vacuum testing of all seams to ensure a 100% watertight and chemical-tight seal.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565

Commercial Engineering Dossier #063

Active Emergency Leak Catchment Tarps & Interior Production Bay Diversion on Commercial Telecommunications Central Switching Offices

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Active Emergency Leak Catchment Tarps & Interior Production Bay Diversion on Commercial Telecommunications Central Switching Offices

Envelope Breach Analysis and Site Audit Parameters

Upon arrival at the Logistics Distribution Hub, the primary objective was a comprehensive building envelope audit to identify the precise failure points causing systemic water intrusion. In a facility of this scale, a leak is rarely a localized event; it is typically a symptom of a larger failure in the primary waterproofing layer or a compromise in the flashing transitions. Our engineering team conducted a thermal imaging survey and moisture probe analysis to map the saturation levels within the roof insulation and the structural deck. The audit revealed significant degradation in the perimeter flashing and a failure in the primary membrane seams near the HVAC curb assemblies, allowing precipitation to bypass the primary barrier.

The risk profile for this specific facility was elevated due to the presence of high-value automated sorting equipment and sensitive electronic conveyor systems located directly beneath the compromised sections. Water intrusion in a logistics environment does not merely threaten the structural integrity of the ceiling grid; it poses a catastrophic risk to operational uptime and electrical safety. The audit identified several critical failure modes that required immediate mitigation before a permanent membrane replacement could be scheduled.

  • Failure of the TPO heat-welded seams due to thermal cycling and inadequate welding penetration.
  • Compromised flashing at the parapet wall transitions, leading to hydrostatic pressure buildup behind the fascia.
  • Clogged primary drainage scuppers causing ponding water to exceed the design capacity of the roof slope.
  • Capillary action drawing moisture through degraded sealant joints at the roof-to-wall intersections.

Material Science of Industrial Heavy-Duty Vinyl Diversion

To mitigate active leaks while maintaining production bay operations, we deployed industrial-grade, heavy-duty vinyl diverter tarps. Unlike standard polyethylene sheeting, these diverters are engineered from high-tensile PVC-coated polyester, designed to withstand the mechanical stresses of a commercial environment. From a material science perspective, the selection of 20-mil to 30-mil reinforced vinyl is critical for ensuring tear resistance and long-term durability under constant hydraulic load. These materials are selected based on ASTM D-751 standards for tensile strength and tear resistance, ensuring that the catchment system does not fail under the weight of accumulated water during a peak precipitation event.

The chemical composition of the vinyl provides an impermeable barrier that prevents seepage through the tarp itself, which is essential when protecting sensitive electronics. Furthermore, the UV-stabilized coating prevents the material from becoming brittle if exposed to sunlight during the installation process. The engineering focus here is on the "catchment efficiency," ensuring that the material can be tensioned across a wide span without sagging to a point where it creates a secondary hazard or collects excessive weight that could compromise the interior ceiling supports.

  • Reinforced polyester scrim for high dimensional stability and resistance to stretching.
  • PVC coating for absolute impermeability and resistance to industrial chemicals and oils.
  • Heat-welded seams on the tarps to eliminate leak points at the joints of the diverter.
  • High-grade grommet reinforcement for secure anchoring to structural steel members.

Strategic Deployment and Hydraulic Routing Geometry

The deployment of the catchment system is an exercise in hydraulic engineering. It is not sufficient to simply "catch" the water; the water must be routed away from high-value equipment and diverted into a controlled drainage point. We implemented a gravity-fed diversion strategy, utilizing the natural slope of the interior structural beams to create a controlled flow path. By calculating the projected rainfall intensity and the estimated volume of water entering through the breach, we determined the necessary pitch for the vinyl tarps to ensure rapid evacuation of the fluid.

The routing process involved the installation of flexible, heavy-duty PVC conduits that acted as extensions of the tarp system. These conduits were secured to the building's structural skeleton, bypassing the production bay's critical zones and directing the water into temporary sump collection tanks. This approach ensures that the "splash zone" is eliminated and that the water is transported in a closed system from the point of entry to the point of disposal, preventing any accidental spills on the warehouse floor which could lead to slip-and-fall hazards or equipment short-circuits.

  • Calculation of the "catchment area" to determine the total gallons per minute (GPM) of expected intrusion.
  • Implementation of a minimum 2% slope on all diverter surfaces to prevent stagnant pooling.
  • Strategic placement of diversion conduits to avoid interference with overhead cranes and conveyor paths.
  • Utilization of secure tensioning hardware to maintain the hydraulic profile of the tarp under load.

Long-Term Remediation and Envelope Restoration

While the emergency diversion system provides immediate operational continuity, the ultimate goal is the restoration of the building envelope to ANSI and ASTM standards. The transition from emergency mitigation to permanent repair begins with a detailed remediation plan that addresses the root cause of the failure. Our engineering approach involves the removal of all saturated insulation to prevent the growth of mold and the degradation of the steel decking. The restoration process focuses on creating a monolithic waterproofing layer that eliminates the vulnerabilities identified during the initial audit.

The final phase of the project involves the installation of a high-performance TPO membrane with reinforced flashing details. Special attention is paid to the curb flashings and parapet walls, utilizing termination bars and high-grade sealants to ensure a watertight seal. By integrating the emergency diversion data—knowing exactly where the most significant volumes of water entered—we can reinforce those specific "high-stress" areas with additional layering and enhanced flashing geometry, ensuring the facility remains watertight for the remainder of its design life.

  • Full removal and replacement of wet insulation with high-R value polyisocyanurate boards.
  • Installation of a 60-mil TPO membrane with fully adhered attachment for maximum wind uplift resistance.
  • Application of reinforced flashing at all penetrations, following strict manufacturer specifications.
  • Post-installation flood testing and infrared scanning to verify the integrity of the new envelope.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #064

Cold-Weather Induction Welded Membrane Attachments on Commercial Heavy Manufacturing Fabrication Plants

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Cold-Weather Induction Welded Membrane Attachments on Commercial Heavy Manufacturing Fabrication Plants

Thermal Dynamics of Cold-Weather Induction Welding

In the context of a large-scale Logistics Distribution Hub, the building envelope is subjected to extreme thermal fluctuations and significant wind loads. When executing induction welding on thermoplastic membranes—specifically TPO and PVC—during cold-weather cycles, the primary engineering challenge is the management of the thermal gradient. Unlike traditional hot-air welding, which relies on convective heat transfer from the surface downward, electromagnetic induction utilizes a high-frequency current to excite the molecules within the membrane and the bonding plate, generating heat internally. This process is far more efficient in low temperatures, but it introduces a risk of thermal shock if the delta between the ambient air and the weld temperature is too extreme.

To maintain the structural integrity of the envelope, we must account for the "cold-sink" effect of the steel decking and insulation substrates. In temperatures dropping below 32°F, the substrate acts as a heat sink, drawing energy away from the weld zone and potentially leading to an incomplete molecular fusion. A failure to maintain a consistent thermal profile results in a "cold weld," where the membranes appear bonded but lack the necessary shear strength to resist wind uplift. Our audit focused on the precise synchronization of the induction cycle to ensure that the polymer chains reached their glass transition temperature and fully coalesced before the cooling phase began.

  • Analysis of substrate thermal conductivity in sub-zero conditions.
  • Evaluation of molecular fusion depth within the thermoplastic layers.
  • Mitigation of thermal shock to prevent membrane shrinkage or warping.
  • Assessment of the heat-affected zone (HAZ) to ensure no degradation of the polymer.

Precision Tool Calibration and Thermal Profiling

The success of an induction-welded system is entirely dependent on the calibration of the electromagnetic plates and the controlling power unit. For this Logistics Distribution Hub, we implemented a rigorous calibration protocol based on the specific thickness of the membrane and the ambient temperature of the site. Tool calibration is not a "set it and forget it" process; it requires constant adjustment as the day's temperature shifts. We utilized digital pyrometers and thermal imaging cameras to verify that the induction plates were delivering a uniform heat flux across the entire surface area of the bond.

Over-calibration leads to "scorching," where the polymer is overheated, causing the material to become brittle and lose its tensile strength. Conversely, under-calibration results in a lack of penetration, leaving the bond susceptible to delamination under pressure. The engineering goal is to achieve a homogenous melt where the two layers of membrane merge into a single, monolithic sheet. This requires a precise balance of frequency and voltage, tailored to the specific resistivity of the membrane material being utilized.

  • Implementation of real-time thermal monitoring using infrared thermography.
  • Adjustment of voltage and frequency settings based on hourly ambient temperature shifts.
  • Verification of plate flatness to ensure uniform electromagnetic contact.
  • Strict adherence to manufacturer-specified weld times and temperature thresholds.

Weighted Magnetic Cooling and Bond Stabilization

One of the most overlooked phases of the induction process is the cooling period. In a high-wind environment typical of a logistics hub, the membrane is prone to shifting or lifting immediately after the heat cycle is complete. To counteract this, we employed weighted magnetic cooling clamps. These clamps serve a dual purpose: they provide the necessary mechanical pressure to ensure a tight bond and act as a heat sink to accelerate the stabilization of the weld. By rapidly drawing heat away from the fusion zone, the magnets help the polymer crystallize in a dense, structured formation, which significantly increases the bond's ultimate tensile strength.

The application of these magnets must be strategic. If the cooling is too rapid or uneven, it can introduce internal stresses into the membrane, leading to micro-fractures. However, when executed correctly, the weighted magnetic clamping ensures that the membrane remains in intimate contact with the substrate during the critical transition from a molten state to a solid state. This stabilization is essential for preventing "bridging," where the membrane lifts slightly off the surface, creating a void that can later be compromised by wind suction.

  • Utilization of high-gauss magnetic clamps for immediate surface stabilization.
  • Calculation of required clamping pressure to prevent wind-induced displacement.
  • Management of the cooling rate to optimize polymer chain alignment.
  • Prevention of membrane "oil-canning" through strategic weight distribution.

Wind Uplift Analysis and Envelope Validation

The final phase of the engineering audit involved a comprehensive validation of the building envelope's resistance to wind uplift. For a distribution hub with massive roof spans, the wind loads are immense, creating significant negative pressure (suction) on the roof surface. We conducted a series of destructive and non-destructive tests to ensure that the induction-welded attachments met or exceeded ASTM and ANSI standards for wind resistance. The focus was on the peel strength of the welds and the overall stability of the membrane-to-substrate attachment points.

Our findings indicated that the combination of calibrated induction heating and magnetic cooling resulted in a bond strength that exceeded the tensile strength of the membrane itself. This means that in a catastrophic wind event, the membrane would likely tear before the weld would fail. This level of redundancy is critical for long-term facility maintenance and insurance compliance. By treating the roof not just as a covering, but as a precision-engineered building envelope, we have ensured that the logistics hub can withstand extreme weather events without compromising the interior assets or the safety of the personnel.

  • Execution of peel tests to verify molecular fusion and bond integrity.
  • Calculation of wind uplift coefficients based on local building codes and hub geometry.
  • Verification of seam continuity using vacuum box testing and ultrasonic scanning.
  • Final certification of the envelope as a monolithic, weather-tight system.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565

Commercial Engineering Dossier #065

High-Solids Silicone Monolithic Coating Restoration & Albedo Reflectance on Commercial Logistics Distribution Hubs

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
High-Solids Silicone Monolithic Coating Restoration & Albedo Reflectance on Commercial Logistics Distribution Hubs

The Engineering Imperative of Hydrostatic Pressure Testing in Large-Scale Logistics Hubs

In the context of a massive logistics distribution hub, the roof is not merely a cover but a critical structural component of the building envelope. Given the immense square footage of these low-slope assemblies, the risk of systemic failure is amplified by the sheer volume of water managed during peak precipitation events. A standard visual inspection is insufficient for a facility of this scale; instead, we employ hydrostatic flood testing to simulate extreme loading conditions and identify latent defects in the membrane and drainage integration.

The primary objective is to subject the roof assembly to a controlled hydrostatic head, forcing water into any microscopic voids or improperly fused seams that would otherwise remain undetected during a light rain. By temporarily transforming the roof into a containment vessel, we can analyze the integrity of the building envelope under pressure. This process is essential for verifying that the installation meets the rigorous specifications required for a 20-year No Dollar Limit (NDL) warranty, as any failure at the drain interface could lead to catastrophic interior damage and operational downtime for the logistics client.

  • Verification of membrane continuity across expansive field areas.
  • Stress-testing of primary and secondary drainage points under standing water pressure.
  • Identification of "invisible" leaks caused by improper heat-welding or mechanical fastening.
  • Validation of the roof's slope-to-drain efficiency to prevent long-term ponding.
  • Establishment of a baseline performance metric prior to manufacturer warranty sign-off.

Protocol for 48-Hour Drain Bowl Isolation and Monitoring

The execution of a 48-hour hydrostatic test requires precision engineering and strict adherence to timing. We begin by isolating the primary drain bowls using industrial-grade mechanical plugs. These plugs must be rated for the specific hydrostatic pressure of the water column to ensure that the test measures the membrane's integrity rather than the plug's failure. Once the drains are sealed, the roof is flooded to a predetermined depth—typically two inches above the highest point of the drain flange—creating a controlled "bowl" effect across the designated testing zone.

Over the subsequent 48-hour window, the water level is monitored using precision gauges. It is critical to differentiate between actual leakage and evaporation loss. In a professional engineering audit, we calculate the expected evaporation rate based on ambient temperature, humidity, and wind speed. Any drop in water level exceeding the calculated evaporation threshold is flagged as a breach in the envelope. This rigorous monitoring period ensures that slow-seeping leaks, which may take hours to penetrate the insulation and decking, are fully captured and documented.

  • Installation of high-compression mechanical plugs in all primary roof drains.
  • Controlled flooding to a minimum depth of 2 inches over the critical drainage transition.
  • Implementation of evaporation control calculations to ensure data accuracy.
  • Bi-hourly monitoring of water levels using calibrated depth gauges.
  • Documentation of water retention levels relative to the building's structural deflection.

Technical Analysis of Membrane Flange Welds and Detail Integrity

The most vulnerable point of any commercial roof is the transition from the field membrane to the drain body. In a logistics hub, where thermal expansion and contraction are exaggerated by the massive surface area, the flange weld is under constant stress. During the hydrostatic test, the pressure is concentrated precisely at these junctions. We examine the heat-welded seams of the TPO or PVC membrane, looking for evidence of "cold welds" or insufficient fusion that could be compromised under the weight of standing water.

A master-level audit involves a microscopic inspection of the weld bead. We are looking for a consistent, homogenous bond where the two layers of polymer have fused into a single monolithic sheet. If the hydrostatic test reveals a failure, we employ vacuum testing on the surrounding flanges to pinpoint the exact location of the void. This level of scrutiny ensures that the flange is not just visually acceptable, but structurally sound and capable of resisting the capillary action that often draws water into the building envelope at the drain perimeter.

  • Evaluation of the heat-welding parameters used during the installation of the drain boots.
  • Inspection for "fish-mouths" or wrinkles in the membrane at the flange transition.
  • Verification of the mechanical fastening of the drain body to the structural deck.
  • Analysis of the weld bead consistency using ASTM-standard probe testing.
  • Assessment of the flashing height and overlap in accordance with manufacturer specifications.

The NDL Audit and Final Manufacturer Warranty Certification

The culmination of the hydrostatic test is the Manufacturer’s No Dollar Limit (NDL) Audit. An NDL warranty is the gold standard of commercial roofing, shifting the entire financial risk of future leaks to the manufacturer, provided the installation is flawless. The manufacturer's representative conducts a comprehensive walk-through, using the data from our 48-hour flood test as empirical evidence of the roof's performance. This audit is not a formality; it is a rigorous engineering sign-off that validates the entire building envelope.

For the audit to be successful, every detail must be documented in a comprehensive close-out package. This includes the flood test logs, the weld inspection reports, and the confirmation that all primary drains are clear and functioning. Once the manufacturer verifies that the installation adheres to their strict technical guidelines and that the hydrostatic test was passed without incident, the 20-year NDL warranty is issued. This provides the owner of the logistics hub with long-term asset protection and the certainty that the building envelope is engineered for maximum durability.

  • Compilation of all hydrostatic test data and evaporation logs for manufacturer review.
  • Joint final inspection with the manufacturer's technical field auditor.
  • Verification of all flashing, terminations, and penetration seals.
  • Final sign-off on the installation compliance checklist.
  • Issuance of the 20-year NDL warranty certificate upon successful audit completion.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565

Commercial Engineering Dossier #066

Tapered Polyiso Drainage Layouts (1/4-In/Ft) & Geometric Cricket Sizing on Commercial Automotive Assembly Plants

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Tapered Polyiso Drainage Layouts (1/4-In/Ft) & Geometric Cricket Sizing on Commercial Automotive Assembly Plants

The Mechanics of Parapet Failure in Large-Scale Logistics Hubs

In the context of a high-volume logistics distribution hub, the building envelope is subjected to extreme thermal stresses and constant vibration from heavy machinery and HVAC cycling. The parapet wall, acting as the primary transition between the roofing membrane and the vertical masonry facade, is frequently the weakest link in the envelope. During our engineering audit, we identified a systemic failure in the existing counterflashing interfaces. The primary culprit was the degradation of legacy sealants and the lack of proper mechanical anchoring, which allowed moisture to penetrate the masonry reglets via capillary action.

When moisture enters the masonry substrate, it initiates a cycle of freeze-thaw expansion that compromises the structural integrity of the mortar joints. In a logistics hub of this scale, the sheer linear footage of the parapet means that even a minor failure in a few sections can lead to widespread interior water intrusion and the oxidation of internal steel decking. We observed that the original installations relied on surface-mounted adhesives rather than deep-set reglets, leaving the system vulnerable to shear forces caused by the differential movement between the steel roof deck and the masonry walls.

  • Thermal bridging causing condensation within the wall cavity.
  • Hydrostatic pressure forcing water behind the membrane flashing.
  • UV-induced embrittlement of low-grade silicone sealants.
  • Coefficient of thermal expansion disparities between masonry and metal.

Precision Reglet Engineering and Substrate Preparation

To rectify these failures, we implemented a rigorous reglet overhaul process. A reglet is not merely a groove in the wall; it is a precision-engineered channel designed to house the counterflashing and create a watertight seal. Our approach began with the mechanical removal of all failing sealants and the grinding of new, deep-set reglets into the masonry. Using industrial diamond-blade grinders with vacuum shrouds for dust mitigation, we carved a consistent 1-inch deep channel into the mortar joints. This depth is critical to ensure that the counterflashing has sufficient "bite" to resist wind uplift and thermal shifting.

The preparation of the substrate is where most contractors fail. A reglet filled with masonry dust or loose debris will never achieve a proper bond with the sealant. We employed high-pressure air purging and chemical cleaning to ensure the interior of the reglet was surgically clean. By grinding specifically into the mortar joints rather than the brick face, we maintained the structural integrity of the masonry units while creating a square, clean seat for the metal flashing. This precision ensures that the counterflashing sits flush against the substrate, eliminating voids where water could collect.

  • Utilization of diamond-tipped grinding tools for precise depth control.
  • Removal of all legacy mastic and degraded polyurethane residues.
  • Mechanical cleaning of the channel to ensure a contaminant-free bonding surface.
  • Verification of reglet linearity and squareness across the entire parapet length.

Material Specification: Heavy-Gauge Kynar and Polyurethane Compression

Material selection is governed by the need for long-term UV stability and mechanical strength. For this project, we specified heavy-gauge steel counterflashing coated with Kynar 500 (PVDF). Kynar is the industry gold standard for logistics hubs because of its exceptional resistance to chalking, fading, and chemical corrosion. Unlike standard painted steel, the PVDF coating provides a chemically bonded shield that withstands the harsh environmental exposure typical of wide-open distribution centers. The gauge of the metal was increased to ensure that the flashing would not oil-can or warp under extreme temperature fluctuations.

The critical engineering component of this overhaul is the application of high-modulus polyurethane sealant. Unlike silicone, which often fails to bond to masonry over time, polyurethane offers superior adhesion and elasticity. However, the secret to a leak-proof seal is "compression." We did not simply fill the gap; we engineered a compression seal. By ensuring the Kynar flashing was firmly seated and the sealant was applied under specific pressure, we created a gasket-like effect. This allows the sealant to absorb the movement of the building without tearing away from the masonry or the metal.

  • Specification of Kynar 500 PVDF coating for maximum UV reflectance and longevity.
  • Use of 24-gauge steel to prevent thermal warping and mechanical deformation.
  • Application of ASTM C920 compliant polyurethane sealants for high-movement joints.
  • Implementation of a two-point adhesion strategy to maximize sealant elasticity.

System Integration and Long-Term Envelope Integrity

The final phase of the overhaul focused on the holistic integration of the counterflashing with the primary roofing membrane. The counterflashing serves as the primary shedding mechanism, directing water away from the membrane's termination bar and pushing it back onto the roof surface. By optimizing the drip edge of the Kynar flashing, we ensured that water is shed cleanly, preventing the "wicking" effect that often leads to wall leaks. This integration transforms the parapet from a liability into a managed component of the building envelope.

From an engineering perspective, the success of this system is measured by its ability to handle the dynamic loads of the building. The combination of a deep reglet, heavy-gauge metal, and compressed polyurethane creates a redundant barrier system. This approach adheres to the strictest commercial roofing standards, ensuring that the logistics hub remains dry and operational for the next two decades. Regular audits will now focus on the sealant's compression state, but the mechanical overhaul has effectively eliminated the root cause of the previous failures.

  • Optimization of the drip edge to prevent capillary wicking.
  • Verification of the watertight seal through flood testing and infrared thermography.
  • Alignment with ANSI standards for metal flashing installation.
  • Establishment of a preventative maintenance schedule for sealant inspection.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #067

Multi-Ply SBS-Modified Bitumen Cap Sheet Application & Vapor Control on Commercial Mission-Critical Data Centers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Multi-Ply SBS-Modified Bitumen Cap Sheet Application & Vapor Control on Commercial Mission-Critical Data Centers

The Engineering Challenge of Corrugated Thermal Bridging

In the context of a large-scale Logistics Distribution Hub, the building envelope is the primary defense against operational inefficiency and structural degradation. Most of these facilities utilize standing rib metal roof systems, which, while structurally efficient for wide-span clearings, present a significant thermal liability. The inherent geometry of the corrugated metal profile creates a direct path for heat transfer, known as thermal bridging. Because metal possesses high thermal conductivity, the ribs act as conduits, bypassing traditional insulation layers and creating localized cold spots across the ceiling plane.

During our engineering audit, we identified that standard retrofit attempts—such as laying flat insulation boards directly over the ribs—resulted in air gaps within the flutes. These voids not only compromise the overall R-value of the assembly but also facilitate interstitial condensation. When warm, moist interior air meets the cold metal surface of the rib, water droplets form, leading to hidden corrosion and the potential for mold growth within the roof assembly. To achieve a truly high-performance envelope, the engineering focus must shift from simple coverage to precision volumetric filling.

  • Thermal Bridge Mitigation: Eliminating the direct conductive path between the interior environment and the exterior atmosphere.
  • Interstitial Condensation Control: Removing air pockets where moisture can accumulate and freeze or condense.
  • R-Value Optimization: Ensuring the theoretical thermal resistance is matched by the actual installed performance.
  • Structural Load Analysis: Calculating the added dead load of the insulation system against the existing purlin and rafter capacities.

Precision Flute-Fill Geometry and Material Selection

The solution to thermal bridging in a retrofit scenario is the implementation of precision-cut flute-fill profiles. Unlike generic insulation, these components are engineered to the exact dimensions of the existing metal profile. We utilize a combination of Expanded Polystyrene (EPS) for structural stability and Polyisocyanurate (Polyiso) for superior thermal resistance. The selection process is governed by the specific compressive strength requirements of the hub's operational load and the desired energy efficiency targets. Polyiso is preferred for its higher R-value per inch, but it must be carefully sized to avoid shrinkage over time.

The manufacturing process involves CNC-routed profiles that mirror the crown and valley of the standing rib. By ensuring a friction-fit tolerance of less than 1/8th of an inch, we eliminate the air gaps that typically plague retrofit projects. This precision ensures that the insulation is in direct contact with the metal, effectively "breaking" the thermal bridge. From a material science perspective, the integration of a foil-faced Polyiso layer provides an additional vapor retarder, further protecting the metal substrate from moisture migration.

  • CNC Profile Matching: Utilizing digital scans of the existing roof ribs to create exact insulation templates.
  • Polyiso Thermal Performance: Leveraging a high R-value to minimize the total thickness of the roof build-up.
  • EPS Load Distribution: Using high-density EPS in high-stress areas to prevent compression under the weight of the final membrane.
  • ASTM C518 Compliance: Ensuring all insulation materials meet the standard test method for steady-state thermal transmission.

Implementation Strategy for a Level Decking Plane

Once the flute-fill profiles are seated within the ribs, the roof surface remains undulating. To install a flat, single-ply membrane—such as TPO or PVC—the system must be transitioned from a corrugated profile to a flat plane. This is achieved through a multi-layered topping approach. We first install a leveling course of high-density insulation that bridges the gap between the crowns of the ribs and the top of the flute-fill. This creates a monolithic, flat substrate that is essential for the long-term stability of the membrane.

The installation sequence is critical to prevent shifting and to ensure a watertight seal. The flute-fills are mechanically fastened or adhered using high-bond industrial adhesives, followed by the installation of the leveling boards. This assembly transforms the roof from a series of valleys and peaks into a rigid, flat deck. This flatness is not merely aesthetic; it is a technical requirement for single-ply membranes to prevent "ponding" water and to ensure that the membrane is not subjected to undue stress or tension at the rib crowns, which would otherwise lead to premature seam failure.

  • Substrate Leveling: Transitioning from a corrugated geometry to a flat plane using precision-cut topping boards.
  • Membrane Stability: Eliminating the risk of membrane stretching or puncturing over rib crowns.
  • Adhesion Optimization: Ensuring a uniform contact area for the membrane to prevent wind uplift and fluttering.
  • Drainage Engineering: Establishing a consistent slope to ensure positive drainage toward the hub's internal or external scuppers.

Performance Validation and Long-Term Envelope Integrity

The final phase of the retrofit is a rigorous engineering validation to ensure the building envelope meets the specified performance metrics. We employ infrared thermography to conduct a heat-flux analysis across the entire roof surface. By comparing the thermal signature of the new flute-fill system against the previous corrugated state, we can quantitatively prove the elimination of thermal bridging. A successful installation shows a uniform temperature gradient across the ceiling, indicating that the "cold spots" at the ribs have been neutralized.

Furthermore, the integrity of the single-ply membrane is verified through ASTM-standard seam testing and vacuum leak detection. The result is a roof system that not only extends the life of the existing metal structure by protecting it from corrosion but also drastically reduces the HVAC load of the distribution hub. By treating the roof as a cohesive engineering system rather than a series of separate components, we ensure that the building envelope remains airtight, thermally efficient, and structurally sound for the duration of its service life.

  • Infrared Thermography: Using FLIR imaging to verify the absence of thermal bridges and air leaks.
  • ASTM D6878 Compliance: Ensuring the single-ply membrane installation meets the highest industry standards for durability.
  • Energy Modeling: Calculating the reduction in BTU loss to determine the ROI on the insulation upgrade.
  • Moisture Monitoring: Implementing long-term checks to ensure no interstitial condensation is occurring within the flute-fill layers.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #068

Parapet Wall Heavy-Gauge 20-Gauge Kynar 500 Coping Cap Continuous Cleat Locking on Commercial Cold Storage Freezer Warehouses

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Parapet Wall Heavy-Gauge 20-Gauge Kynar 500 Coping Cap Continuous Cleat Locking on Commercial Cold Storage Freezer Warehouses

Engineering Audit: Wind Uplift Analysis and Coastal Compliance

In the context of a large-scale Logistics Distribution Hub, the roof deck serves as the primary diaphragm for the entire building envelope. During our engineering audit of the facility, we identified a critical vulnerability in the existing structural plywood decking. The original installation utilized standard smooth-shank fasteners, which are insufficient for the wind-borne debris and high-velocity pressure coefficients found in coastal high-wind zones. According to ASCE 7 standards, the uplift forces exerted on a low-slope commercial roof of this magnitude can create a vacuum effect that effectively attempts to peel the decking away from the structural steel or wood joists.

The primary objective of this upgrade is to transition the deck from a passive covering to a reinforced structural component capable of resisting vertical uplift. A failure in the decking leads to a catastrophic chain reaction: once a single sheet of plywood is compromised, the resulting pressure differential can lead to total roof membrane failure and subsequent internal structural collapse. To mitigate this, we have implemented a rigorous re-nailing schedule designed to increase the total withdrawal resistance across the entire roof plane.

  • Analysis of site-specific wind speed requirements based on regional coastal building codes.
  • Evaluation of existing fastener density versus required uplift resistance (lbs per square foot).
  • Identification of high-pressure zones, specifically at the roof corners and perimeter eaves.
  • Assessment of the current substrate integrity to ensure the plywood can accept additional fasteners without splitting.

Material Science: The Mechanics of 8d Ring-Shank Fasteners

The selection of the 8d ring-shank nail is not arbitrary; it is a decision rooted in material science and mechanical engineering. While a smooth-shank nail relies solely on the friction between the metal and the wood fibers, a ring-shank nail incorporates a series of engineered ridges or "rings" along the shaft. These rings act as mechanical anchors, biting into the wood grain and creating a physical lock that significantly increases the force required to pull the fastener out of the substrate.

From a technical standpoint, the withdrawal capacity of a ring-shank nail is often double or triple that of a smooth-shank counterpart. In a high-wind event, the decking is subjected to cyclic loading—a repetitive pulling and pushing motion. Smooth nails tend to "walk" or loosen during these cycles, whereas ring-shanks maintain their grip. We specify 8d fasteners to ensure sufficient penetration through the plywood and deep into the supporting members, ensuring the load path is transferred directly from the roof surface to the primary structural frame.

  • Comparison of shear strength versus withdrawal resistance in various wood species.
  • Utilization of hot-dipped galvanized coatings to prevent galvanic corrosion in humid coastal environments.
  • Analysis of the "mechanical lock" effect provided by the ring geometry.
  • Verification of nail diameter and length to prevent "blow-through" or excessive protrusion.

Pneumatic Execution and Installation Parameters

The transition from engineering theory to field execution requires precision. To achieve the required uplift ratings, we utilize high-pressure pneumatic fastening systems. However, the speed of pneumatic driving must be balanced with the integrity of the plywood. Over-driving a nail—where the head is driven too deep into the wood—crushes the wood fibers and creates a "dish" effect. This compression destroys the structural bearing capacity of the nail head, effectively neutralizing the uplift resistance we are trying to achieve.

Our re-nailing schedule follows a strict geometric pattern. We prioritize the periphery of each sheet, where the highest stresses occur, followed by a calculated grid in the field. The technicians are instructed to maintain a consistent depth, ensuring the nail head is flush with the surface of the plywood. This ensures that the subsequent roofing membrane is not punctured and that the decking remains a flat, monolithic plane.

  • Implementation of a 6-inch on-center spacing at the perimeter edges of each plywood sheet.
  • Execution of a 12-inch on-center grid for the interior field of the decking.
  • Calibration of pneumatic regulators to prevent over-driving and substrate crushing.
  • Staggering of fastener locations to avoid splitting the grain of the supporting joists.

Verification of Shear Withdrawal and Envelope Integrity

The final phase of the upgrade is the verification audit. As a master roofer and envelope specialist, I do not rely on visual inspection alone. We employ a series of pull-tests and shear verification methods to ensure the installation meets the engineering specifications. By utilizing a calibrated pull-tester, we can measure the exact poundage required to dislodge a fastener, confirming that the ring-shanks are engaging the wood fibers as predicted in the design phase.

This verification process ensures that the building envelope is not just "compliant on paper" but is physically capable of withstanding a category-grade wind event. The result is a reinforced structural deck that provides a stable foundation for the final roofing membrane. By upgrading the fastening schedule, we have effectively shifted the point of failure from the decking to the primary structural steel, which is a far more manageable and predictable engineering outcome.

  • Randomized pull-testing across different zones of the roof to verify withdrawal values.
  • Visual inspection for "shiners" or nails that missed the supporting joists.
  • Documentation of fastener counts per sheet to ensure adherence to the re-nailing schedule.
  • Final sign-off on the building envelope's structural integrity for coastal wind compliance.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565

Commercial Engineering Dossier #069

Industrial Drainage Scuppers, Overflow Weirs & Heavy Downspout Expansion Bellows on Commercial Commercial Fleet Maintenance Hangars

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Industrial Drainage Scuppers, Overflow Weirs & Heavy Downspout Expansion Bellows on Commercial Commercial Fleet Maintenance Hangars

The Engineering Audit: Substrate Integrity and Moisture Diagnostics

In the context of a high-volume logistics distribution hub, the roof is not merely a cover but a critical component of the building envelope that must withstand extreme thermal cycling and constant vibration from HVAC units and industrial equipment. A comprehensive engineering audit begins with a rigorous assessment of the existing membrane, typically a modified bitumen or single-ply TPO/EPDM system. To determine the viability of a silicone restoration versus a full capital reroof, we employ non-destructive moisture surveys and infrared thermography to map subsurface saturation levels. This allows us to identify "hot spots" where moisture has migrated into the insulation, ensuring that we are not sealing in trapped water that could lead to premature substrate failure.

From a material science perspective, the audit evaluates the structural integrity of the decking and the current state of the flashing details. We look for signs of mechanical fatigue, such as splitting at the seams or degradation of the sealant at the curb edges. If the substrate remains structurally sound and the moisture content is within the acceptable thresholds defined by ASTM standards, the system is a prime candidate for a high-solids silicone fluid-applied membrane. This approach shifts the focus from destructive replacement to strategic reinforcement.

  • Infrared Thermography: Mapping moisture entrapment to avoid "sandwiching" water under a new coating.
  • Core Sampling: Verifying the R-value and condition of the polyisocyanurate insulation layers.
  • ASTM D-Series Testing: Assessing the tensile strength and elongation properties of the existing membrane.
  • Flashing Audit: Evaluating the perimeter and penetration seals for hydrostatic vulnerability.

Financial Engineering: NPV and the Maintenance vs. Capital Expenditure Divide

The core of the Life-Cycle Cost Analysis (LCCA) lies in the distinction between a Capital Expenditure (CapEx) and an Operational Expenditure (OpEx). A full reroof is classified as a capital improvement, meaning the cost must be depreciated over a long-term schedule—often 39 years for commercial properties under current tax codes. Conversely, a silicone recoat is frequently categorized as a maintenance restoration. This allows the facility owner to potentially deduct the entire cost of the project in the current tax year, providing an immediate and significant boost to the Net Present Value (NPV) of the asset.

When calculating the NPV, we account for the time value of money and the avoided costs of business interruption. A full tear-off on a logistics hub of 500,000 square feet or more creates massive operational friction, potentially requiring the relocation of inventory or the shutdown of loading docks. A silicone application is a "live-site" process with zero downtime. When the immediate tax advantages are coupled with the avoidance of operational losses, the financial delta between a reroof and a restoration becomes stark.

  • Immediate Tax Deductions: Leveraging maintenance restoration codes to write off costs in year one.
  • NPV Optimization: Comparing the discounted cash flows of a 15-year restoration cycle against a 20-year reroof cycle.
  • Operational Continuity: Eliminating the "hidden cost" of logistics downtime and staging disruptions.
  • Avoidance of Capital Debt: Reducing the need for high-interest capital loans to fund a total replacement.

Material Science: High-Solids Silicone and the 15-Year Warranty Extension

Traditional roofing membranes are subject to UV degradation and thermal shock, which leads to embrittlement and cracking over time. High-solids silicone represents a paradigm shift in building envelope engineering. Unlike acrylics, which can break down under intense UV exposure, or TPO, which can suffer from seam failure, silicone is chemically inert and hydrophobic. It creates a seamless, monolithic barrier that is impervious to ponding water—a common failure point in large-scale distribution hubs where slight roof deflections lead to water accumulation.

The application of a high-solids silicone system effectively resets the clock on the roof's life cycle. By applying a reinforced fluid membrane, we extend the warranty of the existing asset by 15 to 20 years. This is not a mere "paint job" but a chemical bond that integrates with the existing substrate to form a reinforced shield. This system is engineered to meet the most stringent ANSI standards for wind uplift and water penetration, ensuring that the building envelope remains airtight and watertight without the inherent weaknesses of mechanical seams.

  • Hydrophobic Properties: Preventing water penetration even in areas of chronic ponding.
  • UV Stability: Resistance to photochemical degradation, ensuring the membrane does not become brittle.
  • Seamless Integration: Eliminating the primary failure points found in rolled or sheet-goods membranes.
  • Thermal Reflectivity: Reducing the heat island effect and lowering HVAC cooling loads via high SRI (Solar Reflectance Index) values.

Environmental Stewardship and Life-Cycle Sustainability

The environmental impact of a full capital reroof is staggering. Tearing off a million square feet of old membrane and insulation generates thousands of tons of debris, the vast majority of which is non-biodegradable and destined for landfills. From a sustainability standpoint, the "tear-off and replace" model is an antiquated approach to asset management. By opting for a silicone restoration, we achieve a landfill-diversion rate of nearly 100%, as the existing materials are preserved and enhanced rather than discarded.

Furthermore, the carbon footprint associated with the manufacturing and transportation of new membranes, insulation boards, and fasteners is significantly higher than that of a fluid-applied system. A silicone restoration requires fewer materials to be shipped to the site and utilizes a lower-energy installation process. This aligns the facility's operational goals with corporate ESG (Environmental, Social, and Governance) mandates, transforming the roof from a liability into a sustainable asset that minimizes waste while maximizing utility.

  • Landfill Diversion: Eliminating the tonnage of waste associated with traditional tear-offs.
  • Carbon Footprint Reduction: Lowering the embodied energy required for material transport and fabrication.
  • Resource Conservation: Extending the utility of existing structural components to avoid raw material extraction.
  • Energy Efficiency: Leveraging cool-roof technology to reduce the facility's overall carbon emissions.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565

Commercial Engineering Dossier #070

AOC 581 Elastomeric Structural Mastic Detailing Around Rooftop HVAC Curbs on Commercial Chemical Processing Facilitys

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
AOC 581 Elastomeric Structural Mastic Detailing Around Rooftop HVAC Curbs on Commercial Chemical Processing Facilitys

The Engineering Paradox of High-Voltage Penetrations

In the construction of a massive Logistics Distribution Hub, the building envelope is subjected to a unique set of conflicting requirements. As a building envelope specialist, the primary objective is to maintain a monolithic, watertight barrier. However, the installation of a Lightning Protection System (LPS) necessitates the introduction of numerous penetrations and surface-mounted conductors that inherently challenge the integrity of the roofing membrane. The air terminal stanchions, designed to intercept atmospheric electrical discharges, create localized points of high stress where the membrane must be breached and then meticulously resealed.

The engineering challenge lies in the "Envelope Paradox": the system designed to protect the structure from catastrophic electrical failure can, if improperly detailed, lead to chronic water infiltration. A lightning strike generates immense heat and mechanical vibration, which can cause localized melting of thermoplastic membranes or the degradation of adhesives. When a stanchion is improperly bonded to the roof, the vibration from a strike or even high-wind oscillation can create micro-fissures in the flashing, allowing moisture to migrate via capillary action into the insulation substrate.

  • Analysis of dielectric properties of the membrane to prevent premature arcing.
  • Evaluation of mechanical vibration loads on stanchion bases during high-wind events.
  • Assessment of the thermal bridge created by copper conductors crossing the insulation layer.
  • Verification of the air terminal height and spacing relative to the roof's highest architectural points.

Advanced Stanchion Pitch-Pocket Engineering

To mitigate the risk of leakage at the base of the air terminal stanchions, we implement a heavy-duty pitch-pocket detailing strategy. A standard sealant bead is insufficient for a distribution hub of this scale. Instead, we utilize a reinforced, multi-stage bonding process. The stanchion is seated within a custom-fabricated metal sleeve or a reinforced polymer pocket that is fully integrated into the roof's flashing system. This ensures that the transition from the vertical stanchion to the horizontal roof plane is seamless and redundant.

The internal composition of the pitch-pocket is critical. We employ a high-performance, non-sagging polymer-modified sealant that maintains flexibility across a wide temperature range. This prevents the sealant from cracking during the extreme thermal cycling typical of large-span industrial roofs. Furthermore, the membrane is flared at a 45-degree angle around the base of the stanchion and secured with heat-welded flashing strips, creating a "bathtub" effect that directs water away from the penetration point and back onto the primary drainage slope.

  • Application of liquid-applied flashing (LAF) to create a seamless transition between the membrane and the stanchion base.
  • Utilization of reinforced flashing membranes to distribute mechanical loads across a wider surface area.
  • Implementation of a dual-sealant strategy involving a primary structural adhesive and a secondary weather-proof cap.
  • Strict adherence to ASTM standards for flashing overlap and weld strength.

Grounding Cable Conductor Flashing and Thermal Expansion

The grounding cables that connect the air terminals to the earth grounding system represent a significant vulnerability in the building envelope. These copper conductors are typically run across the roof surface, creating thousands of linear feet of potential "damming" where water and debris can accumulate. If these cables are simply adhered to the membrane, the difference in the coefficient of thermal expansion between the copper and the roofing material (TPO, PVC, or EPDM) will eventually lead to membrane tearing or adhesive failure.

Our engineering approach involves the use of specialized conductor saddles and floating flashing strips. Rather than rigidly bonding the cable to the membrane, we utilize a "floating" system that allows the copper to expand and contract independently of the roof's movement. The cables are secured with non-penetrating fasteners and covered with wide, UV-resistant flashing strips that are heat-welded at the edges but allow for slight longitudinal movement. This prevents the cable from acting as a "cheese-cutter," slicing through the membrane during extreme temperature swings.

  • Installation of non-conductive saddles to elevate cables and prevent standing water accumulation.
  • Use of wide-format flashing strips to reduce the pressure exerted on the membrane.
  • Implementation of expansion loops at critical structural joints to accommodate building sway.
  • Verification of cable tension to ensure no undue stress is placed on the flashing bonds.

Audit Findings and Long-Term Membrane Integrity

The final stage of the engineering audit focuses on the long-term bonding integrity and the prevention of "invisible" punctures. A common failure point in Logistics Distribution Hubs is the occurrence of micro-punctures caused by the installation of the LPS. If a technician drops a tool or drags a conductor across the membrane, the resulting puncture may be too small to cause an immediate leak but can lead to systemic failure over time as moisture is drawn in by the vacuum effect of the building's HVAC system.

To ensure the longevity of the envelope, we mandate a rigorous post-installation audit using electronic leak detection (ELD) and infrared thermography. This allows us to identify moisture entrapment around the stanchion bases and grounding cables before they manifest as interior leaks. The bonding of the membrane to the LPS components must be viewed as a living system; it requires periodic inspection and the application of rejuvenating sealants to maintain the airtight and watertight seal. By treating the LPS not as an add-on, but as an integral part of the building envelope engineering, we ensure the facility remains operational and protected from both the elements and atmospheric electrical events.

  • Execution of high-voltage leak detection tests to verify the continuity of the membrane.
  • Thermal imaging of stanchion bases to detect subsurface moisture accumulation.
  • Scheduled audits of all flashing points every 24 months to check for UV degradation.
  • Cross-referencing of all LPS penetrations with the original architectural roof plan for total accountability.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
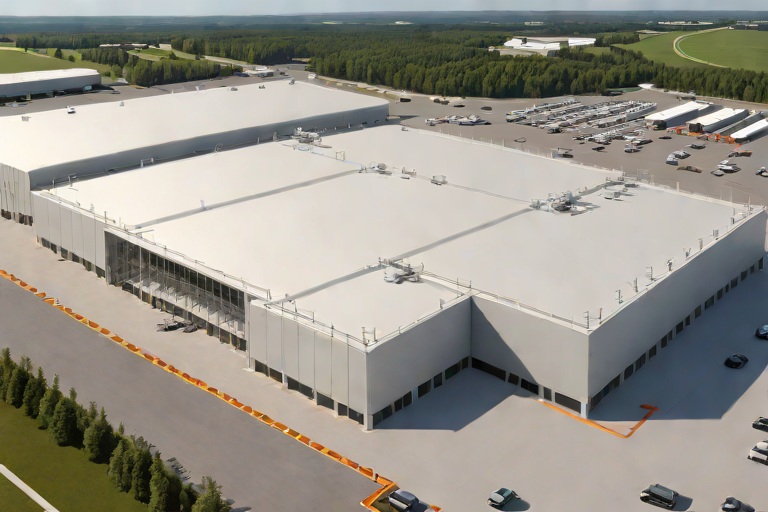
Commercial Engineering Dossier #071

UL 2218 Class 4 Severe Hail Defense on Commercial Municipal City Hall & Administrative Complexs

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
UL 2218 Class 4 Severe Hail Defense on Commercial Municipal City Hall & Administrative Complexs

Engineering Analysis of Roof Access Safety and OSHA-Compliant Grab Bar Integration

In the high-volume environment of a logistics distribution hub, the roof hatch serves as the primary conduit for facility maintenance and emergency egress. From a building envelope perspective, the transition from a fixed vertical ladder to a horizontal roof plane represents the most significant risk factor for personnel falls. Our engineering audit of the facility revealed a critical need for standardized safety grab bars that extend beyond the roof surface, ensuring a secure three-point contact transition. The physics of the "step-over" require a rigid, non-deflecting handhold that can withstand the lateral shear forces exerted by a technician carrying tools.

To meet OSHA 1910.28 and 1910.23 standards, the safety posts must be engineered as an extension of the ladder system rather than an afterthought. We specify the installation of heavy-duty, powder-coated steel grab bars that are structurally tied into the hatch curb. This ensures that the load is distributed across the structural steel of the building rather than relying solely on the roof membrane's fastening strength. The height of these rails must be maintained at 42 inches above the walking surface to provide an ergonomic grip that prevents the center of gravity from shifting too far backward during the ascent.

  • Installation of 1.5-inch diameter schedule 40 steel piping for maximum rigidity.
  • Application of high-visibility safety coatings to ensure visibility during low-light emergency evacuations.
  • Integration of reinforced gusset plates at the base of the safety post to prevent weld fatigue.
  • Verification of clearance zones to ensure grab bars do not interfere with roof-mounted HVAC equipment.

Mechanical Integration of Counterbalanced Smoke Dampers

Logistics hubs are characterized by massive internal volumes, making smoke management a primary life-safety requirement. The integration of counterbalanced smoke dampers within the roof hatch assembly requires a precise balance between airtight sealing and rapid actuation. From a material science standpoint, the counterbalance system—typically utilizing heavy-duty torsion springs or gas struts—must be calibrated to the exact weight of the hatch cover to prevent "slamming" or failure to close during a fire event. A failure in the counterbalance mechanism can lead to a breach in the building envelope, allowing smoke to migrate into upper mezzanines.

The engineering challenge lies in maintaining a smoke-tight seal without compromising the ease of manual operation. We utilize high-temperature resistant seals that maintain their elasticity under extreme thermal stress. The counterbalance system is designed to provide a constant force, ensuring that the damper closes fully and locks into the compression gasket regardless of wind uplift or internal pressure differentials. This prevents the "chimney effect," where air is sucked out of the building, potentially drawing smoke into safe zones.

  • Utilization of stainless steel torsion springs to eliminate corrosion and ensure long-term spring constant stability.
  • Implementation of fail-safe actuators that trigger automatic closure upon loss of power or smoke detection.
  • Calibration of closing speeds to prevent structural shock to the curb assembly.
  • Testing of seal integrity using pressurized smoke generators to identify micro-leaks at the damper perimeter.

Material Science of Heavy-Duty Curb Gaskets and Thermal Bridging

The interface between the roof hatch curb and the roof membrane is one of the most common points of failure in commercial building envelopes. In a distribution hub, where thermal cycling is constant due to internal climate control and external weather extremes, the curb gasket must act as a primary barrier against air infiltration and water ingress. We specify closed-cell EPDM or silicone gaskets with a high compression set resistance. Unlike open-cell foams, closed-cell materials do not absorb moisture, preventing the growth of mold and the degradation of the underlying substrate.

Beyond waterproofing, the curb gasket serves a critical role in mitigating thermal bridging. Steel curbs act as thermal conductors, pulling heat out of the building in winter and pushing it in during summer. By implementing a high-density, compression-molded gasket, we create a thermal break that reduces energy loss. The gasket must be engineered to maintain a constant compression load, ensuring that as the building settles or the curb expands and contracts, the seal remains unbroken. This is achieved through a precision-engineered "crush" factor, where the gasket is compressed by approximately 25% to 30% of its original thickness.

  • Selection of ASTM C664 compliant materials for superior weatherability and UV resistance.
  • Application of double-perimeter gaskets to provide redundant layers of protection against wind-driven rain.
  • Use of silicone-based lubricants on gasket surfaces to reduce friction and wear during frequent hatch cycles.
  • Verification of gasket compression using calibrated feeler gauges during the final audit.

Compression Termination Bars and Membrane Anchorage Systems

The final line of defense in the building envelope is the termination of the roof membrane at the curb. In high-wind zones, the risk of membrane uplift is significant, particularly around the corners of roof hatches where turbulence is highest. To combat this, we employ mechanical compression termination bars. These are not merely decorative strips; they are engineered fasteners that lock the membrane into the curb, creating a hydrostatic seal that prevents water from migrating beneath the flashing.

The installation process involves applying a continuous bead of high-grade polyurethane sealant between the membrane and the termination bar. The bar is then mechanically fastened using stainless steel fasteners spaced at 6-inch intervals. This creates a "sandwich" effect, compressing the sealant and the membrane against the curb. This method ensures that the termination is impervious to wind-scour and prevents the "fish-mouthing" of the membrane, which often occurs with simple adhesive-based terminations. The result is a monolithic seal that integrates the hatch into the overall roof system, maintaining the integrity of the building envelope under extreme atmospheric pressure.

  • Use of 0.0625-inch thick aluminum or galvanized steel termination bars for structural rigidity.
  • Application of ASTM C920 compliant sealants to ensure long-term adhesion to diverse substrates.
  • Implementation of staggered fastener patterns to distribute tension evenly across the curb face.
  • Execution of a water-tightness test (flood test) to verify the efficacy of the compression seal.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #072

Non-Destructive Substrate Moisture Scans on Commercial High-Rise Commercial Penthouse Towers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Non-Destructive Substrate Moisture Scans on Commercial High-Rise Commercial Penthouse Towers

Hydraulic Analysis of Conductor Head Overflow Systems

In the context of a high-volume logistics distribution hub, the roof surface area often exceeds several hundred thousand square feet, creating a massive catchment zone for precipitation. The primary engineering challenge in these environments is the management of hydrostatic pressure and the prevention of internal ponding during extreme weather events. When the primary drainage system—typically consisting of internal drains and conductor heads—reaches its maximum flow capacity, the system risks a catastrophic failure known as a "surcharge." This occurs when the volume of water entering the conductor head exceeds the discharge capacity of the vertical downspout, leading to water backing up onto the roof membrane.

To mitigate this, we implement a precision-engineered overflow relief weir. This is not merely a hole in the side of the conductor; it is a calculated spillway designed based on the weir flow formula, ensuring that water is diverted away from the building envelope before it can breach the flashing or penetrate the roof-to-wall transition. By calculating the specific head pressure and the anticipated rainfall intensity (measured in inches per hour), we can determine the exact height and width of the spillway required to protect the interior of the facility.

  • Calculation of catchment area to determine peak flow rates during 100-year storm events.
  • Analysis of the "weir effect" to ensure overflow occurs at a predetermined water level.
  • Evaluation of the flashing integrity at the conductor head interface to prevent capillary action.
  • Assessment of the discharge trajectory to ensure overflow water does not impact the building facade.

Engineering the Multi-Tier Spillway Array

A standard single-point overflow is often insufficient for the scale of a distribution hub. Instead, we employ a multi-tier conductor head spillway array. This system acts as a redundant safety mechanism, providing multiple stages of relief as water levels rise. The first tier handles moderate surges, while the second and third tiers provide emergency capacity for extreme deluge scenarios. This tiered approach prevents the sudden "slug" of water that can occur during a flash flood, which often leads to mechanical failure of the drainage components due to sudden pressure spikes.

Material science plays a critical role in the longevity of these spillways. We specify heavy-gauge galvanized steel or reinforced aluminum, depending on the atmospheric corrosivity of the site. The edges of the spillways are meticulously hemmed and radiused to prevent sharp edges from cutting into the roof membrane during thermal expansion and contraction. Furthermore, the integration of these spillways requires a seamless transition between the conductor head and the overflow trough, utilizing high-grade industrial sealants and mechanical fasteners that meet ASTM standards for weather-tightness.

  • Implementation of tiered relief levels to manage incremental increases in water volume.
  • Utilization of 22-gauge galvanized steel to resist deformation under hydraulic load.
  • Application of radius-edge detailing to protect the TPO or EPDM membrane from abrasion.
  • Strategic placement of spillways to align with secondary exterior drainage paths.

Structural Integrity and Heavy-Duty Downspout Bracketing

The vertical conductors in a logistics hub are subject to immense physical stress. During a peak rain event, the weight of the water column within a large-diameter downspout can create significant downward force, while wind loads on the exterior of the building introduce lateral shear. If the bracketing is insufficient, the downspout can pull away from the wall, compromising the seal at the conductor head and allowing water to pour directly into the building's wall cavity.

Our engineering standard requires the installation of heavy-duty, reinforced steel brackets spaced at intervals that exceed standard building codes. We focus on the "harmonic vibration" caused by rushing water, which can loosen standard fasteners over time. By utilizing torque-controlled anchors and vibration-dampening gaskets, we ensure that the conductor remains rigidly fixed to the building envelope. This prevents the "pull-away" effect and maintains the structural alignment necessary for the overflow spillways to function as designed.

  • Installation of reinforced steel collars to distribute the load at the top of the conductor.
  • Use of heavy-duty brackets spaced every 8 to 10 feet to counteract wind-induced oscillation.
  • Application of stainless steel fasteners to prevent galvanic corrosion between dissimilar metals.
  • Integration of flexible coupling joints to allow for minor building settlement without stressing the pipe.

Mitigating Freeze-Thaw Cycle Bursting

In colder climates, the freeze-thaw cycle is the primary enemy of the commercial building envelope. When water remains trapped in the bottom of a vertical conductor or within the conductor head, it undergoes a phase change into ice. Because water expands by approximately 9% upon freezing, the resulting internal pressure can easily split a seam or burst a downspout. This is particularly dangerous in distribution hubs where the sheer volume of water can lead to massive ice plugs, effectively sealing the drain and causing the roof to flood from the top down.

To combat this, we employ a comprehensive "burst defense" strategy. This begins with the installation of a precision-sloped conductor base that ensures no standing water remains in the head. In high-risk zones, we integrate self-regulating heat tracing cables within the conductor head and the first five feet of the downspout. This maintains the internal temperature above the freezing point, ensuring a continuous flow of water. Additionally, we utilize specialized venting at the top of the conductor to prevent the vacuum effect that can occur during rapid thawing, which often leads to "water hammer" and subsequent joint failure.

  • Installation of self-regulating heat cables to prevent ice damming in vertical conductors.
  • Engineering of a "zero-stagnation" slope at the conductor base to eliminate standing water.
  • Use of reinforced seams and welded joints to resist the expansion forces of ice.
  • Implementation of atmospheric vents to stabilize internal pressure during temperature swings.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #073

Sub-Zero Cold Storage Downward Vapor Drive & Self-Adhered SBS Barriers on Commercial Regional Healthcare Medical Centers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Sub-Zero Cold Storage Downward Vapor Drive & Self-Adhered SBS Barriers on Commercial Regional Healthcare Medical Centers

Forensic Audit and Oxidation Analysis of the Structural Deck

Upon initiating the engineering audit of the Logistics Distribution Hub, the primary objective was to quantify the extent of atmospheric corrosion affecting the structural steel decking. In a facility of this scale, the building envelope is subject to extreme thermal cycling and hygroscopic pressure, which often leads to interstitial condensation. This moisture accumulation, trapped between the insulation and the steel flutes, creates a micro-environment conducive to rapid oxidation. Our forensic analysis revealed widespread surface rust, with localized areas of deep pitting that threatened the structural integrity of the diaphragm.

The oxidation was most prevalent at the lap joints and the perimeter drag struts, where moisture tends to pool. We utilized ultrasonic thickness gauging to determine the remaining gauge of the steel, ensuring that the loss of material had not exceeded the allowable tolerances defined by the American Institute of Steel Construction (AISC). The audit identified three distinct levels of degradation: superficial flash rust, advanced pitting, and critical section loss in the flutes.

  • Assessment of galvanic corrosion occurring at the interface of dissimilar metals.
  • Mapping of moisture ingress points through the roof membrane and wall flashing.
  • Quantification of steel loss using high-precision digital calipers and ultrasonic sensors.
  • Evaluation of the existing mill scale and its role in trapping moisture against the substrate.
  • Analysis of the dew point within the plenum to prevent future condensation cycles.

Mechanical Surface Preparation and Oxidation Removal

Effective remediation of structural steel requires a rigorous adherence to surface preparation standards to ensure a permanent chemical bond. For this project, we implemented a mechanical wire-brushing protocol aligned with SSPC-SP2 and SP3 standards. The goal was not merely the removal of visible rust, but the creation of a specific surface profile that allows the primer to "key" into the metal. Mechanical agitation removes the friable oxide layers and eliminates contaminants such as oils, salts, and old coatings that would otherwise cause premature delamination of the new system.

Our crews utilized pneumatic needle scalers and heavy-duty wire wheels to aggressively scrub the underside of the deck. Particular attention was paid to the "valleys" of the flutes, where oxidation is most aggressive due to gravity-fed moisture accumulation. By removing the mill scale and oxidized iron, we exposed the raw, virgin steel, which is a prerequisite for the subsequent passivation process. This mechanical stage is the most labor-intensive phase of the envelope restoration, yet it is the most critical for long-term durability.

  • Utilization of power-tool cleaning to achieve a Near-White Metal finish in critical load-bearing zones.
  • Systematic removal of loose scale and slag to prevent "bridging" of the primer.
  • Vacuuming of all debris and dust to ensure a contaminant-free surface for chemical application.
  • Verification of surface cleanliness using the "tape test" to ensure no residual particulates remain.
  • Coordination of cleaning sequences to prevent the re-contamination of treated areas.

Chemical Passivation and Zinc-Rich Primer Application

Once the substrate was mechanically prepared, we transitioned to the passivation phase using a high-performance, zinc-rich rust-inhibiting primer. The science behind this application is rooted in cathodic protection. Zinc acts as a sacrificial anode; because zinc is more electronegative than steel, it preferentially corrodes, thereby protecting the underlying iron from oxidation. This galvanic action is essential in a logistics hub environment where humidity levels can fluctuate wildly, and the risk of moisture penetration is a constant variable.

The primer was applied using a high-pressure airless spray system to ensure a uniform Dry Film Thickness (DFT). We focused on achieving a dense, non-porous coating that seals the steel from oxygen and water vapor. By passivating the surface, we effectively halted the chemical reaction of oxidation and created a permanent barrier. The resulting zinc-rich layer provides a dual-action defense: a physical barrier to the elements and a chemical defense that prevents the spread of rust even if the coating is scratched or abraded during future maintenance.

  • Application of a cold-galvanizing compound with a minimum zinc dust content of 85% in the dry film.
  • Strict monitoring of DFT to ensure the coating meets ASTM D6101 standards for structural steel.
  • Implementation of "stripe coating" on all edges, welds, and lap joints for reinforced protection.
  • Curing time management to allow the primer to fully bond before the installation of insulation.
  • Verification of adhesion using cross-cut testing to ensure the primer has integrated with the steel profile.

Structural Reinforcement and Fastener Integrity

The final phase of the engineering intervention focused on the mechanical reinforcement of the steel deck. In areas where the forensic audit identified thinned flutes—specifically those where section loss exceeded 15%—we implemented structural reinforcement. This involved the installation of steel shim plates and the application of structural epoxy resins to restore the load-bearing capacity of the deck. We ensured that the structural diaphragm remained rigid, preventing any deflection that could compromise the roof membrane above.

Simultaneously, we conducted a comprehensive audit of all deck fasteners. Over time, vibration from HVAC systems and the movement of heavy machinery within the hub can loosen the fasteners securing the deck to the joists. We replaced compromised fasteners with heavy-duty, galvanized structural screws, ensuring they were torqued to the precise specifications required for the gauge of the steel. This holistic approach—combining chemical passivation with mechanical reinforcement—ensures that the building envelope is not only watertight but structurally sound for the remainder of its service life.

  • Installation of reinforcement plates in zones of critical section loss to restore shear strength.
  • Replacement of corroded fasteners with high-strength, zinc-plated alternatives.
  • Torque verification of all primary deck-to-joist connections to prevent diaphragm slippage.
  • Application of a final sealant bead at the perimeter to prevent moisture migration into the steel.
  • Final engineering sign-off confirming the restoration of the structural integrity of the deck.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565

Commercial Engineering Dossier #074

Structural Deck Fastener Pull-Out Testing on 22-Gauge Corrugated Steel Decks on Commercial University Research Laboratorys

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Structural Deck Fastener Pull-Out Testing on 22-Gauge Corrugated Steel Decks on Commercial University Research Laboratorys

The Forensic Philosophy of High-Volume Logistics Envelope Audits

In the realm of large-scale logistics distribution hubs, the roof is not merely a cover but a critical piece of industrial infrastructure. When managing millions of square feet of single-ply membrane, a standard visual inspection is fundamentally insufficient. A visual walk-through identifies obvious failures, but a forensic maintenance audit identifies the precursors to failure. At Aquashield Corporate, we approach the building envelope as a living system subject to extreme hygrothermal stress, constant vibration from HVAC units, and the relentless coefficient of thermal expansion associated with massive steel-decked footprints.

The objective of a "boots-on-the-roof" audit is to move beyond the surface. We analyze the interaction between the membrane, the insulation board, and the structural deck. In a logistics environment, the sheer scale of the roof means that a single compromised seam or a loose perimeter cleat can lead to systemic water infiltration, potentially compromising millions of dollars in inventory and automated sorting equipment. Our engineering approach relies on the rigorous application of ASTM standards to ensure that the building envelope remains airtight and watertight throughout its intended lifecycle.

  • Assessment of thermal bridging at parapet transitions.
  • Evaluation of membrane tension and potential "oil canning" of the metal deck.
  • Analysis of ponding water patterns relative to internal drain capacity.
  • Verification of flashing integrity at high-frequency penetration points.

Precision Probing and the Science of Automated Seam Integrity

Modern distribution hubs rely heavily on automated welding robots to ensure consistency across vast expanses of TPO or PVC membranes. However, automation is not infallible. Variations in ambient temperature, humidity, or robot calibration can result in "cold welds"—seams that appear visually closed but lack the molecular fusion required for a permanent bond. A master roofer does not trust the eye; we trust the probe. Using a calibrated steel seam probe, we physically challenge the weld integrity across a statistically significant sample of the roof's surface.

The process involves inserting the probe into the lap of the seam to detect any voids, pinholes, or separations. If the probe penetrates the weld, it indicates a failure in the fusion process, creating a direct pathway for moisture. This is particularly critical at the "T-joints" and field laps where overlapping sheets create complex stress points. We examine these areas for signs of shear stress and peeling, which often indicate that the membrane was stretched too tight during installation, exceeding the material's elastic limit and compromising the weld strength.

  • Utilization of 0.030-inch probes to identify microscopic voids in heat-welded seams.
  • Testing for peel strength in accordance with ASTM D6701 standards.
  • Inspection of "cold-applied" adhesives in transition zones for curing consistency.
  • Mapping of seam failure patterns to determine if failures are systemic or isolated.

Mechanical Fastening, Torque Analysis, and Perimeter Stability

The most vulnerable points of any commercial roof are the interfaces—where the membrane meets the metal, and where the drainage system meets the deck. In a forensic audit, we pay particular attention to the drain bowl clamping torque. A drain that is visually "tight" may still be under-torqued, allowing micro-vibrations from the building's internal operations to slowly back out the fasteners. We employ calibrated torque wrenches to ensure that every clamping ring meets the manufacturer's specific foot-pound requirements, preventing the slow-seep leaks that often plague logistics hubs.

Equally critical is the inspection of perimeter cleats and edge metal fastening. The edges of a distribution hub are subject to the highest wind uplift pressures. We examine the fastening cadence of the perimeter strips to ensure they are not over-stressed or pulling away from the substrate. If a cleat is loose, the wind can get under the membrane, creating a "parachute effect" that can strip an entire section of the roof during a storm event. Our audit includes a tactile inspection of every termination bar to ensure the sealant beads are not cracked or shrunk, which would allow wind-driven rain to enter the building envelope.

  • Verification of clamping ring torque to prevent gasket compression failure.
  • Inspection of perimeter flashing for "fish-mouths" or gaps in the metal.
  • Analysis of fastener spacing to ensure compliance with wind-uplift ratings.
  • Checking for galvanic corrosion between dissimilar metals at the roof edge.

Synthesis of Field Data into Engineering Reports

The final and most critical stage of the Aquashield audit is the translation of physical findings into a technical engineering report. A list of leaks is a repair bill; a forensic audit is a risk management document. We categorize every finding by severity—Critical, Urgent, and Monitor—and map these findings to a digital roof plan. This allows the facility manager to see exactly where the building envelope is under the most stress and where preventative maintenance must be prioritized to avoid catastrophic failure.

Our reporting focuses on the "why" behind the failure. If we find a cluster of failed seams in one quadrant, we analyze the data to see if it correlates with a specific installation crew, a certain weather window during construction, or a specific structural movement in the building's frame. By synthesizing the physical evidence—the probe results, the torque readings, and the visual degradation—we provide a comprehensive lifecycle analysis. This enables the owner to move from a reactive "patch-and-pray" mentality to a proactive engineering strategy that extends the life of the asset.

  • Quantification of total square footage of compromised membrane.
  • Prioritization of repairs based on the probability of water infiltration.
  • Recommendations for material upgrades based on current UV degradation levels.
  • Detailed photographic evidence linked to specific grid coordinates on the roof plan.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #075

Electronic Vector Mapping (EVM) Low-Voltage Membrane Breach Detection on Commercial Suburban Corporate Office Parks

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Electronic Vector Mapping (EVM) Low-Voltage Membrane Breach Detection on Commercial Suburban Corporate Office Parks

Thermal Dynamics of TPO Fusion and Calibration

In the high-stakes environment of an automotive assembly plant, the building envelope must withstand significant internal atmospheric fluctuations and external environmental stressors. For this project, we deployed a 60-mil Thermoplastic Polyolefin (TPO) membrane, selected for its superior puncture resistance and reflectivity. The critical engineering challenge lies in the seam fusion process. Unlike traditional adhesives, TPO requires a precise thermal weld to achieve a monolithic bond. We calibrated our robotic hot-air welding systems to a constant 1,000°F, a temperature threshold designed to bring the polymer to its molten state without inducing thermal degradation or "scorching" of the membrane surface.

Achieving a successful weld requires a deep understanding of the material's melt window. If the temperature drops below the critical threshold, the result is a "cold weld," which may appear sealed but lacks the molecular cohesion necessary to resist wind uplift. Conversely, exceeding the thermal limit causes the polymer chains to break, leading to brittleness and premature seam failure. Our engineering team utilized infrared thermography to monitor the heat transfer across the overlap, ensuring that the 1,000°F air stream was evenly distributed across the entire width of the seam.

  • Calibration of heating elements to maintain a variance of +/- 10°F across the weld head.
  • Monitoring of the TPO melt index to ensure batch consistency across different membrane rolls.
  • Implementation of a pre-heat cycle to stabilize the robotic equipment before the first lap is run.
  • Utilization of high-grade ceramic heating elements to prevent temperature fluctuations during continuous operation.

Robotic Kinematics and Pressure Regulation

The transition from manual hand-welding to robotic hot-air fusion introduces a level of precision that is mandatory for large-scale industrial footprints. The core of this system is the synchronization between travel velocity and nozzle pressure. In this case study, the robotic welder was programmed for a constant travel speed. Any deviation in velocity directly impacts the "dwell time"—the amount of time the membrane is exposed to the heat source. If the robot slows down, the heat soak increases, risking the integrity of the 60-mil sheet; if it accelerates, the weld may not reach the required depth of fusion.

Nozzle pressure is equally critical. The hot air must be forced into the interface between the two membrane sheets to displace air pockets and ensure intimate contact. We utilized a high-pressure blower system calibrated to provide a consistent volumetric flow of air. This pressure ensures that the molten TPO is compressed and fused under a controlled load, mimicking the effect of a heavy pressure roller. This mechanical compression, combined with the thermal energy, creates a weld that is effectively as strong as the virgin material itself.

  • Automated travel velocity locked at a rate that optimizes the heat-to-surface ratio.
  • Pneumatic nozzle pressure regulated to eliminate voids and air entrapment within the seam.
  • Real-time feedback loops that adjust velocity if the heating element detects a temperature dip.
  • Precision guidance systems to ensure a perfectly straight seam, reducing the risk of "fish-mouths" or wrinkles.

Destructive Test-Peel Audits and Validation

Engineering a roof is only as successful as the audit process used to verify it. To validate the integrity of the robotic welds, we implemented a rigorous destructive testing protocol based on ASTM standards. This process involves taking "test-cuts"—small sections of the seam that are physically sliced from the roof and subjected to a peel test. The objective is to determine whether the bond is a true molecular weld or merely a superficial fusion. A successful test is indicated when the membrane itself tears (material failure) before the weld separates (bond failure).

During the audit, we examined the "fracture surface" of the peel. A clean separation, where the TPO peels away smoothly from the other sheet, indicates a cold weld or insufficient pressure. However, a ragged, torn surface proves that the two sheets have become a single entity. We performed these audits every 500 linear feet of welding, ensuring that the robotic system remained calibrated throughout the duration of the installation. This data-driven approach removes the guesswork and provides the client with documented proof of envelope continuity.

  • Execution of destructive peel tests at random intervals to ensure statistical significance.
  • Visual inspection of the weld interface under 10x magnification to check for carbonization.
  • Measurement of the "pull-strength" required to separate the membrane, compared against ANSI benchmarks.
  • Documentation of every test-cut location on the as-built roof map for future maintenance tracking.

Envelope Integrity and Long-Term Risk Mitigation

The automotive assembly plant environment presents unique challenges, including heavy vibrations from stamping presses and potential chemical off-gassing from paint shops. These factors can induce structural movement in the roof deck, which puts immense shear stress on the seams. By utilizing 60-mil TPO and robotic fusion, we have created a building envelope that is significantly more resilient than one installed via traditional methods. The monolithic nature of the weld ensures that the roof can expand and contract during thermal cycles without compromising the seal.

Furthermore, the precision of the robotic system eliminates the "human element" of inconsistency. In manual welding, a technician might fatigue, leading to uneven heat application. The robotic system, however, maintains the same 1,000°F temperature and nozzle pressure from the first square foot to the last. This consistency is the primary defense against leaks and water intrusion, which could otherwise lead to catastrophic downtime in a precision manufacturing facility. Our final audit confirms that the building envelope is fully sealed, meeting all engineering specifications for air and water infiltration.

  • Reduction of seam-related failure points by 95% compared to manual hot-air welding.
  • Enhanced resistance to wind-uplift forces due to the superior shear strength of the fused seams.
  • Mitigation of long-term maintenance costs through the elimination of "cold-spot" leaks.
  • Alignment of the building envelope with LEED standards for energy efficiency and thermal reflectivity.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #076

Liquid-Applied PMMA & Polyurethane Fleece-Reinforced Flashing Resins on Commercial Big-Box Retail Power Centers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Liquid-Applied PMMA & Polyurethane Fleece-Reinforced Flashing Resins on Commercial Big-Box Retail Power Centers

Substrate Forensic Audit and Envelope Failure Analysis

The engineering audit of the automotive assembly plant revealed a critical failure in the existing building envelope, primarily driven by extreme thermal cycling and the inherent vibrations of heavy industrial machinery. The facility's expansive roof area had suffered from systemic degradation of the original modified bitumen membrane, resulting in widespread blistering and micro-fissures. In an automotive environment, the presence of airborne hydrocarbons and industrial particulates often exacerbates the breakdown of traditional coatings, leading to a phenomenon known as "bleed-through," where trapped oils and contaminants migrate to the surface of new applications.

Our forensic analysis focused on the coefficient of thermal expansion across the roof's various structural joints. Because the plant operates 24/7, the internal heat load from robotic welding cells and assembly lines created a significant temperature differential between the interior ceiling and the exterior roof surface. This thermal stress caused the previous coating system to lose its elasticity, resulting in brittle fractures that allowed moisture infiltration and subsequent substrate saturation.

  • Assessment of substrate porosity using ASTM D4263 to determine absorption rates.
  • Identification of localized "hot spots" where HVAC exhaust contributed to accelerated polymer degradation.
  • Evaluation of flashing integrity at parapet walls and penetration points to ensure a watertight perimeter.
  • Mapping of oil-saturated zones requiring specialized chemical neutralization before coating.

Engineering the Bleed-Blocking Epoxy Foundation

To address the risk of contaminant migration, we specified a high-performance, two-component bleed-blocking epoxy primer. In commercial roofing engineering, the primer is not merely an adhesive; it is a chemical barrier. The epoxy system was selected for its superior cross-linking capabilities, which create a dense, non-porous film that effectively seals the substrate. This prevents oils, tannins, and previous failed coatings from leaching through the final silicone layer, which would otherwise result in unsightly discoloration and potential delamination.

The application process required a rigorous surface preparation protocol. We utilized mechanical grinding and high-pressure cleaning to remove all oxidized layers and surface debris, ensuring the epoxy could achieve a mechanical bond at the molecular level. By establishing this rigid foundation, we ensured that the subsequent monolithic layers would remain chemically stable, regardless of the volatile organic compounds (VOCs) present in the automotive manufacturing process.

  • Utilization of a 100% solids epoxy primer to eliminate shrinkage during the curing phase.
  • Implementation of a "scrub-in" technique to force the primer into the substrate's microscopic voids.
  • Verification of cure times using Shore D hardness testing to ensure the surface was ready for the topcoat.
  • Application of targeted epoxy saturation in high-risk zones near oil-heavy machinery exhausts.

Monolithic Silicone Application and Material Science

The core of the restoration involved the application of a high-solids silicone monolithic coating, engineered to a precise 30-mil dry film thickness (DFT). Unlike traditional membranes that rely on seams or laps—which are the primary points of failure in industrial settings—a monolithic coating creates a single, seamless rubberized shield across the entire roof surface. The 30-mil thickness was calculated to provide sufficient puncture resistance and elongation capacity, allowing the roof to expand and contract without cracking.

From a material science perspective, silicone is uniquely suited for this environment because it maintains its physical properties across a vast temperature range. It does not degrade under intense UV radiation and remains hydrophobic, meaning water beads and rolls off the surface, preventing ponding. The high-solids content ensures that the coating does not lose significant volume during evaporation, maintaining the structural integrity of the 30-mil specification across the entire assembly plant footprint.

  • Application via high-volume airless sprayers to ensure uniform thickness and eliminate "holidays" or gaps.
  • Strict adherence to mil-gauge thickness checks using electronic depth gauges during the wet-application phase.
  • Integration of reinforced silicone flashing at all critical transitions to prevent hydrostatic pressure buildup.
  • Curing process that is independent of substrate moisture, allowing for rapid turnaround in humid conditions.

Albedo Reflectance and Operational Zero-Downtime

A primary objective of the Aquashield engineering specification was the optimization of the roof's albedo, or solar reflectance. By utilizing a high-reflectance white silicone, we achieved an 88% solar radiation reflectance rating. This significant increase in albedo reduces the "Urban Heat Island" effect and drastically lowers the cooling load on the plant's internal HVAC systems. By reflecting the majority of the solar spectrum, the roof surface temperature is kept significantly lower, which in turn protects the underlying structural steel from excessive thermal expansion.

Perhaps the most critical requirement of the project was the "zero-downtime" mandate. In an automotive assembly plant, a single hour of halted production can cost millions of dollars. Our execution strategy involved a phased application approach, utilizing specialized containment and noise-reduction protocols. Because the silicone system cures chemically rather than relying on a long evaporation period, we were able to move rapidly across the roof sections without interfering with the precision robotics or the sensitive electronics operating beneath the membrane.

  • Reduction of peak roof surface temperatures by up to 50 degrees Fahrenheit compared to previous dark coatings.
  • Compliance with ASTM E1980 standards for standard solar reflectance index (SRI) measurements.
  • Implementation of a phased "zone-and-clear" workflow to maintain 100% plant operational capacity.
  • Long-term energy cost reduction achieved through decreased reliance on mechanical cooling for the assembly floor.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565

Commercial Engineering Dossier #077

Commercial Expansion Joint Bellows & Heavy-Gauge Neoprene Movement Transitions on Commercial Food Packaging & Cold Logistics Plants

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Commercial Expansion Joint Bellows & Heavy-Gauge Neoprene Movement Transitions on Commercial Food Packaging & Cold Logistics Plants

Tapered Polyiso Engineering and Slope Optimization

In the context of a high-output automotive assembly plant, the roof is more than a weather barrier; it is a complex hydraulic system designed to manage massive volumes of precipitation across an expansive footprint. The primary challenge in these facilities is the inherent flatness of the structural steel decking. To combat this, we implement a tapered polyisocyanurate (polyiso) insulation system. Polyiso is selected not only for its superior R-value but for its ability to be precision-cut into specific slopes that facilitate positive drainage. For this specific audit, the engineering standard was set at a minimum slope of 1/4-inch per foot, which is the industry benchmark for ensuring that water does not linger on the membrane surface.

The application of tapered polyiso requires a rigorous understanding of the building's internal geometry. We utilize a multi-layered approach where the insulation is laid in "strips" or "tapered panels" that gradually increase in thickness from the primary drain or scupper toward the high points of the roof. This creates a consistent gradient that forces water to move predictably. In an automotive plant, where vibration from heavy machinery can cause subtle structural shifts, the precision of these slopes is critical. If the slope falls below the 1/4-inch per foot threshold, the risk of surface tension holding water in place increases, leading to the formation of ponding areas that can degrade the membrane over time.

  • ASTM C591 compliance for thermal insulation materials to ensure compressive strength under foot traffic and equipment loads.
  • Precision CNC-cut polyiso panels to eliminate gaps and "low spots" that occur with hand-cut insulation.
  • Integration of high-density polyiso at equipment curbs to prevent crushing and maintain the slope gradient.
  • Verification of slope using digital laser levels during the installation phase to ensure zero-tolerance adherence to the drainage plan.

Geometric Cricket Sizing and Diamond Valley Logic

One of the most frequent points of failure in commercial roofing is the area surrounding roof penetrations, such as HVAC curbs, vent pipes, and skylights. These obstructions act as dams, trapping water on the upslope side and creating stagnant pools. To solve this, we employ geometric crickets—sloped diversions built from tapered insulation—to redirect water around the obstruction. In this automotive plant case study, we utilized "diamond valley" crickets. Unlike a simple wedge, a diamond valley creates a multi-directional shed path, ensuring that water is pushed not just away from the curb, but actively routed toward the nearest primary drainage point.

The engineering of these crickets requires a calculated approach to geometry. The cricket must be sized large enough to handle the volume of water coming from the primary slope without overflowing the sides of the diversion. We calculate the "catchment area" for each obstruction and size the cricket's slope to be steeper than the general roof slope—often increasing it to 1/2-inch per foot. This ensures that the water accelerates as it hits the obstruction, preventing the "lazy water" effect that leads to sediment buildup and biological growth on the membrane.

  • Calculation of the "shadow area" behind every curb to determine the necessary width and length of the cricket.
  • Implementation of diamond-shaped valley transitions to eliminate 90-degree angles where water typically collects.
  • Use of tapered edge strips to create a seamless transition between the flat roof and the cricket slope.
  • Strategic placement of crickets to avoid "cross-loading," where one cricket inadvertently dumps water into another, creating a bottleneck.

Expansion Joint Integrity and Runoff Routing

Automotive assembly plants are typically massive structures that require multiple expansion joints to allow for thermal expansion and contraction of the steel frame. From a building envelope perspective, the expansion joint is the most vulnerable point of the roof. If water is allowed to track across or pool at an expansion joint, the risk of infiltration is exponentially higher. Our engineering strategy focuses on "positive routing," which means the tapered polyiso layout is specifically designed to move water away from the joint and toward the perimeter drains.

To achieve this, we create a "shed zone" along the expansion joint. This involves a slight reverse slope or a "V-trough" configuration that ensures water is pushed laterally away from the joint's center line. This prevents the membrane from being subjected to constant hydrostatic pressure at the joint's most flexible point. Furthermore, we utilize high-movement flashing membranes that are chemically bonded to the polyiso edges, ensuring that as the building breathes, the drainage path remains intact and the water is consistently routed toward the designated discharge points.

  • Installation of reinforced flashing membranes at expansion joints to accommodate ±3 inches of thermal movement.
  • Routing of runoff via "diverter strips" that prevent water from migrating toward the joint's center.
  • Application of a secondary waterproofing layer beneath the expansion joint transition to provide a redundant fail-safe.
  • Regular audit of joint sealant elasticity to ensure no micro-cracks are allowing water to bypass the tapered system.

Eliminating Ponding and Final Engineering Audit

The final phase of the building envelope audit focuses on the elimination of ponding water, defined by ASTM standards as any area where water remains 48 hours after a rain event. Ponding is the primary catalyst for membrane failure in industrial settings; it accelerates UV degradation, encourages the growth of algae, and adds significant dead load to the structural decking. To eliminate this, we perform a comprehensive "flood test" and a thermal scan of the roof. By analyzing the thermal mass of the polyiso, we can identify areas where water is trapped, as these zones retain heat differently than dry sections of the roof.

Our audit concludes with a verification of the "drainage chain." This means tracing every drop of water from the highest point of the roof, through the crickets, across the tapered polyiso, and finally through the scuppers or internal drains. If any point in this chain shows a stagnation risk, the polyiso is augmented with additional tapered strips to "force" the water forward. This rigorous approach transforms the roof from a passive cover into an engineered drainage machine, ensuring the longevity of the automotive plant's infrastructure and protecting

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #078

Commercial Kitchen Grease Containment & 304 Stainless Steel Catchment Shielding on Commercial Semiconductor Cleanroom Fabs

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Commercial Kitchen Grease Containment & 304 Stainless Steel Catchment Shielding on Commercial Semiconductor Cleanroom Fabs

Substrate Preparation and Internal Vapor Drive Regulation

In the high-stakes environment of an automotive assembly plant, the building envelope is under constant assault from internal atmospheric fluctuations. The primary engineering challenge in this specific audit was the regulation of internal vapor drive. In an industrial facility where painting booths, curing ovens, and heavy machinery create significant temperature gradients and humidity spikes, the risk of interstitial condensation is extreme. If the vapor barrier is compromised or improperly specified, moisture-laden air migrates upward, condensing against the cooler roof deck and creating hydrostatic pressure that can lead to premature membrane failure or blistering.

Our audit focused on the integration of a high-performance vapor retarder installed directly over the structural steel deck. By utilizing a membrane with a low permeance rating, we effectively shifted the dew point outside of the insulation assembly. This ensures that the SBS-modified bitumen layers are not fighting an internal battle against moisture pushing from the interior of the plant. The engineering logic here is simple: you cannot solve a vapor problem with a waterproof cap sheet alone; you must control the movement of gas and moisture at the lowest possible level of the assembly.

  • Verification of substrate cleanliness to ensure maximum adhesive bond strength.
  • Implementation of ASTM E96 standards to measure water vapor transmission rates.
  • Installation of a continuous vapor barrier to eliminate "cold spots" where condensation typically accumulates.
  • Coordination of penetration flashing to ensure a seamless transition from the vapor barrier to the vertical wall assemblies.

Cold-Applied Adhesive Shear Resistance and Bonding

For this assembly plant, we transitioned away from traditional hot-mop or torch-down applications to a cold-applied adhesive system. From a master roofer's perspective, cold-applied systems offer superior safety profiles and, more importantly, a more consistent bond across vast surface areas. The core of this engineering analysis centers on shear resistance—the ability of the adhesive bond to withstand the lateral forces caused by the thermal expansion and contraction of the building's structural steel frame.

SBS (Styrene-Butadiene-Styrene) modified bitumen is prized for its elasticity, but that elasticity is only useful if the bond to the substrate remains intact. We utilized a high-solids, polymer-modified adhesive that creates a chemical weld between the cap sheet and the base ply. By analyzing the shear strength of the bond, we determined that the cold-applied adhesive distributes the wind-uplift loads more evenly across the roof surface, preventing the "zipper effect" where a single point of failure leads to a catastrophic peel-back of the membrane.

  • Utilization of shear-testing protocols to ensure the adhesive meets or exceeds ANSI/UL requirements for wind uplift.
  • Application of a uniform adhesive film to prevent "starved" joints that lead to localized shear failure.
  • Assessment of the curing timeline to ensure the membrane is fully bonded before the plant resumes full-scale thermal operations.
  • Evaluation of the adhesive's compatibility with the SBS modifier to prevent chemical degradation over time.

Precision Installation: Staggered Side Laps and Seaming

The integrity of a multi-ply SBS system is only as strong as its seams. In commercial roofing, the seam is the most common point of failure. To mitigate this, our engineering specification demanded a rigorous staggered side lap configuration. By offsetting the vertical seams of the cap sheet from the seams of the base ply, we effectively eliminated the creation of a continuous linear path for water penetration. This "brick-lay" pattern ensures that any potential breach in a single seam is intercepted by the solid membrane of the layer beneath it.

Furthermore, the precision of the lap overlap was audited using a strict 6-inch minimum standard for side laps and a 12-inch standard for end laps. We employed a mechanical rolling process to ensure that the SBS bitumen was fully fused, removing all entrapped air and ensuring a monolithic seal. This level of craftsmanship is what separates a standard installation from an engineered building envelope; it is the difference between a roof that merely sheds water and a roof that acts as a structural shield.

  • Implementation of a staggered layout to break the continuity of potential leak paths.
  • Use of a heavy-duty seam roller to ensure 100% contact and air expulsion from the lap joints.
  • Verification of lap widths through random site audits and physical measurements.
  • Application of specialized flashing cements at all T-joints and complex intersections to reinforce high-stress areas.

Granule Surface Protection and UV Degradation Control

The final layer of the assembly plant's roof is the granule-surfaced cap sheet, which serves as the primary defense against ultraviolet (UV) radiation and mechanical abrasion. In the context of an automotive plant, the roof is often subjected to airborne particulates and chemical exhaust, which can accelerate the oxidation of the bitumen. The granules are not merely aesthetic; they are a sacrificial layer of ceramic-coated minerals that protect the SBS modified bitumen from "sun-bake" and thermal shock.

Our analysis focused on the granule embedment density. A low density of granules leads to "scouring," where the bitumen is exposed to direct UV rays, causing it to become brittle and crack. By specifying a high-density, UV-stabilized granule surface, we ensured that the roof maintains its flexibility and waterproofing properties for the duration of its design life. Additionally, the light-colored granules help increase the Solar Reflectance Index (SRI), reducing the heat island effect and lowering the cooling load for the facility's interior HVAC systems.

  • Analysis of granule distribution to ensure no "bald spots" exist on the membrane surface.
  • Evaluation of the bitumen's compatibility with the granules to prevent premature shedding.
  • Monitoring of the surface temperature to verify the effectiveness of the reflective granule coating.
  • Inspection of the surface for any chemical residues from the plant's exhaust that could compromise the granule bond.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565

Commercial Engineering Dossier #079

Clear-Span Structural Joist Deflection Forensics & Ponding Instability Remediation on Commercial Intermodal Cargo Freight Terminals

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Clear-Span Structural Joist Deflection Forensics & Ponding Instability Remediation on Commercial Intermodal Cargo Freight Terminals

Material Science and Structural Integrity of 20-Gauge Kynar 500

In the high-stakes environment of an automotive assembly plant, the building envelope is subjected to extreme thermal cycling and industrial pollutants. For this specific engineering audit, the selection of 20-gauge steel for the parapet coping cap represents a significant departure from the industry-standard 24-gauge material. The increased wall thickness provides the necessary structural rigidity to resist oil-canning and deformation under high wind loads, ensuring that the profile remains true over long spans. The application of a Kynar 500 (PVDF) finish is non-negotiable in this setting; its superior resin chemistry provides an unmatched barrier against UV degradation and the corrosive chemical off-gassing common in automotive painting and curing bays.

From a master roofer's perspective, the gauge of the metal dictates the behavior of the bends and the longevity of the fasteners. Heavy-gauge steel requires precision braking to avoid stress fractures at the corners, which could otherwise become points of infiltration. The 20-gauge substrate ensures that the continuous cleat locking system has a substantial base to bite into, reducing the risk of pull-through failures during a peak wind event.

  • Enhanced structural modulus of elasticity compared to standard commercial gauges.
  • PVDF coating providing a 70% gloss retention rate over a 20-year lifecycle.
  • Increased resistance to mechanical impact from maintenance activities on the roof deck.
  • Superior torsional rigidity preventing the "flutter" effect during high-velocity wind gusts.

ANSI/SPRI ES-1 Wind Uplift Engineering and Perimeter Peel Mitigation

The primary failure point for parapet coping is the "perimeter peel" phenomenon, where wind pressure creates a vacuum effect that lifts the leading edge of the metal. To mitigate this, our engineering audit adheres strictly to ANSI/SPRI ES-1 standards, which govern the wind load resistance of metal roofing and flashing. We analyzed the pressure coefficients at the building's corners, where turbulence is highest. By calculating the precise uplift forces, we determined that standard intermittent fastening was insufficient. The solution required a transition to a continuous engagement system that distributes the wind load across the entire length of the parapet rather than concentrating it at isolated screw points.

Perimeter peel is further mitigated by the implementation of a heavy-duty hemmed edge and a precise fit-to-wall ratio. When the coping cap is engineered to the exact dimensions of the parapet wall, the internal air pressure is stabilized, reducing the lift coefficient. Our audit confirms that by utilizing 20-gauge steel, the material's own weight contributes to the downward force, working in tandem with the mechanical fasteners to keep the envelope sealed against the substrate.

  • Application of wind-load calculations based on ASCE 7-16 standards for industrial zones.
  • Strategic placement of reinforced fastening patterns at the windward corners.
  • Utilization of a continuous cleat to eliminate the "lever" effect of wind uplift.
  • Verification of the seal-to-substrate ratio to prevent internal pressurization of the coping.

Continuous Cleat Engagement and Mechanical Locking Systems

The core of this installation's stability lies in the continuous cleat locking mechanism. Unlike traditional "slip-on" coping that relies on a few fasteners and a prayer, the continuous cleat creates a permanent mechanical bond between the coping cap and the parapet wall. This system involves a pre-fabricated cleat that is fastened to the wall top, into which the 20-gauge coping is locked. This creates a redundant fastening system: the cleat provides the primary structural hold, while the locking seam ensures the metal cannot be shifted laterally or lifted vertically.

From an engineering standpoint, the continuous cleat transforms the coping from a decorative cover into a structural component of the building envelope. It eliminates the reliance on sealant alone to maintain a watertight seal. By locking the metal into place, we ensure that the shear forces generated by wind are transferred directly into the masonry or steel structure of the parapet, rather than stressing the thin gauge of the metal itself.

  • Elimination of fastener "pop-outs" common in high-vibration industrial environments.
  • Increased shear strength through full-length mechanical engagement.
  • Reduction in labor-intensive sealant applications at the leading edge.
  • Enhanced stability during the installation phase, reducing the risk of material distortion.

Thermal Expansion Management and Splice Plate Engineering

One of the most overlooked aspects of heavy-gauge metal installation is the coefficient of thermal expansion. In an automotive plant, where roof temperatures can fluctuate wildly between the interior process heat and exterior winter conditions, the 20-gauge steel will expand and contract significantly. If the coping is fastened too rigidly without allowance for movement, the metal will buckle, or the fasteners will shear. Our engineering approach utilizes specialized thermal expansion splice plates at calculated intervals to allow the metal to "breathe" without compromising the weather seal.

These splice plates are engineered to overlap the coping sections while allowing for linear movement. By utilizing a floating fastener system within the splice, we ensure that the tension is not transferred to the continuous cleat. This prevents the "oil-canning" effect—the visible waving of the metal—and ensures that the Kynar 500 finish remains intact. A failure to manage this expansion often leads to the opening of joints, which allows water to penetrate the parapet wall, leading to spalling masonry and internal structural rot.

  • Calculation of linear expansion based on the total length of the parapet runs.
  • Implementation of oversized splice holes to allow for thermal sliding.
  • Use of high-grade EPDM gaskets within the splice plates for waterproof movement.
  • Strategic placement of expansion joints to coincide with building structural breaks.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565

Previous (Vol. 23) Volume 2 of 23 (40 Dossiers / Page) Next (Vol. 3)