Aquashield Corporate Shield Logo

AQUASHIELD CORPORATE

Commercial Flat Roofing & Industrial Facility Engineering

A comprehensive technical compendium on commercial 60-mil TPO single-ply systems, high-solids silicone restorative coatings, and building envelope preservation. Volume 7 of 23.

Previous (Vol. 6) Volume 7 of 23 (40 Dossiers / Page) Next (Vol. 8)
Commercial Engineering Dossier #240

Non-Destructive Substrate Moisture Scans on Commercial Logistics Distribution Hubs
Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Non-Destructive Substrate Moisture Scans on Commercial Logistics Distribution Hubs

The Engineering Challenge of Large-Scale Logistics Hubs

In the realm of commercial building envelope engineering, logistics distribution hubs present a unique set of challenges due to their immense footprints and the critical nature of their internal operations. When managing a facility exceeding 500,000 square feet, the building envelope is not merely a cover but a complex system that must manage thermal expansion, contraction, and hydrostatic pressure. The primary risk in these structures is the undetected infiltration of moisture through compromised flashing, failing seams, or puncture wounds in the membrane. Because these facilities often utilize high-bay racking and automated sorting systems, a localized leak can quickly evolve into a systemic failure of the roof insulation, leading to subsurface saturation that remains invisible to the naked eye.

A standard visual inspection is fundamentally insufficient for a facility of this scale. Water rarely travels in a straight line; it follows the path of least resistance, often migrating horizontally across the substrate before pooling in low spots or accumulating around structural columns. This phenomenon, known as capillary action, means that the point of entry is rarely the point of saturation. To accurately assess the health of the building envelope, we must shift from a reactive "leak-patch" mentality to a proactive engineering audit that treats the roof as a singular, integrated moisture barrier.

  • Identification of thermal bridging points where moisture typically accumulates.
  • Analysis of structural deflection and ponding water patterns.
  • Evaluation of the interface between the roof membrane and parapet wall flashing.
  • Assessment of the vapor retarder's integrity to prevent interstitial condensation.

Non-Destructive Moisture Detection Methodologies

To establish a precise map of subsurface saturation, we employ Non-Destructive Moisture Detection (NDMD). The cornerstone of this process is Infrared Thermography (IRT), which allows us to visualize the thermal mass of the roof. Water has a significantly higher heat capacity than polyisocyanurate (polyiso) or gypsum board. By scanning the roof during a period of thermal transition—typically during the cooling phase of the evening or the heating phase of the morning—we can identify "hot" or "cold" spots that indicate trapped moisture. These thermal anomalies serve as the primary indicators of subsurface saturation boundaries.

However, thermography provides a relative map, not a quantitative measurement. To refine these findings, we utilize electronic moisture meters that measure the dielectric constant of the substrate. By introducing a controlled electrical current into the insulation, we can determine the conductivity of the material. Since water is a highly conductive medium compared to dry insulation, the meter provides a numerical value that correlates to the moisture percentage. This dual-method approach ensures that we are not chasing "ghost" readings caused by varying insulation densities or structural steel components beneath the deck.

  • Utilization of high-resolution FLIR cameras for wide-area thermal mapping.
  • Application of dielectric constant probes for point-specific moisture verification.
  • Correlation of thermal anomalies with known structural blueprints to rule out false positives.
  • Establishment of a "saturation grid" to track moisture migration over time.

Validating Saturation Boundaries via Core Analysis

While NDMD provides the map, the engineering audit requires physical validation to meet ASTM standards for material science. We transition from non-destructive to destructive testing through strategic core sampling. By extracting cylindrical sections of the entire roof assembly—including the membrane, insulation layers, and the top of the deck—we can perform a gravimetric analysis. This involves weighing the core sample, drying it in a controlled oven, and re-weighing it to determine the exact percentage of water weight relative to the dry mass of the insulation.

The critical threshold for "wet" insulation in a commercial logistics hub is typically established at 30% of the material's original volume or a specific weight gain threshold defined by the manufacturer. When a core sample exceeds this limit, the insulation is considered compromised. Saturated insulation loses its R-value, providing a pathway for heat loss and creating a breeding ground for mold and structural corrosion on the steel deck. By cross-referencing the core sample data with the IRT map, we can mathematically define the saturation boundary, ensuring that the remediation phase is based on empirical data rather than estimation.

  • Execution of core sampling at the center, perimeter, and edge of identified thermal anomalies.
  • Application of gravimetric drying methods to determine precise moisture content.
  • Analysis of the "wicking" effect where moisture travels upward from the deck.
  • Verification of the substrate's pH levels to check for corrosive reactions on the metal deck.

Surgical Excision and Remediation Strategy

Once the saturation boundaries are validated, the objective shifts to surgical wet insulation excision. The traditional industry approach of "rip and replace" for the entire roof section is economically inefficient and creates unnecessary landfill waste. Instead, we employ a surgical approach, removing only the insulation that has exceeded the moisture threshold. This process begins by cutting the membrane along the precisely mapped saturation boundary, ensuring a 24-inch overlap into the "dry" zone to account for any peripheral capillary migration.

After the saturated insulation is removed, the steel deck must be mechanically cleaned and treated with a rust-inhibiting primer if oxidation is present. The remediation is completed by installing new, high-density polyiso insulation, carefully staggered to prevent vertical seams that could act as conduits for future leaks. The final membrane seal is executed using reinforced flashing and heat-welded seams, restoring the building envelope to its original engineered specifications. This surgical method preserves the integrity of the surrounding dry system while eliminating the risk of trapped moisture causing long-term structural degradation.

  • Precision cutting of the membrane based on the validated saturation grid.
  • Mechanical removal of saturated insulation layers to expose the structural deck.
  • Application of industrial-grade corrosion inhibitors to the steel substrate.
  • Installation of new insulation with a focus on tight joints and staggered seams to maintain thermal continuity.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #241

Sub-Zero Cold Storage Downward Vapor Drive & Self-Adhered SBS Barriers on Commercial Automotive Assembly Plants

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Sub-Zero Cold Storage Downward Vapor Drive & Self-Adhered SBS Barriers on Commercial Automotive Assembly Plants

The Physics of Inverted Thermal Envelopes and Downward Vapor Drive

In the specialized environment of a commercial automotive assembly plant, particularly within sub-zero cold storage zones, the building envelope must be engineered to counteract a phenomenon known as inverted vapor drive. In standard commercial construction, vapor typically migrates from the warm interior to the cold exterior. However, when a facility maintains internal temperatures well below freezing, the thermal gradient is reversed. The exterior ambient air, even in winter, is often warmer and more humid than the conditioned interior, creating a powerful pressure differential that drives moisture from the outside in.

This downward vapor drive puts immense pressure on the roof assembly. If the vapor barrier is improperly placed or suffers from punctures, water vapor penetrates the insulation layers and migrates toward the cold interior. Once this vapor reaches a surface that is below its dew point, it undergoes a phase change from gas to liquid. In a sub-zero automotive facility, this often results in interstitial condensation, where moisture traps itself between the roof deck and the insulation, leading to hidden corrosion of structural steel and the eventual degradation of the thermal assembly.

  • Hygrothermal Pressure: The force driving moisture through porous materials based on temperature and humidity gradients.
  • Inverted Gradient: A condition where the interior is colder than the exterior, reversing standard moisture flow.
  • Vapor Permeance: The rate at which water vapor passes through a specific material, measured in perms.
  • Atmospheric Loading: The impact of external weather fluctuations on the stability of the internal cold-chain environment.

Dew Point Migration Control and Interstitial Condensation

Controlling the dew point is the primary objective of any high-performance building envelope audit. The dew point is the exact temperature at which air becomes saturated and moisture begins to condense. In a sub-zero assembly plant, the goal is to ensure that the dew point occurs within a controlled, non-destructive layer of the assembly, rather than on the structural roof deck or within the insulation voids. When the thermal envelope is improperly sequenced, the dew point often migrates to the underside of the metal decking, causing "roof rain" where condensate drips onto sensitive automotive components and machinery.

To mitigate this, we employ a strategy of continuous thermal wrapping. By shifting the dew point toward the exterior of the assembly, we ensure that any condensation that does occur is managed by the primary drainage system rather than being trapped within the building's skeleton. This requires a rigorous application of material science, ensuring that the transition from the roof to the wall—the critical "envelope break"—is seamless. Any gap in the thermal continuity creates a thermal bridge, which acts as a vacuum for moisture, accelerating the localized failure of the roofing system.

  • Thermal Bridging: The process where heat bypasses insulation via highly conductive materials like steel fasteners or beams.
  • Phase Change Management: Engineering the assembly to prevent water vapor from turning into liquid in critical structural zones.
  • ASTM C1128: Adherence to standards regarding the thermal transmittance of insulation materials.
  • Interstitial Space: The gap between the structural deck and the finish membrane where moisture typically accumulates.

Engineering Self-Adhered SBS Barriers for Air-Tight Integrity

For automotive plants with extreme temperature swings, the selection of a Self-Adhered SBS (Styrene-Butadiene-Styrene) modified bitumen membrane is a technical necessity. Unlike traditional torch-down or cold-applied liquids, self-adhered SBS provides a consistent, factory-controlled thickness and a high-strength bond to the substrate. The SBS modification allows the membrane to remain flexible at sub-zero temperatures, preventing the brittle cracking that often plagues standard asphaltic membranes when the building undergoes thermal contraction and expansion.

The primary function of the SBS barrier in this application is to serve as a redundant air and vapor seal. By utilizing a self-adhered system, we eliminate the risk of "human error" associated with torching or mopping, ensuring that every square inch of the roof deck is encapsulated. This creates an airtight seal that resists the downward vapor drive, forcing the moisture to remain outside the thermal envelope. Furthermore, the high elongation properties of SBS allow the membrane to move with the structural steel of the assembly plant without compromising the integrity of the vapor seal.

  • SBS Modification: The addition of styrene-butadiene-styrene to bitumen to improve elasticity and low-temperature performance.
  • Full-Monolithic Seal: A continuous, gap-free barrier that prevents air infiltration and exfiltration.
  • Adhesion Strength: The capacity of the membrane to bond to the substrate, preventing the formation of pockets where vapor can collect.
  • ANSI/ASTM Standards: Compliance with rigorous testing for modified bitumen performance in commercial industrial settings.

Staggered Multi-Layer Polyiso and Thermal Bridging Mitigation

The final layer of defense in a sub-zero envelope is the strategic installation of polyisocyanurate (Polyiso) insulation. To achieve the required R-value while preventing vapor "shortcuts," we implement a staggered, multi-layer installation. If insulation boards are stacked with aligned seams, those seams become linear paths of least resistance for vapor drive. By staggering the joints in a brick-lay pattern, we force the vapor to travel a longer, more tortuous path, effectively increasing the thermal resistance of the assembly and reducing the likelihood of localized condensation.

This staggered approach is critical when dealing with the high-density loads of an automotive plant. We utilize high-density Polyiso to provide the necessary compressive strength to withstand the structural stresses of the roof. By combining this with the self-adhered SBS barrier, we create a composite system that manages both the thermal load and the moisture drive. The result is a building envelope that maintains a stable internal environment, protects the structural integrity of the facility, and significantly reduces the energy expenditure required to maintain sub-zero temperatures.

  • Polyisocyanurate (Polyiso): A closed-cell foam insulation known for its high R-value per inch.
  • Brick-Lay Pattern: The method of offsetting insulation joints to eliminate continuous vertical or horizontal seams.
  • R-Value Optimization: Maximizing the thermal resistance to prevent heat gain from the exterior.
  • Compressive Strength: The ability of the insulation to withstand the weight of the roofing system and maintenance traffic without collapsing.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #242

Structural Deck Fastener Pull-Out Testing on 22-Gauge Corrugated Steel Decks on Commercial Mission-Critical Data Centers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Structural Deck Fastener Pull-Out Testing on 22-Gauge Corrugated Steel Decks on Commercial Mission-Critical Data Centers

Substrate Integrity and the Mission-Critical Envelope

In the realm of mission-critical data centers, the building envelope is not merely a weather barrier; it is the first line of defense for millions of dollars of sensitive server infrastructure. When auditing a facility of this magnitude, the structural deck—specifically 22-gauge corrugated steel—serves as the foundational diaphragm for the entire roofing system. The integrity of this substrate determines the ultimate success of the wind-uplift resistance and the long-term stability of the membrane. In a data center, where equipment vibrations and heavy HVAC rooftop units are common, the fastener-to-deck connection is the most frequent point of systemic failure.

A 22-gauge steel deck provides significant structural rigidity, but its corrugated profile introduces complex geometries that can compromise fastener engagement if not properly managed. The depth of the flute and the thickness of the steel must be precisely matched to the fastener length and thread pitch. If a fastener is over-driven, it can distort the steel web, creating a "bell-mouth" effect that reduces the effective grip. Conversely, under-driven fasteners fail to achieve the necessary compression, leading to premature withdrawal under wind-load stress.

  • Evaluation of gauge consistency across the entire roof plane to ensure no thinning occurred during the milling process.
  • Assessment of the corrugated profile depth to verify compatibility with specified heavy-duty fasteners.
  • Analysis of the deck's load-bearing capacity relative to the weight of high-efficiency cooling towers and generators.
  • Verification of the structural diaphragm's alignment with the building's primary steel frame.

Methodology for Calibrated Mechanical Pull Testing

To move beyond theoretical calculations, we employ calibrated mechanical pull testing to determine the actual in-place withdrawal resistance of the fasteners. This process involves the use of a digital force gauge and a specialized pull-tester that applies a controlled, linear axial load to the fastener head. The goal is to identify the "ultimate load" at which the fastener either pulls completely out of the substrate or the steel deck itself undergoes plastic deformation. This empirical data is the only way to validate that the installation meets the engineering specifications required for high-wind zones.

The testing protocol follows a rigorous sampling pattern, focusing heavily on the perimeter and corner zones, where wind turbulence creates the highest negative pressure. We do not rely on a handful of random samples; instead, we implement a grid-based audit. Each test is performed perpendicular to the roof surface to avoid introducing shear forces that would skew the results. By documenting the peak force reached before failure, we can establish a safety factor that accounts for material fatigue and environmental degradation over the life of the facility.

  • Utilization of ASTM-compliant calibrated gauges to ensure measurement accuracy within +/- 1% of the total load.
  • Implementation of a "slow-pull" technique to observe the gradual transition from elastic to plastic deformation.
  • Strategic sampling of fasteners located at the roof eaves, parapet walls, and central field areas.
  • Documentation of the failure mode, distinguishing between thread stripping, head shear, and substrate pull-through.

Withdrawal Resistance Thresholds and Corrosion Diagnostics

The minimum withdrawal resistance threshold is the non-negotiable benchmark for a mission-critical facility. For 22-gauge steel, the threshold is calculated based on the required uplift pressure of the specific wind zone, typically incorporating a safety factor of 2.0 or higher. If a fastener fails below the engineered minimum, it indicates a systemic installation error, such as improper drilling or the use of incorrect fasteners. We analyze the "yield point" of the connection to ensure that the fastener remains in the elastic range during peak wind events, preventing permanent deformation of the deck.

Beyond mechanical strength, we conduct a deep-dive into fastener corrosion diagnostics. In data centers, the presence of industrial pollutants or coastal salt air can trigger galvanic corrosion between the fastener and the steel deck. We examine the coating integrity of the fasteners—whether they are hot-dipped galvanized, zinc-plated, or stainless steel—to ensure they are compatible with the deck's metallurgy. Any sign of "red rust" or white oxidation at the penetration point suggests a breach in the protective coating, which can lead to a rapid loss of cross-sectional area and a subsequent drop in withdrawal resistance.

  • Comparison of field-tested pull-out values against the manufacturer's theoretical load tables.
  • Inspection for galvanic incompatibility between the fastener alloy and the 22-gauge steel substrate.
  • Evaluation of the "bite" or thread engagement depth to ensure maximum grip in the steel web.
  • Assessment of the sealing washers to prevent moisture ingress and subsequent crevice corrosion.

Wind-Zone Schedules and Long-Term Envelope Stability

The final phase of the engineering audit involves mapping the pull-test results onto the building's wind-zone schedule. According to ASCE 7 standards, a roof is divided into different zones: the interior field, the perimeter edges, and the corners. The corners experience the most extreme suction forces and therefore require the highest fastener density and the strongest individual withdrawal resistance. Our analysis ensures that the fastener spacing in these "Zone 3" areas is tightened to meet the calculated uplift pressures, preventing the membrane from peeling away from the substrate during a storm event.

Long-term envelope stability is not a static state but a managed process. By establishing a baseline of pull-out strength and corrosion levels, Aquashield Corporate can implement a predictive maintenance schedule. We recommend periodic re-testing of a subset of fasteners every five years to monitor for fatigue. This proactive approach transforms the roof from a passive cover into an engineered system, ensuring that the data center remains operational regardless of external atmospheric conditions. The synergy of high-gauge steel, calibrated fastening, and rigorous auditing creates a fail-safe envelope.

  • Alignment of fastener spacing with the specific wind-load maps provided by the structural engineer of record.
  • Verification of the "edge distance" to ensure fasteners are not placed too close to the deck supports, which could cause splitting.
  • Creation of a permanent record of pull-test values for future facility audits and insurance certifications.
  • Final validation of the membrane-to-fastener bond to ensure the entire assembly acts as a single monolithic unit.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #243

Electronic Vector Mapping (EVM) Low-Voltage Membrane Breach Detection on Commercial Cold Storage Freezer Warehouses

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Electronic Vector Mapping (EVM) Low-Voltage Membrane Breach Detection on Commercial Cold Storage Freezer Warehouses

The Criticality of the Thermal Envelope in Cold Storage Environments

In the realm of commercial building envelope engineering, cold storage freezer warehouses represent the most demanding application of moisture control and thermal resistance. Unlike standard warehouse facilities, a freezer warehouse operates on a massive temperature differential, often maintaining internal environments at -20°F or lower while facing external ambient temperatures that can exceed 90°F. This extreme delta creates a powerful vapor drive, where moisture-laden air from the exterior seeks to migrate toward the interior cold zone. If the roof membrane is compromised, even by a microscopic puncture, the resulting vapor infiltration leads to interstitial condensation within the polyisocyanurate insulation layers.

When moisture enters the insulation, it does not simply sit; it undergoes a freeze-thaw cycle that destroys the R-value of the core material and promotes the growth of mold and mildew. More critically, in deep-freeze applications, this moisture can lead to "heaving" where ice lenses form within the roof assembly, potentially lifting the membrane and creating larger structural failures. Traditional leak detection methods, such as flood testing or infrared thermography, are often insufficient for these assets because they identify the symptom—the wet insulation—rather than the precise point of entry. By the time a thermal camera detects a cold spot, the envelope has already failed, and thousands of dollars in insulation have been compromised.

  • Vapor Drive Dynamics: The constant pressure of water vapor moving from high-concentration exterior zones to low-concentration interior zones.
  • Interstitial Condensation: The phenomenon of moisture condensing inside the wall or roof assembly rather than on the surface.
  • Thermal Bridging: Localized areas of high heat transfer that bypass insulation, often occurring at fasteners or seams.
  • R-Value Degradation: The loss of thermal resistance caused by moisture saturation in the insulation core.

Engineering the Conductive Underlayment Vector Grid

To solve the problem of invisible breaches, Aquashield Corporate utilizes Electronic Vector Mapping (EVM). This system begins with the installation of a specialized conductive underlayment beneath the primary waterproofing membrane. This underlayment is engineered as a conductive vector grid—a precision-laid matrix of low-voltage conductive elements that turn the entire roof surface into a giant electrical sensor. The primary membrane, typically a high-performance TPO or PVC, acts as a dielectric insulator, separating the conductive grid from the external environment. This creates a stable electrical field across the entire roof plane.

The engineering brilliance of the vector grid lies in its ability to maintain a constant, low-voltage current. Because the grid is mapped to a specific coordinate system during installation, every square inch of the roof is assigned a unique electronic address. The system is designed to operate at a voltage low enough to be completely safe for personnel and non-interfering with building electronics, yet sensitive enough to detect the slightest change in electrical resistance. When the dielectric integrity of the top membrane is compromised, the conductive grid reacts to the presence of moisture or the physical breach, altering the electrical signature at that specific coordinate.

  • Dielectric Insulation: The use of the roof membrane as a non-conductive barrier that prevents current flow to the surface.
  • Coordinate Mapping: The process of assigning X and Y axes to the roof surface for pinpoint accuracy.
  • Low-Voltage Current: The application of a steady, non-hazardous electrical flow to monitor the envelope's integrity.
  • Conductive Matrix: The physical grid of copper or conductive polymers that forms the sensing layer.

EVM Diagnostics and Microscopic Pinhole Localization

The true value of Electronic Vector Mapping is realized during the diagnostic phase. Traditional "water scanning" requires the roof to be actively leaking and often involves saturating the roof, which can actually exacerbate the damage. In contrast, EVM is a non-destructive process. Using a high-sensitivity vector analyzer, technicians scan the roof. The device measures the impedance and capacitance of the membrane. When the analyzer passes over a breach—even a pinhole puncture smaller than a needle—it detects a "leakage current" or a change in the electrical field caused by the breach of the dielectric layer.

This process allows for the localization of punctures that are invisible to the naked eye. In a cold storage environment, a pinhole can be catastrophic because it acts as a straw, pulling humid air directly into the insulation. The EVM system triangulates the exact coordinates of the breach by analyzing the vector shift in the conductive grid. Instead of cutting large "exploratory" holes in the roof to find a leak, the master roofer can move directly to the coordinate provided by the mapping software and perform a surgical repair. This precision eliminates the guesswork and prevents the unnecessary disruption of the thermal envelope.

  • Impedance Analysis: Measuring the opposition to current flow to identify where the membrane has been breached.
  • Triangulation: Using the vector grid to narrow down a breach to a specific square inch of the roof.
  • Pinhole Detection: Identifying microscopic punctures that would be missed by visual inspections or flood tests.
  • Surgical Repair: The act of patching a precise location without compromising surrounding membrane integrity.

Non-Destructive Certification and Lifecycle Asset Management

From an engineering and insurance perspective, the ability to certify a roof as "breach-free" without destroying parts of the assembly is a paradigm shift. Aquashield Corporate provides a non-destructive quality certification based on the EVM scan results. This certification serves as a baseline for the building's lifecycle asset management. By performing periodic EVM audits, facility managers can track the degradation of the membrane over time and identify new punctures caused by foot traffic, HVAC maintenance, or wind-borne debris before they lead to systemic insulation failure.

Aligning with ASTM and ANSI standards for building envelope integrity, EVM transforms the roof from a passive shield into an active monitoring system. The long-term ROI is found in the extension of the roof's service life and the preservation of the cold storage facility's energy efficiency. When the thermal envelope is certified as airtight and watertight, the refrigeration compressors work less, energy costs drop, and the risk of catastrophic structural failure due to interstitial ice buildup is virtually eliminated. This is the gold standard of commercial roofing: moving from reactive patching to proactive, data-driven engineering.

  • Baseline Certification: Establishing a documented state of the roof's integrity at the time of completion.
  • Lifecycle Monitoring: Using scheduled EVM scans to detect early-stage wear and tear.
  • Energy Efficiency: Reducing the load on refrigeration systems by eliminating thermal leaks.
  • Asset Preservation: Extending the lifespan of the roof and insulation through precision maintenance.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #244

Liquid-Applied PMMA & Polyurethane Fleece-Reinforced Flashing Resins on Commercial Commercial Fleet Maintenance Hangars

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Liquid-Applied PMMA & Polyurethane Fleece-Reinforced Flashing Resins on Commercial Commercial Fleet Maintenance Hangars

The Engineering Challenge of Fleet Maintenance Hangar Envelopes

From a master roofer's perspective, the commercial fleet maintenance hangar represents one of the most demanding environments for building envelope integrity. These structures are characterized by massive open-span footprints, which inherently lead to significant thermal bridging and extreme coefficients of thermal expansion and contraction. When you are dealing with a roof surface that can fluctuate forty degrees in a single afternoon, the stress placed on traditional membrane seams is immense. Furthermore, the internal environment of a fleet hangar is often contaminated with aerosolized oils, degreasers, and combustion byproducts, all of which can migrate toward the roof deck and compromise traditional adhesives.

A comprehensive engineering audit of these facilities typically reveals that the primary points of failure are not the field membranes, but the transitions. The intersection where the roof deck meets the structural steel, specifically the I-beam stanchions and perimeter parapets, is where water infiltration most frequently occurs. Traditional sheet-goods flashing often fails in these areas because they cannot conform to the complex, multi-planar geometry of heavy industrial steel. To solve this, we shift our focus from mechanical fastening and taped seams to a monolithic, liquid-applied chemical bond that treats the building envelope as a single, continuous skin.

  • Thermal Shock Resistance: The ability of the roofing system to withstand rapid temperature swings without cracking or delaminating.
  • Chemical Compatibility: Ensuring the resin does not react negatively to industrial solvents used in fleet maintenance.
  • Structural Movement: Accommodating the subtle shifting of large-span steel frames during wind events or seismic activity.
  • Vapor Drive: Managing the internal humidity and exhaust fumes that push against the underside of the roof assembly.

Material Science of PMMA and Polyurethane Cold-Applied Resins

The core of the Aquashield approach relies on the advanced polymerization of Polymethyl Methacrylate (PMMA) and high-performance Polyurethane (PU). Unlike traditional bitumen or PVC, PMMA is a cold-applied resin that cures through a chemical reaction rather than the evaporation of solvents. This is critical in a hangar environment where torch-applied systems pose an unacceptable fire risk. The cure kinetics of PMMA are exceptionally rapid; we are talking about a system that can reach full structural cure in as little as 45 to 90 minutes, depending on the ambient temperature and the specific catalyst used. This allows for immediate foot traffic and eliminates the costly downtime associated with traditional curing windows.

While PMMA provides the hardness, UV stability, and rapid cure, the Polyurethane components provide the necessary elasticity. By blending these chemistries or applying them in a layered system, we create a membrane that possesses high tensile strength yet remains flexible enough to bridge hairline cracks in the substrate. This hybrid approach ensures that the roof does not become brittle over time, a common failure point in older epoxy-based systems. The result is a chemically bonded layer that fuses to the substrate at a molecular level, creating a waterproof barrier that is virtually impervious to the elements.

  • Rapid Polymerization: Fast-cure cycles that reduce project timelines and operational disruptions.
  • UV Stability: High resistance to degradation from solar radiation, preventing the "chalking" common in lower-grade resins.
  • Cold-Application: Elimination of open flames or high-heat tools, ensuring safety in volatile industrial zones.
  • Adhesion Profiles: Superior bonding capabilities to galvanized steel, concrete, and existing modified bitumen.

Fleece-Reinforced Embedding and Structural Integration

A liquid resin, no matter how high the quality, is essentially a thin film. To transform this film into a structural membrane capable of withstanding the rigors of a commercial hangar, we employ a fleece-reinforced embedding process. This involves the saturation of a non-woven polyester fleece within the PMMA resin. The fleece acts as the "skeleton" of the roofing system, distributing mechanical loads across a wider area and providing the necessary reinforcement to prevent tear propagation. When the resin is applied, the fleece is embedded into the wet resin and then "over-coated" to lock it into a permanent, monolithic matrix.

This "sandwich" technique is particularly vital when dealing with jointing and lap seams. By embedding the fleece across the transition from the roof deck to the vertical flashing, we eliminate the need for mechanical fasteners that create potential leak paths. The fleece-reinforced PMMA creates a bridge that can accommodate significant movement without rupturing. During our engineering audits, we look for "saturation consistency"—ensuring that there are no dry spots or air pockets within the fleece, as these would represent points of weakness where water could eventually migrate through capillary action.

  • Tensile Distribution: Using polyester fleece to prevent localized stress concentrations from causing membrane failure.
  • Monolithic Bonding: Creating a seamless transition between horizontal and vertical surfaces.
  • Crack Bridging: The ability of the reinforced resin to span gaps up to 5mm without losing integrity.
  • Impact Resistance: Enhanced durability against hail or dropped tools during facility maintenance.

Critical Flashing Detail for I-Beam Stanchions and Penetrations

The most technically challenging aspect of the hangar envelope is the flashing of I-beam stanchions. These structural members create intricate "nooks and crannies" where water tends to pond and freeze. Traditional flashing often leaves gaps at the interior corners of the I-beam, leading to slow-leak scenarios that can rust the structural steel from the inside out. Our engineering solution involves a multi-stage liquid-applied flashing detail. First, a PMMA primer is used to ensure a high-energy bond to the steel. Then, a thick layer of base resin is applied, followed by a custom-cut piece of fleece that is meticulously wrapped around the geometry of the beam.

This process is repeated in multiple layers, effectively "molding" the resin around the steel. Because the PMMA is a liquid during application, it penetrates every void and crevice of the I-beam, leaving no room for air or water. The final top-coat provides the necessary UV protection and chemical resistance. This method transforms the stanchion from a liability into a sealed component of the building envelope. Our audit concludes that this liquid-applied approach reduces the probability of flashing failure by over 80% compared to traditional sheet-metal flashing, as it removes the reliance on sealants and mechanical fasteners.

  • Void Filling: The liquid resin's ability to penetrate tight tolerances in structural steel.
  • Geometry Conformation: Perfect adherence to complex shapes without the need for stretching or cutting sheet goods.
  • Corrosion Inhibition: Sealing the steel completely to prevent moisture-induced oxidation.
  • Audit Verification: Using infrared thermography to confirm the absence of thermal

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #245

Commercial Expansion Joint Bellows & Heavy-Gauge Neoprene Movement Transitions on Commercial Chemical Processing Facilitys

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Commercial Expansion Joint Bellows & Heavy-Gauge Neoprene Movement Transitions on Commercial Chemical Processing Facilitys

Structural Dynamics and Differential Settlement in Chemical Processing Facilities

In the realm of heavy industrial building envelopes, chemical processing facilities present a unique set of engineering challenges. Unlike standard commercial warehouses, these facilities are often composed of multiple independent wings, each housing equipment with vastly different weights and vibration profiles. This disparity leads to differential structural settlement, where one section of the building sinks or shifts at a different rate than the adjacent wing. When these structures are tied together without adequate movement transitions, the resulting stress manifests as catastrophic shear failure in the roofing membrane and structural cracking in the parapet walls.

From a master roofer's perspective, the primary objective is to decouple these structural masses while maintaining a continuous, watertight seal. The movement is rarely linear; it is typically a combination of thermal expansion, seismic drift, and the settling of heavy reactor foundations. If the building envelope is too rigid, the membrane will bridge, stretch, and eventually tear at the points of highest stress. We analyze these movements using a combination of historical settlement data and real-time monitoring of the joint gaps to determine the necessary range of motion for the expansion assemblies.

  • Analysis of soil bearing capacity and its impact on multi-wing structural independence.
  • Calculation of the coefficient of thermal expansion for steel-frame industrial superstructures.
  • Evaluation of vibration-induced fatigue at the interface of mechanical mezzanines and roof decks.
  • Assessment of seismic joint requirements according to local building codes and ANSI standards.

Engineering Heavy-Gauge Neoprene Movement Transitions

When the calculated movement exceeds the capacity of standard flashing, we implement heavy-gauge neoprene bellows. Neoprene is selected over standard EPDM or PVC in chemical environments due to its superior resistance to ozone, weathering, and a wide array of corrosive chemical vapors that are common in processing plants. The "bellows" design is critical; by creating a series of folds, the material can expand and contract like an accordion, distributing the mechanical stress across a larger surface area rather than concentrating it at a single fold point.

The engineering of these transitions requires a deep understanding of material science. We specify heavy-gauge neoprene to ensure the bellows can withstand the negative pressure events and wind uplift common in industrial zones. The thickness of the neoprene must be balanced with its elasticity; too thick, and the material becomes too rigid to accommodate the movement; too thin, and it becomes susceptible to puncture or chemical degradation. Each bellows assembly is custom-engineered to the specific width of the expansion joint, ensuring that the material remains in its elastic deformation zone and never reaches the point of plastic deformation.

  • Utilization of ASTM D2000 standards for rubber material specifications to ensure chemical compatibility.
  • Implementation of multi-ply neoprene construction for enhanced tear resistance and durability.
  • Design of bellows geometry to allow for multi-axial movement, including lateral shift and vertical settlement.
  • Integration of reinforced neoprene gaskets to prevent "blow-out" during high-pressure weather events.

The Criticality of Watertight Tie-ins and Interface Engineering

The most frequent point of failure in any expansion joint system is not the bellows itself, but the tie-in where the neoprene meets the primary roof membrane. This interface is a transition between two materials with entirely different thermal expansion coefficients and bonding characteristics. A failure here leads to immediate water infiltration, which, in a chemical facility, can lead to the corrosion of expensive processing equipment located directly beneath the roof deck.

To achieve a permanent, watertight seal, we employ a rigorous multi-stage flashing process. We begin by mechanically fastening the neoprene bellows to the structural steel or concrete curb using heavy-duty termination bars and neoprene gaskets. This ensures a positive mechanical connection that does not rely solely on adhesives. We then transition to the roof membrane—typically a reinforced TPO or PVC—using a combination of heat-welding and high-grade elastomeric sealants. The flashing is designed with a "relief fold" to ensure that as the building moves, the membrane is not pulled taut against the termination bar, which would otherwise lead to a "zipper" failure.

  • Application of reinforced flashing membranes to bridge the gap between the bellows and the field roofing.
  • Use of stainless steel termination bars to prevent galvanic corrosion in chemical-rich environments.
  • Installation of redundant sealant beads using high-modulus silicone or polyurethane polymers.
  • Execution of rigorous flood testing and infrared thermography to verify the integrity of the tie-in.

Audit Findings and Long-Term Maintenance Protocols

A comprehensive building envelope audit of a chemical processing facility reveals that movement joints are dynamic components, not "install and forget" solutions. Over time, neoprene can suffer from "compression set," where the material loses its ability to return to its original shape after being compressed. Furthermore, the accumulation of chemical residues on the surface of the bellows can lead to premature hardening or cracking. Our audits focus on identifying these early warning signs of material fatigue before they evolve into leaks.

The maintenance protocol for these systems must be stringent. We recommend a quarterly inspection cycle that includes a physical "stretch test" of the bellows to ensure they are still operating within their designed elastic range. Any evidence of cupping, surface crazing, or detachment at the termination bars is addressed immediately. By treating the expansion joints as critical mechanical components of the building—similar to the processing equipment they protect—facility managers can extend the lifecycle of the roof and avoid the massive costs associated with unplanned structural repairs and production downtime.

  • Scheduled visual inspections for ozone cracking and chemical pitting on neoprene surfaces.
  • Verification of fastener torque on termination bars to prevent wind-driven water intrusion.
  • Monitoring of joint gap widths to ensure structural settlement remains within engineered tolerances.
  • Implementation of a lifecycle replacement plan for elastomeric components based on UV exposure data.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #246

Commercial Kitchen Grease Containment & 304 Stainless Steel Catchment Shielding on Commercial Municipal City Hall & Administrative Complexs

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Commercial Kitchen Grease Containment & 304 Stainless Steel Catchment Shielding on Commercial Municipal City Hall & Administrative Complexs

The Mechanics of Lipid Degradation on Single-Ply Membranes

In the context of a Municipal City Hall and Administrative Complex, the building envelope is often subjected to disparate stressors. While the administrative wings face standard UV exposure and thermal cycling, the integrated commercial kitchen facilities introduce a volatile chemical variable: animal fat lipids. During the engineering audit of these facilities, we frequently observe a critical failure point where exhaust fans vent grease-laden air directly over single-ply roofing membranes, such as Thermoplastic Polyolefin (TPO) or Ethylene Propylene Diene Monomer (EPDM). Animal fats are not merely surface contaminants; they are chemically aggressive agents that initiate a process of lipid degradation.

When lipids settle on a membrane, they undergo oxidation and polymerization, creating a sticky, acidic residue. This residue penetrates the polymer matrix of the roofing material, leading to plasticizer migration. In PVC or TPO systems, the loss of these essential plasticizers results in the membrane becoming brittle, losing its elasticity, and eventually developing micro-fissures. These fissures are not immediately visible to the naked eye but serve as conduits for moisture ingress, compromising the entire building envelope and risking structural rot in the underlying decking.

  • Accelerated embrittlement of thermoplastic membranes due to chemical solvent interaction.
  • Loss of tensile strength in the membrane's upper wear layer.
  • Increased susceptibility to puncture and mechanical damage during routine maintenance.
  • Chemical breakdown of seam welds, leading to systemic failure of the watertight seal.

Engineering 304 Stainless Steel Catchment Shielding

To mitigate the destructive impact of grease-laden condensate and exhaust, the implementation of 304 Stainless Steel catchment shielding is mandatory. We specify 304 grade stainless steel because of its superior chromium-nickel composition, which provides the necessary corrosion resistance against the acidic nature of oxidized animal fats. Unlike galvanized steel, which can succumb to white rust in high-moisture, high-grease environments, 304 stainless steel maintains its structural integrity and surface passivity.

The engineering of these catchment boxes requires a precision-fit approach to ensure that all effluent is directed away from the primary roof surface. The shielding must be designed with a positive slope to prevent "ponding" of grease, which can lead to anaerobic bacterial growth and further chemical aggression. We utilize custom-fabricated troughs with integrated drip edges that extend beyond the roof curb, ensuring that the grease is captured and channeled into a dedicated drainage system rather than overflowing onto the membrane.

  • Fabrication of heavy-gauge 304 Stainless Steel to resist thermal warping and mechanical stress.
  • Implementation of seamless welding at all joints to prevent lipid seepage into the substrate.
  • Installation of oversized catchment basins to accommodate peak exhaust volumes during high-capacity events.
  • Strategic placement of shielding to account for wind-driven rain and aerosolized grease drift.

Sacrificial Chemical-Resistant Coatings and Barrier Layers

Even with high-grade stainless steel shielding, the risk of "over-splash" or accidental spills remains a reality in municipal kitchen operations. To address this, we employ a dual-layer protection strategy involving sacrificial chemical-resistant coatings. These coatings act as a primary line of defense, absorbing the chemical brunt of lipid exposure and protecting the underlying single-ply membrane from direct contact. We typically specify high-build, aliphatic polyurethane or specialized polymer coatings that are engineered to withstand high pH and low pH fluctuations.

The "sacrificial" nature of these coatings is a deliberate engineering choice. Rather than attempting to create an indestructible surface, we create a renewable layer that can be audited and reapplied without disturbing the primary waterproofing membrane. This prevents the need for costly membrane replacements and ensures that the building envelope remains intact. The application process involves a rigorous surface preparation phase, including the removal of all existing lipids via industrial degreasers to ensure a molecular bond between the coating and the roof surface.

  • Application of high-solids polymer coatings to create a non-porous, lipid-repellent barrier.
  • Use of reinforced mesh within the coating layer to prevent cracking during thermal expansion.
  • Strategic zoning of coatings around exhaust vents and grease traps to optimize material usage.
  • Regular thickness testing to ensure the sacrificial layer meets the minimum mil-thickness specifications.

Audit Protocols and ASTM Compliance for Municipal Envelopes

A master-level engineering audit of a Municipal City Hall complex requires a systematic approach to monitoring the degradation of the building envelope. We align our audit protocols with ASTM and ANSI standards to ensure that the facility remains compliant with national building codes and safety regulations. The focus is on the "Critical Transition Zones"—the areas where the stainless steel shielding meets the roofing membrane. These junctions are the most common points of failure due to the differing coefficients of thermal expansion between the metal and the polymer.

Our audit process involves infrared thermography to detect subsurface moisture trapped beneath grease deposits and the use of electronic leak detection (ELD) to verify the integrity of the seams. By establishing a baseline of the membrane's current state, we can predict the lifecycle of the sacrificial coatings and schedule maintenance before a catastrophic failure occurs. This proactive approach transforms the roof from a liability into a managed asset, ensuring the longevity of the municipal infrastructure.

  • Adherence to ASTM E2128 for the evaluation of roof membrane integrity and seam strength.
  • Implementation of quarterly lipid-residue sampling to monitor the efficiency of the catchment systems.
  • Utilization of thermal imaging to identify "hot spots" where grease accumulation is impeding thermal performance.
  • Detailed documentation of coating degradation rates to refine the sacrificial layer replacement cycle.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #247

Clear-Span Structural Joist Deflection Forensics & Ponding Instability Remediation on Commercial High-Rise Commercial Penthouse Towers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Clear-Span Structural Joist Deflection Forensics & Ponding Instability Remediation on Commercial High-Rise Commercial Penthouse Towers

Forensic Analysis of Structural Joist Deflection and Load Distribution

In the high-stakes environment of high-rise commercial penthouse towers, the integrity of the building envelope is often compromised not by membrane failure, but by structural movement. A comprehensive engineering audit begins with a forensic examination of clear-span structural joists. When these members are subjected to long-term dead loads and environmental stressors, they may exhibit center-span deflection. This phenomenon, often exacerbated by the lack of intermediate support in penthouse architectural designs, creates a concave profile that contradicts the original design intent of a positive slope toward primary drains.

To accurately quantify this deflection, our team employs precision laser leveling and string-line forensics to map the roof's topography. We look for the "belly" of the joist, where the vertical displacement exceeds the allowable L/360 deflection limit common in commercial steel and concrete standards. When a joist deflects, it creates a catchment area that traps precipitation, initiating a dangerous feedback loop known as ponding instability. The added weight of the standing water further increases the load on the joist, leading to more deflection and, consequently, more water accumulation.

  • Utilization of high-precision laser levels to establish a true horizontal datum line across the penthouse footprint.
  • Calculation of the actual vs. theoretical slope to identify localized depressions and structural sagging.
  • Assessment of joist camber and the evaluation of whether the deflection is elastic or has transitioned into permanent plastic deformation.
  • Analysis of the structural connection points to ensure that deflection is not a result of connection slippage or weld failure at the bearing plates.

The Mechanics of Ponding Instability and Envelope Degradation

Ponding instability is a critical failure state in building envelope engineering. It occurs when the rate of water accumulation exceeds the structural capacity of the roof system to shed that water via gravity. In a penthouse tower, where wind uplift and extreme thermal expansion are constant variables, standing water does more than just add weight; it accelerates the degradation of the waterproofing membrane. Water trapped in center-span depressions undergoes constant freeze-thaw cycles, which can lead to micro-cracking in the membrane and the eventual infiltration of moisture into the structural deck.

From a material science perspective, the hydrostatic pressure exerted by several inches of standing water forces moisture through the smallest imperfections in the flashing and seams. This is particularly perilous in high-rise structures where the penthouse serves as the primary shield for the floors below. If the structural joists have deflected to the point where the roof is effectively "cupping," the risk of a catastrophic structural failure increases as the water weight reaches a critical threshold, potentially exceeding the design live load of the roof assembly.

  • Identification of "ponding" as defined by ASTM standards, where water remains on the roof for more than 48 hours after a rain event.
  • Evaluation of the membrane's chemical resistance to stagnant water and the potential for biological growth or sediment buildup.
  • Monitoring of the thermal bridging effects where standing water cools the structural steel, potentially leading to condensation and corrosion on the underside of the deck.
  • Assessment of the impact of standing water on the overall R-value of the insulation, as saturated insulation loses its thermal efficiency.

Engineering Remediation via Custom Tapered Polyiso Crickets

To remediate center-span deflection without the prohibitive cost and weight of structural steel reinforcement, we implement a precision-engineered tapered insulation system. The primary tool in this remediation is the custom-fabricated polyisocyanurate (polyiso) cricket. Polyiso is selected for its high compressive strength and superior thermal resistance, providing a lightweight solution that does not add significant dead load to the already stressed joists. By installing these tapered sections, we effectively "fill" the depression created by the joist deflection, restoring the necessary slope to move water toward the drains.

The engineering of these crickets requires a meticulous layout. We do not simply lay flat boards; we design a geometric transition that guides water away from the center-span low points and toward the perimeter or internal drains. This process involves creating a "valley" and "ridge" system using tapered polyiso panels that are adhered to the deck using low-VOC, high-strength adhesives. This ensures that the insulation remains monolithic and does not shift under the weight of the final membrane application, maintaining the integrity of the new slope over the long term.

  • Design of custom tapered polyiso layouts based on the forensic laser map of the roof's existing depressions.
  • Application of high-density polyiso with a minimum compressive strength of 25 psi to withstand foot traffic and structural movement.
  • Implementation of a staggered joint pattern to prevent the creation of linear leak paths and to increase the overall stability of the insulation layer.
  • Precision trimming of insulation edges to ensure a seamless transition between the tapered crickets and the existing roof insulation.

Hydraulic Routing and Final Envelope Integration

The final phase of the remediation process is the strategic routing of water outward to the primary drainage system. Once the tapered polyiso crickets have established the correct geometry, the building envelope must be sealed with a high-performance membrane—typically a reinforced TPO or PVC system—that is heat-welded at the seams. The goal is to create a seamless, impervious skin that leverages the new slope to accelerate water runoff. We focus heavily on the transition points where the new crickets meet the existing parapet walls and scuppers, as these are the most common points of failure in high-rise envelopes.

Effective water routing requires more than just a slope; it requires a comprehensive understanding of hydraulic flow. We ensure that the water is not merely moved off the center-span joists but is routed through a clear path to the drains without creating new "dead spots" or secondary ponding areas. By integrating the tapered insulation with professional-grade flashing and reinforced edge strips, we create a robust, redundant system that protects the penthouse tower from the elements while ensuring the structural joists are no longer subjected to the risks of ponding instability.

  • Installation of a fully adhered, heat-welded membrane to ensure a monolithic waterproof barrier across the new tapered slopes.
  • Reinforcement of all flashing details at the perimeter and around penetration points to prevent capillary action and water ingress.
  • Verification of flow rates through a controlled water test, ensuring that all standing water is routed to the drains within the acceptable timeframe.
  • Final audit of the building envelope to confirm that the structural deflection has been neutralized by the geometric correction of the insulation system.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #248

Complete Old Roof Tear-Offs Down to Clean Wood Decking & Substrate Remediation on Commercial Regional Healthcare Medical Centers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Complete Old Roof Tear-Offs Down to Clean Wood Decking & Substrate Remediation on Commercial Regional Healthcare Medical Centers

The Engineering Audit and Failure Analysis of Multi-Layer Assemblies

In the context of regional healthcare medical centers, the building envelope is not merely a shelter but a critical component of infection control and operational continuity. A comprehensive engineering audit often reveals a history of "recover" installations, where new membranes were layered over failing legacy systems. This practice, while cost-effective in the short term, creates a dangerous thermal and moisture trap. Over time, these multi-layer assemblies suffer from interstitial condensation and the degradation of bitumen-based adhesives, leading to systemic failure that cannot be patched.

From a material science perspective, the accumulation of multiple layers of modified bitumen or built-up roofing (BUR) increases the dead load on the structural decking, often exceeding the original design specifications of the building. When water penetrates the uppermost membrane, it migrates through the layers, saturating the substrate without providing a clear path for evaporation. This leads to the slow decay of the structural wood decking, which remains hidden until a catastrophic failure occurs.

  • Identification of thermal bridging points where insulation has compressed or shifted.
  • Assessment of moisture vapor transmission rates across legacy membranes.
  • Evaluation of dead load increases caused by redundant roofing layers.
  • Mapping of saturated zones using infrared thermography to pinpoint substrate rot.

Systematic Deconstruction and Assembly Stripping Protocols

The transition from an audit to a full tear-off requires a surgical approach to deconstruction. In a healthcare environment, this process must be managed to avoid disrupting critical facility operations. The objective is a total strip-down to the original wood decking, removing every trace of old flashing, adhesives, and insulation. This process is fundamentally different from a standard removal; it is an engineering exercise in uncovering the true condition of the building's skeleton.

Utilizing heavy-duty mechanical stripping equipment, the crew removes the layers in a phased sequence to maintain the integrity of the building envelope. Special attention is paid to the perimeter edges and parapet walls, where water typically accumulates. The removal of old tar and gravel layers requires precise handling to ensure that no residual bitumen remains on the wood deck, as old adhesives can interfere with the bonding of new substrate patches or the adhesion of modern membranes.

  • Implementation of phased removal zones to maintain partial building enclosure.
  • Mechanical stripping of modified bitumen and BUR layers to expose the raw substrate.
  • Removal of all legacy flashing and rusted metal edge components.
  • Strict adherence to ANSI safety standards for debris removal and load management on the roof deck.

Substrate Evaluation and Structural Wood Remediation

Once the decking is exposed, the master roofer performs a forensic inspection of the wood substrate. In many older medical centers, the decking consists of heavy-duty planking or early-generation plywood. We look for signs of fungal decay, delamination, and "soft spots" that indicate internal rot. The structural integrity of the wood is paramount; any section that exhibits more than 10% loss of thickness due to decay or moisture damage is flagged for immediate remediation.

Remediation is not a matter of simple patching but of structural replacement. We employ a "cut-back" method, where damaged wood is removed well past the point of visible rot until sound, dry timber is reached. New panels are selected to match the existing thickness and grade of the original decking to ensure a flush surface. This prevents "lippage," which can cause premature wear and puncture points in the new roofing membrane. All new wood is secured using heavy-duty fasteners that meet current structural load requirements.

  • Moisture content testing of wood decking using calibrated hygrometers.
  • Removal of decayed wood panels back to the nearest structural joist or support.
  • Installation of CDX grade plywood or OSB that matches the original substrate thickness.
  • Verification of fastener spacing and pull-out strength to ensure a rigid diaphragm.

Final Substrate Preparation and Envelope Integration

The final phase of the remediation process is the preparation of the "clean wood deck." A substrate that is merely "fixed" is not sufficient; it must be engineered for the next thirty years of service. This involves the meticulous cleaning of the entire surface to remove old nails, splinters, and residual bitumen. A clean substrate is the only way to ensure that the new insulation and membrane system achieve a uniform bond and that mechanical fasteners provide consistent hold-down strength across the entire roof plane.

Integration of the new envelope requires a seamless transition between the remediated wood decking and the new flashing systems. We focus on the critical junctions—the roof-to-wall transitions and the penetration points for HVAC and medical gas venting. By ensuring the substrate is perfectly level and structurally sound, we eliminate the risk of ponding water, which is the primary catalyst for future substrate failure. The result is a monolithic building envelope that adheres to the highest standards of commercial roofing engineering.

  • Surface grinding and sanding of transition joints to eliminate protrusions.
  • Application of high-performance primers where required by the membrane manufacturer.
  • Installation of new drip edges and reinforced flashing at all perimeter boundaries.
  • Final engineering sign-off verifying that the substrate meets ASTM standards for load-bearing capacity.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #249

Stripping Old Shingles Down to Clean Wood Sheathing Across Commercial Eaves on Commercial University Research Laboratorys

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Stripping Old Shingles Down to Clean Wood Sheathing Across Commercial Eaves on Commercial University Research Laboratorys

Systematic Deconstruction and Multi-Layer Envelope Auditing

In the context of a University Research Laboratory, the roofing system is not merely a cover but a critical component of the building envelope that protects sensitive instrumentation and hazardous materials. During our engineering audit, we encountered a common commercial failure: the accumulation of multiple layers of asphalt shingles over several decades. This "layering" practice creates a massive dead load on the structural rafters and traps moisture against the wood sheathing, leading to anaerobic decay. A true master-level restoration requires a complete strip-down to the original wood substrate to evaluate the true condition of the building envelope.

The removal process must be executed with surgical precision to avoid compromising the existing sheathing. Using heavy-duty tear-off equipment, we systematically removed the redundant layers, ensuring that the underlying decking was not gouged or splintered. This phase of the project is critical because it allows the specialist to identify "soft spots" and localized rot that are invisible during a standard visual inspection. By stripping the eaves entirely, we expose the drip edge and fascia interfaces, where the majority of water infiltration typically occurs in commercial laboratory structures.

  • Implementation of a phased tear-off sequence to maintain the laboratory's internal climate control.
  • Utilization of magnetic sweepers and debris containment to prevent nail contamination of the university grounds.
  • Detailed mapping of the sheathing condition to identify areas of fungal decay or moisture saturation.
  • Verification of the existing flashing integrity at the transition from the eaves to the vertical masonry walls.

Fastener Withdrawal Resistance and Substrate Analysis

Once the clean wood sheathing is exposed, the focus shifts from demolition to material science. A critical failure point in aging commercial roofs is the loss of fastener withdrawal resistance. Over time, the repeated expansion and contraction of the roof deck, coupled with the chemical degradation of the wood fibers, reduce the "grip" of the nails. In a high-wind event, a roof is only as strong as its fasteners; if the wood has degraded to a point of "nail sickness," the entire system is prone to catastrophic uplift.

Our engineering approach involves testing the withdrawal resistance of the remaining fasteners and the structural integrity of the sheathing. We utilize a calibrated pull-test method to ensure that the wood can support the required load paths according to ANSI standards. If the wood fibers have crushed or rotted around the fastener holes, the substrate is deemed compromised. This is particularly prevalent at the eaves, where capillary action often draws moisture upward from the gutter line into the rafter tails, compromising the shear strength of the wood.

  • Assessment of wood species and grain density to determine the appropriate fastener schedule for the new system.
  • Measurement of moisture content using a pin-type meter to ensure the substrate is below 19% before new installation.
  • Analysis of fastener corrosion levels to determine if galvanic reactions have occurred between the nails and the shingle nails.
  • Calculation of the required fastener spacing to meet local building codes and wind-uplift requirements.

Structural Remediation and Rafter Sistering

During the audit of the University Research Laboratory, we identified several compromised rafters at the eave intersections. When the building envelope fails, water typically settles in the same locations, leading to localized structural failure. To restore the load-bearing capacity of the roof, we employ a process known as sistering. This involves installing a new, structurally sound member alongside the compromised rafter, effectively transferring the load to a healthy section of the building frame.

The sistering process is not a simple matter of nailing a new board to an old one. To achieve true structural continuity, we utilize kiln-dried lumber or LVL (Laminated Veneer Lumber) for superior strength-to-weight ratios. The new members are secured using a combination of structural adhesives and staggered heavy-duty bolts. This ensures that the load path is continuous from the ridge down to the wall plate, eliminating any deflection that could cause pooling water or "ponding" on the final roof surface.

  • Precision cutting of sister members to ensure a tight, gap-free fit against the existing rafter.
  • Application of industrial-grade structural adhesives to create a monolithic bond between the old and new wood.
  • Installation of galvanized carriage bolts to prevent oxidation and ensure long-term shear resistance.
  • Verification of the load distribution across the eave to prevent uneven settling of the roofline.

Establishing Flat Decking Planes for High-Performance Envelopes

The final and most technical phase of the substrate preparation is the establishment of a flat decking plane. A common mistake in commercial roofing is installing a new membrane over a wavy or uneven deck. In a research laboratory, where drainage must be absolute to prevent interior leaks, any dip in the decking can lead to hydrostatic pressure buildup against the seams of the roofing material. A perfectly planar surface is the foundation of a high-performance building envelope.

To achieve this, we employ a process of grinding high spots and shimming low spots. If the sheathing has warped due to previous moisture cycles, we install thin, high-density plywood overlays or specialized leveling strips. This process ensures that the final roofing membrane sits flush against the substrate, eliminating air pockets where condensation can form. By creating a uniform plane across the eaves, we ensure that water is shed efficiently toward the scuppers and gutters, adhering to the strictest engineering specifications for commercial drainage.

  • Utilization of a laser level to map the variance in the decking plane across the entire eave section.
  • Sanding and grinding of protruding nail heads and wood knots to prevent "telegraphing" through the new membrane.
  • Installation of OSB or marine-grade plywood patches in areas where the original sheathing has lost its dimensional stability.
  • Final verification of the slope-to-drain ratio to ensure that no standing water will accumulate on the laboratory roof.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #250

Low-VOC Cold-Applied Adhesives & HVAC Air Intake Odor Mitigation Protocols on Commercial Suburban Corporate Office Parks

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Low-VOC Cold-Applied Adhesives & HVAC Air Intake Odor Mitigation Protocols on Commercial Suburban Corporate Office Parks

The Engineering Challenge of Corporate Office Park Envelopes

In the realm of Class A suburban corporate office parks, the building envelope is not merely a shell but a complex atmospheric regulator. The primary engineering challenge arises when critical roof-level repairs or modifications are required on occupied structures. Most of these facilities utilize massive rooftop air handling units (AHUs) that create significant negative pressure zones, effectively acting as vacuum cleaners for any airborne particulates or chemical vapors released during the construction process. When traditional solvent-based adhesives or hot-applied membranes are introduced, the risk of "vapor migration" becomes a liability. If volatile organic compounds (VOCs) are drawn into the HVAC intake, the result is a building-wide odor event that can trigger emergency evacuations and compromise indoor air quality (IAQ) standards.

A comprehensive engineering audit of these sites reveals that the intersection of the roofing membrane and the HVAC curb is the most frequent point of failure. These areas are subject to extreme thermal cycling and structural vibration, which often lead to hairline fractures in traditional sealants. To maintain the integrity of the building envelope without disrupting corporate operations, a shift toward cold-applied, low-VOC chemistry is mandatory. The goal is to achieve a monolithic bond that meets ASTM standards for wind uplift and water penetration while ensuring that the chemical footprint of the installation remains undetectable to the building's occupants.

  • Analysis of AHU intake proximity to repair zones to establish "danger radii" for off-gassing.
  • Evaluation of existing substrate compatibility with polyurethane bonding agents.
  • Assessment of thermal bridging at curb flashing points that contribute to adhesive failure.
  • Mapping of internal airflow patterns to predict the trajectory of potential vapor plumes.

Material Science of Low-VOC Polyurethane Bonding Agents

The transition from solvent-borne adhesives to advanced polyurethane (PU) bonding agents represents a significant leap in material science. Traditional adhesives rely on solvents that evaporate rapidly, releasing pungent odors and hazardous fumes. In contrast, modern low-VOC cold-applied adhesives utilize a cross-linking chemical reaction that cures through moisture or a secondary catalyst, rather than evaporation. This ensures that the adhesive does not "off-gas" into the atmosphere during the curing phase. From an engineering perspective, these PU agents provide superior elasticity, allowing the bond to expand and contract in tandem with the building's structural movements, which is critical in the fluctuating temperatures of suburban corporate parks.

To meet the rigorous demands of commercial roofing, these adhesives must adhere to strict ANSI and ASTM guidelines regarding shear strength and peel resistance. The chemistry is engineered to penetrate the microscopic pores of the substrate, creating a mechanical lock that is often stronger than the materials being bonded. Rapid-setting formulas are particularly valuable in these environments; by reducing the "open time" and accelerating the initial set, the window for potential contamination or vapor migration is drastically narrowed. This allows the master roofer to secure the envelope quickly, ensuring that the waterproofing layer is fully functional before the next weather event.

  • Utilization of moisture-cure polyurethane for deep-pore substrate penetration.
  • Implementation of zero-solvent formulations to eliminate the risk of HVAC contamination.
  • Application of high-modulus bonding agents to resist wind-uplift forces in open suburban landscapes.
  • Verification of cure rates via shore-hardness testing to ensure rapid-setting performance.

Air Intake Containment and Odor Mitigation Protocols

Even with low-VOC materials, a master tradesman employs a "defense-in-depth" strategy to ensure zero-downtime execution. The primary protocol involves the establishment of physical containment barriers. These are not merely plastic sheets but engineered shrouds designed to encapsulate the application area. By creating a temporary sealed environment around the repair zone, any residual odors are trapped and diverted away from the HVAC intakes. In high-risk scenarios, negative pressure machines with activated carbon filtration are deployed within the shroud to scrub the air before it is released into the surrounding environment.

Coordination with the facility's building automation system (BAS) is equally critical. The protocol requires a synchronized shutdown of specific AHU zones during the peak application window. By temporarily switching the HVAC system to a "recirculation mode" or adjusting the dampers to limit intake from the affected roof sector, the engineering team can virtually eliminate the possibility of odors entering the office space. This surgical approach to air management allows the corporate office to remain fully operational, with employees unaware that critical envelope repairs are occurring just a few feet above their workstations.

  • Installation of reinforced polyethylene shrouds around all active work zones.
  • Deployment of carbon-filtration scrubbers to neutralize trace chemical vapors.
  • Strategic adjustment of HVAC dampers to prevent intake suction during adhesive application.
  • Real-time monitoring of IAQ sensors within the building to verify odor-free conditions.

Execution Strategy and Long-Term Envelope Performance

The final phase of the engineering process is the precise execution of the bonding sequence. Surface preparation is the most critical step; the substrate must be mechanically cleaned and chemically primed to remove all contaminants, including oils and oxidation. Once the surface is optimized, the low-VOC polyurethane adhesive is applied using a controlled-delivery system to ensure uniform thickness and avoid "voiding," which can lead to premature failure. The rapid-setting nature of these adhesives allows for an immediate transition to the final capping layer, sealing the envelope against the elements in a fraction of the time required by traditional heat-welded systems.

Long-term performance is verified through a rigorous post-installation audit. This includes infrared thermography to detect any trapped moisture or air pockets within the bond line and flood testing to ensure the containment barriers have not compromised the overall waterproofing. By integrating material science with strict containment protocols, Aquashield Corporate ensures that the building envelope is not only restored to its original engineering specifications but is enhanced for future durability. The result is a seamless, odorless, and high-performance roofing system that protects the asset without interrupting the productivity of the corporate environment.

  • Mechanical abrasion of substrates to increase the surface area for polyurethane bonding.
  • Application of specialized primers to ensure chemical compatibility between layers.
  • Use of infrared scanning to verify the homogeneity of the cured adhesive bond.
  • Final validation through ASTM-standard water penetration testing at all curb interfaces.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #251

Solar Photovoltaic Ballasted Racking Point-Load Defense & Sacrificial Slip Sheets on Commercial Big-Box Retail Power Centers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Solar Photovoltaic Ballasted Racking Point-Load Defense & Sacrificial Slip Sheets on Commercial Big-Box Retail Power Centers

The Mechanics of Ballasted Point-Load Compression and Insulation Fatigue

In the context of Big-Box Retail Power Centers, the transition to solar photovoltaic (PV) arrays introduces a complex set of static and dynamic loads that the original building envelope was not necessarily engineered to sustain. A ballasted system, while advantageous for avoiding thousands of roof penetrations, converts the roof surface into a series of high-pressure point-load zones. The primary concern from an engineering standpoint is the compression set of the underlying insulation, typically polyisocyanurate (ISO) board. When heavy concrete blocks are placed atop the membrane, the load is concentrated through the racking feet, creating a localized stress point that can exceed the compressive strength of the insulation.

If the insulation undergoes a permanent compression set, it creates a localized depression or "bowl" effect. This is a critical failure point because it disrupts the established slope-to-drain characteristics of the roof. Once a depression forms, water begins to pond around the base of the racking system, increasing the risk of hydrostatic pressure forcing moisture through the seams or laps. To mitigate this, we analyze the load-bearing capacity based on ASTM standards for thermal insulation, ensuring that the combined weight of the PV modules and the ballast does not exceed the allowable pounds per square foot (PSF) for the specific density of the ISO board installed.

  • Analysis of compressive strength: Evaluating 2.5 pcf versus 4.0 pcf polyisocyanurate to determine the threshold of permanent deformation.
  • Load distribution calculations: Calculating the total static load per racking foot to prevent "punch-through" failures.
  • Slope-to-drain verification: Utilizing laser leveling to ensure that ballast depressions do not create stagnant water pockets.
  • Thermal bridging assessment: Examining how concentrated loads affect the R-value and heat flow at the point of contact.

Sacrificial Slip-Sheets and the Mitigation of Membrane Abrasion

One of the most overlooked failure modes in ballasted solar installations is the phenomenon of wind-induced vibration. While the ballast is intended to keep the system grounded, the racking is not completely static. High-wind events create micro-movements where the rubber or plastic feet of the racking system rub against the TPO or EPDM membrane. This constant friction acts as a low-grit sandpaper, gradually wearing down the own membrane's wear layer and eventually breaching the waterproofing barrier. This is where the implementation of heavy-duty sacrificial slip-sheets becomes non-negotiable for a high-performance envelope.

A professional-grade slip-sheet serves as a sacrificial interface, absorbing the shear stress and abrasion so the primary roof membrane remains intact. We specify reinforced, high-density polyethylene (HDPE) or oversized TPO-welded pads that extend beyond the footprint of the racking foot. By introducing this secondary layer, we decouple the racking hardware from the building's primary water-tight seal. This approach follows the principle of "planned obsolescence" for the slip-sheet; it is far more cost-effective to replace a localized pad during a 10-year audit than to perform a full-scale membrane replacement due to systemic abrasion holes.

  • Material selection: Utilizing UV-stabilized, high-density polymers that resist chemical degradation from concrete leaching.
  • Friction coefficient analysis: Reducing the "grip" between the racking foot and the roof to prevent membrane stretching during thermal expansion.
  • Overlap specifications: Ensuring slip-sheets extend at least 3 inches beyond the ballast perimeter to prevent edge-cutting.
  • Installation auditing: Verifying that slip-sheets are laid flat without wrinkles, which could create secondary pressure points.

Pre-fabricated Target Patches and Strategic Reinforcement Zones

To further harden the building envelope, Aquashield advocates for the use of pre-fabricated target patches. Rather than relying on the general field membrane to support the ballast, target patches are engineered reinforcements placed precisely where the racking feet will reside. These patches are often composed of a multi-layered composite—combining a reinforced scrim with a thicker membrane gauge—and are heat-welded to the roof surface using industry-standard robotic welding parameters. This creates a "hardened zone" that can withstand the intense localized pressure and potential chemical reactions between the concrete ballast and the roof surface.

The engineering logic behind target patches is to create a predictable failure point that is easily monitored. During a quarterly engineering audit, a technician can visually inspect the target patch for signs of distress, such as "tenting" or "fish-mouthing" at the edges. Because these patches are distinct from the main field, they allow for targeted repairs without disturbing the surrounding membrane. This modular approach to envelope defense ensures that the integrity of the Big-Box retail center's roof is maintained even as the solar array ages and the ballast settles over time.

  • Welding verification: Utilizing electronic leak detection (ELD) to ensure the target patch is 100% fused to the field membrane.
  • Load spreading: Using the patch to distribute the vertical load over a wider surface area, reducing the PSI on the insulation.
  • Chemical barrier properties: Selecting patch materials that are resistant to the alkaline nature of concrete masonry units (CMUs).
  • Maintenance accessibility: Designing patches that allow for the lifting of racking to inspect the underlying substrate.

Cable Tray Routing and the Preservation of Drainage Integrity

The final component of a comprehensive envelope audit involves the routing of electrical conduits and cable trays. In many poorly executed solar installs, cable trays are laid haphazardly across the roof, often crossing over critical drainage paths or resting directly on the membrane without support. This creates two primary risks: the creation of "water dams" that trap rain on the roof, and the risk of "cable chafe," where the weight of the copper cabling causes the tray to saw into the membrane during thermal cycling of the building.

Proper engineering requires that cable trays be routed parallel to the roof's slope and elevated slightly off the membrane using non-penetrating supports. This ensures that water can flow freely beneath the trays to the scuppers or internal drains. Furthermore, we mandate the use of protective conduits at all transition points where cables enter the building envelope. By treating the cable routing as a structural element of the roof system rather than an afterthought, we prevent the common issue of "ponding-induced leaks" that often occur around the perimeter of solar arrays in large retail environments.

  • Hydraulic flow analysis: Mapping the cable tray layout to ensure it does not obstruct the primary flow of water to the drains.
  • Support system specifications: Using rubberized stand-offs to prevent the metal trays from contacting the TPO membrane.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #252

OSHA-Compliant Skylight Fall-Protection Curbs & Heavy-Duty Security Screens on Commercial Food Packaging & Cold Logistics Plants

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
OSHA-Compliant Skylight Fall-Protection Curbs & Heavy-Duty Security Screens on Commercial Food Packaging & Cold Logistics Plants

Structural Engineering of 200-lb Fall-Arrest Screen Anchoring

In the high-stakes environment of food packaging and cold logistics plants, the roof is more than just a cover; it is a critical component of the building envelope that must withstand extreme temperature differentials and rigorous safety audits. A primary failure point in these facilities is the skylight opening. To meet OSHA 1910.28 and ANSI Z359 standards, we implement heavy-duty security screens designed to prevent personnel from falling through fragile skylight glazing. The engineering challenge lies in the anchoring system, which must support a concentrated point load of 200 lbs without compromising the structural integrity of the curb or the watertight seal of the roof membrane.

Our approach utilizes a reinforced steel frame anchored directly into the structural masonry or steel curb of the skylight. We avoid superficial fasteners, instead employing heavy-duty stainless steel expansion bolts or chemical anchors that distribute the load across the curb's vertical face. This ensures that in the event of a fall, the energy is transferred into the building's primary structure rather than the flashing or the glazing. The screens themselves are constructed from high-tensile galvanized steel mesh, welded to a rigid perimeter frame that prevents bowing under pressure.

  • Utilization of 316-grade stainless steel fasteners to prevent galvanic corrosion in high-humidity food processing zones.
  • Implementation of load-spreading backing plates to prevent the "pull-through" effect on thin-walled metal curbs.
  • Rigid adherence to the 200-lb impact threshold to ensure worker safety during emergency roof egress.
  • Precision-engineered tolerances to ensure the screen sits flush against the curb, eliminating gaps where debris or pests could enter.

Curb Flashing Elevation and Hydrological Management

Water infiltration at the skylight curb is the leading cause of interior mold and structural decay in cold logistics plants. Because these facilities often experience significant condensation and heavy snow loads, the curb flashing elevation must be calculated with a precision that exceeds standard commercial specifications. We mandate a minimum flashing height that accounts for the "splash-back" effect and the potential for standing water during extreme weather events. The goal is to move the termination point of the roof membrane well above the critical flood line of the roof surface.

The integration of the flashing involves a multi-stage layering process. We start with a reinforced base sheet, followed by the primary membrane, which is then wrapped up the curb and secured. To prevent capillary action—where water is drawn upward into the joint—we utilize a counter-flashing system. This ensures that gravity works in our favor, directing water away from the curb's interior and back onto the roof's drainage plane. In cold storage environments, we specifically account for the thermal expansion and contraction of the metal curb, which can shift several millimeters between the freezer interior and the exterior roof temperature.

  • Calculation of flashing heights based on local 100-year storm surge and snow drift data.
  • Application of heat-welded TPO or PVC membranes to ensure a monolithic bond to the curb.
  • Installation of drip edges on the curb perimeter to prevent water from tracking back under the flashing.
  • Verification of slope-to-drain patterns to ensure no ponding occurs at the base of the skylight assembly.

Compression Termination Bars and Mechanical Fastening

While adhesives and heat-welding are effective, they are insufficient for the high-wind uplift pressures found on large-scale industrial plants. To guarantee a permanent, airtight seal at the roof-to-wall or roof-to-curb transition, we employ heavy-duty compression termination bars. These aluminum or galvanized steel bars are mechanically fastened over the top of the membrane, effectively "sandwiching" the material against the substrate. This creates a mechanical lock that is impervious to the wind-scouring effects common in open-lot logistics hubs.

The installation process requires a disciplined fastening schedule. We utilize a staggered bolt pattern to avoid creating a "perforation line" in the substrate, which could lead to structural cracking. Each fastener is torqued to a specific tension to ensure uniform compression across the entire length of the bar. This prevents the membrane from bridging or pulling away, which is a common failure point in facilities that undergo significant thermal cycling. The result is a termination point that is not only watertight but also serves as a secondary reinforcement for the building envelope.

  • Use of continuous-strip termination bars to eliminate the risk of joint failure.
  • Application of high-grade polyurethane sealants beneath the bar to provide a secondary chemical bond.
  • Fastening intervals spaced every 12 inches to ensure consistent pressure and prevent membrane "ballooning."
  • Selection of fasteners compatible with the substrate to prevent oxidation and long-term degradation.

Thermal Gaskets and Cold Logistics Envelope Integrity

In cold logistics plants, the temperature delta between the interior freezer (often -10°F or lower) and the exterior roof can be staggering. This creates a massive thermal gradient that encourages condensation and potential ice damming at the skylight curbs. To mitigate this, we integrate high-performance thermal gaskets and closed-cell EPDM seals. These gaskets act as a thermal break, preventing the "cold bridge" effect where heat from the exterior is sucked into the facility, or interior cold leaks out, causing condensation on the roof surface.

The science of the gasket selection is critical. We utilize materials with a low compression set, meaning the gasket retains its shape and sealing ability even after years of pressure. These gaskets are positioned at the interface of the security screen and the curb, as well as within the skylight frame itself. By sealing these gaps, we prevent the infiltration of humid exterior air into the cold zone, which would otherwise lead to frost buildup on the interior of the skylight, obstructing light and creating a safety hazard for workers below.

  • Integration of closed-cell EPDM gaskets to provide an airtight seal that resists ozone and UV degradation.
  • Implementation of thermal breaks to reduce energy loss and lower operational costs for the logistics provider.
  • Use of compression-molded seals to ensure a tight fit regardless of the curb's surface irregularities.
  • Regular audit of gasket elasticity to ensure the envelope remains sealed against the pressures of extreme temperature swings.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #253

Rooftop Mechanical Unit Vibration Isolation Rails & Spring-Mounted Curb Seals on Commercial Semiconductor Cleanroom Fabs

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Rooftop Mechanical Unit Vibration Isolation Rails & Spring-Mounted Curb Seals on Commercial Semiconductor Cleanroom Fabs

The Engineering Challenge of Semiconductor Fab Envelopes

In the realm of commercial roofing, few environments demand as much precision as a semiconductor cleanroom fabrication plant. These facilities are not merely buildings; they are highly tuned instruments where a single micron of dust or a slight tremor in the floor slab can result in millions of dollars in lost wafer yield. The building envelope, therefore, must perform a dual role: it must provide an absolute, watertight seal against the elements while simultaneously managing the massive mechanical loads and kinetic energy generated by industrial-scale HVAC and air filtration systems.

The primary conflict in these installations arises from the juxtaposition of rigidity and flexibility. A standard commercial roof is designed to shed water and withstand wind uplift, typically relying on a tight, adhered, or mechanically fastened membrane. However, the massive chillers, cooling towers, and air handling units (AHUs) required for cleanroom climate control generate significant harmonic vibrations. If these units are bolted directly to the structural deck, the resulting resonance can cause fatigue cracking in the roof membrane and, more critically, transmit vibrations into the cleanroom environment, disrupting the lithography process.

  • Requirement for zero-leakage tolerance to prevent moisture-driven contamination of the cleanroom.
  • Management of extreme point loads from heavy mechanical equipment.
  • Mitigation of structural resonance to protect sensitive fabrication equipment.
  • Integration of disparate materials, including galvanized steel, TPO or PVC membranes, and high-performance polymers.

Harmonic Vibration Mitigation and Spring-Isolated Curb Assemblies

To solve the vibration dilemma, we implement spring-isolated equipment curbs and isolation rails. Rather than a static curb, these systems utilize heavy-duty steel rails supported by calibrated helical steel springs. These springs act as a mechanical filter, absorbing the kinetic energy of the equipment's compressors and fans before that energy can migrate into the building's structural steel or concrete slab. From an engineering perspective, this is a matter of shifting the natural frequency of the system away from the operating frequency of the machinery.

The installation of these rails requires a master-level understanding of load distribution. We ensure that the isolation rails are seated on reinforced concrete housekeeping pads that are chemically decoupled from the primary roof deck. This prevents the "drumming" effect where the roof membrane acts as a diaphragm, amplifying sound and vibration. By isolating the equipment, we not only protect the internal cleanroom processes but also extend the lifespan of the roof membrane by reducing the constant mechanical rubbing and shearing forces at the curb interface.

  • Utilization of open-spring isolators to prevent the transmission of acoustic energy.
  • Precision leveling of isolation rails to ensure uniform load distribution across the spring array.
  • Implementation of neoprene pads as secondary damping layers to eliminate high-frequency "chatter."
  • Calculation of static deflection to ensure the equipment remains stable during seismic events or high-wind loads.

Advanced Sealant Science: Fiber-Reinforced Structural Mastic

The most critical failure point in any rooftop mechanical installation is the transition zone—the gap where the vibrating equipment curb meets the static roof membrane. Traditional caulking or standard silicone sealants are insufficient here; they lack the tensile strength to withstand the constant micro-movements of a spring-isolated system. For these applications, we specify fiber-reinforced structural mastic. This material is engineered with a high concentration of synthetic fibers that provide internal reinforcement, allowing the sealant to stretch and recover without tearing or "alligatoring."

The application of this mastic must follow a rigorous substrate preparation protocol. We employ a multi-stage cleaning process to remove all contaminants, followed by the application of a high-tack primer to ensure a chemical bond between the metal rail and the roof membrane. The mastic is then applied in a wide, overlapping bead that creates a flexible, waterproof bridge. This bridge is designed to accommodate the coefficient of thermal expansion differences between the steel rails and the polymer roof membrane, ensuring that as the building breathes and the equipment vibrates, the watertight seal remains unbroken.

  • Application of ASTM-compliant elastomeric mastics with high movement capability (up to 50% elongation).
  • Integration of non-woven polyester reinforcement fabrics embedded within the mastic for added shear resistance.
  • Strict adherence to cure-time protocols to prevent premature exposure to moisture.
  • Verification of bond strength through destructive and non-destructive field testing.

Audit Findings and Long-Term Watertight Integrity

A comprehensive engineering audit of a semiconductor fab roof reveals that the longevity of the envelope depends entirely on the integrity of the flashing and the maintenance of the vibration seals. During our inspections, we look for signs of "fatigue cracking" around the perimeter of the spring-mounted curbs. If the isolation system is failing or if the mastic has lost its elasticity, we see small, hairline fractures that allow moisture to penetrate via capillary action. In a cleanroom environment, this is unacceptable, as moisture ingress can lead to mold growth or humidity spikes that compromise the fab's atmospheric controls.

The final layer of protection is a rigorous maintenance schedule that includes infrared thermography to detect trapped moisture and ultrasonic testing to ensure the vibration isolators are still operating within their specified frequency range. By treating the rooftop mechanical units not as separate entities, but as integrated components of the building envelope, we ensure a seamless transition from the structural steel to the final waterproof membrane. This holistic approach is the hallmark of master craftsmanship in commercial roofing, blending material science with mechanical engineering to protect the most sensitive industrial environments on earth.

  • Quarterly infrared scanning to identify subsurface moisture accumulation around curbs.
  • Annual torque verification of all isolation rail fasteners to prevent bolt loosening from vibration.
  • Visual inspection of mastic seals for signs of UV degradation or ozone cracking.
  • Recalibration of spring mounts if equipment loads change due to mechanical upgrades.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #254

Industrial Corrosive Chemical Fume Exhaust Defense on Commercial Intermodal Cargo Freight Terminals

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Industrial Corrosive Chemical Fume Exhaust Defense on Commercial Intermodal Cargo Freight Terminals

Chemical Load Analysis and Environmental Site Audit

In the high-stakes environment of an intermodal cargo freight terminal, the building envelope is subjected to a relentless chemical assault that far exceeds the parameters of standard commercial warehousing. A comprehensive engineering audit reveals that the primary threats are not merely weather-related but are systemic chemical stressors originating from heavy machinery and industrial maintenance. The presence of battery charging stations for electric forklifts and heavy-duty freight handlers introduces sulfuric acid fumes into the immediate atmosphere. These fumes, when combined with ambient humidity, create a corrosive condensate that settles on the roof membrane, leading to premature degradation of polymer chains.

Furthermore, the constant idling of diesel-powered locomotives and drayage trucks contributes a dense layer of hydrocarbon particulates and motor oil mists. These oils act as solvents that can penetrate the surface of a poorly specified membrane, leading to a phenomenon known as chemical softening. When these oils interact with the roof surface, they do not simply sit on top; they migrate into the material, altering its physical properties and compromising the integrity of the welded seams. A master roofer knows that the failure of a roof in this environment is rarely a result of a single puncture, but rather a systemic failure of the material's chemical resistance.

  • Sulfuric acid condensate from industrial battery arrays.
  • Hydrocarbon saturation from diesel exhaust and vaporized motor oils.
  • Atmospheric pollutants and particulate matter from intermodal rail traffic.
  • Thermal cycling exacerbated by high-albedo requirements for energy efficiency.
  • Hygroscopic salt accumulation from winter de-icing agents tracked into the facility.

Plasticizer Migration and Polymer Stability

One of the most critical engineering challenges in this scenario is the retention of plasticizers within the roofing membrane. Plasticizers are the essential additives that keep thermoplastic membranes, such as PVC, flexible and resilient. However, in a freight terminal environment, the presence of industrial oils and chemical fumes triggers a process called plasticizer migration. The oils act as a catalyst, drawing the plasticizers out of the membrane and into the surrounding environment or the underlying substrate. This results in a catastrophic loss of elasticity, causing the membrane to become brittle and prone to "alligatoring" or stress cracking.

From a material science perspective, the loss of these additives leads to a significant increase in the modulus of elasticity, meaning the roof can no longer expand and contract with the building's natural thermal movements. Once the plasticizer levels drop below a critical threshold, the membrane loses its ability to bridge small gaps or accommodate the movement of the structural steel. This brittleness is particularly dangerous at the points of attachment and around mechanical penetrations, where the physical stress is highest. An authoritative audit must evaluate the membrane's current state using a durometer test to ensure the polymer has not reached a state of permanent embrittlement.

  • Accelerated leaching of phthalates due to hydrocarbon exposure.
  • Increase in material brittleness leading to micro-fractures in the field of the roof.
  • Loss of tensile strength at the welded seams and lap joints.
  • Reduction in puncture resistance as the polymer matrix collapses.
  • Differential movement failure between the rigid membrane and the flexible building frame.

Membrane Selection and Engineering Specifications

Selecting the correct membrane for a corrosive chemical environment requires a departure from standard TPO (Thermoplastic Olefin) applications. While TPO is cost-effective, it often lacks the inherent chemical resistance required to withstand concentrated acid fumes and oil saturation. For an intermodal terminal, a high-performance, reinforced PVC (Polyvinyl Chloride) membrane or a specialized modified bitumen system with a chemical-resistant cap sheet is mandatory. PVC is naturally more resistant to the corrosive effects of acids and bases, provided the grade is specifically engineered for industrial chemical exposure. The reinforcement scrim must be a high-strength polyester to ensure dimensional stability under extreme thermal loads.

Engineering specifications must adhere to ASTM and ANSI standards for chemical compatibility. The selection process should prioritize membranes that demonstrate low permeability to hydrocarbons and high resistance to acid-induced hydrolysis. Furthermore, the integration of a non-woven polyester reinforcement layer helps distribute mechanical stresses across the roof surface, preventing the localized failures common in non-reinforced membranes. The goal is to create a monolithic shield that is chemically inert to the specific pollutants identified during the site audit, ensuring that the building envelope remains an impenetrable barrier against the elements and industrial byproducts.

  • Preference for reinforced PVC over TPO for superior acid and oil resistance.
  • Implementation of ASTM-certified chemical resistance testing for all specified materials.
  • Utilization of high-density polyester scrims to prevent membrane stretching and deformation.
  • Selection of high-albedo coatings to reduce thermal gain without sacrificing chemical stability.
  • Requirement for heat-welded seams to eliminate the reliance on chemical adhesives that may degrade.

Execution, Detailing, and Lifecycle Defense

The most advanced material selection is useless without master-level installation and detailing. In a chemical fume environment, the "critical interfaces"—such as exhaust vent flashing, curb details, and drainage points—are the first areas to fail. The exhaust stacks for chemical fumes must be flashed with a specialized chemical-resistant flashing membrane and sealed with a high-grade industrial sealant that is compatible with the primary roof membrane. A common failure point is the use of incompatible sealants that react with the PVC, leading to a "melt-back" effect that opens a direct path for water and chemicals to enter the building envelope.

A lifecycle defense strategy requires a rigorous maintenance schedule that includes periodic chemical neutralizing washes. Because acid fumes can build up on the roof surface, a scheduled cleaning regimen prevents the accumulation of corrosive salts and oils. Furthermore, the installation of a comprehensive drainage system is essential to ensure that contaminated rainwater does not pond on the roof, as standing water increases the rate of chemical penetration. By combining precision craftsmanship with a proactive engineering approach, the building envelope is transformed from a passive cover into an active defense system, extending the service life of the asset and protecting the critical infrastructure of the intermodal terminal.

  • Precision heat-welding of all seams with continuous electronic leak detection.
  • Custom-fabricated flashing for all chemical exhaust penetrations to ensure a gastight seal.
  • Application of a chemical-resistant liquid-applied flashing at all complex transitions.
  • Implementation of a quarterly chemical wash to remove acidic deposits

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #255

Active Emergency Leak Catchment Tarps & Interior Production Bay Diversion on Commercial Port Marine Shipping Warehouses

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Active Emergency Leak Catchment Tarps & Interior Production Bay Diversion on Commercial Port Marine Shipping Warehouses

The Anatomy of Port Marine Envelope Failure

In the high-stakes environment of port marine shipping warehouses, the building envelope is under constant assault from a corrosive maritime microclimate. The combination of salt-laden air, extreme wind-driven rain, and significant thermal cycling creates a volatile condition for commercial roofing systems. When a breach occurs in a large-span warehouse roof, the result is rarely a simple drip; it is often a systemic failure of the flashing or the primary membrane, leading to high-volume water intrusion that threatens millions of dollars in high-value cargo and sensitive electronic logistics equipment.

The primary challenge in these facilities is the sheer scale of the roof area, which often masks the exact point of entry due to internal wind currents and the migration of water along structural steel beams. This phenomenon, known as capillary action and tracking, means that a leak appearing in a production bay may actually originate fifty feet away at a compromised curb or a failed penetration seal. An engineering audit of these sites typically reveals that the most critical failure points are the parapet caps and the transition zones where the roof meets the vertical wall, where hydrostatic pressure forces water beneath the flashing during storm events.

  • Atmospheric salt crystallization which degrades the chemical bonds of older modified bitumen membranes.
  • Wind-scour effects that strip away protective granules or tear TPO seams at the perimeter.
  • Thermal expansion and contraction of long-span steel decking, leading to fatigue cracks in the flashing.
  • Clogged internal drainage systems that cause ponding, increasing the likelihood of membrane puncture.

Engineering the Diversion Strategy and Material Science

When an active leak is identified in a production bay, the immediate priority is not the permanent patch—which may be impossible during a storm—but the implementation of a strategic diversion system. For Aquashield Corporate, we move beyond consumer-grade plastics and deploy industrial-grade, heavy-duty vinyl diverter tarps. These are not standard poly-tarps; they are high-denier PVC-coated polyester fabrics engineered for extreme tensile strength and puncture resistance. The material science behind these diverters ensures that they can withstand the weight of pooled water without stretching or tearing, maintaining the structural integrity of the catchment area.

The selection of material is governed by the need for a non-porous, hydrophobic surface that allows water to slide rapidly toward the collection point. We utilize 18oz to 22oz vinyl, which provides the necessary durability to resist abrasion from the underside of the roof deck. Furthermore, these materials are treated for UV stability and chemical resistance, ensuring that they do not degrade if the emergency diversion remains in place for several weeks during the procurement of permanent replacement materials. The goal is to create a temporary, waterproof "skin" beneath the failure point that mimics the performance of the primary roof membrane.

  • Utilization of heat-welded seams over stitched edges to prevent leakage at the joints.
  • Application of reinforced grommets and heavy-duty webbing for secure mechanical fastening.
  • Selection of materials meeting ASTM standards for water vapor transmission and tear strength.
  • Implementation of a high-gloss finish to reduce friction and accelerate water runoff.

Deployment Logistics and Drainage Routing

The installation of a catchment system in a production bay requires a precise understanding of gravity and fluid dynamics. A common mistake in emergency roofing is simply hanging a tarp; without proper tension and slope, the tarp will "belly," creating a secondary ponding issue that can lead to a catastrophic collapse of the diversion system. Our engineering approach involves the "Catch-and-Channel" method. We secure the vinyl diverter at a high point and create a calculated pitch, ensuring that water is directed away from high-value machinery, electrical panels, and shipping containers.

Routing is the most critical phase of the deployment. We utilize industrial-grade PVC piping or flexible reinforced hoses attached to the lowest point of the vinyl catchment. This creates a closed-loop system that transports the intruding water directly to a floor drain or an exterior discharge point. By controlling the path of the water, we eliminate the risk of "splash-over" and ensure that the production bay remains operational. The fastening systems used are non-invasive to the primary structure, utilizing heavy-duty clamps and tensioning straps that distribute the load across the structural steel, preventing localized stress points.

  • Establishment of a minimum 2% slope within the diverter tarp to prevent water stagnation.
  • Strategic placement of "drip edges" to ensure water does not track back along the underside of the tarp.
  • Integration of temporary collection drums with overflow sensors for high-volume events.
  • Use of mechanical tensioners to eliminate fabric oscillation caused by warehouse HVAC systems.

Long-term Remediation and Envelope Stabilization

Once the emergency diversion system has stabilized the interior environment, the focus shifts from triage to permanent engineering remediation. An emergency tarp is a bandage, not a cure. The final phase of the Aquashield protocol involves a comprehensive building envelope audit using infrared thermography to identify hidden moisture pockets within the insulation. This allows us to determine if the leak was an isolated puncture or a systemic failure of the flashing detail. We then transition from the temporary vinyl diversion to a permanent, reinforced membrane system, often utilizing a liquid-applied PMMA or a fully adhered TPO system for superior wind-uplift resistance.

The transition from emergency catchment to permanent repair must be seamless. We ensure that all flashing is integrated according to ANSI standards, providing a redundant layer of protection at the most vulnerable points of the warehouse. The final stabilization includes the installation of high-performance sealants at all penetration points and the reinforcement of parapet caps. By documenting the failure point and the success of the diversion strategy, we provide the client with a forensic analysis that informs future preventative maintenance schedules, reducing the likelihood of future emergency interventions.

  • Conducting moisture scans to ensure the roof deck is fully dried before applying new membranes.
  • Upgrading flashing details to exceed minimum building code requirements for coastal zones.
  • Implementing a scheduled quarterly audit of all roof penetrations and drainage outlets.
  • Installing permanent flashing reinforcements at high-stress transition points.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #256

Cold-Weather Induction Welded Membrane Attachments on Commercial Municipal Sports & Convention Arenas

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Cold-Weather Induction Welded Membrane Attachments on Commercial Municipal Sports & Convention Arenas

Thermal Dynamics and Substrate Interface in Cold-Weather Environments

When auditing the building envelope of a municipal sports and convention arena, the primary engineering challenge is the massive surface area coupled with extreme thermal fluctuations. In cold-weather scenarios, the coefficient of thermal expansion for thermoplastic membranes—such as TPO or PVC—creates a significant risk of shrinkage and tension at the seams. In a municipal arena, where the roof spans hundreds of thousands of square feet, the cumulative movement can lead to premature failure if the attachment method is not precisely engineered for low-ambient temperatures.

The substrate interface is where most failures originate. In sub-zero conditions, the membrane becomes less pliable, increasing the likelihood of "bridging" over fasteners or structural ribs. To mitigate this, our engineering approach focuses on the molecular bonding of the membrane to the plate. Traditional hot-air welding often fails in these conditions because the ambient air strips heat away from the weld zone too quickly, resulting in a "cold weld" that lacks the necessary fusion to withstand structural movement.

  • Analysis of substrate temperature to ensure it remains within the manufacturer's specified bonding window.
  • Evaluation of membrane plasticity and the risk of stress-cracking during the deployment phase.
  • Assessment of thermal bridging where structural steel penetrates the insulation layer, creating localized cold spots.
  • Verification of the chemical compatibility between the membrane compound and the induction-ready bonding plates.

Precision Calibration of Electromagnetic Induction Tooling

To overcome the limitations of convective heat, we employ electromagnetic induction welding. Unlike traditional methods, induction welding uses a high-frequency alternating current to create an electromagnetic field, which induces eddy currents directly within the metallic bonding plate. This generates heat internally and instantaneously, ensuring that the fusion occurs from the bottom up, regardless of the freezing air temperature surrounding the roof surface.

The critical engineering variable here is tool temperature calibration. If the induction tool is under-calibrated, the membrane will not reach its melting point, leading to a lack of fusion. Conversely, over-calibration can lead to polymer degradation, where the membrane is scorched, destroying its UV-resistant properties and creating a brittle point of failure. We utilize a closed-loop feedback system to maintain a precise temperature window, typically calibrated to within two degrees of the material's optimal fusion point.

  • Implementation of real-time pyrometry to monitor the interface temperature during the weld cycle.
  • Calibration of the induction frequency to ensure deep penetration through the membrane thickness.
  • Adjustment of the dwell time based on the specific gauge of the membrane and the conductivity of the plate.
  • Verification of the "weld-through" consistency across the entire surface area of the bonding plate.

Weighted Magnetic Cooling Clamping and Weld Integrity

The most overlooked phase of the induction process is the cooling cycle. In a high-wind, cold-weather environment, the rapid dissipation of heat can cause the membrane to pull away from the plate before the molecular bond has fully crystallized. This creates a void or a "fish-mouth" in the seam, which compromises the water-tight integrity of the building envelope. To prevent this, we utilize weighted magnetic cooling clamps that provide constant, uniform pressure during the critical cooling phase.

These clamps serve a dual purpose: they ensure the membrane remains in intimate contact with the heated plate and they regulate the rate of cooling. By slowing the cooling process slightly, we allow the polymer chains to align more effectively, resulting in a weld that is often stronger than the surrounding virgin material. This process is essential for municipal arenas, where the roof is subject to significant vibration from HVAC systems and the movement of thousands of occupants below.

  • Application of magnetic clamps to maintain a constant 50-psi pressure on the weld zone.
  • Monitoring of the cooling curve to ensure the transition from liquid to solid state occurs without shrinkage.
  • Use of non-marring weighted plates to avoid puncturing the membrane during the clamping process.
  • Sequential clamping patterns to prevent the accumulation of lateral tension across the roof plane.

Wind Uplift Analysis and Long-Term Envelope Stability

The ultimate metric of success for any commercial roofing system is its ability to withstand wind uplift. For large-span arenas, the "parachute effect" can create immense suction forces on the roof membrane. Our engineering audit focuses on the peel strength of the induction-welded attachments compared to traditional mechanical fastening. By utilizing electromagnetic bonding, we distribute the wind load across a wider surface area, reducing the stress concentrations that typically lead to fastener pull-out.

Following the installation, we conduct rigorous testing in accordance with ASTM and ANSI standards. This includes vacuum testing and pull-tests to verify that the bond strength exceeds the calculated wind-load requirements for the specific geographic region. The result is a monolithic building envelope where the membrane and the attachment plates function as a single structural unit. This not only increases the lifespan of the roof but significantly reduces the maintenance overhead for the municipality.

  • Calculation of maximum wind-load pressures based on the arena's height and surrounding topography.
  • Execution of destructive peel tests on sample coupons to verify the fusion quality.
  • Assessment of the "edge-lift" resistance at the perimeter of the roof, where wind turbulence is highest.
  • Long-term monitoring of the membrane's tensile stability under varying thermal loads.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #257

48-Hour Drain Bowl Hydrostatic Flood Testing & Manufacturer 20-Year NDL Audits on Commercial Multi-Family Urban Residential Towers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
48-Hour Drain Bowl Hydrostatic Flood Testing & Manufacturer 20-Year NDL Audits on Commercial Multi-Family Urban Residential Towers

The Engineering Logic of Hydrostatic Flood Testing in Urban High-Rises

In the realm of commercial building envelope engineering, a visual inspection is merely a preliminary survey. For multi-family urban residential towers, where a single leak can migrate through twenty floors of luxury finishes and structural concrete, the margin for error is zero. The 48-hour hydrostatic flood test represents the gold standard in verifying the integrity of a roofing system. Unlike a simple hose test, which only targets specific flashing points, a full-scale hydrostatic test subjects the entire membrane assembly to a consistent column of water, simulating extreme weather events and identifying systemic failures in the field.

The primary objective is to establish a controlled environment where the membrane is under constant hydrostatic pressure. By filling the roof deck to a depth of 2 to 4 inches, we create a "head" of pressure that forces water into any microscopic void, pinhole, or improperly fused weld. This process is governed by the principles of fluid dynamics; the water seeks the path of least resistance, ensuring that any vulnerability in the membrane—whether it be a failed seam or a compromised penetration—is revealed before the manufacturer's final audit.

  • Verification of membrane continuity across expansive urban roof footprints.
  • Identification of substrate depressions that may lead to premature ponding and membrane fatigue.
  • Validation of the flashing integrity around complex HVAC curbs and parapet walls.
  • Simulation of extreme precipitation events to ensure the building envelope remains impermeable.

Technical Execution of Drain Bowl Plugging and Pressure Retention

The execution of a drain bowl test requires precision craftsmanship and an understanding of the internal drainage architecture. To transform a functional roof into a testing reservoir, the primary drains must be temporarily plugged using engineered mechanical plugs. These plugs must be seated firmly to prevent "seepage leakage," which could be mistaken for a membrane failure. Once the primary drains are sealed, water is introduced across the deck until the desired depth is achieved, typically maintaining a minimum of two inches of cover over the highest point of the roof.

The critical phase of this operation is the 48-hour retention window. During this period, the water level is monitored using calibrated gauges. A drop in water level that exceeds the calculated evaporation rate indicates a breach in the envelope. We analyze the rate of decline to determine if the leak is a "catastrophic" failure—such as a missed seam—or a "capillary" failure, where water is being drawn through a microscopic void via surface tension. This diagnostic phase is essential for pinpointing the exact location of the failure without having to tear up large sections of the membrane.

  • Installation of heavy-duty mechanical plugs in primary and secondary scuppers.
  • Controlled flooding using high-volume pumps to avoid localized "washing" of the membrane.
  • Continuous monitoring of water levels using graduated cylinders or electronic sensors.
  • Calculation of evaporation offsets based on ambient temperature and humidity.

Critical Analysis of Membrane Flange Welds and Thermal Fusion

The most vulnerable point of any commercial roofing system is the interface between the membrane and the drain flange. In urban residential towers, the thermal expansion and contraction cycles are extreme, placing immense stress on these welds. We focus our audit on the thermal fusion process, specifically looking for "cold welds" where the heat welder did not reach the required temperature to achieve a molecular bond between the TPO or PVC layers. A proper weld should exhibit a seamless transition, showing a slight "bead" of melted material that indicates a complete fusion of the polymers.

Using a calibrated probe, our specialists perform a physical audit of every flange weld. We are looking for any sign of shrinkage or separation at the heel of the weld. If the hydrostatic test reveals moisture at the drain bowl, it is often a sign that the flange was not properly seated or that the membrane was stretched too thin during the wrapping process. Material science dictates that any tension placed on the membrane during the welding process will eventually lead to a stress crack; therefore, we verify that the membrane was "relaxed" into the drain bowl before the final heat-set was applied.

  • Inspection of weld temperatures to ensure adherence to manufacturer specifications.
  • Probe testing of all perimeter seams and flashing laps to identify voids.
  • Analysis of the "overlap" width to ensure it meets the minimum ANSI standards for commercial roofing.
  • Evaluation of the mechanical fastening system to ensure it supports the membrane without creating puncture points.

The Path to the 20-Year NDL Warranty and Final Sign-Off

The culmination of the engineering audit is the transition from a completed installation to a certified 20-year No Dollar Limit (NDL) warranty. An NDL warranty is the highest tier of protection available in the industry, meaning the manufacturer assumes all costs for labor and materials for the duration of the term. However, manufacturers will not issue an NDL sign-off without a rigorous audit trail. This includes the documented results of the 48-hour hydrostatic test, the weld logs, and the final building envelope survey.

Our role as specialists is to act as the bridge between the installation crew and the manufacturer's representative. We ensure that every detail—from the lap-seam width to the flashing of the parapet caps—is executed to a master-craftsman standard. The final audit involves a comprehensive walkthrough where every drain is unplugged, the roof is allowed to drain naturally to verify the slope and flow, and a final "dry-walk" is performed to ensure no debris or fasteners were left behind. Only after these stringent criteria are met do we submit the engineering packet for the 20-year warranty certification.

  • Compilation of hydrostatic pressure logs and evaporation data for manufacturer review.
  • Final verification of all penetration flashings and termination bars.
  • Coordination of the manufacturer's representative for the final site inspection.
  • Formal issuance of the NDL warranty, securing the asset's value for the building owner.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #258

Masonry Parapet Counterflashing Reglet Overhauls & Polyurethane Sealant Compression on Commercial Public Transit Maintenance Bus Barns

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Masonry Parapet Counterflashing Reglet Overhauls & Polyurethane Sealant Compression on Commercial Public Transit Maintenance Bus Barns

Failure Analysis of Legacy Parapet Interfaces in Transit Facilities

In the rigorous environment of a public transit maintenance bus barn, the building envelope is subjected to extreme stressors that standard commercial warehouses rarely encounter. During our engineering audit, we identified a systemic failure at the masonry parapet transitions. The primary catalyst for water ingress was the degradation of legacy counterflashing, which had been installed as a surface-mounted strip rather than a true embedded reglet system. Over time, the differential thermal expansion coefficients between the masonry substrate and the metal flashing caused the original sealant joints to fatigue and shear, creating direct pathways for hydrostatic pressure to drive moisture into the wall assembly.

The bus barn environment introduces additional variables, including heavy diesel exhaust particulates and constant vibrations from heavy vehicle movement. These factors accelerate the carbonation of mortar joints and the embrittlement of low-grade sealants. When the parapet cap fails to shed water effectively, the resulting "wash-down" effect saturates the masonry, leading to efflorescence and the eventual spalling of the brick face. To resolve this, a comprehensive overhaul of the reglet system was required to ensure a watertight transition that adheres to ASTM E2112 standards for moisture-resistive barriers.

  • Identification of capillary suction within porous masonry substrates.
  • Analysis of thermal bridging at the roof-to-wall interface.
  • Evaluation of sealant failure due to UV degradation and chemical exposure from bus exhaust.
  • Assessment of structural vibrations causing micro-fissures in legacy mortar joints.

Precision Reglet Engineering and Mortar Joint Preparation

The core of the remediation strategy involves the creation of a precision-engineered reglet—a recessed groove cut directly into the masonry to house the counterflashing. This is not a mere cutting operation but a surgical extraction of mortar to ensure the metal is fully embedded. Using industrial-grade diamond grinding equipment, our teams executed a controlled grind of the horizontal mortar joints. The objective was to create a consistent 3/8-inch deep by 1/2-inch wide channel, ensuring that the flashing sits flush with the masonry face to eliminate any ledge where water could pool.

Precision is paramount during this phase; over-grinding can compromise the structural integrity of the masonry wythe, while under-grinding leads to "proud" flashing that fails to provide the necessary overlap with the roofing membrane. We utilized laser-leveling tools to ensure the reglet remained perfectly horizontal across the entire perimeter of the bus barn. This ensures that the counterflashing maintains a uniform distance from the roof surface, allowing for proper drainage and preventing the metal from "bottoming out" against the membrane, which would otherwise cause premature wear and puncture.

  • Utilization of variable-speed diamond grinders to prevent masonry fracturing.
  • Strict adherence to a 3/8-inch depth specification for optimal flashing seating.
  • Mechanical cleaning of the reglet using compressed air and wire brushes to remove all debris.
  • Verification of reglet linearity to ensure seamless metal installation.

Material Science of Heavy-Gauge Kynar and Polyurethane Compression

For the counterflashing material, we specified heavy-gauge steel finished with a Kynar 500 (PVDF) coating. In a transit facility, the resilience of the finish is critical. Kynar is selected not for its aesthetics, but for its superior resistance to atmospheric pollutants and its ability to maintain a hard, non-porous surface that resists the adhesion of grime and oils. The heavy gauge is essential to prevent "oil-canning" or warping under the extreme temperature swings common in open-bay maintenance facilities. This rigidity ensures that the flashing maintains its geometry, providing a consistent drip edge that directs water away from the building envelope.

The critical engineering component of this assembly is the polyurethane sealant compression. Unlike standard silicone, high-modulus polyurethane sealants provide the necessary elasticity to accommodate the movement between the metal and the masonry. We implemented a "two-stage" sealing process. First, a backing rod was inserted to control the depth of the sealant and prevent three-sided adhesion. Then, the polyurethane was injected under pressure into the reglet. As the sealant cures, it creates a compressed gasket effect, effectively locking the Kynar flashing into the masonry. This compression ensures that the joint remains watertight even as the building undergoes thermal expansion and contraction.

  • Specification of Kynar 500 for maximum chemical and UV resistance.
  • Application of heavy-gauge metal to withstand wind-uplift and mechanical vibration.
  • Use of closed-cell backing rods to ensure proper sealant joint geometry.
  • Implementation of high-modulus polyurethane for superior bond strength and elasticity.

System Validation and Long-Term Envelope Integrity

The final phase of the overhaul is the rigorous validation of the building envelope. A counterflashing system is only as successful as its weakest point; therefore, we conducted a comprehensive water-penetration test. This involved applying a controlled spray to the parapet face to simulate a high-wind rain event. By monitoring the interior side of the masonry wall with infrared thermography, we were able to confirm that the polyurethane compression seals were holding and that no moisture was migrating into the wall cavity. This data-driven approach confirms that the reglet overhaul has successfully eliminated the leak paths.

From an engineering perspective, the integration of the counterflashing with the underlying roofing membrane is the final line of defense. The Kynar flashing was installed with a minimum 2-inch overlap over the membrane, creating a redundant shedding system. By shifting the water-shedding responsibility from a surface-level sealant bead to an embedded mechanical system, we have significantly extended the lifecycle of the roof. The result is a hardened envelope that protects the transit facility's interior assets, reduces maintenance overhead, and ensures the structural longevity of the masonry parapets.

  • Execution of ASTM-standard hose tests to verify water-tightness.
  • Infrared thermographic scanning to detect hidden moisture pockets.
  • Verification of the 2-inch minimum overlap for redundant water shedding.
  • Establishment of a long-term maintenance schedule for sealant inspection every 60 months.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #259

Flute-Fill EPS/Polyiso Insulation Sizing for Standing Rib Metal Roof Retrofits on Commercial Government Secure Records Archives

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Flute-Fill EPS/Polyiso Insulation Sizing for Standing Rib Metal Roof Retrofits on Commercial Government Secure Records Archives

The Engineering Challenge of Corrugated Substrates in Secure Archives

When conducting a building envelope audit for a Government Secure Records Archive, the stakes extend beyond simple leak prevention. These facilities house irreplaceable historical and legal documents that require stringent climate control and a near-zero tolerance for interstitial condensation. The primary architectural challenge encountered in these retrofits is the existing standing rib metal roof system. While structurally sound, the corrugated profile of the metal decking creates significant voids that act as conduits for uncontrolled air infiltration and thermal bypass.

In a standard retrofit, many contractors make the mistake of laying insulation boards directly over the ribs, leaving the "flutes" or valleys of the metal empty. This creates a fragmented thermal envelope where the R-value is inconsistent across the roof plane. For a secure archive, this inconsistency leads to localized cold spots, which can trigger condensation events on the interior ceiling, potentially risking mold growth or water damage to sensitive records. To achieve a truly high-performance envelope, the engineering focus must shift from simple coverage to total volume displacement within the metal profile.

  • Identification of thermal bypass zones within the standing rib valleys.
  • Analysis of dew point calculations to prevent interior condensation in secure zones.
  • Evaluation of existing fastener integrity to ensure the substrate can support additional insulation loads.
  • Assessment of the building's overall air leakage rate through the roof-to-wall transitions.

Precision-Cut Flute-Fill Engineering and Material Selection

To eliminate the voids inherent in corrugated metal, we employ a precision-cut flute-fill strategy. This involves the fabrication of insulation inserts specifically sized to the exact geometry of the roof's ribs. We utilize a hybrid approach combining Expanded Polystyrene (EPS) and Polyisocyanurate (Polyiso). The EPS is often utilized for its dimensional stability and ability to be precision-cut into rigid blocks that slide perfectly into the flutes, while the Polyiso provides the high thermal resistance (R-value) required to meet modern energy codes and government mandates.

The sizing of these inserts is a matter of microns. If the flute-fill is too loose, air can circulate around the insulation, rendering the thermal break ineffective. If it is too tight, the resulting compression can compromise the R-value of the Polyiso or, worse, induce structural stress on the metal decking. Our process involves a comprehensive field measurement of the rib height, width, and pitch, followed by the use of CNC-cut profiles that ensure a friction-fit seal. This creates a continuous thermal mass that transforms the corrugated surface into a functionally flat substrate.

  • Utilization of CNC-routed EPS for exact geometry matching of the standing rib profile.
  • Strategic layering of Polyiso to achieve a targeted R-30 or R-40 rating across the entire assembly.
  • Implementation of a "compression-fit" tolerance to ensure zero gaps between the insulation and the metal flange.
  • Application of high-density adhesives at the flute edges to prevent wind-scour and air migration.

Mitigating Thermal Bridging and Vapor Drive

Thermal bridging occurs when a highly conductive material—in this case, the steel roof decking—creates a path for heat to bypass the insulation. In a secure archive, thermal bridging is the primary enemy of the HVAC system. When the metal ribs are not filled, the steel acts as a radiator, pulling heat out of the building in winter and pushing it in during summer. By filling the flutes, we effectively break this bridge, ensuring that the heat flow is perpendicular to the roof surface rather than lateral through the metal. This is critical for maintaining the stable Relative Humidity (RH) levels required for archival preservation.

Furthermore, the flute-fill system addresses the issue of vapor drive. In uninsulated voids, warm, moist interior air can migrate upward and condense against the cold underside of the metal roof. This moisture then drips back onto the ceiling, often undetected until significant damage has occurred. By filling the void with closed-cell Polyiso and EPS, we eliminate the air space where condensation occurs. The insulation acts as both a thermal barrier and a vapor retarder, forcing the dew point to occur outside the building's interior envelope and protecting the secure records below.

  • Reduction of the "Cold Bridge" effect by eliminating air pockets within the metal profile.
  • Stabilization of interior surface temperatures to prevent localized condensation.
  • Alignment with ASTM C1224 standards for thermal performance of roof insulation.
  • Prevention of convective loops that typically occur in empty corrugated valleys.

Final Membrane Integration and System Validation

Once the flute-fill insulation is seated and a leveling course of Polyiso is installed over the top, the roof is effectively converted from a corrugated surface to a flat, monolithic plane. This allows for the installation of a single-ply membrane—typically a reinforced TPO (Thermoplastic Polyolefin) or PVC—without the need for complex rib-strips or oversized flashing. The membrane is mechanically attached or fully adhered, depending on the wind-uplift requirements of the specific government site. Because the substrate is now level, the membrane can be welded with maximum precision, ensuring a watertight seal across the entire expanse.

The final phase of the engineering process is system validation. We do not rely on visual inspection alone. To ensure the integrity of the secure archive's envelope, we employ infrared thermography to scan the roof for any remaining thermal leaks. Any "hot" or "cold" spots identified during the thermographic scan are addressed immediately. This rigorous approach ensures that the building envelope operates as a single, cohesive unit, providing the long-term security and environmental stability that government records demand.

  • Installation of a reinforced single-ply membrane over a leveled insulation substrate.
  • Execution of heat-welded seams to ensure a monolithic, waterproof barrier.
  • Conducting infrared thermographic audits to verify the absence of thermal bridging.
  • Final validation of the vapor barrier continuity from the roof deck to the parapet walls.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #260

Structural Plywood Deck Re-Nailing Schedules on Commercial Pharmaceutical Production Facilitys

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Structural Plywood Deck Re-Nailing Schedules on Commercial Pharmaceutical Production Facilitys

Engineering Audit of Coastal Wind Uplift Dynamics in Pharmaceutical Facilities

In the specialized realm of pharmaceutical production facilities, the building envelope is not merely a shell but a critical component of the facility's containment and operational integrity. During our recent engineering audit for Aquashield Corporate, we focused on a coastal facility subject to high-velocity hurricane zones. The primary concern was the structural integrity of the plywood roof decking when subjected to extreme negative pressure, commonly known as wind uplift. In these environments, the roof acts as a giant wing; as high-velocity winds pass over the leading edge of the building, a vacuum effect is created that attempts to pull the decking away from the structural rafters.

To meet current ASCE 7 standards for coastal high-wind zones, the existing fastening patterns were found to be insufficient. The original construction relied on smooth-shank nails with wide spacing, which provided adequate gravity loads but failed to meet the required uplift resistance. A comprehensive audit revealed that the diaphragm action of the plywood was compromised by fastener fatigue and inadequate penetration depths. To mitigate this risk, a rigorous re-nailing schedule was mandated to ensure the assembly could withstand peak gust pressures without catastrophic failure of the building envelope.

  • Analysis of wind-tunnel data to determine peak suction zones at roof corners and perimeters.
  • Evaluation of existing fastener corrosion levels in salt-air environments.
  • Calculation of required pounds-per-square-foot (PSF) uplift resistance based on local building codes.
  • Assessment of the structural load path from the roof membrane down to the primary steel frames.

Material Science of Pneumatically Driven Ring-Shank Fasteners

The transition from smooth-shank to ring-shank fasteners is a fundamental requirement for achieving the necessary withdrawal resistance in high-wind zones. From a material science perspective, a smooth-shank nail relies solely on friction and the compression of wood fibers to remain seated. In contrast, a ring-shank fastener features a series of annular rings molded into the shank. These rings act as mechanical anchors, locking into the wood fibers of the plywood and the underlying framing members. This mechanical interlock significantly increases the force required to pull the nail out of the substrate, effectively multiplying the withdrawal resistance.

The use of pneumatic nailers allows for a consistent driving force, ensuring that the fastener is seated flush with the decking without splitting the plys. However, the precision of the pneumatic drive is critical. Over-driving can crush the wood fibers, reducing the "grip" of the rings, while under-driving leaves the fastener head proud, which can puncture the roofing membrane. Our specification requires high-grade, galvanized ring-shank nails to prevent galvanic corrosion, which is a common failure point in pharmaceutical facilities where chemical vapors or coastal salts may penetrate the envelope.

  • Comparison of smooth-shank versus ring-shank withdrawal values in Douglas Fir and Southern Pine substrates.
  • Optimization of pneumatic PSI settings to ensure consistent head seating without substrate crushing.
  • Verification of fastener coating thickness to meet ASTM B117 salt spray standards.
  • Analysis of shank diameter relative to the plywood thickness to prevent delamination.

Verifying Shear Withdrawal Resistance and Plywood Interface

Shear withdrawal resistance is the measure of a fastener's ability to resist lateral and vertical forces acting simultaneously. In a pharmaceutical facility, the roof deck must function as a rigid diaphragm, transferring lateral wind loads to the shear walls. When wind uplift occurs, the fasteners are subjected to intense shear stress. If the fasteners are placed too close to the edge of the plywood sheet, the wood is prone to "tear-out," where the fastener simply rips through the grain, leading to a total loss of connection. Our engineering approach emphasizes the critical importance of edge distance and fastener spacing.

The interaction between the ring-shank nail and the cross-laminated layers of the plywood is where the structural battle is won or lost. By strategically placing fasteners in a staggered pattern, we distribute the shear load across a wider area of the wood fiber. This prevents the creation of a "perforation line" that could lead to structural failure. We utilize a specific re-nailing schedule that increases fastener density at the perimeter—where the highest pressures occur—while maintaining a calculated grid in the field to ensure the entire deck moves as a single, cohesive unit.

  • Calculation of minimum edge distance to prevent splitting and tear-out failure.
  • Evaluation of the "shear plane" relative to the nail diameter and wood species.
  • Testing of fastener pull-out strength using calibrated hydraulic testers.
  • Analysis of the load-sharing capacity across multiple fastener points during a wind event.

Implementation of the Re-Nailing Schedule and Quality Assurance

The execution of a re-nailing schedule on an active pharmaceutical site requires a surgical approach to minimize disruption to production. The process begins with a comprehensive mapping of the existing deck. Our crews implement a tiered fastening approach: 6 inches on center at the perimeter and edges, and 12 inches on center in the interior field. This ensures that the most vulnerable areas of the building envelope are reinforced to a higher standard. Every fastener is driven perpendicular to the substrate to ensure the full engagement of the ring-shanks, as skewed nails significantly reduce the effective withdrawal resistance.

Quality assurance is the final and most critical step of the engineering process. A master roofer does not rely on visual inspection alone. We implement a rigorous audit trail involving random sampling and destructive testing. By removing a small section of the decking or utilizing pull-tests on non-critical areas, we can verify that the fasteners are achieving the predicted load values. This data is then compiled into a final engineering report for Aquashield Corporate, providing the facility owners with documented proof that their building envelope meets or exceeds the coastal high-wind uplift standards required for their high-value assets.

  • Deployment of a tiered fastening grid: 6" O.C. (edges) and 12" O.C. (field).
  • Strict adherence to perpendicular driving angles to maximize mechanical interlock.
  • Utilization of random-sample pull tests to verify real-world withdrawal resistance.
  • Final documentation of fastener counts and spacing for municipal building department approval.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #261

Life-Cycle Cost Analysis (LCCA) on Commercial Historic Sanctuary & Education Annexs

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Life-Cycle Cost Analysis (LCCA) on Commercial Historic Sanctuary & Education Annexs

Comprehensive Building Envelope Audit and Diagnostic Framework

The structural integrity of a historic sanctuary paired with a modern education annex presents a unique engineering challenge. In this case study, the primary objective was to conduct a forensic building envelope audit to identify systemic failures before implementing a Life-Cycle Cost Analysis (LCCA). Historic sanctuaries often suffer from antiquated flashing details and degraded masonry, while education annexes typically face issues with thermal bridging and membrane fatigue due to high occupancy loads. Our approach utilized ASTM E2128 standards for infrared thermography to map subsurface moisture entrapment and identify anomalies in the insulation layers.

The diagnostic phase revealed that the sanctuary's steep-slope roofing had suffered from chronic capillary action at the valley transitions, while the annex's flat roof exhibited widespread blistering and ponding water. By analyzing the vapor drive and hydrostatic pressure acting upon the building envelope, we determined that the existing systems had reached their theoretical end-of-life. The audit focused on the critical intersections where the historic masonry meets the modern annex expansion, as these joints are the most common points of failure for water infiltration.

  • Infrared thermographic scanning to detect latent moisture in polyisocyanurate insulation.
  • Core sampling of existing membranes to evaluate chemical degradation and plasticizer loss.
  • Comprehensive moisture surveys conducted per ANSI/ASTM standards to map saturation levels.
  • Evaluation of flashing integrity at parapet walls, scuppers, and HVAC curb penetrations.
  • Assessment of the building's Solar Reflectance Index (SRI) to determine heat island contributions.

Net Present Value (NPV) and Life-Cycle Cost Analysis

From a master roofer's perspective, the cheapest bid is rarely the most economical solution. To demonstrate this, we employed a Net Present Value (NPV) calculation to compare three distinct strategies: a standard "tear-off and replace" approach, a "patch-and-maintain" cycle, and a high-performance engineering restoration. The NPV analysis accounts for the time value of money, discounting future maintenance costs and energy expenditures back to today's dollars. This allows the client to see the true cost of ownership over a 30-year horizon rather than focusing solely on the initial capital expenditure.

The "patch-and-maintain" strategy showed a deceptive low entry cost but a skyrocketing NPV due to the frequency of emergency repairs and the inevitable acceleration of interior water damage. Conversely, the engineering restoration—utilizing a high-mil reinforced membrane with enhanced tapered insulation—offered the lowest NPV. By increasing the R-value of the education annex, we significantly reduced the HVAC load, creating a permanent reduction in operational expenses that offset the higher initial material cost within seven years.

  • Calculation of the Internal Rate of Return (IRR) for high-performance membrane upgrades.
  • Comparison of "Cost of Failure" metrics, including potential damage to sanctuary archives.
  • Analysis of energy savings derived from increased thermal resistance (R-value).
  • Projection of maintenance intervals, shifting from reactive to predictive scheduling.
  • Evaluation of the discount rate applied to future repair costs over a 25-year period.

Fiscal Strategy: Tax Deductions and Warranty Extensions

Maximizing the financial viability of a commercial roofing project requires a deep understanding of tax law and risk mitigation. For the historic sanctuary, we leveraged specific tax deductions available for maintenance restoration and historic preservation. By classifying the roof restoration as a capital improvement rather than a simple repair, the client was able to utilize accelerated depreciation schedules. This fiscal maneuver effectively reduced the net cost of the project by recapturing a significant percentage of the investment through tax credits designed to preserve the architectural heritage of the community.

Furthermore, we secured a 15-year extended warranty that transcends the standard manufacturer's guarantee. This was achieved by adhering to strict installation protocols, including the use of certified applicators and rigorous pull-tests on all adhered sections. A 15-year warranty extension serves as a hedge against inflation and material price volatility. It transforms the roof from a liability into a guaranteed asset, ensuring that the building envelope remains watertight without requiring additional capital appropriations for the next decade and a half.

  • Utilization of Section 179 deductions for immediate expensing of qualifying equipment and materials.
  • Application for historic preservation tax credits to offset restoration costs.
  • Implementation of a comprehensive warranty package covering both labor and materials.
  • Establishment of a funded reserve based on the LCCA's projected maintenance schedule.
  • Coordination with insurance underwriters to lower premiums based on improved roof resilience.

Sustainable Material Science and Landfill Mitigation

Modern commercial roofing is no longer just about keeping water out; it is about the science of waste mitigation. A traditional tear-off of a sanctuary and annex complex generates hundreds of tons of debris, much of which consists of non-biodegradable bitumen and contaminated insulation. Our engineering approach focused on avoiding landfill waste by implementing a recovery system where possible. By utilizing a high-performance capping membrane over existing stable substrates, we were able to divert approximately 60% of the projected waste from local landfills.

The material science behind this decision involved selecting a membrane with a high Solar Reflectance Index (SRI) and high thermal emissivity. This not only protects the building from UV degradation but also reduces the urban heat island effect. By integrating a sustainable drainage system and utilizing recycled-content insulation, the project met stringent environmental guidelines while maintaining the structural requirements of a commercial building envelope. The result is a resilient, breathable system that respects the historic nature of the sanctuary while providing the modern efficiency required by the education annex.

  • Diversion of old roofing materials to specialized recycling facilities to reduce landfill impact.
  • Selection of Low-VOC adhesives and membranes to improve indoor air quality in the annex.
  • Installation of a "cool roof" system to lower peak cooling demands during summer months.
  • Use of high-density polyethylene (HDPE) liners in critical drainage areas for longevity.
  • Implementation of a circular economy model for the disposal and repurposing of metal flashing.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #262

Lightning Protection System Air Terminal Stanchion Flashing & Membrane Bonding on Commercial Financial Institution Data Vaults

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Lightning Protection System Air Terminal Stanchion Flashing & Membrane Bonding on Commercial Financial Institution Data Vaults

The Criticality of Data Vault Envelope Integrity and LPS Integration

In the realm of high-security commercial construction, the data vault of a financial institution represents the most critical asset within the building envelope. These structures are designed for maximum security and environmental stability, yet they present a unique engineering paradox: the requirement for a comprehensive Lightning Protection System (LPS) necessitates the introduction of multiple penetrations through the primary waterproofing membrane. From a master roofer's perspective, every penetration is a potential failure point. When dealing with air terminal stanchions—the vertical rods designed to intercept lightning strikes—the risk is magnified by the extreme thermal energy associated with a strike.

The primary objective of a building envelope audit for these facilities is to ensure that the transition from the air terminal to the roof substrate is seamless. A failure in the flashing at a stanchion base does not merely result in a slow leak; it can lead to catastrophic water intrusion during a storm, potentially compromising the server racks and physical archives housed within the vault. We evaluate these systems based on the intersection of NFPA 780 standards for lightning protection and ASTM guidelines for roofing membrane application.

  • Assessment of membrane compatibility between the LPS hardware and the roof surface (TPO, PVC, or Modified Bitumen).
  • Evaluation of the thermal expansion coefficients of the stanchion materials versus the roofing substrate.
  • Verification of the structural load-bearing capacity of the vault roof to support heavy-duty stanchion mounts.
  • Analysis of the drainage slope around the stanchion base to prevent ponding water from infiltrating the flashing.

Engineering the High-Performance Stanchion Pitch-Pocket Detail

Standard flashing boots are insufficient for the rigors of a financial data vault. Instead, we employ a heavy-duty pitch-pocket detailing strategy. A pitch-pocket is essentially a reinforced containment vessel integrated into the roof membrane that allows the stanchion to be "potted" in a high-grade, non-shrink sealant or specialized potting compound. This creates a redundant, multi-layered seal that can withstand the mechanical vibrations of the building and the thermal cycling of the roof surface.

The engineering of the pocket begins with a reinforced membrane curb, which is heat-welded or chemically bonded to the field membrane. The interior of the pocket is then lined with a high-temperature modified bitumen or a liquid-applied flashing membrane. The stanchion is centered within this pocket, and the void is filled with a professional-grade polyurethane sealant that maintains flexibility over a wide temperature range. This prevents the "pumping" action that typically occurs during freeze-thaw cycles, which often pulls standard flashing away from the metal pipe.

  • Utilization of ASTM D6690 compliant sealants to ensure long-term adhesion to the metal stanchion.
  • Implementation of a dual-stage flashing process: a primary membrane wrap followed by a secondary liquid-applied flashing.
  • Integration of a thermal break to prevent the stanchion from acting as a thermal bridge, which can cause condensation inside the vault.
  • Application of a UV-resistant top coat to the pocket to prevent premature degradation of the sealant.

Grounding Cable Conductor Flashings and Membrane Bonding

While the air terminal handles the strike, the grounding cables—the conductors that carry the current to the earth—must traverse the roof surface. These cables are often overlooked during routine audits, yet they represent a significant risk for "wicking" water. Capillary action can pull moisture along the length of the copper conductor, leading it directly into the roof penetration. To mitigate this, we implement a rigorous bonding and flashing protocol for every conductor exit point.

The conductor flashing must be engineered to accommodate the movement of the cable without tearing the membrane. We utilize a combination of reinforced flashing membranes and specialized gaskets. The cable is first sleeved in a protective conduit where it penetrates the roof, and this conduit is then bonded to the membrane using a high-strength adhesive. The transition from the conduit to the cable is sealed with a flexible, weather-tight boot that is mechanically fastened and then chemically bonded to the roof surface. This ensures that the cable cannot shift and create a "tear-point" in the membrane during high-wind events.

  • Application of galvanic corrosion inhibitors where copper conductors contact aluminum or steel flashing components.
  • Use of reinforced flashing strips (flashing patches) to distribute the mechanical stress across a wider area of the membrane.
  • Verification of the "drip edge" geometry on the conductor flashing to ensure water is shed away from the penetration.
  • Periodic testing of the bond strength between the conductor sleeve and the membrane using non-destructive pull tests.

Mitigating Lightning Strike Membrane Punctures and Thermal Shock

The most violent event a roof can experience is a direct lightning strike. The plasma arc generated by a strike can reach temperatures exceeding 30,000 Kelvin, which is more than enough to instantaneously vaporize standard TPO or EPDM membranes. If the air terminal is not properly bonded and flashed, the current may "jump" or arc to the roof surface, causing a "blow-out" puncture. This creates an immediate hole in the envelope, leading to rapid water intrusion during the accompanying thunderstorm.

To prevent this, the building envelope must be designed for maximum heat dissipation. We specify the use of high-temp modified bitumen or thick-gauge reinforced membranes at the base of every stanchion. By increasing the mass of the membrane at the point of potential arcing, we provide a thermal buffer. Furthermore, the bonding of the stanchion to the roof must be absolute; any air gap between the metal and the membrane can act as a combustion chamber during a strike, leading to an explosive failure of the flashing. Our audit process includes a thermal imaging scan to identify any voids in the potting compound or gaps in the membrane bonding.

  • Installation of sacrificial "sac-plates" or conductive metal pads that are integrated into the flashing to provide a controlled path for current.
  • Implementation of a rigorous post-strike audit protocol to inspect for microscopic "pin-hole" punctures caused by thermal shock.
  • Use of high-density cross-linked polyethylene (PEX) or similar materials in the sub-base to prevent structural cracking under thermal stress.
  • Coordination with electrical engineers to ensure the impedance of the grounding path is low enough to prevent surface arcing.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #263

Commercial Roof Hatch Safety Grab Bars & Compression Curb Gasket Weatherproofing on Commercial Telecommunications Central Switching Offices

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Commercial Roof Hatch Safety Grab Bars & Compression Curb Gasket Weatherproofing on Commercial Telecommunications Central Switching Offices

The Criticality of the Building Envelope in Telecommunications Hubs

In the realm of commercial building envelope engineering, Telecommunications Central Switching Offices (CSOs) represent some of the most demanding environments a master roofer can encounter. These facilities are not merely warehouses; they are mission-critical infrastructure hubs housing millions of dollars in sensitive switching gear, fiber optic terminations, and high-density server arrays. The primary objective of the building envelope in a CSO is the absolute mitigation of water ingress and the maintenance of a controlled internal atmosphere. Because these buildings often utilize massive HVAC systems to dissipate heat from the switching equipment, they frequently experience significant internal pressure differentials, which can effectively "suck" moisture through any compromised seal or flashing detail.

The roof hatch serves as a primary point of vulnerability within this envelope. While often viewed as a simple access point, the hatch assembly—comprising the cover, the curb, the gasket, and the surrounding flashing—is a complex intersection of mechanical movement and static waterproofing. A failure at the curb interface does not just result in a ceiling stain; it risks the catastrophic failure of the electrical infrastructure below. Therefore, an engineering audit of these systems must prioritize the synergy between structural safety and hydrostatic resistance.

  • Assessment of thermal bridging at the curb interface to prevent condensation.
  • Evaluation of membrane continuity from the field of the roof to the hatch flashing.
  • Analysis of wind-uplift pressures on the hatch cover during high-velocity wind events.
  • Verification of the structural integrity of the curb-to-deck attachment points.

OSHA Compliance and Structural Integrity of Roof Hatch Safety Posts

Safety on a commercial roof is governed by strict OSHA and ANSI standards, particularly regarding the transition from a ladder to the roof surface. In a CSO environment, where technicians may be accessing the roof under emergency conditions or during severe weather, the installation of engineered safety grab bars and ladder posts is non-negotiable. A master tradesman recognizes that a safety post is not merely a handrail, but a load-bearing structural component that must withstand the dynamic forces of a technician climbing out of the hatch.

The engineering focus here is on the metallurgy and the anchoring system. We specify heavy-duty galvanized steel or powder-coated aluminum to prevent oxidation and galvanic corrosion. The safety posts must be securely bolted to the hatch curb using high-tensile fasteners that do not compromise the waterproofing of the curb's flashing. Furthermore, the integration of counterbalanced smoke dampers within the hatch assembly ensures that the cover can be opened with minimal effort while remaining securely sealed when closed, preventing the "chimney effect" that can pull smoke or contaminants into the facility during a fire event.

  • Installation of OSHA-compliant grab bars with a minimum diameter of 1.25 inches for a secure grip.
  • Utilization of counterbalanced spring-assist hinges to reduce the physical exertion required for emergency egress.
  • Application of corrosion-resistant coatings to all exposed metalwork to ensure a 20-year service life.
  • Verification of post-stability under a lateral load of 200 pounds as per ANSI standards.

Dynamic Sealing and Compression Curb Gasket Engineering

The interface between the roof hatch cover and the curb is where the most frequent failures occur. To achieve a truly weather-tight seal, we employ heavy-duty compression curb gaskets. Unlike standard weatherstripping, these gaskets are engineered from high-density EPDM or closed-cell neoprene, materials chosen for their exceptional memory and resistance to UV degradation. The goal is to create a continuous, airtight seal that maintains its integrity despite the constant expansion and contraction cycles caused by thermal fluctuations on the roof surface.

From a material science perspective, the compression gasket must be sized to provide a consistent "squeeze" across the entire perimeter of the curb. If the gasket is too loose, wind-driven rain will penetrate the seal; if it is too tight, the mechanical stress on the hatch hinges will lead to premature failure. We implement a dual-seal approach: a primary compression gasket for the main seal and a secondary drip edge to divert water away from the curb face. This redundancy is critical in CSO environments where the cost of a leak far outweighs the cost of premium gasketry.

  • Selection of EPDM gaskets with a Shore A hardness rating optimized for compression set resistance.
  • Implementation of a continuous perimeter seal to eliminate "point-leaks" at the corners of the curb.
  • Integration of a smoke-seal gasket to prevent the migration of gases between the roof and the interior.
  • Regular torque audits of the hatch clamping mechanisms to ensure uniform gasket pressure.

Termination Bar Integration and Long-Term Weatherproofing Audits

The final line of defense in the roof hatch assembly is the compression termination bar. This is the mechanical fastening system that secures the roof membrane to the vertical face of the hatch curb. In a professional engineering application, simply adhering the membrane with mastic is insufficient. We utilize a heavy-duty aluminum or galvanized steel termination bar, which is mechanically fastened through the membrane and into the curb substrate. This creates a "sandwich" effect, locking the membrane in place and preventing the capillary action that often draws water upward behind the flashing.

A comprehensive building envelope audit concludes with a rigorous inspection of these termination points. We look for signs of "fish-mouthing" or wrinkles in the membrane, which indicate improper tensioning. The termination bar must be installed with a consistent fastener spacing—typically every 6 to 12 inches—to ensure that the membrane is under constant, even tension. Once the bar is secured, a high-grade polyurethane sealant is applied to the top edge of the bar to create a seamless transition from the metal to the membrane, effectively sealing the envelope against the elements.

  • Use of stainless steel fasteners to eliminate the risk of rust-jacking and membrane puncture.
  • Application of a reinforced flashing membrane at the curb corners to prevent stress cracking.
  • Execution of a water-tightness test using a controlled hose test to verify the seal of the termination bar.
  • Annual infrared thermography scans to detect hidden moisture

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #264

Multi-Tier Conductor Head Overflow Spillways & Freeze-Thaw Downspout Burst Defense on Commercial Heavy Manufacturing Fabrication Plants

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Multi-Tier Conductor Head Overflow Spillways & Freeze-Thaw Downspout Burst Defense on Commercial Heavy Manufacturing Fabrication Plants

The Engineering Challenge of High-Volume Drainage in Heavy Manufacturing

In the realm of heavy manufacturing fabrication plants, the building envelope is subjected to extreme environmental stressors and massive roof surface areas that generate immense volumes of stormwater runoff. When dealing with sprawling footprints—often exceeding 500,000 square feet—the drainage system cannot be viewed as a mere accessory; it is a critical life-safety component of the structural engineering. A failure in the primary drainage system during a 100-year rain event does not simply result in a leak; it leads to catastrophic ponding, which can exceed the structural load capacity of the roof deck, potentially leading to a total collapse of the ceiling grid and endangering personnel and high-value machinery below.

From a master roofer's perspective, the primary vulnerability in these facilities is the transition point between the internal roof drainage and the external conveyance system. In heavy fabrication plants, we often see a reliance on oversized internal drains that feed into massive conductor heads. However, if these conductor heads are not engineered with precise overflow relief mechanisms, the system becomes a bottleneck. The goal of a professional building envelope audit is to ensure that the hydrostatic pressure generated during peak flow does not compromise the flashing or the membrane-to-metal seals, which are the most common points of failure in industrial settings.

  • Assessment of roof slope consistency to prevent "birdbaths" or stagnant water pockets.
  • Evaluation of membrane compatibility with conductor head flashing to ensure watertight integrity.
  • Analysis of catchment area ratios to determine if the existing drain density meets current ANSI/ASTM standards.
  • Inspection of parapet scuppers as a secondary fail-safe for primary drain blockage.

Multi-Tier Conductor Head Design and Overflow Relief Weir Calculations

The conductor head serves as the critical junction where water transitions from a horizontal roof plane to a vertical downspout. In high-capacity manufacturing plants, a standard conductor head is often insufficient. We implement multi-tier conductor head systems that incorporate overflow relief weirs. A weir is essentially a calibrated notch or opening that allows water to escape the system once the primary downspout reaches maximum capacity. This prevents the "bathtub effect," where water rises above the roof membrane level and begins to seep under the flashing or into the building's interior cladding.

Calculating the overflow relief requires a deep understanding of fluid dynamics and the specific rainfall intensity of the region. We utilize the weir flow formula to determine the exact height and width of the spillway opening. By calibrating the spillway to trigger at a specific water depth—typically 2 to 4 inches above the roof surface—we ensure that the primary downspout handles the bulk of the load while the spillway prevents a catastrophic overflow. This precision engineering ensures that water is directed safely away from the building envelope and onto the perimeter grading, rather than allowing it to back up into the building's structural core.

  • Implementation of stainless steel or heavy-gauge galvanized conductor heads to resist corrosion.
  • Precision cutting of spillway weirs to match calculated peak-flow discharge rates.
  • Integration of debris screens to prevent organic matter from clogging the primary throat.
  • Strategic placement of overflow outlets to avoid discharging water directly onto pedestrian walkways or equipment loading zones.

Structural Integrity: Heavy-Duty Downspout Bracketing and Load Distribution

The sheer weight of water moving through a 12-inch or 16-inch downspout is substantial, and when you add the weight of ice and snow accumulation in colder climates, the mechanical stress on the building envelope is immense. Standard light-commercial brackets are wholly inadequate for heavy manufacturing plants. We specify heavy-duty, oversized steel brackets that are mechanically fastened into the structural girts or masonry of the building. These brackets must be designed to distribute the load across a wider surface area to prevent the pulling or shearing of fasteners from the building facade.

Furthermore, the vibration caused by high-velocity water flow can lead to "fastener fatigue," where the screws or bolts gradually loosen over time, creating gaps in the building envelope. To combat this, we utilize vibration-dampening gaskets and reinforced mounting plates. The alignment of the downspout is equally critical; any deviation in the vertical plumb line can create turbulence within the pipe, which increases the risk of leaks at the joints and puts uneven pressure on the brackets. A master-level installation ensures that the downspout is a rigid, integrated extension of the building's structural framework.

  • Use of 14-gauge or 16-gauge steel for downspout fabrication to withstand physical impact and internal pressure.
  • Installation of reinforced strap brackets every 8 to 10 feet to maintain vertical stability.
  • Application of industrial-grade sealants at all bracket-to-wall interfaces to prevent water infiltration.
  • Utilization of stainless steel fasteners to eliminate galvanic corrosion between dissimilar metals.

Mitigating Freeze-Thaw Cycles and Burst Defense Strategies

In temperate and cold climates, the freeze-thaw cycle is the primary enemy of the commercial drainage system. When water traps in the bottom of a downspout or within a joint, it expands upon freezing, exerting thousands of pounds of pressure per square inch. In a heavy manufacturing plant, where roof temperatures may fluctuate due to internal heat generation and external cold, this cycle happens rapidly and repeatedly. This often leads to "bursting," where the metal seams of the downspout split open, leading to uncontrolled water discharge against the building's foundation and potentially causing basement seepage or foundation erosion.

To defend against this, we employ a "burst-defense" strategy centered on thermal management and drainage efficiency. This includes the installation of heat trace cables in critical zones and the use of specialized "expansion joints" that allow the metal to contract and expand without buckling. Additionally, we ensure that the downspouts are perfectly sloped toward the discharge point, leaving no room for standing water to pool and freeze. By managing the thermal bridge between the heated interior of the plant and the frozen exterior envelope, we can significantly reduce the frequency of freeze-thaw failures.

  • Installation of self-regulating heat tape within conductor heads to prevent ice damming.
  • Integration of telescopic expansion joints to accommodate thermal movement of the metal.
  • Ensuring all downspouts terminate in a proper splash block or underground storm system to prevent base-level icing.
  • Application of hydrophobic coatings to the interior of the downspouts to accelerate water transit and reduce clinging.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #265

Sub-Zero Cold Storage Downward Vapor Drive & Self-Adhered SBS Barriers on Commercial Logistics Distribution Hubs

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Sub-Zero Cold Storage Downward Vapor Drive & Self-Adhered SBS Barriers on Commercial Logistics Distribution Hubs

The Physics of Inverted Thermal Envelopes and Downward Vapor Drive

In standard commercial construction, building envelope engineers typically design for an upward vapor drive, where warm, moist interior air seeks to migrate toward the colder exterior. However, in the context of a sub-zero logistics distribution hub, we encounter an inverted thermal envelope. When the interior of a facility is maintained at temperatures significantly below freezing—often ranging from -10°F to -40°F—the vapor pressure differential is reversed. The exterior environment, characterized by higher temperatures and ambient humidity, becomes the primary source of moisture pressure, driving water vapor inward toward the cold storage core.

This downward or inward vapor drive creates a high-risk scenario for interstitial condensation. If the building envelope is not engineered to be completely impermeable from the exterior, moisture-laden air will penetrate the outer cladding and migrate through the insulation. As this warm air hits the cold interior surfaces or the chilled structural steel, it reaches its dew point, transitioning from a gas to a liquid or solid. In a sub-zero environment, this often manifests as "frosting" within the insulation layers, which drastically reduces the thermal resistance (R-value) of the polyiso and can lead to catastrophic structural degradation over time.

  • Vapor Pressure Differential: The driving force caused by the temperature gap between the exterior ambient air and the sub-zero interior.
  • Inverted Thermal Gradient: A condition where the "warm side" of the envelope is the exterior, necessitating a shift in vapor barrier placement.
  • Hygroscopic Loading: The accumulation of moisture within porous materials, which can lead to icing and material failure.
  • Atmospheric Permeability: The rate at which water vapor passes through a specific material, measured by ASTM E96 standards.

Dew Point Migration and Interstitial Condensation Control

The primary objective in a logistics hub audit is to locate the dew point—the exact temperature at which air becomes saturated and moisture precipitates—and ensure it occurs outside the structural assembly. In a poorly designed envelope, the dew point often occurs mid-way through the insulation layers. When moisture condenses inside the wall or roof assembly, it creates a hidden reservoir of water that can corrode metal decking, rot blocking, and compromise the adhesive bonds of the roofing system.

To mitigate this, the vapor barrier must be placed on the "warm side" of the assembly. In a cold storage facility, this means the primary air and vapor seal must be integrated into the outermost layers of the roof and wall systems. By preventing the humid exterior air from ever entering the insulation matrix, we ensure that the polyisocyanurate remains dry. Dry insulation is efficient insulation; once polyiso becomes saturated with interstitial ice, its ability to resist heat flow is compromised, leading to increased energy costs and potential "sweating" on the interior warehouse ceilings, which creates a safety hazard for personnel and equipment.

  • Dew Point Location: The critical engineering goal of shifting the condensation point to the exterior of the structural deck.
  • Interstitial Condensation: Moisture that forms between layers of building materials, often invisible until structural failure occurs.
  • Thermal Bridging: The process where heat bypasses insulation through highly conductive materials like steel fasteners or beams.
  • R-Value Degradation: The loss of thermal efficiency that occurs when insulation is compromised by moisture or ice.

Engineering the Seal with Self-Adhered SBS Barriers

For high-performance logistics hubs, traditional torch-down or mechanically fastened membranes are often insufficient due to the risk of punctures and seams. We specify self-adhered SBS (Styrene-Butadiene-Styrene) modified bitumen barriers because they provide a monolithic, seamless seal that adheres aggressively to the substrate. Unlike mechanically fastened systems, which introduce thousands of potential leak paths through the fastener holes, a self-adhered SBS membrane creates a continuous chemical bond across the entire surface area of the roof deck.

The material science of SBS allows the membrane to remain flexible at extreme temperature fluctuations, which is critical in environments where the exterior roof surface may be 100°F while the interior is -20°F. This elasticity prevents the membrane from cracking or pulling away from the corners and parapets under thermal shock. Furthermore, the self-adhering nature of the SBS barrier ensures that the vapor seal is maintained even under the heavy compressive loads of multi-layer insulation and heavy-duty roofing membranes. This creates a redundant, multi-stage defense against the inward vapor drive.

  • SBS Modification: The addition of styrene-butadiene-styrene to bitumen to enhance elasticity and low-temperature flexibility.
  • Monolithic Sealing: The creation of a single, continuous barrier that eliminates the risk of seam failure.
  • Adhesion Strength: The ability of the membrane to bond to the substrate without the need for mechanical fasteners.
  • Thermal Shock Resistance: The capacity of the material to expand and contract without losing its structural integrity.

Staggered Multi-Layer Polyiso and Thermal Bridging Mitigation

Even with a perfect vapor barrier, the method of installing the thermal insulation can introduce vulnerabilities. A common failure in commercial roofing is the alignment of insulation joints. If the seams of the first layer of polyisocyanurate align perfectly with the seams of the second layer, a "thermal chimney" is created. This straight-line gap allows any air that manages to penetrate the outer barrier to travel rapidly through the insulation, creating a direct path for heat loss and moisture migration.

Our engineering standard requires a staggered multi-layer approach. By offsetting the joints of each subsequent layer of polyiso by at least 12 to 24 inches, we force any potential air leakage to take a tortuous path, effectively neutralizing the chimney effect. We utilize high-density polyiso for its superior compressive strength and thermal performance, ensuring that the layers are tightly butted and sealed. When combined with the SBS barrier, this staggered configuration ensures that the building envelope functions as a cohesive, airtight system, maintaining the sub-zero interior while protecting the structural integrity of the logistics hub.

  • Staggered Jointing: The practice of offsetting insulation seams to prevent linear air leakage and thermal bridging.
  • Thermal Chimney Effect: The rapid movement of air through aligned gaps in insulation layers.
  • Polyisocyanurate (Polyiso): A closed-cell

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
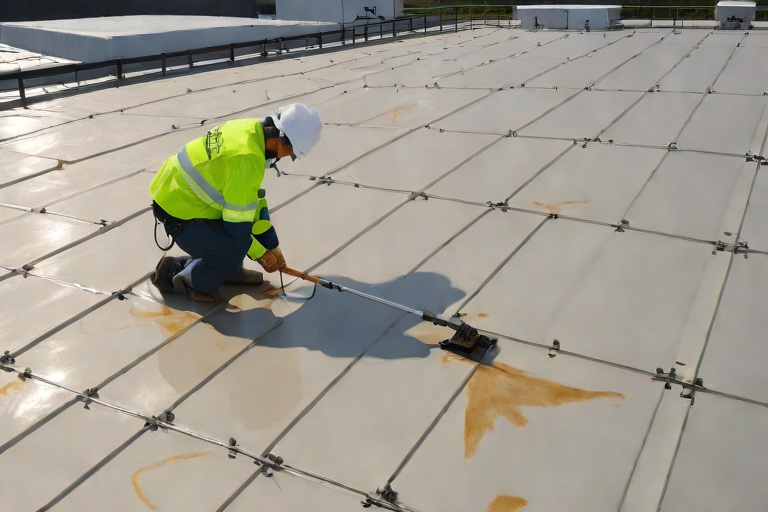
Commercial Engineering Dossier #266

Structural Deck Fastener Pull-Out Testing on 22-Gauge Corrugated Steel Decks on Commercial Automotive Assembly Plants

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Structural Deck Fastener Pull-Out Testing on 22-Gauge Corrugated Steel Decks on Commercial Automotive Assembly Plants

Engineering Audit Framework for Automotive Assembly Envelopes

In the high-stakes environment of a commercial automotive assembly plant, the building envelope is subjected to extreme stressors that exceed standard warehouse conditions. The structural integrity of the roofing system relies entirely on the connection between the membrane fastening system and the 22-gauge corrugated steel deck. An engineering audit of this scale requires a forensic approach to substrate analysis, as the heavy machinery and industrial vibrations inherent in automotive manufacturing can induce micro-shifts in the decking, potentially compromising the mechanical bond of the fasteners.

The 22-gauge steel deck provides a robust foundation, yet its corrugated profile creates specific challenges regarding fastener placement and engagement. To ensure the envelope remains airtight and wind-resistant, we implement a rigorous audit protocol that focuses on the "critical zone" of the deck—the areas most susceptible to uplift and shear stress. Our approach prioritizes the verification of the fastener's grip within the steel web, ensuring that the structural capacity of the metal is not compromised by over-driving or improper hole sizing.

  • Assessment of deck gauge consistency to verify 22-gauge specifications across all bays.
  • Evaluation of the corrugated profile depth and its impact on fastener thread engagement.
  • Mapping of high-vibration zones near stamping presses and assembly lines.
  • Identification of previous roof penetrations and repair patches that may weaken the substrate.
  • Analysis of the existing insulation thickness and its effect on fastener embedment depth.

Calibrated Mechanical Pull Testing Methodology

To quantify the actual holding power of the roof assembly, we utilize calibrated mechanical pull testers. This process is not a mere sampling but a systematic stress test designed to push fasteners to the point of failure or to a predetermined safety threshold. The tester applies a controlled, vertical tensile load to the fastener head, measuring the exact poundage at which the fastener either pulls through the steel deck or the threads strip from the substrate. This data is critical for determining if the current fastening pattern meets the engineered requirements for the building's specific wind-zone classification.

The methodology requires a strategic distribution of test points. We do not simply test the center of the roof; we focus heavily on the perimeter and corner zones, where wind-uplift pressures are exponentially higher. By utilizing a digital load cell, we can record the "peak load" and the "residual strength" of the fastener. This allows us to determine if the fastener failed catastrophically or if there was a gradual loss of tension, which often indicates a degradation of the steel deck's structural integrity around the hole.

  • Deployment of digital force gauges calibrated to NIST standards for precision.
  • Execution of "destructive" and "non-destructive" tests to establish a failure baseline.
  • Strategic sampling of fasteners in Zone 1 (interior), Zone 2 (perimeter), and Zone 3 (corners).
  • Measurement of the "pull-out" distance to evaluate the elasticity of the fastener shaft.
  • Comparison of field results against the manufacturer's theoretical withdrawal specifications.

Withdrawal Resistance Thresholds and Material Science

The core of our analysis centers on the minimum withdrawal resistance threshold. For a 22-gauge corrugated steel deck, the fastener must achieve a specific poundage threshold to be considered compliant with ASCE 7 wind-load standards. Withdrawal resistance is a function of the fastener's thread geometry, the hardness of the steel deck, and the coefficient of friction between the two materials. When a fastener is driven into 22-gauge steel, it creates a mechanical interlock; if the hole is oversized or the steel is too soft, the "thread strip" occurs, leading to a total loss of uplift resistance.

Material science plays a pivotal role here, particularly regarding the interaction between the fastener coating and the galvanized steel of the deck. We examine the shear strength of the fastener shaft to ensure that the head does not shear off before the pull-out resistance is fully tested. In automotive plants, where temperature fluctuations can be extreme due to industrial heating and cooling, the thermal expansion and contraction of the steel deck can "loosen" the fastener over time. This phenomenon, known as thermal cycling, can reduce the effective withdrawal resistance by as much as 15% over a decade.

  • Calculation of the "Safety Factor" by dividing the ultimate failure load by the required design load.
  • Analysis of thread pitch and diameter relative to the 22-gauge steel thickness.
  • Evaluation of the "pull-through" failure mode versus the "thread-strip" failure mode.
  • Assessment of the impact of insulation compression on the fastener's vertical alignment.
  • Verification of the fastener's tensile strength in accordance with ASTM standards.

Corrosion Diagnostics and Wind-Zone Compliance

A fastener may pass a pull test today, but its long-term viability depends on its resistance to corrosion. In an automotive assembly plant, the atmosphere often contains airborne chemicals, lubricants, and moisture, which can trigger galvanic corrosion. This occurs when two dissimilar metals—such as a zinc-coated fastener and a galvanized steel deck—react in the presence of an electrolyte. We perform forensic diagnostics on extracted fasteners to look for "pitting" or "white rust," which indicates that the protective coating has been breached, leaving the structural core of the fastener vulnerable to oxidation.

Finally, all data is synthesized into a wind-zone compliance schedule. We map the pull-test results against the building's architectural wind-load requirements. If the fasteners in the corner zones (Zone 3) fail to meet the required withdrawal threshold, we mandate a "densification" of the fastening pattern. This involves installing additional fasteners to distribute the uplift load across a larger area of the 22-gauge deck, thereby ensuring that the roof remains securely attached during a peak wind event. This engineering-led approach transforms the roof from a simple cover into a high-performance structural component of the building envelope.

  • Inspection for galvanic corrosion at the fastener-to-deck interface.
  • Testing for the integrity of the fastener's weather-seal washer to prevent moisture ingress.
  • Cross-referencing pull-out data with ASCE 7 wind-uplift pressure maps.
  • Development of a remedial fastening schedule for under-performing zones.
  • Final certification of the building envelope's structural readiness for extreme weather events.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
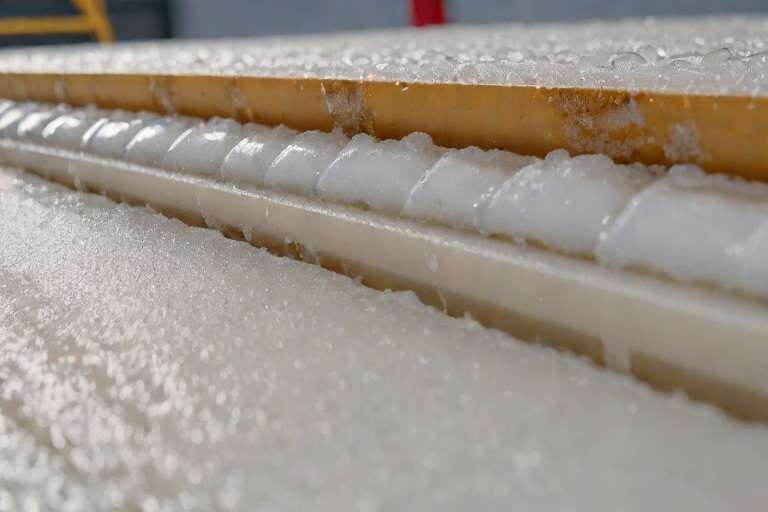
Commercial Engineering Dossier #267

Electronic Vector Mapping (EVM) Low-Voltage Membrane Breach Detection on Commercial Mission-Critical Data Centers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Electronic Vector Mapping (EVM) Low-Voltage Membrane Breach Detection on Commercial Mission-Critical Data Centers

The Criticality of the Building Envelope in Mission-Critical Environments

In the realm of mission-critical data centers, the building envelope is not merely a shell; it is the primary line of defense for millions of dollars in high-density computing hardware. A single breach in the roofing membrane, even one as small as a microscopic pinhole, can lead to catastrophic failure if moisture migrates into the plenum or directly onto server racks. Traditional roofing methodologies rely heavily on visual inspections and infrared thermography, but these methods are reactive. They identify a leak only after moisture has already infiltrated the substrate and saturated the insulation, often leaving the actual entry point hidden by the time the symptom is visible.

To mitigate this risk, we shift our focus from reactive maintenance to proactive engineering. The challenge with modern high-performance membranes, such as TPO or modified bitumen, is that the most dangerous leaks are not the gaping holes, but the "invisible" punctures caused by improper fastener installation, wind-driven rain forced through seam failures, or debris punctures during the commissioning phase. In a data center environment, where uptime is measured in "five nines," the tolerance for moisture ingress is zero. This necessitates a transition toward electronic verification systems that can certify the integrity of the membrane across the entire roof plane without compromising the material.

  • Elimination of capillary action risks at flashing and curb interfaces.
  • Prevention of interstitial condensation within the insulation layers.
  • Reduction of unplanned downtime caused by water-induced electrical shorts.
  • Shift from subjective visual "walk-throughs" to objective, data-driven audits.

Engineering the Conductive Underlayment Vector Grid

Electronic Vector Mapping (EVM) represents a paradigm shift in membrane quality assurance. Unlike standard roofing, EVM utilizes a specialized conductive underlayment that functions as a continuous, low-voltage electrical grid. This grid is installed beneath the primary waterproofing membrane, creating a controlled electrical field across the entire roof surface. By applying a low-voltage DC current, the system establishes a baseline of electrical resistance. Because the primary membrane acts as a dielectric insulator, the current remains contained within the vector grid unless the membrane's integrity is compromised.

The "vector" component of this technology refers to the precise X and Y coordinate system established by the conductive layers. When a breach occurs—such as a pinhole puncture—the moisture entering the breach creates a conductive path between the atmosphere (or standing water) and the underlying grid. This change in electrical impedance is instantly detected by the monitoring system. The system doesn't just signal that a leak exists; it triangulates the exact coordinates of the breach by measuring the voltage drop across the vector grid, allowing for surgical precision in repairs.

  • Deployment of a conductive copper or carbon-based mesh underlayment.
  • Establishment of a calibrated dielectric barrier to prevent false positives.
  • Utilization of low-voltage DC current to ensure safety and non-interference with data center EMI standards.
  • Integration of high-sensitivity sensors capable of detecting micro-ampere fluctuations.

Precision Diagnostics and Microscopic Pinhole Identification

The true value of EVM is revealed during the non-destructive testing (NDT) phase of a building envelope audit. Traditional "flood testing" requires pumping thousands of gallons of water onto a roof and waiting for it to seep through—a process that is time-consuming and introduces the very moisture we are trying to avoid. In contrast, EVM allows for an electronic "stress test" of the membrane. By scanning the vector grid, we can identify "weak points" where the membrane is thin or where a microscopic puncture has occurred, even if the leak has not yet manifested as a visible drip in the ceiling.

From a material science perspective, these pinholes are often the result of mechanical stress during the installation of HVAC curbs or the use of oversized fasteners that slightly tear the membrane. Because the EVM system monitors the electrical continuity of the envelope, it can pinpoint these breaches to within a few square inches. This eliminates the "search and destroy" method of roofing, where contractors cut large holes in a perfectly good membrane searching for a leak, often creating more problems than they solve. Instead, the master roofer can navigate directly to the coordinate provided by the vector map and apply a targeted, permanent seal.

  • Real-time triangulation of membrane breaches using impedance mapping.
  • Identification of "near-miss" punctures that have not yet failed but are compromised.
  • Avoidance of destructive "exploratory" cutting of the roof membrane.
  • Rapid verification of repair efficacy through immediate re-scanning of the vector coordinate.

Non-Destructive Quality Certification and Lifecycle Management

For Aquashield Corporate, the goal is to provide a "birth certificate" for the roof—a certified document proving that the building envelope is 100% watertight at the moment of handover. By utilizing EVM, we provide a non-destructive quality certification that aligns with ASTM and ANSI standards for membrane integrity. This level of certification is essential for insurance underwriting and facility management in the data center sector, where the cost of a single leak can exceed the total cost of the roofing system itself.

Beyond the initial installation, the vector grid remains an active asset for the life of the building. It transforms the roof from a passive slab of plastic and rubber into an intelligent sensor. Lifecycle management is simplified because the system provides continuous monitoring; if a technician drops a tool or a piece of equipment vibrates a seam loose three years into the warranty, the EVM system triggers an alert immediately. This allows for "micro-maintenance," where a five-minute patch prevents a million-dollar disaster. This is the pinnacle of commercial roofing engineering: moving from the era of the leaking bucket to the era of the digital envelope.

  • Provision of a comprehensive "Zero-Defect" electronic audit report upon completion.
  • Alignment with ASTM E2127 for standard practice in leak detection.
  • Implementation of a permanent monitoring system for real-time envelope health tracking.
  • Reduction in long-term OpEx by eliminating the need for annual manual infrared surveys.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #268

Liquid-Applied PMMA & Polyurethane Fleece-Reinforced Flashing Resins on Commercial Cold Storage Freezer Warehouses

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Liquid-Applied PMMA & Polyurethane Fleece-Reinforced Flashing Resins on Commercial Cold Storage Freezer Warehouses

The Thermal Dynamics of Cold Storage Envelope Failures

In the realm of commercial building envelope engineering, cold storage freezer warehouses represent the most punishing environment for roofing and flashing systems. The primary challenge is the extreme temperature differential between the interior freezer environment—often maintained at -20°F or lower—and the exterior ambient conditions, which can fluctuate wildly based on regional climate. This delta creates a persistent thermal gradient that induces significant stress on the building's structural components, leading to chronic thermal bridging and differential movement.

Traditional membrane systems, such as modified bitumen or single-ply TPO, frequently fail at the transition points where the roof deck meets vertical structural elements. The coefficient of thermal expansion differs between the steel I-beam stanchions and the concrete or metal decking, causing traditional adhesives to shear and membranes to tear. When these seals breach, moisture enters the assembly, leading to interstitial condensation and the formation of ice lenses, which further accelerate the degradation of the substrate through a freeze-thaw cycle.

  • Thermal Bridging: The transfer of heat through highly conductive materials, such as steel stanchions, which creates localized condensation points.
  • Differential Movement: The varying rates of expansion and contraction between the structural steel and the roof insulation.
  • Interstitial Condensation: Moisture that traps within the envelope layers, leading to hidden corrosion and mold growth.
  • Mechanical Fatigue: The repeated stressing of flashing joints due to the constant temperature cycling of the freezer units.

Material Science of PMMA and Polyurethane Hybrid Resins

To combat these failures, we utilize a high-performance engineering approach centered on Polymethyl Methacrylate (PMMA) cold-applied resins and polyurethane fleece-reinforced systems. Unlike traditional solvent-based adhesives, PMMA is a thermosetting resin that undergoes a rapid polymerization process. This chemical reaction allows the resin to cure almost instantaneously, regardless of the substrate temperature, making it an ideal candidate for cold storage facilities where traditional heat-welding is impractical or dangerous.

The integration of a non-woven polyester fleece reinforcement transforms the liquid resin into a reinforced composite membrane. By embedding the fleece into the PMMA, we create a "bridge" that can accommodate significant structural movement without rupturing. The polyurethane components provide the necessary elasticity and elongation properties, ensuring that the flashing remains pliable even at sub-zero temperatures. This hybrid approach ensures that the flashing is not merely a coating, but a structural component of the building envelope that distributes mechanical stress across a wider surface area.

  • Rapid Cure Kinetics: PMMA resins cure via a chemical catalyst, allowing for foot traffic and water-tightness within minutes of application.
  • Fleece Embedding: The non-woven fleece acts as a reinforcement matrix, preventing the propagation of cracks and tears.
  • Cold-Applied Versatility: The ability to apply these resins without torches or heat guns reduces the risk of fire and substrate damage.
  • Chemical Resistance: PMMA provides an impervious barrier against industrial pollutants and UV radiation, ensuring long-term surface stability.

Engineering the Critical Detail: I-Beam Stanchion Flashing

The most intricate point of failure in a freezer warehouse is the I-beam stanchion. These structural supports create complex geometries with multiple 90-degree angles and narrow flanges that are notoriously difficult to seal. A master roofer knows that a "wrap and tape" approach is insufficient. Instead, we employ a multi-stage liquid-applied process to ensure a monolithic seal that eliminates all potential points of ingress.

The process begins with rigorous substrate preparation, involving the mechanical grinding of the steel to a bright metal finish to ensure maximum adhesion. We then apply a specialized PMMA primer to neutralize the surface energy of the steel. The flashing is built up in layers: a base coat of PMMA resin, followed by the precision fitting of the fleece reinforcement into the "crotch" of the I-beam, and finally, a saturating top coat of resin. This "sandwich" method ensures that the resin fully penetrates the fleece, creating a seamless, waterproof transition from the horizontal roof deck to the vertical stanchion face.

  • Substrate Profiling: Utilizing diamond-grinding to achieve a CSP 3 (Concrete Surface Profile) or equivalent on steel for optimal mechanical bond.
  • Geometry Management: Applying the resin in a way that eliminates "voids" or air pockets in the tight corners of the I-beam flanges.
  • Monolithic Integration: Creating a single, continuous chemical bond that removes the need for mechanical fasteners or seams.
  • Beveling: Shaping the final resin layer to ensure positive water drainage away from the stanchion base.

Quality Assurance and Long-Term Envelope Integrity

An engineering audit of a cold storage facility is not complete without a rigorous validation of the cure and adhesion. Because PMMA systems rely on precise mixing ratios of resin and catalyst, we employ field-testing protocols to ensure the material has reached its full shore hardness. We utilize pull-tests and needle-probe inspections to verify that there are no delaminations between the resin and the steel substrate, which would otherwise indicate a failure in the surface preparation phase.

From a lifecycle perspective, the shift toward liquid-applied fleece-reinforced systems significantly reduces the maintenance burden on the facility owner. By adhering to ASTM and ANSI standards for commercial roofing, we ensure that the envelope is not only watertight but also vapor-tight. This is critical in freezer warehouses, as the infiltration of warm, moist air into the insulation layer can lead to "ice-jacking," where freezing moisture expands and physically lifts the roofing membrane off the deck.

  • Shore Hardness Testing: Verifying that the PMMA has fully polymerized to its engineered specification.
  • Vapor Drive Analysis: Ensuring the flashing system prevents the migration of water vapor from the warm exterior to the cold interior.
  • Adhesion Testing: Performing ASTM-standard pull tests to confirm the bond strength exceeds the tensile strength of the substrate.
  • Lifecycle Audit: Implementing a bi-annual inspection schedule to monitor the elasticity of the polyurethane components.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #269

Commercial Expansion Joint Bellows & Heavy-Gauge Neoprene Movement Transitions on Commercial Commercial Fleet Maintenance Hangars

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Commercial Expansion Joint Bellows & Heavy-Gauge Neoprene Movement Transitions on Commercial Commercial Fleet Maintenance Hangars

Structural Dynamics and Differential Settlement in Large-Span Hangars

In the engineering of commercial fleet maintenance hangars, the primary challenge is the management of massive structural footprints that are subject to extreme thermal cycling and uneven soil bearing capacities. These facilities often consist of multiple wings or interconnected bays, each acting as an independent structural mass. When these masses are tied together without proper articulation, the resulting internal stresses manifest as shear failure in the roof membrane or catastrophic cracking in the slab. Differential settlement occurs when one wing of the hangar settles at a different rate than the adjacent section, creating a void or a compression point at the building envelope interface.

To mitigate these forces, we implement a strategy of controlled movement. Rather than attempting to resist the movement of several hundred thousand square feet of steel and concrete, we engineer "sacrificial" zones of flexibility. This requires a deep understanding of structural drift and the specific seismic or wind-load requirements of the region. The goal is to ensure that the building envelope remains airtight and watertight regardless of whether the structure is expanding due to summer heat or contracting during a winter freeze.

  • Analysis of thermal expansion coefficients for structural steel versus reinforced concrete.
  • Evaluation of soil compaction reports to predict long-term differential settlement patterns.
  • Identification of critical articulation points where multi-wing junctions meet.
  • Calculation of maximum anticipated displacement across the X, Y, and Z axes.

Engineering the Heavy-Gauge Neoprene Bellows System

The core of our movement transition strategy is the installation of heavy-gauge neoprene expansion bellows. Unlike standard flashing or basic joint fillers, a commercial-grade bellows system is designed to act as a flexible bridge. We specify neoprene for these applications due to its superior resistance to ozone, UV radiation, and the caustic chemicals often found in fleet maintenance environments, such as aviation fuel and degreasers. The material science here focuses on the Shore A hardness and the compression set of the elastomer, ensuring the bellows can return to their original shape after thousands of cycles of expansion and contraction.

The geometry of the bellows is critical. A convoluted design allows the material to stretch and compress without experiencing excessive tensile stress, which would otherwise lead to premature tearing or "necking" of the rubber. By utilizing a heavy-gauge thickness, we provide the necessary structural integrity to withstand wind-driven rain and pressure differentials caused by the massive hangar doors opening and closing, which can create a vacuum effect within the building envelope.

  • Specification of ASTM D2000 compliant neoprene for maximum chemical and weather resistance.
  • Utilization of convoluted bellows geometry to distribute strain across multiple folds.
  • Implementation of reinforced neoprene blends to prevent puncture from wind-borne debris.
  • Engineering of bellows diameters that exceed the maximum calculated structural drift by a safety factor of 1.5.

Critical Tie-In Mechanics and Watertight Integration

The most frequent point of failure in any expansion joint is not the bellows itself, but the tie-in where the elastomer meets the rigid roof or wall assembly. A master roofer knows that a movement joint is only as good as its termination. We employ a redundant sealing strategy that combines mechanical fastening with high-performance elastomeric sealants. The transition from the neoprene bellows to the roof membrane—typically a TPO or modified bitumen system—requires a custom-fabricated transition flashing that allows for lateral movement without peeling away from the substrate.

We utilize heavy-duty stainless steel termination bars and continuous welds to secure the bellows to the structural steel. This prevents the "ballooning" effect during high-wind events. The sealant interfaces are carefully selected to ensure chemical compatibility; using a silicone sealant on a neoprene substrate without the proper primer can lead to adhesion failure. Our process involves a rigorous cleaning sequence and the application of a specialized bonding agent to ensure a molecular bond between the transition flashing and the building envelope.

  • Installation of stainless steel clamping rings to ensure a secure, non-slip grip on the bellows.
  • Application of dual-stage flashing laps to create a "shingle effect" for shedding water.
  • Use of high-modulus polyurethane sealants for superior adhesion to non-porous surfaces.
  • Integration of a secondary internal drainage gutter to capture any seepage before it enters the facility.

Audit Findings and Lifecycle Maintenance Protocols

A comprehensive engineering audit of a fleet maintenance hangar reveals that the majority of leaks occur due to "bottoming out" or "over-extension" of the joint. When a building settles beyond the engineered limits of the bellows, the material is stretched to its limit, leading to stress whitening and eventual rupture. Our audit process involves a physical inspection of the bellows' current state of extension compared to the original "as-built" specifications. We look for signs of ozone cracking—small, perpendicular fissures in the rubber—which indicate that the material has reached the end of its service life due to UV degradation.

To ensure the longevity of the envelope, we establish a strict lifecycle maintenance protocol. This includes quarterly inspections of the termination bars and the re-application of sealants every three to five years. By treating the expansion joints as active mechanical components rather than static building materials, we can predict failure points before they result in water intrusion. This proactive approach protects the high-value assets inside the hangar, including aircraft and diagnostic equipment, from moisture and environmental contaminants.

  • Quarterly verification of bellows elasticity and tension using calibrated measuring tools.
  • Detailed mapping of settlement markers across the hangar floor to track structural drift.
  • Scheduled replacement of sacrificial sealant beads to maintain the primary watertight seal.
  • Thermal imaging scans of the joint interfaces to detect hidden moisture accumulation.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #270

Commercial Kitchen Grease Containment & 304 Stainless Steel Catchment Shielding on Commercial Chemical Processing Facilitys

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Commercial Kitchen Grease Containment & 304 Stainless Steel Catchment Shielding on Commercial Chemical Processing Facilitys

Lipid Degradation and Chemical Interaction with Single-Ply Membranes

In the high-stakes environment of a commercial chemical processing facility, the building envelope is the first line of defense against catastrophic internal and external failures. One of the most overlooked threats to roof longevity in these facilities is the migration of animal fat lipids, typically originating from industrial kitchen exhaust systems or food-grade processing vents. When these lipids settle on a single-ply membrane, such as Thermoplastic Polyolefin (TPO) or Polyvinyl Chloride (PVC), they do not merely sit on the surface; they initiate a complex chemical reaction that compromises the polymer chain.

The primary mechanism of failure is plasticizer migration. Single-ply membranes rely on plasticizers to maintain flexibility and elasticity under extreme thermal cycling. Animal fats act as organic solvents that penetrate the membrane, leaching out these essential plasticizers. This process leads to "embrittlement," where the membrane loses its elongation properties, becomes prone to hairline fractures, and eventually develops deep fissures. In a chemical processing plant, this vulnerability is compounded by the presence of airborne caustic agents, which accelerate the degradation of the lipid-soaked membrane.

  • Plasticizer leaching resulting in a loss of membrane elasticity and increased brittleness.
  • Chemical synergy between animal fats and industrial atmospheric pollutants, creating an acidic slurry.
  • Accelerated UV degradation in areas where lipid deposits have stripped the protective surface layers.
  • Increased risk of puncture failure due to the loss of the membrane's inherent tensile strength.

Engineering 304 Stainless Steel Catchment Shielding

To mitigate the risk of lipid saturation, a master-level engineering approach requires the installation of dedicated catchment systems. We specify 304 Stainless Steel for these shields due to its superior corrosion resistance and ability to withstand the aggressive cleaning agents used in chemical facilities. Unlike galvanized steel or aluminum, 304 Stainless Steel maintains its structural integrity when exposed to the high-temperature grease runoff typical of industrial kitchen vents, preventing the "pitting" that leads to premature leaks.

The design of the catchment box must prioritize fluid dynamics to ensure that grease does not pool or overflow onto the surrounding roof field. This involves precision-engineered sloping—typically a minimum of 1/4 inch per foot—leading to a removable collection tray. The interface between the stainless steel shield and the roof membrane is the most critical point of failure; therefore, we utilize a custom-fabricated flashing detail that allows for thermal expansion and contraction without stressing the membrane bonds.

  • Utilization of 14-gauge 304 Stainless Steel to ensure rigidity and long-term resistance to oxidation.
  • Implementation of precision-welded seams using TIG (Tungsten Inert Gas) welding to ensure a leak-proof containment vessel.
  • Integration of removable grease traps for simplified maintenance and waste disposal.
  • Strategic use of neoprene gasket seals at the penetration points to maintain the building envelope's airtightness.

Sacrificial Chemical-Resistant Coatings and Surface Protection

Even with the most robust catchment systems, the possibility of "over-spill" or accidental discharge remains. To protect the primary roof membrane, we implement a sacrificial coating strategy. A sacrificial coating is a high-build, chemically resistant layer applied over the primary membrane, designed to take the brunt of chemical and lipid exposure. This layer acts as a sacrificial anode in a way, absorbing the damage and preventing the underlying TPO or PVC from coming into direct contact with corrosive lipids.

The preferred material for this application is a reinforced aliphatic polyurea or a specialized chemical-resistant liquid-applied membrane. These coatings are engineered to provide a seamless, non-porous barrier that is virtually impervious to animal fats and common industrial solvents. Because these coatings are "sacrificial," they can be stripped and reapplied every five to ten years without needing to replace the entire roof system, significantly reducing the facility's long-term capital expenditure.

  • Application of high-solids polyurea coatings to create a monolithic, waterproof barrier.
  • Use of reinforced fiberglass mesh within the coating layers to prevent cracking under mechanical stress.
  • Selection of aliphatic chemistry to ensure the coating does not yellow or degrade under intense UV exposure.
  • Strategic zoning of coatings to high-risk "splash zones" around exhaust vents and processing equipment.

Audit Methodology and Long-Term Envelope Integrity

A comprehensive engineering audit of a chemical processing facility's roof must go beyond a simple visual inspection. We employ a rigorous methodology based on ASTM standards to evaluate the health of the building envelope. This begins with a "core sampling" technique, where small sections of the membrane are extracted and analyzed for plasticizer loss and lipid penetration. This quantitative data allows us to predict the remaining service life of the roof and schedule preventative interventions before a leak occurs.

Furthermore, we utilize infrared thermography to identify subsurface moisture and grease pockets that are not visible to the naked eye. In a facility where chemical processing occurs, any breach in the envelope can lead to the ingress of moisture, which may react with internal chemicals to create hazardous conditions. By maintaining a strict audit cycle and adhering to ANSI standards for commercial roofing, we ensure that the containment systems and sacrificial coatings are performing as designed, preserving the structural integrity of the entire facility.

  • Conducting quarterly infrared scans to detect thermal anomalies indicating moisture or grease accumulation.
  • Performing ASTM-standard pull tests on flashing and membrane seams to ensure bond strength.
  • Evaluating the thickness of sacrificial coatings using ultrasonic gauges to determine the timing for re-application.
  • Reviewing drainage efficiency to ensure that grease-laden water is being diverted away from critical structural supports.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #271

Clear-Span Structural Joist Deflection Forensics & Ponding Instability Remediation on Commercial Municipal City Hall & Administrative Complexs

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Clear-Span Structural Joist Deflection Forensics & Ponding Instability Remediation on Commercial Municipal City Hall & Administrative Complexs

Forensic Evaluation of Clear-Span Joist Deflection

In the execution of a comprehensive building envelope audit for a Municipal City Hall and Administrative Complex, the primary engineering challenge often resides in the behavior of long-span structural steel joists. Over decades of service, these members can exhibit center-span deflection, a phenomenon where the structural member bows under its own dead load and the added weight of superimposed loads. When this deflection occurs in a flat-roof assembly, it creates a localized depression that disrupts the intended positive drainage slope, leading to the accumulation of standing water.

To accurately quantify this failure, our team employed high-precision laser-leveling forensics. By establishing a datum line across the primary support columns, we measured the vertical deviation at the mid-point of each joist. We observed that several clear-span sections had exceeded the allowable L/240 deflection limit, creating "bowls" in the roof deck. This is not merely an aesthetic concern; it is a structural vulnerability. Standing water exerts a hydrostatic load of approximately 5.2 pounds per square foot per inch of depth, which further increases the downward force on the joists, exacerbating the deflection in a destructive feedback loop.

  • Utilization of laser-guided topographic mapping to identify low-point basins.
  • Calculation of dead load versus live load capacity under saturated conditions.
  • Assessment of joist camber and potential fatigue in the structural steel webs.
  • Evaluation of the existing deck profile to determine the degree of slope reversal.

The Mechanics of Ponding Instability and Membrane Stress

Ponding instability occurs when the structural deflection of a roof system creates a depression that collects more water than the existing slope can evacuate. As water accumulates, the additional weight causes the joists to deflect further, which in turn allows the basin to hold even more water. In the case of the Municipal Complex, this cycle had reached a critical threshold. The standing water was not only stressing the structural steel but was also subjecting the roofing membrane to prolonged hydrostatic pressure and thermal cycling.

From a material science perspective, the constant presence of water leads to the degradation of the membrane's chemical bonds and increases the risk of seepage through lap seams. In a municipal environment, where the roof often houses critical HVAC equipment and administrative archives, a breach in the envelope can lead to catastrophic interior losses. We identified that the existing membrane was experiencing "ballooning" at the seams due to the weight of the water pushing the membrane into the substrate, creating micro-fissures that allowed moisture to penetrate the insulation layer.

  • Analysis of hydrostatic pressure on heat-welded and adhered seams.
  • Identification of "ponding basins" where water depth exceeded 2 inches for more than 48 hours.
  • Examination of the insulation's saturation levels and subsequent loss of R-value.
  • Measurement of the structural "creep" resulting from long-term loading.

Engineering Remediation via Custom Tapered Polyiso Crickets

To remediate the ponding instability without the prohibitive cost of structural steel reinforcement, we engineered a custom tapered insulation system. The objective was to artificially restore a positive slope to the roof surface, effectively "filling in" the deflection basins. We specified the use of high-density polyisocyanurate (Polyiso) insulation, chosen for its superior compressive strength and thermal resistance. Unlike traditional leveling courses, tapered Polyiso allows for precise control over the water's path, ensuring that gravity works in favor of the building envelope.

The installation involved the fabrication of custom crickets—sloped insulation inserts designed to divert water away from the center-span low points and toward the primary drainage outlets. Each cricket was meticulously cut to match the specific contours of the measured deflection. By installing these tapered sections, we shifted the lowest point of the roof from the center of the joist span to the perimeter drainage system. This process requires a master tradesman's precision to ensure that the transitions between the flat deck and the tapered insulation are seamless, preventing the creation of new, smaller ponding areas.

  • Design of a 1/4" per foot minimum slope to comply with ASTM standards for drainage.
  • Implementation of high-density Polyiso to withstand foot traffic and equipment loads.
  • Precision cutting of tapered panels to eliminate "flat spots" in the remediation zone.
  • Adherence to strict bonding protocols to prevent wind uplift at the tapered edges.

Final Envelope Integration and Outward Water Routing

The final phase of the remediation focused on the integration of the new tapered system into the overall building envelope. Once the Polyiso crickets were secured, the entire assembly was capped with a high-performance, reinforced membrane. The critical engineering focus here was the routing of water. It is not enough to simply move water away from the center; it must be routed efficiently to the scuppers and internal drains without overloading any single point of the perimeter flashing.

We implemented a strategic routing plan that utilized the existing roof geometry to accelerate water flow. By coordinating the taper of the insulation with the placement of the primary drains, we ensured that water followed a predictable, linear path toward the exterior. This eliminated the risk of "water tracking," where moisture travels along the underside of the membrane. The result is a structurally sound, hydraulically efficient roof system that protects the Municipal City Hall from the risks of ponding instability and structural fatigue, ensuring the longevity of the administrative complex for decades to come.

  • Installation of reinforced membrane flashing at all transition points and parapet walls.
  • Verification of scupper capacity to handle increased flow rates from the new slopes.
  • Conducting a final flood test to confirm the total elimination of standing water.
  • Application of a UV-resistant capping layer to protect the polyiso substrate from thermal shock.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #272

Complete Old Roof Tear-Offs Down to Clean Wood Decking & Substrate Remediation on Commercial High-Rise Commercial Penthouse Towers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Complete Old Roof Tear-Offs Down to Clean Wood Decking & Substrate Remediation on Commercial High-Rise Commercial Penthouse Towers

Phase I: Engineering Audit and Total Deconstruction Strategy

In the context of high-rise commercial penthouse towers, the building envelope is subject to extreme atmospheric pressures, high wind-uplift forces, and intense UV degradation. A common industry failure is the practice of "recoveries," where new membranes are installed over existing ones. From an engineering perspective, this creates a catastrophic failure point by masking substrate decay and adding dead load to the structural frame. Our approach at Aquashield Corporate begins with a comprehensive forensic audit, utilizing infrared thermography and moisture probes to map subsurface anomalies before a single square of roofing is removed.

The deconstruction phase is not merely a demolition process but a systematic stripping of the building's protective skin. We execute a complete tear-off down to the original wood decking to eliminate the "sandwich effect," where trapped moisture between legacy layers accelerates the rot of the substrate. This process ensures that the structural integrity of the penthouse tower is fully visible and verifiable, removing all compromised bitumen, felt, and degraded insulation boards.

  • Elimination of cumulative dead load to reduce stress on the building's primary structural members.
  • Removal of legacy adhesives and tars that can outgas and compromise new membrane adhesion.
  • Identification of hidden flashing failures at parapet walls and mechanical curb penetrations.
  • Verification of the original decking layout to ensure alignment with modern load-bearing specifications.

Phase II: Forensic Analysis of Failing Multi-Layer Assemblies

When examining the failed assemblies of a commercial high-rise, we often find a history of reactive maintenance rather than proactive engineering. The failure typically begins at the perimeter, where thermal bridging allows moisture to migrate into the substrate. Over time, capillary action draws this moisture deep into the multi-layer assembly, creating a saturated environment that promotes fungal growth and wood fiber degradation. By stripping the roof to the wood deck, we can analyze the specific failure points of the previous system's chemistry and physics.

Material science dictates that different layers of roofing materials expand and contract at varying rates. In high-rise environments, the temperature differential between the roof surface and the interior penthouse can be extreme. This thermal cycling causes shear stress between layers, leading to delamination and the creation of voids. These voids act as reservoirs for rainwater, which then seeps into the wood decking, compromising the structural capacity of the penthouse floor.

  • Analysis of hygroscopic moisture movement within the old felt and bitumen layers.
  • Evaluation of fastener fatigue and "backing out" caused by decades of thermal expansion.
  • Assessment of chemical degradation in legacy primers and bonding agents.
  • Documentation of water tracking patterns to identify systemic drainage failures.

Phase III: Structural Wood Decking Inspection and Remediation

Once the substrate is exposed, the master roofer's focus shifts to a rigorous structural inspection. Wood decking in high-rise towers must maintain a specific modulus of elasticity to support the roof load and the technicians working upon it. We employ a "probe and press" methodology, utilizing steel probes to check for soft spots and measuring moisture content with calibrated meters. Any section of wood exhibiting signs of wet rot, dry rot, or significant delamination is flagged for immediate remediation.

Remediation is not a matter of simple patching; it is a surgical replacement of compromised structural elements. We ensure that all replacement panels match the original thickness and grade of the existing decking to prevent "lippage," which can cause premature wear on the new membrane. Every new panel is secured using heavy-duty, corrosion-resistant fasteners according to ANSI standards, ensuring that the decking acts as a monolithic diaphragm capable of resisting wind uplift and seismic shifts.

  • Removal of all decayed wood fibers to ensure a clean, sound perimeter for new panel integration.
  • Installation of CDX grade plywood or OSB panels that meet or exceed the original structural specifications.
  • Application of blocking and bridging to ensure seamless transitions between old and new decking.
  • Verification of fastener spacing and penetration depth to prevent substrate splitting.

Phase IV: Substrate Preparation and Engineering for the New Envelope

The final stage of substrate remediation is the preparation of the "clean deck." A clean deck is the foundation of the entire building envelope; if the substrate is contaminated with dust, oils, or old adhesives, the bond of the new system is compromised. We utilize industrial-grade grinding and vacuuming to ensure the wood surface is smooth and free of debris. This preparation phase is critical for the application of high-performance primers that bridge the gap between the organic wood substrate and the synthetic roofing membrane.

From an engineering standpoint, the transition from the wood deck to the final membrane must be seamless. We implement a rigorous quality control checklist that adheres to ASTM D2395 standards for moisture detection and substrate stability. By ensuring the wood decking is dried to a specific moisture percentage before sealing, we prevent the entrapment of water vapor, which would otherwise lead to blistering and premature failure of the new commercial roof system.

  • Mechanical sanding of high points to ensure a perfectly level plane for membrane installation.
  • Application of specialized wood-fiber primers to seal the substrate and enhance chemical bonding.
  • Installation of reinforced flashing at all critical junctions, including HVAC curbs and drainage scuppers.
  • Final engineering sign-off verifying that the substrate is structurally sound and moisture-free.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #273

Stripping Old Shingles Down to Clean Wood Sheathing Across Commercial Eaves on Commercial Regional Healthcare Medical Centers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Stripping Old Shingles Down to Clean Wood Sheathing Across Commercial Eaves on Commercial Regional Healthcare Medical Centers

Systematic Deconstruction and Multi-Layer Audit Protocols

In the context of regional healthcare medical centers, the building envelope is not merely a shelter but a critical component of patient safety and facility uptime. During our engineering audit of these facilities, we frequently encounter the "layering legacy"—a dangerous practice where subsequent roofing contractors installed new shingles over existing ones without stripping the old substrate. This creates a compounding dead load on the roof structure that often exceeds the original design specifications of the rafters and eaves. A master-level approach to stripping these layers requires a systematic deconstruction strategy that prioritizes the preservation of the underlying wood sheathing while ensuring the total removal of all legacy fasteners.

The removal process must be executed with precision to avoid "skinning" the wood sheathing, which occurs when aggressive tearing of shingles rips the top ply of the plywood or OSB. We employ a phased stripping method, utilizing specialized pneumatic power brooms and manual prying tools to lift materials in manageable sections. This allows the engineering team to inspect the eave transitions in real-time, identifying areas of moisture infiltration that may have been hidden for decades. By stripping down to the clean wood, we expose the true condition of the building envelope, allowing for a forensic analysis of the wood's cellular integrity.

  • Assessment of cumulative dead load increases caused by multi-layer shingle installations.
  • Implementation of phased stripping to prevent sudden structural shifts in aged rafters.
  • Utilization of high-torque removal tools to extract legacy nails without splitting the sheathing.
  • Continuous monitoring of eave drip edges for signs of chronic saturation and fungal decay.
  • Establishment of a debris management zone to prevent healthcare facility operational disruptions.

Fastener Withdrawal Resistance and Substrate Analysis

Once the decking is stripped clean, the focus shifts to the material science of the substrate. A critical failure point in commercial medical centers is the loss of fastener withdrawal resistance. Over time, the repeated cycle of heating and cooling, combined with potential moisture intrusion, causes the wood fibers around old nail holes to degrade. This phenomenon, often referred to as "nail sickness," means that new fasteners may not achieve the required grip, leading to wind uplift vulnerabilities that violate ANSI and ASTM standards for commercial roofing.

Our engineering protocol involves a rigorous testing phase where we measure the pull-out strength of fasteners in various zones of the eave. If the wood sheathing exhibits signs of delamination or "punky" wood—where the lignin has broken down—the substrate is deemed compromised. We analyze the difference between legacy planking and modern engineered wood products, as each reacts differently to fastener stress. In healthcare environments, where the roof must withstand extreme weather events to protect sensitive medical equipment, ensuring that every fastener is anchored into sound, dense wood is a non-negotiable requirement of the building envelope audit.

  • Conducting pull-tests to quantify the Newton-meters of force required for fastener failure.
  • Evaluating the chemical composition of the wood for signs of dry rot or wet rot.
  • Analyzing the spacing of original rafters to ensure they meet current structural load codes.
  • Identifying "ghosting" patterns where previous leaks have weakened the internal wood fibers.
  • Mapping fastener patterns to avoid reusing compromised holes in the new installation.

Structural Remediation and Rafter Sistering Techniques

The eaves of a medical center are the most vulnerable points of the roof system, often bearing the brunt of water shedding and snow accumulation. During the stripping process, we frequently discover rafters that have suffered from longitudinal splitting or localized rot. When a rafter's structural integrity is compromised, simple patching is insufficient. We employ a professional "sistering" technique, which involves installing a new, high-grade structural member alongside the existing rafter to redistribute the load and restore the original design strength.

Sistering is not merely about adding more wood; it is an engineering exercise in load path continuity. We specify the use of LVL (Laminated Veneer Lumber) or kiln-dried Douglas Fir, depending on the existing material. The new member is precision-cut to fit tightly against the ridge and the eave plate, then secured using a staggered nailing pattern and structural adhesives. This creates a composite beam that is often stronger than the original. This process ensures that the roof can support the new roofing system and any additional HVAC or medical gas venting equipment required by the facility's expansion.

  • Selection of sistering materials based on the original species and moisture content of the rafters.
  • Application of structural-grade adhesives to ensure a monolithic bond between the old and new members.
  • Implementation of staggered fastening patterns to prevent splitting the existing wood.
  • Verification of load-bearing transfers from the eave to the primary wall plates.
  • Inspection of all sistered joints for gaps that could allow moisture to bypass the envelope.

Establishing the Flat Decking Plane for Membrane Integration

The final stage of the stripping and remediation process is the establishment of a perfectly flat decking plane. In commercial roofing, particularly when transitioning to high-performance membranes or modified bitumen, any irregularity in the substrate can lead to "ponding" or premature membrane fatigue. After stripping old shingles and sistering rafters, the decking often exhibits "waves" or dips. These irregularities are the result of years of structural settling and the uneven removal of legacy materials.

To achieve a professional engineering grade surface, we perform a comprehensive leveling operation. This involves the removal of any remaining nail heads, the sanding of high spots, and the installation of tapered sleepers or shims in low-lying areas. We treat the decking as a singular, monolithic plane, ensuring that the transition from the main roof field to the eaves is seamless. This precision prevents the formation of air pockets and ensures that the new roofing system adheres uniformly across the entire surface, providing the medical center with a watertight seal that meets the highest industry standards for building envelope longevity.

  • Mechanical grinding of high spots to prevent "telegraphing" through the new roof membrane.
  • Installation of marine-grade plywood patches to replace sections of rotted sheathing.
  • Verification of the plane using laser levels to ensure positive drainage toward the eaves.
  • Application of a primer or sealant to the clean wood to prevent moisture absorption before membrane lay-down.
  • Final audit of the decking surface to confirm a zero-tolerance fit for the new commercial roofing system.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #274

Low-VOC Cold-Applied Adhesives & HVAC Air Intake Odor Mitigation Protocols on Commercial University Research Laboratorys

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Low-VOC Cold-Applied Adhesives & HVAC Air Intake Odor Mitigation Protocols on Commercial University Research Laboratorys

The Engineering Challenge: Envelope Integrity in High-Sensitivity Environments

When auditing a University Research Laboratory, the building envelope is not merely a weather barrier; it is a critical component of the facility's life-safety and research integrity systems. In these environments, the primary engineering challenge is the management of pressure differentials. Research labs often operate under negative pressure to prevent hazardous materials from escaping the lab, but this creates a vacuum effect that can pull external contaminants through the building envelope if the seal is compromised. The specific focus of this case study involves the remediation of flashing failures and membrane bonding near primary HVAC air intake plenums.

The risk profile for this project was heightened by the presence of sensitive mass spectrometry equipment and clean-room environments. Traditional solvent-based adhesives, which rely on volatile organic compounds (VOCs) for rapid evaporation and bonding, were ruled out immediately. The introduction of solvent fumes into the HVAC intake would have triggered facility-wide alarms, forced the evacuation of researchers, and potentially contaminated multi-year longitudinal studies. Therefore, the engineering objective was to identify a bonding system that provided industrial-grade structural adhesion without the associated off-gassing profiles.

  • Assessment of existing EPDM and TPO membrane degradation at the curb transitions.
  • Analysis of HVAC intake proximity to roof-level flashing points.
  • Evaluation of substrate moisture content to prevent osmotic blistering during adhesive application.
  • Mapping of air-flow vectors to determine the "critical zone" for odor mitigation.

Material Science: Low-VOC Polyurethane Bonding Agents

To meet the stringent requirements of the university, we transitioned from traditional solvent-based primers to a high-performance, cold-applied polyurethane (PU) bonding agent. From a material science perspective, polyurethane adhesives are superior in this application because they rely on a chemical reaction between a polyol and an isocyanate, rather than the evaporation of a solvent. This results in a "zero-VOC" or "low-VOC" profile that eliminates the risk of odor migration into the building's interior air supply.

The selected polyurethane agent was engineered for rapid-setting capabilities, achieving a structural tack within minutes and a full cure within 24 hours. This is critical for commercial roofing where wind uplift and thermal cycling can compromise a slow-curing bond. Furthermore, the adhesive's coefficient of thermal expansion was matched to the existing roof membrane, ensuring that as the building shifts and breathes under varying temperatures, the bond remains flexible and resistant to delamination. We adhered to ASTM D-series standards for peel strength and shear resistance to validate the bond's longevity.

  • Utilization of moisture-curing polyurethane for enhanced substrate wetting.
  • Implementation of a two-part mixing ratio to ensure consistent cross-linking of the polymer chains.
  • Verification of shore hardness to ensure the bond is not too brittle for high-vibration areas near HVAC fans.
  • Application of a UV-stable capping sealant to protect the PU bond from solar degradation.

Containment Protocols: HVAC Air Intake Mitigation

Even with low-VOC materials, a master-level engineering approach requires a "defense-in-depth" strategy for air intake containment. The protocol began with the establishment of a physical containment barrier. We utilized 6-mil flame-retardant polyethylene sheeting to encapsulate the HVAC intake plenums, creating a temporary airtight seal. This ensured that any incidental odors from the cleaning of the substrate—such as the use of specialized degreasers—were trapped and filtered before they could enter the building's ventilation system.

To further mitigate risk, we employed a localized negative pressure strategy. By utilizing portable HEPA-filtered air scrubbers positioned on the roof, we created a directional airflow that pulled air away from the intake and toward the filtration unit. This created a "safe zone" around the work area, ensuring that the air pressure at the intake was higher than the pressure at the application point. This engineering control effectively neutralized the possibility of fumes migrating downward into the laboratory spaces, allowing the facility to remain fully operational during the remediation process.

  • Installation of temporary gaskets around intake curbs to prevent seepage.
  • Deployment of real-time VOC monitors at the intake perimeter to trigger immediate work stoppage if thresholds were exceeded.
  • Strategic placement of air scrubbers to maintain a constant outward flow from the intake zone.
  • Strict adherence to a "clean-to-dirty" workflow to prevent cross-contamination of the roof surface.

Execution and Validation: Zero-Downtime Implementation

The execution phase was designed around the concept of zero-downtime. In a university research setting, the cost of a facility shutdown exceeds the cost of the roofing project by several orders of magnitude. We employed a phased approach, dividing the roof into quadrants and executing the bonding and sealing process in rapid successions. By utilizing cold-applied adhesives, we eliminated the need for heat-welding or open flames, which would have triggered the building's fire suppression systems and required a "fire watch" protocol, further complicating the timeline.

Validation of the repair was conducted through a series of non-destructive tests. We utilized infrared thermography to ensure there were no voids or air pockets within the polyurethane bond, as these could lead to future leaks or structural failures. Additionally, we performed a vacuum-box test on the critical seals around the HVAC curbs to verify a 100% airtight seal. The final audit confirmed that the building envelope's integrity was restored, the air intake remained uncontaminated throughout the process, and the research labs continued their operations without a single minute of interruption.

  • Phased application schedule to maintain continuous roof drainage and safety.
  • Post-installation thermal imaging to validate bond homogeneity.
  • Vacuum-box testing to certify the airtightness of the curb-to-membrane transition.
  • Final documentation of ASTM compliance for the university's facilities management records.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #275

Solar Photovoltaic Ballasted Racking Point-Load Defense & Sacrificial Slip Sheets on Commercial Suburban Corporate Office Parks

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Solar Photovoltaic Ballasted Racking Point-Load Defense & Sacrificial Slip Sheets on Commercial Suburban Corporate Office Parks

The Mechanics of Point-Load Compression in Ballasted Systems

In the context of suburban corporate office parks, the shift toward solar photovoltaic (PV) integration often leads to the implementation of ballasted racking systems. While these systems are favored for avoiding roof penetrations, they introduce significant static point-loads that can compromise the building envelope if not engineered with precision. As a master roofer, I have observed a recurring failure in the industry: the failure to account for the compression set of the underlying insulation. Most commercial roofs utilize Polyisocyanurate (Polyiso) insulation, which, while thermally efficient, has a finite compressive strength. When heavy concrete blocks are placed directly onto the membrane, the load is concentrated into a small footprint, potentially crushing the insulation cells.

This compression set leads to a permanent deformation of the roof deck, creating "low spots" where ponding water accumulates. Once the insulation is crushed, the structural integrity of the thermal barrier is lost, and the membrane is subjected to increased stress during thermal cycling. To mitigate this, we must analyze the load distribution through the lens of ASTM standards for compressive resistance. The goal is to ensure that the pounds-per-square-inch (PSI) exerted by the ballast does not exceed the rated capacity of the insulation board.

  • Analysis of dead loads versus live loads to determine total roof stress.
  • Evaluation of Polyiso density ratings to prevent long-term cellular collapse.
  • Assessment of structural steel decking to ensure no localized bowing occurs under ballast weight.
  • Calculation of the "footprint" of the racking system to distribute weight across a broader surface area.

Sacrificial Slip-Sheet Engineering and Abrasion Mitigation

The interface between a concrete ballast block and a TPO or EPDM membrane is a high-friction zone. Over time, the building undergoes natural thermal expansion and contraction, causing the solar array to shift incrementally. Without a protective barrier, this movement creates a "grinding" effect, where the concrete block acts as an abrasive, slowly wearing through the membrane's wear layer. To combat this, Aquashield Corporate utilizes heavy-duty sacrificial slip-sheets. These are not mere scraps of rubber, but engineered barriers designed to decouple the ballast from the primary waterproofing layer.

The material science behind these slip-sheets focuses on a low coefficient of friction and high puncture resistance. By installing a reinforced, non-adhered slip-sheet, we create a sacrificial layer that absorbs the mechanical energy of the shift. If the slip-sheet is compromised over a twenty-year lifecycle, it can be replaced without needing to strip the entire roof system. This approach transforms the point of failure from the critical building envelope to a replaceable accessory, ensuring the primary membrane remains untouched by the abrasive forces of the concrete blocks.

  • Utilization of high-density polyethylene (HDPE) or reinforced TPO liners as slip-sheets.
  • Implementation of oversized dimensions to ensure the ballast block never overhangs the protection.
  • Monitoring of thermal drift patterns to determine the necessary thickness of the abrasion barrier.
  • Application of UV-stabilized materials to prevent degradation at the edges of the slip-sheet.

Pre-fabricated Target Patches and Strategic Membrane Reinforcement

A common oversight in corporate office park solar installs is the reliance on the standard membrane thickness to handle concentrated loads. In my experience, the most robust defense is the implementation of pre-fabricated target patches. Rather than attempting to reinforce the entire roof, we identify the exact coordinates where the racking feet and ballast blocks will reside. We then install fully adhered, reinforced membrane patches—essentially "armor plating" for the roof—at these specific points. These patches are typically thicker than the field membrane and are heat-welded or chemically bonded to create a seamless, monolithic bond.

These target patches serve two purposes: they provide an extra layer of puncture resistance and they distribute the vertical load more evenly across the insulation. By increasing the thickness of the membrane at the point of contact, we reduce the risk of "stress cracking" that occurs when a membrane is stretched tight over a hard edge. This engineering approach aligns with ANSI standards for roof durability, ensuring that the most vulnerable points of the envelope are the most heavily reinforced.

  • Precision mapping of racking layouts to align target patches with ballast locations.
  • Use of reinforced PVC or TPO patches with a minimum thickness of 60 mils.
  • Heat-welding of patch perimeters to eliminate water infiltration paths.
  • Verification of bond strength through non-destructive pull tests on sample patches.

Cable Tray Routing and Envelope Integrity Management

The final stage of a solar installation is often the most dangerous for the building envelope: the routing of electrical conduits and cable trays. In many corporate office parks, installers simply lay cable trays across the roof, securing them with additional ballast. However, if these trays are not routed correctly, they can create "debris traps" where organic matter and pollutants accumulate, leading to chemical degradation of the membrane. Furthermore, the points where these cables penetrate the roof to enter the building are the primary sources of leaks if not executed with master-level craftsmanship.

We mandate the use of engineered cable trays that are elevated slightly off the roof surface, allowing for proper drainage and inspection. For the penetrations, we move away from standard "boot" flashing in favor of custom-fabricated curb flashings and liquid-applied flashing membranes. This ensures a redundant seal that can withstand the vibration of the building and the thermal movement of the conduits. Proper routing prevents the cables from rubbing against the membrane and ensures that the building envelope remains a closed system, free from the haphazard punctures often associated with rapid solar deployments.

  • Installation of elevated cable trays to maintain clear drainage paths to roof drains.
  • Use of liquid-applied flashing systems for complex conduit penetrations.
  • Routing cables away from high-traffic maintenance zones to prevent accidental damage.
  • Implementation of stainless steel fasteners and supports to prevent galvanic corrosion.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #276

OSHA-Compliant Skylight Fall-Protection Curbs & Heavy-Duty Security Screens on Commercial Big-Box Retail Power Centers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
OSHA-Compliant Skylight Fall-Protection Curbs & Heavy-Duty Security Screens on Commercial Big-Box Retail Power Centers

Structural Integrity and Fall-Arrest Anchoring Systems

In the context of Big-Box Retail Power Centers, the roof is a massive, monolithic expanse where skylights represent critical vulnerabilities. From an engineering perspective, a skylight is not merely a light source but a potential void in the walking surface. To meet OSHA 1910.28 and 1910.29 standards, the installation of fall-protection screens must move beyond basic aesthetics to true structural load-bearing capacity. The primary objective is the mitigation of a fall-through event, requiring the system to withstand a concentrated load of 200 lbs without catastrophic failure of the anchoring mechanism or the underlying curb.

The engineering of these screens begins with the load path. When a worker falls into a screen, the force is not static; it is a dynamic impact. We calculate the shear strength of the fasteners based on the substrate—typically galvanized steel curbs or reinforced concrete. Using oversized stainless steel fasteners with integrated washers ensures that the pull-out force is distributed across a wider surface area of the curb, preventing the "zipper effect" where fasteners tear through the metal during a high-velocity impact.

  • Calculation of point-load distribution to ensure the curb does not buckle under 200-lb impact.
  • Utilization of Grade 5 or higher structural bolts to ensure shear resistance.
  • Implementation of heavy-duty expanded metal mesh (minimum 10-gauge) to prevent limb penetration.
  • Verification of weld integrity on screen frames to ensure the frame acts as a single rigid body.

Curb Flashing Elevation and Water Management Strategy

The building envelope is only as strong as its weakest transition. In commercial roofing, the skylight curb is one of the most frequent points of failure. Proper curb flashing elevation is not a suggestion; it is a requirement for long-term waterproofing. If the flashing is set too low, wind-driven rain—especially in high-velocity wind zones common to large-scale retail parks—can be forced upward and under the membrane via capillary action, leading to interior leaks and structural rot.

Our standard for Big-Box installations requires a minimum flashing height of 8 inches above the finished roof surface. This elevation creates a sufficient buffer against snow accumulation and prevents "ponding" at the base of the curb. We utilize a multi-layered approach, starting with a base ply of reinforced TPO or EPDM, followed by a custom-fabricated metal drip edge that is mechanically fastened and chemically sealed. This ensures that water is shed away from the curb interface and back onto the primary roof membrane.

  • Application of a reinforced flashing membrane to eliminate stress cracks at the curb corners.
  • Installation of a secondary water-stop sealant at the transition between the metal curb and the roof deck.
  • Evaluation of slope-to-drain patterns to ensure water does not migrate toward the skylight assembly.
  • Use of high-performance flashing adhesives that maintain flexibility during extreme thermal cycling.

Compression Termination Bars and Mechanical Fastening

A common failure in commercial roofing is the reliance on adhesives alone to secure the membrane at the curb. In a high-wind event, the "vacuum effect" created over the roof of a Big-Box center can create massive uplift forces. To counteract this, we implement compression termination bars. These are heavy-duty aluminum or galvanized steel bars that mechanically lock the membrane against the vertical face of the curb, creating a permanent, airtight, and watertight seal.

The engineering focus here is on the "compression set." The termination bar must be fastened at precise intervals—typically every 6 to 12 inches—to ensure uniform pressure across the entire length of the membrane. This prevents the membrane from "ballooning" or pulling away from the substrate. We specify the use of stainless steel fasteners with neoprene washers to provide a gasketed seal, ensuring that the fastener itself does not become a leak path into the building envelope.

  • Selection of 1-inch by 1/2-inch aluminum termination bars for maximum rigidity.
  • Application of a termination sealant bead behind the bar to create a redundant moisture barrier.
  • Strict adherence to fastener spacing to prevent membrane bridging or sagging.
  • Verification of torque specifications to avoid crushing the membrane while maintaining a tight seal.

Thermal Gaskets and Material Science in the Envelope

The final layer of a professional skylight installation involves the management of thermal bridging and air infiltration. Big-Box retail centers are subject to extreme temperature fluctuations, causing the metal curbs and the roof membrane to expand and contract at different rates. Without proper thermal gaskets, this movement leads to fatigue in the sealants and eventually results in air leaks that compromise the HVAC efficiency of the facility.

We utilize closed-cell EPDM or silicone gaskets between the security screen frame and the curb. These materials are chosen for their high compression set and resistance to UV degradation. Unlike standard caulking, which can harden and crack over time, a high-grade thermal gasket maintains its elasticity, absorbing the movement of the building. This not only prevents water ingress but also stops the infiltration of unfiltered air, which is critical for maintaining the internal climate of a large-scale retail environment.

  • Integration of high-density EPDM gaskets to eliminate thermal bridging between the curb and the screen.
  • Use of silicone-based sealants for their superior adhesion to non-porous metal surfaces.
  • Analysis of the Coefficient of Thermal Expansion (CTE) to select materials that move in tandem.
  • Implementation of a continuous thermal break to reduce energy loss through the roof penetration.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #277

Rooftop Mechanical Unit Vibration Isolation Rails & Spring-Mounted Curb Seals on Commercial Food Packaging & Cold Logistics Plants

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Rooftop Mechanical Unit Vibration Isolation Rails & Spring-Mounted Curb Seals on Commercial Food Packaging & Cold Logistics Plants

The Engineering Challenge of High-Output Mechanicals in Cold Logistics

In the specialized environment of food packaging and cold logistics plants, the rooftop is more than a weather barrier; it is a critical component of the facility's thermal envelope and structural integrity. These facilities typically house massive industrial refrigeration units, high-capacity HVAC systems, and heavy-duty exhaust fans that operate on 24/7 cycles. The primary engineering challenge lies in the intersection of extreme temperature differentials—where interior cold storage meets exterior ambient heat—and the immense mechanical energy generated by these systems. When these units are bolted directly to a roof curb, the resulting energy transfer can lead to premature fatigue of the roof membrane and structural compromise of the decking.

A comprehensive building envelope audit reveals that the most frequent points of failure occur at the penetration points where mechanical curbs meet the roof surface. In cold logistics, the constant cycling of compressors creates a rhythmic oscillation. If this energy is not managed, it manifests as harmonic vibration, which can physically "saw" through a standard TPO or PVC membrane over time. To prevent this, a master-level approach requires moving beyond standard flashing and implementing a decoupled system that isolates the mechanical load from the waterproof membrane.

  • Thermal Bridging: The risk of heat gain entering the cold storage zone through uninsulated mechanical curbs.
  • Differential Movement: The tendency of heavy equipment to shift at a different rate than the building's structural steel during thermal expansion.
  • Membrane Abrasion: The physical wearing down of the flashing due to micro-movements caused by equipment vibration.
  • Load Distribution: The necessity of spreading the point-load of heavy refrigeration units across a wider structural footprint to avoid decking deflection.

Harmonic Vibration Mitigation and Spring-Isolated Rail Systems

To address the issue of mechanical resonance, we implement vibration isolation rails utilizing spring-mounted curb systems. Unlike simple neoprene pads, which can degrade under UV exposure and lose their elasticity, spring-isolated systems provide a calculated spring constant that offsets the natural frequency of the equipment. By decoupling the mechanical unit from the roof structure, we ensure that the kinetic energy produced by the motors is absorbed by the spring assembly rather than being transmitted into the roof deck. This prevents the development of stress cracks in the substrate and protects the watertight seal of the building envelope.

From an engineering standpoint, the goal is to move the system's resonant frequency away from the operating frequency of the equipment. This is achieved by selecting rails with specific load-bearing capacities and damping coefficients. When these rails are properly integrated into the curb design, they act as a shock absorber for the entire rooftop assembly. This is particularly critical in food packaging plants where precision equipment inside the facility can be affected by external rooftop vibrations, potentially impacting the calibration of weighing and packaging machinery.

  • Frequency Tuning: Adjusting the spring stiffness to ensure the equipment does not hit a harmonic peak that could cause structural resonance.
  • Damping Coefficients: Utilizing high-damping alloys in the spring mounts to dissipate energy as heat rather than motion.
  • Load Leveling: Ensuring the rails are perfectly plumb to prevent uneven weight distribution, which could lead to localized membrane tearing.
  • ANSI/ASTM Compliance: Adhering to strict standards for mechanical vibration isolation to ensure long-term structural stability.

Advanced Sealant Science: Fiber-Reinforced Structural Mastics

The transition between a rigid, spring-isolated curb and a flexible roof membrane is the most vulnerable area of the building envelope. Standard caulking or sealant beads are insufficient for this application because they cannot withstand the shear forces generated by the movement of the isolation rails. Instead, we employ fiber-reinforced structural mastics. These materials are engineered with a high solids content and integrated synthetic fibers that provide internal reinforcement, allowing the sealant to bridge gaps and maintain a watertight seal even under significant stress.

The chemistry of these mastics is designed for high elasticity and superior adhesion to both the metal of the curb and the polymer of the roof membrane. By creating a "bridge" of fiber-reinforced material, we establish a redundant seal that accommodates the coefficient of thermal expansion (CTE) differences between the steel rails and the roof surface. This ensures that as the building breathes and the equipment vibrates, the seal stretches and recovers without developing the micro-fissures that typically lead to capillary leaks and subsequent insulation saturation.

  • Tensile Strength: The ability of the fiber-reinforced mastic to resist tearing under the lateral pull of vibrating equipment.
  • Elongation Properties: Ensuring the sealant can stretch up to 300% of its original width without losing its bond.
  • Adhesion Promotion: The use of specialized primers to ensure a chemical bond between the mastic and the TPO/PVC membrane.
  • UV Stability: Utilizing materials that resist ozone degradation and solar radiation to prevent the sealant from becoming brittle.

Long-Term Envelope Integrity and Maintenance Auditing

A successful installation is only as good as its long-term performance. In the context of cold logistics, the auditing process must be rigorous and recurring. We utilize a multi-stage verification process to ensure that the vibration isolation systems and curb seals remain intact. This begins with a flood test or electronic leak detection (ELD) to confirm the initial watertight integrity of the curb flashing. Following this, we implement a scheduled audit cycle that focuses on the physical inspection of the mastic seals and the tension of the spring mounts.

The final layer of protection is the monitoring of thermal bridging. In cold storage plants, if the curb is not properly thermally broken, condensation can form on the interior side of the curb, leading to hidden corrosion and mold growth. By integrating closed-cell spray foam insulation around the curb and sealing it with the same fiber-reinforced mastics used on the exterior, we create a continuous thermal and moisture barrier. This holistic approach ensures that the mechanical efficiency of the plant is maintained while the structural integrity of the roof is preserved for the duration of its design life.

  • Infrared Thermography: Using thermal imaging to detect heat leaks or moisture accumulation around the mechanical curbs.
  • Compression Set Analysis: Checking the spring mounts to ensure they have not "bottomed out" or lost their ability to isolate vibration.
  • Sealant Creep Monitoring: Inspecting the mastic for signs of permanent deformation or pulling away from the substrate.
  • Water Penetration Testing: Performing ASTM-standard hose tests to verify that the curb-to-roof transition remains impervious to wind-driven rain.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #278

Industrial Corrosive Chemical Fume Exhaust Defense on Commercial Semiconductor Cleanroom Fabs

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Industrial Corrosive Chemical Fume Exhaust Defense on Commercial Semiconductor Cleanroom Fabs

Atmospheric Corrosive Audits and the Semiconductor Envelope

In the high-stakes environment of semiconductor fabrication, the building envelope is not merely a weather barrier; it is the primary line of defense against a volatile internal atmosphere. During our recent engineering audit of a Tier-1 Cleanroom Fab, we identified a critical vulnerability in the roof assembly surrounding the chemical exhaust scrubbers. These facilities utilize aggressive acid-gas scrubbing systems that, while effective at cleaning the air, often create localized "corrosive corridors" where residual hydrofluoric (HF) and nitric acid (HNO3) fumes can linger near the roof surface during atmospheric inversions or equipment malfunctions.

A master-level audit requires looking beyond the surface membrane to evaluate how these fumes interact with the entire assembly. We observed that standard commercial roofing specifications often fail to account for the synergistic effect of high-velocity exhaust heat and chemical condensation. When these acid fumes settle on a cool membrane, they create a low-pH environment that can rapidly degrade standard polymers, leading to premature embrittlement and systemic failure of the waterproofing layer.

  • Evaluation of exhaust plume dispersion patterns to identify high-risk "hot zones" for chemical deposition.
  • Assessment of substrate pH levels to determine the extent of acid penetration through the primary membrane.
  • Inspection of flashing details around oversized HVAC curbs and scrubber penetrations for signs of chemical etching.
  • Analysis of the interface between the roof membrane and metal cladding to prevent galvanic corrosion.

Material Science and Chemical Resistance Profiles

Selecting a membrane for a semiconductor fab requires a deep dive into polymer science. Most commercial roofers default to TPO (Thermoplastic Polyolefin) due to cost and reflectivity, but in a corrosive chemical environment, TPO can be a liability. The polyolefin component is susceptible to certain industrial solvents and oils, which can cause the membrane to swell or lose its structural integrity. For this specific application, we evaluated the chemical resistance of Reinforced PVC (Polyvinyl Chloride) and Modified Bitumen, weighing their performance against ASTM standards for chemical compatibility.

PVC membranes, when engineered with a high-grade plasticizer package, offer superior resistance to the acids typically found in semiconductor exhaust. The chlorine content in the PVC polymer chain provides a natural defense against the oxidative stress caused by nitric acid fumes. However, the critical failure point is often not the membrane face, but the seams. We specify heat-welded seams over adhesive-bonded laps because a weld creates a monolithic bond that eliminates the "glue line" vulnerability where chemicals can seep and dissolve the adhesive bond.

  • PVC (Polyvinyl Chloride): High resistance to acids and bases, excellent weldability, but sensitive to certain plasticizer-leaching oils.
  • TPO (Thermoplastic Polyolefin): Good UV resistance, but prone to degradation when exposed to aggressive industrial solvents.
  • Modified Bitumen: Robust physical properties, but lacks the chemical agility and seamless integration required for cleanroom environments.
  • ASTM D5313: Utilizing standard test methods for assessing the chemical resistance of plastics to ensure long-term stability.

Plasticizer Retention and the Impact of Industrial Oils

One of the most overlooked aspects of building envelope engineering in industrial settings is plasticizer migration. PVC membranes rely on plasticizers—small molecules embedded in the polymer matrix—to remain flexible. In a semiconductor fab, the roof is often subjected to motor oils from massive centrifugal chillers and lubricants from exhaust fan bearings. When these oils come into contact with the membrane, they can trigger a process called "leaching," where the plasticizers migrate out of the membrane and into the oil, or conversely, external oils penetrate the membrane and disrupt the polymer chain.

This migration leads to a catastrophic loss of elasticity. A membrane that was once flexible enough to handle thermal expansion and contraction becomes brittle. Once the plasticizer levels drop below a critical threshold, the membrane develops "micro-cracks." In a corrosive environment, these cracks act as conduits, allowing acid fumes to bypass the membrane and attack the insulation and roof deck. Our audit revealed that without a dedicated oil-resistant capping layer or a high-performance fluoropolymer coating, the membrane's service life is effectively halved.

  • Monitoring the "Shore A" hardness of the membrane over time to track the loss of flexibility.
  • Implementing oil-containment curbs and drip pans to prevent direct lubricant contact with the roofing system.
  • Analyzing the migration rate of phthalates to ensure the membrane maintains its design elongation properties.
  • Evaluating the use of non-plasticized PVC (nPVC) in high-oil zones to eliminate the risk of leaching entirely.

Engineering the Defense: Final Specification and Execution

To secure the building envelope of a semiconductor fab, we move away from commodity roofing and toward a specialized engineering specification. The goal is to create a chemically inert, seamless shield. Our recommended specification involves a dual-layer approach: a reinforced, high-performance PVC base membrane for structural waterproofing, topped with a chemical-resistant liquid-applied polyurea or a fluoropolymer coating in the exhaust zones. This "belt and suspenders" approach ensures that even if the top coating is mechanically damaged, the primary PVC layer remains protected from direct chemical attack.

Execution is where the master tradesman separates himself from the general contractor. We mandate a rigorous quality control protocol that includes vacuum testing of every single weld and the use of electronic leak detection (ELD) across the entire roof field. Furthermore, the termination details must be executed with chemical-resistant sealants that are compatible with the membrane's chemistry, preventing the "edge-creep" that often leads to leaks at the parapet walls. By adhering to these stringent engineering standards, we ensure the fab's critical infrastructure remains dry and the cleanroom environment remains uncontaminated.

  • Specification of a minimum 60-mil reinforced PVC membrane with a specialized acid-resistant formulation.
  • Requirement for robotic heat-welding on all primary seams to ensure 100% consistency and eliminate human error.
  • Installation of a secondary chemical-resistant fluid-applied membrane around all scrubber exhaust vents.
  • Implementation of a quarterly thermal imaging and pH-sweep audit to detect early-stage chemical degradation.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565

Commercial Engineering Dossier #279

Active Emergency Leak Catchment Tarps & Interior Production Bay Diversion on Commercial Intermodal Cargo Freight Terminals

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Active Emergency Leak Catchment Tarps & Interior Production Bay Diversion on Commercial Intermodal Cargo Freight Terminals

Building Envelope Forensic Audit of Intermodal Freight Terminals

In the high-stakes environment of an intermodal cargo freight terminal, the building envelope is subject to extreme mechanical stresses and environmental volatility. A comprehensive engineering audit of these facilities often reveals a pattern of systemic failure centered around thermal bridging and structural deflection. Because these terminals utilize massive clear-span roof systems to accommodate cargo movement, the roof is prone to significant ponding and diaphragm movement. When the primary waterproofing membrane—typically a modified bitumen or a single-ply TPO system—suffers a breach, the resulting infiltration is not a mere drip but a high-volume hydraulic event that threatens millions of dollars in logistics equipment.

The failure points are typically concentrated at the critical junctions where the roof deck meets the parapet walls or around oversized HVAC penetrations. In intermodal facilities, the constant vibration from heavy machinery and gantry cranes can accelerate the fatigue of flashing membranes, leading to hairline fractures in the sealant. Once the building envelope is compromised, the water typically follows the path of least resistance along the underside of the insulation board, often traveling several feet from the actual leak source before manifesting as a ceiling breach. This phenomenon makes precise leak detection difficult and necessitates an immediate, aggressive diversion strategy to prevent catastrophic interior damage.

  • Structural deflection causing "bowl" effects and localized ponding.
  • Thermal expansion and contraction cycles leading to membrane splitting at the seams.
  • Vibration-induced fatigue of flashing and counter-flashing assemblies.
  • Degradation of sealant joints due to industrial pollutants and exhaust.
  • Compromised fasteners leading to wind-uplift and membrane tearing.

Engineering the Industrial Vinyl Diversion System

When a primary roof system fails in a production bay, the immediate priority is the deployment of an active emergency leak catchment system. We do not utilize standard polyethylene tarps, which lack the tensile strength and puncture resistance required for industrial environments. Instead, we specify heavy-duty, reinforced PVC vinyl diverter tarps. These materials are engineered with a high-denier polyester scrim that provides the necessary dimensional stability to withstand the weight of accumulated rainwater without stretching or sagging, which would otherwise create new pockets of standing water.

The engineering of the catchment system relies on the principle of controlled gravity diversion. The vinyl tarps are strategically suspended beneath the roof deck using high-tension aircraft cable or heavy-duty industrial strapping. By creating a precise slope—typically a minimum of 1/4 inch per foot—we ensure that water is captured at the breach point and channeled rapidly toward a designated collection area. This prevents the water from migrating across the ceiling joists and dropping onto sensitive electronic sorting systems or cargo containers.

  • Utilization of 18oz to 22oz reinforced PVC vinyl for maximum puncture resistance.
  • Implementation of heat-welded seams to ensure a 100% watertight catchment area.
  • Tensioning via galvanized steel cabling to prevent "belly" formation and water pooling.
  • Strategic placement of catchment "funnels" to concentrate flow into drainage conduits.
  • Application of industrial-grade grommets for secure anchoring to the building's structural steel.

Hydraulic Routing and Asset Protection Strategies

Capturing the water is only half of the engineering challenge; the critical second phase is the routing of that water away from high-value assets. In an intermodal terminal, the production bay often houses automated guided vehicles (AGVs), conveyor systems, and expensive computing hardware. A failure in the diversion routing can lead to electrical shorts or structural corrosion. We employ a closed-loop drainage system where the vinyl catchment tarp feeds directly into a reinforced PVC or flexible HDPE hose system. This ensures that the water is contained from the moment of capture to the point of discharge.

The routing must be designed to avoid "trapped air" pockets and ensure a continuous downward gradient. We utilize magnetic mounting brackets and heavy-duty zip-ties to secure the drainage lines to the building's structural columns, ensuring that the hoses do not interfere with overhead crane movements or personnel walkways. The final discharge point is typically routed to an exterior scupper or a designated interior floor drain, ensuring that the water is moved entirely out of the production environment without crossing any active operational zones.

  • Integration of large-diameter flexible hoses to prevent hydraulic backup.
  • Use of magnetic standoff brackets to secure routing without drilling into structural steel.
  • Calculation of flow rates to ensure hose capacity exceeds maximum rainfall intensity.
  • Strategic discharge into existing facility storm-water management systems.
  • Clear marking of diversion lines with high-visibility caution tape to prevent accidental damage.

Transition to Permanent Envelope Remediation

While active diversion systems provide the necessary stability to maintain operations, they are temporary measures. The transition to permanent repair requires a rigorous adherence to ASTM and ANSI standards for commercial roofing. Once the interior is stabilized and the assets are protected, we move to the "dry-in" phase. This involves a forensic stripping of the compromised membrane to identify the full extent of the moisture infiltration. We often find that the underlying insulation—such as polyisocyanurate—has become saturated, which can lead to "wet-insulation syndrome" and potential mold growth if not properly addressed.

The permanent repair involves the installation of a reinforced flashing system and a new membrane section, heat-welded to the existing roof using a robotic hot-air welder to ensure a molecular bond. We specify a high-mil TPO or PVC membrane with an increased puncture rating to withstand the specific rigors of the intermodal environment. Following the repair, a comprehensive electronic leak detection (ELD) test is performed. This process involves applying a controlled electrical current to the roof surface to identify any remaining microscopic voids in the membrane, ensuring the building envelope is fully restored to its engineered specifications.

  • Removal of saturated insulation to prevent long-term structural rot.
  • Installation of ASTM-compliant reinforced flashing at all critical penetrations.
  • Heat-welding of new membrane sections to ensure a monolithic, seamless surface.
  • Execution of Electronic Leak Detection (ELD) to verify the integrity of the repair.
  • Final audit of the building envelope to ensure thermal bridging has been eliminated.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565

Previous (Vol. 6) Volume 7 of 23 (40 Dossiers / Page) Next (Vol. 8)