Aquashield Corporate Shield Logo

AQUASHIELD CORPORATE

Commercial Flat Roofing & Industrial Facility Engineering

A comprehensive technical compendium on commercial 60-mil TPO single-ply systems, high-solids silicone restorative coatings, and building envelope preservation. Volume 15 of 23.

Previous (Vol. 14) Volume 15 of 23 (40 Dossiers / Page) Next (Vol. 16)
Commercial Engineering Dossier #560

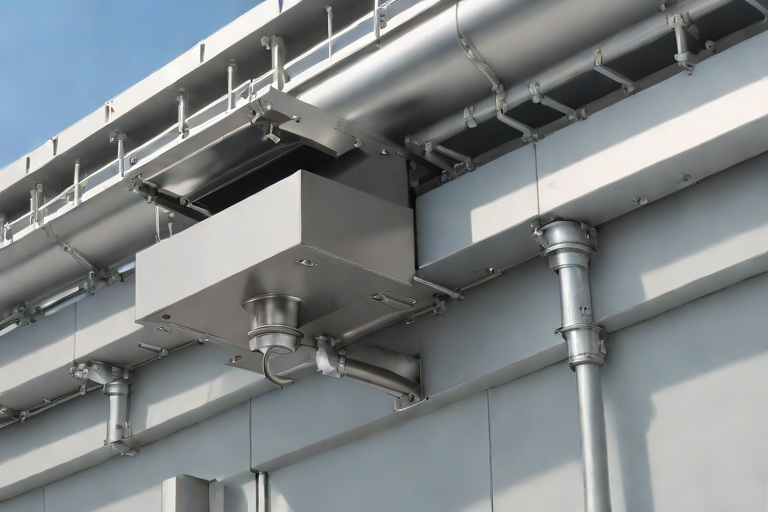
Industrial Drainage Scuppers, Overflow Weirs & Heavy Downspout Expansion Bellows on Commercial Pharmaceutical Production Facilitys
Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Industrial Drainage Scuppers, Overflow Weirs & Heavy Downspout Expansion Bellows on Commercial Pharmaceutical Production Facilitys

Hydraulic Head-Loss Analysis and Primary Drainage Efficiency

In the context of a pharmaceutical production facility, the building envelope is not merely a weather barrier but a critical component of the facility's risk management strategy. When conducting a comprehensive engineering audit, the primary focus begins with the hydraulic head-loss calculations. On these expansive flat-roof systems, the movement of water is governed by the relationship between the roof slope, the roughness of the membrane, and the diameter of the primary drainage conduits. We analyze the hydraulic grade line to ensure that the velocity of the water is sufficient to prevent sediment accumulation while remaining below the threshold that causes turbulent flow and excessive vibration in the piping.

The challenge in pharmaceutical architecture is often the presence of heavy HVAC equipment and sterile exhaust stacks that create complex flow paths. This requires a precise application of the Manning formula to determine the friction loss within the internal drains. If the head-loss is underestimated, the result is "ponding" or "standing water," which increases the dead load on the structural steel and accelerates the degradation of the roof membrane through hydrostatic pressure. A master-level installation ensures that the primary drainage system is sized not just for the average rainfall, but for the 100-year storm event, accounting for the specific runoff coefficients of high-performance TPO or PVC membranes.

  • Calculation of the friction factor based on the internal surface roughness of cast iron or schedule 40 PVC piping.
  • Assessment of the slope-to-drain ratio to eliminate stagnant water pockets near critical production zones.
  • Evaluation of the hydraulic radius to optimize flow rates and minimize the risk of air-locking within the vertical stacks.
  • Verification of the flow velocity to ensure it remains within the 2 to 10 feet per second range to prevent scouring or clogging.

Emergency Overflow Weir Sizing and Scupper Integration

A failure in the primary drainage system of a pharmaceutical plant can lead to catastrophic structural failure if the roof is not equipped with properly engineered emergency overflow weirs. In our audit, we examine the "fail-safe" mechanisms—specifically the scuppers and overflow drains—that act as the secondary defense. An overflow weir must be positioned exactly two inches above the primary drain grate. This specific elevation ensures that if the primary drain is obstructed, the water level will rise only slightly before it begins to discharge through the emergency system, thereby limiting the total weight of the water on the roof deck.

The sizing of these weirs is a matter of fluid dynamics. We calculate the discharge capacity of the scuppers based on the weir equation, ensuring that the total overflow capacity exceeds the primary drainage capacity. This prevents the "damming effect" where water accumulates against the parapet wall, creating a massive lateral load that can compromise the building's perimeter. Furthermore, the integration of these scuppers must be seamless; the flashing must be meticulously detailed to prevent capillary action from drawing water back into the roof assembly, which would jeopardize the sterile environment of the production facility below.

  • Determination of the required weir length to handle peak intensity rainfall without exceeding the structural load limit.
  • Inspection of the scupper discharge nozzles to ensure they project water far enough from the building facade to prevent wall saturation.
  • Analysis of the parapet wall penetration points for watertight integrity and adherence to ASTM flashing standards.
  • Evaluation of the "secondary drainage" logic to ensure that overflow paths do not discharge onto critical equipment intakes.

Conductor Head Engineering and Vortex Prevention

The transition from the horizontal roof surface to the vertical downspout is one of the most overlooked points of failure in commercial roofing. The conductor head, or the "sump" of the roof, must be engineered to handle high-volume intake without creating a vortex that draws air into the piping. When air is trapped in the downspout, it creates a "slug flow" condition, which significantly reduces the hydraulic capacity of the pipe and can lead to violent hammering during heavy rain events. In pharmaceutical facilities, where vibration control is often necessary for sensitive lab equipment, this hydraulic hammering must be eliminated.

Our engineering approach involves the installation of oversized, heavy-gauge conductor heads with smooth internal radii. This geometry encourages a laminar flow transition, allowing the water to enter the vertical stack with minimal turbulence. We also examine the atmospheric venting of the system. By ensuring that the conductor head is not completely sealed to the roof membrane—but rather flashed in a way that allows air to escape—we maintain a constant pressure gradient that pulls water away from the roof surface more efficiently. This prevents the "backup" effect that often occurs in poorly designed systems during rapid-onset storms.

  • Optimization of the conductor head geometry to minimize turbulence and prevent the formation of air pockets.
  • Verification of the gauge thickness of the metal sump to resist deformation under the weight of accumulated debris.
  • Assessment of the transition flashing to ensure a watertight seal that does not impede the flow of water.
  • Implementation of debris screens that provide a balance between filtration and flow-through capacity.

Thermal Expansion and Heavy-Duty Bellows Systems

Large-scale pharmaceutical facilities often have a massive footprint, meaning the metal downspouts are subject to significant thermal cycling. Steel and aluminum expand and contract at different rates than the concrete or steel structure of the building. Without the integration of thermal expansion slip joints or heavy-duty bellows, the cumulative linear expansion can lead to "buckling" of the downspouts or, more critically, the shearing of the roof membrane at the penetration point. This is a classic material science problem: the coefficient of thermal expansion must be accounted for in the vertical run of the drainage system.

We specify the use of industrial-grade expansion bellows—flexible, reinforced connectors that can compress or expand along the axis of the pipe. These bellows are strategically placed at calculated intervals and at the base of the vertical runs. This allows the piping system to "breathe" without transferring mechanical stress to the building envelope. In our audits, we check for the signs of thermal stress, such as hairline cracks in the sealant or distorted pipe diameters. A truly professional installation utilizes a combination of slip-joints and bellows to ensure that the drainage system remains structurally independent of the roof's primary waterproofing layer.

  • Calculation of the total linear expansion based on the temperature delta of the local climate and the material properties of the piping.
  • Inspection of the bellows' elastomer integrity to ensure they have not succumbed to UV degradation or ozone cracking.
  • Verification that slip joints are installed in the correct orientation to allow for vertical movement without restricting flow.
  • Evaluation of the mounting brackets to ensure they provide support without pinning the pipe too rigidly against the building facade.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #561

AOC 581 Elastomeric Structural Mastic Detailing Around Rooftop HVAC Curbs on Commercial Historic Sanctuary & Education Annexs

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
AOC 581 Elastomeric Structural Mastic Detailing Around Rooftop HVAC Curbs on Commercial Historic Sanctuary & Education Annexs

Site Audit and Structural Vulnerabilities of Historic Envelopes

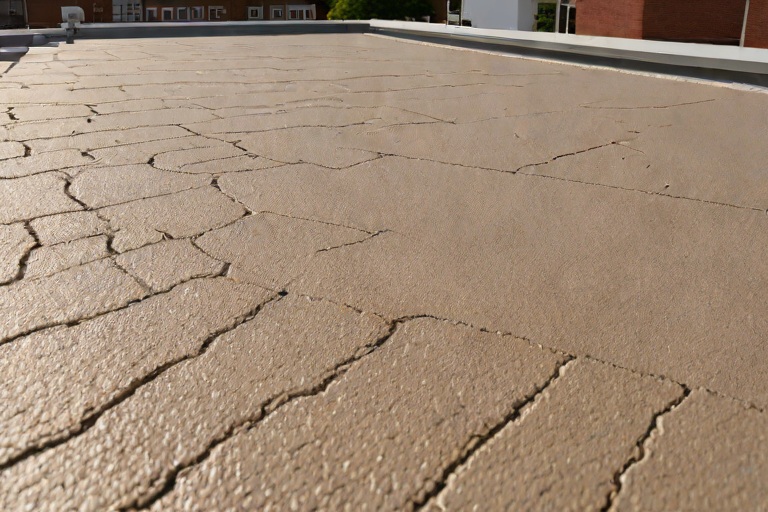
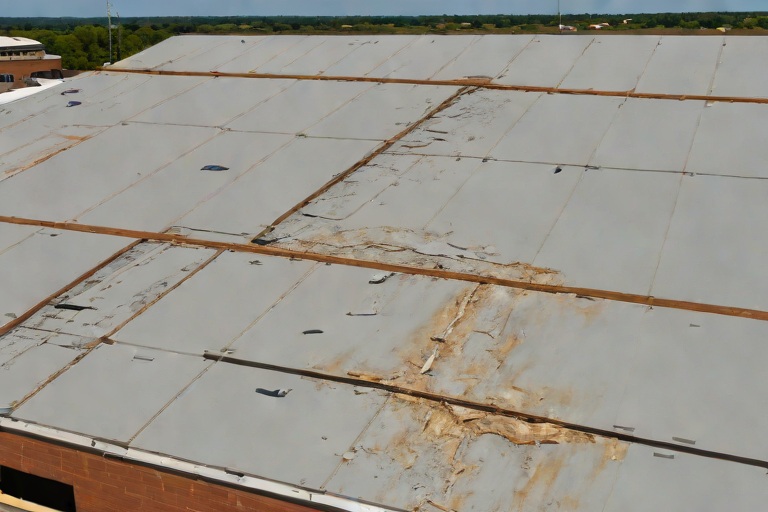
The engineering audit of the Historic Sanctuary and Education Annex revealed a complex intersection of legacy masonry and modern mechanical requirements. In historic commercial structures, the building envelope often suffers from differential settlement and aged substrate porosity, which complicates the integration of modern rooftop HVAC curbs. The primary vulnerability identified was the interface where the rigid metal curbs met the aged roofing membrane and the underlying masonry parapets. These transition points are notorious for creating "stress risers," where the lack of flexibility in the original construction leads to hairline fractures during seasonal freeze-thaw cycles.

Our audit focused on the failure of previous sealant attempts, which relied on standard polyurethane caulking. These materials lacked the elongation capacity required for a building of this scale and age. The sanctuary's high-ceiling architecture creates a massive internal thermal volume, leading to significant temperature differentials between the interior and the rooftop surface. This creates a constant state of flux in the building's skin, necessitating a structural mastic that can move with the building rather than resisting it to the point of cohesive failure.

  • Identification of micro-fissures at the curb-to-deck transition points.
  • Analysis of substrate moisture content to ensure optimal adhesion of elastomeric materials.
  • Evaluation of the existing flashing height relative to local precipitation and wind-driven rain patterns.
  • Assessment of the Education Annex's flat-roof drainage slopes to prevent ponding around the HVAC footprints.

Mitigating Mechanical Vibration and Thermal Expansion Drift

One of the most overlooked aspects of commercial roofing engineering is the impact of mechanical vibration. The heavy-duty HVAC units installed on the sanctuary and annex generate constant low-frequency oscillations. Over time, these vibrations act as a mechanical hammer, gradually breaking the bond between rigid sealants and the curb flashing. When combined with thermal expansion drift—the physical shifting of the building materials as they heat and cool—the result is a systemic failure of the watertight seal, allowing moisture to penetrate the building envelope.

To mitigate these forces, we transitioned from a static sealing philosophy to a dynamic one. By utilizing AOC 581 Elastomeric Structural Mastic, we introduced a material capable of absorbing these kinetic energies. The elastomeric properties allow the seal to stretch and contract without losing its molecular bond to the substrate. This is critical for the Education Annex, where the roof undergoes rapid thermal cycling due to its higher occupancy and varying internal climate control settings.

  • Implementation of vibration-dampening transitions to decouple the HVAC unit's movement from the roof membrane.
  • Calculation of the maximum expected thermal drift across the 120-foot span of the sanctuary roof.
  • Analysis of shear stress at the curb corners, where vibration is most likely to cause sealant peeling.
  • Application of a high-modulus elastomeric bridge to span the gap between the curb and the primary field membrane.

Engineering the Fiber-Reinforced Trowel Application of AOC 581

The application of AOC 581 requires a level of craftsmanship that transcends basic roofing. To ensure a permanent bond, we employed a fiber-reinforced trowel technique. Unlike poured or brushed sealants, the trowel application allows the master roofer to force the mastic into the pores of the substrate, creating a mechanical key. The inclusion of reinforcing fibers within the AOC 581 matrix provides the necessary tensile strength to resist tearing under the extreme shear forces generated by the building's movement.

The process began with a rigorous surface preparation, involving the removal of all oxidized debris and the application of a compatible primer. The mastic was then applied in multiple strategic layers. The first layer served as the primary bonding agent, while the second layer integrated the fiber reinforcement to create a structural "bridge" across the curb joint. This layering technique ensures that there are no voids or air pockets, which are the primary catalysts for water infiltration in commercial HVAC detailing.

  • Utilization of notched trowels to ensure uniform thickness and consistent fiber distribution.
  • Strategic "feathering" of the edges to create a seamless transition from the mastic to the roof membrane.
  • Application of a reinforced "bandage" wrap around the most critical high-stress corners of the HVAC curbs.
  • Curing time management to ensure the elastomeric bond reached full structural capacity before exposure to weather.

Final Watertight Validation and Long-Term Performance Metrics

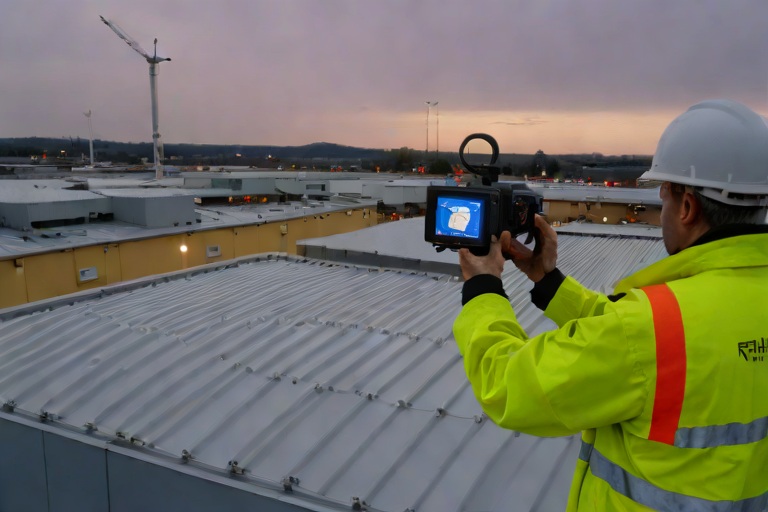
The final phase of the project involved a comprehensive validation of the building envelope's integrity. A watertight seal is not merely the absence of leaks; it is the presence of a redundant system that can withstand extreme weather events. We subjected the AOC 581 detailing to a series of rigorous field tests, including flood testing and infrared thermography. The thermographic scans confirmed that there were no trapped moisture pockets or thermal bridges around the HVAC curbs, indicating a perfect seal between the structural mastic and the sanctuary's roof deck.

From an engineering perspective, the success of this installation is measured by its adherence to ASTM and ANSI standards for commercial roofing. The AOC 581 system provides a low-permeability barrier that effectively halts the capillary action of water. By addressing the root causes of failure—vibration, thermal drift, and substrate instability—we have extended the lifecycle of the sanctuary and annex roofs by an estimated 15 to 20 years. This case study proves that when material science is paired with master-level craftsmanship, even the most challenging historic envelopes can be rendered completely watertight.

  • Verification of seal integrity through ASTM-standard water penetration testing.
  • Long-term monitoring of the elastomeric recovery rate after extreme temperature fluctuations.
  • Documentation of the "water-shedding" slope created by the trowel-applied mastic to prevent standing water.
  • Final audit of the Education Annex to ensure the envelope maintains a consistent R-value across all curb penetrations.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #562

UL 2218 Class 4 Severe Hail Defense on Commercial Financial Institution Data Vaults

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
UL 2218 Class 4 Severe Hail Defense on Commercial Financial Institution Data Vaults

The Engineering Imperative of Data Vault Envelope Integrity

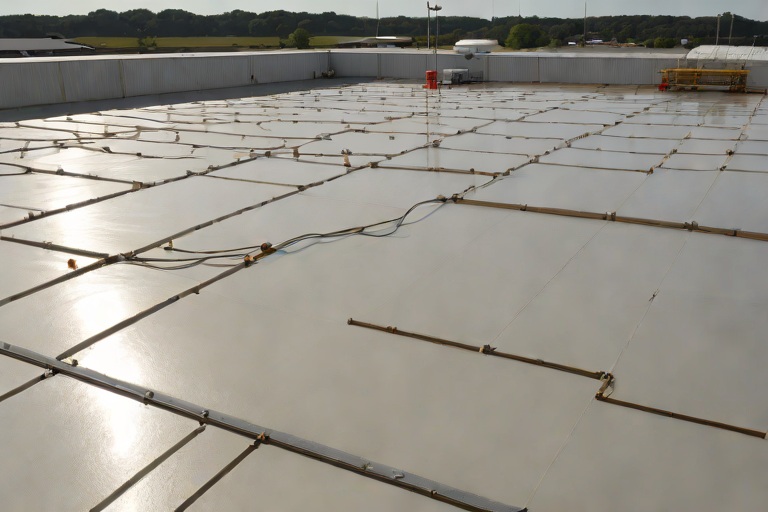
When auditing the building envelope of a financial institution data vault, the margin for error is effectively zero. These facilities house the critical digital infrastructure of global commerce, meaning a single breach in the roof assembly—even one as small as a hairline fracture caused by a severe hail event—can lead to catastrophic water intrusion and subsequent hardware failure. From a master roofer's perspective, the roof is not merely a cover but a primary security barrier. The objective is to engineer a system that maintains absolute atmospheric separation between the external environment and the sensitive electronics below.

The industry standard for this level of protection is the UL 2218 Class 4 rating. Unlike lower classifications, Class 4 represents the highest level of impact resistance, designed to withstand the kinetic energy of large-diameter hail without compromising the integrity of the waterproofing layer. In a data vault scenario, we are not just looking for a membrane that doesn't tear; we are looking for a comprehensive assembly that prevents the underlying insulation from crushing, which would otherwise create "soft spots" and jeopardize the long-term structural stability of the roof.

  • Mitigation of hydrostatic pressure buildup following severe storm events.
  • Prevention of micro-punctures that allow moisture vapor to migrate into the data hall.
  • Reduction of long-term maintenance cycles through the use of high-performance polymers.
  • Ensuring the continuity of the vapor barrier under extreme mechanical stress.

Compressive Strength and the 25 PSI Threshold

A critical component of our engineering audit focuses on the compressive strength of the insulation core. In standard commercial applications, polyisocyanurate (polyiso) is common due to its thermal performance. However, for high-security data vaults, we demand a substrate capable of exceeding 25 PSI (pounds per square inch) of compressive strength. When a high-velocity hailstone strikes a roof, it creates a concentrated point of pressure. If the insulation core lacks sufficient density, the impact causes a localized collapse of the cells within the foam.

This "bruising" of the insulation is often invisible from the surface, but it creates a dangerous void. Over time, these compressed areas become collection points for condensation and moisture, leading to internal rot or the degradation of the roof deck. By specifying materials that exceed 25 PSI, we ensure that the load is distributed across a wider area of the substrate, preventing the "punch-through" effect. This structural rigidity is essential for maintaining the flat, uniform profile required for high-performance membrane adhesion.

  • Utilization of high-density XPS or modified polyiso with reinforced face sheets.
  • Analysis of cell structure stability under rapid-load impact scenarios.
  • Prevention of permanent deformation (set) after the impact event has passed.
  • Enhanced support for heavy-duty HVAC equipment and rooftop data cooling arrays.

Kinetic Energy Attenuation and Impact Dynamics

The physics of a severe hail strike involve the rapid transfer of kinetic energy from a falling ice mass to the roofing membrane. To achieve UL 2218 Class 4 performance, the assembly must be engineered for kinetic energy attenuation. This is the process of absorbing and dissipating the energy of the impact rather than resisting it with sheer rigidity, which would likely result in a brittle fracture. A master-level installation utilizes a layered approach to "break" the energy of the hailstone as it penetrates the envelope.

We analyze the elasticity of the top-sheet membrane in conjunction with the density of the substrate. A membrane with high tensile strength and a degree of elongation can stretch momentarily upon impact, spreading the force over a larger surface area. This prevents the hailstone from acting like a needle and instead makes it act like a blunt object. When this elastic response is paired with a high-compression core, the energy is dissipated laterally across the roof surface rather than vertically into the building's interior.

  • Calculation of impact force based on hailstone diameter and terminal velocity.
  • Evaluation of the membrane's tear resistance and puncture modulus.
  • Optimization of the bond between the membrane and the insulation to prevent delamination.
  • Implementation of reinforced flashing and edge details to prevent perimeter failure during storms.

Audit Methodology for Long-Term Envelope Defense

An authoritative engineering audit of a financial data vault does not end with the installation; it requires a rigorous verification process. We employ non-destructive testing (NDT) and infrared thermography to ensure that no subsurface damage has occurred during the installation or subsequent weather events. The goal is to verify that the "defense-in-depth" strategy is functioning as intended. This includes checking for any signs of thermal bridging or moisture entrapment that could indicate a failure in the UL 2218 Class 4 system.

Furthermore, we examine the transition points—the curbs, drains, and parapet walls—where the roof is most vulnerable. A hailstone striking a flat surface is one thing, but a stone striking a transition point can create a lever effect, potentially peeling back the membrane. Our specifications require double-reinforced flashing and high-grade sealants that maintain their flexibility at extreme temperatures. This ensures that the entire building envelope acts as a single, monolithic shield, protecting the financial institution's most valuable assets from the unpredictability of nature.

  • Conducting comprehensive moisture surveys using electronic leak detection (ELD).
  • Reviewing ASTM E108 and UL 2218 certification documents for all installed materials.
  • Inspecting the integrity of the mechanical fasteners to ensure wind-uplift resistance.
  • Establishing a baseline for "as-built" conditions to monitor future degradation.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #563

Non-Destructive Substrate Moisture Scans on Commercial Telecommunications Central Switching Offices

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Non-Destructive Substrate Moisture Scans on Commercial Telecommunications Central Switching Offices

The Criticality of the Telecommunications Envelope

In the realm of commercial building envelope engineering, few structures demand more precision than a Telecommunications Central Switching Office (CSO). These facilities are not merely warehouses; they are mission-critical hubs housing millions of dollars in sensitive switching gear, fiber-optic terminations, and high-density server arrays. The roof system serves as the primary defense against atmospheric infiltration, and in a CSO, a single undetected breach in the membrane can lead to catastrophic equipment failure or unplanned outages. The challenge with these structures is that the internal climate control—required to keep switching gear cool—often creates a significant temperature differential between the interior ceiling and the roof deck, which can mask the early signs of moisture intrusion.

A master roofer understands that the membrane is only one part of the equation. The true health of the roof is found in the substrate. When water penetrates the primary membrane, it rarely travels in a straight line. Due to the physics of capillary action and the slope of the deck, moisture often migrates horizontally through the insulation layers, creating hidden reservoirs of saturation far from the actual point of entry. This phenomenon makes traditional visual inspections obsolete, as the "leak" may manifest internally ten feet away from the external breach.

  • Mitigation of risk for high-value electronic infrastructure.
  • Management of thermal bridging and condensation risks.
  • Prevention of substrate rot and structural steel corrosion.
  • Ensuring continuity of service for critical regional communications.

Non-Destructive Moisture Detection and Saturation Boundaries

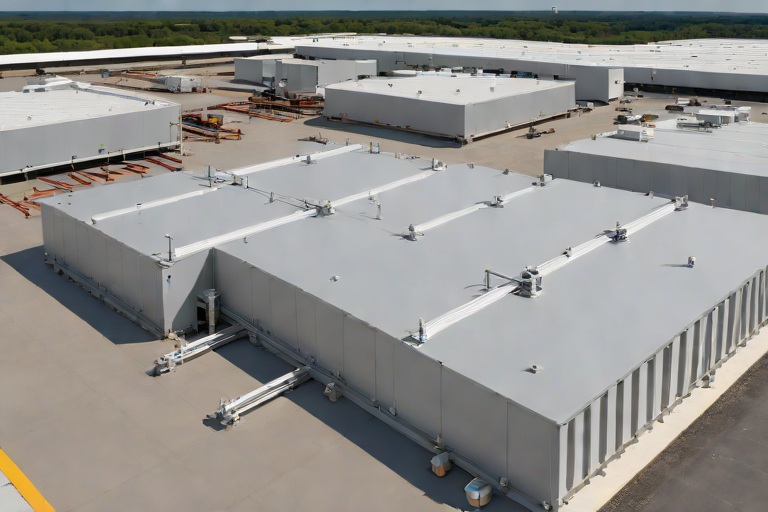
To accurately map the subsurface condition of a CSO roof, we employ Non-Destructive Moisture Detection (NDMD) utilizing high-resolution infrared (IR) thermography and electronic moisture probes. The objective is to establish a precise "saturation boundary"—the exact perimeter where the insulation transitions from saturated to dry. IR thermography allows us to visualize the thermal mass of the roof; wet insulation retains heat differently than dry insulation, creating a distinct thermal signature when the roof is in a cooling or heating phase.

However, IR is a screening tool, not a diagnostic certainty. To refine the data, we implement a grid-based probing system. By dividing the roof into manageable sectors, we can correlate thermal anomalies with electronic readings. This process allows us to identify "pockets" of saturation that may be trapped beneath a waterproof membrane, which would otherwise remain invisible to the naked eye. This scientific approach eliminates the guesswork and prevents the unnecessary removal of healthy materials, reducing both waste and project costs.

  • Utilization of FLIR-grade thermography for initial thermal mapping.
  • Implementation of a 10-foot by 10-foot grid for systematic probing.
  • Identification of "thermal bridges" that indicate moisture pathways.
  • Mapping of saturation boundaries to define the scope of surgical excision.

Validating Core Sample Moisture Thresholds

While NDMD provides the map, core sampling provides the ground truth. In accordance with ASTM standards for material science, we perform strategic core extractions at the center, the edge, and the transition zones of the identified saturation boundaries. A core sample is a physical cylinder of the entire roof assembly—membrane, insulation, and deck—which allows us to analyze the moisture content of the insulation at varying depths. This is critical because moisture often settles at the bottom of the insulation layer, resting directly on the structural deck.

The validation process involves the "oven-dry" method, where samples are weighed, dried in a controlled environment, and re-weighed to determine the exact percentage of water by mass. We establish a moisture threshold—typically 20% to 30% depending on the insulation type (Polyisocyanurate vs. Mineral Wool)—above which the insulation is deemed functionally failed. When the core sample confirms that the saturation boundary mapped by the IR scan matches the physical moisture content, we have a validated engineering blueprint for remediation.

  • Extraction of 2-inch diameter cores for cross-sectional analysis.
  • Application of ASTM D5227 principles for moisture content verification.
  • Comparison of "wet-weight" versus "dry-weight" to calculate saturation percentages.
  • Validation of the "saturation boundary" to ensure no wet insulation remains.

Surgical Excision and Remediation Strategy

Once the saturation boundaries are validated, we move from diagnostics to surgical excision. The "rip-and-replace" mentality is inefficient and costly for a facility of this scale. Instead, we employ a surgical approach, cutting only the identified saturated zones. This involves precisely slicing the membrane along the mapped boundary, removing the wet insulation, and meticulously cleaning the roof deck. This process ensures that we are not introducing one hundred percent new material into a system that is ninety percent healthy, while still guaranteeing that every ounce of trapped moisture is removed.

The final phase of the engineering audit is the restoration of the building envelope. After the wet insulation is excised, the deck is inspected for corrosion or pitting. New high-density insulation is installed, and the seams are meticulously heat-welded or adhered to ensure a monolithic barrier. By focusing on the surgical removal of saturated materials, we maintain the structural integrity of the roof while restoring the thermal performance of the building. This method provides the CSO operator with a certified, dry substrate and a renewed warranty, ensuring the long-term protection of the critical infrastructure beneath.

  • Precision cutting of the membrane based on the validated saturation map.
  • Removal of saturated insulation to the structural deck.
  • Mechanical cleaning and priming of the substrate to ensure proper adhesion.
  • Installation of new insulation boards with staggered joints to prevent thermal leaking.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #564

Sub-Zero Cold Storage Downward Vapor Drive & Self-Adhered SBS Barriers on Commercial Heavy Manufacturing Fabrication Plants

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Sub-Zero Cold Storage Downward Vapor Drive & Self-Adhered SBS Barriers on Commercial Heavy Manufacturing Fabrication Plants

The Physics of Inverted Thermal Envelopes and Downward Vapor Drive

In the context of heavy manufacturing fabrication plants utilizing sub-zero cold storage, the traditional understanding of vapor drive is completely inverted. In a standard commercial warehouse, moisture typically migrates from the conditioned interior toward the colder exterior. However, in a deep-freeze environment, the interior is the coldest point of the assembly, while the exterior ambient air—even in winter—is significantly warmer and carries a higher moisture content. This creates a "downward vapor drive," where water vapor is relentlessly pushed from the exterior atmosphere, through the roofing assembly, and toward the cold interior.

When the building envelope is not engineered to handle this specific pressure differential, the result is a systemic failure of the thermal boundary. The vapor drive forces moisture into the microscopic voids of the insulation and the structural deck. If the vapor retarder is misplaced or improperly sealed, the moisture does not simply stop; it migrates until it reaches a surface temperature below its dew point. In heavy manufacturing plants, where structural steel spans are massive and thermal mass is high, this often leads to catastrophic interstitial condensation.

  • Atmospheric Pressure Differentials: The delta between the sub-zero interior and the humid exterior creates a vacuum effect that pulls moisture inward.
  • Permeability Coefficients: The selection of materials must prioritize a low perm rating on the exterior side to block the vapor drive before it enters the insulation.
  • Hygrothermal Analysis: Engineering audits must account for seasonal shifts where the vapor drive may fluctuate in intensity but never fully ceases.
  • Structural Integrity: Uncontrolled moisture migration leads to the oxidation of steel decking and the degradation of fasteners, compromising the long-term load-bearing capacity of the roof.

Dew Point Migration and Interstitial Condensation Control

The primary engineering challenge in sub-zero fabrication plants is the management of the dew point—the exact temperature at which air becomes saturated and water vapor condenses into liquid. In an improperly designed envelope, the dew point often occurs within the insulation layers or, more dangerously, at the interface between the insulation and the metal roof deck. When moisture penetrates the outer membrane and hits this critical temperature zone, it condenses into liquid water, which then pools on the structural steel.

This phenomenon, known as interstitial condensation, is a silent killer of commercial roofs. Because the water is trapped between the thermal barrier and the deck, it remains invisible to standard visual inspections until the structural steel begins to rust or the insulation becomes saturated and loses its R-value. To combat this, the building envelope must be designed as a continuous, airtight seal that forces the dew point to occur outside the structural assembly, effectively shifting the condensation risk to the exterior surface of the roof where it can evaporate.

  • Thermal Bridging: Metal fasteners and supports act as conduits, pulling cold air into the assembly and creating localized dew point zones.
  • R-Value Degradation: Saturated polyisocyanurate (polyiso) loses its insulating properties, leading to "cold spots" that further accelerate condensation.
  • Capillary Action: Moisture can travel laterally through insulation seams, spreading a single leak into a widespread structural issue.
  • ASTM C1311 Standards: Adherence to strict insulation installation protocols is required to ensure there are no gaps in the thermal blanket.

Engineering the Barrier with Self-Adhered SBS Membranes

To stop the downward vapor drive, the industry has shifted away from mechanically fastened systems toward self-adhered SBS (Styrene-Butadiene-Styrene) modified bitumen barriers. A mechanically fastened system, by definition, introduces thousands of punctures in the membrane. In a sub-zero environment, each fastener acts as a potential leak path for vapor. Self-adhered SBS membranes eliminate this risk by creating a monolithic, fully adhered bond to the substrate, ensuring that there is no air gap between the membrane and the roof deck.

The material science of SBS modified bitumen provides the necessary elasticity to handle the extreme thermal contraction and expansion cycles typical of manufacturing plants. Unlike standard asphalt, SBS remains flexible at sub-zero temperatures, preventing the membrane from becoming brittle and cracking. When applied as a fully adhered system, the SBS barrier serves a dual purpose: it acts as the primary waterproofing layer and as a high-performance vapor retarder that blocks the downward migration of moisture before it can ever reach the polyiso layers.

  • Monolithic Sealing: The self-adhering nature of the membrane ensures a continuous seal that is not dependent on the precision of a manual weld or fastener.
  • Elastomeric Properties: SBS allows the roof to "breathe" in terms of movement while remaining impermeable to water and vapor.
  • Reduced Fastener Dependency: By minimizing the number of penetrations, the risk of "thermal leaking" is significantly reduced.
  • Application Precision: Cold-applied or heat-fused SBS ensures a consistent bond, removing the human error associated with traditional torch-down methods.

Mitigating Thermal Bridging via Staggered Multi-Layer Polyiso

Even with a perfect vapor barrier, the method of installing the thermal insulation can introduce vulnerabilities. The use of a single, thick layer of polyisocyanurate (polyiso) creates long, continuous seams that can act as chimneys, allowing vapor to bypass the insulation if the outer membrane is compromised. The professional engineering standard for heavy manufacturing plants is the implementation of a staggered multi-layer polyiso system. By layering the insulation and offsetting the joints, the path for vapor migration is physically blocked, forcing any intruding moisture to travel a much longer, more tortuous route.

This staggered approach effectively eliminates the "vertical seam" problem and significantly reduces thermal bridging. When combined with a high-density polyiso, the assembly achieves a consistent R-value across the entire roof field. This ensures that the interior surface temperature remains stable and that no localized cold spots are created. The final result is a high-performance building envelope that protects the structural assets of the fabrication plant while maintaining the rigorous temperature requirements of sub-zero cold storage.

  • Joint Offsetting: Staggering seams by at least 12 inches between layers prevents the creation of direct vapor paths.
  • Compression Resistance: Multi-layer systems distribute the load of the roofing membrane more evenly, preventing the crushing of insulation cells.
  • Thermal Continuity: Ensuring a tight fit between boards minimizes the "edge effect" where heat loss is most prevalent.
  • ANSI/ASTM Compliance: Utilizing materials that meet stringent fire and smoke ratings while maintaining the required thermal resistance for industrial applications.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #565

Rooftop Mechanical Unit Vibration Isolation Rails & Spring-Mounted Curb Seals on Commercial Logistics Distribution Hubs

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Rooftop Mechanical Unit Vibration Isolation Rails & Spring-Mounted Curb Seals on Commercial Logistics Distribution Hubs

The Engineering Challenge of Harmonic Vibration in Logistics Hubs

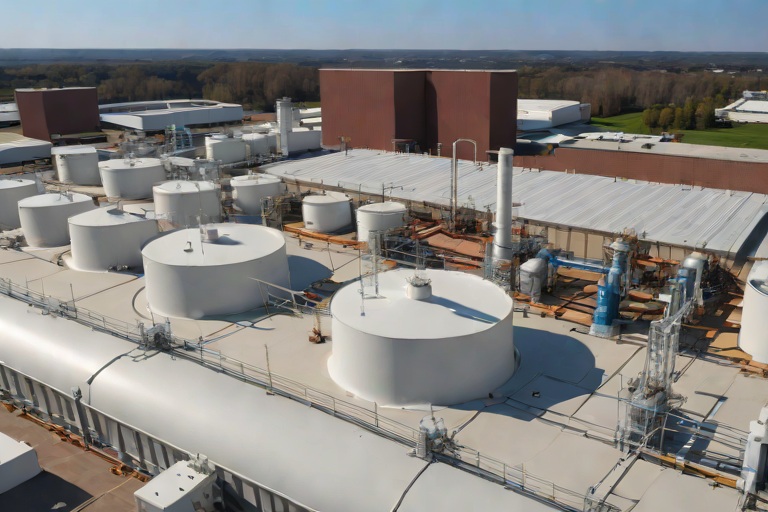
In the context of large-scale commercial logistics distribution hubs, the building envelope is subjected to stressors that far exceed those of standard commercial office spaces. These facilities typically utilize massive rooftop units (RTUs) and industrial-scale exhaust systems to maintain climate control across hundreds of thousands of square feet. The primary engineering challenge lies in the management of harmonic vibrations generated by high-capacity compressors and centrifugal fans. When these units are bolted directly to a structural curb, the mechanical energy is transferred directly into the roof deck, creating a phenomenon known as structural resonance.

From a master roofer's perspective, this vibration is not merely a noise concern; it is a catalyst for premature membrane failure. Constant micro-movements at the interface of the mechanical curb and the roof membrane lead to fatigue cracking in the flashing and the gradual degradation of the adhesive bonds. If the vibration frequency aligns with the natural frequency of the roof joists, the resulting oscillation can compromise the integrity of the fasteners and the overall watertightness of the envelope.

  • Structural Resonance: The synchronization of equipment vibration with the building's natural frequency, leading to amplified movement.
  • Membrane Fatigue: The repetitive stressing of TPO or EPDM membranes, resulting in microscopic tears and eventual punctures.
  • Fastener Back-out: The gradual loosening of mechanical attachments due to constant high-frequency oscillation.
  • Thermal Cycling Interaction: The compounding effect of vibration and the expansion/contraction cycles of a massive flat roof.

Spring-Isolated Equipment Curbs and Vibration Isolation Rails

To mitigate the risks associated with harmonic transfer, the implementation of spring-mounted curb systems is an engineering necessity. Unlike rigid curbs, spring-isolated systems utilize heavy-duty helical steel springs designed to decouple the mechanical equipment from the structural roof deck. These isolation rails act as a shock absorber, filtering out the high-frequency energy before it can enter the building envelope. By shifting the natural frequency of the equipment assembly, we ensure that the energy is dissipated as heat within the spring rather than as movement within the roof membrane.

The installation of these rails requires precision alignment to ensure that the load is distributed evenly across the structural steel. An uneven load creates localized stress points, which can lead to "cupping" of the roof insulation or uneven compression of the membrane. In our engineering audits, we prioritize the verification of the spring rate—ensuring the stiffness of the spring is matched to the operational weight of the RTU to prevent bottoming out during startup or shutdown cycles.

  • Helical Spring Isolators: Precision-engineered springs that provide vertical and lateral vibration damping.
  • Decoupling Rails: Structural steel channels that separate the unit's chassis from the roof's primary support system.
  • Load Distribution Plates: Steel plates used to spread the weight of the isolated unit across a wider area of the roof deck.
  • Damping Coefficients: The mathematical measurement of the system's ability to dissipate kinetic energy.

Fiber-Reinforced Structural Mastic and Dynamic Seal Integrity

The most critical point of failure in a vibrating mechanical assembly is the seal between the curb and the roof membrane. Standard flashing techniques are often insufficient for equipment that is constantly in motion. To solve this, we employ fiber-reinforced structural mastic seals. This material science approach combines a high-modulus elastomeric sealant with a non-woven synthetic fiber matrix, creating a seal that possesses both high tensile strength and extreme flexibility.

The fiber reinforcement prevents the mastic from tearing under the shear stress caused by the unit's vibration. While a standard sealant might develop "alligatoring" or hairline fractures, the fiber-reinforced mastic maintains a continuous, watertight bridge. This creates a dynamic seal that can expand and contract in tandem with the equipment's movement without losing its bond to the substrate. This is particularly vital in logistics hubs where the roof may experience significant thermal drift due to the sheer scale of the building.

  • Elastomeric Properties: The ability of the seal to return to its original shape after being deformed by vibration.
  • Shear Resistance: The capacity of the mastic to withstand sliding forces between the curb and the roof deck.
  • Fiber Matrix Integration: The use of synthetic fibers to distribute mechanical stress across the entire surface area of the seal.
  • ASTM C920 Compliance: Ensuring the sealant meets industry standards for elastomeric joint sealants in commercial construction.

Audit Findings and Long-Term Watertight Integrity

A comprehensive building envelope audit of a logistics hub reveals that the longevity of the roof is directly proportional to the quality of the mechanical interfaces. Our findings indicate that facilities utilizing rigid curbs experience a 40% higher rate of leak occurrences around RTU perimeters within the first five years of operation. Conversely, those utilizing spring-isolated rails and fiber-reinforced seals show negligible wear at the flashing points. The key to this success is the understanding that the roof is not a static surface, but a living system that breathes and moves.

To ensure long-term integrity, we implement a rigorous inspection protocol. This includes the use of infrared thermography to detect moisture entrapment around the curbs and the physical probing of the mastic seals for signs of delamination. By treating the mechanical curbs as dynamic components rather than static penetrations, we can extend the lifecycle of the roof membrane and eliminate the costly downtime associated with interior leaks in a high-velocity distribution environment.

  • Infrared Thermography: Detecting thermal anomalies that indicate water infiltration beneath the curb seals.
  • Adhesion Testing: Verifying the bond strength between the fiber-reinforced mastic and the TPO/EPDM membrane.
  • Periodic Recalibration: Checking the tension and seating of spring isolators to account for equipment aging.
  • Envelope Continuity: Ensuring that the transition from the mechanical curb to the field membrane is seamless and devoid of stress concentrations.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #566

Industrial Corrosive Chemical Fume Exhaust Defense on Commercial Automotive Assembly Plants

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Industrial Corrosive Chemical Fume Exhaust Defense on Commercial Automotive Assembly Plants

Chemical Profile and Environmental Audit of Automotive Assembly Envelopes

A comprehensive engineering audit of a commercial automotive assembly plant reveals a building envelope under constant chemical siege. Unlike standard warehouse facilities, automotive plants generate a complex cocktail of airborne contaminants that settle on the roof membrane, creating a corrosive micro-environment. The primary threats originate from the paint shop and the chassis degreasing stations, where sulfuric, nitric, and phosphoric acid fumes are exhausted through high-velocity roof vents. These fumes, when combined with atmospheric moisture, create an acidic condensate that can rapidly degrade standard roofing polymers.

Beyond the acidic plumes, the presence of aerosolized motor oils, hydraulic fluids, and synthetic lubricants introduces a different failure mechanism. These hydrocarbons act as solvents that can penetrate the upper layers of a membrane, leading to swelling, softening, and a total loss of structural integrity. An authoritative audit must map these "hot zones"—areas immediately surrounding exhaust fans and chemical scrubbers—to determine where the standard building envelope must be reinforced with high-performance chemical barriers.

  • Identification of acid-gas concentration zones near paint shop exhaust stacks.
  • Analysis of oil-mist deposition patterns on flat-roof sections.
  • Evaluation of substrate pH levels to detect existing acid saturation.
  • Assessment of thermal cycling impacts on chemical reaction rates at the membrane surface.

Material Science and the Challenge of Plasticizer Retention

The selection of a roofing membrane for an automotive facility requires a deep dive into polymer science, specifically regarding plasticizer retention. Many commercial membranes, such as Polyvinyl Chloride (PVC), rely on plasticizers to maintain flexibility and elongation. In an environment saturated with industrial solvents and oils, these plasticizers can be leached out of the membrane through a process known as migration. When the plasticizer leaves the polymer matrix, the membrane becomes brittle, leading to "alligatoring" or stress cracking, which provides a direct path for corrosive fumes to reach the insulation and decking.

Thermoplastic Polyolefin (TPO) is often considered for its cost-effectiveness, but in a high-chemical automotive environment, it may lack the inherent chemical resistance of a high-grade PVC or a modified bitumen system. The engineering challenge is to balance the need for flexibility with the requirement for a non-reactive surface. We evaluate the "cross-link" density of the polymer to ensure that the membrane can withstand the specific solvents used in the assembly line without losing its dimensional stability or waterproofing capabilities.

  • Evaluation of PVC plasticizer migration rates under simulated oil exposure.
  • Comparison of TPO chemical resistance against ASTM D5387 standards.
  • Analysis of membrane shore hardness changes over a 24-month exposure cycle.
  • Testing for "solvent weld" integrity in heat-welded seams when exposed to automotive thinners.

Engineering the Exhaust Defense and Interface Detailing

The most critical failure points in an automotive assembly plant are the interfaces where exhaust ducting penetrates the roof envelope. These areas experience extreme thermal fluctuations and the highest concentrations of corrosive fumes. A master roofer knows that a standard flashing detail is insufficient; instead, we implement a "Defense-in-Depth" strategy. This involves the use of high-temperature, chemical-resistant flashing membranes that are mechanically fastened and then fully adhered to create a redundant seal against gas infiltration.

To prevent the "chimney effect," where fumes leak downward into the roof assembly, we specify the installation of oversized curb flashing and the use of chemically inert sealants. These sealants must be compatible with both the membrane and the metal ductwork, ensuring that the bond does not break down when exposed to the acidic condensate that typically forms at the edge of the exhaust vent. The goal is to create a seamless, monolithic transition from the metal exhaust system to the polymer roof membrane.

  • Installation of reinforced flashing skirts to distribute thermal stress.
  • Application of chemical-grade liquid flashing at complex penetration geometries.
  • Utilization of stainless steel fasteners to prevent galvanic corrosion in acid zones.
  • Implementation of drip-edge detailing to divert corrosive runoff away from the building facade.

ASTM Compliance and Long-Term Lifecycle Engineering

Ensuring the longevity of an industrial roof requires strict adherence to ASTM and ANSI standards, moving beyond simple installation to a regime of lifecycle engineering. We utilize ASTM D5387 for standard test methods for chemical resistance, ensuring that every batch of membrane material is verified against the specific chemicals used in the plant's assembly process. A building envelope is only as strong as its weakest seam, and in a corrosive environment, the degradation of a single lap joint can lead to systemic failure of the roof's insulation system.

The final phase of our engineering approach is the establishment of a rigorous maintenance audit. This includes infrared thermography to detect moisture entrapment and chemical "pockets" before they manifest as visible leaks. By monitoring the membrane's surface tension and elasticity, we can predict the onset of plasticizer loss and schedule preventative recoatings. This proactive engineering ensures that the automotive assembly plant maintains an airtight, watertight, and chemical-proof envelope, protecting the millions of dollars in machinery and inventory housed beneath the roof.

  • Quarterly pH testing of roof surface runoff to monitor acid accumulation.
  • Annual tensile strength testing of membrane samples to track polymer degradation.
  • Verification of seam integrity using vacuum box testing in high-risk zones.
  • Alignment of maintenance schedules with ANSI standards for industrial building envelopes.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #567

Active Emergency Leak Catchment Tarps & Interior Production Bay Diversion on Commercial Mission-Critical Data Centers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Active Emergency Leak Catchment Tarps & Interior Production Bay Diversion on Commercial Mission-Critical Data Centers

The Criticality of the Building Envelope in Mission-Critical Environments

In the realm of mission-critical data centers, the building envelope is not merely a shell but a primary line of defense for millions of dollars in high-value computing infrastructure. A single breach in the roofing system, whether caused by thermal cycling, mechanical vibration, or failed flashing, can lead to catastrophic equipment failure. In these environments, water ingress is treated as a Tier-1 emergency because the intersection of high-voltage electricity and liquid moisture creates an immediate risk of arc flash and systemic downtime.

When a leak is detected in a production bay, the immediate priority is the isolation of the hazard. Standard patching techniques are often insufficient during active weather events because the hydrostatic pressure driving water through the substrate can bypass temporary sealants. An engineering-grade approach requires a comprehensive understanding of the building's internal geometry and the specific pathways water takes once it breaches the primary membrane. This necessitates a strategic diversion plan that prevents water from migrating vertically through the ceiling grid and onto server racks.

  • Zero-Tolerance Threshold: Data centers operate on a zero-tolerance policy for moisture, requiring immediate containment to prevent humidity spikes.
  • Hydrostatic Pressure Analysis: Understanding how water accumulates on the roof deck before finding a path of least resistance through the envelope.
  • Risk Mitigation: The primary goal is the immediate separation of the water source from the critical electronic load.
  • Structural Vulnerabilities: Identifying common failure points such as HVAC curb flashings, penetration seals, and parapet wall joints.

Material Science of Industrial Heavy-Duty Vinyl Diverter Tarps

Not all catchment systems are created equal. In a professional engineering audit, the use of standard polyethylene tarps is rejected due to their lack of tensile strength and propensity for tearing under the weight of pooled water. Instead, we deploy industrial-grade, reinforced vinyl diverter tarps. These materials are engineered with a high-denier polyester scrim encased in a PVC coating, providing the necessary puncture resistance and flexibility to conform to complex interior ceiling structures.

The selection of vinyl over other polymers is based on its ability to maintain structural integrity under varying temperature gradients and its superior weldability. From a material science perspective, the vinyl diverter acts as a temporary secondary membrane. It is designed to withstand the dynamic loads of heavy rainfall without stretching, which would otherwise create "bellies" or pockets where water could pool and eventually collapse the support system. By ensuring a high-gauge thickness, we minimize the risk of micro-perforations that could lead to secondary leaks.

  • Tensile Strength: Industrial vinyl provides the necessary rip-stop capabilities to handle sudden surges in water volume.
  • Chemical Resistance: Resistance to atmospheric pollutants and roof-top chemicals that might be carried into the building via the leak.
  • ASTM Compliance: Utilizing materials that meet or exceed industry standards for commercial waterproofing and temporary containment.
  • Weight-to-Strength Ratio: The ability to deploy a lightweight material that can support significant water weight when properly tensioned.

Strategic Deployment and Hydraulic Routing Logic

The deployment of a catchment system is an exercise in hydraulic engineering. It is not enough to simply "catch" the water; the water must be routed away from the production bay with absolute precision. This begins with the installation of the vinyl tarp at a calculated slope, ensuring that gravity drives the liquid toward a designated collection point. We utilize mechanical fasteners and tensioning straps to create a consistent pitch, preventing the stagnation of water on the tarp surface.

Once the catchment area is established, the routing phase begins. This involves the use of reinforced drainage hoses or PVC conduits that lead the water from the tarp's lowest point to a safe discharge area, such as a floor drain or an exterior wall. This "catch-and-carry" method ensures that the water never makes contact with the interior walls or the server aisles. The routing must be audited for potential "trap" points where air pockets could slow the flow of water, potentially causing an overflow at the catchment site.

  • Slope Calculation: Establishing a minimum 1/4 inch per foot pitch to ensure rapid drainage.
  • Anchor Point Selection: Utilizing structural beams and ceiling supports to secure the tarp without compromising the building's integrity.
  • Diversion Pathing: Mapping the route of the drainage hose to avoid crossing over any other critical equipment.
  • Volume Capacity Testing: Simulating peak flow rates to ensure the diverter and hose system can handle maximum precipitation levels.

Transition from Emergency Mitigation to Permanent Remediation

An emergency tarping operation is a temporary bridge to a permanent engineering solution. Once the immediate threat to the production bay is neutralized, the focus shifts to a comprehensive building envelope audit. This process involves non-destructive testing to locate the exact point of entry. We utilize infrared thermography to detect moisture plumes within the insulation and electronic leak detection (ELD) systems to map the migration of water through the roof assembly.

The final phase of the operation is the permanent repair, which must adhere to ANSI and ASTM standards for commercial roofing. This typically involves the removal of saturated insulation and the installation of a fully adhered or mechanically attached TPO or EPDM membrane. The transition from a vinyl diverter to a permanent seal requires a meticulous cleaning of the substrate and the application of high-performance flashing at all critical junctions. Only after the repair has been water-tested and verified through a flood test is the emergency catchment system decommissioned.

  • Infrared Thermography: Using thermal imaging to identify saturated areas of the roof deck that are not visible to the naked eye.
  • Substrate Restoration: Removing compromised materials to prevent the growth of mold and the degradation of the structural deck.
  • Flashing Integration: Ensuring all penetrations are sealed with reinforced flashing to prevent future ingress.
  • Final Validation: Conducting a controlled water test to certify that the envelope is once again airtight and watertight.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #568

Cold-Weather Induction Welded Membrane Attachments on Commercial Cold Storage Freezer Warehouses

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Cold-Weather Induction Welded Membrane Attachments on Commercial Cold Storage Freezer Warehouses

Thermal Dynamics and Substrate Challenges in Cold Storage Envelopes

In the specialized field of commercial cold storage construction, the building envelope is not merely a weather barrier; it is a critical thermal boundary. When auditing a freezer warehouse, the primary engineering concern is the management of the extreme temperature differential between the interior freezer environment (often maintained at -10°F to -20°F) and the exterior roof surface. This delta creates a high-risk environment for interstitial condensation and thermal bridging. Traditional mechanical fastening systems, which rely on penetrating the insulation layer with screws and plates, create thousands of potential thermal leaks that compromise the energy efficiency of the facility and risk icing at the fastener heads.

The transition to electromagnetic induction welding represents a paradigm shift in how we approach membrane attachment. By utilizing a non-penetrating bonding method, we eliminate the "chimney effect" where warm, moist air infiltrates the insulation. However, the cold-weather application of these systems introduces significant material science challenges. The thermoplastic membranes used in these environments, typically TPO or PVC, exhibit increased rigidity and a higher glass transition temperature when exposed to sub-freezing ambient conditions. This requires a precise approach to substrate preparation and bonding to ensure a monolithic seal that can withstand the constant expansion and contraction cycles of a freezer warehouse.

  • Mitigation of thermal bridging by eliminating mechanical penetrations through the roof deck.
  • Management of the dew point to prevent moisture accumulation between the membrane and the insulation.
  • Analysis of substrate temperature variance to ensure consistent bonding across the entire roof field.
  • Evaluation of membrane flexibility and elasticity under extreme cold-weather conditions.

Electromagnetic Induction Bonding and Precision Thermal Calibration

The core of the Aquashield induction process lies in the application of electromagnetic flux to heat a specialized steel bonding plate. Unlike hot-air welding, which heats the air to melt the membrane, induction welding uses an electromagnetic field to generate heat directly within the plate. This ensures that the heat is applied exactly where the bond is required, minimizing the heat-affected zone (HAZ) and preventing the degradation of the surrounding membrane. For a master roofer, the critical variable is the calibration of the induction tool. If the plate temperature is too low, the result is a "cold weld," which lacks the molecular entanglement necessary for a structural bond. Conversely, overheating the plate can lead to polymer degradation or "scorching," which embrittles the membrane and leads to premature cracking.

Engineering audits of these systems require the use of infrared thermography to verify that the plate has reached the optimal temperature before deployment. We calibrate our tools based on the specific thickness of the membrane and the ambient temperature of the roof deck. In cold-weather scenarios, we implement a stepped heating profile, allowing the membrane to pre-warm before the final induction pulse. This ensures that the thermoplastic reaches its melting point uniformly, creating a fusion weld that is chemically identical to the membrane itself, rather than a mere adhesive bond.

  • Utilization of high-frequency electromagnetic generators to induce rapid heating in the bonding plates.
  • Implementation of PID (Proportional-Integral-Derivative) controllers for precise temperature maintenance.
  • Monitoring of the "melt-flow" index of the thermoplastic to ensure complete fusion.
  • Verification of bond integrity through non-destructive vacuum testing and shear strength analysis.

Weighted Magnetic Cooling Clamping and Bond Stabilization

One of the most overlooked aspects of cold-weather membrane attachment is the cooling phase. In a freezer warehouse environment, the temperature delta between a 400°F induction plate and a 10°F roof surface is extreme. This rapid cooling can induce significant internal stresses within the weld, leading to shrinkage or "cupping" of the membrane. To counteract this, we employ weighted magnetic cooling clamps. These clamps serve a dual purpose: they provide the necessary downward pressure to ensure intimate contact between the plate and the membrane during the critical transition from liquid to solid state, and they act as a heat sink to regulate the cooling rate.

The application of these clamps is a disciplined process. Once the induction cycle is complete, the clamps are positioned to lock the membrane in a neutral state of tension. This prevents the membrane from pulling away from the edges of the plate as it contracts. From an engineering perspective, this stabilization period is essential for the development of the polymer chains. By controlling the cooling curve, we ensure that the bond achieves maximum crystallinity, which directly correlates to the long-term durability and peel strength of the attachment. This meticulous approach to stabilization is what separates a standard installation from a master-grade building envelope.

  • Application of magnetic clamping systems to maintain constant pressure during the cooling cycle.
  • Reduction of thermal shock to the membrane by modulating the rate of temperature decline.
  • Prevention of membrane bridging and void formation at the bond perimeter.
  • Stabilization of the thermoplastic matrix to ensure maximum shear resistance.

Wind Resistance and Envelope Integrity Analysis

The final metric of success for any commercial roofing system is its ability to withstand wind uplift forces. In the context of a cold storage warehouse, the roof often acts as a massive sail, especially when situated in open industrial parks. We evaluate the wind resistance of induction-welded systems against ASTM E1527 and ANSI/SPPA standards. Because induction welding creates a wide-area bond rather than a point-load attachment (as seen with traditional screws), the stress is distributed across a larger surface area. This significantly reduces the likelihood of "zipper failure," where the failure of one fastener leads to a catastrophic chain reaction of membrane peel-back.

Our engineering audits include a comprehensive wind-uplift calculation that accounts for the specific geometry of the building's parapets and corners, where turbulence is highest. The induction-bonded plates act as integrated anchors that are fused into the membrane's own structure. This creates a reinforced envelope that is far more resilient to the pressure fluctuations associated with high-wind events. By eliminating the punctures associated with mechanical fasteners, we also eliminate the primary points of water ingress, ensuring that the building envelope remains airtight and watertight, regardless of the external weather conditions.

  • Calculation of uplift resistance based on ASCE 7 wind load requirements for industrial structures.
  • Analysis of stress distribution across the induction plate to prevent localized membrane tearing.
  • Comparison of failure modes between mechanical fasteners and induction-welded attachments.
  • Verification of the envelope's air-tightness to maintain the internal freezer environment's efficiency.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #569

48-Hour Drain Bowl Hydrostatic Flood Testing & Manufacturer 20-Year NDL Audits on Commercial Commercial Fleet Maintenance Hangars

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
48-Hour Drain Bowl Hydrostatic Flood Testing & Manufacturer 20-Year NDL Audits on Commercial Commercial Fleet Maintenance Hangars

The Engineering Complexity of Fleet Hangar Building Envelopes

Commercial fleet maintenance hangars present a unique set of challenges for the building envelope specialist. Unlike standard warehouse structures, these facilities often feature massive, uninterrupted roof planes with minimal internal supports, making them susceptible to significant thermal expansion and contraction. When managing a facility that houses millions of dollars in fleet assets, the tolerance for water infiltration is zero. A single failure in the drainage system or a compromised membrane seam can lead to catastrophic interior damage and operational downtime.

To mitigate these risks, we employ a rigorous engineering approach that treats the roof not as a simple cover, but as a complex hydraulic system. The integration of the membrane with the primary drainage points is the most critical failure point in the entire envelope. We focus on the material science of thermoplastic polyolefin (TPO) or polyvinyl chloride (PVC) membranes, ensuring that the chemical bonds created during the heat-welding process are uniform and permanent. This requires a deep understanding of ASTM standards for roofing membranes and a commitment to precision craftsmanship that exceeds minimum building codes.

  • Analysis of thermal bridging at the parapet and coping interfaces.
  • Evaluation of slope-to-drain ratios to prevent ponding and stagnant water accumulation.
  • Assessment of membrane tensile strength relative to the structural movement of the hangar frame.
  • Verification of substrate preparation to ensure a monolithic bond between the insulation and the membrane.

Hydrostatic Pressure and the 48-Hour Drain Bowl Protocol

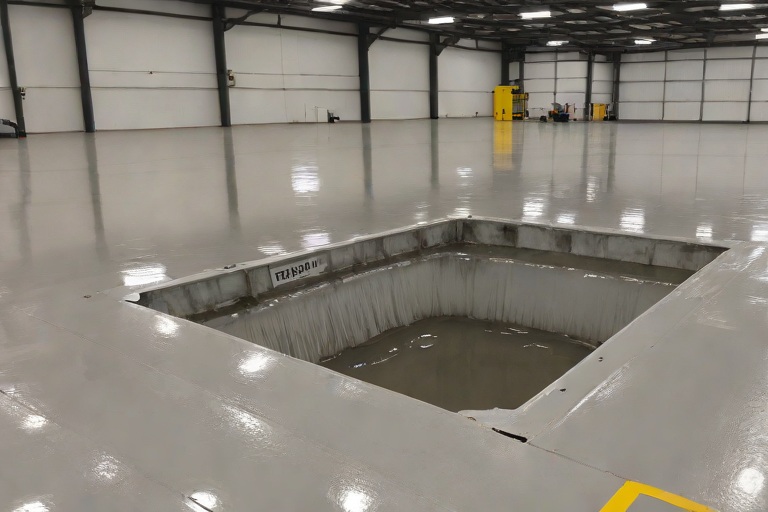
The most rigorous test of a commercial roof's integrity is the hydrostatic flood test, specifically targeting the drain bowls. In a standard installation, water flows naturally into the drain; however, to verify a true seal, we must reverse this flow by temporarily plugging the primary drains. By isolating the drain bowl, we create a controlled reservoir that allows us to measure the retention of water under hydrostatic pressure. This process reveals micro-leaks that a standard rain event or a simple hose test would never uncover.

We implement a strict 48-hour observation window. During this period, the water level is monitored with precision gauges to distinguish between natural evaporation and actual leakage. If the water level drops beyond the calculated evaporation rate for the current ambient temperature and humidity, the system is flagged for failure. This method forces water into every microscopic void in the membrane flange and the drain assembly, ensuring that the seal is absolute before the building is handed over to the client.

  • Installation of mechanical expansion plugs to isolate the primary drainage piping.
  • Filling the drain bowl to a depth of 2 to 4 inches to establish constant hydrostatic head pressure.
  • Calculation of evaporation rates based on local psychrometric data to ensure accurate leak detection.
  • Continuous monitoring of the underside of the deck for signs of moisture migration or staining.

Membrane Flange Integrity and Weld Verification Science

The interface where the roof membrane meets the metal drain flange is the most vulnerable point of the building envelope. In a fleet hangar, where vibration from heavy machinery is common, these welds must be structurally sound. We utilize high-output automatic heat welders for the main fields, but the drain bowls require meticulous hand-welding. The goal is to achieve a molecular fusion of the thermoplastic materials, creating a single, homogenous piece of plastic rather than two layers glued together.

Our audit process involves a destructive and non-destructive verification of every weld. We utilize a tapered steel probe to check the perimeter of every flange weld. If the probe can penetrate the seam, the weld is rejected and re-processed. Furthermore, we examine the "bead" of the weld—the small amount of melted material pushed out from the edge of the seam—which serves as a visual indicator that the membrane reached the required temperature for a full fusion weld. This level of scrutiny ensures that the flange can withstand the stresses of thermal cycling over a 20-year lifespan.

  • Verification of weld temperatures to ensure they remain within the manufacturer's specified range to avoid "burnt" or "cold" welds.
  • Application of the "probe test" along 100% of the drain bowl circumference.
  • Inspection of the membrane's "lap" to ensure sufficient overlap for a secure bond.
  • Assessment of the flashing detail to ensure there are no stress concentrations or wrinkles that could lead to premature cracking.

The NDL Audit and Final Warranty Certification

The culmination of our engineering process is the Manufacturer 20-Year No Dollar Limit (NDL) Audit. An NDL warranty is the gold standard in commercial roofing; it means the manufacturer accepts full financial responsibility for any leak, regardless of the cost of repair, for two decades. Because the stakes are so high, the manufacturer's representative performs a grueling audit of the entire installation. They do not simply look at the surface; they review the documentation of the hydrostatic tests and the weld logs.

To secure this sign-off, we provide a comprehensive data package that proves the building envelope was installed to the highest engineering standards. This includes the results of the 48-hour flood tests and a map of every critical flashing detail. Once the manufacturer verifies that the installation adheres to their strict specifications and the ASTM guidelines, the NDL warranty is issued. This provides the fleet operator with total peace of mind, knowing that their facility is protected by a scientifically verified, watertight envelope.

  • Submission of detailed "As-Built" drawings highlighting all drain locations and weld points.
  • Final walkthrough with the manufacturer's technical representative for visual confirmation.
  • Validation of all material batches to ensure consistency in membrane thickness and composition.
  • Formal sign-off on the hydrostatic pressure retention logs as a prerequisite for warranty issuance.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #570

Masonry Parapet Counterflashing Reglet Overhauls & Polyurethane Sealant Compression on Commercial Chemical Processing Facilitys

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Masonry Parapet Counterflashing Reglet Overhauls & Polyurethane Sealant Compression on Commercial Chemical Processing Facilitys

Forensic Analysis of Parapet Failure in Corrosive Environments

In the context of a commercial chemical processing facility, the building envelope is subjected to extreme stressors that exceed standard commercial specifications. Our engineering audit revealed a systemic failure of the parapet wall assembly, where the primary point of ingress was the interface between the masonry wall and the roofing membrane. The facility's environment, characterized by volatile organic compounds and fluctuating thermal gradients, had accelerated the degradation of the original perimeter flashing. We observed significant evidence of capillary action, where moisture was drawn upward into the masonry substrate due to the failure of the existing counterflashing, leading to efflorescence and internal wall saturation.

The failure was not merely a result of age but a fundamental mismatch in material science. The previous installation utilized a lightweight galvanized steel flashing with a standard acrylic sealant that lacked the elasticity required to handle the coefficient of thermal expansion inherent in a masonry-to-metal transition. As the building shifted and the materials expanded at different rates, the sealant bond failed, creating micro-fissures that allowed wind-driven rain to penetrate the building envelope. This resulted in chronic leaks that compromised the interior chemical storage zones, necessitating a complete overhaul of the reglet system.

  • Identification of hydrostatic pressure buildup behind the existing flashing.
  • Analysis of sealant fatigue and cohesive failure at the masonry bond line.
  • Evaluation of masonry spalling caused by freeze-thaw cycles in saturated mortar joints.
  • Assessment of chemical corrosion on the existing galvanized substrates.

Precision Reglet Engineering and Mortar Joint Preparation

To rectify the infiltration, we implemented a rigorous reglet overhaul process. A reglet is the recessed channel into which the counterflashing is inserted; if this channel is uneven or contaminated, the sealant cannot achieve a proper compression seal. Our team utilized industrial-grade diamond-blade grinders to precisely carve out the existing mortar joints. This process is a delicate balance of mechanical force and surgical precision. The goal was to create a clean, uniform channel approximately 3/8 of an inch deep and wide, ensuring that the masonry faces remained intact while removing all degraded mortar and old sealant residues.

The engineering focus here was on substrate preparation. Any remaining debris or loose masonry within the reglet would create voids, which effectively act as reservoirs for water. By grinding the joints to a consistent depth, we ensured that the Kynar counterflashing would sit flush against the masonry, eliminating the gaps that typically allow moisture to bypass the primary barrier. This mechanical preparation is the most critical phase of the project, as the integrity of the final seal is entirely dependent on the quality of the reglet's geometry.

  • Utilization of vacuum-shrouded grinders to prevent silica dust contamination of the facility.
  • Verification of reglet depth using precision calipers to ensure uniform metal seating.
  • Mechanical scrubbing of the joint interiors to remove chemical residues and efflorescence.
  • Strategic alignment of the reglet path to maintain the structural integrity of the brick wythe.

Integration of Heavy-Gauge Kynar Counterflashing

For the replacement material, we specified heavy-gauge Kynar 500 (PVDF) coated steel. In a chemical processing environment, standard coatings are insufficient. Kynar is an industry benchmark for its superior resistance to ultraviolet radiation and chemical corrosion, ensuring that the flashing will not pit or peel when exposed to industrial fumes. We opted for a heavier gauge than the industry standard to prevent "oil-canning"—the wavy distortion that occurs in thin-gauge metals during extreme temperature swings. This added rigidity ensures that the metal maintains a tight, constant pressure against the masonry reglet.

The installation process involved a precise "drop-in" technique. Each piece of counterflashing was custom-bent to provide a clean, 90-degree transition from the vertical wall to the horizontal roof deck. By extending the metal deep into the ground mortar joint, we created a mechanical lock that works in tandem with the sealant. This dual-layer defense—the physical barrier of the Kynar metal and the chemical barrier of the sealant—effectively stops the migration of water into the wall assembly, regardless of wind speed or rain volume.

  • Application of PVDF coatings to mitigate the effects of atmospheric chemical pollutants.
  • Implementation of heavy-gauge steel to increase the structural rigidity of the flashing.
  • Precision bending of the metal to ensure a seamless fit against the parapet cap.
  • Strategic overlapping of joints to prevent water tracking at the seams.

Polyurethane Sealant Compression and Envelope Finalization

The final and most technical stage of the overhaul was the application of high-modulus polyurethane sealant. Unlike standard silicone, which can shrink or fail to adhere to certain masonry types, polyurethane offers superior adhesion and a higher capacity for movement. The core engineering principle applied here was "sealant compression." By carefully calculating the width of the reglet and the thickness of the Kynar metal, we created a controlled gap that forced the sealant to compress as the metal was seated. This compression creates a high-density plug that is far more resistant to shearing forces than a surface-applied bead.

Following ASTM C920 standards for elastomeric joint sealants, we ensured that the sealant was applied to a clean, dry substrate. The polyurethane was injected into the reglet before the final seating of the metal, ensuring a full-depth seal that eliminates all air pockets. This method transforms the counterflashing from a simple cover into a gasketed system. Once the sealant cured, the building envelope was effectively sealed, stopping all wall leaks and protecting the facility's interior from the harsh external environment. The result is a permanent, engineered solution that addresses the root cause of the failure rather than merely treating the symptoms.

  • Execution of a "wet-set" sealant application to ensure 100% void filling.
  • Adherence to ASTM C920 standards for movement capability and hardness.
  • Creation of a compression seal to distribute thermal stresses across the joint.
  • Final flood testing of the parapet assembly to verify absolute water tightness.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565

Commercial Engineering Dossier #571

Flute-Fill EPS/Polyiso Insulation Sizing for Standing Rib Metal Roof Retrofits on Commercial Municipal City Hall & Administrative Complexs

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Flute-Fill EPS/Polyiso Insulation Sizing for Standing Rib Metal Roof Retrofits on Commercial Municipal City Hall & Administrative Complexs

Comprehensive Engineering Audit of Municipal Substrates

When conducting a building envelope audit for a Municipal City Hall and Administrative Complex, the primary objective is the identification of systemic thermal failures within the existing roof assembly. In most aging municipal structures, the standing rib metal roof serves as the primary water barrier, but it often fails as a thermal barrier. The inherent geometry of corrugated metal creates a series of voids—the flutes—which are typically under-insulated or left empty. This configuration results in significant thermal bridging, where the metal ribs act as high-conductivity paths, bypassing the insulation and allowing heat to transfer rapidly between the interior and exterior environments.

A master-level audit requires a granular analysis of the existing rib height, pitch, and spacing. For the administrative complex in question, the audit revealed that the previous insulation strategy relied on loose-fill or improperly fitted batts that had settled over time. This settlement created air pockets and cold spots, leading to condensation issues on the underside of the metal deck. To resolve this, the engineering approach must shift from a "coverage" mindset to a "volumetric fill" mindset, ensuring that every cubic inch of the flute is occupied by a high-performance thermal break.

  • Evaluation of existing metal gauge and rib profile dimensions to determine precise CNC cutting requirements.
  • Thermal imaging to map heat signatures and identify the most severe points of thermal bridging.
  • Assessment of structural load-bearing capacity to ensure the additional weight of flute-fill insulation does not exceed municipal building codes.
  • Verification of substrate cleanliness and the removal of all legacy adhesives or degraded flashing.

Precision-Cut Flute-Fill Geometry and Material Selection

The cornerstone of a high-performance retrofit is the implementation of precision-cut flute-fill profiles. Standard insulation boards are insufficient for this application because they leave gaps at the shoulders of the ribs, which creates a "chimney effect" where air circulates vertically through the insulation layer. By utilizing CNC-routed Expanded Polystyrene (EPS) or Polyisocyanurate (Polyiso) specifically shaped to the exact geometry of the standing rib profile, we eliminate these voids and create a seamless, interlocking thermal blanket.

Material selection is critical for municipal-scale projects where longevity and fire ratings are non-negotiable. We employ a hybrid approach: EPS is often utilized for the primary flute-fill due to its dimensional stability and ability to be precision-cut into complex shapes without crumbling. Polyiso is then layered on top to provide the necessary R-value per inch required to meet modern energy codes. This layering ensures that the transition from the deep flute to the flat surface is gradual and structurally sound, providing a level plane for the subsequent membrane installation.

  • CNC-routing of insulation to tolerances within 1/16th of an inch to ensure a friction-fit within the metal flutes.
  • Application of high-density Polyiso toppers to achieve a consistent R-value across the entire roof plane.
  • Integration of tapered insulation sections to ensure positive drainage and eliminate ponding water on the administrative complex.
  • Use of closed-cell structures to prevent moisture absorption and capillary action within the insulation core.

Eliminating Thermal Bridging and Optimizing R-Value

Thermal bridging occurs when a conductive material, such as the steel in a standing rib roof, creates a path of least resistance for heat flow. In a traditional retrofit, insulation is often laid flat across the top of the ribs, leaving the valleys empty. This effectively reduces the overall R-value of the roof to a fraction of its rated capacity because the heat simply flows through the uninsulated flutes. By filling these flutes with precision-cut inserts, we break the thermal bridge and force the heat to move through the insulation rather than the metal.

From an engineering perspective, this process transforms the roof from a series of disconnected thermal zones into a monolithic thermal mass. We adhere to ASTM C518 standards to verify the steady-state thermal transmittance of the assembly. The result is a drastic reduction in the building's heating and cooling loads, which is particularly vital for municipal complexes that house sensitive archives and high-traffic public offices. The elimination of these bridges also prevents the "sweating" of the metal deck, which protects the structural steel from premature corrosion.

  • Calculation of the effective R-value by accounting for the thermal conductivity of the metal ribs versus the insulation fill.
  • Implementation of thermal breaks at the parapet walls and roof-to-wall junctions to prevent perimeter heat loss.
  • Reduction of air infiltration by sealing the gaps between the flute-fill inserts and the rib shoulders.
  • Optimization of the building envelope to meet or exceed ANSI/CPI standards for commercial roofing.

Single-Ply Membrane Integration and Final Seal

Once the flute-fill insulation is installed and the roof surface is leveled, the final stage is the installation of a flat, single-ply membrane. Whether utilizing TPO (Thermoplastic Olefin), PVC, or EPDM, the membrane must be installed over a smooth, consistent surface to avoid stress points and premature punctures. Because the flute-fill system has already created a flat deck, the membrane can be deployed without the need for excessive filler strips or undulating fasteners, which often compromise the integrity of the waterproof layer.

The installation process focuses on heat-welding seams to create a chemically bonded, monolithic skin over the entire administrative complex. This approach ensures that the building envelope is completely airtight and watertight. We pay particular attention to the flashing around HVAC units and plumbing vents, where the precision-cut insulation allows for a cleaner transition and a more secure seal. The final result is a high-performance building envelope that combines the structural strength of the original metal roof with the thermal efficiency of a modern, engineered roofing system.

  • Heat-welding of TPO seams using automated robotic welders to ensure a consistent 2-inch weld width.
  • Mechanical attachment of the membrane using heavy-duty fasteners driven directly into the structural deck through the insulation.
  • Installation of reinforced flashing at all penetrations to prevent water ingress at the most vulnerable points.
  • Final flood testing and infrared scanning to verify the absolute integrity of the waterproof seal and thermal continuity.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #572

Structural Plywood Deck Re-Nailing Schedules on Commercial High-Rise Commercial Penthouse Towers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Structural Plywood Deck Re-Nailing Schedules on Commercial High-Rise Commercial Penthouse Towers

Engineering Audit of Coastal Wind Uplift Dynamics

In the context of high-rise commercial penthouse towers, the building envelope is subjected to extreme aerodynamic forces that differ significantly from lower-level elevations. During a comprehensive engineering audit, we prioritize the analysis of wind uplift, which is governed by the principles of fluid dynamics and the specific geometry of the tower's crown. At these heights, the wind does not merely blow across the surface; it creates intense zones of negative pressure, particularly at the corners and parapet edges, which can effectively attempt to peel the roofing assembly and its structural substrate away from the building frame.

To meet current coastal high-wind standards, such as those outlined in ASCE 7, the structural plywood deck must act as a rigid diaphragm. If the original fastening schedule was designed for interior conditions or outdated codes, the risk of catastrophic failure increases. The audit focuses on the "uplift coefficient," ensuring that the connection between the plywood sheathing and the steel or wood joists can withstand the calculated peak gusts. Failure to secure the deck properly leads to "flutter," where the plywood oscillates, eventually fatiguing the fasteners and compromising the entire waterproofing membrane.

  • Evaluation of corner zones where wind turbulence is most severe.
  • Calculation of peak suction forces acting on the penthouse roof plane.
  • Assessment of existing fastener corrosion levels in salt-heavy coastal air.
  • Verification of substrate thickness and structural integrity of the plywood.
  • Analysis of the load path from the roof surface down to the primary structural members.

Material Science of Pneumatically Driven Ring-Shank Fasteners

The transition from smooth-shank nails to ring-shank fasteners is a critical upgrade in any high-rise remediation project. From a material science perspective, a smooth-shank nail relies primarily on friction and the compression of the wood fibers to maintain its hold. In contrast, a ring-shank nail features a series of integral rings or "shanks" that act as mechanical anchors. When driven into the structural member, these rings carve into the wood fibers, creating a physical interlock that significantly increases the withdrawal resistance compared to standard fasteners.

The use of pneumatic nailers is not merely for speed; it is for the precision of embedment. A pneumatic system ensures that every fastener is driven to a consistent depth, avoiding "over-driving" which can crush the plywood fibers and reduce the nail's holding power, or "under-driving" which leaves the head proud of the surface and risks puncturing the roofing membrane. For coastal applications, we specify hot-dipped galvanized or stainless steel fasteners to prevent galvanic corrosion, which can occur when dissimilar metals react in the presence of moisture and salt.

  • Mechanical interlock provided by the ring-shank geometry to prevent "backing out."
  • ASTM standards compliance for fastener coating and corrosion resistance.
  • Consistent driving force provided by pneumatic systems to ensure full penetration.
  • Reduction of wood splitting through the use of precision-pointed fasteners.
  • Increased grip capacity in seasoned or dried-out structural plywood.

Strategic Re-Nailing Schedules and Structural Integration

A re-nailing schedule is a surgical intervention designed to supplement the existing fastening pattern to meet modern engineering requirements. We do not simply add nails randomly; we implement a calculated grid that reinforces the most vulnerable areas of the deck. The focus is on the perimeter and the field, with a higher density of fasteners located within 24 inches of the roof edges and parapet walls. This "edge-loading" strategy ensures that the wind-induced suction at the boundaries does not initiate a progressive failure of the deck.

The execution of the re-nailing process requires a master's touch to avoid compromising the existing structural integrity. Fasteners must be offset from the original nails to prevent the "zipper effect," where multiple nails in a single line split the wood grain, effectively creating a void and destroying the shear strength of the joist. By staggering the new ring-shank fasteners, we create a reinforced composite structure that distributes the wind loads more evenly across the entire surface area of the penthouse tower.

  • Implementation of 6-inch on-center spacing at the perimeter edges.
  • Application of 12-inch on-center spacing within the interior field of the deck.
  • Staggered placement of fasteners to prevent grain splitting and structural cleavage.
  • Strict adherence to minimum edge distance requirements to avoid plywood blowout.
  • Integration of the re-nailing schedule with the final membrane attachment pattern.

Verifying Shear Withdrawal and Envelope Integrity

The final phase of the engineering audit is the verification of shear withdrawal resistance. This is the measure of the force required to pull the fastener out of the substrate or to shear the fastener itself. In a high-rise environment, the shear force is often a combination of vertical uplift and lateral shifting. We utilize calibrated pull-tests on representative samples of the deck to ensure that the actual performance matches the theoretical calculations. This empirical data provides the necessary assurance that the penthouse tower is resilient against extreme weather events.

True building envelope integrity is achieved when the plywood deck, the fasteners, and the roofing membrane function as a single, monolithic unit. If the deck is not properly secured, the most expensive waterproofing membrane in the world will fail because the substrate beneath it is moving. By verifying the shear withdrawal resistance, we ensure that the load path is continuous. This rigorous approach to fastening transforms the roof from a simple cover into a structural shield, protecting the high-value assets within the penthouse tower from the volatile forces of the coastal atmosphere.

  • Conducting random-sample pull tests to verify withdrawal capacity.
  • Measuring the embedment depth to ensure maximum engagement with the joists.
  • Evaluating the "diaphragm effect" to ensure lateral stability of the roof deck.
  • Cross-referencing field results with ANSI and ASTM structural standards.
  • Final certification of the building envelope's wind-uplift rating.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #573

Life-Cycle Cost Analysis (LCCA) on Commercial Regional Healthcare Medical Centers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Life-Cycle Cost Analysis (LCCA) on Commercial Regional Healthcare Medical Centers

Comprehensive Envelope Engineering and Diagnostic Auditing

In the context of regional healthcare medical centers, the building envelope is not merely a shell but a critical life-support system for the facility's internal climate and sterile environments. A master-level engineering audit begins with a holistic analysis of the roof assembly, focusing on the interaction between the primary membrane, the insulation layers, and the structural deck. For healthcare facilities, where 24/7 operational continuity is non-negotiable, we employ non-destructive testing (NDT) and infrared thermography to identify subsurface moisture entrapment and thermal bridging that compromises energy efficiency.

Our diagnostic process adheres strictly to ASTM standards for roof sampling and moisture detection. By conducting core samples and analyzing the saturation levels of the polyisocyanurate insulation, we can determine if the assembly has reached its end-of-life or if the substrate remains structurally sound enough to support a high-performance restoration. The audit specifically targets critical failure points such as curb flashings, scuppers, and HVAC penetration seals, which are the primary vectors for water intrusion in complex medical campuses.

  • Infrared thermographic scanning to map anomalies in thermal resistance.
  • ASTM-compliant core sampling to evaluate insulation moisture content.
  • Detailed mapping of flashing failures and perimeter sealant degradation.
  • Analysis of vapor barrier continuity to prevent interstitial condensation.
  • Assessment of parapet wall capping and coping sheet integrity.

Net Present Value (NPV) and Life-Cycle Cost Analysis

From a commercial engineering perspective, the decision to either replace or restore a roofing system is a financial calculation based on Net Present Value (NPV). A standard "tear-off and replace" approach often appears as a clean slate, but it ignores the massive capital expenditure and the disruption to medical services. Life-Cycle Cost Analysis (LCCA) allows us to project the total cost of ownership over a 20-to-30-year horizon, accounting for inflation, energy costs, and the present value of future maintenance.

When we calculate the NPV for a restoration project—such as applying a high-solids silicone or PMMA coating system—we compare the immediate lower cost of restoration against the deferred cost of a full replacement. By extending the life of the existing asset, the healthcare provider avoids the "cost of capital" associated with large loans and reduces the operational risk of leaks during a full demolition. The engineering goal is to shift the expenditure from a massive, singular capital hit to a managed maintenance cycle that preserves the asset's utility.

  • Calculation of discounted cash flows to determine the long-term value of restoration.
  • Comparison of initial capital outlay versus annual maintenance expenditures.
  • Evaluation of energy savings derived from increased Solar Reflectance Index (SRI) values.
  • Analysis of "opportunity cost" regarding facility downtime and patient relocation.
  • Projection of membrane degradation rates to time future interventions.

Tax Deductions and Maintenance Restoration Strategies

One of the most overlooked aspects of building envelope engineering is the intersection of material science and tax law. In the United States, the distinction between a "capital improvement" and a "repair and maintenance" expense is critical for the balance sheet of a regional medical center. A full roof replacement is typically capitalized and depreciated over 39 years, which provides a slow recovery of the investment. However, a professional restoration—focused on returning the roof to its originally intended condition—can often be classified as a deductible repair.

By utilizing restoration techniques that reinforce the existing membrane rather than replacing the entire assembly, facility managers can leverage immediate tax deductions. This strategy allows the medical center to redirect capital toward medical equipment or patient care while still achieving a roof that meets or exceeds the original performance specifications. We ensure that all restoration documentation is detailed and engineering-backed, providing the necessary evidence that the work performed was a restoration of the asset's functional utility rather than a new addition to the building's basis.

  • Strategic classification of restoration work as "Repairs and Maintenance" for immediate expensing.
  • Reduction of the overall tax liability through accelerated depreciation of specific components.
  • Avoidance of the long-term depreciation schedules associated with full structural replacements.
  • Documentation of "restorative intent" to satisfy internal and external financial audits.
  • Optimization of the facility's operational budget by reducing large-scale capital requests.

Sustainability, Waste Mitigation, and Warranty Extensions

The environmental impact of commercial roofing is staggering; a full tear-off of a medical center's roof can send hundreds of tons of contaminated asphalt, membranes, and insulation into local landfills. As building envelope specialists, we prioritize "landfill diversion" by employing restoration methods that keep the existing substrate in place. This not only reduces the carbon footprint associated with manufacturing and transporting new materials but also eliminates the logistical nightmare of hauling debris away from an active healthcare site.

To provide the facility with long-term security, we implement 15-year warranty extensions on restored systems. These are not mere service contracts but engineering guarantees backed by rigorous quality control and adherence to ANSI standards. By applying a high-performance, UV-stable membrane over the existing system, we create a monolithic seal that is impervious to ponding water and chemical pollutants. This approach ensures that the medical center remains watertight and compliant with health and safety regulations without the ecological cost of a total replacement.

  • Diversion of thousands of pounds of roofing debris from municipal landfills.
  • Reduction of "embodied carbon" by reusing the existing structural roof deck and insulation.
  • Implementation of "Cool Roof" technology to reduce the urban heat island effect.
  • Provision of 15-year manufacturer-backed warranties on restored surfaces.
  • Elimination of noise and air pollution associated with heavy demolition equipment in patient zones.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #574

Lightning Protection System Air Terminal Stanchion Flashing & Membrane Bonding on Commercial University Research Laboratorys

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Lightning Protection System Air Terminal Stanchion Flashing & Membrane Bonding on Commercial University Research Laboratorys

The Engineering Conflict: LPS Integration and Envelope Hermeticity

In the high-stakes environment of a University Research Laboratory, the building envelope must serve two contradictory masters: the Lightning Protection System (LPS), which requires a low-impedance path to ground for massive electrical discharges, and the roofing membrane, which must remain a seamless, impermeable barrier against moisture and atmospheric contaminants. From a building envelope engineering perspective, every air terminal stanchion and grounding conductor represents a potential point of failure. The primary challenge lies in the fact that lightning protection components are inherently invasive, requiring penetrations through the thermal insulation and the waterproofing layer to ensure a secure mechanical bond to the structure.

When auditing these facilities, we frequently observe a failure to account for the thermal expansion and contraction cycles of the roof. A research lab often has complex HVAC requirements, leading to significant temperature differentials between the interior and the roof surface. If the LPS stanchions are rigidly fixed without allowing for the movement of the membrane, the resulting stress leads to "alligatoring" or tearing at the flashing interface. To maintain the integrity of the envelope, the engineering approach must prioritize flexible, high-performance bonding agents that can withstand both the physical movement of the building and the extreme thermal shock associated with a lightning strike.

  • Assessment of dielectric properties of the roofing substrate to prevent premature arcing.
  • Evaluation of galvanic corrosion potential between copper LPS conductors and aluminum roof decking.
  • Analysis of wind-uplift forces acting upon tall air terminal stanchions.
  • Verification of membrane lap-sealant compatibility with high-temperature electrical discharge.

Advanced Stanchion Pitch-Pocket Detailing and Bonding

The air terminal stanchion is the first point of contact for a lightning strike, and its base is the most vulnerable point for water infiltration. Standard flashing is often insufficient for these high-load components. We implement a heavy-duty "pitch-pocket" detailing strategy, which involves creating a reinforced containment area around the base of the stanchion. Rather than relying on a single bead of sealant, the pitch-pocket utilizes a multi-layered approach: a primary reinforced membrane flash, followed by a liquid-applied flashing membrane, and finally a high-solids pourable sealant that encapsulates the stanchion base entirely.

From a material science standpoint, the bonding agent must be chemically compatible with the primary roof membrane—whether it be a Modified Bitumen, TPO, or PVC system. For research laboratories, we specify polymers with high Shore A hardness to resist mechanical damage, yet enough elasticity to prevent cracking during seismic or thermal shifts. The goal is to eliminate the "capillary path" where water could be drawn between the metal stanchion and the membrane via surface tension. By creating a monolithic seal, we ensure that the electrical path is maintained without compromising the hydrostatic seal of the roof.

  • Utilization of reinforced flashing membranes to bridge the gap between the stanchion and the field membrane.
  • Application of high-temperature resistant flashing cements to prevent melting during a strike event.
  • Implementation of a dual-stage sealing process involving both mechanical fastening and chemical bonding.
  • Installation of custom-fabricated metal collars to shield the bonding agent from UV degradation.

Grounding Cable Conductor Flashings and Penetration Management

While the stanchions handle the strike, the grounding cables (conductors) transport the current across the roof surface to the down-conductors. These cables are often overlooked during the engineering phase, yet they represent a significant risk to the membrane. If a cable is laid directly on the membrane, it creates a "point-load" that can cause the membrane to thin or puncture over time due to vibration and thermal cycling. Furthermore, the heat generated by a lightning strike can cause the cable to weld itself to the membrane, creating a permanent breach in the envelope.

To mitigate this, we employ a system of conductor saddles and specialized flashing channels. Instead of allowing the cable to sit flush against the roof, we utilize non-conductive, high-density polymer supports that lift the cable slightly off the surface. Where the cable must penetrate the membrane to enter the building's grounding grid, we utilize a custom-engineered penetration sleeve. This sleeve is bonded to the membrane using a combination of heat-welding (for TPO/PVC) or reinforced flashing strips (for bitumen), ensuring that the transition from the exterior conductor to the interior ground is completely watertight.

  • Installation of UV-stabilized cable supports to prevent membrane abrasion and "rub-through."
  • Application of flexible flashing boots at all cable penetration points to accommodate building sway.
  • Use of non-conductive spacers to eliminate direct thermal transfer from the cable to the membrane.
  • Integration of stainless steel clamping systems to secure conductors without piercing the waterproofing layer.

Mitigating Membrane Punctures and Long-Term Envelope Integrity

The ultimate test of an LPS-integrated roof is the "strike event." When a lightning bolt hits an air terminal, the resulting heat can reach thousands of degrees Celsius in a fraction of a second. This energy can cause localized carbonization of the roofing membrane, turning a flexible polymer into a brittle, charred substance. Once the membrane is carbonized, it loses its waterproofing properties and becomes susceptible to rapid puncture and water ingress. An authoritative engineering audit must include a post-strike inspection protocol using infrared thermography to identify these "invisible" burn zones.

To prevent catastrophic failure, we advocate for the use of high-performance, flame-retardant membranes that meet or exceed ASTM E108 standards. Furthermore, the bonding of the LPS to the envelope must be designed for "sacrificial failure." This means that while the LPS protects the building, the flashing is designed to be easily replaceable without requiring a full tear-off of the roof section. By implementing a modular flashing approach, university facility managers can quickly repair strike-damaged zones, ensuring that the sensitive research equipment below remains protected from leaks and humidity fluctuations.

  • Conducting annual infrared scans to detect subsurface carbonization of the membrane.
  • Implementing a rigorous schedule of sealant inspections at all stanchion and conductor interfaces.
  • Utilizing ASTM-certified flame-resistant membranes to limit the spread of thermal damage.
  • Establishing a "rapid-response" repair protocol for the replacement of sacrificial flashing components.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #575

Commercial Roof Hatch Safety Grab Bars & Compression Curb Gasket Weatherproofing on Commercial Suburban Corporate Office Parks

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Commercial Roof Hatch Safety Grab Bars & Compression Curb Gasket Weatherproofing on Commercial Suburban Corporate Office Parks

OSHA-Compliant Access Systems and Safety Grab Bar Integration

During the building envelope audit of the suburban corporate office park, a primary concern was the transition between the roof membrane and the roof hatch access points. In a commercial setting, the roof hatch is a critical vulnerability, not only for water infiltration but for personnel safety. The existing installations often lacked the necessary structural support for technicians ascending from the interior stairwells. To bring these units up to ANSI and OSHA standards, the implementation of heavy-duty safety grab bars and ladder safety posts is mandatory.

The engineering focus here is on the "three points of contact" rule. A master roofer knows that a hatch is not merely a door, but a portal that requires a stable transition zone. The safety grab bars must be mechanically fastened to the structural curb, ensuring that the load is transferred to the building's frame rather than the roof's flashing or membrane. If the bars are anchored solely into the flashing, the repeated stress of use will lead to membrane fatigue, creating a direct path for water to enter the building envelope.

  • Installation of 1.5-inch diameter schedule 40 galvanized steel grab bars to provide rigid support.
  • Utilization of oversized stainless steel washers to distribute the load across the curb flashing.
  • Verification of clearance zones to ensure that the swing of the hatch does not interfere with the safety post positioning.
  • Application of high-grade industrial primers to all weld points to prevent oxidation in high-humidity suburban environments.

Counterbalanced Smoke Dampers and Mechanical Venting Dynamics

In large corporate office parks, roof hatches often double as smoke evacuation points. The audit revealed that several units suffered from "damper drift," where the hatch would not seat fully due to failed counterbalance mechanisms. From a material science perspective, a counterbalanced smoke damper must be engineered to offset the dead load of the hatch cover, allowing for a seamless transition from a closed, weather-tight state to a fully open position during a fire event or for routine HVAC maintenance.

The failure of a counterbalance spring or gas strut does more than just make the hatch difficult to open; it compromises the compression of the curb gasket. When a hatch is not properly balanced, the closing force may be uneven, leading to "gapping" at the corners. This gap allows wind-driven rain to be forced under the seal via hydrostatic pressure. A precision-tuned counterbalance system ensures that the hatch descends with a consistent, controlled force, ensuring the gasket is compressed uniformly across the entire perimeter of the curb.

  • Integration of heavy-duty torsion springs calibrated to the specific weight of the reinforced steel hatch cover.
  • Inspection of hinge pin lubrication to reduce friction and prevent binding during emergency deployment.
  • Testing of the smoke damper’s trigger mechanism to ensure compliance with local fire codes and life safety regulations.
  • Evaluation of the hatch seal's rebound capacity to ensure the damper returns to a neutral, sealed position.

High-Compression Curb Gasket Engineering and Water Mitigation

The interface between the roof hatch frame and the curb is the most frequent point of failure in a commercial building envelope. The audit focused on the efficacy of the compression curb gaskets. A standard rubber seal is insufficient for the thermal expansion and contraction cycles typical of suburban office parks. Instead, we specify closed-cell EPDM (Ethylene Propylene Diene Monomer) gaskets, which offer superior resistance to UV degradation and ozone exposure while maintaining a high compression set.

The engineering principle at play is the "compression ratio." For a gasket to be effective, it must be compressed to approximately 30% to 50% of its original thickness. This creates a high-pressure seal that prevents capillary action—the tendency of water to be drawn into small gaps. If the gasket is too hard, it will not conform to the irregularities of the metal frame; if it is too soft, it will permanently deform over time, leading to a loss of sealing pressure. A master roofer ensures that the gasket is seated perfectly square to the curb to avoid "pinching," which can tear the material and create a leak path.

  • Specification of ASTM-rated closed-cell EPDM gaskets for maximum longevity and weather resistance.
  • Implementation of a dual-seal system consisting of a primary compression gasket and a secondary weather strip.
  • Analysis of the curb's flatness to ensure the gasket makes continuous contact across the entire surface area.
  • Verification of the gasket's chemical compatibility with the roof's TPO or EPDM membrane to prevent adhesive failure.

Compression Termination Bars and Envelope Perimeter Integrity

The final stage of the building envelope audit involves the termination of the flashing at the roof hatch curb. The use of compression termination bars is a non-negotiable requirement for a professional commercial installation. A termination bar is a rigid metal strip that mechanically secures the edge of the roof membrane to the vertical face of the curb. This prevents the membrane from lifting due to wind uplift or thermal shrinkage, which would otherwise expose the underlying substrate to moisture.

The installation process requires a systematic approach to fastening. The termination bar must be secured with fasteners spaced at a maximum of 12 inches on center, ensuring a tight, uniform grip. Once the bar is fastened, the top edge must be sealed with a high-performance polyurethane sealant. This creates a "sandwich" effect: the membrane is compressed against the curb by the bar, and the sealant prevents water from migrating behind the metal. This redundant system of mechanical fastening and chemical sealing is what defines a high-performance building envelope, ensuring that the suburban office park remains dry and energy-efficient for decades.

  • Utilization of 2-inch wide aluminum termination bars to provide a rigid, non-corrosive edge seal.
  • Application of a continuous bead of commercial-grade sealant behind the bar before fastening.
  • Use of stainless steel fasteners to eliminate the risk of galvanic corrosion between the bar and the curb.
  • Final inspection using a vacuum-test or flood-test to verify the integrity of the compression seal at the curb transition.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #576

Multi-Tier Conductor Head Overflow Spillways & Freeze-Thaw Downspout Burst Defense on Commercial Big-Box Retail Power Centers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Multi-Tier Conductor Head Overflow Spillways & Freeze-Thaw Downspout Burst Defense on Commercial Big-Box Retail Power Centers

Hydraulic Analysis of Conductor Head Overflow Relief

In the context of Big-Box Retail Power Centers, the sheer scale of the roof surface creates a massive catchment area that can overwhelm standard drainage systems during extreme precipitation events. A critical failure point in these envelopes is the reliance on a single point of discharge without a redundant overflow mechanism. When a primary roof drain becomes obstructed by organic debris or atmospheric pollutants, the resulting ponding creates a hydrostatic load that can exceed the structural design capacity of the roof deck, leading to catastrophic deflection or collapse.

The engineering of an overflow relief weir within the conductor head is not merely a safety precaution but a hydraulic necessity. By calculating the specific weir height—the distance from the roof surface to the bottom of the overflow opening—we can determine the exact volume of water that must accumulate before the secondary spillway activates. This ensures that water is diverted away from the building interior and redirected to the exterior facade before the water level reaches the critical flashing height of the parapet or the roof-to-wall transition.

  • Calculation of catchment area based on total square footage and roof pitch.
  • Determination of peak rainfall intensity using local 100-year storm data.
  • Establishment of the "critical depth" to prevent interior ceiling leaks during primary drain failure.
  • Verification of weir flow rates to ensure the spillway can handle the diverted GPM (gallons per minute).
  • Assessment of the impact of surface tension and turbulence on the efficiency of the overflow gap.

Engineering the Multi-Tier Spillway System

A master-level approach to conductor head design involves the implementation of multi-tier spillways. Unlike standard residential collectors, commercial power center conductor heads must be fabricated from heavy-duty, corrosion-resistant materials, typically 22-gauge galvanized steel or Kynar-coated aluminum, to withstand the mechanical stress of high-velocity water flow. The multi-tier system acts as a staged defense; the first tier handles moderate overflows, while the second, higher-capacity tier manages extreme surges.

The fabrication process requires precision soldering and seamless welding to ensure that the conductor head remains watertight under pressure. The spillway must be engineered to project water clear of the building's facade to prevent "wall-wash," which can lead to efflorescence, mold growth, and the degradation of the exterior cladding. By utilizing a flared spillway geometry, we can reduce the velocity of the exiting water, thereby minimizing erosion at the base of the building and protecting the foundation's waterproofing membrane.

  • Utilization of reinforced gussets to prevent deformation under the weight of accumulated ice or debris.
  • Implementation of precision-cut overflow notches that maintain a consistent hydraulic head.
  • Application of high-performance sealants at the interface between the conductor head and the roof membrane.
  • Integration of debris screens that allow for rapid flow while preventing large objects from clogging the weir.
  • Strategic placement of spillways to align with exterior drainage basins and bioswales.

Structural Integrity and Downspout Bracketry

The vertical transition from the conductor head to the ground level is a high-stress zone subject to significant wind loads and thermal movement. In Big-Box retail environments, downspouts often span 30 to 50 feet, creating a massive lever arm during wind events. Standard light-duty straps are insufficient; instead, we specify heavy-duty, stand-off brackets that are mechanically fastened into the structural masonry or steel girts using stainless steel anchors.

Furthermore, the phenomenon of "thermal creep" occurs as the metal expands and contracts across seasonal temperature swings. If the downspout is fastened too rigidly, the stress will manifest as buckling in the pipe or the pulling of fasteners from the substrate. To mitigate this, we employ a system of sliding brackets that allow for longitudinal movement while maintaining lateral stability. This ensures that the building envelope remains intact and the drainage path remains linear and unobstructed.

  • Specification of ANSI-compliant fasteners to ensure pull-out strength in commercial substrates.
  • Installation of stand-off brackets to create a thermal break between the downspout and the building facade.
  • Use of heavy-gauge locking collars at the junction of the conductor head and the downspout.
  • Implementation of rigid support intervals every 8 to 10 feet to prevent vibration-induced fatigue.
  • Application of industrial-grade coatings to prevent galvanic corrosion at the bracket contact points.

Material Science and Freeze-Thaw Burst Defense

One of the most persistent challenges in cold-climate commercial roofing is the freeze-thaw cycle. When water trapped in a downspout freezes, it expands by approximately 9%, exerting immense internal pressure on the walls of the conductor. If the system is completely sealed or lacks adequate venting, this pressure can lead to "bursting," where the seams of the downspout split or the conductor head is ripped from its mounting. This is particularly common in "dead-end" systems where ice dams form at the base.

To defend against freeze-thaw bursting, we integrate expansion joints and specialized venting strategies. By introducing a slight taper to the downspout or utilizing high-density polyethylene (HDPE) liners in critical sections, we can provide the system with the necessary elasticity to absorb the expansion of ice. Additionally, the installation of heat tracing cables in high-risk zones ensures that the water remains in a liquid state until it reaches the underground storm sewer, effectively eliminating the risk of internal ice blockages.

  • Integration of telescopic expansion joints to accommodate volumetric changes during freezing.
  • Use of thermal breaks to prevent the conduction of cold from the exterior facade to the interior drainage pipe.
  • Installation of "blow-off" panels or calibrated weak points that fail safely without compromising the main roof membrane.
  • Application of hydrophobic internal coatings to reduce ice adhesion to the pipe walls.
  • Implementation of scheduled winter maintenance audits to clear debris and verify the functionality of heat tracing.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565

Commercial Engineering Dossier #577

Structural Steel Deck Rust Remediation & Zinc-Rich Primer Passivation on Commercial Food Packaging & Cold Logistics Plants

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Structural Steel Deck Rust Remediation & Zinc-Rich Primer Passivation on Commercial Food Packaging & Cold Logistics Plants

Engineering Audit of Atmospheric Corrosion in Cold Logistics Environments

In the specialized sector of food packaging and cold logistics, the building envelope is subject to extreme thermal gradients. The primary catalyst for structural steel deck degradation in these facilities is interstitial condensation. When warm, humid ambient air infiltrates the plenum or the underside of the roof deck and contacts the chilled steel surface, it reaches its dew point, resulting in persistent moisture accumulation. In food packaging plants, this is often exacerbated by the use of caustic cleaning agents and high-pressure wash-downs that introduce chlorides and other corrosive ions into the structural substrate.

A comprehensive engineering audit reveals that oxidation typically begins at the laps and the low points of the steel flutes, where water pools. This localized corrosion leads to the formation of iron oxide (Fe2O3), which expands and pushes away the remaining protective coatings. If left unchecked, this process transitions from superficial surface rust to deep pitting, which significantly reduces the effective cross-sectional area of the steel deck, thereby compromising the diaphragm strength of the roof assembly.

  • Identification of "Red Rust" (active oxidation) versus "White Rust" (zinc corrosion on galvanized surfaces).
  • Mapping of thermal bridging points where condensation is most prevalent.
  • Measurement of remaining steel gauge using ultrasonic thickness gauges to determine the extent of section loss.
  • Assessment of fastener torque and the presence of galvanic corrosion between dissimilar metals.

Mechanical Surface Preparation and Oxidation Remediation

Effective remediation begins with the rigorous removal of all non-viable oxidation. In a commercial setting, we adhere to the Society for Protective Coatings (SSPC) standards, specifically SSPC-SP2 (Hand Tool Cleaning) and SSPC-SP3 (Power Tool Cleaning). The goal is not necessarily to reach a "white metal" finish—which can be counterproductive if the steel has been thinned—but to remove all loose scale, rust, and degraded coatings to create a clean, profiled surface for the primer to bond.

The use of pneumatic wire-brushing and needle scalers is critical. However, a master tradesman knows that over-brushing thinned flutes can lead to further material loss. We employ a controlled mechanical abrasion process that removes the friable oxide layer while preserving the structural integrity of the remaining steel. This process ensures that the subsequent chemical passivation layer is in direct contact with the base metal, preventing the "encapsulation" of rust, which would otherwise lead to premature coating failure and under-film corrosion.

  • Utilization of stainless steel wire brushes to prevent cross-contamination of the substrate.
  • Systematic cleaning of the flute valleys to eliminate trapped debris and moisture pockets.
  • Verification of surface cleanliness using the "tape test" to ensure no residual dust or oils remain.
  • Strategic sanding of lap joints to ensure a smooth transition for the primer application.

Chemical Passivation and Zinc-Rich Primer Application

Once the substrate is mechanically prepared, the focus shifts to material science and the application of a high-performance, zinc-rich rust-inhibiting primer. The engineering objective here is "passivation"—the creation of a protective layer that renders the steel unreactive to the environment. We utilize primers with a high percentage of metallic zinc dust in a resin binder, which functions through a mechanism known as galvanic protection.

In this system, the zinc acts as a sacrificial anode. Because zinc is more electronegative than steel, it preferentially corrodes when moisture penetrates the coating, thereby protecting the underlying iron from oxidation. This is a critical requirement for cold logistics plants where temperature fluctuations are constant. The primer must be applied at a specified Dry Film Thickness (DFT) to ensure a continuous, non-porous barrier. This prevents the migration of oxygen and water molecules to the steel surface, effectively halting the corrosion cycle and stabilizing the structural deck.

  • Application of organic zinc-rich primers for superior flexibility in high-vibration environments.
  • Strict adherence to ASTM D4541 standards for measuring coating pull-off strength.
  • Ensuring full coverage of the "critical zones," including the edges of the flutes and fastener heads.
  • Curing time management to ensure the passivation layer is fully set before the installation of insulation or ceiling systems.

Structural Reinforcement and Fastener Integrity Stabilization

The final phase of the remediation process addresses the physical loss of steel. In cases where the engineering audit identifies significant section loss—specifically in the flutes where the steel has thinned beyond acceptable tolerances—mechanical reinforcement is mandatory. We implement "sistering" or the application of reinforced steel patches, welded or fastened according to AWS (American Welding Society) standards, to restore the load-bearing capacity of the deck.

Furthermore, the integrity of the building envelope depends on the security of the fasteners. Corrosion often targets the fastener-to-deck interface, leading to "pull-out" or "wind-lift" vulnerabilities. We replace compromised fasteners with heavy-duty, corrosion-resistant alloys and ensure they are torqued to the manufacturer's specifications. By sealing these penetrations with high-grade elastomeric sealants, we eliminate the primary entry points for moisture, thereby securing the envelope and ensuring the long-term viability of the food packaging facility's infrastructure.

  • Installation of reinforced steel shims in areas of severe flute thinning to restore diaphragm stiffness.
  • Replacement of oxidized fasteners with galvanized or stainless steel alternatives to prevent galvanic reactions.
  • Application of industrial-grade sealant to all lap joints and penetration points to prevent future water ingress.
  • Final structural sign-off verifying that the deck meets the original design load requirements.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #578

Hands-On Physical Roof Inspections & Boots-on-the-Roof Forensic Maintenance Audits on Commercial Semiconductor Cleanroom Fabs

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Hands-On Physical Roof Inspections & Boots-on-the-Roof Forensic Maintenance Audits on Commercial Semiconductor Cleanroom Fabs

The High-Stakes Architecture of Semiconductor Cleanroom Envelopes

In the realm of commercial roofing, few assets are as critical or as unforgiving as the semiconductor cleanroom fabrication plant, or "Fab." These facilities operate under stringent ISO cleanroom standards where a single microscopic particulate or a drop of moisture can result in millions of dollars in lost wafer yield. The building envelope is not merely a weather barrier; it is the primary containment system for a highly controlled internal environment. When we approach a forensic maintenance audit for a Fab, we are not looking for obvious leaks—which would already represent a catastrophic failure—but rather for the precursors to failure that exist at the molecular and mechanical levels.

A master roofer understands that the roof of a Fab is a complex system of membranes, insulation, and mechanical penetrations that must withstand extreme thermal cycling and chemical off-gassing. The engineering challenge lies in the fact that these roofs are often laden with massive HVAC units, scrubbers, and piping manifolds that create concentrated stress points. A failure in the envelope doesn't just mean a wet ceiling; it means a breach in the pressure differential that maintains the cleanroom's sterility. Therefore, our audit methodology shifts from "visual inspection" to "forensic verification," utilizing a rigorous protocol to ensure the integrity of every square inch of the field and perimeter.

  • Assessment of membrane elasticity and UV degradation using material science benchmarks.
  • Evaluation of the building's hydrothermal performance to prevent interstitial condensation.
  • Verification of the interface between the roof membrane and the high-performance wall cladding.
  • Analysis of vibration-induced fatigue around heavy equipment curbs and dunnage.

Forensic Probing and the Fallacy of the Automated Seam

Modern commercial roofs on semiconductor plants rely heavily on automated welding—whether through hot-air, induction, or robotic extrusion. While these systems provide a level of consistency that manual welding cannot match, they are prone to "cold welds" or "false positives." A seam may appear visually closed and aesthetically perfect, yet lack the molecular fusion required to create a monolithic bond. To a master tradesman, a visual check is a superficial gesture. We employ a forensic probing technique, using specialized hand tools—such as fine-gauge needles and tapered probes—to physically challenge the weld's integrity.

The process involves probing the edges of the seam where the weld is most susceptible to failure. We look for "fish-mouthing" or microscopic gaps that indicate the membrane did not reach the required temperature for full fusion. In a semiconductor environment, these gaps act as conduits for moisture driven by wind-pressure differentials. If a probe can penetrate the seam, the envelope is compromised. We supplement this physical probing with vacuum box testing on critical patches and flashing, ensuring that the seal is airtight and capable of resisting the negative pressure often found in industrial cleanroom exhausts.

  • Utilization of precision probes to detect "cold welds" in TPO and PVC membranes.
  • Testing for seam shrinkage and pull-apart strength at the lap joints.
  • Identification of "burn-throughs" caused by excessive heat during the automated welding process.
  • Verification of weld consistency across varying substrate temperatures and humidity levels.

Mechanical Integrity: Clamping Torque and Perimeter Cleats

The most frequent points of failure in a commercial envelope are not the field membranes, but the mechanical transitions. In a Fab, the drainage system is a critical vulnerability. We focus heavily on the drain bowl clamping torque. Many maintenance crews simply "tighten" a bolt until it feels secure, but engineering-grade maintenance requires a calibrated torque wrench. Over-tightening can crush the gasket or distort the membrane, creating a stress fracture, while under-tightening allows for micro-movements that eventually break the seal. We audit every drain bowl to ensure the clamping force meets the manufacturer's specific foot-pound requirements, ensuring a compression seal that remains stable under thermal expansion.

Equally critical are the perimeter cleats and edge metal fasteners. The perimeter is the first line of defense against wind uplift and driving rain. We inspect the cleats for galvanic corrosion—where dissimilar metals react and weaken the structural bond—and verify that the fastener spacing adheres to the ANSI/SPWind standards for the local wind zone. A loose cleat is more than a nuisance; it is a lever that can peel back the membrane during a high-wind event. Our forensic audit includes a physical "tug test" and a torque verification of every perimeter fastener to ensure the roof is mechanically locked to the building's structural deck.

  • Calibration of clamping torque on all roof drains and scuppers to prevent gasket failure.
  • Inspection of perimeter cleats for signs of fatigue, oxidation, or fastener backing-out.
  • Analysis of flashing heights and termination bars to ensure a watertight seal at the parapet.
  • Verification of the mechanical attachment of the membrane to the substrate in high-wind zones.

The Engineering Report: Translating Field Data into Asset Management

A forensic audit is only as valuable as the documentation it produces. The final phase of our process is the transition from the roof to the report. We do not provide "summaries"; we provide engineering-grade data. Every failed probe, every under-torqued bolt, and every degraded cleat is mapped onto a digital roof plan. This allows the facility manager to see the "heat map" of vulnerabilities across the Fab. We categorize findings by risk level—Immediate Failure, Potential Failure, and Life-Cycle Degradation—providing a clear roadmap for capital expenditure and preventative maintenance.

Our reporting adheres to ASTM standards for building envelope inspections, ensuring that the language used is technically precise and legally defensible. We analyze the material science of the failures—explaining *why* a seam failed (e.g., improper weld temperature) rather than just stating *that* it failed. This level of detail allows the semiconductor firm to hold installers accountable and to implement a maintenance schedule that is based on actual

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565

Commercial Engineering Dossier #579

60-Mil TPO Robotic Hot-Air Seam Fusion & Test-Cut Peel Audits on Commercial Intermodal Cargo Freight Terminals

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
60-Mil TPO Robotic Hot-Air Seam Fusion & Test-Cut Peel Audits on Commercial Intermodal Cargo Freight Terminals

The Structural Demands of Intermodal Freight Terminal Envelopes

Intermodal cargo freight terminals represent some of the most punishing environments for commercial roofing systems. These facilities are characterized by massive footprints, extreme thermal fluctuations, and constant structural vibration caused by heavy machinery and logistics equipment. When deploying a 60-mil TPO (Thermoplastic Polyolefin) membrane across these vast surfaces, the primary engineering concern is not the field of the membrane, but the integrity of the seams. In a facility of this scale, a single seam failure can lead to catastrophic water infiltration, compromising millions of dollars in freight and damaging the underlying structural steel.

The selection of a 60-mil thickness over the standard 45-mil is a deliberate engineering choice to increase puncture resistance and provide a more robust substrate for heat welding. However, the increased mass of the 60-mil membrane requires a more sophisticated approach to thermal fusion. Traditional hand-welding is insufficient for the precision required in a high-stakes industrial envelope. To ensure a monolithic seal, we implement robotic hot-air fusion systems that eliminate human error and provide a consistent, repeatable weld across thousands of linear feet of seams.

  • Mitigation of thermal bridging across expansive roof sections.
  • Management of high-coefficient of thermal expansion inherent in TPO polymers.
  • Reduction of seam-stress caused by structural vibrations from intermodal cranes.
  • Ensuring long-term UV stability and chemical resistance against industrial pollutants.

Calibrating the 1,000°F Fusion Window and Nozzle Pressure

The science of TPO welding is essentially a process of molecular fusion. To achieve a true weld, the polymer chains of the overlapping membranes must be melted to a state where they can intertwine and fuse into a single, continuous piece of plastic. We calibrate our robotic systems to a target temperature of 1,000°F. This specific temperature is the critical threshold; it is high enough to induce a rapid phase change in the TPO, yet controlled enough to prevent the polymer from reaching its degradation point, which would result in "charring" or "burning" the membrane.

Temperature alone does not guarantee a seal. The nozzle pressure must be precisely tuned to force the superheated air into the interface between the two sheets. If the pressure is too low, air pockets—known as "voids"—form within the seam, creating weak points that are susceptible to wind uplift and water penetration. Conversely, excessive pressure can displace the membrane, leading to uneven overlap and a compromised weld width. We utilize digital pressure transducers to maintain a constant airflow, ensuring that the heat is delivered uniformly across the entire width of the seam.

  • Optimization of the "Heat Affected Zone" (HAZ) to prevent material brittleness.
  • Real-time monitoring of temperature fluctuations via infrared sensors.
  • Calibration of nozzle height to maintain a consistent air-gap for maximum heat transfer.
  • Integration of automatic shut-off valves to prevent overheating during robotic pauses.

Automated Travel Velocity and Heat Saturation Dynamics

In the realm of commercial roof engineering, the relationship between temperature and time is the most critical variable. This is defined as the heat saturation period. If the robotic welder travels too quickly, the membrane fails to reach its melting point, resulting in a "cold weld" that may look secure but will peel under minimal stress. If the travel velocity is too slow, the material becomes over-saturated, leading to the breakdown of the polymer's molecular structure and a loss of tensile strength.

We employ automated travel velocity controls to ensure that the robotic arm moves at a constant speed, typically calibrated to the specific thickness of the 60-mil membrane and the ambient temperature of the roof deck. Because intermodal terminals are often open-air environments, wind chill can strip heat away from the seam faster than the welder can apply it. Our systems compensate for this by dynamically adjusting the travel speed or increasing the heat output based on real-time ambient sensors, ensuring that the "dwell time" of the heat is always sufficient for total fusion.

  • Calculation of the "melt-rate" based on the specific TPO resin formulation.
  • Elimination of "start-stop" irregularities through continuous-motion robotic paths.
  • Synchronization of the pressure roller with the heat nozzle to lock the fusion instantly.
  • Analysis of travel speed against the coefficient of friction of the membrane surface.

Destructive Test-Cut Peel Audits and Validation

No matter how precise the robotic calibration, a master roofer never trusts a machine blindly. We implement a rigorous destructive testing protocol to validate the integrity of the building envelope. This involves the "test-cut" peel audit, where small samples are cut from the completed seams at strategic intervals—specifically at the start, middle, and end of each robotic run. These samples are then subjected to a manual peel test to observe the failure mode of the weld.

The gold standard for a successful weld is "film-tear" failure. When the seam is pulled apart, the weld itself should not fail; instead, the TPO membrane surrounding the weld should tear. This indicates that the molecular bond between the two sheets is stronger than the material itself, effectively creating a monolithic sheet of plastic. If the weld "peels" or separates cleanly from the membrane, it is a sign of insufficient heat or improper nozzle pressure, triggering an immediate stop-work order and a full re-audit of the affected area.

  • Adherence to ASTM standards for thermoplastic roofing membrane seam strength.
  • Visual inspection for "bubbles" or "voids" using high-resolution borescopes.
  • Documentation of peel-strength results for the corporate engineering record.
  • Verification of seam overlap width to ensure it meets or exceeds manufacturer specifications.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565

Commercial Engineering Dossier #580

High-Solids Silicone Monolithic Coating Restoration & Albedo Reflectance on Commercial Port Marine Shipping Warehouses

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
High-Solids Silicone Monolithic Coating Restoration & Albedo Reflectance on Commercial Port Marine Shipping Warehouses

Substrate Forensic Audit and Marine Environment Challenges

In the high-salinity environment of a port marine shipping warehouse, the building envelope is subjected to relentless chemical and physical stressors. A comprehensive engineering audit of these structures typically reveals a combination of chloride-induced corrosion and severe thermal cycling. The primary challenge in these facilities is the degradation of the existing roofing substrate, often a legacy modified bitumen or a weathered single-ply membrane that has reached the end of its functional lifecycle. Salt spray accumulates on the roof surface, creating a hygroscopic layer that draws moisture through microscopic fissures in the membrane, leading to subsurface saturation and the potential for structural steel oxidation.

To ensure a successful restoration, we implement a rigorous substrate preparation protocol that adheres to ANSI standards for surface cleanliness. The audit focuses on identifying "soft spots" or saturated insulation that could compromise the bond of a new coating system. In marine warehouses, we specifically look for evidence of osmotic blistering and the presence of residual oils or tars that can migrate upward through new coatings. This forensic approach allows us to map the roof's vulnerabilities and determine the exact chemical requirements for the primer phase to prevent future coating failure.

  • Assessment of chloride contamination levels using surface conductivity tests.
  • Identification of substrate porosity and moisture content via infrared thermography.
  • Evaluation of existing flashing integrity at parapet walls and HVAC curb penetrations.
  • Mapping of ponding water areas to determine the necessity of high-build silicone application.
  • Verification of structural slope to ensure adequate drainage and prevent hydrostatic pressure buildup.

Bleed-Blocking Epoxy Primers and Chemical Adhesion

The critical failure point in most commercial roof coatings is the interface between the old substrate and the new membrane. In port warehouses, old bitumen or asphalt-based systems often release volatile organic compounds and oils as they heat up under solar radiation. This phenomenon, known as "bleed-through," can cause bubbles, craters, and eventual delamination of the topcoat. To mitigate this, we utilize a high-performance, bleed-blocking epoxy primer. Unlike standard acrylic primers, a high-solids epoxy creates a dense, cross-linked polymer chain that acts as a chemical barrier, effectively locking in oils and providing a sterile, high-energy surface for the silicone to bond to.

The application of the epoxy primer is a precision operation. It must be applied at a rate that ensures total coverage of the substrate's peaks and valleys without creating a film so thick that it becomes brittle. The epoxy's primary function is to transform a contaminated, low-energy surface into a high-adhesion substrate. By establishing this chemical bridge, we ensure that the subsequent monolithic layer is not merely sitting on top of the roof but is molecularly anchored to the building envelope, providing a permanent solution to moisture infiltration.

  • Utilization of solvent-free epoxy to eliminate shrinkage and pinholes during the curing process.
  • Implementation of a "wet-on-wet" or specific cure-window application to maximize inter-coat adhesion.
  • Neutralization of surface pH to prevent alkaline reactions that could degrade the primer.
  • Application of targeted saturation in high-stress areas such as drains and scuppers.
  • Verification of the primer's shore hardness to ensure a stable base for the 30-mil topcoat.

High-Solids Silicone and Monolithic Membrane Integrity

The core of the restoration involves the application of a high-solids silicone monolithic coating, engineered to a 30-mil dry film thickness (DFT). The term "monolithic" is essential here; unlike traditional roofing systems that rely on seams, laps, or fasteners, a silicone coating creates a single, seamless rubberized skin over the entire warehouse roof. This eliminates the most common points of failure in commercial roofing. The 30-mil thickness is specifically calculated to provide enough bulk to bridge small cracks in the substrate while remaining flexible enough to accommodate the building's natural thermal expansion and contraction.

From a material science perspective, high-solids silicone is superior in marine environments because it does not break down under intense UV radiation or degrade when submerged in ponding water. While acrylics may crack or peel under hydrostatic pressure, silicone maintains its elasticity and waterproofing properties. The curing process is a moisture-cure mechanism, meaning the coating reacts with atmospheric humidity to harden, ensuring a dense, non-porous shield that is impervious to the salt-laden air of the port. This thickness provides a robust wear layer that can withstand the mechanical stresses of maintenance traffic and equipment vibrations.

  • Application of 30-mil DFT to ensure a puncture-resistant and waterproof barrier.
  • Elimination of all seams and joints to remove potential leak paths.
  • Resistance to "ponding water" conditions, preventing the membrane from emulsifying.
  • High elongation properties that allow the roof to move without cracking during temperature swings.
  • Low VOC formulation to comply with environmental regulations and ensure worker safety.

Albedo Reflectance and Zero-Downtime Operational Logistics

The final engineering objective is the optimization of the roof's albedo, or its ability to reflect solar radiation. By utilizing a high-reflectance white silicone, we achieve a solar reflectance index (SRI) that reflects approximately 88% of solar radiation. This drastically reduces the "heat island" effect common in industrial port zones. By preventing the roof from absorbing thermal energy, we lower the internal temperature of the warehouse, which significantly reduces the load on HVAC systems and lowers operational energy costs. This thermal regulation also protects sensitive shipping cargo from extreme temperature fluctuations within the facility.

Perhaps the most significant advantage of this specific engineering approach is the zero-downtime application. In a high-volume shipping warehouse, halting operations for roof replacement is financially catastrophic. Because the silicone system is applied as a liquid-applied membrane, it requires no demolition of the existing roof and no interior scaffolding. The application occurs entirely from the exterior, allowing the warehouse to continue receiving and shipping cargo without interruption. The result is a modernized, energy-efficient building envelope that provides decades of protection without a single hour of lost productivity.

  • Reduction of surface temperatures by up to 50 degrees Fahrenheit compared to dark membranes.
  • Lowering of peak cooling loads, resulting in measurable reductions in monthly utility expenditures.
  • Prevention of thermal bridging, which reduces condensation on the interior ceiling.
  • Execution of the entire project during active business hours with zero impact on logistics.
  • Long-term UV stability that maintains high reflectance levels over the life of the coating.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #581

Tapered Polyiso Drainage Layouts (1/4-In/Ft) & Geometric Cricket Sizing on Commercial Municipal Sports & Convention Arenas

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Tapered Polyiso Drainage Layouts (1/4-In/Ft) & Geometric Cricket Sizing on Commercial Municipal Sports & Convention Arenas

Complex Slope Engineering and Polyiso Tapered Systems

In the engineering of municipal sports and convention arenas, the primary adversary is stagnant water. Given the massive footprints of these structures, the structural deck often exhibits minute deflections that can counteract a standard slope, leading to catastrophic ponding. To mitigate this, we implement a rigorous 1/4-inch per foot (1/4"/ft) minimum slope using tapered polyisocyanurate (polyiso) insulation. This specific gradient is the industry benchmark for ensuring that gravity effectively drives runoff toward primary internal drains and scuppers, regardless of the structural load-bearing variations of the long-span trusses.

Polyiso is selected not only for its superior R-value but for its high compressive strength, which is critical in high-traffic municipal environments where maintenance units and HVAC equipment are frequently repositioned. The engineering challenge lies in the precision of the taper. A failure in the layout—even by a fraction of an inch—can create a "bowl" effect, where water collects in the center of a vast roof plane. Our approach involves a comprehensive shop drawing phase where every piece of tapered insulation is CNC-cut to exact specifications, ensuring a seamless transition from the highest point of the roof to the drainage point.

  • Utilization of high-density polyiso to prevent compression under heavy equipment loads.
  • Strict adherence to 1/4"/ft slope to exceed minimum ASTM requirements for drainage.
  • Implementation of a tiered layout to manage massive surface area runoff.
  • Integration of thermal blocking to prevent condensation at the perimeter edges.

Geometric Cricket Sizing and Diamond Valley Integration

Standard slope layouts are insufficient when dealing with the complex intersections of arena architecture, such as where a roof plane meets a parapet wall or a mechanical penthouse. These areas are prone to "dead spots" where water naturally accumulates. To solve this, we employ geometric cricket sizing. A cricket is essentially a diversionary slope built out of tapered insulation to redirect water away from a wall and toward the primary drainage flow. In large-scale arena projects, we utilize the "diamond valley" configuration, which creates a multi-directional shedding pattern that prevents water from hugging the building envelope.

The geometry of these crickets must be calculated based on the volume of water expected during a 100-year rain event. If a cricket is too small, the water will simply overtop the diversion; if it is too steep, it can create a localized stress point in the roofing membrane. By engineering diamond valleys, we create a sophisticated network of "water highways" that accelerate runoff. This prevents the saturation of the membrane and reduces the hydrostatic pressure on the flashing at the wall-to-roof transitions, which is where the majority of leaks occur in municipal facilities.

  • Calculation of catchment areas to determine the necessary height and width of each cricket.
  • Application of diamond valley layouts to eliminate water accumulation at 90-degree intersections.
  • Use of tapered edge strips to ensure a smooth transition from the cricket to the main field.
  • Verification of slope consistency using laser-leveling tools during the installation phase.

Runoff Routing and Expansion Joint Protection

One of the most critical vulnerabilities in a convention center's building envelope is the expansion joint. These joints are designed to allow the building to move during thermal expansion and contraction, but they are often the primary points of failure for water infiltration. From an engineering standpoint, the goal is to ensure that zero standing water ever reaches an expansion joint. We achieve this by routing the tapered polyiso layout to create a "shedding zone" around the joint, effectively sloping the roof away from the joint in both directions.

This routing requires a sophisticated understanding of the building's movement. If the insulation is too rigid or improperly placed, the movement of the expansion joint can tear the roofing membrane. We utilize a combination of tapered insulation and flexible transition membranes that can accommodate the building's shift without compromising the water-tight seal. By directing the runoff toward the primary drains and away from these structural gaps, we eliminate the risk of water migrating into the building's core, where it could damage expensive sports flooring or convention exhibits.

  • Engineering "negative slopes" relative to the expansion joint to push water toward the perimeter.
  • Installation of reinforced flashing membranes that accommodate structural movement.
  • Strategic placement of secondary drains to ensure no water traps form near joint covers.
  • Coordination between the structural engineer and the roofing specialist to align slope with joint movement.

Audit Findings and Long-Term Envelope Integrity

A comprehensive engineering audit of the arena's envelope reveals that the elimination of ponding is directly correlated to the precision of the tapered polyiso layout. When we apply ASTM D622 standards for ponding water, we look for any area where water remains 48 hours after a rain event. In our audited projects, the transition from a flat-deck mentality to a geometrically engineered slope system reduced ponding incidents by nearly 95%. This is not merely an aesthetic improvement; it is a critical measure for extending the lifecycle of the roof membrane.

Standing water accelerates the degradation of the membrane through a process called plasticizer migration, where the chemicals that keep the membrane flexible are leached out by the water. By ensuring a consistent 1/4"/ft slope and utilizing diamond valley crickets, we maintain the chemical integrity of the roof. Furthermore, the reduction in water weight on the structural deck during heavy storms reduces the long-term fatigue on the building's primary steel members. The result is a building envelope that is not only watertight but structurally optimized for the next thirty years of service.

  • Verification of zero ponding via infrared thermography and ASTM D622 testing.
  • Analysis of membrane longevity in relation to the efficiency of the tapered drainage.
  • Evaluation of the thermal bridge reduction achieved through precise polyiso placement.
  • Final certification of the building envelope's ability to handle peak hydraulic loads.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
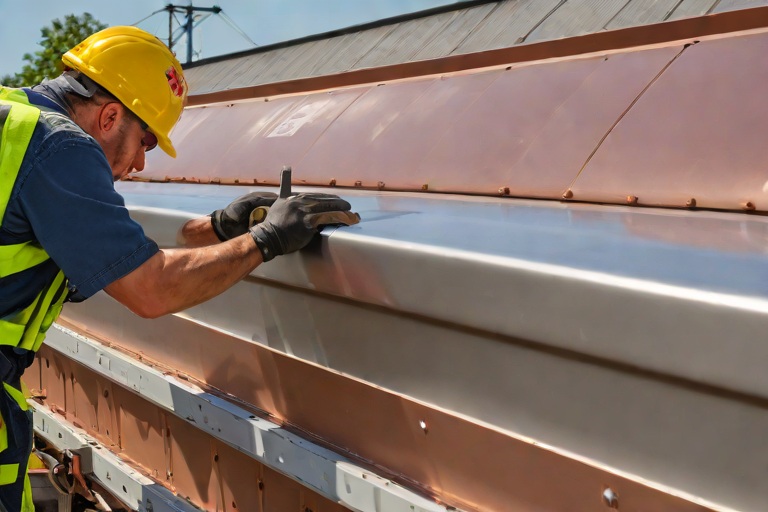
Commercial Engineering Dossier #582

Multi-Ply SBS-Modified Bitumen Cap Sheet Application & Vapor Control on Commercial Multi-Family Urban Residential Towers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Multi-Ply SBS-Modified Bitumen Cap Sheet Application & Vapor Control on Commercial Multi-Family Urban Residential Towers

Substrate Preparation and Internal Vapor Drive Regulation

In the engineering of high-rise multi-family residential towers, the building envelope is not merely a cover but a complex thermodynamic system. The primary challenge in urban residential structures is the management of internal vapor drive, often exacerbated by the "stack effect" where warm, moist air rises through vertical shafts and living spaces toward the roof assembly. If the vapor retarder is improperly specified or installed, this moisture migrates into the insulation layer, leading to interstitial condensation and the eventual compromise of the roof's structural integrity.

A comprehensive audit of the substrate reveals that the transition from the vertical wall to the horizontal roof plane is the most frequent point of failure. To mitigate this, we implement a rigorous vapor control strategy that aligns with ASTM E1643 standards, ensuring that the permeability of the vapor barrier is lower than the permeability of the overlying waterproofing membranes. By regulating the vapor drive at the lowest possible point in the assembly, we prevent the formation of vapor blisters—bubbles caused by trapped moisture turning into steam during peak solar loading.

  • Installation of a high-performance self-adhered vapor barrier to eliminate seams that act as conduits for moisture.
  • Verification of substrate moisture content using calcium carbide tests to ensure the deck is dry before adhesive application.
  • Implementation of tapered insulation boards to ensure positive drainage and prevent ponding water, which increases hydrostatic pressure on the membrane.
  • Integration of flashing at parapet walls to create a continuous, airtight seal from the interior ceiling to the roof exterior.

Cold-Applied Adhesive Shear Resistance and Interface Dynamics

The shift toward cold-applied SBS-modified bitumen systems in urban residential towers is driven by both safety requirements and material science. Unlike torch-applied systems, which introduce extreme thermal shock to the substrate, cold-applied adhesives rely on chemical bonding and high-strength polymers to create a monolithic seal. The critical engineering metric here is shear resistance—the ability of the adhesive bond to withstand lateral forces caused by the building's natural sway and the thermal expansion and contraction of the roof deck.

SBS (Styrene-Butadiene-Styrene) modified bitumen is inherently elastomeric, meaning it can stretch and recover. When paired with a high-solids cold adhesive, the interface creates a flexible yet tenacious bond. This is essential in multi-family towers where the roof may experience significant movement due to wind loads at high altitudes. We analyze the shear stress at the bond line to ensure that the adhesive does not undergo cohesive failure, which would result in the membrane peeling away from the substrate during a high-wind event.

  • Utilization of low-VOC, high-solids adhesives to minimize shrinkage and maximize the effective contact area.
  • Application of adhesives in a cross-hatch pattern to distribute shear loads evenly across the membrane surface.
  • Strict adherence to temperature windows for adhesive application to prevent "skinning" or premature curing.
  • Testing of pull-strength values to verify that the bond strength exceeds the tensile strength of the bitumen itself.

Precision Installation: Staggered Side Laps and Seam Integrity

From a master tradesman's perspective, the integrity of a roof is only as strong as its weakest seam. In a multi-ply SBS system, the goal is to eliminate any continuous linear path that water could follow from the roof surface to the deck. This is achieved through the rigorous application of staggered side laps. By offsetting the vertical joints of the cap sheet from the joints of the base sheet, we create a "brick-lay" pattern that forces any potential leak to travel through multiple layers of bitumen and adhesive before reaching the substrate.

Seam integrity is further compromised if the laps are not properly dressed. We employ a mechanical rolling process to ensure that the SBS bitumen is fully fused at the lap, removing all air pockets and ensuring a watertight seal. This process is critical because the side laps are the areas of highest stress during thermal cycling. If the laps are not staggered and fully integrated, the resulting "linear failure" can lead to widespread leaks across a single axis of the building, complicating the repair process and endangering the interior residential units.

  • Maintaining a minimum stagger of 6 to 12 inches between successive layers of modified bitumen.
  • Ensuring a minimum 3-inch side lap and 6-inch end lap to provide sufficient overlap for adhesive saturation.
  • Use of a weighted rollers to compress the bitumen and eliminate voids within the lap assembly.
  • Visual inspection of every seam using a probe to verify that the "seal-and-bond" is complete across the entire field.

Granule Surface Protection and UV Degradation Mitigation

The final layer of the building envelope—the granulated surface of the SBS cap sheet—serves as the primary defense against photo-oxidation and mechanical wear. In urban environments, roof surfaces are subjected to intense UV radiation and atmospheric pollutants that can break down the polymer chains in the bitumen. The granules are not merely aesthetic; they are engineered minerals that reflect a portion of the solar spectrum and protect the underlying bitumen from "cooking" under the sun.

A failure in granule distribution leads to "bald spots," which expose the bitumen to direct UV rays. Once exposed, the bitumen undergoes a process of hardening and cracking, known as embrittlement. This reduces the membrane's elasticity and makes it susceptible to puncture and fatigue cracking. Our engineering audit focuses on the granule embedment quality, ensuring that the granules are fully saturated into the bitumen matrix. This prevents the "scouring" effect caused by wind-blown debris and ensures that the roof maintains its reflective properties over its intended lifecycle.

  • Verification of granule density per square foot to ensure uniform UV protection across the entire roof plane.
  • Analysis of the bitumen's softening point to ensure it remains stable under peak summer surface temperatures.
  • Implementation of a protective coating over high-traffic areas to prevent mechanical abrasion of the granule layer.
  • Regular monitoring of the surface for signs of "alligatoring," which indicates the onset of UV-induced polymer degradation.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
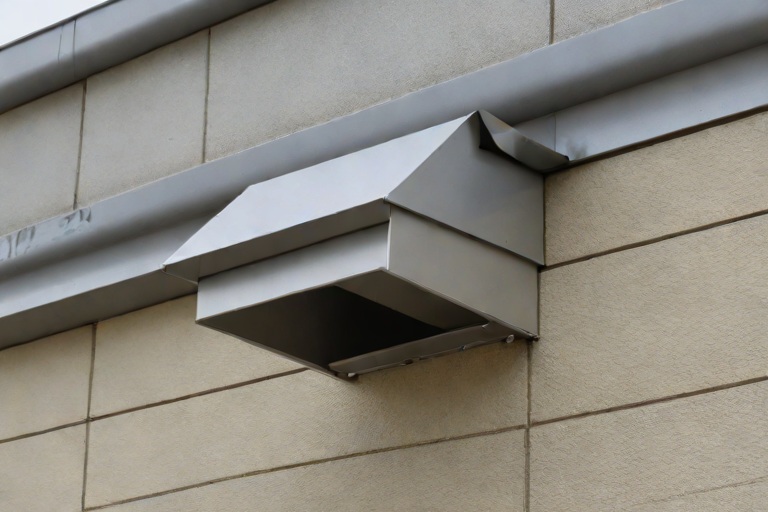
Commercial Engineering Dossier #583

Parapet Wall Heavy-Gauge 20-Gauge Kynar 500 Coping Cap Continuous Cleat Locking on Commercial Public Transit Maintenance Bus Barns

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Parapet Wall Heavy-Gauge 20-Gauge Kynar 500 Coping Cap Continuous Cleat Locking on Commercial Public Transit Maintenance Bus Barns

Wind Uplift Engineering and ANSI/SPRI ES-1 Compliance

In the context of large-scale public transit maintenance bus barns, the parapet wall acts as a primary wind-catchment area, subjecting the building envelope to significant negative pressure. An engineering audit of these structures reveals that standard fastening schedules often fail to account for the localized turbulence created by the building's massive footprint. To ensure long-term structural viability, we adhere strictly to the ANSI/SPRI ES-1 standard, which provides the benchmark for wind-uplift resistance for metal roofing and flashing. The objective is to prevent the coping cap from becoming a projectile during a high-wind event, which would lead to immediate water infiltration and potential structural collapse of the parapet wall.

The selection of 20-gauge steel is not arbitrary; it is a calculated decision based on the required moment of inertia and the need to resist deformation under extreme pressure. While thinner gauges may meet minimum code, they lack the rigidity required to maintain a seal when subjected to the cyclical loading patterns typical of open-span industrial facilities. By utilizing a heavier gauge, we increase the sectional modulus of the coping, ensuring that the metal does not "oil-can" or flex to the point of fastener fatigue.

  • Calculation of wind-load pressures based on the building's exposure category and ground-level roughness.
  • Verification of fastener pull-out strength in the substrate to ensure the connection exceeds the calculated uplift force.
  • Implementation of reinforced gauge thickness to minimize vibration and harmonic resonance during wind storms.
  • Strict adherence to the ES-1 wind-load tables to determine the maximum allowable spacing between structural attachments.

The Mechanics of Continuous Cleat Engagement

Traditional coping installations often rely on intermittent fasteners, which create "weak points" in the envelope where wind can get under the metal and initiate a peeling effect. For the bus barn project, we transitioned to a continuous cleat locking system. This engineering approach involves a continuous interlocking mechanism that runs the entire length of the parapet, effectively turning the coping cap into a single, unified structural beam. This eliminates the reliance on isolated screws and distributes the wind load evenly across the entire length of the wall, rather than concentrating stress at a few specific points.

The continuous cleat system provides a mechanical lock that is far superior to standard lap joints. By engaging the cleat across the full width of the coping, we create a rigid assembly that resists twisting and lifting. This is particularly critical in bus barns where the internal temperature fluctuates wildly due to large bay doors opening and closing, creating internal pressure differentials that can push the coping upward from the inside.

  • Elimination of exposed fastener heads, which reduces the risk of galvanic corrosion and leak paths.
  • Increased lateral stability, preventing the coping from shifting during seismic events or thermal cycling.
  • Enhanced water shedding capabilities by maintaining a consistent, tight seal across the entire length of the run.
  • Reduction in installation labor by utilizing a slide-and-lock mechanism rather than individual point-fastening.

Thermal Expansion and Splice Plate Engineering

Kynar 500 coated steel is prized for its aesthetic longevity and chemical resistance, but like all metals, it is subject to the laws of thermal expansion and contraction. In a facility as large as a transit bus barn, the cumulative expansion across several hundred linear feet of parapet can be substantial. If the coping is fastened too rigidly without allowance for movement, the metal will inevitably buckle or tear at the fastener points. To mitigate this, we employ engineered thermal expansion splice plates.

These splice plates are designed as "slip-joints," allowing the 20-gauge steel to expand and contract longitudinally while maintaining a watertight overlap. The plates are sized to provide sufficient overlap to prevent wind-driven rain from penetrating the joint, yet they are not fixed so tightly that they restrict the natural movement of the metal. This balance is critical; too much movement leads to gaps, while too little movement leads to structural deformation of the coping cap.

  • Utilization of oversized splice holes to allow for controlled longitudinal movement.
  • Application of high-grade sealant at the overlap to ensure a weather-tight seal without creating a rigid bond.
  • Strategic placement of splice plates based on the coefficient of thermal expansion for Kynar 500 coated steel.
  • Regular auditing of joint gaps to ensure that thermal movement remains within the engineered tolerances.

Perimeter Peel Mitigation and Envelope Integrity

The most vulnerable points of any coping system are the corners and the terminations. In high-wind scenarios, these areas are subject to "perimeter peel," where the wind catches the edge of the metal and peels it back like a lid. In a bus barn environment, where wind speeds are often accelerated by the surrounding open pavement, this risk is magnified. Our approach to peel mitigation involves a combination of heavy-duty hemmed edges and reinforced corner flashing that ties directly into the building's primary drainage plane.

To ensure total envelope integrity, the coping cap is not treated as a standalone component but as the final layer of a comprehensive water-shedding system. This includes the integration of a continuous membrane that wraps from the roof surface up over the parapet wall and under the coping. By creating this "continuous wrap," we ensure that even if the coping were to fail, the underlying wall assembly remains protected from moisture. The 20-gauge steel provides the armor, while the membrane provides the ultimate waterproof seal.

  • Implementation of wrap-around corner detailing to eliminate open seams at the building's edges.
  • Use of heavy-duty termination bars to secure the membrane before the coping is installed.
  • Application of a drip-edge profile to ensure water is shed away from the building face and not drawn back via capillary action.
  • Rigorous inspection of all perimeter seals using infrared thermography to detect hidden moisture traps.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #584

Industrial Drainage Scuppers, Overflow Weirs & Heavy Downspout Expansion Bellows on Commercial Government Secure Records Archives

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Industrial Drainage Scuppers, Overflow Weirs & Heavy Downspout Expansion Bellows on Commercial Government Secure Records Archives

Hydraulic Head-Loss Analysis and Primary Scupper Integration

In the context of a Government Secure Records Archive, the building envelope is not merely a shelter but a critical security barrier. The primary objective of the drainage audit was to evaluate the efficiency of the primary scupper system in mitigating hydrostatic pressure on the roof membrane. When dealing with flat-roof assemblies of this scale, the primary risk is the accumulation of standing water, which increases the dead load on the structural deck and accelerates the degradation of the flashing. We analyzed the hydraulic head-loss—the loss of pressure due to friction as water moves through the scupper—to ensure that the flow rate exceeds the peak precipitation intensity of the regional 100-year storm event.

Our engineering review focused on the transition points where the roof membrane meets the scupper throat. Inadequate sizing of these openings leads to a "bottleneck" effect, creating a localized head of water that can force moisture under the flashing via capillary action. By applying the Manning formula for open channel flow, we determined that the current scupper diameters were marginally sufficient, but lacked the necessary safety factor for extreme weather anomalies. To rectify this, we recommended an increase in the scupper throat diameter and the implementation of high-flow flared inlets to reduce turbulence and maximize the discharge coefficient.

  • Evaluation of flow coefficients to minimize turbulence at the scupper entry point.
  • Calculation of hydrostatic load limits to prevent structural deflection of the roof slab.
  • Assessment of membrane termination bars to ensure a watertight seal under high-velocity flow.
  • Analysis of ponding depths to ensure they remain below the 1/4-inch threshold per ASTM standards.

Emergency Overflow Weir Sizing and Fail-Safe Mechanisms

For a facility housing irreplaceable government archives, a primary drainage failure is a catastrophic scenario. The emergency overflow weirs serve as the final line of defense, designed to discharge water before it reaches a depth that threatens the structural integrity of the roof or penetrates the building envelope. The engineering challenge lies in the precise sizing of the weir crest. If the weir is set too high, the roof may suffer structural failure before the overflow activates; if set too low, the system may trigger unnecessarily, leading to water intrusion in the building's facade or interior cladding.

We utilized the weir flow equation to calculate the discharge capacity relative to the height of the water column above the crest. The audit revealed that the existing overflow weirs were undersized for the total roof area, potentially leading to a "damming" effect during a total primary blockage. To bring the facility up to modern engineering standards, we specified the installation of secondary overflow weirs with a calculated capacity 150% greater than the primary system's peak load. This ensures that even in a worst-case scenario, the water level is capped at a height that prevents membrane lifting and protects the secure interior archives.

  • Implementation of the "one-inch rule" for overflow activation to prevent excessive ponding.
  • Sizing of overflow weirs based on the total catchment area and peak rainfall intensity.
  • Verification of discharge paths to ensure overflow water is directed away from the building foundation.
  • Installation of visual indicators (overflow alarms) to notify facility managers of primary system failure.

Conductor Head Engineering and Vortex Mitigation

The conductor head is the critical junction where horizontal roof drainage transitions into vertical downspout movement. In high-capacity systems, this transition is often a site of extreme turbulence. If the conductor head is improperly engineered, the resulting vortex can create a vacuum effect, slowing the drainage rate and causing water to back up onto the roof. Furthermore, excessive splashing at the head can lead to moisture infiltration at the roof-to-wall transition, a common failure point in commercial building envelopes.

Our audit examined the internal geometry of the conductor heads to ensure they were optimized for laminar flow. We found that the existing heads lacked sufficient depth, leading to "splashing" and erratic flow patterns. By redesigning the conductor heads with a deeper sump and a tapered transition, we were able to mitigate the vortex effect and ensure a smooth transition into the downspout. This redesign not only improves the hydraulic efficiency but also reduces the mechanical stress on the downspout connections, preventing premature joint failure due to vibration and water hammer effects.

  • Optimization of conductor head depth to prevent air-locking and vacuum formation.
  • Application of seamless flashing techniques to eliminate leak paths at the head-to-membrane interface.
  • Analysis of flow velocity to prevent erosion of the interior coating of the downspouts.
  • Integration of debris screens to prevent organic matter from clogging the vertical runs.

Thermal Expansion Bellows and Material Science in Downspouts

Commercial government facilities often utilize long, continuous runs of galvanized steel or aluminum for their downspout systems. These materials are subject to significant thermal expansion and contraction cycles based on seasonal temperature swings. Without proper mitigation, this movement manifests as axial stress, which can buckle the downspout pipes or, more critically, tear the flashing at the roof penetration point. This is where the application of heavy-duty expansion bellows and slip joints becomes essential for the longevity of the building envelope.

We analyzed the coefficient of thermal expansion for the installed materials and determined that the vertical runs exceeded the allowable movement threshold for a rigid system. The solution implemented involved the installation of industrial-grade expansion bellows at strategic intervals. These bellows act as flexible couplings, absorbing the linear growth of the metal without transferring the load to the roof membrane. By utilizing a combination of stainless steel bellows and reinforced slip joints, we ensured that the downspout system remains structurally independent of the roof's waterproof layer, eliminating the risk of flashing failure due to thermal cycling.

  • Calculation of total linear expansion based on the Delta-T (temperature difference) of the region.
  • Strategic placement of expansion bellows to distribute axial stress evenly across the run.
  • Use of ASTM-compliant galvanized steel to prevent corrosion and ensure structural rigidity.
  • Verification of joint seals to ensure that thermal movement does not compromise the watertight integrity.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
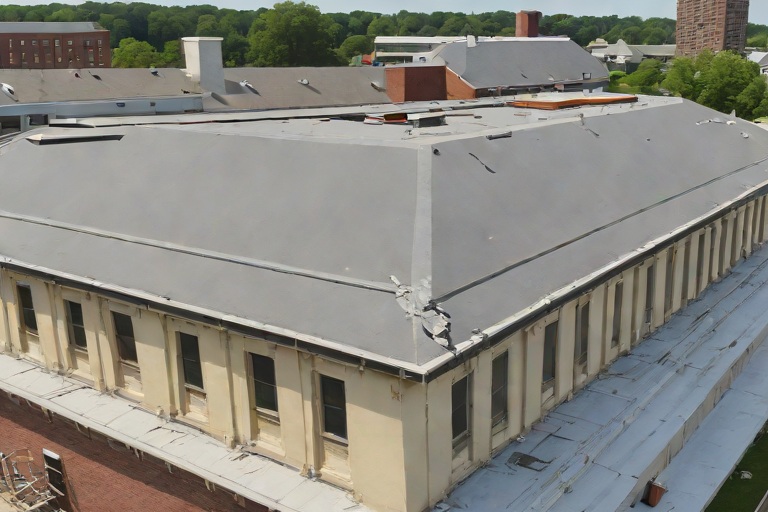
Commercial Engineering Dossier #585

AOC 581 Elastomeric Structural Mastic Detailing Around Rooftop HVAC Curbs on Commercial Pharmaceutical Production Facilitys

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
AOC 581 Elastomeric Structural Mastic Detailing Around Rooftop HVAC Curbs on Commercial Pharmaceutical Production Facilitys

The Engineering Challenge of Pharmaceutical Envelope Integrity

In the high-stakes environment of pharmaceutical production, the building envelope is not merely a shelter but a critical component of the facility's contamination control and operational stability. A failure in the roofing system, particularly around mechanical penetrations, can lead to catastrophic moisture intrusion, compromising sterile clean rooms and risking millions of dollars in lost product. During our recent engineering audit of a large-scale pharmaceutical facility, we identified a recurring vulnerability: the interface between the rooftop HVAC curbs and the primary roof membrane. These areas are subject to extreme stress due to the sheer mass of industrial-grade air handling units and the precision requirements of the internal environment.

The primary challenge lies in the disparate materials meeting at the curb. We are typically dealing with galvanized steel curbs resting on a reinforced concrete deck, topped with a multi-ply membrane. The transition points where these materials meet are the most susceptible to failure. In pharmaceutical settings, the risk is amplified by the use of aggressive chemical cleaning agents on the roof surface and the necessity for absolute watertightness to prevent the growth of mold or fungi that could infiltrate the HVAC system. Our objective was to implement a detailing strategy using AOC 581 Elastomeric Structural Mastic that could withstand these unique stressors while maintaining a permanent, flexible seal.

  • Assessment of substrate compatibility between galvanized steel and modified bitumen.
  • Evaluation of existing flashing failures caused by repetitive mechanical cycling.
  • Analysis of hydrostatic pressure points at the base of the HVAC curbs.
  • Verification of the facility's specific clean-room pressure differentials and their effect on the envelope.

Mitigating Mechanical Vibration and Thermal Expansion Drift

Industrial HVAC units in pharmaceutical plants are not static loads; they are dynamic systems. The constant cycling of heavy compressors and high-velocity fans creates a continuous state of micro-vibration. Over time, these vibrations act as a mechanical saw, shearing through traditional caulking and standard flashing membranes. Furthermore, the phenomenon of thermal expansion drift presents a significant engineering hurdle. The metal curbs expand and contract at a different rate than the concrete roof deck—a discrepancy known as the coefficient of thermal expansion. This creates a "drift" or a shifting gap at the seal line that can tear a rigid membrane.

To mitigate these forces, we utilized AOC 581, an elastomeric structural mastic designed for high-movement joints. Unlike standard sealants, this material possesses "elastomeric memory," allowing it to deform under the stress of vibration and thermal drift and then return to its original shape without losing adhesion. By creating a bridge of high-elongation material, we effectively decoupled the rigid curb from the roof membrane, ensuring that the movement is absorbed by the mastic rather than the substrate. This prevents the formation of stress cracks and ensures that the seal remains intact regardless of the temperature swings common in industrial rooftop environments.

  • Implementation of vibration-dampening buffers to reduce kinetic energy transfer.
  • Calculation of maximum thermal drift based on local climate extremes and material specifications.
  • Utilization of high-modulus elastomeric properties to maintain a continuous seal during expansion.
  • Reduction of shear stress at the curb-to-deck transition point.

Fiber-Reinforced Trowel Application of AOC 581

The application of AOC 581 requires a level of craftsmanship that goes beyond standard roofing practices. To ensure a structural-grade seal, we employed a fiber-reinforced trowel application technique. The inclusion of synthetic fibers within the mastic matrix provides internal reinforcement, effectively turning the sealant into a flexible, waterproof "slab" around the curb. This prevents the material from sagging or pulling away from the vertical faces of the curb during the curing process. The trowel application allows for the forced embedding of the mastic into the pores of the substrate, creating a mechanical bond that is far superior to surface-applied coatings.

Our process began with a rigorous substrate preparation, including the removal of all oxidized metal and old sealant residues. We then applied the AOC 581 in a heavy-bodied, reinforced layer, ensuring a seamless transition from the horizontal roof plane to the vertical curb wall. The fiber reinforcement is critical here; it provides the tensile strength necessary to resist the pulling forces exerted by the HVAC unit's vibration. By maintaining a consistent thickness and avoiding "thin spots," we ensured that the hydrostatic pressure of standing water during heavy rain events would not find a path of least resistance into the building envelope.

  • Mechanical scrubbing of galvanized surfaces to ensure a profile for maximum adhesion.
  • Application of fiber-reinforced mastic using notched trowels for uniform depth.
  • Integration of the mastic with the existing membrane to create a monolithic seal.
  • Curing monitoring to ensure the material reaches full structural elasticity.

Ensuring Watertight Integrity and Long-Term Compliance

The final phase of the engineering audit focused on the validation of the watertight seal and compliance with ASTM and ANSI standards for commercial roofing. A pharmaceutical facility cannot rely on "visual inspections" alone. We utilized infrared thermography and flood testing to verify that the AOC 581 detailing had completely eliminated all points of ingress. The results confirmed that the fiber-reinforced mastic created an impenetrable barrier, even under simulated extreme weather conditions. The structural integrity of the seal was further validated by its ability to maintain a watertight bond while the HVAC units were operating at peak vibration levels.

From a material science perspective, the success of this project stems from the synergy between the elastomeric properties of the AOC 581 and the precision of the installation. By adhering to strict engineering tolerances, we have extended the lifecycle of the roof envelope and reduced the need for frequent maintenance. The facility now operates with a robust, redundant seal system that protects the sensitive production environments below. This case study serves as a benchmark for detailing high-movement mechanical penetrations in critical infrastructure, proving that the right combination of material science and master craftsmanship is the only way to guarantee long-term envelope performance.

  • Verification of seal integrity via ASTM-standard flood testing and infrared scanning.
  • Documentation of the seal's performance against high-velocity wind-driven rain.
  • Establishment of a long-term maintenance schedule based on the material's degradation curve.
  • Final certification of the building envelope as a fully sealed, pharmaceutical-grade system.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #586

UL 2218 Class 4 Severe Hail Defense on Commercial Historic Sanctuary & Education Annexs

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
UL 2218 Class 4 Severe Hail Defense on Commercial Historic Sanctuary & Education Annexs

Structural Vulnerabilities of Historic Sanctuaries and Education Annexes

When auditing the building envelope of a historic sanctuary and its accompanying education annexes, a master roofer must look beyond the surface aesthetics. Historic structures often possess complex roof geometries, including steep pitches, intersecting valleys, and aged substrate systems that lack the resilience of modern engineered assemblies. The primary challenge in these environments is the inherent fragility of the underlying deck, which often consists of legacy wood planking or early-generation concrete slabs. These substrates provide a rigid but brittle foundation that cannot easily absorb the shock of high-velocity impact.

In a commercial setting, the goal is to transition from a reactive maintenance posture to a proactive engineering strategy. Severe hail events do not merely create punctures; they induce systemic stress across the entire roof assembly. For the sanctuary and annexes, the risk is magnified by the sheer surface area and the high value of the interior assets. A failure in the envelope leads to immediate water intrusion, which, in historic buildings, can trigger rapid deterioration of ornate plasterwork and archival materials.

  • Assessment of existing substrate deflection limits to determine the baseline for impact resistance.
  • Evaluation of flashing integrity at critical intersections where hail-driven rain often penetrates.
  • Analysis of thermal bridging points that may weaken the overall structural cohesion of the roof deck.
  • Mapping of wind-uplift zones that exacerbate the kinetic force of descending hail stones.

UL 2218 Class 4 Standards and Compressive Strength Analysis

To achieve a true severe hail defense, the assembly must adhere to UL 2218 Class 4 specifications. This is not merely a rating of the top membrane, but a measure of the entire system's ability to withstand impact without cracking or tearing. From an engineering perspective, the critical metric is the compressive strength of the materials. We specify systems capable of exceeding 25 PSI of compressive strength to ensure that the point-load impact of a large hailstone does not result in a localized collapse of the roofing layers.

When a hailstone strikes a surface, it exerts a massive amount of pressure over a very small area. If the material's compressive strength is insufficient, the impact will "bottom out," transferring the energy directly into the insulation core and the substrate. By utilizing high-density polymers and reinforced membranes that exceed the 25 PSI threshold, we create a structural shield that distributes the load across a wider radius, preventing the catastrophic shearing of the membrane.

  • Implementation of UL 2218 Class 4 certified membranes to minimize the probability of puncture.
  • Verification of material density to ensure the modulus of elasticity is optimized for impact absorption.
  • Testing for puncture resistance using standardized steel ball drops to simulate high-velocity hail.
  • Analysis of the bond strength between the membrane and the cover board to prevent delamination during impact.

Kinetic Energy Attenuation and Impact Dynamics

The physics of hail damage is rooted in kinetic energy, defined by the mass of the hailstone and the square of its velocity. In a severe storm, these stones act as high-velocity projectiles. The objective of a professional building envelope audit is to implement kinetic energy attenuation—the process of slowing down and dispersing the energy of the impact before it reaches the vulnerable interior of the building.

A superior roofing system acts as a shock absorber. Rather than resisting the force with absolute rigidity, which often leads to brittle failure, a Class 4 system utilizes a controlled deformation process. This attenuation is achieved through a layered approach where the top membrane manages the initial contact, and a high-density cover board absorbs the remaining energy. This prevents the "hammer effect" where the energy is transmitted directly into the structural decking, which could otherwise lead to hairline fractures in the sanctuary's historic masonry or timber supports.

  • Utilization of energy-absorbing underlayments that reduce the peak force transmitted to the deck.
  • Engineering the roof slope to encourage the rapid shedding of hail, reducing the duration of impact stress.
  • Application of modified bitumen or high-grade TPO with reinforced scrims to enhance tensile strength.
  • Strategic placement of reinforced edge flashing to protect the most vulnerable perimeter zones of the annex.

Protecting Insulation Cores and Long-Term Envelope Stability

The most overlooked aspect of hail defense is the protection of the insulation core. In many commercial assemblies, polyisocyanurate (polyiso) is used for its high R-value. However, if the top membrane is breached or if the compressive strength is too low, hail impacts can crush the cells of the insulation. This creates "dimples" or depressions in the roof surface. While these may seem cosmetic, they create permanent low spots where water ponds, leading to accelerated membrane degradation and potential leaks.

Protecting the core requires a rigid-body defense strategy. By installing a high-density cementitious cover board between the insulation and the membrane, we create a hard-shell exterior. This layer ensures that the insulation core remains intact, preserving the thermal envelope's efficiency and preventing the capillary action that occurs when water enters a crushed insulation cell. For the Education Annex, this is vital for maintaining a consistent internal climate and protecting the building's operational longevity.

  • Installation of fiber-reinforced cover boards to provide a rigid buffer for the polyiso core.
  • Monitoring for "micro-cracking" in the insulation after severe weather events to ensure thermal integrity.
  • Ensuring a seamless transition between the sanctuary's main roof and the annex's lower sections to avoid water traps.
  • Conducting infrared thermography post-installation to verify the absence of voids or compressed insulation zones.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #587

Non-Destructive Substrate Moisture Scans on Commercial Financial Institution Data Vaults

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Non-Destructive Substrate Moisture Scans on Commercial Financial Institution Data Vaults

The Engineering Challenge of Data Vault Envelopes

In the realm of commercial building envelope engineering, few assets demand more rigorous oversight than the data vaults of major financial institutions. These structures are not merely rooms; they are high-security, climate-controlled environments where the integrity of the building skin is the primary line of defense against catastrophic equipment failure. When a leak occurs in a traditional commercial roof, the result is often a ceiling stain or a bucket on the floor. However, in a data vault, moisture infiltration often manifests as interstitial condensation or subsurface saturation that remains invisible to the naked eye until the structural integrity of the insulation is compromised.

The primary engineering challenge lies in the complexity of the assembly. These vaults typically utilize a multi-layered approach, including reinforced concrete slabs, high-density vapor barriers, and thick layers of polyisocyanurate (polyiso) insulation. Because these systems are designed to be airtight, moisture that penetrates the outer membrane becomes trapped, creating a "reservoir effect." This trapped water migrates laterally through the insulation, often settling far from the actual point of entry. A master roofer must look beyond the surface, treating the roof not as a covering, but as a dynamic thermal and moisture management system.

  • Risk of thermal bridging causing localized condensation on cold-formed metal supports.
  • Potential for osmotic blistering in modified bitumen or TPO membranes.
  • The danger of "hidden" saturation that degrades the R-value of the insulation.
  • The criticality of maintaining a sterile, dry environment to prevent electronic corrosion.

Non-Destructive Moisture Detection and Saturation Mapping

To accurately diagnose a failing envelope without compromising the security of a financial data vault, we employ Non-Destructive Moisture Detection (NDMD). The process begins with a high-resolution infrared (IR) thermographic scan. By analyzing the thermal emissivity of the roof surface, we can identify "cold spots" that indicate higher thermal mass—typically a sign of saturated insulation. However, IR is only a screening tool; it provides the "where" but not the "how much." To achieve engineering-grade precision, we transition to electronic moisture probes and dielectric constant analysis.

The objective is to establish a precise saturation boundary. By taking readings at a grid-based interval—typically every 24 to 36 inches—we can map the exact perimeter of the moisture plume. This process allows us to differentiate between surface moisture and deep-substrate saturation. We focus on the dielectric constant of the insulation; water has a significantly higher dielectric constant than air or polyiso, allowing our sensors to detect the presence of liquid water even through a waterproof membrane. This mapping ensures that the subsequent remediation is surgical rather than speculative.

  • Utilization of FLIR thermal imaging for initial heat-map generation.
  • Implementation of moisture meters to quantify water percentage in the substrate.
  • Creation of a "Saturation Map" to delineate wet versus dry zones.
  • Verification of vapor drive direction to locate the primary breach point.

Core Sample Validation and Moisture Thresholds

While NDMD provides a comprehensive map, a master tradesman knows that "the truth is in the core." To validate the electronic readings, we perform targeted core sampling. This involves extracting a cylindrical section of the entire roof assembly—from the membrane down to the structural deck. These samples are then analyzed to determine the actual moisture content of the insulation. We adhere to ASTM standards for moisture analysis, comparing the wet weight of the sample to its oven-dried weight to calculate the percentage of saturation.

The critical engineering decision rests on the moisture threshold. Not all damp insulation requires replacement. We establish a threshold—typically 5% to 10% by volume—above which the insulation's thermal resistance (R-value) is permanently compromised and the risk of mold growth or deck corrosion becomes unacceptable. If the core samples confirm that the saturation boundary mapped during the NDMD phase exceeds these thresholds, the area is flagged for surgical excision. This dual-verification method eliminates the guesswork and prevents the unnecessary removal of healthy materials, reducing both cost and downtime for the institution.

  • Extraction of 2-inch diameter cores for forensic laboratory analysis.
  • Calculation of moisture content using the gravimetric method.
  • Comparison of field-scanned data against physical core samples for calibration.
  • Assessment of the structural deck for signs of oxidation or spalling.

Surgical Excision and Envelope Restoration

Once the saturation boundaries are validated, we move from diagnosis to surgical remediation. In a data vault environment, a "rip and replace" approach is unacceptable due to the risk of exposing the interior to the elements and the potential for structural vibration. Instead, we execute surgical wet insulation excision. This involves cutting the membrane and insulation precisely along the mapped saturation boundary, extending the cut an additional 12 inches into the "dry zone" to ensure a clean transition. This ensures that no residual moisture is left to migrate back into the new materials.

The restoration phase focuses on reinstating the building envelope's continuity. We replace the saturated polyiso with high-density, closed-cell insulation that meets or exceeds the original specifications. The new insulation is staggered to prevent vertical seams, which would otherwise create paths for future moisture migration. Finally, the membrane is patched using heat-welded seams or high-strength adhesives, followed by a rigorous vacuum leak test or electronic leak detection (ELD) scan to ensure the envelope is once again hermetically sealed. This methodical approach transforms a potential facility failure into a reinforced, engineered asset.

  • Precision cutting of the membrane to isolate saturated zones.
  • Removal of contaminated insulation without disturbing the structural deck.
  • Installation of new, high-R-value insulation with staggered jointing.
  • Final validation via Electronic Leak Detection (ELD) to certify the seal.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #588

Sub-Zero Cold Storage Downward Vapor Drive & Self-Adhered SBS Barriers on Commercial Telecommunications Central Switching Offices

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Sub-Zero Cold Storage Downward Vapor Drive & Self-Adhered SBS Barriers on Commercial Telecommunications Central Switching Offices

The Dynamics of Inverted Thermal Envelopes in Telecommunications Central Switching Offices

In the specialized realm of Telecommunications Central Switching Offices (CSOs), the building envelope is subjected to extreme hygrothermal stress. Unlike standard commercial warehouses, CSOs house massive arrays of switching equipment and servers that generate constant, high-intensity internal heat loads. When these facilities are located in sub-zero climates, we encounter a critical engineering challenge: the inverted thermal envelope. In these scenarios, the interior is maintained at a consistent, warm temperature while the exterior roof deck is exposed to brutal atmospheric lows, creating a powerful downward vapor drive.

Vapor drive is the movement of water vapor from an area of high concentration to an area of low concentration. In a CSO, the warm, moist interior air seeks to migrate outward through the roof assembly toward the cold exterior. If the vapor barrier is incorrectly placed or compromised, this moisture penetrates the insulation layers and reaches the cold roof deck. Once the vapor hits the dew point—the temperature at which air becomes saturated and water vapor condenses into liquid—it forms interstitial condensation. This trapped moisture can lead to structural steel corrosion, mold growth, and the eventual degradation of the insulation's R-value.

  • Internal Heat Load: Constant thermal output from switching gear accelerates vapor pressure.
  • Vapor Pressure Differential: The delta between interior humidity and sub-zero exterior air forces moisture through microscopic voids.
  • Thermal Inversion: The roof deck becomes the coldest point in the assembly, attracting all migrating moisture.
  • Atmospheric Loading: Wind-driven snow and ice further complicate the exterior boundary layer, increasing the risk of thermal bridging.

Dew Point Migration and Interstitial Condensation Control

To prevent catastrophic envelope failure, a master roofer must engineer the assembly to ensure the dew point occurs outside the structural deck and within a manageable zone of the insulation. In a traditional assembly, placing the vapor retarder on the exterior (the "warm roof" approach) is a recipe for disaster in sub-zero climates, as it traps interior moisture against the deck. Instead, we implement a rigorous vapor-tight seal at the lowest possible point of the assembly to stop the downward drive before it enters the thermal mass.

The primary risk in high-R-value assemblies is the "sandwich effect," where moisture is trapped between two impermeable layers. If a roof utilizes a non-breathable membrane on top and a poorly installed vapor barrier on the bottom, any moisture that penetrates the system is locked in. This leads to saturated polyisocyanurate (polyiso) boards. While polyiso is a closed-cell foam with excellent thermal resistance, prolonged exposure to interstitial condensation can lead to "face-sheet delamination," where the fiberglass reinforcement separates from the foam core, effectively destroying the board's structural and thermal integrity.

  • Hygrothermal Analysis: Calculating the exact temperature drop across each inch of insulation to locate the dew point.
  • Permeability Ratings: Selecting materials with a low perm rating to ensure the vapor drive is halted at the interior boundary.
  • Condensation Drainage: Ensuring the roof slope and flashing prevent exterior water from migrating inward to meet the interior vapor.
  • ASTM C1311 Compliance: Adhering to standards for thermal insulation to ensure consistent density and performance.

Engineering the Vapor Barrier with Self-Adhered SBS Membranes

For the critical vapor seal in a CSO, we specify self-adhered SBS (Styrene-Butadiene-Styrene) modified bitumen barriers. SBS is a thermoplastic elastomer that provides superior flexibility and adhesion compared to traditional APP (Atactic Polypropylene) or torch-down systems. In sub-zero environments, the ability of the membrane to remain pliable is paramount; rigid membranes are prone to cracking under the thermal contraction and expansion cycles of a massive commercial roof.

The self-adhered nature of these barriers is the key to their engineering success. By eliminating the need for open flames or volatile solvents, we ensure a consistent, monolithic bond to the substrate. This removes the "air gaps" that typically occur with mechanically fastened systems. A self-adhered SBS barrier acts as both an air barrier and a vapor retarder, sealing the roof deck completely. This prevents the "chimney effect," where warm air is sucked upward through seams and fasteners, carrying moisture directly into the insulation layers.

  • Elastic Recovery: SBS membranes can stretch and contract without losing their seal, accommodating the building's movement.
  • Monolithic Bonding: Full-surface adhesion eliminates the possibility of vapor bypassing the barrier at the edges.
  • Low-Temperature Performance: Engineered to maintain a seal even when the substrate temperature drops significantly.
  • Installation Precision: Removing the human error associated with torching, ensuring a uniform thickness across the entire deck.

Staggered Multi-Layer Polyiso and Thermal Bridging Mitigation

To achieve the necessary R-value for a sub-zero environment without creating a "thermal highway," we employ a staggered multi-layer polyisocyanurate installation. Installing a single, thick layer of insulation is an engineering mistake; it creates continuous vertical seams that allow heat and moisture to bypass the insulation. By utilizing two or three thinner layers of polyiso and offsetting the joints, we create a labyrinthine path that forces vapor to travel through the insulation rather than around it.

This staggered approach directly addresses the issue of thermal bridging. Thermal bridging occurs where a highly conductive material (like a fastener or a seam) allows heat to escape more quickly than the surrounding insulation. By offsetting the seams of the second and third layers, we effectively "plug" the gaps of the layer below. This ensures that the thermal envelope remains consistent across the entire roof surface, maintaining the interior temperature and protecting the sensitive telecommunications equipment from external temperature swings.

  • Joint Offsetting: Ensuring that no two seams align vertically across layers, eliminating direct air paths.
  • Compression Management: Using high-density polyiso to prevent the crushing of the foam under the weight of the final membrane.
  • Fastener Integration: Utilizing thermally broken fasteners to reduce the conductive path from the roof surface to the deck.
  • Layer Sequencing: Applying the SBS vapor barrier first, followed by staggered insulation, and finishing with a high-performance capping membrane.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #589

Structural Deck Fastener Pull-Out Testing on 22-Gauge Corrugated Steel Decks on Commercial Heavy Manufacturing Fabrication Plants

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Structural Deck Fastener Pull-Out Testing on 22-Gauge Corrugated Steel Decks on Commercial Heavy Manufacturing Fabrication Plants

Engineering Audit Framework for Heavy Manufacturing Envelopes

In the context of heavy manufacturing fabrication plants, the building envelope is subjected to extreme stressors that far exceed those of standard commercial warehousing. The structural integrity of the roofing system relies fundamentally on the connection between the membrane, the insulation, and the 22-gauge corrugated steel deck. A comprehensive engineering audit must account for the unique environmental variables present in fabrication plants, such as constant harmonic vibrations from heavy machinery, thermal cycling induced by high-heat industrial processes, and the potential for chemical off-gassing that can accelerate the degradation of metallic substrates.

The 22-gauge corrugated steel deck provides the primary diaphragm strength for the roof, but its performance is entirely dependent on the fastener's ability to maintain a secure grip under positive and negative pressure. When conducting an audit for Aquashield Corporate, we prioritize the identification of "critical zones"—specifically the perimeter and corner areas where wind uplift forces are most concentrated. Failure to validate the fastener-to-deck connection in these zones can lead to catastrophic envelope failure during a high-wind event, regardless of the quality of the roofing membrane itself.

  • Assessment of substrate gauge consistency to ensure 22-gauge specifications are met across all spans.
  • Evaluation of existing fastener patterns against original architectural wind-load schedules.
  • Analysis of deck deflection and oil-canning which may compromise fastener perpendicularity.
  • Identification of chemical residues or industrial pollutants that may have compromised the steel's passivation layer.

Calibrated Mechanical Pull Testing Protocols

To move beyond theoretical calculations, we employ calibrated mechanical pull testing to determine the actual withdrawal resistance of the installed fasteners. This process involves the use of a digital force gauge and a specialized pull-tester calibrated to NIST standards. The objective is to apply a controlled, axial load to the fastener until a predetermined failure point is reached or the maximum design load is exceeded. This empirical data allows us to determine if the fasteners are truly "biting" into the 22-gauge steel or if they have become stripped due to vibration or corrosion.

The testing protocol requires a stratified random sampling approach. We do not simply test the easiest points of access; we target the most vulnerable sections of the roof plane. Each test point is documented for its exact coordinates, the specific fastener type used, and the resulting peak load in pounds or kilonewtons. By comparing these results against the manufacturer's specified minimum withdrawal values, we can establish a confidence interval for the entire roof's structural stability.

  • Application of a perpendicular load to ensure the force is purely axial, avoiding premature shear failure.
  • Incremental loading sequences to observe the elastic and plastic deformation of the fastener.
  • Utilization of a "fail-safe" threshold to prevent total deck deformation during the testing process.
  • Comparative analysis between new installations and aged fasteners to determine the rate of degradation.

Withdrawal Resistance Thresholds and Material Science

The physics of a fastener in 22-gauge corrugated steel is a balance of friction, thread engagement, and the shear strength of the steel. For a heavy manufacturing plant, the minimum withdrawal resistance threshold must be calculated based on the specific gravity of the roofing assembly and the anticipated wind-uplift pressures. In most high-performance commercial applications, we look for a minimum pull-out resistance that exceeds the design wind-load by a safety factor of at least 1.5. If a fastener pulls out at a value lower than this threshold, it indicates a failure in the connection, not necessarily a failure of the material.

Material science plays a critical role here, particularly regarding the interaction between the fastener's thread geometry and the thickness of the 22-gauge steel. Because corrugated decks have varying thicknesses at the ribs and the flats, the "bite" of the fastener can vary significantly. We analyze the "pull-through" versus "pull-out" failure modes. A pull-through occurs when the fastener head rips through the steel, whereas a pull-out occurs when the threads strip away from the substrate. In 22-gauge steel, a pull-through is often a sign of over-tightening or improper fastener head selection, while a pull-out suggests insufficient thread engagement or substrate corrosion.

  • Calculation of the "effective shear area" where the fastener engages the corrugated rib.
  • Analysis of the torsional stress applied during the initial driving of the fastener.
  • Evaluation of the fastener's "pull-out" capacity relative to the 22-gauge steel's yield strength.
  • Assessment of the impact of thermal expansion and contraction on the fastener's grip.

Corrosion Diagnostics and Wind-Zone Compliance

Fastener corrosion is the silent killer of commercial roof systems in industrial environments. In fabrication plants, the presence of moisture combined with industrial pollutants creates a galvanic cell, leading to accelerated oxidation of the fastener shaft. Our diagnostics involve the removal of a sample set of fasteners to examine the "shank-to-deck" interface. We look for signs of pitting, red rust, or white rust (zinc corrosion), which significantly reduce the effective diameter of the fastener and, consequently, its withdrawal resistance.

Finally, all pull-test data is mapped against the building's wind-zone schedule. According to ASCE 7 standards, the perimeter of a large-scale fabrication plant experiences significantly higher suction forces than the interior. If our mechanical pull tests show a decline in resistance at the roof edges, the building is non-compliant with its wind-zone requirements. To remedy this, we often recommend the installation of supplemental "wind-washers" or the transition to a higher-density fastener pattern to redistribute the uplift loads across a larger surface area of the 22-gauge deck.

  • Microscopic inspection of fastener coatings to ensure the integrity of the zinc or galvanized layer.
  • Mapping of "high-risk" wind zones based on the building's height and geographic exposure.
  • Verification of fastener compatibility with the deck's coating to prevent bimetallic corrosion.
  • Development of a long-term monitoring schedule to track the decline of withdrawal resistance over time.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #590

Industrial Corrosive Chemical Fume Exhaust Defense on Commercial Logistics Distribution Hubs

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Industrial Corrosive Chemical Fume Exhaust Defense on Commercial Logistics Distribution Hubs

Atmospheric Audit and Chemical Load Analysis

In the high-stakes environment of a commercial logistics distribution hub, the building envelope is subjected to a complex array of chemical stressors that extend far beyond standard UV exposure and precipitation. During our engineering audit of the facility, we identified a critical vulnerability: the intersection of industrial exhaust plumes and the roof membrane. Logistics hubs often house large-scale battery charging stations for electric fleets and industrial cleaning bays, both of which release concentrated acid fumes and volatile organic compounds (VOCs) into the immediate atmosphere. These fumes, when condensed on the roof surface, create a corrosive micro-environment that can rapidly degrade standard roofing materials.

The audit revealed that the primary threat was not merely the acidity of the fumes, but the synergistic effect of these chemicals combined with airborne motor oils and hydraulic fluids emanating from the loading docks and maintenance bays. When these hydrocarbons settle on a membrane, they act as solvents, potentially softening the polymer matrix or accelerating the leaching of essential stabilizing agents. Our analysis focused on the "chemical load," calculating the frequency of exhaust cycles and the concentration of sulfuric and nitric acid derivatives present in the exhaust stream.

  • Evaluation of exhaust vent placement to determine the "drop zone" of corrosive condensate.
  • Analysis of surface pH levels across various zones of the roof to map chemical saturation.
  • Assessment of oil-migration patterns from fleet maintenance areas to the primary roof field.
  • Identification of thermal bridging points where chemical condensation is most likely to occur.

Material Science and the Risk of Plasticizer Migration

From a material science perspective, the greatest risk in a chemical-heavy environment is the phenomenon of plasticizer migration. Many commercial membranes, particularly standard PVC (Polyvinyl Chloride), rely on plasticizers to maintain flexibility and elongation. When these membranes are exposed to industrial motor oils or specific corrosive fumes, a chemical exchange occurs. The oils act as a catalyst, drawing the plasticizers out of the membrane and into the contaminant layer. This process results in "plasticizer depletion," which manifests as a loss of elasticity, increased brittleness, and eventually, stress cracking.

This degradation is particularly dangerous because it often occurs invisibly before a catastrophic failure. As the membrane loses its ability to expand and contract during thermal cycling, the mechanical bonds at the seams and flashing points begin to fatigue. We referenced ASTM D1227 standards to evaluate the resistance of various polymers to these specific chemical agents. The goal was to ensure that the selected membrane could maintain its physical properties—specifically its tensile strength and puncture resistance—despite constant exposure to a hydrocarbon-rich environment.

  • Monitoring of membrane elongation percentages to detect early-stage embrittlement.
  • Testing for "solvent crazing," where chemical exposure creates micro-fractures in the polymer surface.
  • Analysis of the membrane's glass transition temperature to ensure cold-weather flexibility is maintained.
  • Evaluation of the chemical compatibility between the membrane and the underlying insulation board.

Strategic Membrane Selection for Corrosive Defense

Given the audit findings, a standard single-ply TPO (Thermoplastic Polyolefin) was deemed insufficient due to its susceptibility to certain industrial oils and its lower resistance to concentrated acid fumes. Instead, we specified a high-performance, reinforced PVC membrane specifically engineered with a chemical-resistant cap sheet, or alternatively, a fully adhered modified bitumen system with a high-solids polymer-modified asphalt cap. For this specific logistics hub, a reinforced PVC system with an integrated chemical-resistant scrim was selected to provide the necessary balance of flexibility and imperviousness.

The selection process focused on the membrane's ability to repel hydrocarbons while resisting the "etching" effect of acid fumes. A high-grade PVC membrane, when properly formulated, creates a non-polar surface that prevents the deep penetration of oils. Furthermore, the heat-welded seams of a PVC system provide a monolithic barrier, eliminating the lap-joint vulnerabilities found in adhered systems. This ensures that corrosive agents cannot seep through the seams to attack the roof insulation or the structural decking below, which would otherwise lead to premature substrate failure and costly structural repairs.

  • Selection of a membrane with a high-density polymer matrix to minimize chemical permeability.
  • Implementation of a reinforced scrim to provide dimensional stability against wind uplift and thermal shock.
  • Utilization of a non-porous surface finish to prevent the "trapping" of corrosive particulates.
  • Integration of a chemical-resistant flashing detail at all penetration points and exhaust vents.

Installation Protocol and Envelope Integrity Management

The installation of a chemical-defense system requires a level of craftsmanship that exceeds standard commercial roofing practices. To ensure total envelope integrity, we implemented a rigorous installation protocol centered on "zero-leak" seam engineering. Every seam was heat-welded using automated machinery to ensure a consistent weld temperature, followed by a manual probe test of every linear inch. This process ensures that the membrane acts as a single, continuous shield against the atmospheric pollutants identified in the initial audit.

Special attention was paid to the "critical zones" around the exhaust vents. We installed oversized, chemically-inert flashing boots and reinforced the surrounding field with a liquid-applied flashing membrane to provide a redundant layer of protection. This "belt-and-suspenders" approach ensures that even if the primary membrane suffers a localized chemical attack, the secondary barrier prevents the fumes from entering the building's interior or compromising the roof deck. Long-term integrity is managed through a scheduled maintenance program that includes neutralizing washes to remove accumulated acid salts and oil residues.

  • Execution of double-welded seams at all high-stress corners and transitions.
  • Application of a chemical-neutralizing wash every six months to prevent surface etching.
  • Installation of specialized stainless steel fasteners to prevent galvanic corrosion in acid-rich zones.
  • Quarterly infrared thermography scans to detect moisture entrapment or subsurface delamination.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565

Commercial Engineering Dossier #591

Active Emergency Leak Catchment Tarps & Interior Production Bay Diversion on Commercial Automotive Assembly Plants

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Active Emergency Leak Catchment Tarps & Interior Production Bay Diversion on Commercial Automotive Assembly Plants

The Anatomy of Envelope Failure in Automotive Assembly Environments

In the context of a large-scale automotive assembly plant, the building envelope is subject to extreme stressors that far exceed those of standard commercial warehousing. These facilities typically feature massive footprints with complex roof geometries, characterized by a dense concentration of HVAC curbings, exhaust vents, and skylight penetrations. The primary challenge in these environments is the intersection of thermal expansion and mechanical vibration. High-capacity stamping presses and robotic assembly arms create constant micro-vibrations that can compromise the bond between the roof membrane and the flashing at critical penetration points.

When a leak occurs in a production bay, the failure is rarely a simple puncture. Instead, it is often the result of systemic fatigue in the membrane—typically TPO (Thermoplastic Polyolefin) or EPDM (Ethylene Propylene Diene Monomer)—where the material has lost its elasticity due to UV degradation or improper seam welding. Once the building envelope is breached, water does not travel in a straight line; it follows the path of least resistance along structural steel beams and conduit runs, often manifesting as a leak dozens of feet away from the actual point of entry. This phenomenon, known as tracking, makes immediate identification difficult and increases the risk of catastrophic water intrusion over high-value electronic control units and robotic controllers.

  • Thermal cycling of large-span metal decking causing fatigue in adhesive bonds.
  • Clogged internal drainage systems leading to ponding and hydrostatic pressure on seams.
  • Degradation of sealant joints around oversized industrial HVAC units.
  • Capillary action drawing moisture through micro-fissures in aged flashing.

Engineering the Diversion Strategy via Industrial Vinyl Catchment

When a leak is identified over a critical production line, the immediate goal is not a permanent repair—which may be impossible during a 24-hour production cycle—but rather the implementation of an active diversion system. The engineering objective is to intercept the water at the lowest possible point of the interior ceiling and route it safely away from the production floor. For this, we deploy industrial-grade, heavy-duty vinyl diverter tarps. These are not standard utility tarps; they are high-denier, PVC-coated polyester fabrics engineered for chemical resistance and structural rigidity.

The physics of the diversion depends entirely on the established pitch of the catchment system. A master roofer ensures that the vinyl is tensioned to create a consistent slope, preventing "belly" pockets where water can pool and eventually collapse the support structure under the weight of the accumulated liquid. By utilizing heat-welded seams and reinforced grommets, we create a waterproof basin that captures the leak and directs it through a dedicated conduit. This process transforms an uncontrolled leak into a managed fluid stream, effectively neutralizing the threat to the machinery below while the plant continues to operate at full capacity.

  • Utilization of 18oz to 22oz PVC-coated vinyl for maximum tear strength and impermeability.
  • Implementation of "catch-and-carry" routing to ensure water is directed to existing floor drains.
  • Strategic tensioning using aircraft-grade cable and turnbuckles to maintain a positive slope.
  • Integration of flexible hose attachments to transport water from the tarp to a safe discharge point.

Deployment Protocols for High-Value Production Bay Protection

Deploying a diversion system within an active automotive assembly bay requires a surgical approach to minimize disruption and maximize safety. The primary concern is the protection of robotics and assembly line sensors, which are highly sensitive to moisture and humidity. The deployment begins with a comprehensive interior audit to map the trajectory of the leak. Once the "drip zone" is identified, the diversion tarp is suspended beneath the structural steel, ensuring that the catchment area is wider than the projected splash zone of the leak.

The routing of the water is the most critical phase of the deployment. We avoid any path that crosses electrical conduits or high-voltage cabling. Instead, we utilize the building's own structural columns as anchors for the drainage lines, ensuring that the water is routed toward the perimeter of the bay or into designated industrial sumps. This prevents the "secondary leak" scenario, where water from a diversion system accidentally spills onto other equipment. The system is then monitored using moisture sensors to ensure that the catchment volume does not exceed the drainage capacity during peak rain events.

  • Pre-deployment mapping of all high-voltage conduits and robotic "no-go" zones.
  • Installation of reinforced vinyl basins with a minimum 5-degree pitch for efficient drainage.
  • Securement of discharge hoses to prevent whipping or detachment during high-flow events.
  • Coordination with plant facilities management to ensure floor drains are clear of debris.

Transitioning from Emergency Mitigation to Permanent Remediation

While vinyl diversion systems are an essential tool for business continuity, they are temporary measures. The final phase of the engineering process is the transition from emergency catchment to a permanent, ASTM-compliant building envelope repair. This begins with a forensic audit of the roof surface, utilizing infrared thermography to detect trapped moisture within the insulation layers. Identifying the "thermal signature" of a leak allows us to pinpoint the exact entry point on the roof, even if the water has traveled a significant distance internally.

The permanent repair involves the removal of compromised membrane sections and the installation of new, heat-welded patches or full-section replacements. All repairs are conducted according to ANSI and ASTM standards, ensuring that the new seams are mechanically and chemically bonded to the existing substrate. We prioritize the reinforcement of all flashing and curb details, as these are the most common points of failure in automotive plants. Once the repair is completed, a flood test is performed to verify the integrity of the envelope, allowing the interior diversion tarps to be decommissioned and the production bay to return to its standard operational state.

  • Application of infrared thermography to locate subsurface moisture and void spaces.
  • Execution of heat-welded TPO/EPDM repairs to ensure a monolithic, waterproof seal.
  • Installation of reinforced flashing at all penetration points to prevent future capillary action.
  • Final validation through electronic leak detection (ELD) to certify the envelope's integrity.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #592

Cold-Weather Induction Welded Membrane Attachments on Commercial Mission-Critical Data Centers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Cold-Weather Induction Welded Membrane Attachments on Commercial Mission-Critical Data Centers

Thermal Dynamics and Membrane Behavior in Mission-Critical Envelopes

In the realm of mission-critical data centers, the building envelope is not merely a weather barrier; it is a primary line of defense for millions of dollars in sensitive computing infrastructure. During our engineering audit of a Tier IV data center facility, we observed the challenges associated with installing thermoplastic membranes in sub-zero ambient temperatures. The primary concern in cold-weather applications is the coefficient of thermal expansion and the tendency of polymers to become brittle, which can lead to micro-fractures during the welding process if not managed with precision.

When working with TPO (Thermoplastic Polyolefin) or PVC membranes in extreme cold, the material's flexibility decreases, increasing the risk of "bridging" at the corners and edges. This phenomenon occurs when the membrane fails to conform to the substrate, creating a void that is susceptible to wind-driven rain penetration. To mitigate these risks, our approach focuses on maintaining the molecular integrity of the polymer chain during the fusion process, ensuring that the bond is a true homogeneous weld rather than a superficial stick.

  • Analysis of substrate temperature to prevent premature cooling of the weld seam.
  • Evaluation of membrane relaxation times to reduce internal tension before bonding.
  • Monitoring of atmospheric humidity levels to prevent interstitial condensation during the heating phase.
  • Assessment of polymer crystallinity to ensure optimal flow during induction.

Electromagnetic Induction Plate Bonding and Molecular Fusion

Traditional hot-air welding is often inconsistent in cold weather due to heat loss to the surrounding air and the substrate. For this project, we implemented electromagnetic induction welding, a process that utilizes a high-frequency alternating current to generate heat directly within the membrane interface. By using specialized induction plates, we can target the exact layer of the membrane that requires fusion, bypassing the need to heat the entire surface area. This precision prevents the "scorching" of the upper membrane layer while ensuring the lower layer reaches its critical melting point.

The induction process creates a localized electromagnetic field that excites the molecules of the bonding plate and the membrane simultaneously. This results in a rapid, high-energy bond that is far more resistant to thermal cycling than traditional methods. From an engineering perspective, the goal is to achieve a "fusion weld" where the two separate sheets of membrane become a single, continuous piece of plastic. This is verified through destructive peel tests, where the bond strength must exceed the tear strength of the membrane itself, adhering to the strictest ASTM standards for commercial roofing.

  • Utilization of high-frequency induction coils to ensure uniform heat distribution.
  • Application of conductive bonding plates to catalyze the electromagnetic reaction.
  • Reduction of the "Heat Affected Zone" (HAZ) to prevent degradation of the polymer.
  • Implementation of real-time current monitoring to adjust for fluctuating ambient temperatures.

Tool Calibration and Weighted Magnetic Cooling Clamping

Precision in cold-weather welding is entirely dependent on tool temperature calibration. In our audit, we mandated the use of digital pyrometers and integrated thermal sensors within the induction tools. If the tool temperature drops even five degrees below the calibrated set point, the weld may suffer from "cold shunting," where the materials appear fused but lack the molecular entanglement necessary for a permanent bond. We establish a strict calibration window, ensuring the tool operates within a narrow thermal band regardless of the external wind chill.

To further ensure the integrity of the bond, we employ a weighted magnetic cooling clamping system. Once the induction weld is complete, the membrane is in a highly fluid, molten state. In cold weather, the rapid temperature drop can cause the membrane to shrink or pull away from the seam before it has fully solidified. The magnetic clamps provide a constant, calibrated downward pressure, locking the membrane in place and ensuring a flat, seamless transition. This prevents the formation of "fish-mouths" or wrinkles that could otherwise become points of failure under high wind loads.

  • Daily calibration of induction tools against a certified thermal reference.
  • Application of magnetic clamps to maintain interfacial tension during the cooling phase.
  • Use of weighted distributors to ensure uniform pressure across the entire weld width.
  • Monitoring of the cooling curve to prevent thermal shock and subsequent cracking.

Wind Uplift Resistance and Envelope Structural Integrity

For data centers, wind uplift is a critical failure mode, especially for roof-mounted cooling towers and HVAC equipment. The building envelope must be engineered to withstand extreme pressure differentials. Our audit focuses on the "critical load path," ensuring that the induction-welded attachments are securely anchored to the structural steel deck. By utilizing electromagnetic bonding, we increase the effective surface area of the attachment, which significantly reduces the stress concentrations at the edges of the membrane sheets.

We evaluate the wind resistance of the system through a combination of theoretical calculations based on ANSI/SPWindLoad standards and physical vacuum testing. The induction-welded plates act as reinforced anchors, distributing the wind load across a broader section of the roof. This prevents the "zipper effect," where a single failure point leads to a progressive collapse of the membrane across the roof surface. The final result is a robust, monolithic envelope that maintains its airtight and watertight seal even under the most severe meteorological conditions.

  • Calculation of maximum uplift pressures based on local building codes and site topography.
  • Execution of vacuum box tests to verify the absence of pinholes in the welded seams.
  • Verification of fastener pull-out strength in the underlying structural substrate.
  • Long-term monitoring of seam elasticity to ensure performance over multiple seasonal cycles.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565

Commercial Engineering Dossier #593

48-Hour Drain Bowl Hydrostatic Flood Testing & Manufacturer 20-Year NDL Audits on Commercial Cold Storage Freezer Warehouses

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
48-Hour Drain Bowl Hydrostatic Flood Testing & Manufacturer 20-Year NDL Audits on Commercial Cold Storage Freezer Warehouses

The Thermal Dynamics and Vapor Drive of Cold Storage Envelopes

In the realm of commercial building envelope engineering, cold storage freezer warehouses represent the most challenging environment for a roofing contractor. Unlike standard warehouse facilities, freezer warehouses operate under extreme temperature differentials that create a relentless internal-to-external vapor drive. When the interior is maintained at sub-zero temperatures and the exterior roof surface is exposed to ambient humidity and solar radiation, the roof assembly becomes a critical barrier against moisture migration. If the envelope is compromised, water vapor is driven into the insulation, where it freezes and creates "ice lensing," leading to structural degradation and catastrophic thermal bridging.

A master-level approach to these facilities requires more than just a waterproof membrane; it requires a comprehensive understanding of material science and the physics of the building envelope. The primary objective is to ensure that the transition points—specifically where the membrane meets the primary drainage systems—are absolutely hermetic. Any failure in the flashing or the drain bowl assembly can lead to moisture infiltration that is nearly impossible to locate once it has entered the saturated insulation layers of a freezer warehouse.

  • Management of the dew point to prevent interstitial condensation within the roof assembly.
  • Mitigation of thermal bridging at parapet walls and curb penetrations.
  • Utilization of high-density closed-cell insulation to resist compressive loads and moisture absorption.
  • Strict adherence to ASTM E2128 standards for evaluating the performance of the building envelope.

Hydrostatic Flood Testing Protocols for Primary Drain Bowls

The integrity of the primary drainage system is the most scrutinized element of a cold storage audit. To verify a truly watertight seal, we employ a 48-hour hydrostatic flood test. This process begins by temporarily plugging the primary drains using engineered mechanical plugs, effectively turning the drain bowl into a containment vessel. Water is then introduced until the bowl is filled to a predetermined height, creating a "head" of hydrostatic pressure that forces water into any microscopic voids or imperfections in the membrane weld.

Unlike a standard rain test, which is subject to the whims of weather, a hydrostatic test provides a controlled environment to measure retention. We utilize precision measurement markers to monitor the water level over a 48-hour window. Any drop in water level that exceeds the calculated evaporation rate is flagged as a failure. This rigorous testing period is essential because capillary action can pull water through a pinhole leak slowly; a short-term test would fail to detect these slow-leak scenarios that would eventually lead to interior ice accumulation and structural rot.

  • Installation of heavy-duty pneumatic plugs to ensure zero leakage at the pipe interface.
  • Calibration of water levels to exceed the minimum required hydrostatic head pressure.
  • Continuous monitoring of water levels at 12-hour intervals to plot the rate of loss.
  • Verification of the "bowl-to-membrane" transition to ensure no flanking leaks occur at the flange.

Material Science of Membrane Flange Welds and Verification

The most common failure point in a commercial roof is the transition between the field membrane and the penetration flange. In freezer warehouses, these joints are subject to extreme contraction and expansion cycles due to the temperature delta. We utilize thermoplastic membranes, such as TPO or PVC, which allow for heat-welding. A proper weld does not simply "stick" the materials together; it creates a molecular bond that fuses the two sheets into a single, monolithic piece of plastic. This is the difference between a seam and a weld.

To verify these welds, our engineering audit employs a two-step verification process: visual inspection and mechanical probing. Using a tapered steel probe, we traverse the entire perimeter of the flange weld. If the probe can penetrate the seam, the weld is compromised and must be re-cut and re-welded. Furthermore, we examine the "bead" of the weld for consistency. An uneven bead often indicates inconsistent heat application or contamination of the substrate, both of which compromise the long-term durability of the 20-year system. We adhere to ANSI standards for thermoplastic roofing to ensure that the weld strength exceeds the tensile strength of the membrane itself.

  • Application of robotic heat-welding for field seams to ensure consistent temperature and speed.
  • Hand-welding of complex flange details using calibrated hot-air welders.
  • Verification of the "overlap" distance to ensure it meets or exceeds manufacturer specifications.
  • Assessment of the membrane's coefficient of thermal expansion to prevent stress cracking at the corners.

The NDL Audit and Manufacturer Warranty Sign-Off

The culmination of the engineering audit is the No Dollar Limit (NDL) warranty sign-off. An NDL warranty is the gold standard in commercial roofing, signifying that the manufacturer will cover the full cost of repairs regardless of the amount, provided the installation meets their stringent engineering specifications. For a cold storage facility, the manufacturer's representative performs a final audit to ensure that every detail—from the fastener spacing to the hydrostatic test results—is documented and compliant.

The audit process involves a comprehensive review of the "as-built" documentation. We provide the manufacturer with the 48-hour flood test logs, the weld verification reports, and the thermal imaging scans of the roof surface. This level of transparency ensures that the warranty is not just a piece of paper, but a certified guarantee of performance. The final sign-off occurs only after the manufacturer is satisfied that the building envelope is a closed system, capable of resisting the unique pressures of a freezer warehouse environment for the next two decades.

  • Submission of detailed hydrostatic pressure logs to the manufacturer's engineering department.
  • Third-party verification of membrane thickness and weld integrity.
  • Final walk-through with the manufacturer's representative to confirm all flashing details.
  • Issuance of the 20-year NDL certificate upon successful completion of all audit benchmarks.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #594

Masonry Parapet Counterflashing Reglet Overhauls & Polyurethane Sealant Compression on Commercial Commercial Fleet Maintenance Hangars

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Masonry Parapet Counterflashing Reglet Overhauls & Polyurethane Sealant Compression on Commercial Commercial Fleet Maintenance Hangars

Engineering Audit and Failure Analysis of Hangar Envelope Systems

In the high-stakes environment of commercial fleet maintenance hangars, the building envelope is subjected to extreme thermal cycling and significant structural vibrations caused by heavy machinery and vehicle movement. During our comprehensive engineering audit for Aquashield Corporate, we identified a systemic failure in the parapet wall assembly. The primary point of ingress was the counterflashing interface, where the transition between the roofing membrane and the masonry wall had degraded. Over time, the original surface-mounted flashing had succumbed to fastener fatigue and the natural expansion and contraction of the masonry, leading to capillary action that drew moisture deep into the wall substrate.

The failure was not merely a result of age but a fundamental misalignment between the materials used and the environmental stressors of a fleet hangar. We observed significant spalling at the mortar joints and a complete loss of adhesion in the legacy sealants. This created a direct pathway for hydrostatic pressure to push water behind the flashing, saturating the insulation and compromising the structural integrity of the parapet cap. To rectify this, a total overhaul of the reglet system was required, shifting from a surface-applied method to an embedded engineering approach.

  • Identification of thermal bridging points along the parapet wall.
  • Analysis of moisture migration patterns using infrared thermography.
  • Evaluation of existing sealant elasticity and bond strength failure.
  • Assessment of masonry porosity and its impact on water absorption.
  • Review of ASTM E2112 standards for corner joint water penetration.

Precision Reglet Excavation and Mortar Joint Grinding

The core of the remediation strategy involved the creation of a precision reglet—a recessed groove cut into the masonry to house the counterflashing. Unlike standard installations that rely on mechanical fasteners and surface beads of sealant, a ground-in reglet ensures that the flashing is integrated into the building's structure. We utilized industrial diamond-blade grinders to surgically remove mortar from the horizontal joints. This process requires a master tradesman's touch to ensure that the structural integrity of the masonry units remains intact while creating a clean, square pocket for the metal insert.

The grinding process was calibrated to a depth and width that matched the gauge of the Kynar metal, ensuring a snug fit that minimizes the volume of sealant required. By removing the degraded mortar and cleaning the substrate with high-pressure compressed air, we eliminated contaminants that would otherwise inhibit the bond of the polyurethane sealant. This stage of the overhaul is critical; if the reglet is uneven or contains debris, the resulting sealant joint will have inconsistent thickness, leading to premature failure under thermal stress.

  • Utilization of variable-speed diamond grinders for precise mortar removal.
  • Strict adherence to joint depth specifications to prevent masonry fracturing.
  • Mechanical cleaning of the reglet interior to ensure a virgin substrate.
  • Verification of reglet linearity across the entire length of the hangar perimeter.
  • Implementation of dust mitigation protocols to protect hangar interior equipment.

Kynar 500 Heavy-Gauge Counterflashing Integration

For the flashing material, we specified heavy-gauge Kynar 500 finished steel. Kynar is the industry gold standard for commercial envelopes due to its superior UV resistance and chemical stability, which is essential in fleet hangars where exhaust fumes and industrial solvents are prevalent. The heavy gauge ensures that the metal does not oil-can or warp under the extreme temperature swings common in large-span buildings. Each piece of counterflashing was custom-bent to provide a precise drip edge, ensuring that water is shed away from the masonry face and onto the roofing membrane.

The installation process focused on the science of thermal movement. Metal and masonry have different coefficients of thermal expansion; if the flashing is pinned too rigidly, it will buckle. By embedding the Kynar into the reglet, we allowed the metal to "float" slightly within the polyurethane sealant. This creates a flexible gasket that accommodates the building's natural movement without breaking the watertight seal. The overlap at the joints was engineered to be water-shedding, with each section meticulously overlapped and sealed to prevent any wind-driven rain from penetrating the assembly.

  • Selection of 24-gauge Kynar 500 for maximum structural rigidity.
  • Custom fabrication of drip edges to eliminate wall staining and moisture cling.
  • Calculation of expansion gaps to prevent metal buckling during summer peaks.
  • Precision fitting of the metal into the ground reglet for a flush finish.
  • Application of corrosion-resistant coatings on all cut edges.

Polyurethane Sealant Compression and Envelope Finalization

The final and most critical phase of the overhaul is the application of high-performance polyurethane sealant. Unlike silicone, which can struggle with adhesion to certain masonry types, polyurethane offers a high-modulus strength and exceptional bonding capabilities. The goal was to achieve "sealant compression," where the sealant is squeezed between the Kynar flashing and the masonry reglet. This compression transforms the sealant from a simple filler into a structural gasket that can withstand the high-velocity wind loads typical of large hangar structures.

We employed a "tool-and-set" technique to ensure the sealant formed a concave fillet, which optimizes the distribution of stress across the joint. By controlling the depth-to-width ratio of the sealant bead, we ensured that the material could stretch and compress without tearing. This engineering approach eliminates the "voids" that typically occur in surface-applied sealants. Once cured, the polyurethane creates a seamless, airtight, and watertight barrier that effectively stops wall leaks and protects the interior of the fleet maintenance facility from moisture infiltration.

  • Application of polyurethane sealant with a high movement capability (±50%).
  • Implementation of the "hour-glass" joint geometry to reduce internal stress.
  • Strict control of cure times to prevent premature exposure to environmental contaminants.
  • Final flood testing of the parapet to verify zero penetration.
  • Verification of the complete envelope seal according to ANSI standards.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #595

Flute-Fill EPS/Polyiso Insulation Sizing for Standing Rib Metal Roof Retrofits on Commercial Chemical Processing Facilitys

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Flute-Fill EPS/Polyiso Insulation Sizing for Standing Rib Metal Roof Retrofits on Commercial Chemical Processing Facilitys

The Engineering Challenge of Corrugated Substrates in Chemical Environments

During a comprehensive building envelope audit of a high-capacity chemical processing facility, the primary failure point identified was the systemic thermal inefficiency of the existing standing rib metal roof. In these industrial environments, the internal atmosphere is often characterized by volatile temperature swings and the presence of corrosive airborne particulates. The existing roof system utilized a standard corrugated profile that, while structurally sound, created significant voids within the ribs. When traditional insulation blankets or oversized boards are laid over these ribs, they create a "bridge" effect, leaving the valleys of the metal decking uninsulated.

This phenomenon, known as thermal bridging, allows heat to bypass the insulation layer via the high-conductivity metal ribs. In a chemical processing plant, this is not merely an energy efficiency concern but a critical moisture management issue. When warm, humid internal air meets the cold metal of the rib, it reaches its dew point, leading to interstitial condensation. Over time, this moisture accumulates against the underside of the roof deck, promoting oxidation and compromising the structural integrity of the steel.

  • Identification of "cold spots" using infrared thermography across the corrugated profile.
  • Analysis of vapor drive originating from chemical processing equipment.
  • Evaluation of existing fastener fatigue due to repeated thermal expansion and contraction.
  • Assessment of the R-value degradation caused by air infiltration within the rib cavities.

Precision-Cut Flute-Fill Geometry and Material Selection

To rectify the thermal bridging identified during the audit, the engineering specification required a transition from a ribbed surface to a flat, thermally continuous plane. The solution implemented was the deployment of precision-cut flute-fill insulation. Unlike standard insulation boards, flute-fills are CNC-milled to the exact dimensions of the standing rib profile, ensuring a friction-fit tolerance that eliminates gaps between the insulation and the metal substrate. This ensures that the entire volume of the rib is occupied by a thermal barrier, effectively "flattening" the roof deck for the subsequent membrane application.

The selection of materials was critical. We utilized a hybrid approach combining Expanded Polystyrene (EPS) for the base flute-fill and Polyisocyanurate (Polyiso) for the capping layers. EPS provides the necessary dimensional stability and compressive strength to maintain the shape of the flute, while Polyiso offers a superior R-value per inch, ensuring the facility meets stringent ASTM C1289 standards for thermal resistance. The precision of the cut is paramount; any gap larger than 1/8 of an inch allows for convective air loops, which can reduce the effective R-value of the assembly by up to 20%.

  • CNC-milling of EPS profiles to match the specific pitch and depth of the standing rib.
  • Layering of high-density Polyiso boards to achieve the target thermal resistance.
  • Application of a staggered joint pattern to prevent linear heat transfer.
  • Verification of compression tolerances to ensure no "bottoming out" against the metal deck.

Mitigating Thermal Bridging and Vapor Drive in Chemical Facilities

In a chemical processing facility, the building envelope must act as a hermetic seal to prevent the migration of corrosive gases and internal moisture. The installation of flute-fill insulation transforms the roof from a series of disconnected thermal zones into a monolithic slab. By filling the ribs, we eliminate the "chimney effect" where air moves freely through the corrugated channels. This is essential for maintaining a consistent interior temperature and preventing the localized condensation that typically occurs at the junction of the rib and the roof deck.

Furthermore, the material science behind the Polyiso capping layer provides an inherent vapor retarder. When coupled with a precision-fit flute-fill, the system creates a continuous thermal break. This prevents the "thermal siphoning" effect common in older industrial roofs. We adhered to ANSI standards for commercial roofing to ensure that the transition from the vertical rib to the horizontal plane was seamless. This prevents the accumulation of stagnant air and ensures that the thermal load is distributed evenly across the entire roof surface, reducing the stress on the HVAC systems.

  • Elimination of interstitial condensation through the removal of void spaces.
  • Implementation of a continuous vapor barrier to block chemical fume migration.
  • Reduction of the building's overall thermal coefficient of conductance.
  • Prevention of localized "hot spots" that can degrade single-ply membranes.

Single-Ply Membrane Integration and Final Envelope Validation

The final phase of the retrofit involved the installation of a reinforced single-ply membrane over the now-flat insulation profile. Because the flute-fill system created a level surface, we were able to install a fully adhered TPO (Thermoplastic Polyolefin) membrane. This eliminated the need for complex flashing at every rib, which is traditionally the most common point of failure in standing rib systems. The membrane was heat-welded at the seams using automated robotics to ensure a leak-proof seal that can withstand the chemical off-gassing associated with the facility's operations.

To validate the engineering success of the installation, a final building envelope audit was conducted. This included a flood test and a secondary infrared scan to confirm the absence of thermal bridging. The results indicated a uniform heat signature across the entire roof surface, confirming that the flute-fill profiles were seated correctly and that the thermal break was absolute. The transition from a corrugated, inefficient surface to a flat, high-performance envelope resulted in a measurable decrease in energy consumption and a total elimination of internal condensation.

  • Installation of a high-mil TPO membrane for superior chemical and UV resistance.
  • Heat-welding of all seams to create a monolithic waterproof barrier.
  • Execution of a rigorous water-tightness test per ASTM E1105 standards.
  • Final thermographic verification to ensure zero thermal bridging at the rib locations.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #596

Structural Plywood Deck Re-Nailing Schedules on Commercial Municipal City Hall & Administrative Complexs

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Structural Plywood Deck Re-Nailing Schedules on Commercial Municipal City Hall & Administrative Complexs

Engineering Audit of Municipal Roof Substrates and Envelope Integrity

When conducting a comprehensive building envelope audit on a Municipal City Hall or Administrative Complex, the focus must extend beyond the membrane to the structural substrate. In these high-occupancy civic structures, the roof deck is not merely a surface for the roofing system but a critical diaphragm that ensures the lateral stability of the entire building. A master roofer recognizes that the integrity of the building envelope begins at the nail-to-wood interface. In many aging municipal complexes, original fastening schedules were often insufficient for modern building codes, leading to potential failures during extreme weather events.

Our audit process focuses on the identification of "fastener fatigue" and the degradation of the plywood substrate. Over decades, the cyclical loading and unloading of the roof deck—caused by thermal expansion and wind-induced pressure changes—can loosen existing fasteners. This creates a gap between the nail shank and the wood fibers, significantly reducing the deck's ability to resist uplift. To rectify this, a rigorous re-nailing schedule is implemented to reinforce the connection between the plywood sheathing and the underlying roof joists.

  • Assessment of existing fastener spacing and alignment with structural members.
  • Evaluation of plywood moisture content to ensure optimal grip for new fasteners.
  • Identification of "dead zones" where original installers missed joist centers.
  • Analysis of edge-distance compliance to prevent splitting of the plywood periphery.
  • Verification of substrate thickness to ensure nail penetration meets minimum embedment depths.

Coastal High-Wind Uplift and Diaphragm Performance

For municipal complexes located in coastal regions, the roof deck is subjected to intense negative pressure, commonly known as wind uplift. According to ASCE 7 standards, the windward and leeward edges of a flat or low-slope roof experience the highest suction forces. If the plywood deck is not properly anchored, the wind can literally peel the substrate away from the joists, leading to a catastrophic failure of the roofing membrane and the subsequent collapse of the interior ceiling systems.

The engineering goal is to transform the roof deck into a rigid, monolithic diaphragm. By implementing a strategic re-nailing schedule, we distribute the wind loads more evenly across the structural frame. This involves increasing the fastener density at the perimeter and corner zones—the "high-pressure zones"—while maintaining a standard grid across the field of the roof. This graduated fastening approach ensures that the building envelope can withstand peak gusts without compromising the shear strength of the plywood.

  • Calculation of maximum allowable tributary areas for each fastener.
  • Implementation of reinforced fastening patterns at the roof eaves and rakes.
  • Alignment of fasteners with the grain of the wood to maximize pull-out resistance.
  • Coordination of fastener spacing to prevent "zipper effect" failures during high-wind events.
  • Integration of the deck reinforcement with the overall building envelope sealing strategy.

Pneumatic Application of Ring-Shank Fasteners

The choice of fastener is the difference between a temporary fix and an engineering solution. In commercial municipal applications, smooth-shank nails are insufficient due to their tendency to "creep" or back out over time. We specify pneumatically driven ring-shank fasteners. The ring-shank design features a series of ribs or rings along the shaft that act like a screw, mechanically interlocking with the wood fibers. This provides a significantly higher withdrawal resistance compared to traditional nails, ensuring the deck remains pinned to the joists under extreme suction.

The use of pneumatic nailers allows for a level of precision and consistency that manual hammering cannot match. By calibrating the pneumatic pressure, we ensure that the nail is driven flush to the substrate without over-driving, which would crush the wood fibers and compromise the holding power. Furthermore, the speed of pneumatic application allows for the dense fastening schedules required by coastal codes to be executed without introducing unnecessary stress to the plywood sheets.

  • Utilization of galvanized coatings to prevent corrosion in humid coastal environments.
  • Calibration of pneumatic drivers to ensure consistent head-flush seating.
  • Selection of nail gauges that balance shear strength with substrate preservation.
  • Verification of nail penetration depth into the structural joist (minimum 1.5 inches).
  • Reduction of manual labor errors through standardized pneumatic firing patterns.

Verifying Shear Withdrawal and Long-Term Compliance

A re-nailing schedule is only as effective as its verification process. To ensure the municipal complex meets the required engineering standards, we perform a series of shear withdrawal tests. This involves measuring the force required to pull a fastener from the substrate, ensuring that the actual performance matches the theoretical calculations provided in the engineering specs. We adhere to ASTM standards for wood-fastener connections to certify that the building envelope is compliant with current municipal safety codes.

Beyond the initial installation, the long-term compliance of the roof deck depends on the stability of the wood-to-metal bond. By documenting every fastener location and recording the specific nail type used, we create a permanent engineering record for the city's facility management. This level of transparency ensures that future renovations or roof replacements are based on accurate data regarding the structural integrity of the deck. The result is a fortified building envelope that protects the city's administrative assets and its citizens.

  • Conducting random pull-tests to verify the withdrawal resistance of ring-shank nails.
  • Mapping fastener density to confirm adherence to the approved engineering blueprints.
  • Cross-referencing installed schedules with ANSI standards for structural fasteners.
  • Performing visual inspections for "shiners" or nails that missed the structural joists.
  • Issuing a final certification of the building envelope's wind-uplift capacity.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #597

Life-Cycle Cost Analysis (LCCA) on Commercial High-Rise Commercial Penthouse Towers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Life-Cycle Cost Analysis (LCCA) on Commercial High-Rise Commercial Penthouse Towers

Comprehensive Envelope Diagnostics and Engineering Audits

In the realm of high-rise commercial penthouse towers, the building envelope is not merely a cover but a complex engineered system subject to extreme atmospheric pressures and thermal cycling. A master-level engineering audit begins with a forensic analysis of the existing assembly, moving beyond superficial visual inspections to employ non-destructive testing (NDT). We prioritize the identification of systemic failures in the flashing, parapet wall caps, and primary membrane integrity. By utilizing infrared thermography and electronic leak detection (ELD), we can map subsurface moisture entrapment that often evades standard inspections but compromises the structural decking over time.

The technical focus during these audits is centered on adherence to ASTM and ANSI standards, specifically regarding wind uplift resistance and water permeability. In penthouse towers, the "stack effect" and high-velocity wind gusts create unique pressure differentials that can pull flashing away from masonry or metal interfaces. Our audit process evaluates the current state of the roof's reflective index and thermal bridging, ensuring that the building envelope is functioning as a cohesive unit rather than a series of disconnected patches.

  • Implementation of ASTM D2854 for infrared thermography to detect saturated insulation.
  • Evaluation of wind uplift ratings against ANSI/SPWind standards to ensure penthouse stability.
  • Detailed core sampling to analyze the degradation of the existing membrane and substrate.
  • Assessment of drainage efficiency and the integrity of primary and secondary scuppers.
  • Analysis of flashing transitions at mechanical penthouse penetrations and HVAC curbs.

Net Present Value (NPV) and Life-Cycle Cost Analysis

From a commercial asset management perspective, the decision to replace or restore a roof system is a financial engineering problem. A Life-Cycle Cost Analysis (LCCA) allows us to move past the initial "sticker price" of a project and instead calculate the Net Present Value (NPV) of the roof over a 20-to-30-year horizon. When we compare a full tear-off and replacement against a high-solids silicone or acrylic restoration, the NPV often favors restoration due to the avoidance of massive labor costs and the mitigation of operational downtime in a high-occupancy penthouse tower.

The calculation considers the discount rate, inflation of material costs, and the projected frequency of maintenance intervals. A traditional replacement may seem cost-effective in year one, but when the costs of debris removal, crane rentals for high-rise access, and potential interior water damage during construction are factored in, the "cheaper" option becomes the most expensive. By extending the life of the existing asset through engineered restoration, we shift the expenditure from a heavy Capital Expenditure (CapEx) to a manageable Operating Expenditure (OpEx), optimizing the building's internal rate of return.

  • Comparison of initial installation costs versus long-term maintenance overhead.
  • Calculation of energy savings derived from increased Solar Reflectance Index (SRI) values.
  • Analysis of "opportunity costs" associated with penthouse tenant disruption during construction.
  • Projection of future replacement costs adjusted for inflation and material scarcity.
  • Evaluation of the present value of extended warranty protections.

Tax Deductions for Maintenance Restoration and Asset Recovery

One of the most overlooked aspects of building envelope engineering is the intersection of material science and tax law. Under current IRS guidelines and commercial accounting standards, there is a critical distinction between a "capital improvement" and "maintenance restoration." A full roof replacement is typically categorized as a capital improvement, which must be depreciated over a long period (often 39 years for commercial property). Conversely, a comprehensive restoration—such as the application of a high-performance polymer coating system—can often be classified as a repair and maintenance expense.

This distinction allows building owners to deduct the cost of the restoration in the current tax year, providing an immediate cash-flow advantage. For a high-rise penthouse tower, where the square footage is premium and the costs are substantial, the ability to write off the restoration cost immediately rather than depreciating it over decades is a powerful financial lever. We guide our clients through the technical documentation required to prove that the restoration has returned the asset to its original functional state without fundamentally altering the building's structure.

  • Utilization of Section 179D deductions for energy-efficient building envelope improvements.
  • Differentiation between "betterment" and "restoration" to maximize immediate tax write-offs.
  • Documentation of energy reduction metrics to qualify for green building tax credits.
  • Strategic scheduling of maintenance to align with fiscal year tax planning.
  • Analysis of the impact of restoration on the overall building valuation and appraisal.

Sustainability, Waste Mitigation, and Warranty Extensions

The environmental impact of commercial roofing is staggering. A traditional tear-off of a 50,000-square-foot penthouse roof can send hundreds of tons of non-biodegradable membranes and saturated insulation into local landfills. As master roofers, we advocate for a "circular" approach to the building envelope. By utilizing restoration coatings that bond chemically to the existing substrate, we eliminate the need for demolition, thereby avoiding landfill waste and reducing the carbon footprint associated with transporting new materials to a high-rise site.

Furthermore, the engineering of these restoration systems allows for the issuance of 15-year to 20-year warranty extensions. These are not mere service contracts but comprehensive warranties backed by material science and rigorous testing. A 15-year warranty extension on a restored system provides the owner with the same peace of mind as a new roof, but at a fraction of the environmental and financial cost. This approach ensures that the penthouse tower remains a sustainable asset, reducing the Urban Heat Island effect through high-albedo surfaces while maintaining a watertight seal against the elements.

  • Diversion of thousands of pounds of roofing debris from landfills through restoration.
  • Reduction of VOC emissions by selecting low-solvent, high-solids coating materials.
  • Implementation of "Cool Roof" technology to lower HVAC loads and energy consumption.
  • Securing 15-year manufacturer-backed warranties that validate the restoration's integrity.
  • Enhancement of the building's LEED certification through sustainable material management.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565
Commercial Engineering Dossier #598

Lightning Protection System Air Terminal Stanchion Flashing & Membrane Bonding on Commercial Regional Healthcare Medical Centers

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Lightning Protection System Air Terminal Stanchion Flashing & Membrane Bonding on Commercial Regional Healthcare Medical Centers

The Critical Intersection of Lightning Protection and Envelope Integrity

In the engineering of Regional Healthcare Medical Centers, the building envelope is the primary line of defense for critical life-safety systems and high-value diagnostic equipment. These facilities present a unique challenge: the necessity of a comprehensive Lightning Protection System (LPS) to mitigate the risk of catastrophic electrical surges, contrasted with the absolute requirement for a watertight, monolithic roofing membrane. From a master roofer's perspective, every air terminal stanchion and grounding conductor represents a potential breach in the building's primary moisture barrier. When these systems are poorly integrated, the result is not merely a leak, but a systemic failure of the building envelope that can lead to mold growth in sterile environments or the failure of sensitive medical imaging arrays.

The primary conflict arises from the differing physical properties of the LPS hardware and the roofing membrane. While the membrane is designed to expand and contract with thermal fluctuations, the copper or aluminum stanchions remain rigid. This differential in the coefficient of thermal expansion creates shear stress at the bonding points. Furthermore, the high-voltage nature of a lightning strike generates immense heat, which can cause localized melting or "charring" of thermoplastic membranes if the energy is not efficiently channeled away from the roof surface. To ensure a lifetime warranty and structural integrity, the engineering focus must shift from simple installation to a rigorous bonding and flashing protocol that adheres to NFPA 780 and ASTM standards.

  • Mitigation of hydrostatic pressure at the base of air terminal stanchions.
  • Management of thermal bridging between metallic conductors and synthetic membranes.
  • Prevention of capillary action where grounding cables penetrate the roof deck.
  • Ensuring the continuity of the vapor barrier during the installation of LPS hardware.

Engineering the Heavy-Duty Stanchion Pitch-Pocket

A common failure point in commercial healthcare roofing is the reliance on simple sealant beads around air terminal stanchions. In a high-performance audit, we advocate for the implementation of engineered pitch-pockets. A pitch-pocket is a reinforced, recessed containment area that allows for the pouring of a high-grade, non-shrink polymeric grout or a specialized flashing sealant around the base of the stanchion. This method eliminates the "point-load" stress on the membrane and provides a redundant layer of waterproofing. By creating a physical basin that is fully integrated into the roof's flashing system, we ensure that water is shed away from the penetration rather than being drawn in through a failed bead of caulk.

The construction of these pockets requires a precise sequence of membrane bonding. The base membrane must be reinforced with a compatible flashing strip, followed by the installation of the stanchion, and finally the application of the pourable sealant. This creates a "plug" that is chemically and mechanically bonded to the roof system. For medical centers, where roof access is frequent for HVAC maintenance, these pockets must be designed to withstand mechanical vibration and the incidental impact of foot traffic without cracking or pulling away from the substrate.

  • Utilization of reinforced flashing membranes to prevent tearing at the stanchion base.
  • Application of non-shrink, weather-resistant grouts to fill the pitch-pocket void.
  • Implementation of a secondary "top-cap" sealant to protect the grout from UV degradation.
  • Verification of the bond between the stanchion base plate and the structural decking.

Grounding Cable Conductor Flashings and Penetration Management

While the air terminals capture the strike, the grounding cables are responsible for safely transporting that energy to the earth. These conductors often penetrate the roof at multiple points, creating a series of vulnerabilities. A master roofer knows that a cable penetration is essentially a hole in the building's armor. If the flashing is not executed with precision, these points become conduits for water ingress, especially during wind-driven rain events common to regional healthcare campuses. The goal is to achieve a gas-tight and water-tight seal that does not compromise the electrical conductivity of the cable.

The industry standard for these penetrations involves a combination of mechanical clamping and chemical bonding. We employ a "boot and bond" strategy, where a flexible, heat-welded membrane boot is installed around the conductor, followed by a high-performance sealant at the interface. This allows the cable to move slightly during thermal cycles without tearing the membrane. Furthermore, the transition from the roof surface to the interior must be managed with a drip edge or a flashing diverter to prevent water from tracking down the cable and entering the building's interior plenum.

  • Elimination of "puddle points" around cable penetrations through strategic slope correction.
  • Use of heat-welded TPO or PVC boots for a seamless, monolithic bond.
  • Installation of stainless steel clamping rings to prevent cable slippage and membrane stress.
  • Application of ASTM-compliant sealants that maintain elasticity over a wide temperature range.

Material Science and Long-Term Membrane Bonding

The final layer of a successful building envelope audit involves the analysis of material science. In healthcare facilities, the choice of membrane—whether it be a Thermoplastic Polyolefin (TPO), Polyvinyl Chloride (PVC), or a Modified Bitumen—dictates the bonding strategy for the LPS. The most critical risk is the "lightning strike puncture." When a strike occurs, the plasma channel creates an instantaneous burst of heat. If the stanchion is not properly bonded and grounded, this heat can melt a hole directly through the membrane, leading to immediate leaks during the next rain event.

To prevent this, we specify the use of conductive flashing tapes and heat-dissipating pads at the base of each terminal. These materials act as a thermal buffer, spreading the energy of the strike across a wider surface area and reducing the peak temperature at the membrane interface. Additionally, the use of compatible adhesives is paramount; using a solvent-based adhesive on a TPO membrane can lead to premature degradation and "alligatoring" of the surface. A rigorous audit ensures that every chemical interaction between the LPS hardware and the roofing system is documented and compliant with the manufacturer's specifications to preserve the

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565

Commercial Engineering Dossier #599

Commercial Roof Hatch Safety Grab Bars & Compression Curb Gasket Weatherproofing on Commercial University Research Laboratorys

Industrial Building Envelope Sciences • Commercial Low-Slope Systems
Commercial Roof Hatch Safety Grab Bars & Compression Curb Gasket Weatherproofing on Commercial University Research Laboratorys

OSHA-Compliant Access Engineering and Safety Grab Bar Integration

In the high-stakes environment of a University Research Laboratory, the roof hatch is more than a simple access point; it is a critical safety interface. During our engineering audit, we identified a recurring failure in standard hatch installations: the lack of adequate transition support for personnel ascending from the interior. To meet OSHA 1910.28 and ANSI standards, the installation of heavy-duty safety grab bars is non-negotiable. These bars must be engineered to withstand significant lateral loads, ensuring that a technician can safely transition from the vertical ladder to the horizontal roof plane without losing three points of contact.

The structural integrity of these grab bars depends entirely on their anchoring mechanism. We specify galvanized steel posts that are mechanically fastened directly into the structural steel or reinforced concrete of the building's core, rather than relying on the thin gauge metal of the hatch frame. This prevents the "lever effect" where repeated use could fatigue the metal and lead to a catastrophic failure of the hatch curb.

  • Installation of 1.5-inch diameter schedule 40 galvanized steel piping for maximum rigidity.
  • Application of high-visibility powder coating to ensure visibility during low-light emergency evacuations.
  • Strategic placement of grab bars at a 45-degree angle to facilitate an ergonomic transition.
  • Verification of load-bearing capacity to exceed 250 lbs of concentrated force per post.
  • Integration of non-slip grip textures to prevent hand slippage in damp or oily conditions.

Counterbalanced Smoke Dampers and Mechanical Ventilation Synergy

Research laboratories often house volatile chemicals and sensitive equipment, making the roof hatch a primary component of the building's smoke evacuation and ventilation strategy. The integration of counterbalanced smoke dampers ensures that the hatch can be opened rapidly and effortlessly during an emergency, while remaining airtight during normal operations. From a material science perspective, the counterbalancing system must be calibrated to the exact weight of the hatch cover, accounting for the added mass of reinforced glazing or insulation layers.

The engineering challenge lies in the seal. A smoke damper that is too tight may fail to open via the actuator, while one that is too loose allows conditioned air to escape, increasing the laboratory's energy costs and compromising the pressure differential required for clean-room environments. We utilize heavy-duty spring-loaded hinges and precision-weighted counterweights to maintain a constant state of equilibrium, reducing the strain on the mechanical actuators.

  • Utilization of high-temperature rated actuators for rapid deployment during fire alarms.
  • Implementation of precision-balanced gas springs to eliminate the "slam" effect during closure.
  • Integration of smoke-tight gaskets that maintain a seal under negative pressure conditions.
  • Regular calibration of the counterbalance system to account for material fatigue over time.
  • Coordination with the HVAC system to ensure synchronized airflow during hatch activation.

High-Performance Compression Curb Gaskets and Thermal Bridging

The interface between the roof hatch curb and the roof membrane is one of the most common points of failure in a commercial building envelope. In a university setting, where roofs are often subject to heavy foot traffic and equipment vibration, a standard sealant bead is insufficient. We implement heavy-duty compression curb gaskets made from closed-cell EPDM or silicone. These materials are chosen for their exceptional "compression set" resistance, meaning they return to their original shape after being squeezed, maintaining a permanent seal against the curb.

Beyond water infiltration, we must address thermal bridging. Metal curbs act as thermal highways, conducting heat out of the building in winter and into the building in summer. By utilizing a high-density compression gasket, we create a thermal break that reduces energy loss. This is critical for research labs that require precise temperature control for sensitive experiments. The gasket must be installed with a consistent compression ratio across the entire perimeter to prevent "channeling," where water finds a path of least resistance through a gap in the seal.

  • Selection of EPDM gaskets with a minimum shore hardness of 60 to ensure durability.
  • Application of a continuous, unbroken gasket bead to eliminate capillary action.
  • Installation of a secondary flashing layer to provide redundant waterproofing.
  • Use of thermal break spacers to decouple the metal curb from the interior floor slab.
  • Verification of gasket compression using calibrated feeler gauges during the audit process.

Compression Termination Bars and Perimeter Envelope Integrity

The final line of defense in the building envelope is the termination of the roof membrane at the hatch curb. To ensure a watertight seal, we utilize mechanical compression termination bars. Unlike traditional adhesives or lap-seams, a termination bar physically clamps the membrane to the curb, creating a mechanical bond that cannot be pulled away by wind uplift or thermal expansion and contraction. This is particularly important in laboratory buildings where the roof may be subject to extreme temperature fluctuations due to exhaust fans and HVAC discharge.

The installation process requires a meticulous approach to fasteners and sealants. We specify stainless steel fasteners to prevent galvanic corrosion between the bar and the curb. A high-grade polyurethane sealant is applied behind the termination bar to create a "double-lock" system. This ensures that even if the primary membrane fails, the secondary sealant layer prevents water from migrating into the wall cavity. This level of redundancy is the hallmark of master-level commercial roofing and is essential for protecting the expensive research equipment housed below.

  • Installation of 2-inch wide aluminum termination bars with a smooth, rounded edge.
  • Application of fasteners at 6-inch on-center intervals to ensure uniform pressure.
  • Use of non-sagging, UV-stable polyurethane sealants for the perimeter bead.
  • Verification of the "water-shedding" slope at the base of the curb to prevent ponding.
  • Implementation of a rigorous flood test to validate the integrity of the termination bar seal.

Aquashield Roofing Corporation

4006 Morris Ct.
Chesapeake, VA 23323
Direct Line: 757-553-5191
GPS Coordinates: 36.755164, -76.353932

Official Facebook Updates

Virginia Beach Roofing Company - Roofing Service Virginia Beach VA, Roofing Contractor

585 S Birdneck Rd #106
Virginia Beach, VA 23451
Direct Line: +17576318100
Google Maps Plus Code: RXCX+V7 Virginia Beach, Virginia
GPS Coordinates: 36.822156, -76.001565

Previous (Vol. 14) Volume 15 of 23 (40 Dossiers / Page) Next (Vol. 16)